Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
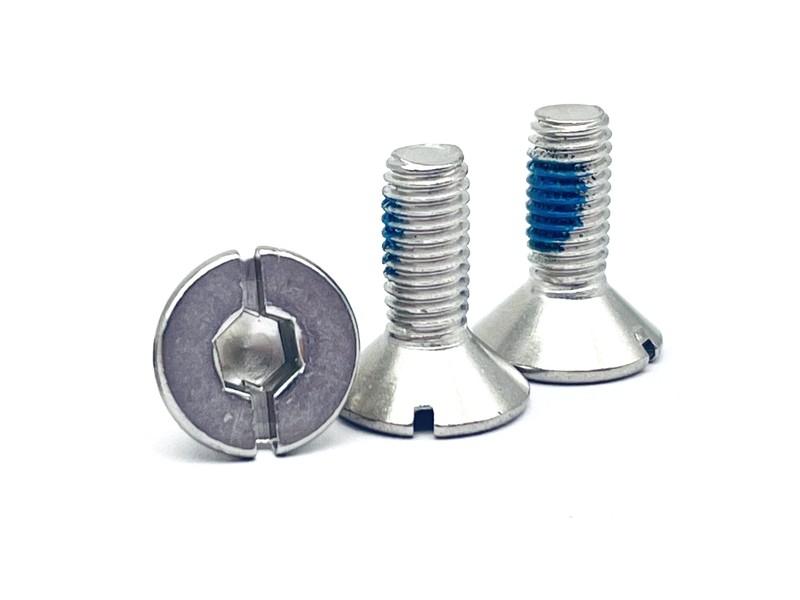
Type:Slotted Pan Head Screw
Materials:Steel
Surface treatment:Blue Zinc Plated
Head Type:Pan Head
Drive:Slotted
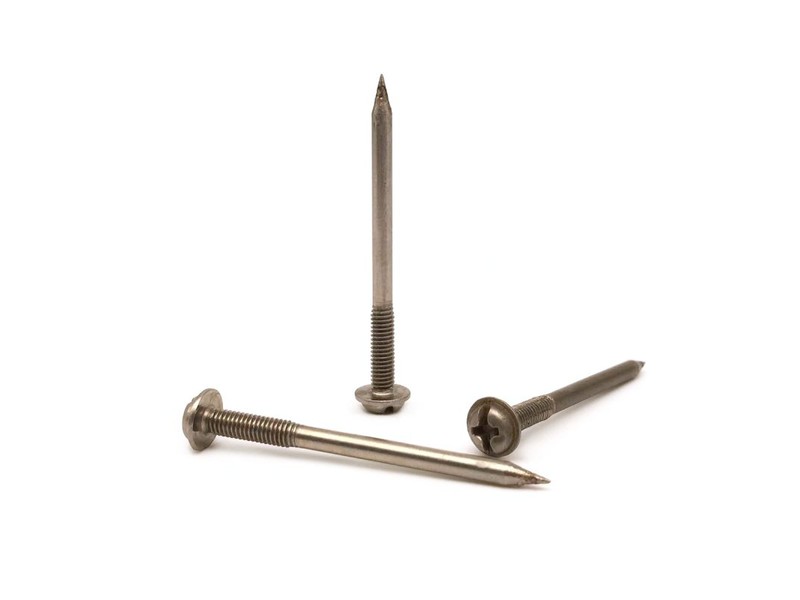
Thread:Self Tapping Thread
Point:Blunt Flat Point
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:833
We make slotted pan head screws in blue zinc plated steel, a self-tapping screw with a blunt flat point for moulded bosses, quoting them from M1 to M14. Point, thread, slot and boss sizes come from your drawing, and the first article is driven into your own boss.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
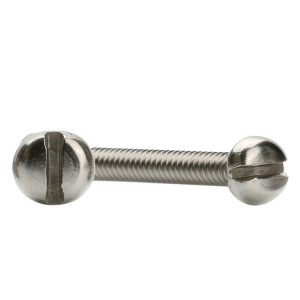
A slotted pan head screw is a screw with a low domed head, a single slot and a thread that forms its own thread in the hole, supplied here with a blunt flat point in blue zinc plated steel. The blunt point is the giveaway: this is a screw made to go into a formed hole, most often a moulded boss in a plastic part. The family is quoted from M1 to M14 with Number 833.
Pan head. A low dome with a wide flat bearing face, standard for screws that bear on a flat surface.
Single slot. One straight slot, driven by a flat blade with the torque controlled by hand.
Blunt flat point. A flat end with a short chamfer, made to enter a drilled or moulded hole rather than to find its own way.
Blue zinc. A zinc deposit with a blue-bright passivate, the standard finish for hardware sold by the box.
Driving a self-tapping screw into steel and driving one into plastic are two different problems. Steel resists, so the thread cuts and the torque is high; plastic yields, so the thread forms its own groove by displacing material, and the torque is low but the material around the hole is easily damaged. A slotted pan head screw with a blunt point is built for the second case.
The blunt point is the first sign of that. A sharp point is designed to find a hole and hold alignment; a blunt point assumes the hole is already there and that the screw will be driven straight into a boss. In a moulded plastic part that is exactly what happens, and a sharp point would be worse: it can catch on a feature at the bottom of the boss and start a crack.
On a slotted pan head screw the thread form is the second consideration. A thread that forms in plastic needs a coarse pitch and a relatively sharp crest, so it displaces material into the spaces between the threads instead of cutting it away. What it must not do is split the boss. That is why the thread pitch is matched to the boss diameter rather than to the screw alone, and why the same screw can be right for one boss and wrong for the next.
The slot drive suits the material. Plastic strips at a low torque and gives no warning, so a drive that lets the operator feel the joint and stop is an advantage. A flat blade in a slot gives that feel; a power driver with a cross bit does not, and it is the usual reason a plastic boss fails on the line.
Blue zinc is a sensible finish here because the joint is indoors and the screw is cheap. The coating is sacrificial and thin, so it does not change the thread geometry much, and a scratched head on a plastic part is an appearance issue rather than a corrosion one. Where the part is washed, the same screw in stainless is the answer.
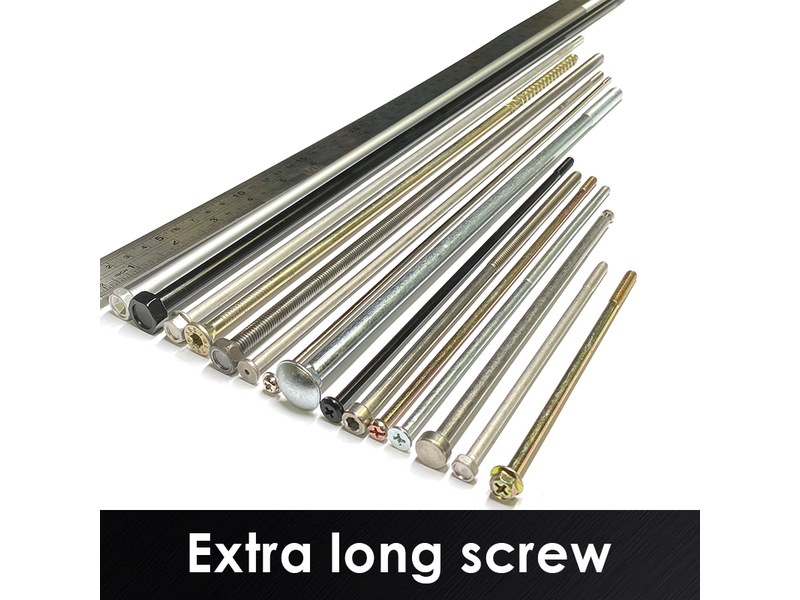
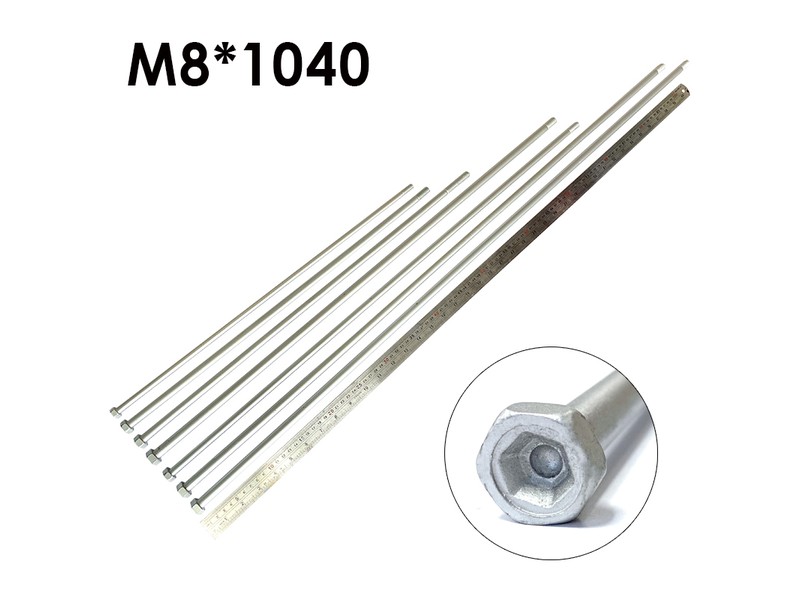
The recorded range is M1 to M14, covering M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For a slotted pan head screw the quotation carries head diameter and height, slot width and depth, thread size, point form and length, because in plastic the point and the thread pitch do the work.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Pan head, flat face | Head diameter and height |
| Slot | Single slot | Slot width, depth and burr |
| Thread | Self-tapping, coarse pitch | Pitch and major diameter, gauged |
| Point | Flat, blunt with short chamfer | Point diameter and chamfer |
| Finish | Blue zinc | Deposit thickness and adhesion |
| Length | Under the head | Measured on the shop plate |
Length matters more than usual in plastic because a screw that bottoms in a blind boss stops turning and starts stripping. The usable thread is the length from under the head to the point, and in a blind boss that is reduced by the boss depth and by the point geometry. Quoting the length without the boss depth is how a design ends up with a screw that cannot seat.
The thread size should be matched to the boss, and that is a moulding decision as much as a fastener one. A boss with too thin a wall splits; one with too wide a hole lets the screw turn without forming a thread. The screw maker can supply the thread, but the hole and the wall have to come from the same design.
Three features define this part: the blunt point, the coarse thread and the slot. The first says the hole is formed, the second forms the thread in plastic, and the third keeps the torque in a range a plastic boss can take.
| Feature | What it gives | What it costs |
|---|---|---|
| Blunt point | Straight entry into a moulded boss | Will not start without a hole |
| Coarse self-tapping thread | Forms a thread by displacing plastic | Splits a thin boss if over-tightened |
| Single slot | Feel and torque control by hand | Blade can slip out sideways |
| Wide pan face | Load spread on the plastic | Stands above the surface |
| Blue zinc | Cheap, thin, sacrificial | Indoor only |
On a slotted pan head screw the combination of features is deliberately modest. This screw is not trying to carry a structural load; it is closing a plastic cover, holding a small plate or fixing a component in a housing. What it has to do reliably is start straight, form a thread without cracking the boss, and stop before the plastic gives — and each of the three features helps with one of those.
The main risk is over-tightening. There is no lock, no defined torque and no cam-out limit on a slot; the joint tightens until the boss yields, and then it is loose forever. Where the part is assembled by hand that is a matter of technique; where it is assembled with a power driver, a torque setting is what protects the design.
The recorded finish is blue zinc, which is what a general-purpose indoor screw is normally bought with. It is thin enough not to change the thread significantly, sacrificial enough to protect the head from light damp, and cheap. On a plastic part the finish matters less than on metal, because there is no galvanic pairing and no rust staining of the surface.
| Option | How it protects | Effect on thread and point | Typical use |
|---|---|---|---|
| Blue zinc | Sacrificial zinc | Thin; thread as plated | Indoor general work |
| White zinc | Sacrificial zinc, trivalent | Thin; neutral tone, RoHS compliant | Indoor, regulated markets |
| Black zinc | Sacrificial zinc, dark | Thin; marks dark panels less | Dark equipment |
| Nickel plated | Barrier deposit, bright | Decorative; wears at the slot | Visible silver hardware |
| Stainless, plain | Passive chromium oxide film | Thread as cut | Damp and washdown |
Where the fastener sits in a damp environment, the finish stops being a formality. A zinc-plated screw in a wet housing rusts at the head and at the thread root, and the rust stains the plastic around it — a defect that cannot be cleaned off. The stainless version of the same screw costs more and removes the problem.
The coating also enters the thread fit on a self-tapping screw, because the crest that forms the thread in the plastic is a few microns thicker after plating. That is one reason the first article is driven into the actual boss rather than into a test plate.
Three assemblies where slotted pan head screws are the fixing:
| Where it sits | The screw closes a cover or fixes a component into a moulded boss, where the hole is formed and the thread is displaced rather than cut. |
| When it goes wrong | A thin boss splits, or the screw strips it by being driven after the head seats. |
| Why it happens | The boss is moulded, the material yields, and the drive is by hand. |
| What we control | Point form and thread pitch checked, first article driven into the boss. |
| Where it sits | The screw fixes a plastic trim, a bracket or a cover on a unit assembled in volume, where a hand driver is still the norm. |
| When it goes wrong | An over-driven screw leaves a loose fixing, and a plated head rusts in a damp appliance. |
| Why it happens | The material is plastic, the fixing is repeated, and the volume is high. |
| What we control | Thread gauged per batch, first article fitted to the part. |
| Where it sits | The screw closes a plastic box or fixes a terminal plate where the thread forms in the moulded body. |
| When it goes wrong | A cracked boss leaves the cover loose, and a stripped thread cannot be repaired in plastic. |
| Why it happens | The body is moulded, the fixing is serviced, and the part is indoors. |
| What we control | Head and slot checked, first article trialled in the box. |
Four reasons that matter on a screw driven into plastic, each tied to what the drawing has to prove:
|
Point and boss reviewed
The blunt point, the thread pitch and the boss are reviewed together, because a screw that suits one moulded boss can split the next one. Basis: Point, thread and boss agreed. |
Head, thread and point in one route
The pan head and the slot are formed in the heading stroke, the thread is rolled and the blunt point is formed, with plating last. Basis: One route from wire to plated screw. |
|
Driven into the actual boss
The first article is driven into the customer boss and checked for cracking and for strip torque, because that is the only test that covers the joint. Basis: First article driven into the boss. |
First article fixes the setting
The first article fixes the wire, the point die and the plating; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these slotted pan head screws from carbon steel wire on single-die headers that form the pan head and cut the slot in one stroke, rolls the self-tapping thread, forms the blunt flat point and plates the parts in blue zinc. The first part of every run is measured on the head and point, driven into a sample boss and entered into a thread gauge before the batch continues.


|

|
The point is the tooling that decides whether the screw starts. A blunt point has to be square to the axis and cleanly chamfered; a point that is slightly off-centre makes the screw start crooked in the boss and load one side of the thread, which is the beginning of a cracked boss rather than a stripped thread.
What decides whether slotted pan head screws pass is the point, the thread, the slot and the plate. The inspection agreement covers those, and the criteria come from the drawing.

Point and slot on the projector |

Thread gauged per batch |

Hardness checked on the wire |

Salt-spray testing of the plate |
The point is checked for diameter, squareness and chamfer, the thread is gauged per batch, and the slot is measured and driven with the production blade. The head is checked for diameter and height, and the plate for thickness and adhesion.
Every first article is driven into a sample boss and pulled to the strip point. On a plastic joint that number is the whole design: a screw that holds in a steel plate can still split a moulded boss, and the only place to find that out is in the boss itself.
Every shipment of slotted pan head screws is traceable to the wire it was made from and to the plating batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the plating record is kept with the inspection file.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the plating. The documents carry the drawing revision and the batch number, so a repeat order is made to the same point and thread that was approved.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a self-tapping part the first article is driven into the customer’s own boss, because the joint is the function. Buyers visit during the process to review samples and to see how the parts are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the plating line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
Because the hole is already formed, usually a moulded boss. A sharp point is for finding a hole; a blunt point is for going straight into one without catching.
It can. A thin wall, an oversized screw or an over-driven joint will crack the boss, which is why the first article has to be driven into the real part.
Only with a torque setting. Plastic strips at low torque, and a slot gives no cam-out warning before the boss gives way.
Short enough not to bottom in a blind boss, long enough to engage the thread properly. The boss depth is part of the calculation.
No. It is an indoor finish, and rust stains on plastic cannot be cleaned off. Use stainless for damp or outdoor joints.
Thread size and length, point form, head diameter and height, slot width, the boss diameter and depth, and the finish.
How a slotted pan head screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the boss it goes into
|
→ |
2
Point, thread and slot agreed
|
→ |
3
First article driven into your boss
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size and length, the point form, the head diameter and height, the slot width, and the boss diameter and depth.
|
Thread size
|
Length
|
Point form
|
|
Head diameter
|
Slot width
|
Boss depth
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com