Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
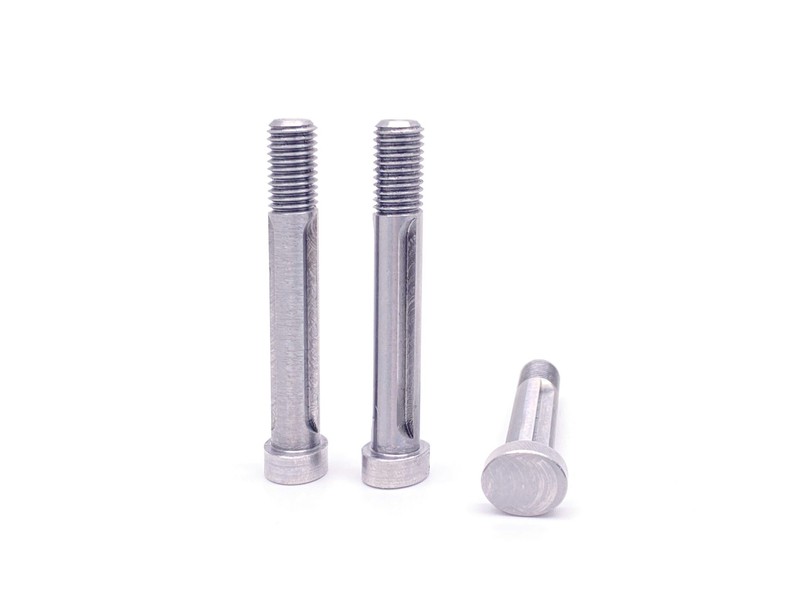
Type:Extra long dacromet screw
Materials:Carbon steel
Surface treatment:Dacromet (silver)
Head Type:Hex head
Drive type:Hex socket (internal)
Thread:Partial (half) machine thread, chamfered end
Forming:Split-die cold heading (one-piece)
Number:1354
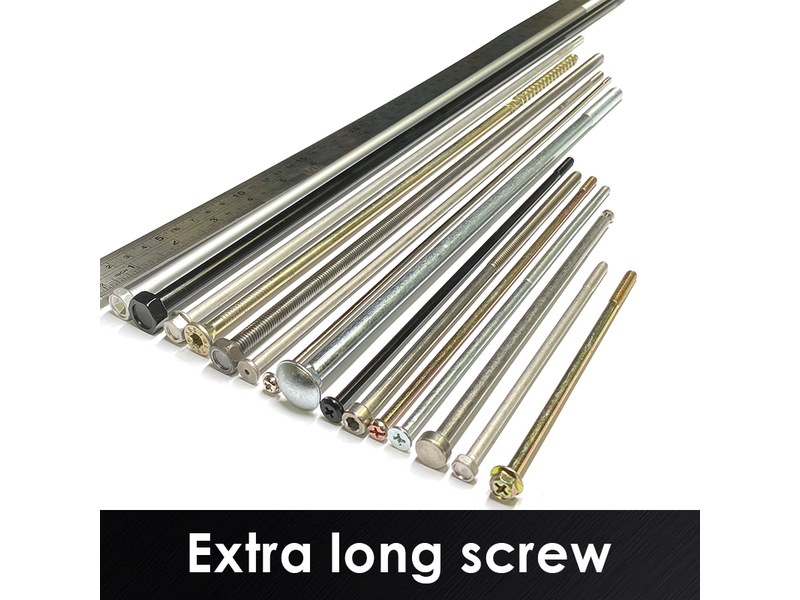
We manufacture extra-long dacromet hex-head screws in carbon steel, with an external hex head and an internal hex socket, from M1.4 to M12 and up to 2,000 mm, formed one-piece by split-die cold heading with a partial machine thread and a chamfered end. Length, thread position, coating thickness and the gauging condition are made to your drawing, and the coating is released on an acceptance sample.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A dacromet screw is a carbon-steel fastener with a thin zinc-aluminium flake coating instead of electroplating. On an extra-long dacromet screw the coating has to stay uniform along a metre or more of shank, and it has to leave the thread and the socket inside the tolerances stated on the drawing.
Coating thickness and the thread. The flake layer is thin but it is not zero: it builds on the thread flank and inside the hex socket. If the drawing does not say whether the thread is gauged before or after coating, the dacromet screw that passes at the bench can fail at the customer’s gauge.
External hex and internal socket. The hex head takes a wrench and the internal hex socket takes a driver, so the same dacromet screw can be driven from either side of a joint – useful where one face is inaccessible after assembly.
Plain shank and thread position. The plain shank carries the unsupported span and fixes where the thread begins; the chamfered end leads the thread into a nut or tapped block at the far end of a long run.
The hex head and the socket carry torque in two different ways: the external hex is loaded through its flats by a wrench, the socket through its walls by a driver. Both are dimensioned on the drawing, because the socket depth inside the head sets how much material is left under the bearing face on a head that is already small relative to a long shank.
Together these settle what the dacromet screw does on site: it goes through the frame without binding, it seats without false torque, and the coating survives long enough that the joint can still be released in service. That is the problem a custom dacromet screw is bought to solve.
A long dacromet screw is formed in one piece on a split-die header: the die opens along the shank so a part much longer than a standard heading window can still be headed, and the head and shank come from the same billet. A welded or joined shank is not offered as the default.
The seam of a welded joint is a corrosion path and a fatigue origin on a coated part, and the coating hides it from the outside. The die set fixes head form, plain shank and thread start together; the thread is rolled after forming, so the grain runs along the shank instead of being cut across it, and lengths outside the split-die window are turned from bar and coated the same way.
A split die for a dacromet screw wears on the split line, so the die is checked between runs and the first parts of each run are measured for head height, across flats and shank diameter. When the run changes length, the die insert and the thread roll change with it; the drawing revision, the die set and the coating batch are recorded so a repeat order reproduces the same part.
Dacromet screws are quoted from M1.4 to M12 and up to 2,000 mm. Length is usually held to +0/-2 mm on the drawing, and anything outside these bands is reviewed against the drawing before a quotation is issued.
| Item | How it is defined | What we control |
|---|---|---|
| Total length | From the datum under the head to the tip | Datum stated on the drawing; length measured on the shop plate |
| Thread length and position | Where the thread starts and how far it runs | Thread start checked against the drawing, not against a sample |
| Plain shank length | The unthreaded span that sits in the supports | Shank length and diameter held to the assembly stack |
| Head across flats and height | Head envelope that the socket sits in | Head and socket checked in the same operation |
| Coated fit | Dimensions after dacromet coating | Gauging condition stated on the drawing |
Diameter and length are quoted per part; each dacromet screw combination is checked against the drawing before a quotation is issued. A long thin part and a short thick one in the same diameter class take different routes, so the check confirms that the route can hold the length and the thread start.
On a dacromet screw, length is measured from the datum under the head, not over the thread, and the thread length is checked as a position from the same datum. Head across flats, head height and socket depth are gauged together, because a socket cut deeper than the head allows leaves too little material under the bearing face.
For a dacromet screw the drawing fixes five things: thread size and pitch, thread length and position, plain shank length, total length and its datum, and right- or left-hand direction. On a coated part one more line is needed: the condition in which the thread is gauged.
| Parameter | Why it matters on a long coated part | What we control |
|---|---|---|
| Thread start position | It sets where the plain shank ends and where the part can be supported | Start dimension checked on the first article and per batch |
| Engaging length | Too short leaves the joint weak; too long runs the thread into the support | Thread length and position taken from the drawing |
| Chamfer | The lead-in decides whether the thread starts square in a blind or floating hole | End form per drawing, checked with the threading operation |
| Handedness | A left-hand thread on a right-hand assembly will not pull the joint closed | Direction marked on the part and on the packing |
Dacromet is a zinc-aluminium flake coating applied from a dispersion and cured, not an electroplated layer. It covers the shank and the recess evenly, it carries no hydrogen-embrittlement risk from plating on high-strength parts, and it is specified with a thickness target and an acceptance sample rather than by colour. On a dacromet screw the coating is part of the fit, not a cosmetic layer.
| Coating | How it protects | Effect on thread and recess | Typical use |
|---|---|---|---|
| Dacromet (flake) | Zinc-aluminium flakes bonded in a cured film; barrier plus sacrificial action | Thin and even along the shank; thread and socket filled by a few microns | Wet or outdoor service; high-strength parts where plating hydrogen is a risk |
| Zinc electroplated | Sacrificial zinc layer | Build-up on the flank and in the socket; the drive feels tighter | General indoor machine screws |
| Zinc-nickel | Zinc alloy with higher corrosion resistance | Thicker film; masking may be needed at precision features | Damp service on smaller parts |
| Black oxide (oiled) | Conversion film with an oil carrier; no added thickness | No dimensional change; protection is limited without oil | Indoor parts where fit matters more than corrosion |
| Plain / passivated | Stainless surface; no coating | No added thickness; the machined surface is the finish | Stainless long parts |
The coating is applied after forming and thread rolling: degrease, coating, cure, then gauge. Threads and sockets that must stay at size are masked or plugged, and the drawing says which features are protected and which are kept clear. That is why a dacromet screw is specified by a drawing and an acceptance sample rather than by a colour name.
Salt-spray exposure and the acceptance state are agreed per project and written on the drawing; long parts are packed braced so the shank cannot take a set in transit, and the ends are protected so the coating is not chipped in handling. Batch and coating information go on the label, so the part that arrives is the part that was gauged.
Three assembly conditions where a coated long screw carries the joint, and what the dacromet screw has to do instead:
Outdoor and wet-service steel structures
|
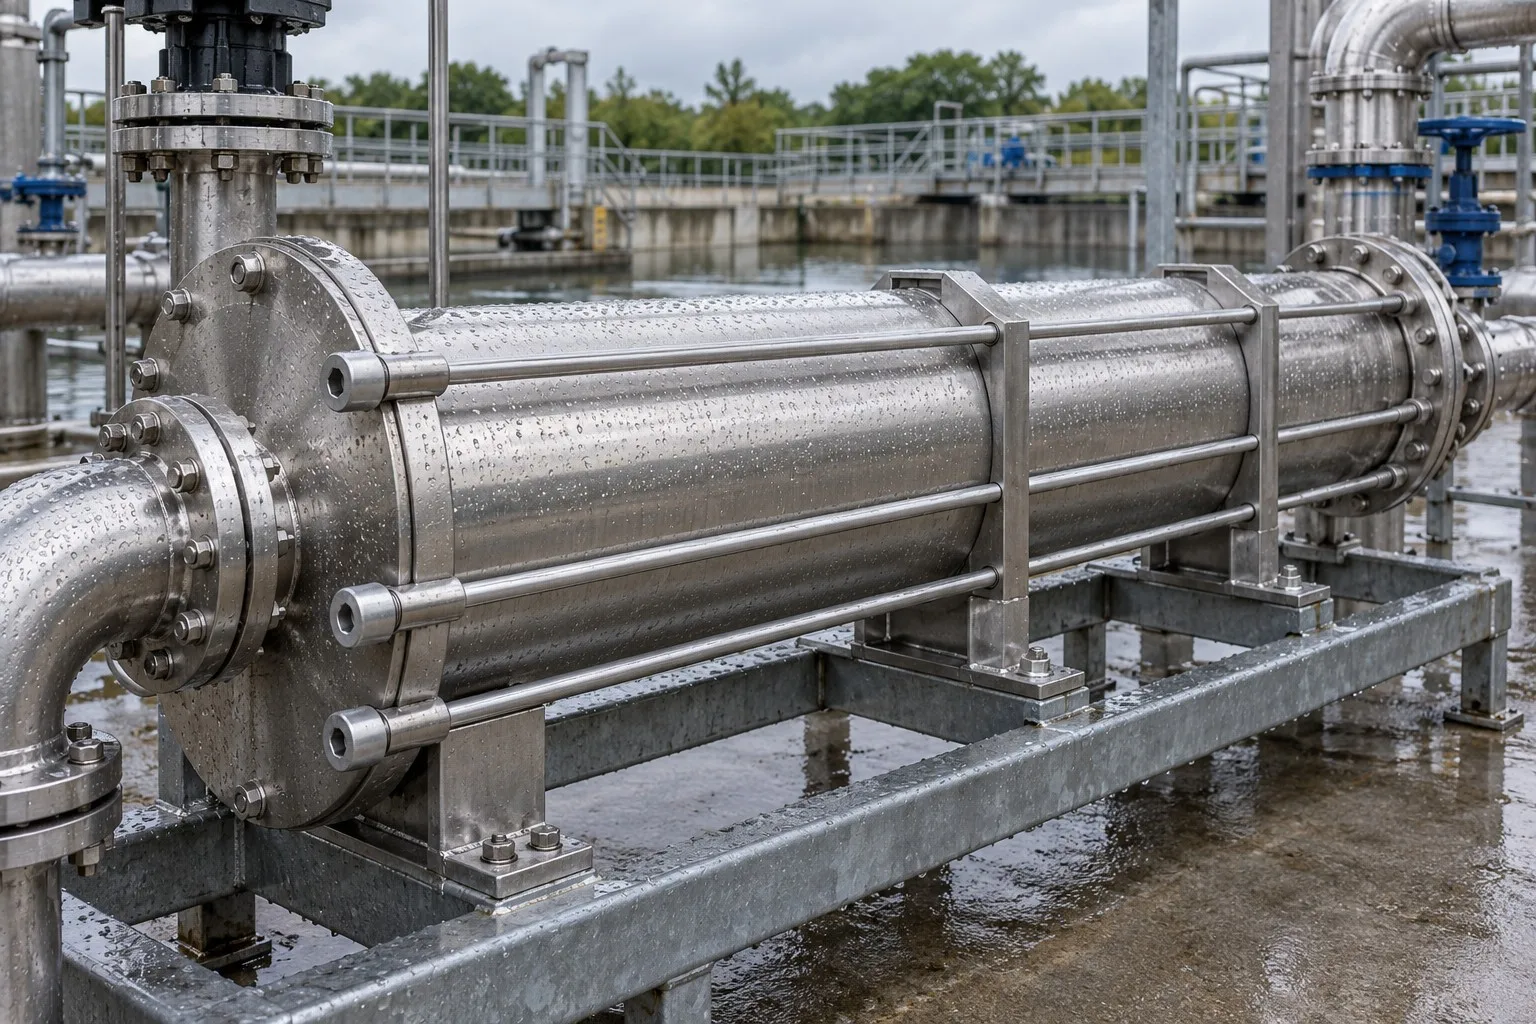
Wet / outdoor service – flake coating protects the long part |
Machined frame modules
|
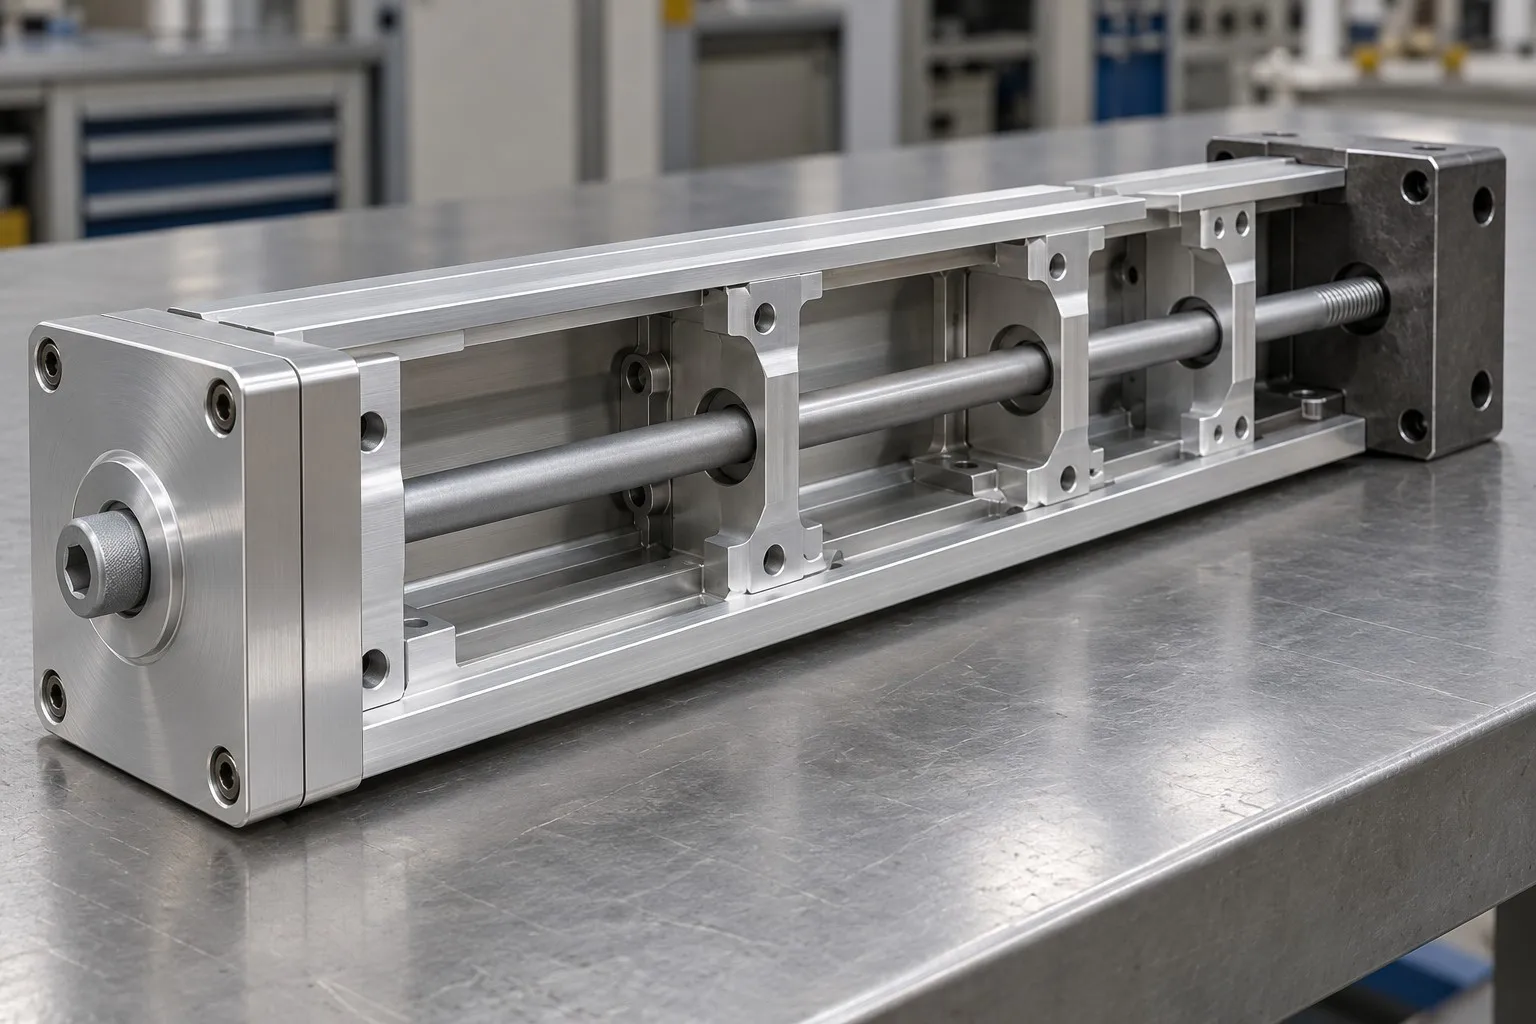
Machined frame – long-distance through-connections |
High-strength die stacks
|
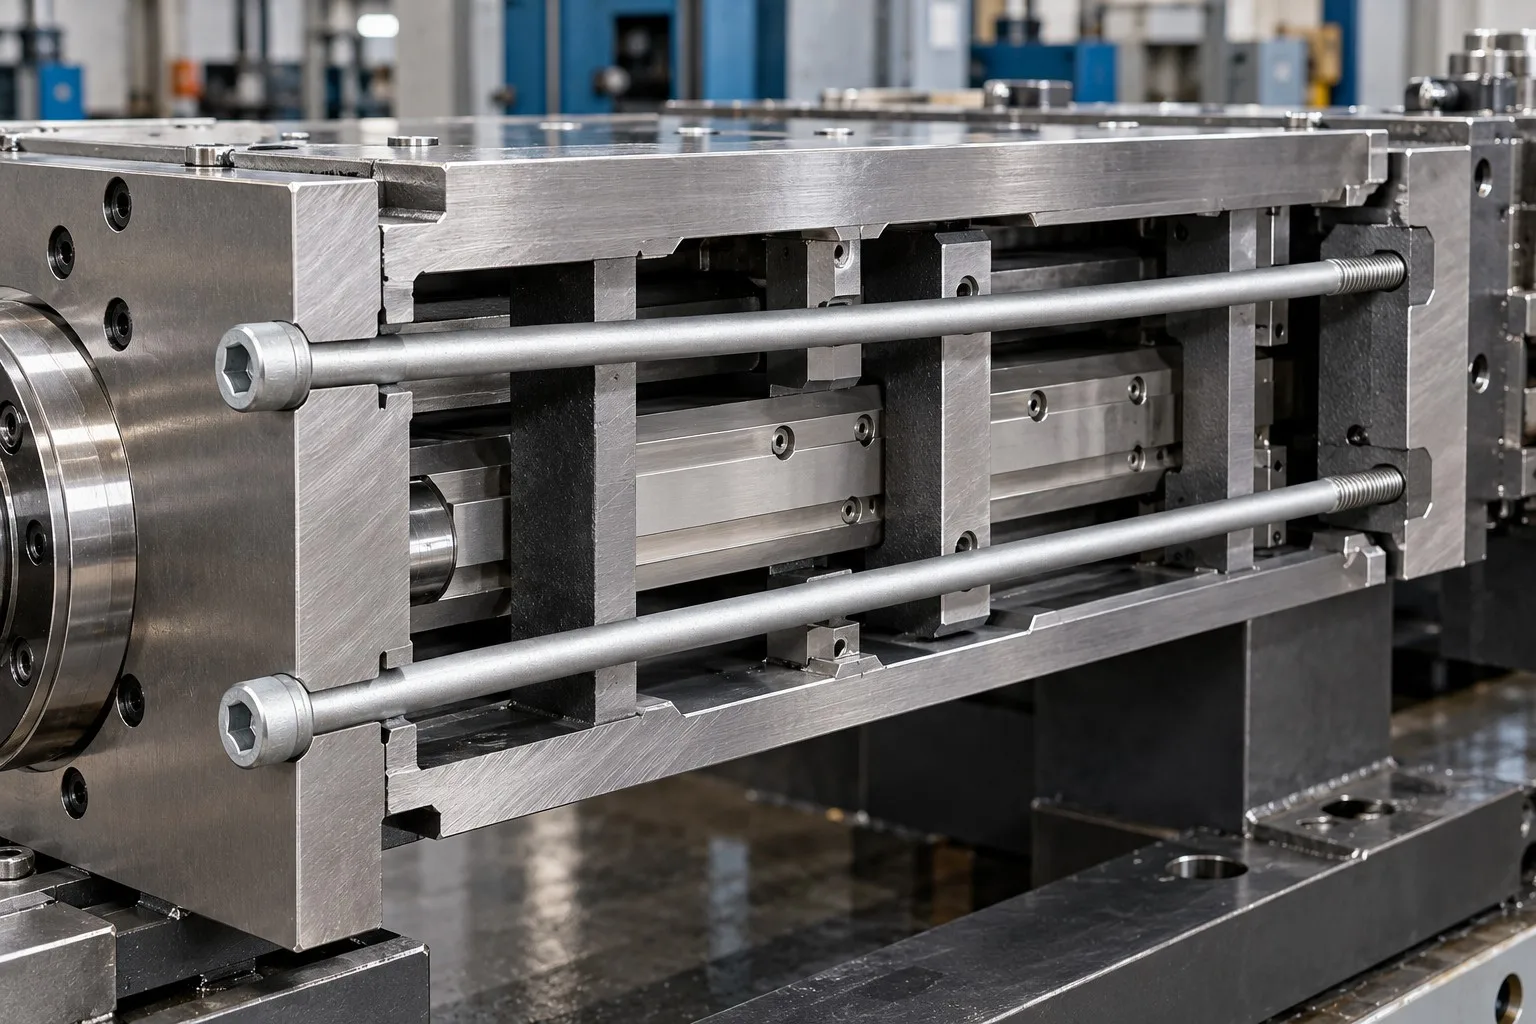
High-strength connections – flake coating on preloaded long screws |
Four reasons that matter specifically on a coated extra-long screw, each tied to what the drawing has to prove:
|
Engineering review before tooling
The thread start, plain shank and coating thickness are settled before a die is cut, so the first sample is measured against the drawing rather than against a guess. Basis: Drawing or sample reviewed before tooling is released. |
One piece, formed in a split die
A long dacromet screw is headed in one piece on a split-die header or turned from bar. A welded shank is never the default, so the joint cannot hide a corrosion path under the coating. Basis: One-piece split-die heading or turning route, no welded shank. |
|
Coating and thread fit planned together
Thickness band, masking and the gauging condition are agreed before the run, so the thread the customer receives is the thread that was gauged. Basis: Gauging condition stated on the drawing and recorded per batch. |
From approved sample to repeat production
The first article fixes the drawing revision, material batch, die set, coating batch and measuring method; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
These dacromet screws are formed, not assembled. Wire goes through the heading aisle; on a split-die header the die opens along the shank so the head and the first part of the shank come from the same billet, and the operator sets the die and checks the first parts against the drawing before the run is released. The thread is rolled after forming, and the coating is applied and cured as a flake layer before final gauge.
Between dacromet screw runs the die is changed to the drawing length and head form; the first parts go to the gauges before the run continues, and the setting is recorded. Parts that pass the bench checks are packed in layers so a long shank is supported over its length rather than hanging from the head.


|

|
What decides whether a dacromet screw passes is not its appearance: it is length from the datum, thread fit in the condition it ships in, and the coating evidence the drawing asks for. The inspection agreement covers those, and the criteria are the ones written on the drawing rather than a generic standard.
Each dacromet screw batch is recorded against the drawing revision: length and thread position from the first article, thread gauging per batch in the coated condition, and the coating checked on the acceptance sample. Where a third-party report is required for the material or the coating, it is listed on the drawing so the paperwork ships with the parts.
If a gauge fails, the parts back to the last good setting are held and re-checked before anything ships; the die and the coating batch are traced from the same record, so a re-run can be compared with the original batch rather than starting from a blank sheet.

Thread gauging against GO/NO-GO gauges |

Profile and dimensions on the optical projector |

Hardness testing of the base material |

Salt-spray testing on the agreed finish |
Every dacromet screw shipment is traceable to the material it was made from. The grade, heat number and standard are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.
With each dacromet screw batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the coating. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. Buyers visit during the process to review samples and to see the forming, threading and coating steps their parts will go through.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header, the thread rolling and the coating line can be seen on the day the parts run. What is agreed on the drawing is checked against the same gauges on the floor.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
A dacromet screw is a carbon-steel fastener coated with a zinc-aluminium flake layer instead of electroplating. The flake coating gives corrosion protection without the hydrogen risk of plating, which matters on high-strength parts.
Dacromet screws are quoted from M1.4 to M12 and up to 2,000 mm, with length usually held to +0/-2 mm. Each combination is checked against the drawing, and custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
By coat type, thickness band, masking and the condition in which the thread is gauged. The finish is released on an acceptance sample, not on a colour name.
In the condition written on the drawing. Because the flake layer adds to the thread flank, the practical position is to gauge in the coated condition the customer receives.
The hex head takes a wrench and the socket takes a driver, so the joint can be driven from either side – useful where one face is hard to reach after assembly.
Thread size and pitch, thread length and position, plain shank, total length and datum, head across flats and socket size, material grade, coating specification and the gauging condition.
How a dacromet screw project runs from drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
DFM review and quotation
|
→ |
3
First article approval
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a dacromet screw quotation, send the drawing with thread size and position, plain shank and total length with its datum, head and socket, material grade, dacromet specification and the gauging condition. Length, thread position and coating condition are confirmed with you before production.
|
Thread size, pitch and length position
|
Plain shank length
|
Total length and datum
|
|
Head across flats and socket
|
Dacromet spec and thickness band
|
Quantity and inspection criteria
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com