Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
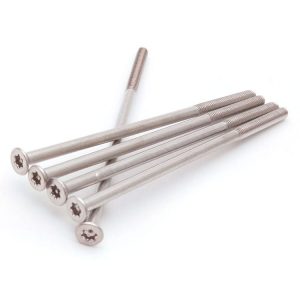
Type:Security Machine Screws, Button Head
Materials:Stainless Steel
Surface treatment:Plain
Head Type:Button Head
Drive:Five-Point Pin-In Recess
Thread:Machine Thread
Point:Blunt
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:488
We make security machine screws in passivated stainless, a button head with a five-point recess and a centre pin that no ordinary driver can turn, quoting them from M1 to M14. Recess size, pin diameter, head and thread come from your drawing, and the first article is driven and removed with your own driver.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Security machine screws are machine screws whose recess cannot be turned by an ordinary driver, and on this item the drive is a five-point recess with a pin standing in the middle of it. The pin blocks the centre, so a flat blade cannot span the recess and a normal bit cannot seat; the matching driver has a hole in its face. The family is made in passivated stainless with a button head, quoted from M1 to M14 with Number 488.
Button head. A shallow dome on a short wall, with nothing to catch a hand or a tool.
Pin-in-head recess. Five flats with a central pin. The pin is the security element; the five-point shape is what makes the driver rare.
Machine thread. A rolled thread for a tapped hole or a nut, ending in a blunt chamfer.
Passivated stainless. No coating, so the recess is as cut and the alloy carries the protection.
A security recess is judged by what it stops, and a pin in the middle stops the simplest tool there is. Any recess that a flat blade can cross is a recess a flat blade can turn; a pin interrupts that line, so the blade cannot engage two opposite flanks. It is a small feature that defeats the most common improvisation, which is why pin-in-head screws are used on fittings that are otherwise only lightly protected.
On a security machine screw the five-point shape does the rest. A pentagon is not in any driver set sold to the public, and a pin-in five-point is rarer still, so the tool has to be bought or made. That combination is a stronger deterrent than either feature alone, and it is why the older pin-in forms still turn up on public equipment long after better-known security drives appeared.
On security machine screws the button head is a sensible partner for the form. It is a low dome with no edge, so there is nothing to grip with pliers and nothing to lever against, and the fixing does not invite the attention a raised head would. A screw that cannot be turned by a driver but can be gripped by a tool at the head is not secure; the dome removes that option.
On security machine screws none of this defeats a determined person. A pin-in recess stops a casual attempt and slows an opportunist; it does not stop a drill, and it does not make the joint stronger. Reading the part honestly is important, because a design that treats a security screw as a lock will be disappointed, while one that treats it as access control backed by a locking enclosure will not.
Stainless is the material that makes the part last. The recess is the only place a tool touches, and a plain stainless recess has no coating to chip or wear off in the hands of whoever services the joint legitimately. On equipment that is washed or installed outside, that is the difference between a screw that can be opened in two years and one that has to be cut out.
The recorded range is M1 to M14, covering M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For security machine screws the quotation carries head diameter and height, recess size and pin diameter, the thread and the finish, because the recess is the security feature and its geometry has to match the driver the customer will use.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Button head, domed | Head diameter and height |
| Recess | Five-point with centre pin | Recess size, depth and pin diameter |
| Thread | Machine thread | Pitch and length, gauged per batch |
| End | Blunt, chamfered | Chamfer cut, not deburred |
| Finish | Passivated stainless | Surface condition and film |
| Length | Under the head | Measured on the shop plate |
Pin diameter should be specified, not assumed. The pin has to be narrow enough to leave usable flats for the driver and thick enough to survive a screwdriver being forced into the recess; on a small head that window is narrow, and two suppliers can fall on different sides of it.
Recess depth is what makes the drive workable. A shallow pin-in recess takes very little of the driver, and on a domed head the material available is limited, so the depth is a design decision that belongs on the drawing rather than in a catalogue.
Three features define this part: the central pin, the five-point recess and the button head. The first blocks the blade, the second keeps the tool rare, and the third removes anything that could be gripped.
| Feature | What it gives | What it costs |
|---|---|---|
| Centre pin | Defeats a flat blade and a normal bit | Needs a hollow driver |
| Five-point recess | Rare tool, harder to improvise | Bit has to be sourced and stocked |
| Button head | Nothing to grip or lever | Shallow recess in a low head |
| Stainless body | Recess stays usable | Galls if driven dry and hard |
| Machine thread | Repeatable clamp in a tapped hole | Needs a nut or a tapped insert |
On security machine screws the value of the pin is that it costs almost nothing to make and stops the most common attack. A flat blade, a coin, a nail file: none of them can turn a pin-in recess, and each of those is what a curious person actually has. The five-point shape then stops anyone who has a screwdriver set, because that shape is not in it.
The cost lands on the legitimate user. The driver has to be bought, kept and not lost, and a joint that is opened once a year will be opened by someone who has to find the tool first. That is a real operational cost and it belongs in the design decision, not in the purchase order afterwards.
The recorded finish is passivation with no coating. On a pin-in recess that is the only practical choice: a coating would narrow the flats, thicken the pin and blunt the corners the driver engages, and on a small recess those changes decide whether the bit fits at all. Passivation leaves the geometry as cut and gives the alloy its corrosion resistance.
| Option | How it protects | Effect on recess | Typical use |
|---|---|---|---|
| A2 stainless, passivated | Passive chromium oxide film | Recess as cut | Outdoor equipment and panels |
| A4 stainless, passivated | Passive film with molybdenum | Recess as cut | Coastal and chemical |
| Steel, zinc plated | Sacrificial zinc | A few microns; recess re-checked | Indoor sealed products |
| Steel, black oxide | Conversion film, oiled | No measurable build | Internal mechanisms |
| Steel, nickel plated | Barrier deposit, bright | Decorative; wears at the recess | Visible fittings |
On security machine screws with a coating, the recess has to be re-checked after plating. A deposit that lands on the five flats narrows the opening and rounds the corners, and a driver that has to be forced in is a driver that will damage the recess the first time it is used. That check is part of the first article, not an afterthought.
On security machine screws stainless is the version to choose wherever the joint is exposed. The recess holds water, and a plated steel socket rusts from the inside; on a security screw that is worse than usual, because a rusted recess is precisely the part that cannot be re-cut.
Three assemblies where security machine screws are the fixing:
| Where it sits | The screw holds a cover, a panel or a fitting that the public can reach and that should not be opened with a pocket tool. |
| When it goes wrong | A standard recess invites tampering, and a rusted pin-in recess cannot be opened even with the right driver. |
| Why it happens | The joint is exposed, it is opened by staff, and the fixing is visible. |
| What we control | Recess and pin checked, first article driven with the production driver. |
| Where it sits | The screw closes a cover whose interior is for authorised access only, where the fastener is a barrier rather than a lock. |
| When it goes wrong | A damaged recess blocks the service visit, and an improvised tool damages the flats. |
| Why it happens | The joint is closed to users, it is serviced, and the tool is controlled. |
| What we control | Pin diameter and recess depth checked, first article driven and removed. |
| Where it sits | The screw fixes a panel over cash or media, where the fixing slows an opportunistic attempt without being the security system. |
| When it goes wrong | A recess that is worn after several services leaves nothing to turn, and the panel has to be drilled. |
| Why it happens | The joint is high value, it is opened on a schedule, and the driver is held by staff. |
| What we control | Recess driven repeatedly on the sample to check wear. |
Four reasons that matter on a pin-in-head fastener, each tied to what the drawing has to prove:
|
Recess and driver matched
The recess size, the pin diameter and the driver that will be used are confirmed together, because a pin-in recess that does not accept the customer’s driver is unusable. Basis: Recess and driver agreed. |
Head, recess and pin in one route
The button head, the five-point recess and the centre pin are formed in the heading stroke, the thread is rolled and the parts are passivated. Basis: One route from wire to passivated screw. |
|
Driven and turned out again
The first article is driven and removed with the production driver, because removal is where a security recess shows whether it was made well. Basis: First article driven and removed. |
First article fixes the setting
The first article fixes the wire, the pin punch and the passivation; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these security machine screws from stainless wire on single-die headers that form the button head, cut the five-point recess and leave the centre pin standing in one stroke, roll the machine thread and passivate the finished parts. The first part of every run is measured on the head and recess, driven and removed with the production driver before the batch continues.


|

|
On security machine screws the pin is the easiest part of the punch to break and the hardest to see. It is a thin column standing in the middle of the recess, and it has to survive thousands of strokes without bending; a pin that is slightly bent leaves a recess that looks right and refuses a driver, because the hollow driver cannot get over the pin. That is checked with the driver on the first article of every run.
What decides whether security machine screws pass is the recess, the pin, the thread and the alloy. The inspection agreement covers those, and the criteria come from the drawing.

Recess and pin on the projector |

Thread gauged per batch |

Hardness checked on the wire |

Salt-spray testing of the grade |
On security machine screws the recess is checked for size, depth and flat condition, and the pin for diameter and for sitting true at magnification. Then the first article is driven and removed with the production driver; a recess that measures correctly and refuses the driver is the failure this part is prone to, and only the driver finds it.
The thread is gauged per batch and the alloy is confirmed on the certificate. A salt-spray sample is run where the environment asks for it, because a security recess that rusts shut is the worst outcome for the part: the owner cannot open the joint even with the correct tool.
Every shipment of security machine screws is traceable to the wire it was made from and to the passivation batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the grade or the passivation. The documents carry the drawing revision and the batch number, so a repeat order is made to the same recess geometry that was approved.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a security part the first article is driven and removed with the customer’s own driver, because the recess is the function. Buyers visit during the process to review samples and to see how the heads and recesses are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the passivation line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
It stops a flat blade or an ordinary bit from spanning the recess. The correct driver has a hole in its face that fits over the pin.
It stops casual attempts and improvised tools. It does not stop a drill, so it is access control, not a lock.
No. The pin prevents it from seating, and forcing one damages the flats. The driver is part of the specification.
Because there is nothing to grip with pliers and nothing to lever. A security recess on a raised head can still be turned by gripping the head.
For exposed joints, yes. A rusted recess on a plated screw cannot be opened, and it cannot be re-cut on a security part.
Thread size and length, head diameter and height, recess size and depth, the pin diameter, the grade and the driver that will be used.
How a security machine screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the driver you use
|
→ |
2
Recess size, pin diameter and head agreed
|
→ |
3
First article driven and removed with your driver
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size and length, the head diameter and height, the recess size and depth, the pin diameter and the grade.
|
Thread size
|
Length
|
Head diameter
|
|
Recess size
|
Pin diameter
|
Grade
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com