Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
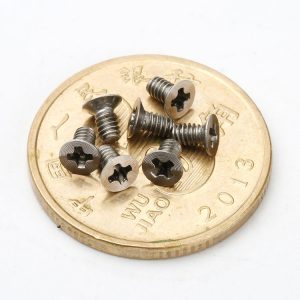
Type:Tiny Screws For Sunglasses Pan Head
Materials:Steel
Surface treatment:Nickel Plated
Head Type:Pan Head
Drive:Phillips and slot (combined)
Thread:Machine thread, half thread
Point:Blunt
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:382
We make tiny screws for sunglasses in nickel plated carbon steel, a pan head with a combined Phillips and slot recess and a half thread, quoted from M1 to M14. Both recess depths, thread length, shank diameter and plating come from your drawing, and the first article is fitted in your hinge.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Tiny screws for sunglasses are miniature pan head machine screws used in eyewear hinges, temples and lens mounts, where the head is around a millimetre across and the thread is M1.2 to M1.6. This one is made in carbon steel with a nickel finish, a combined Phillips and slot recess and a half thread, quoted from M1 to M14 with Number 382.
Pan head. A low dome on a small bearing ring, the usual form on an eyewear hinge because it is smooth against the skin and still carries the joint.
Phillips and slot recess. A cross and a straight slot cut into the same head, so the screw can be driven with a PH00 bit or an ordinary flat blade.
Half thread. A threaded length that stops part way down, leaving a plain shank that passes through the first hinge leaf.
Nickel plated steel. A bright, hard deposit over carbon steel, which is the finish eyewear has used for decades because it polishes and takes wear without showing the base metal.
A combined Phillips and slot recess on tiny screws for sunglasses puts two driving shapes into a head that is barely a millimetre deep. The slot is a straight cut across the top; the cross is a pyramid cut into the same face, and where the two intersect the metal between them becomes a set of thin wedges. Those wedges are the part that fails: a flat blade rocks in the slot and breaks the corners of the cross, and once the cross corners are gone the bit has nothing to bite.
The reason the combination exists is the repair kit. Sunglasses are serviced with a jeweller’s screwdriver, and an owner who has lost the PH00 driver can still turn the screw with the blade. The screw gives up a little drive strength to be serviceable with whatever tool is at hand, and on a hinge that is tightened once and left, that is a fair trade.
Depth is the number that decides how the trade comes out on tiny screws for sunglasses. A slot cut to full depth leaves the cross shallow and the blade seats well while the cross does not; a slot cut shallow leaves a cross that works but a blade that skips. Both recesses have to finish inside the head height, so on the smallest sizes the drawing should name the recess depths rather than rely on a standard form.
The half thread is the second half of the design. In a hinge the screw passes through a leaf on one side and threads into the other, so the unthreaded shank acts as a pin in the first hole and the thread only does work in the far leaf. If the thread runs all the way to the head, it cuts into the first leaf as the hinge closes and the joint binds.
Nickel plating is what makes the assembly look right and holds up in service. On a screw this small the deposit is a measurable part of the recess, so the head is cut and the recess gauged with the plating in mind, and the plated part is what the customer’s driver has to fit.
The recorded range is M1 to M14, with M1, M2 and M3 covering the eyewear work. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For tiny screws for sunglasses the quotation carries head diameter, head height, recess depths, thread length and overall length, because on a hinge screw the unthreaded shank length is as important as the thread.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Pan head, low dome | Head diameter and height |
| Recess | Phillips cross plus straight slot | Both recess depths and corner form |
| Thread | Half thread, machine thread | Threaded length and shank diameter |
| Shank | Plain length through the first leaf | Diameter and surface condition |
| End | Blunt, chamfered | Chamfer cut, not deburred |
| Material | Carbon steel | Grade and heat number on the certificate |
| Finish | Nickel plated | Coating thickness and appearance |
Threaded length should be quoted against the hinge, not against the screw. A half thread that is a fraction long will not let the leaf close, and one that is short leaves too few threads in the far leaf to hold the joint.
Shank diameter is the other number to put on the drawing. It has to be a running fit in the first leaf, and a shank that is oversized turns the hinge into a press fit that binds as soon as it is tightened.
Three features define tiny screws for sunglasses: the small pan head, the two recesses cut into it and the half thread below. The first makes it an eyewear screw, the second makes it serviceable with a flat blade, and the third lets it act as a hinge pin and a fastener at the same time.
| Feature | What it gives | What it costs |
|---|---|---|
| Pan head | Smooth against the skin | Small bearing ring |
| Combined recess | Driven with a bit or a blade | Thin metal between the two cuts |
| Half thread | Acts as a pin in the first leaf | Threaded length must match the hinge |
| Nickel plating | Bright, hard, familiar finish | Build narrows both recesses |
| Steel body | Takes a fine thread and holds it | Needs the plating to resist moisture |
Being serviceable with any tool is the practical value of tiny screws for sunglasses. With tiny screws for sunglasses a single small screwdriver from a repair kit can tighten a hinge or replace a lens screw, and the owner does not need a box of bits for a two-minute job.
The cost is concentrated in the corners of the cross, and it is paid during repair rather than assembly. A flat blade that is too thick for the slot will still go in part way, and the pressure it puts on the cross corners is what strips them.
The recorded finish on tiny screws for sunglasses is nickel plating over carbon steel. On an eyewear screw that is the traditional choice: it polishes to a bright finish, it is hard enough to keep the recess sharp through normal use, and it takes the colour of the hinge parts it sits beside. The deposit does add a few microns inside both recesses, and at M1.2 that is a real fraction of the recess depth.
| Finish | How it protects | Effect on the combined recess | Typical use |
|---|---|---|---|
| Nickel plated | Hard barrier deposit, bright | Build re-checked on both recesses | Metal hinges and temple screws |
| Black nickel | Dark decorative deposit | Build re-checked; appearance led | Black frames and hardware |
| Zinc plated | Sacrificial zinc, bright | Softer; recess wears faster | Low-cost general work |
| Stainless, passivated | Passive film | None; recess as cut | Salt-water and sports frames |
| Brass, plain | No coating needed | Softer head; slot wears | Decorative vintage hardware |
Where the frame is worn against skin, nickel release is a consideration in some markets, and the plated parts have to meet the release limit for the grade and the plating specification. That is a conversation worth having before the parts are plated, because it decides the deposit and sometimes the base material.
For sport and marine frames stainless is often the better answer: passivated 304 keeps the recess as cut and does not depend on a coating for corrosion resistance, which matters on a screw that is never looked at until it fails.
Three assemblies where tiny screws for sunglasses are the fixing:
| Where it sits | The screw joins the temple to the front frame and has to be tightened from the outside with a small driver, then left alone. |
| When it goes wrong | The cross corners break when a flat blade is used, and the hinge cannot be tightened again. |
| Why it happens | The joint is small, exposed, and serviced by hand. |
| What we control | Both recess depths checked, edge plating clean, first article fitted in the hinge. |
| Where it sits | The screw retains a rimless lens or a nose pad arm where the head sits close to the lens and must not stand out. |
| When it goes wrong | The plated head is proud or sharp, and it marks the lens or the wearer. |
| Why it happens | The joint is visible, it is handled, and the finish is part of the product. |
| What we control | Head height and plating edge checked; recess driven after plating. |
| Where it sits | The screw closes a case back or a clasp where the same combined drive is used so a single screwdriver serves the whole product. |
| When it goes wrong | A slot that is too shallow lets the blade slip and mark the case. |
| Why it happens | The joint is a small threaded assembly with a visible head. |
| What we control | Slot depth and cross depth agreed with the tool the customer supplies. |
Four reasons that matter on an eyewear screw, each tied to what the drawing has to prove:
|
Both recess depths agreed
The slot depth and the cross depth are settled with the head height before tooling, because both have to fit inside a head of about a millimetre. Basis: Both recess depths agreed. |
Headed, threaded, plated in one route
The pan head and combined recess are formed in one stroke, the half thread is rolled and the parts are nickel plated in the same route. Basis: One route from wire to plated screw. |
|
Recess gauged after plating
Both recesses are checked after plating with the tools the customer uses, because the deposit is a real fraction of a small recess. Basis: Recess gauged after plating. |
First article fitted in the hinge
The first article is fitted into the customer hinge and checked for shank fit and thread engagement, not just measured on the bench. Basis: First article fitted in the hinge. |
Shi Shi Tong forms tiny screws for sunglasses from carbon steel wire on single-die headers that form the pan head and cut the combined recess in one stroke, rolls the half thread to a blunt chamfered end, and nickel plates the finished parts. The first part of every run is measured on head height, both recesses and thread length before the batch continues.


|

|
Cutting two recesses into one small head is where the part is decided. The cross is cut first and the slot across it second, and the punch for the slot has to stop before it breaks through the thin metal left by the cross. A punch that is slightly deep leaves a head that looks finished and fails the first time a blade is used.
What decides whether tiny screws for sunglasses pass is the head, both recesses, the unthreaded shank, the thread and the plating. The inspection agreement covers those, and the criteria come from the drawing.

Head and recesses on the projector |

Thread gauged per batch |

Hardness checked on the wire |

Coating proved by salt spray |
Both recesses are checked for depth and for the metal left between them, the head for diameter and height, and the shank for diameter where it runs in the first leaf. The thread is gauged per batch, and the plating is checked for thickness and appearance against the approved sample.
For tiny screws for sunglasses the first article is also driven with both tools: the PH00 bit at the assembly torque and the flat blade by hand, because the blade is how the screw will be serviced and it is the tool that finds a shallow slot.
Every shipment of tiny screws for sunglasses is traceable to the wire it was made from and to the plating batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the coating or the nickel release limit. The documents carry the drawing revision and the batch number, so a repeat order is made to the same recess depths that were approved.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On an eyewear screw the first article is fitted into the customer hinge, because shank fit and thread length are properties of the pair. Buyers visit during the process to review samples and to see how the heads are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the plating line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
So the screw can be tightened with a PH00 bit or with a flat blade from a repair kit. The combination gives up a little strength to be serviceable anywhere.
The plain shank runs in the first hinge leaf like a pin, and the thread only engages the far leaf. A full thread binds the hinge as it closes.
The corners of the cross, when a blade that is too thick is forced into the slot. Both recess depths have to be cut to leave metal between them.
Usually M1.2 to M1.6 with a head around a millimetre across. The exact size follows the hinge thread in the frame.
Nickel release is regulated in some markets. The plating and the base material are chosen to meet the limit where the frame is worn against skin.
Overall length, thread length and shank diameter, head diameter and height, both recess sizes and depths, the material and the plating.
How a tiny sunglasses screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the hinge it fits
|
→ |
2
Recess depths, shank and thread length agreed
|
→ |
3
First article fitted into your hinge
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the overall length, thread length and shank diameter, head diameter and height, both recess depths, the material and the plating.
|
Overall length
|
Thread length
|
Shank diameter
|
|
Head diameter
|
Recess depths
|
Plating
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com