Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
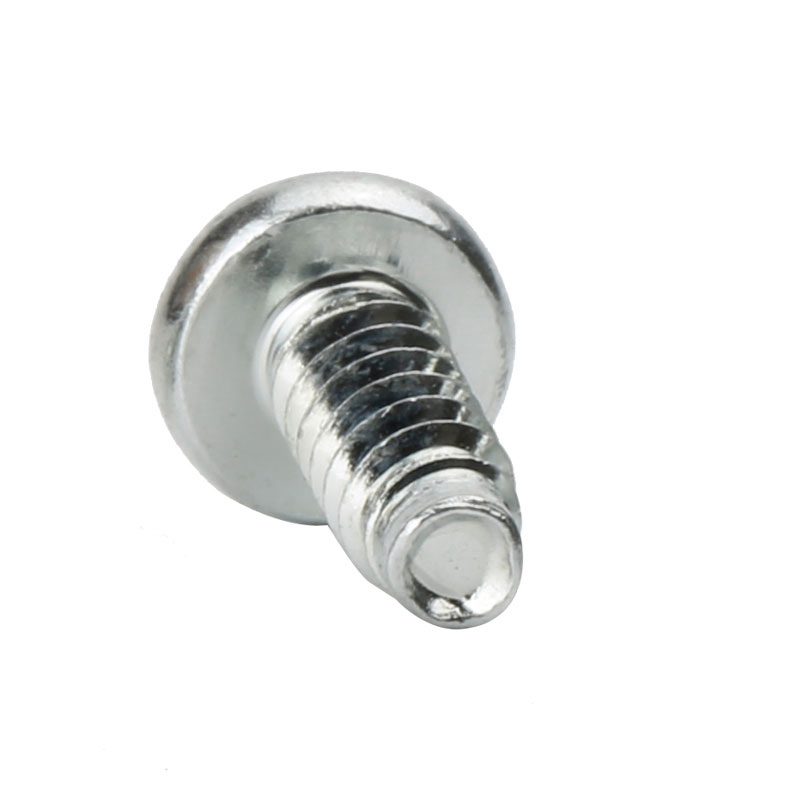
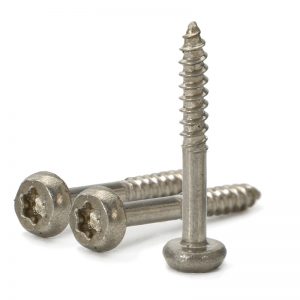
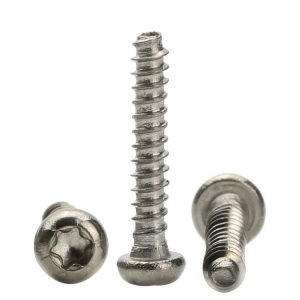
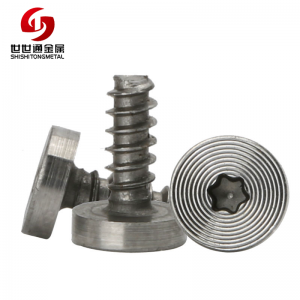
Type:Thread Forming Screws For Steel
Materials:Carbon Steel
Surface treatment:White Zinc Plated
Head Type:Pan Head
Drive:Torx six-lobe recess (T-size matched to the thread)
Thread:Trilobular thread-forming thread, rolled, full length under the head
Point:Flat end with a small chamfer; no drill point, no sharp taper
Forming:Single-die heading, trilobular thread rolling, end trimmed flat, white zinc plating, sorting
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:294
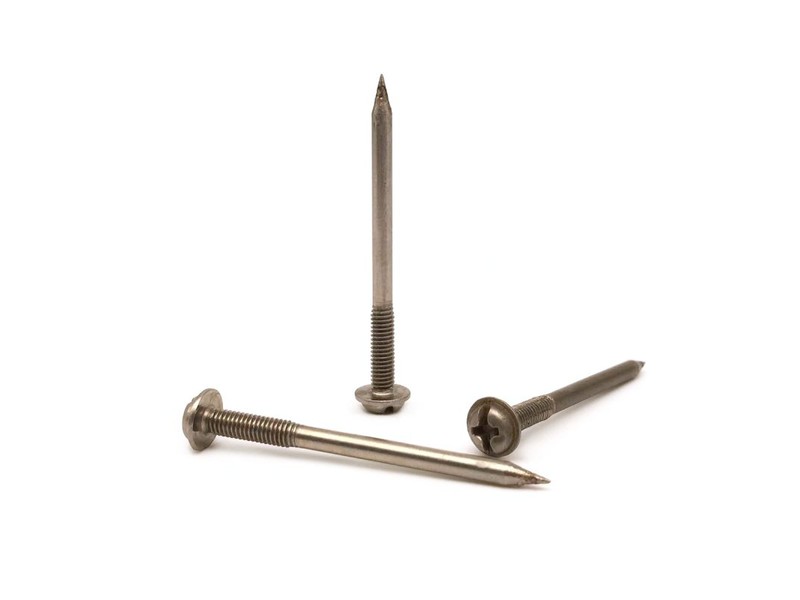
We manufacture thread forming screws for steel with a trilobular thread, a flat end and a Torx drive under a pan head, in carbon steel with a white zinc finish. Lobe form, hole size, head and length are taken from your drawing.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Thread forming screws for steel are fasteners that form a thread in a drilled hole by displacing the material rather than cutting it away. The recorded item on this page is carbon steel with a white zinc finish, a pan head, a Torx drive, a trilobular thread and a flat end, quoted from M1 to M14 with Number 294.
Trilobular thread. The thread is not round in cross-section; it carries three shallow lobes. As the screw turns the lobes press the hole wall into the thread form, and the relief between them gives the displaced material somewhere to go.
Flat end. The point is blunt, so the screw cannot drill and stops when the hole ends. On steel that is the arrangement that keeps the joint from breaking through a thin panel.
No chips. Forming removes nothing, so there is no swarf in the assembly — which is why this type is used inside enclosures and on equipment where loose metal is a fault.
Torx drive. Six lobes for a matching star bit. A forming screw needs sustained torque while the thread is being pressed into the steel, and a star bit stays seated through that.
White zinc. A bright sacrificial finish that protects the steel and keeps the part clean, applied thin so the thread form is not changed.
The pan head and the star recess are formed in one heading stroke, so the recess stays concentric with the shank. On a forming screw that matters: a recess that is off centre makes the bit push the head sideways while the lobes are pressing the steel, and the screw goes in at an angle.
The thread is rolled with the trilobular profile. The three lobes run the full length and are slightly larger than the pitch diameter, so they compress the hole wall; the relief between them is what keeps the material from being over-stressed.
The end is trimmed flat after rolling. A forming screw with a point would try to start its own hole and would push material ahead of the thread, which in thin steel is how a hole gets distorted. The flat end makes the pilot hole the only thing that decides where the screw goes.
White zinc follows the rolling. The coating is thin, so the lobes keep their form and the thread is gauged in the plated condition — the condition that will actually press into the steel.
The recorded part has no plain shank, so the whole length under the head carries thread and engages. On a forming screw that is normal: the thread is the tool as well as the fastener.
The family is quoted from M1 to M14, with M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14 in the recorded range. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission; thread forming screws for steel are normally short, because the thread is working through sheet or a thin section rather than clamping a stack.
| Item | How it is defined | What we control |
|---|---|---|
| Thread | Trilobular forming thread, rolled, full length | Gauged per batch after plating |
| Hole | Sized to the lobes and the sheet gauge | Confirmed in a sample of the customer’s steel |
| Head | Pan head with a Torx recess | Diameter, height and recess checked |
| End | Flat with a small chamfer | Checked on the projector |
| Length | From under the head to the flat end | Measured on the shop plate |
| Finish | White zinc, thin | Thickness and tone checked per batch |
The hole size is the customer’s dimension and the one that decides whether the joint works. A forming screw needs a hole close to the pitch diameter of the thread, which is not the same as the hole a cutting screw of the same thread takes. Where a drawing converts one to the other without changing the hole, the joint either strips or never closes.
Length is measured from under the head, and with a full thread the usable length is the whole shank. In a blind hole the depth has to be at least the length minus the panel thickness; a forming screw that bottoms will deform the sheet rather than the thread, which is harder to see and to correct.
A trilobular screw is often described as a plastic fastener, but the version on this page is specified for steel — and in steel the behaviour is different in three ways worth knowing.
| Behaviour | What it means in steel | What to do about it |
|---|---|---|
| Displacement | Material is compressed into the thread form | Hole size close to pitch diameter |
| No chips | Nothing to clear from an enclosure | Suitable for sealed assemblies |
| Higher strip risk | A formed thread in thin steel strips sooner than a cut one | Right hole and right torque |
| Reuse limit | Each re-drive wears the formed thread | A joint opened often needs a machine thread |
| Forming torque | Higher than cutting, and it peaks early | Star drive and a torque-controlled driver |
The advantage over a cutting screw is that the thread in the sheet is denser and has no chip channel weakening it, so pull-out is better for the same size. The advantage over a self-drilling screw is that there is no swarf and no point to break through, so a sealed enclosure stays sealed.
The limit is thin material. A formed thread in a very thin sheet has little wall to press into, and it strips at a lower torque than a machine thread in a tapped insert would. Where the joint will be opened more than a few times, a machine screw and an insert is the honest specification, not a forming screw re-driven into a worn hole.
The recorded finish is white zinc, applied after the thread is rolled. It is thin, bright and sacrificial, and on a forming screw the thinness is what matters: the lobes have to press into the steel, and a heavy coating blunts them.
| Finish | How it protects | Effect on the lobes | Typical use |
|---|---|---|---|
| White zinc | Sacrificial zinc, blue-white passivation | Thin; thread gauged after | Indoor general assembly |
| Yellow zinc | Sacrificial zinc, yellow passivation | Thin; gauged after | Warm-tone indoor hardware |
| Black zinc | Zinc with black passivation | A few microns; thread re-checked | Dark panels |
| Dacromet | Zinc-aluminium flake layer, cured | Thin film; lobes re-checked | Outdoor and wet assemblies |
| Stainless (equivalent part) | Alloy provides protection | No coating | Wash-down and coastal work |
The lobes are the cutting-and-forming edges of this screw, and a coating that rounds them changes how much material is displaced. That is why the finish is kept thin, the thread is gauged after plating, and the first article is driven into a sample of the actual sheet rather than into a test plate.
Where the assembly is outdoors, white zinc is the wrong answer even though it looks right on the bench. A Dacromet or stainless version of the same form is what holds up, and on thread forming screws for steel the environment should be named on the drawing rather than inferred from the finish.
Three assemblies where a chip-free thread in steel is the point:
| Where it sits | The screw fixes a plate or a component into a formed hole in sheet steel, where loose swarf inside the box is a fault. |
| When it goes wrong | A cutting screw leaves chips that can bridge a terminal, and a pointed screw can break through a thin wall. |
| Why it happens | The enclosure is sealed, the sheet is thin, and the fixing is driven on a line. |
| What we control | Hole size confirmed in the sheet sample, lobes checked on the first article. |
| Where it sits | The screw joins a bracket or a cover to a coated steel skin where the joint has to close without damaging the coating on the far side. |
| When it goes wrong | A drill point cuts through and chips the coating, and a loose chip rattles in the product. |
| Why it happens | The panel is coated and thin, the fixing repeats, and the assembly is tested for noise. |
| What we control | Point form checked flat, thread gauged, first article driven in a coated sample. |
| Where it sits | The screw holds a cover on a sheet frame where the joint is opened for service and the thread has to survive a few cycles. |
| When it goes wrong | A formed thread in thin sheet strips after a few re-drives, and a head that is too small dishes the cover. |
| Why it happens | The joint is serviced, the sheet is thin, and the fixing is in reach. |
| What we control | Hole and lobes checked, torque set from the first article, and the re-drive limit agreed. |
Four reasons that matter on a trilobular forming screw, each tied to what the drawing has to prove:
|
Hole and lobes reviewed together
The hole size, the lobe form and the sheet gauge are reviewed as one set, so a screw that would strip is raised before tooling. Basis: Hole and lobes reviewed as one set. |
Head, thread and flat end in one route
The pan head and the star recess are formed in one stroke, the trilobular thread is rolled, and the end is trimmed flat. Basis: One route from wire to plated screw. |
|
Lobes and thread checked on the part
The lobes are checked on a section, the thread is gauged after plating, and the first article is driven into the customer sheet. Basis: First article driven in the sheet sample. |
First article to repeat production
Drawing revision, wire heat, die set and thread roll are fixed at the first article and used as the comparison for repeat orders. Basis: First article signed off before the batch is released. |
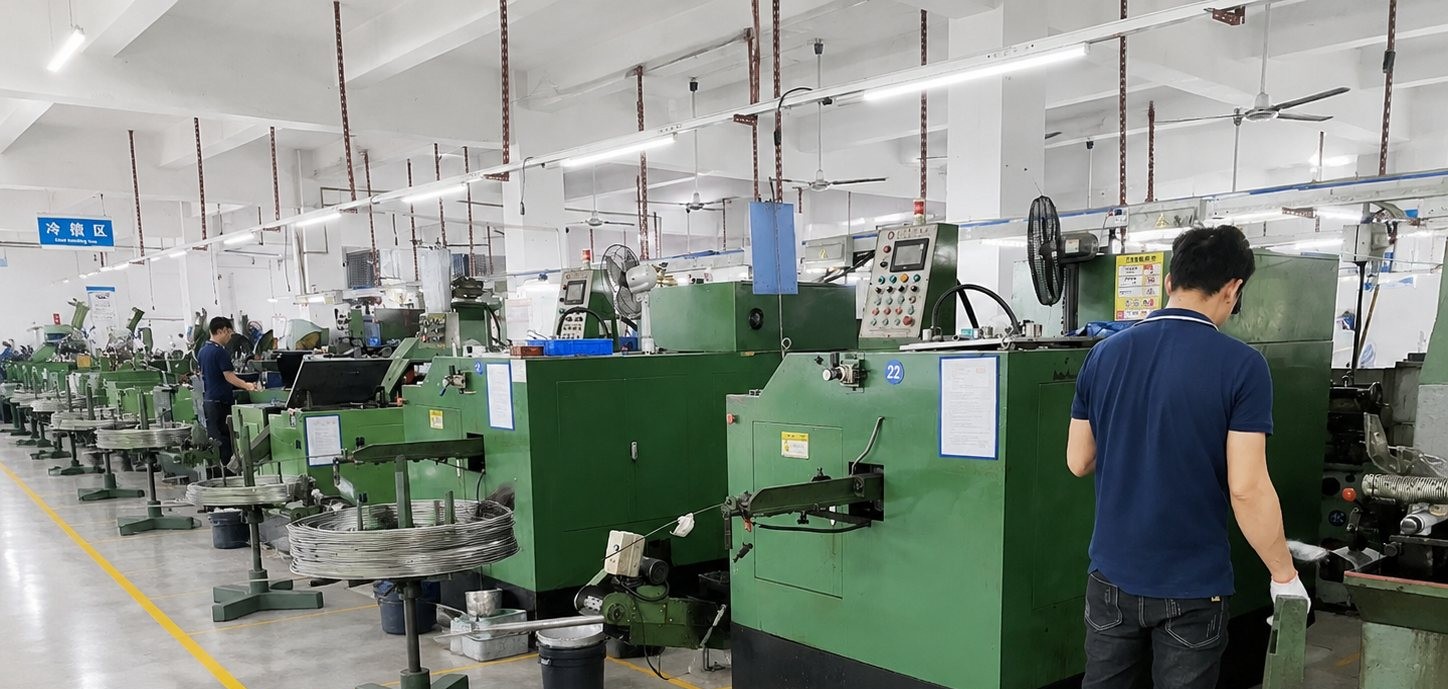
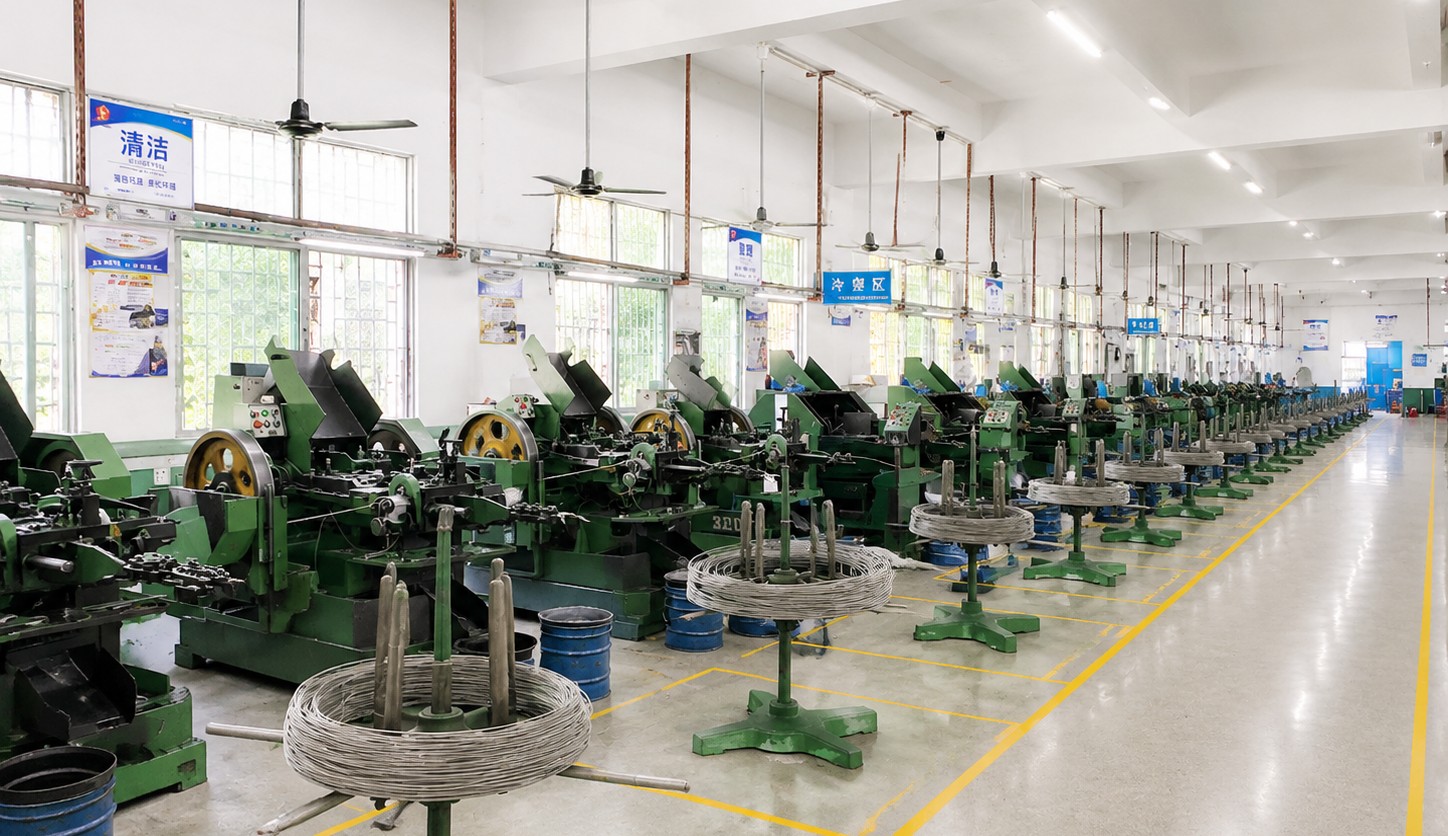
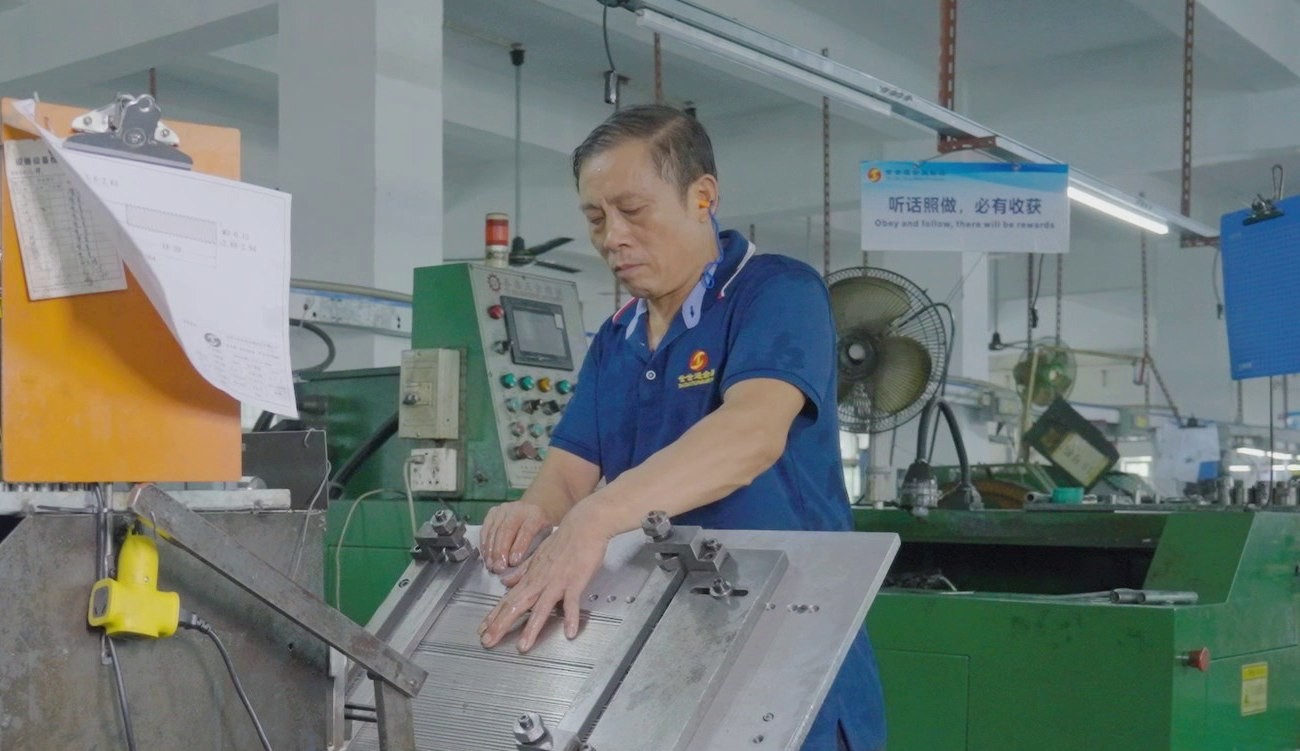
Shi Shi Tong forms these thread forming screws for steel on a single-die header that upsets the pan head and the star recess in one stroke, rolls the trilobular thread over the full length and trims the end flat with a small chamfer. The parts are white zinc plated. The first part of every run is measured on the head, checked on a thread section and driven into a sample of the customer’s steel, before the batch continues.
|
|
The trilobular roll is the tool that defines the part. The three lobes have to be equally spaced and equally deep, because an uneven spacing drives the screw off-line and strips the hole on one side. That is checked on a section of the first article rather than by eye, and the roll is changed on that evidence.
What decides whether thread forming screws for steel pass is the lobe form, the head, the thread and the finish. The inspection agreement covers those, and the criteria come from the drawing.
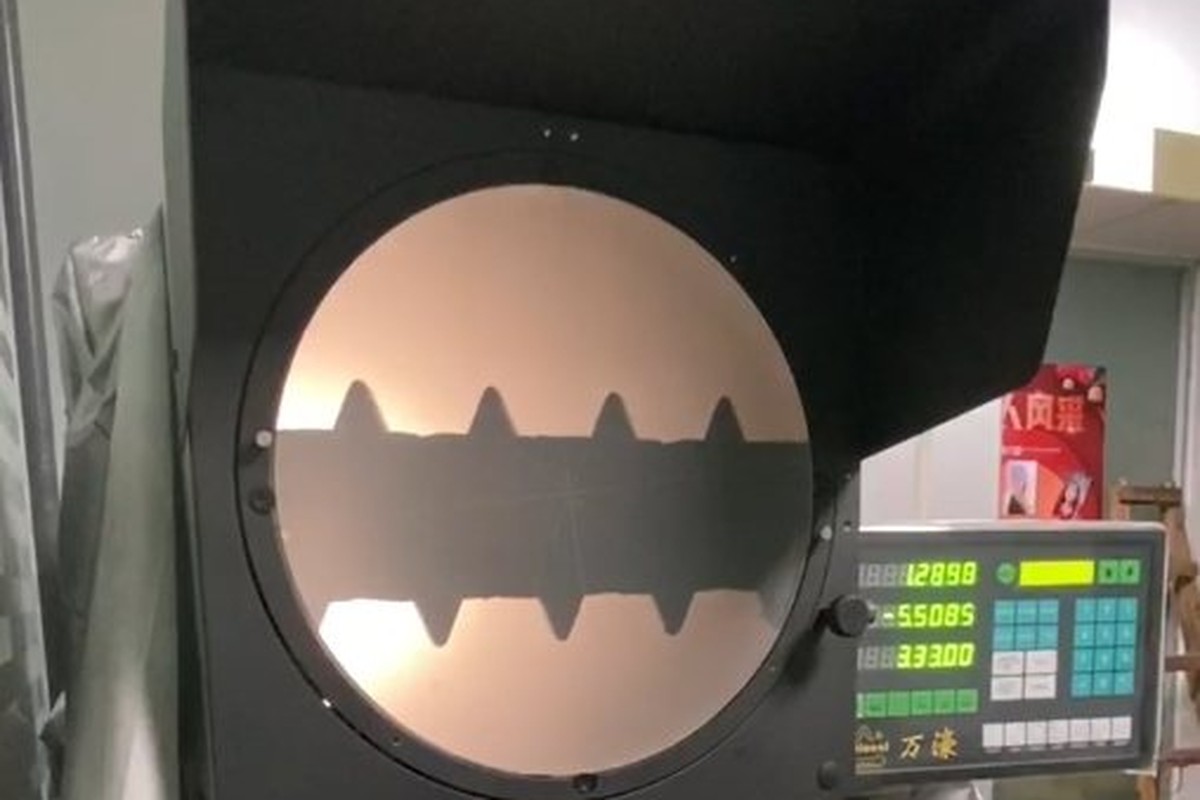
Lobe form on the projector |
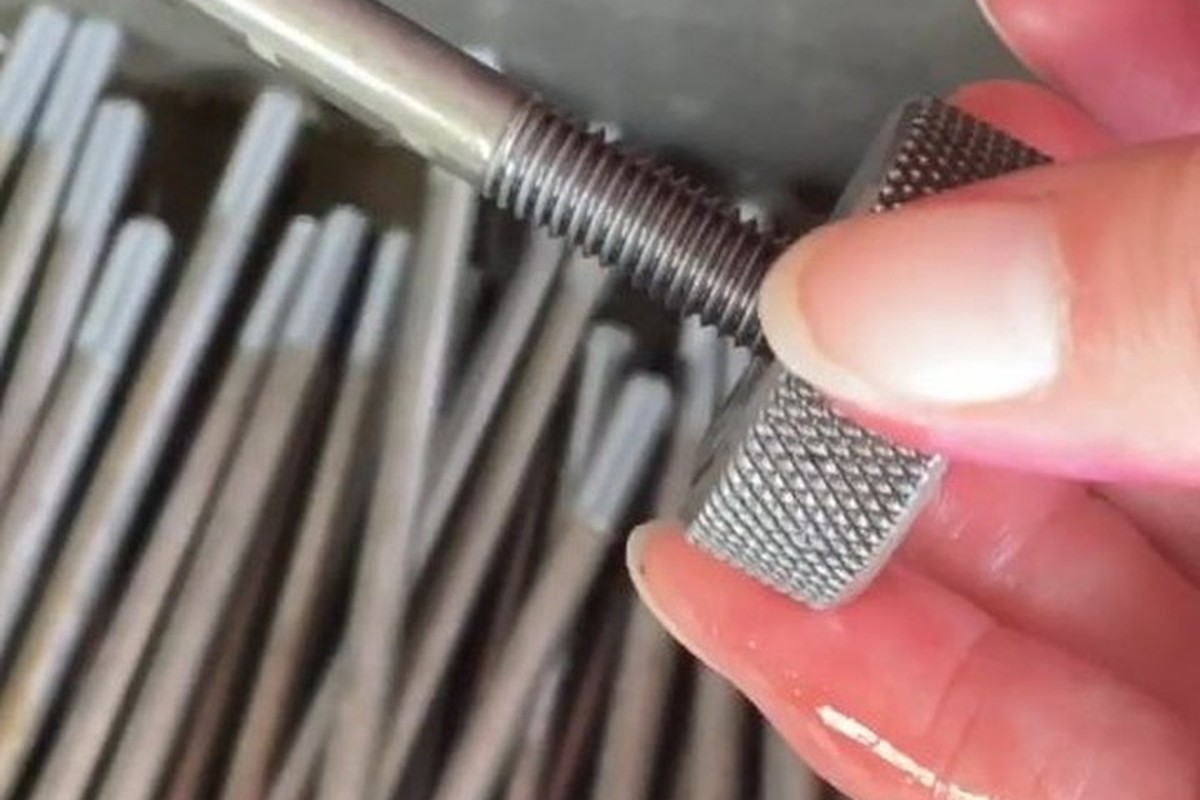
Thread gauged after plating |
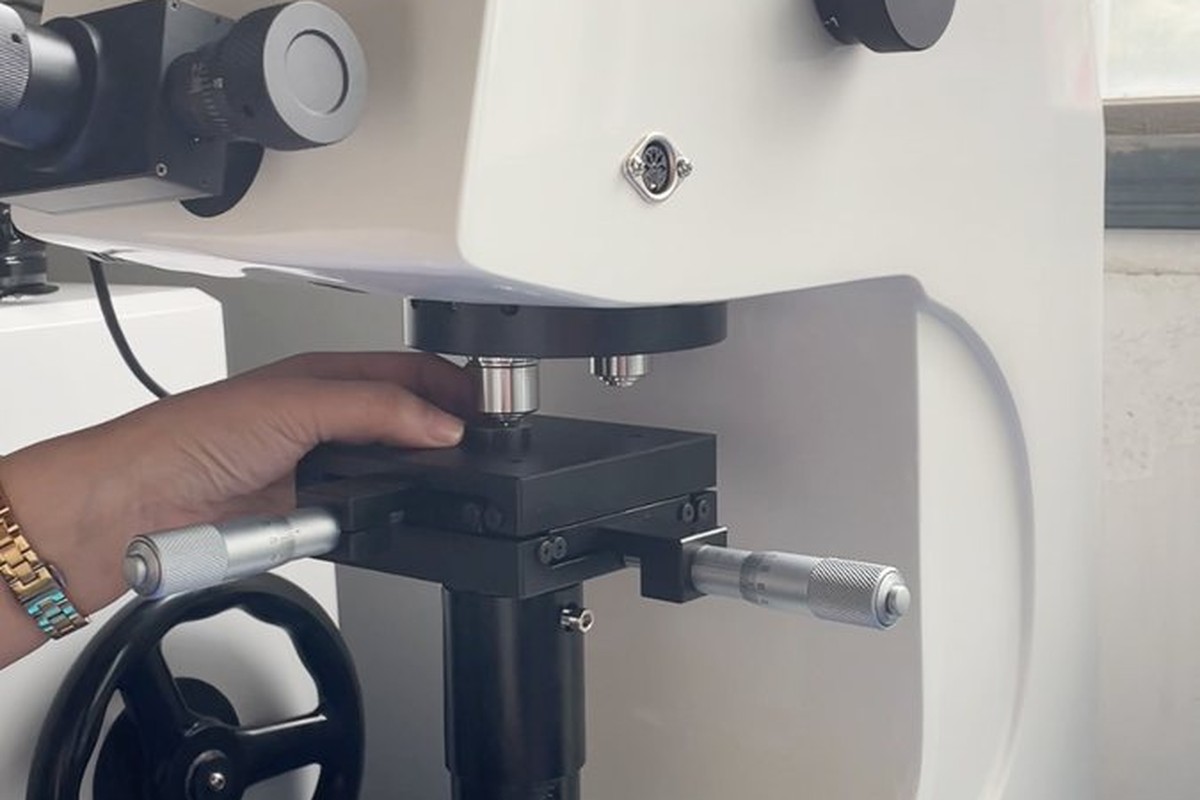
Hardness testing against the property class |
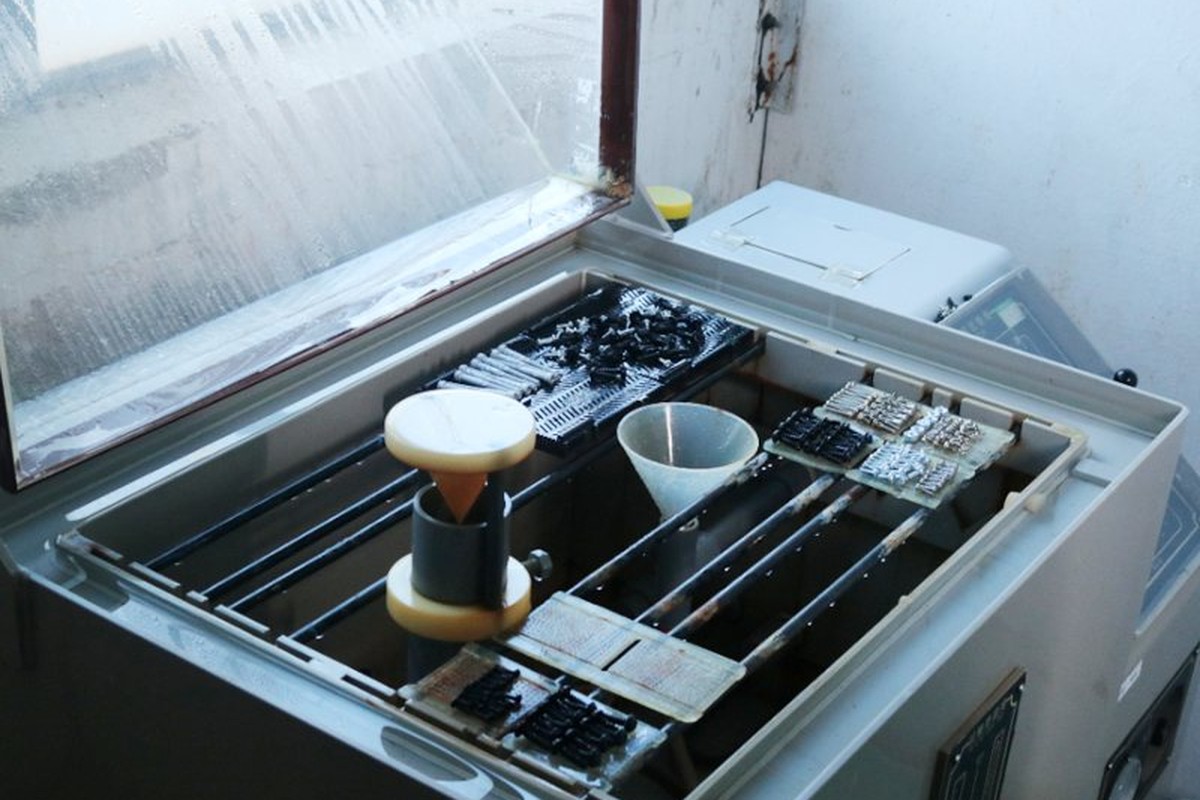
Salt-spray testing of the white zinc plate |
The lobes are checked on a section of the first article, because the difference between the lobe crest and the relief is what the screw is for and it cannot be judged from the outside. A batch that measures right on the major diameter and has drifted on the lobes behaves as a different part.
The driving test is done in the customer’s steel. A forming screw that strips its hole has failed even if every dimension is right, and the only way to catch it is to drive one into the sheet and look at the thread it formed.
Every shipment of thread forming screws for steel is traceable to the wire it was made from and to the plating batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.
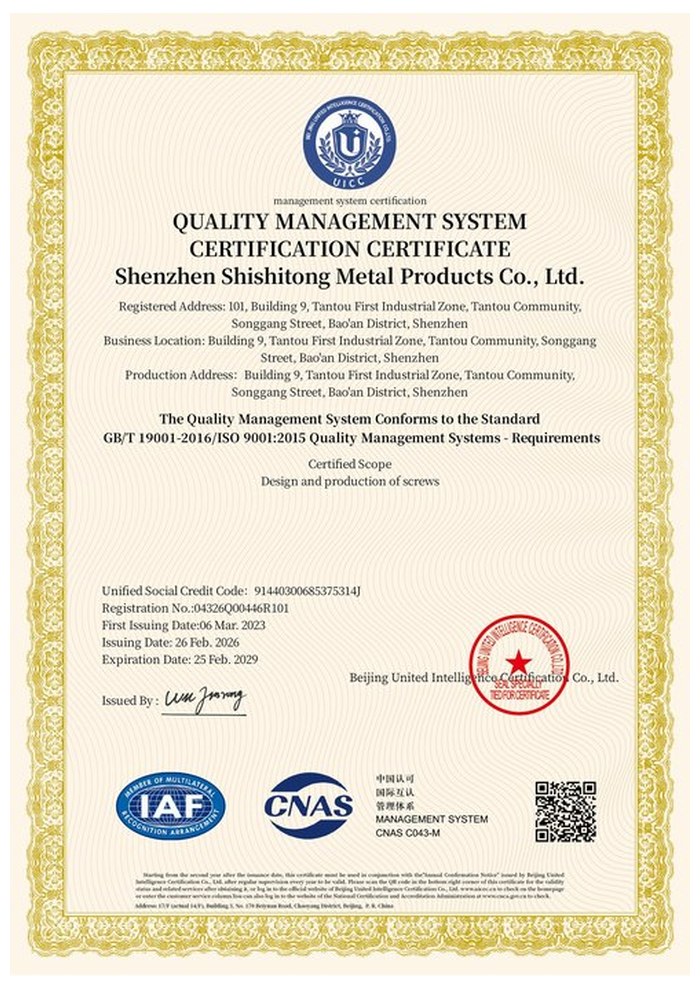
ISO 9001:2015 |
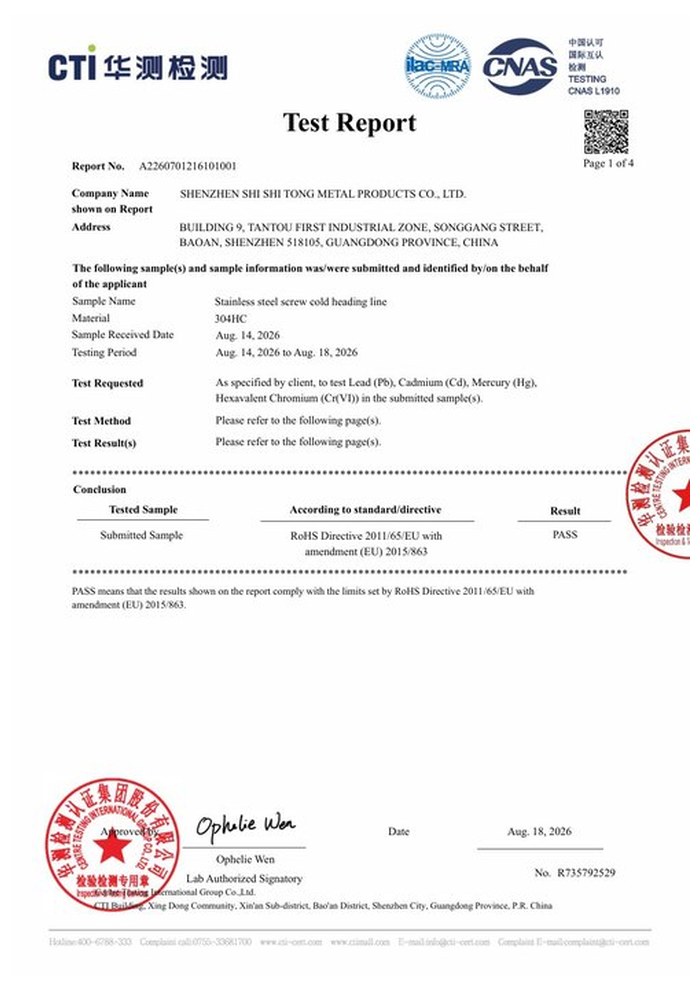
RoHS test report |
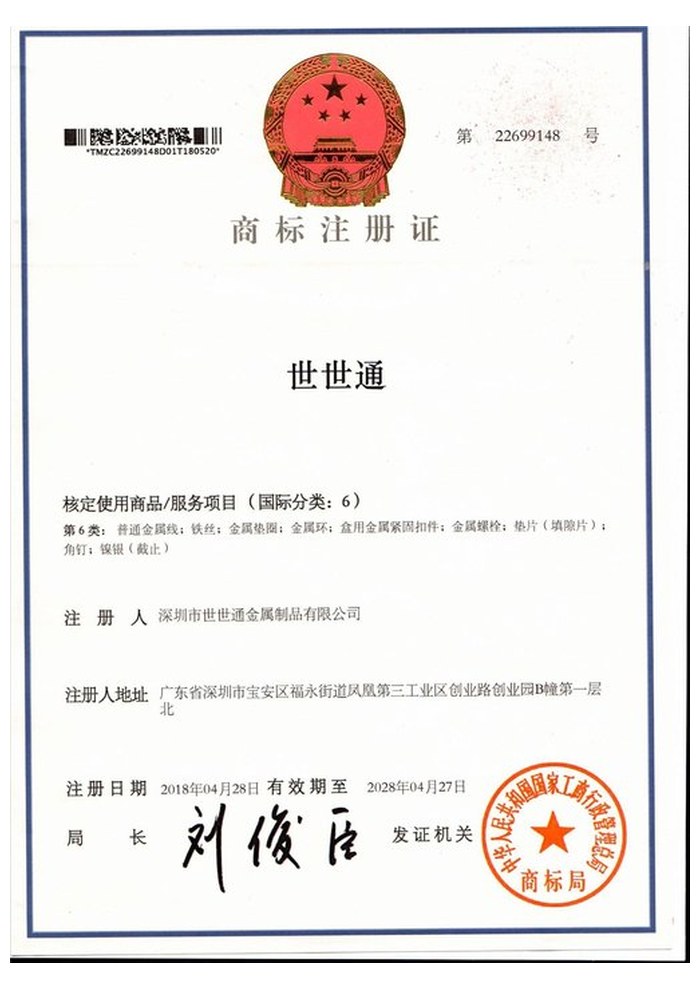
Registered trademark |
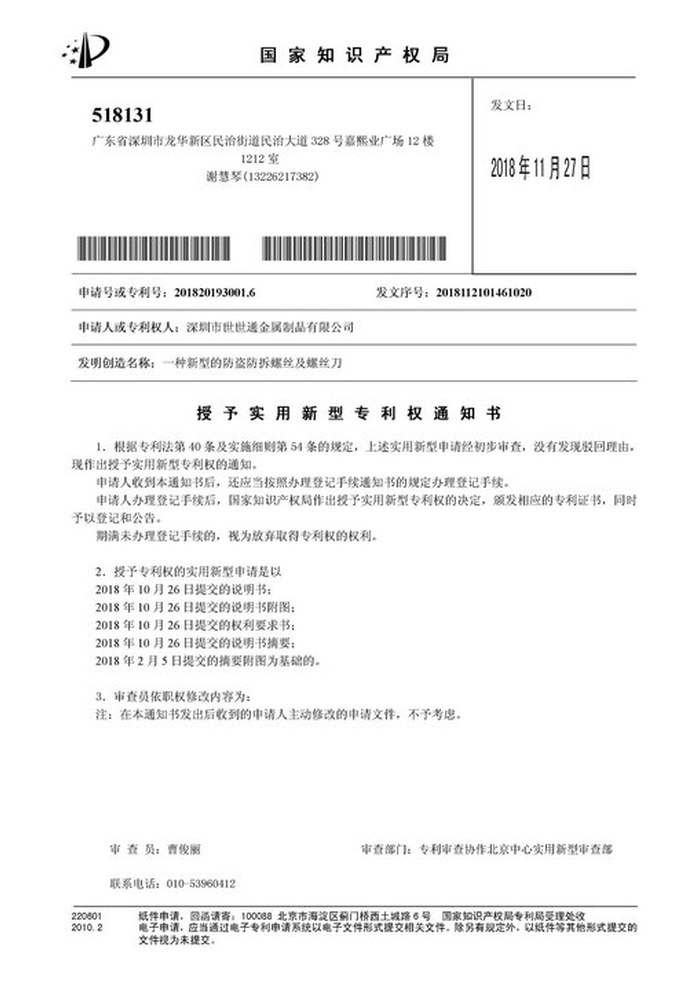
Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the plating. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a forming screw the first article is driven into the customer’s steel and the hole is recorded with the result, because the two only work as a pair. Buyers visit during the process to review samples and to see how the threads are rolled.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header and the plating line can be seen on the day the parts run.
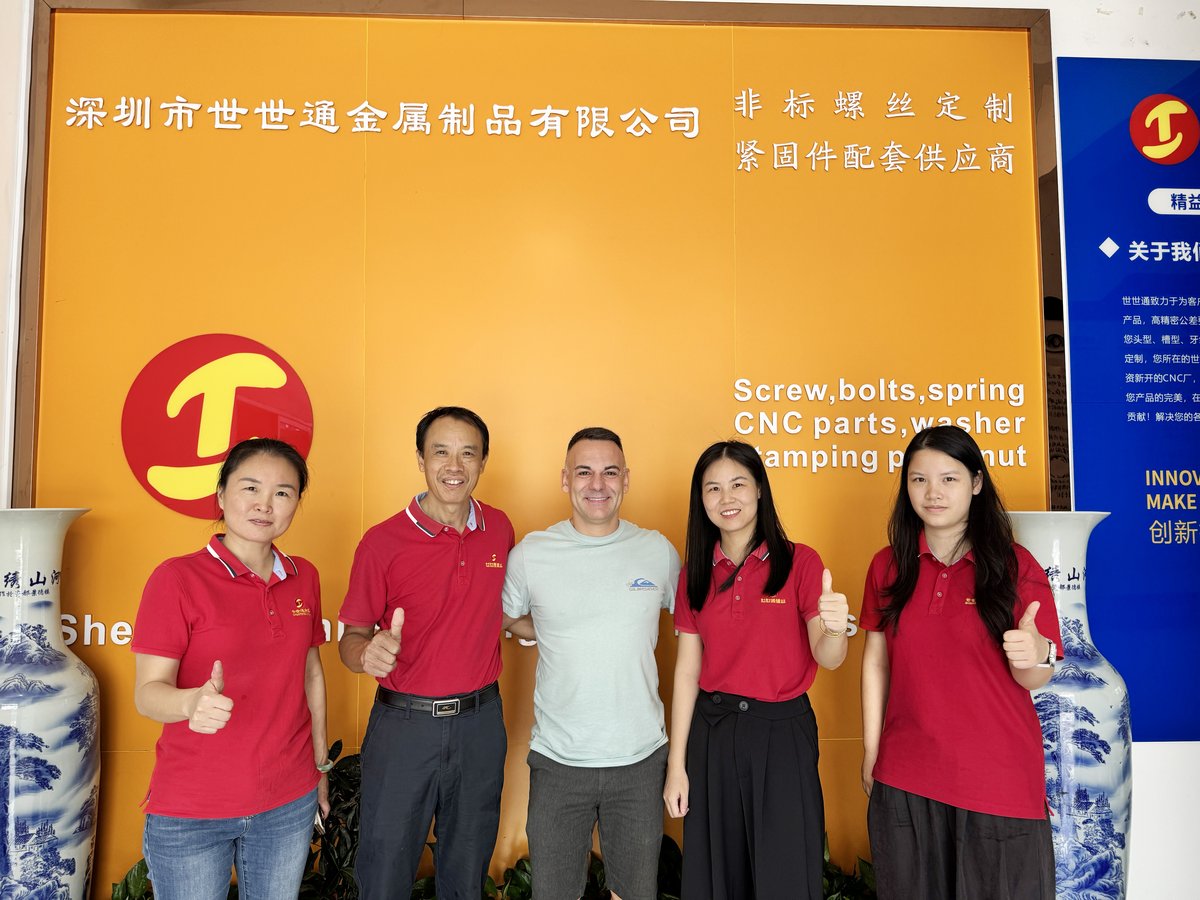
Customer group visit – sample review |
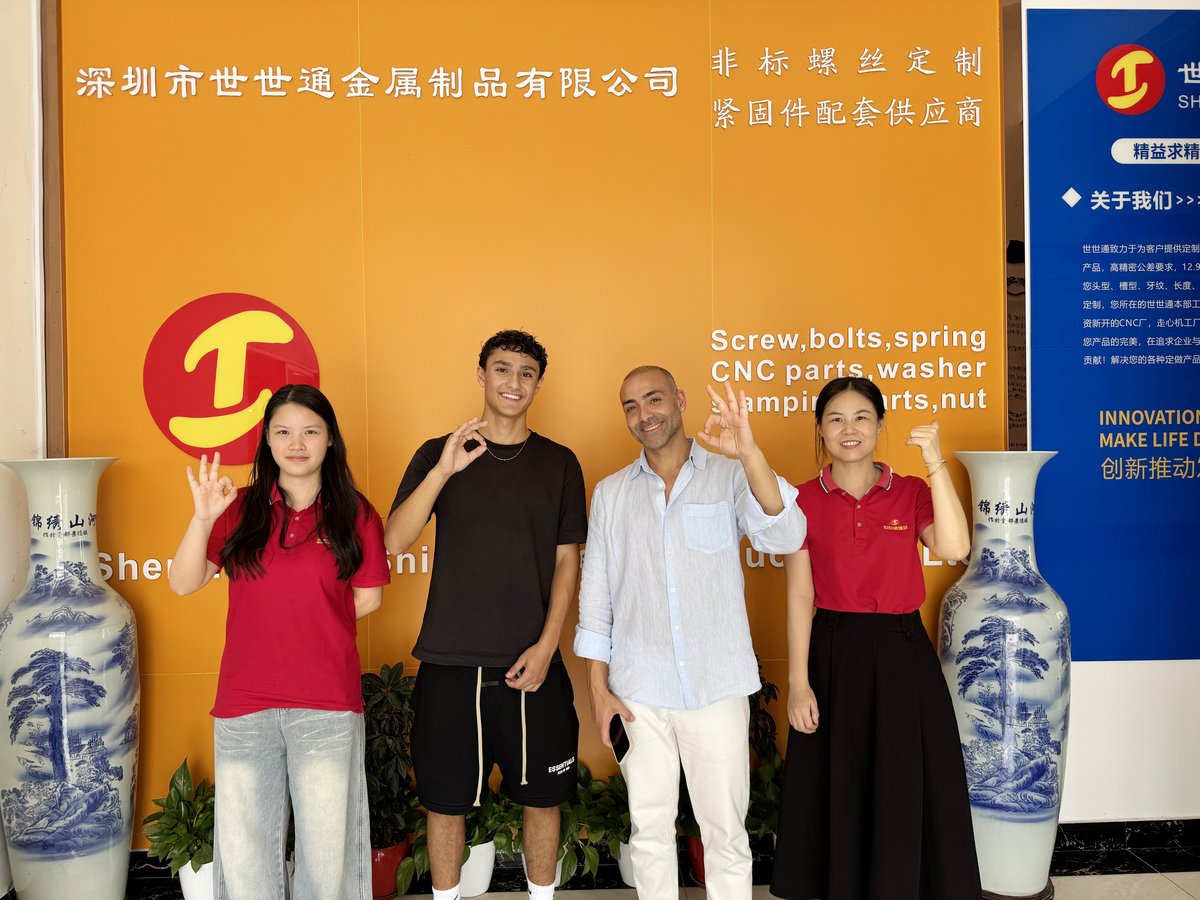
Customer group visit – process discussion |
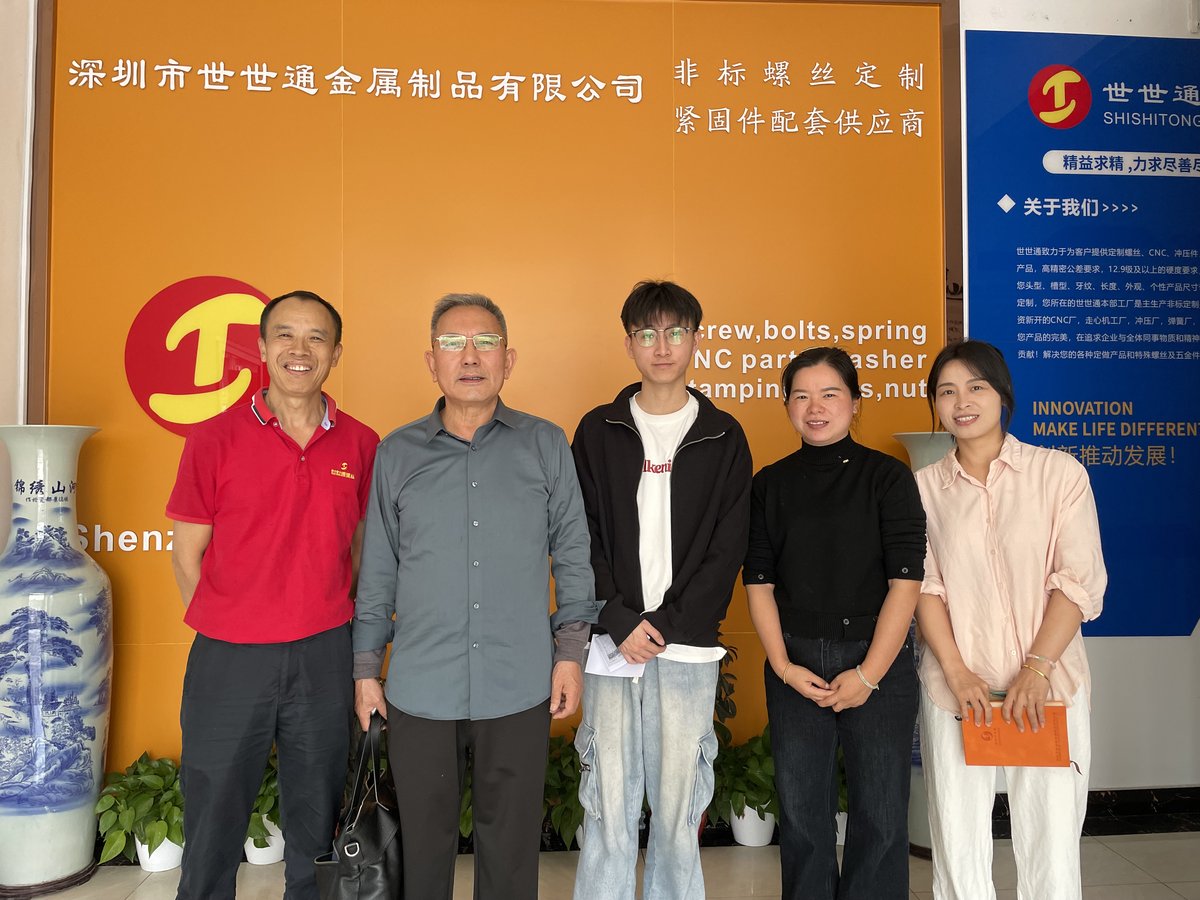
Customer group visit – factory tour |
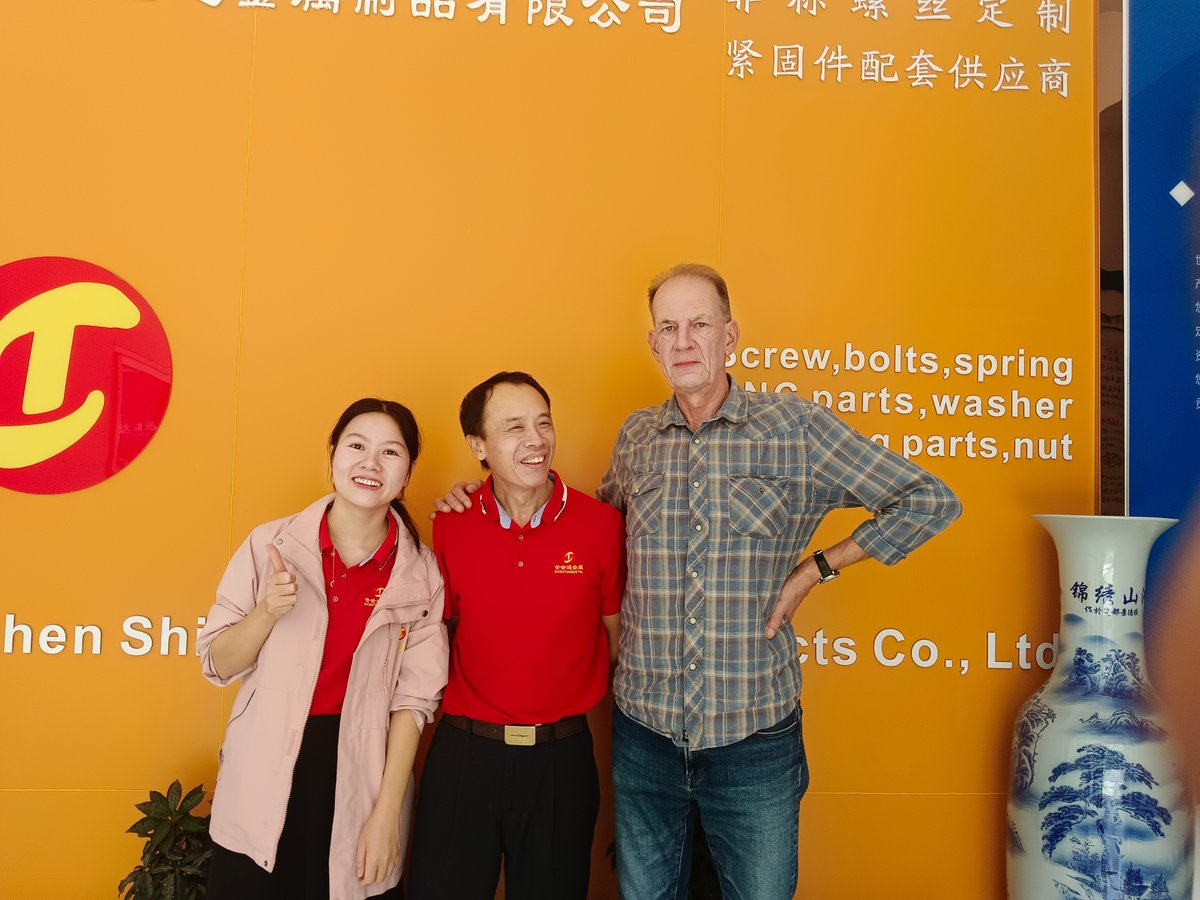
Customer visit – project kick-off |
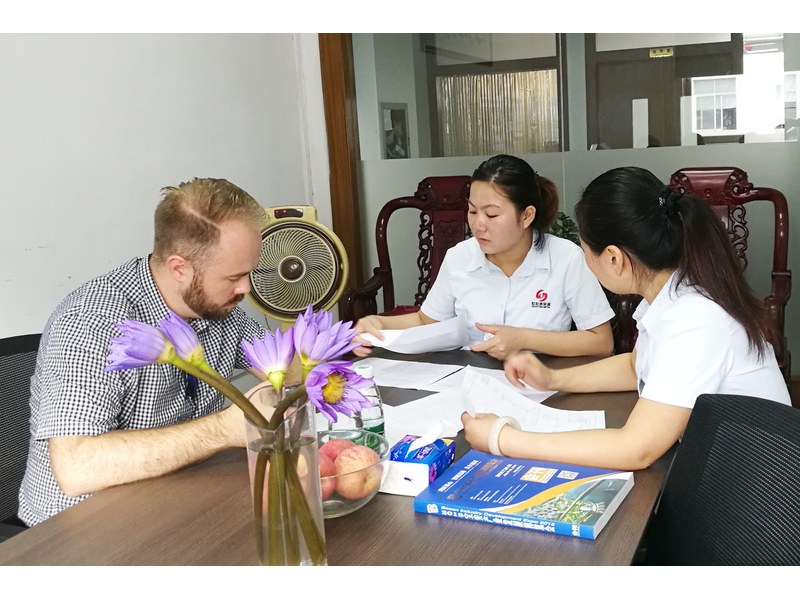
Danish customer – drawing review |
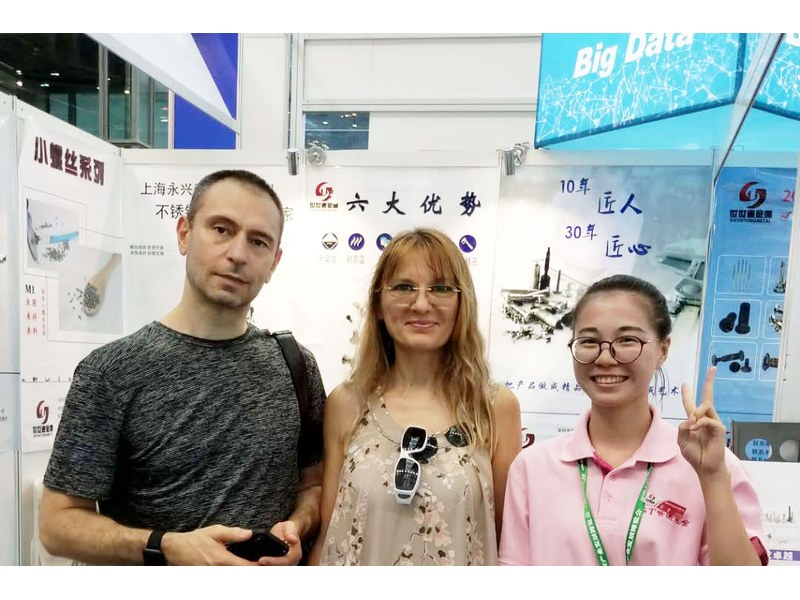
Industry exhibition – meeting customers |
The screw presses material into a thread form instead of cutting it away, so no chips are produced and the thread in the sheet is denser than a cut one.
One close to the pitch diameter of the thread — not the same as the hole for a cutting screw. It belongs on the drawing and is tested in the actual sheet.
So the screw cannot drill or break through, and stops when the hole ends. It also means the hole has to be drilled or punched first.
Only a few times. Each re-drive wears the formed thread in the sheet, and in thin steel it strips sooner than a machine thread in an insert.
Forming torque is higher than cutting and peaks early, so the bit has to stay seated. A star bit does that; a cross recess cams out.
Thread size, head diameter and height, star recess size, length and datum, hole size, material and finish.
How a thread forming screw project runs from drawing to repeat delivery:
|
1
Send the drawing and a sheet sample
|
→ |
2
Hole and lobe review
|
→ |
3
First article driven in the steel
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size, head diameter and height, star recess size, length and datum, hole size, material and finish.
|
Thread size
|
Head diameter and height
|
Star recess
|
|
Hole size
|
Length and datum
|
Material and finish
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.
 +86 13143444311
 sst@szsst88.com