Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
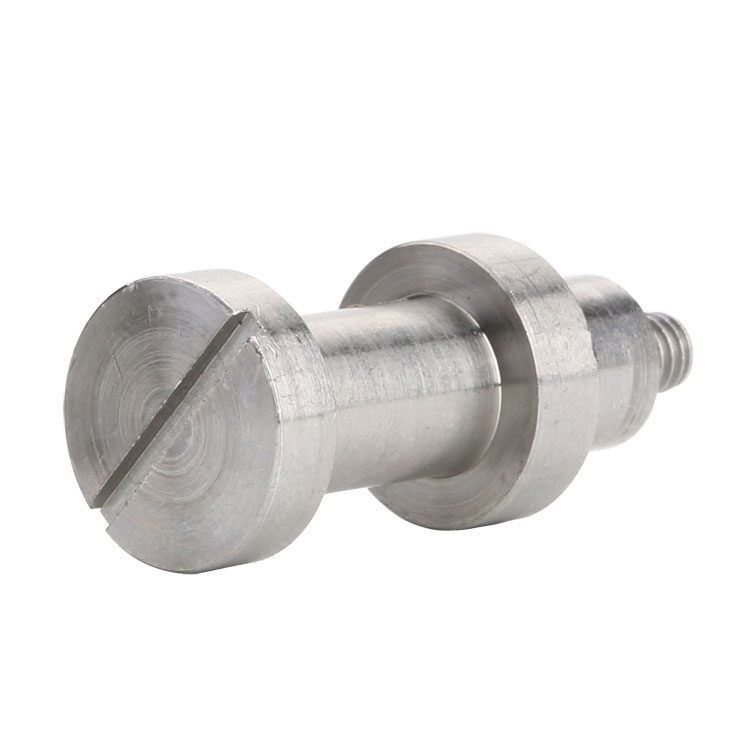
Type:Turned Slotted Cap Screw, Non-Standard
Materials:Stainless Steel
Surface treatment:Plain (cleaned and passivated)
Head Type:Cylindrical Head (cheese head) with single slot
Drive type:Single straight slot milled across the full head diameter
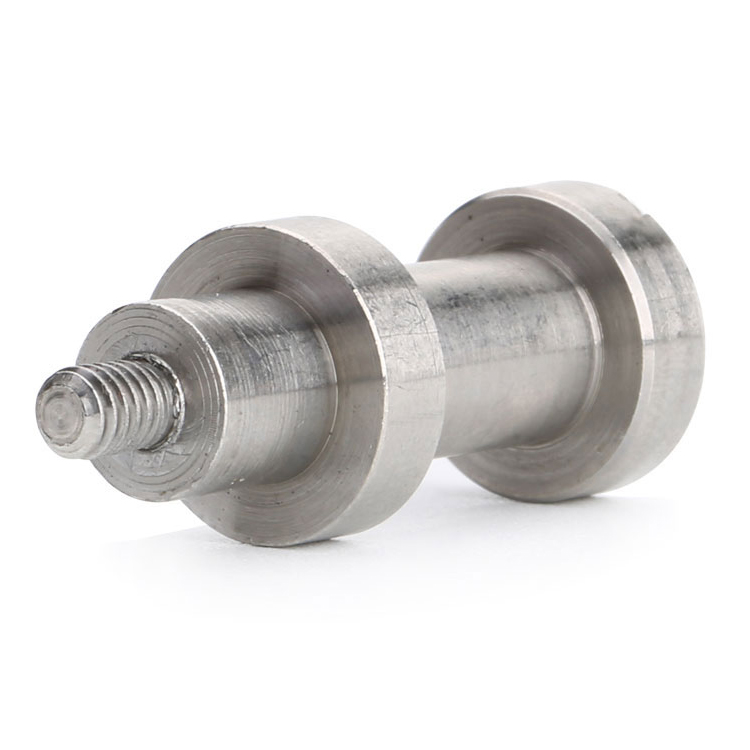
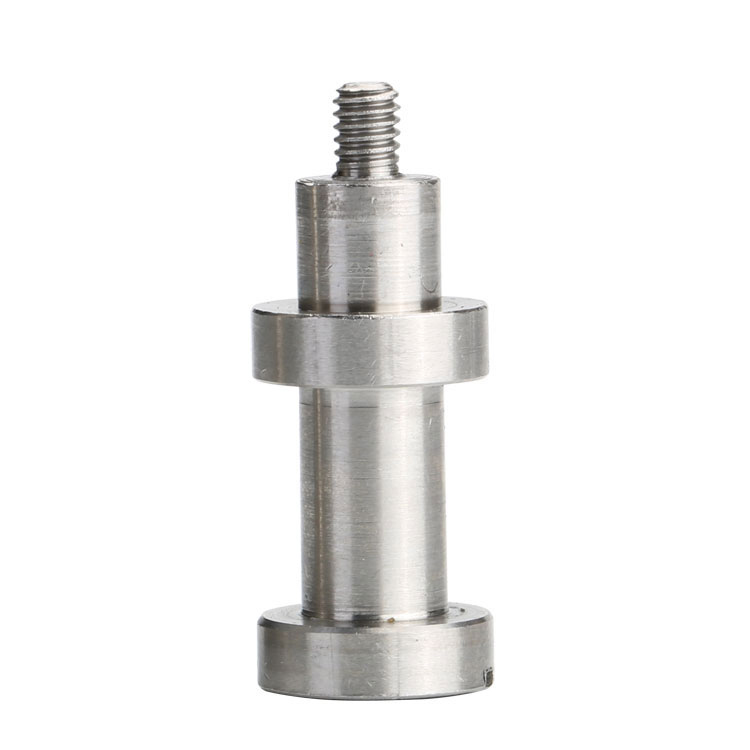
Shank:Long plain journal (bearing diameter) + integral collar + reduced neck
Process:Turned from bar, slot milled, thread cut/rolled, passivated
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Thread:Short machine thread below a reduced neck, rolled; thread start as drawn
Number:52-1
We manufacture slotted cap screws as turned non-standard parts: a cylindrical head with a full-width slot, a plain bearing journal, an integral collar, a reduced neck and a short machine thread, in stainless, quoted from M1 to M14. Journal, collar, neck, slot and thread are taken from your drawing.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A slotted cap screw is a screw with a cylindrical head and a single straight slot across it, driven with a flat blade. The recorded item on this page is a turned non-standard version: a stainless body with a long plain journal, an integral collar, a reduced neck and a short machine thread, with the slot milled across the full head diameter, quoted from M1 to M14 with Number 52-1.
Cylindrical head with a full-width slot. The head is a turned cylinder, and the slot runs across its whole diameter rather than being a short cut in the middle. That lets a wider blade seat deeper, which matters when the part also has to be turned by hand during adjustment.
Plain journal. The long unthreaded section is a bearing diameter, not just a shank. It runs in a bore, so its diameter and surface are held to the drawing and it is the feature the part is really made for.
Integral collar. The collar between the journal and the thread is an axial stop. It seats against a face and takes the end load, so the journal cannot walk through the bore.
Reduced neck. A smaller diameter between the collar and the thread gives the thread room to finish and gives the mating part a clear shoulder to seat against.
Together these decide the part: the journal runs in the bore, the collar stops it axially, the neck clears the end of the thread, the thread clamps, and the slotted head lets it be adjusted. That is why a slotted cap screw of this type is specified by journal, collar, neck and thread together rather than by thread size alone.
The body of this slotted cap screw is stainless bar, turned in one setup so that the journal, the collar and the head stay concentric. The grade is fixed on the drawing; for a part that runs in a bore, the grade is chosen for corrosion and for how it behaves against the mating material rather than for strength alone.
On a slotted cap screw of this type the journal is the working surface. Its diameter is held to the drawing and its surface is finished to suit the bore it runs in; a journal that is undersize lets the part rattle, and one that is oversize will not enter. Because it is unthreaded, it can be re-fitted without damaging anything.
The collar of a slotted cap screw is turned square to the axis. It is the axial stop, so a collar that is not square loads one side of the face and lets the part tilt; squareness is checked on the first article rather than assumed from the turning.
The reduced neck sits between the collar and the thread. It gives the thread a place to finish and gives the mating part a shoulder to seat against, which is what stops the thread from bottoming in a blind hole and holding the collar off its face.
The slot is milled across the full head diameter after turning. Milling it after the turning means the slot is cut into a finished cylinder, so the head stays round and the slot edges stay clean instead of being dragged by a second operation.
Slotted cap screws of this non-standard type are quoted against the drawing rather than a catalogue; the recorded configuration is a turned stainless part quoted from M1 to M14 for the thread, with the journal, collar and neck set per drawing. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
| Item | How it is defined | What we control |
|---|---|---|
| Journal diameter | The bearing diameter that runs in the bore | Measured on the first article against the bore |
| Journal length | The bearing length | Measured from under the head |
| Collar diameter and thickness | The axial stop | Checked square to the axis on the projector |
| Neck diameter | The relief between collar and thread | Measured on the first article |
| Slot width and depth | The blade that fits the head | Checked with the matching blade |
| Thread size and length | The clamping section | Gauged per batch |
Each slotted cap screw is quoted against the bore and the face it works with. The journal diameter and length, the collar thickness and the bore depth are reviewed together, because the part is located by the journal and stopped by the collar — the thread only clamps what is already aligned.
Length is stated four times on a drawing of this kind: overall, journal, collar and thread. A drawing that gives only the overall length leaves the machinist to divide it up, and on a part with three shoulders that division changes the fit.
This part has four features that each do a different job, and the drawing has to describe all four. It is a good example of why a non-standard turned screw cannot be specified by thread size alone.
| Feature | What it does | What goes wrong if it is wrong | What we control |
|---|---|---|---|
| Journal | Runs in the bore and locates the part | Undersize rattles, oversize will not enter | Diameter and surface measured against the bore |
| Collar | Axial stop against a face | Out of square tilts the part and loads one side | Squareness checked on the projector |
| Neck | Relief where the thread ends | Thread bottoms and the collar never seats | Diameter and length measured on the first article |
| Full-width slot | Blade access for adjustment | A short slot limits blade width and depth | Width and depth checked with the blade |
On a slotted cap screw the neck is the feature most often left off a drawing and most often needed. Without it the thread runs straight into the collar, the mating part has no shoulder to seat on, and the joint is clamped by the thread rather than by the collar face — which is exactly the load path this part is designed to avoid.
The full-width slot is a deliberate choice over a short slot. A wider blade engages more of the head, which suits a part that is turned by hand for adjustment, and it lets the slot be cleaned out if the head gets coated or dirty in service.
Turning holds the relationship between the features. The journal, the collar and the head come off one setup, so they stay concentric; the slot is milled afterwards into that finished geometry. That sequence is what keeps the part running true in its bore.
This slotted cap screw is supplied cleaned and passivated, with no coating. On a part with a bearing journal that is not a cost decision: a coating on the journal would change the running clearance, and a coating on the collar would change where the part stops.
| Finish | How it protects | Effect on journal and slot | Typical use |
|---|---|---|---|
| Plain, passivated stainless | Passive film after machining | No build-up; journal as turned | Bearings, instruments and fixtures |
| Electropolished | Surface levelled, chromium enriched | A few microns removed; journal re-measured | Visible and hygienic assemblies |
| Bead blasted | Uniform matte surface | No dimensional change; finish changes | Parts where glare matters |
| Black oxide (stainless) | Chemical conversion, thin film | Minimal thickness | Dark mechanisms |
| Hard chrome (on steel equivalents) | Hard wear layer | Thickness matters; journal re-ground | High-cycle pivots in steel |
Salt-spray exposure is agreed per project and written on the drawing; plain stainless is tested in the condition it ships in. Where the journal runs in a plain bore, the finish question is a wear question as much as a corrosion one, and a hard coating on a steel equivalent would need the journal re-ground after coating.
Packing protects the journal and the slot of a slotted cap screw. The parts are bagged in counted quantities, labelled with the batch, the heat number and the journal diameter, and packed so the journals cannot knock against each other, because a burr on a bearing diameter is a functional defect.
Three assemblies that need a turned part with a bearing journal rather than a standard screw:
| Where it sits | The journal runs in a bore and the collar seats against a face, so the part acts as a pivot pin with a threaded end for adjustment. |
| When it goes wrong | A journal with clearance lets the lever wobble, and a collar out of square tilts it and wears one side of the bore. |
| Why it happens | The mechanism is small, the part is adjusted in service, and the joint is opened for maintenance. |
| What we control | Journal diameter and collar squareness checked on the first article, and the thread gauged per batch. |
| Where it sits | The part carries a small component on its journal and clamps it with the thread at the end, with the slotted head used to make the adjustment. |
| When it goes wrong | A journal that runs tight will not turn by hand, and a neck that is missing lets the thread bottom and hold the collar off. |
| Why it happens | The assembly is adjusted by hand, the parts are small, and the setting has to hold. |
| What we control | Journal fit measured against the bore, neck checked, and the slot checked with the blade. |
| Where it sits | The part replaces a standard screw in a fixture where the stack height, the bore and the axial stop are all fixed by the existing hardware. |
| When it goes wrong | A part made to thread size but not to the journal will not fit the fixture, and re-machining it in place is not possible. |
| Why it happens | The assembly already exists, the drawing is fixed, and the part must match it exactly. |
| What we control | All four features measured on the first article against the drawing, before the batch runs. |
Four reasons that matter on a turned non-standard part, each tied to what the drawing has to prove:
|
Four features reviewed, not just the thread
The journal, collar, neck and thread are reviewed together against the bore and the face before the bar is cut, so a part that will not seat is raised first. Basis: Journal, collar, neck and thread reviewed together. |
Turned and milled in one route
The journal, collar and head come off one turning setup and the slot is milled into that finished geometry, so the axes stay concentric. Basis: One route from bar to finished part. |
|
Journal and collar checked on the part
The journal is measured against the bore, the collar checked for squareness and the thread gauged, on the first article. Basis: First article checked against the bore and face. |
First article to repeat production
The first article fixes the drawing revision, heat number and machining programme; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong turns these slotted cap screws from stainless bar: the journal, collar, neck and head are produced in one setup, the slot is then milled across the head, and the thread is cut or rolled on the end section. The parts are cleaned and passivated. The first part of every run is measured on all four features and checked with the blade, before the batch continues.


|

|
On a turned part the programme carries the quality, so the first article is measured feature by feature rather than checked for overall size. The journal is measured against the bore it will run in, and the collar is checked for squareness on the projector; any change to the programme is proved on a part before the run continues.
What decides whether a slotted cap screw passes is the journal diameter and length, the collar diameter, thickness and squareness, the neck diameter, the slot and the thread class. The inspection agreement covers all of them, and the criteria come from the drawing.

Collar squareness and head on the projector |

Thread gauged per batch |

Hardness testing where the drawing requires it |

Salt-spray testing of the passivated part |
Each batch is recorded against the drawing revision: journal, collar, neck and slot from the first article, the thread gauged per batch, and the material heat kept with the record. If any measurement is out, the parts back to the last good setting are held and re-checked.
An outside report on the material, where the drawing asks for one, is filed with the batch so the paperwork and the parts share one batch number.
Every shipment of slotted cap screws is traceable to the bar it was made from. The grade, heat number and standard are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a non-standard turned part the first article is measured feature by feature and offered up to the customer’s bore, so the journal and the collar are signed off in the assembly they locate. Buyers visit during the process to review samples and to see how the parts are turned.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the turning cell and the inspection room can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
It is a screw with a cylindrical head and a single straight slot, driven with a flat blade. This one is a turned non-standard version with a bearing journal, a collar, a neck and a short machine thread.
So a wider blade can seat deeper. On a part that is turned by hand for adjustment, that gives more contact and lets the slot be cleaned out in service.
It runs in a bore as a bearing diameter. The part is located by the journal and stopped axially by the collar, so the thread only clamps what is already aligned.
It gives the thread a place to finish and gives the mating part a shoulder to seat against. Without it the thread bottoms and the collar never touches its face.
Not if the bore and the axial stop are fixed by the existing hardware. A standard screw has no journal or collar, so the fit and the load path both change.
Journal diameter and length, collar diameter, thickness and squareness, neck diameter, slot width and depth, thread size and length, overall length, material and finish.
How a slotted cap screw project runs from drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
Journal, collar and thread review
|
→ |
3
First article in the bore
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the journal diameter and length, collar diameter, thickness and squareness, neck diameter, slot width and depth, thread size and length, overall length, material and finish, and the bore the journal runs in.
|
Journal diameter and length
|
Collar diameter and thickness
|
Neck diameter
|
|
Slot width and depth
|
Thread size and length
|
Bore and material
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com