Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
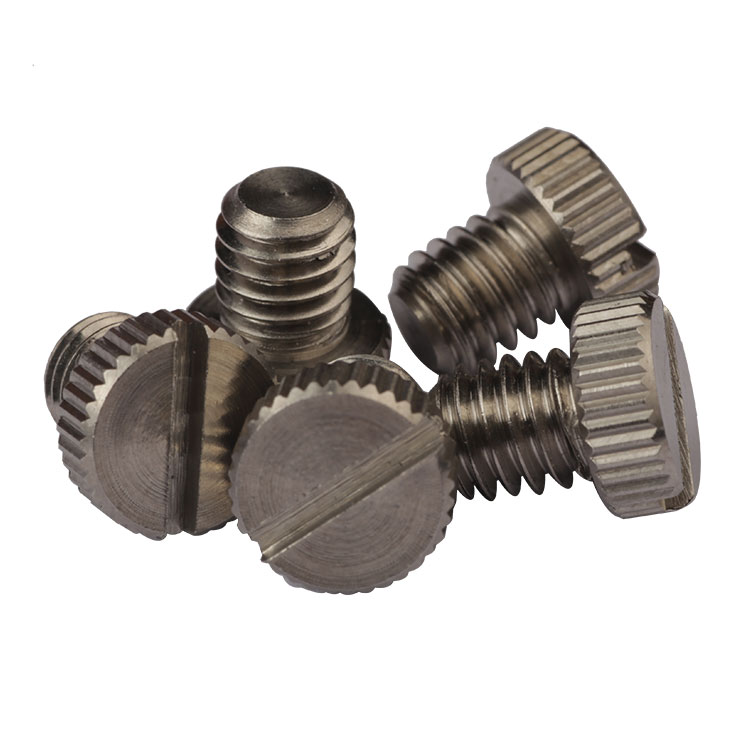
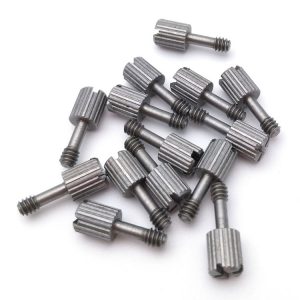
Type:Slotted Thumb Screw
Materials:SUS
Surface treatment:Plain
Head Type:Cap Head
Drive:Single slot across the full face; hand drive on the wide head
Thread:Metric machine thread, rolled 60 degrees, full to the head
Point:Blunt end with a small chamfer; no taper, no drill point
Forming:Single-die heading, slot cut across the face, thread rolling, cleaning and passivation, sorting
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:544
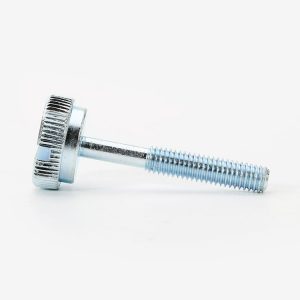
We manufacture slotted thumb screws with a wide flat cap head and one slot across the face, a rolled machine thread and a blunt end, in plain stainless steel. Head diameter and height, slot width and depth, thread and length are taken from your drawing.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A slotted thumb screw is a machine screw with a plain cylindrical head and one straight slot across its face, sized so it can be turned by hand or finished with a flat blade. The recorded item on this page is SUS with a plain passivated finish, a cap head and a single slot, quoted from M1 to M14 with Number 544.
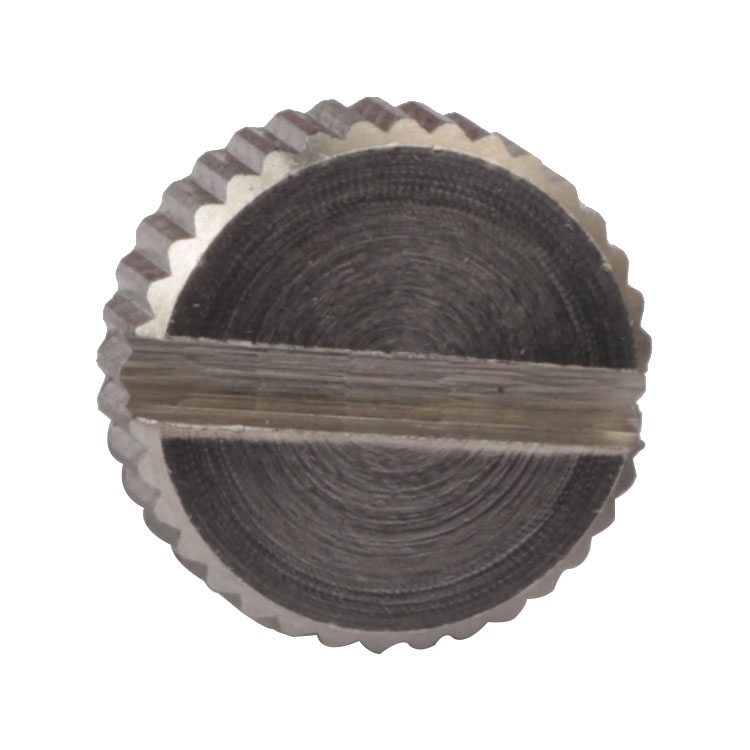
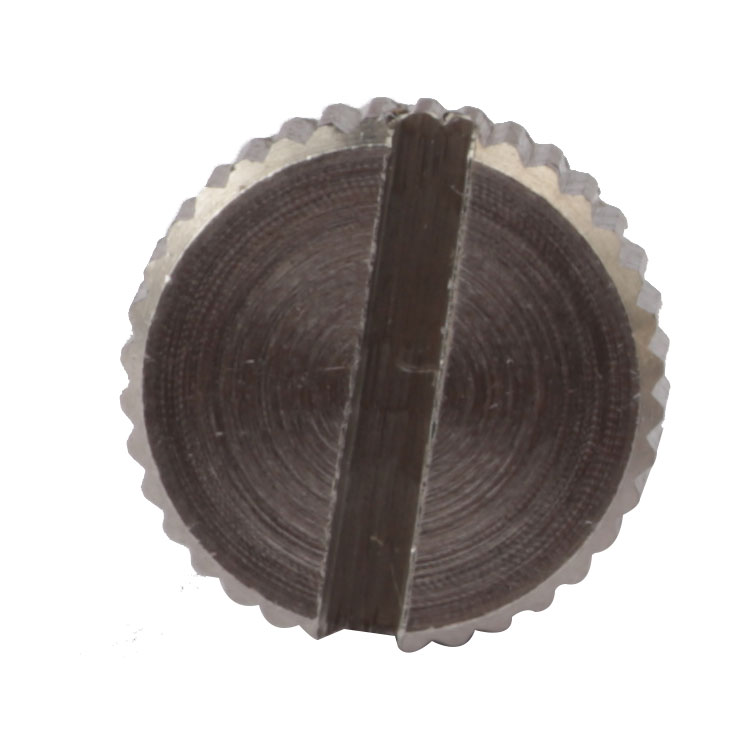
Cap head. A plain cylinder with a flat top and a full flat bearing face. There is no knurl and no recess, so the head reads as a clean disc on the panel — and the flat top is where the slot is cut.
One slot. A single straight slot across the full face. It takes a flat blade, and if the head is wide enough it also gives the thumb something to press against when the screw is turned by hand.
Thumb screw. The head size is what makes it a thumb screw rather than a slotted machine screw: wide enough for the fingers to grip, so the joint can be adjusted without a driver and finished with one when it has to be tight.
Machine thread. A rolled thread for a tapped hole or a nut, with a blunt end. The screw does not cut its own thread: the hole is already there, and the slot is the only drive.
Plain stainless. The alloy provides the protection, so the slot and the thread are bare alloy at their formed size — which on a slotted head is what keeps the blade fit consistent.
The cap head is formed in one heading stroke, and the slot is cut after the head is upset. Cutting it afterwards is what keeps the slot square to the axis; a slot pressed in with the head can lean, and a blade that sits in a leaning slot tilts the screw as it turns.
The slot width and depth are set against the head height. A slot that is too deep thins the material under it, and on a small head that is where the cap deforms under torque; one that is too shallow stands the blade proud and lets it slip out, which on a stainless head leaves a bright mark across the flat top.
The head height is deliberately modest. A slotted thumb screw sits against a panel or in a shallow recess, and a head that is too tall fouls the cover it holds. The flat top and the straight side wall keep the head looking like part of the surface rather than a fitting on it.
The thread is rolled from under the head to the blunt end. Rolling work-hardens the stainless flank and leaves a smooth surface, and it is what lets the screw be turned in and out by hand without galling after a few cycles.
Cleaning and passivation follow, and the recorded finish is plain. Nothing is applied to the slot or the thread, so the blade fits the slot as formed and the thread gauges as shipped. On a slotted thumb screw that is the only drive that has to be checked with a tool.
The family is quoted from M1 to M14, with M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14 in the recorded range. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission; on a slotted thumb screw the head diameter, the slot width and the length are the three numbers that decide whether it can be used by hand at all.
| Item | How it is defined | What we control |
|---|---|---|
| Head diameter | Wide enough for the fingers | Checked on the projector |
| Head height | Plain cylinder, flat top | Measured from the bearing face |
| Slot width | Matched to the blade used | Checked with the blade on the first article |
| Slot depth | Set against the head height | Checked on the section |
| Thread | Metric machine thread, rolled | Gauged per batch |
| Length | From under the head to the end | Measured on the shop plate |
The head diameter is the number that makes it a thumb screw. Below about twice the thread the fingers cannot get enough grip to seat a joint, and above about three times it starts to need more room than the panel has. The practical range sits between those, and it is worth agreeing on the drawing rather than leaving it to the standard.
The slot width has to match the blade. A slot cut for a thin blade will not take a heavier one, and one that is too wide lets the blade rock and rounds the slot edges — which on stainless shows as a polished line on both sides of the slot.
A slotted thumb screw is a joint that can be set by hand and finished with a tool. Both parts of that matter, and the balance between them is what the drawing decides.
| Feature | What it gives | What it costs |
|---|---|---|
| Wide flat head | Grip for the fingers | Needs room around the fixing |
| Single slot | A flat blade can finish the joint | Blade must match the slot width |
| Plain stainless | Slot stays sharp; no coating to fill it | Galls against stainless |
| Machine thread | Runs in and out freely | Backs out under vibration without a lock |
| Blunt end | Stops at the thread end in a tapped hole | Cannot start in an unthreaded hole |
The hand drive is what the part is for. A thumb screw with a wide head can be set, adjusted and removed without a tool, which is why it appears on covers, instrument mounts and anything adjusted in service — and why the head is the dimension that decides whether the joint can be tightened enough by hand.
The slot is the fallback. When the joint has been closed for a while, or a gasket has taken a set, fingers are not enough; a flat blade in the slot will finish it or break it free. That is the difference between this part and a knurled thumb screw with no drive at all, which cannot be helped by a tool once it is tight.
The trade is that a slot on a stainless head is a place where a worn blade shows. A blade that is too thin cuts into the slot edges, and the mark stays. Checking the slot with the blade the customer uses, rather than with a gauge, is what keeps that from happening on the first assembly.
The recorded finish is plain stainless, cleaned and passivated, with no coating. On a slotted head that is the practical default: a coating on the slot walls narrows it, and a coating on the flat top blunts the edge where a blade bears.
| Option | What it does | Effect on slot and thread | Typical use |
|---|---|---|---|
| Cleaned and passivated | Removes free iron after forming | No dimensional change | General and wet service |
| Satin bead blast | Even matte face on the head | Slot edges softened slightly | Visible panels |
| Bright passivated | Cleaner, brighter surface | No dimensional change | Instruments and appliances |
| Electropolished | Levels micro peaks | Slot edges rounded a little; fit checked | Hygienic service |
| Dry film on the thread | Reduces galling in stainless joints | Film kept off the slot | Joints opened often |
Passivation is the only treatment that can be added without touching the slot. It removes the embedded iron from the head and the thread roots and leaves the geometry alone, so the blade still fits the way it was cut — which on a slotted head is the whole function.
A dry film is worth specifying on a joint that is opened more than once, because stainless threads gall. It is applied to the thread only; a film that reaches the slot makes the blade slip, and a slipping blade on a stainless head leaves a mark that cannot be polished out.
Three assemblies where a fixing is adjusted by hand and finished with a blade:
| Where it sits | The screw holds a module or a cover that is opened during setup, where the head is turned by hand and the slot is used when the joint has to be tight. |
| When it goes wrong | A screw with only a knurl cannot be tightened enough for a gasket, and a cross recess in a small head rounds before the joint is closed. |
| Why it happens | The panel is visible, the joint is serviced, and no tool is wanted during adjustment. |
| What we control | Head diameter and slot width checked, blade tried on the first article. |
| Where it sits | The screw closes a small cover or a sensor mount that is removed for cleaning, on stainless equipment. |
| When it goes wrong | A cross recess holds water in its corners, and a plated head loses its coating in the wash. |
| Why it happens | The equipment is stainless, it is washed, and the cover comes off daily. |
| What we control | Grade and passivation recorded, slot checked with the blade, thread gauged per batch. |
| Where it sits | The screw fixes a plate or an accessory where the head is seen and the fixing is adjusted by hand between setups. |
| When it goes wrong | A knurled head reads as a tool part, and a cross recess shows wear quickly on a visible face. |
| Why it happens | The face is finished, the fixing repeats, and the adjustment is frequent. |
| What we control | Head height and slot checked, tone matched to the surrounding hardware. |
Four reasons that matter on a hand-drive slotted screw, each tied to what the drawing has to prove:
|
Head and slot reviewed together
The head diameter, the head height and the slot width are reviewed as one set, so a slot that would thin the head is raised before tooling. Basis: Head and slot reviewed as one set. |
Head, slot and thread in one route
The cap head is upset in one stroke, the slot is cut after heading, and the machine thread is rolled to a blunt end. Basis: One route from wire to passivated screw. |
|
Slot and thread checked on the part
The slot is checked with the blade the customer uses, and the thread is gauged per batch in the finished condition. Basis: First article checked with the blade. |
First article to repeat production
The first article fixes the drawing revision, wire heat, die set, slot width and thread roll; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these slotted thumb screws on a single-die header that upsets the cap head, cuts the slot across the face and rolls the machine thread to a blunt chamfered end. The parts are cleaned and passivated. The first part of every run is measured on the head, checked with the production blade and gauged on the thread, before the batch continues. The same blade test applies to slotted thumb screw in every size in the range.


|

|
The slot is the operation that has to be right. It is cut after the head is formed, so the blade sits square to the axis and the screw drives straight; a slot that is off centre or cut at an angle makes the blade tilt the head, and on a thumb screw that shows as a bright crescent across the flat top.
What decides whether slotted thumb screws pass is the head, the slot, the thread and the surface. The inspection agreement covers those, and the criteria come from the drawing.

Head and slot on the projector |

Thread gauged per batch |

Hardness testing of the wire |

Salt-spray testing where the service requires it |
The slot is checked with the blade, at the joint torque, on the first article. A slot that measures correct and still lets the blade rock has walls that are not parallel, and a rocking blade rounds the edges on the first hard turn — which on a plain stainless head is permanent. Every batch of slotted thumb screw is checked on that blade test.
The head is checked by turning it by hand. Diameter is a dimension; whether a thumb can grip it when the joint is at torque is a judgement, and on a thumb screw that judgement is the specification.
Every shipment of slotted thumb screws is traceable to the wire it was made from. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a hand-drive part the first article is handled as well as measured, because grip and blade fit are the specification. Buyers visit during the process to review samples and to see how the heads are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header and the passivation line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
A machine screw with a wide flat head and one slot across it, turned by hand or finished with a flat blade.
The slot is the tool drive: when the joint is tight, a blade in the slot will finish it or free it. A knurled head with no slot cannot be helped by a tool.
Wide enough for the fingers to grip — roughly two to three times the thread. Below that it cannot be turned hard enough by hand; above it, it needs room the panel may not have.
A hollow-ground flat blade matching the slot width. A thin blade cuts the slot edges; a thick one will not seat.
A plain machine thread can back out under vibration. A nylon patch or a thread insert is specified on the drawing where that matters.
Thread size and pitch, head diameter and height, slot width and depth, length and datum, stainless grade and finish.
How a slotted thumb screw project runs from drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
Head and slot review
|
→ |
3
First article turned by hand and by blade
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size and pitch, head diameter and height, slot width and depth, length and datum, stainless grade and finish.
|
Thread and pitch
|
Head diameter and height
|
Slot width and depth
|
|
Length and datum
|
Grade
|
Finish
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com