Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
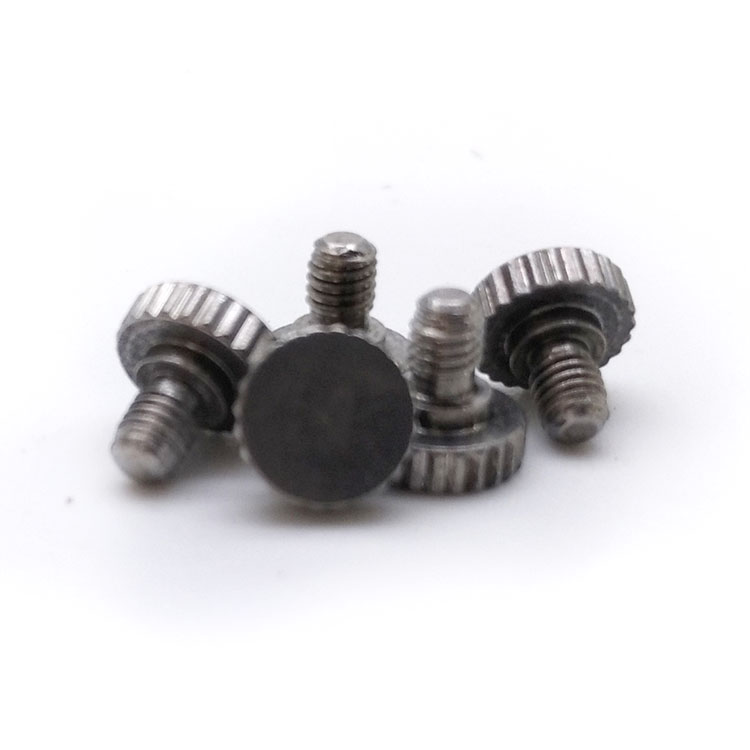
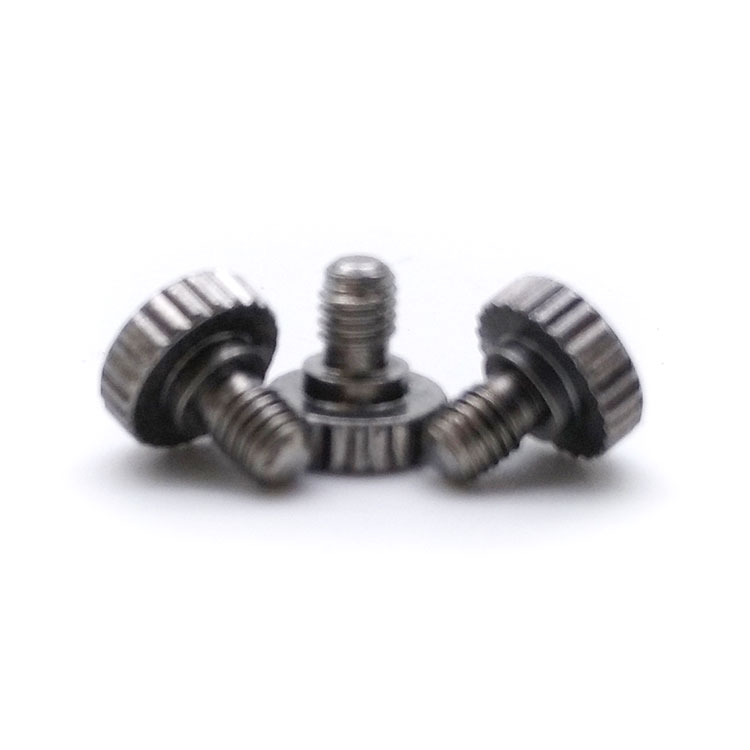
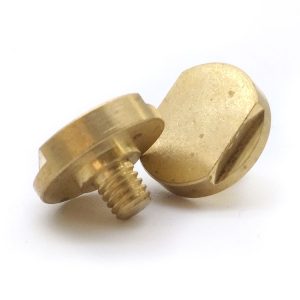
Type:Shoulder Thumb Screw Stainless Steel 303
Materials:Stainless Steel
Surface treatment:Plain
Head Type:Cap Head
Drive:Knurled head, hand adjustment
Thread:Machine thread
Point:Chamfered
Forming:Turned from bar
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:636
We turn shoulder thumb screws from 303 stainless with a knurled cap head, no drive recess, a plain shoulder and a machine thread, quoting them from M1 to M14. Head diameter, knurl pitch and depth, shoulder tolerance and thread come from your drawing, and the first article is turned by hand at your joint.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A shoulder thumb screw is a stainless fastener with a knurled head, no drive recess, a plain shoulder and a machine thread, meant to be turned by hand. This one is turned from 303 stainless, quoted from M1 to M14 with Number 636, and the knurling on the head is the only drive it has.
Knurled cap head. A cylindrical head with a straight knurl cut around it, giving the fingers something to grip.
No recess. There is no slot, cross or socket; the head is adjusted by hand alone, with no tool to supply torque.
Shoulder. A plain section that runs in a bore and locates or pivots the part being adjusted.
303 stainless. A free-cutting grade, chosen for turned parts because it machines cleanly and takes a sharp knurl.
A shoulder thumb screw is specified where a part has to be set by hand between jobs and held where it is put: a stop on an instrument, a clamp on an optical mount, a panel that is opened for service without a tool in reach.
On a shoulder thumb screw the knurl is the drive, and that changes every number on the drawing. A bit or a wrench can supply far more torque than a thread needs; a knurled head supplies whatever two fingers can manage, so the joint has to be designed to be held by fit and by hand torque rather than by preload.
The knurl has to be cut well to be usable. A straight knurl of the right pitch grips at any rotation and does not care which way the hand comes at it; a shallow or worn knurl looks correct and slips under a thumb, and the operator compensates by pinching harder rather than by turning.
Knurl depth is the variable that matters. Too shallow and there is nothing to grip; too deep and the crests are thin and fold over after a few adjustments, leaving a smooth patch exactly where the thumb goes. On a turned part the knurl is cut with a tool that wears, and the wear shows as a loss of depth part way through a batch.
The head diameter is the leverage. A larger head gives more hand torque at the same grip, which is why thumb screws have heads noticeably larger than the thread. On this part the head is a cap form, so the knurl runs the full height and there is no edge to catch.
The shoulder does the locating, and on a thumb screw that is usually the point of the part: a stop, a clamp plate or a lever needs to be set to a position by hand and then held there. The shoulder sets the height or the line, the thread holds it, and the knurled head is how the operator moves it.
The recorded range is M1 to M14, with the sizes used on instrument panels and adjustable stops. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For a shoulder thumb screw the quotation carries the head diameter and height, knurl pitch and depth, shoulder diameter and length, and the thread.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Cap form, knurled | Head diameter, height and knurl form |
| Knurl | Straight knurl around the head | Pitch, depth and crest condition |
| Shoulder | Plain bearing section | Diameter, tolerance and length |
| Thread | Machine thread | Pitch, length and gauging |
| Ends | Chamfered | Chamfer and thread start |
| Material | 303 stainless | Grade and heat number on the certificate |
| Finish | Passivated | Surface condition and knurl appearance |
Knurl pitch and depth belong on the drawing as a pair. Diametral pitch sets the number of crests, depth sets how much of a finger catches, and the two together decide whether the part can be turned with a thumb or needs a pinch.
Shoulder length is measured separately from overall length, and the thread runs from the shoulder end. A thumb screw quoted by overall length alone leaves the division between shoulder and thread to the shop.
Three features define the part: the knurled head, the absent recess and the shoulder. The first is the drive, the second is the promise that nothing is needed to adjust it, and the third is what it adjusts.
| Feature | What it gives | What it costs |
|---|---|---|
| Knurled head | Grip for hand adjustment | Limited torque; knurl wears |
| No recess | Nothing to chip or fill with dirt | No way to apply real torque |
| Large head diameter | Leverage for fingers | Needs clearance around the joint |
| Shoulder | Locates the adjusted part | Fit must be held |
| 303 stainless | Clean turning and sharp knurl | Less corrosion resistance than 316 |
The toolless promise is the reason these parts exist. A cover that is opened for cleaning, a stop that is reset between jobs or a clamp that is adjusted by hand should not require a tool, and a knurled head is the simplest way to make that true.
The cost is torque. Anything that needs to stay tight under vibration needs a drive and a locking feature; a thumb screw holds by being turned firmly, and on a vibrating joint it will move.
The recorded finish is passivation with no coating on 303 stainless. On a knurled head that matters because a coating would round the crests: the knurl depends on sharp edges to grip, and a deposit of a few microns is enough to turn a crisp knurl into a polished one.
| Option | How it protects | Effect on knurl and shoulder | Typical use |
|---|---|---|---|
| 303 stainless, passivated | Passive film; free-cutting grade | Crests sharp; shoulder as turned | Instrument panels and stops |
| 304 stainless, passivated | Passive film, better weldability | Knurl cuts less cleanly | General stainless work |
| 316 stainless, passivated | Passive film with molybdenum | Knurl cuts less cleanly | Marine and medical |
| Steel, black oxide | Conversion film, oiled | No measurable build | Internal mechanisms |
| Aluminium, anodised | Grown oxide, coloured | Rounds the crests slightly | Lightweight adjustment knobs |
303 is the grade to choose when the knurl matters. It machines with a clean chip and takes a sharp crest, which is why thumb screws and knurled knobs are usually made from it rather than from 304 or 316, which tear at the crest and need more finishing.
Where the part is wet, the grade has to change to 316 and the knurl has to be accepted as slightly less crisp. A thumb screw that corrodes in a marine panel is worse than one that needs a firmer pinch.
Three assemblies where a shoulder thumb screw is the fixing:
| Where it sits | The screw is the adjustment for a stop, a clamp or a cover that an operator sets by hand, where a tool would slow the job down. |
| When it goes wrong | A knurl that is too shallow slips under a thumb, and the operator pinches harder to compensate. |
| Why it happens | The joint is adjusted often, there is no tool, and the head is small. |
| What we control | Knurl pitch and depth checked; first article adjusted by hand. |
| Where it sits | The screw locks a sliding element where the lock has to be released and re-tightened by hand between positions. |
| When it goes wrong | The shoulder lets the element shift when the screw is loosened, and the position is lost. |
| Why it happens | The joint is released and re-set by hand, and repeatability matters. |
| What we control | Shoulder tolerance and length held; first article cycled through its positions. |
| Where it sits | The screw holds a panel that is opened for service, where a knurled head means no tool is needed at the machine. |
| When it goes wrong | The head is turned too hard and the knurl folds, or too lightly and the panel rattles. |
| Why it happens | The joint is opened regularly, the head is exposed, and the panel is thin. |
| What we control | Head diameter and knurl depth checked; torque by hand agreed with the customer. |
Four reasons that matter on a hand-adjusted part, each tied to what the drawing has to prove:
|
Knurl and shoulder agreed
Knurl pitch and depth, head diameter, shoulder tolerance and thread are agreed together, because on a shoulder thumb screw the grip and the fit are both the function. Basis: Knurl and shoulder agreed. |
Turned, knurled, threaded in one route
The head, the knurl, the shoulder and the thread are turned in one route, so the knurl and the shoulder stay concentric. Basis: One route from bar to finished part. |
|
Knurl checked by hand
The first article is turned by hand at the joint, because a knurl that measures correctly can still be too fine to grip. Basis: First article adjusted by hand. |
Knurl tool life recorded
The knurl tool change is recorded against the batch, so a repeat order does not arrive with crests that have stopped biting. Basis: Knurl tool life recorded. |
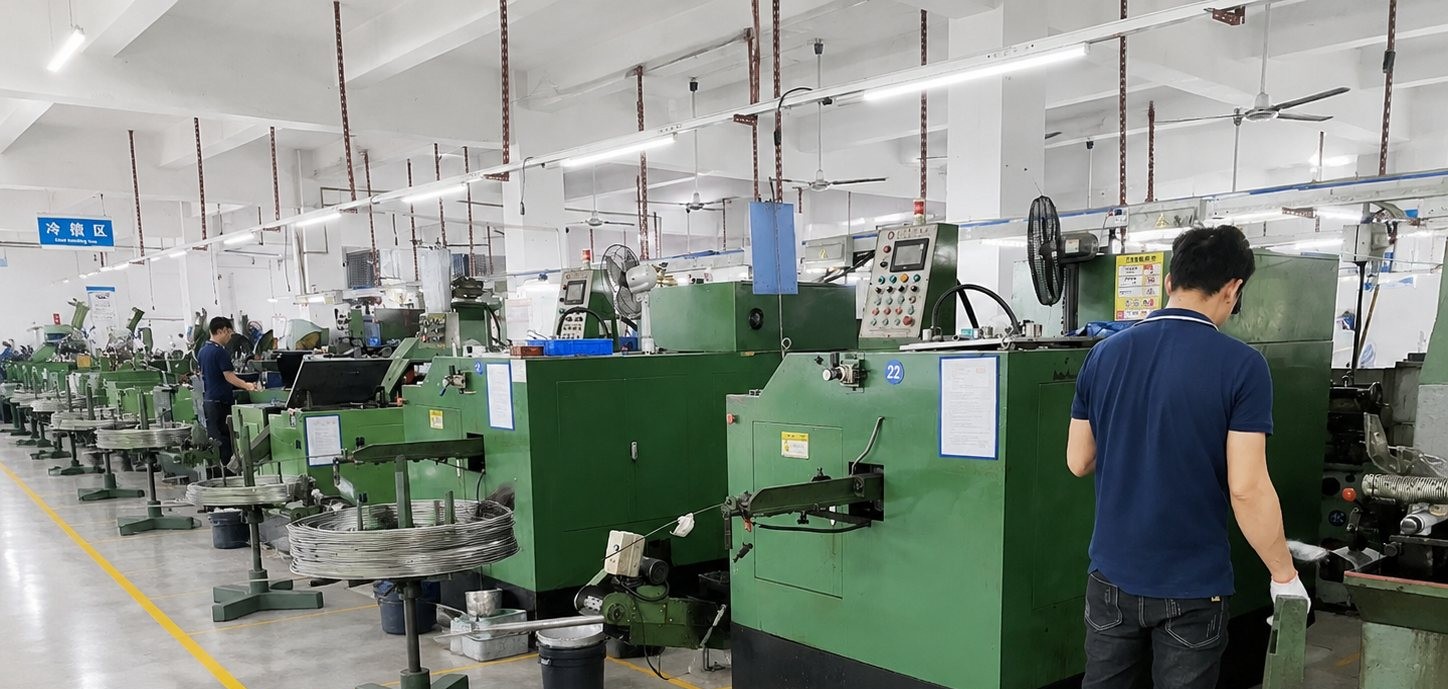
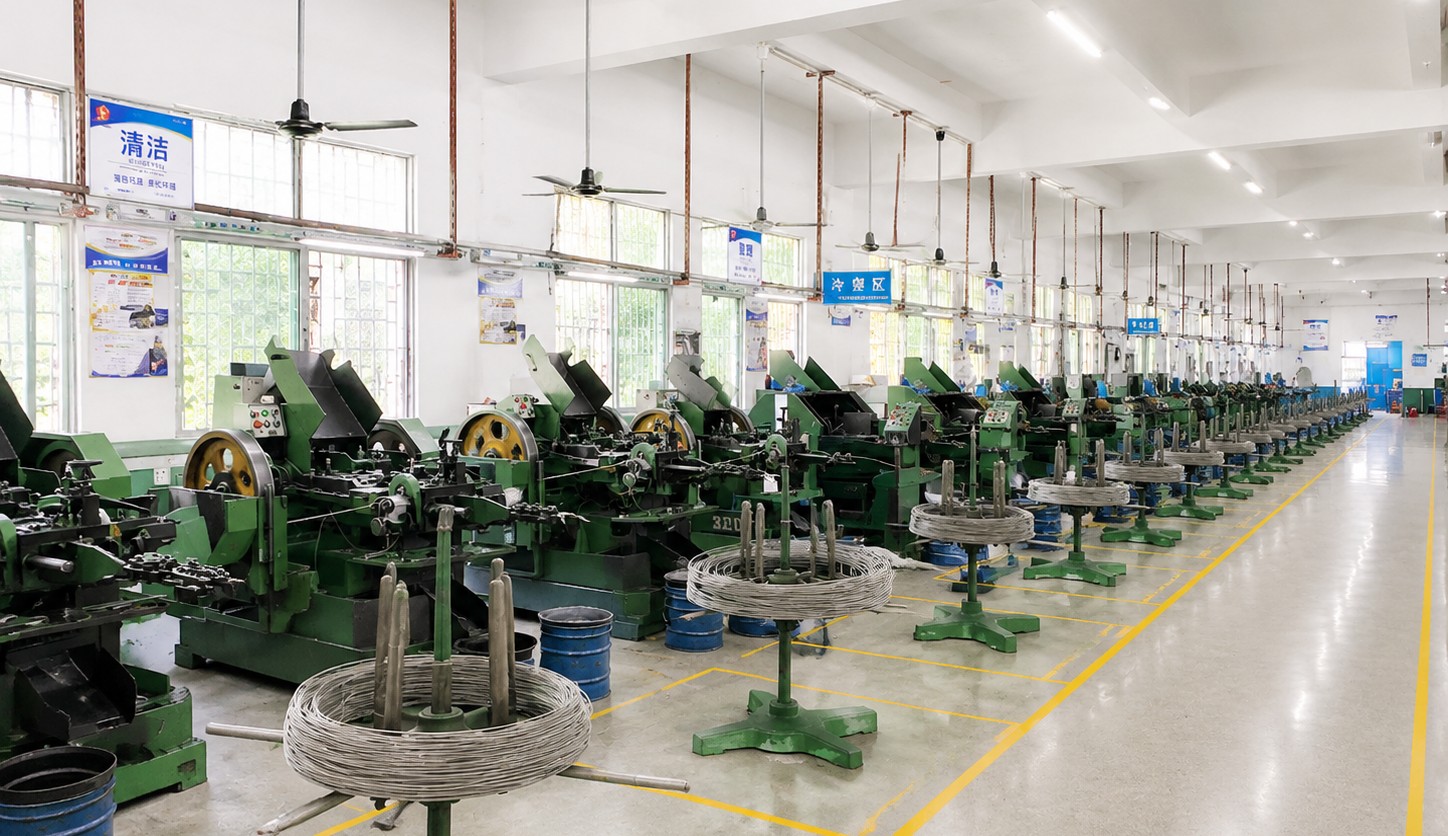
Shi Shi Tong turns shoulder thumb screws from 303 stainless bar, cutting the head, the knurl, the shoulder and the thread in sequence so that the knurl and the shoulder stay concentric. The first part of every run is measured on head diameter, knurl pitch and depth, shoulder diameter and length before the batch continues.
|
|
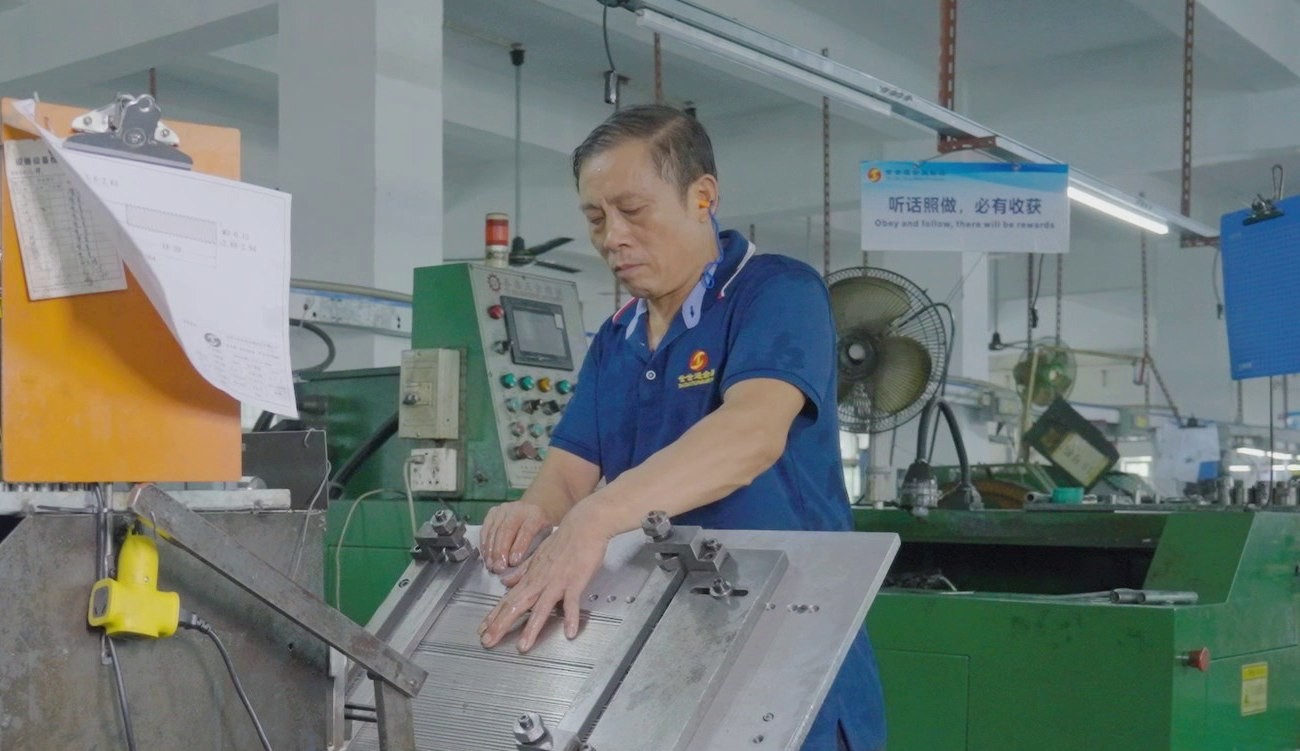
Rolling or cutting the knurl is where the part is decided. The knurl tool wears steadily, and the wear is not visible on the part until the crests stop reaching full depth; a batch made with a worn tool looks right in a photograph and cannot be turned by a dry thumb.
What decides whether shoulder thumb screws pass is the knurl, the head, the shoulder and the thread. The inspection agreement covers those, and the criteria come from the drawing.
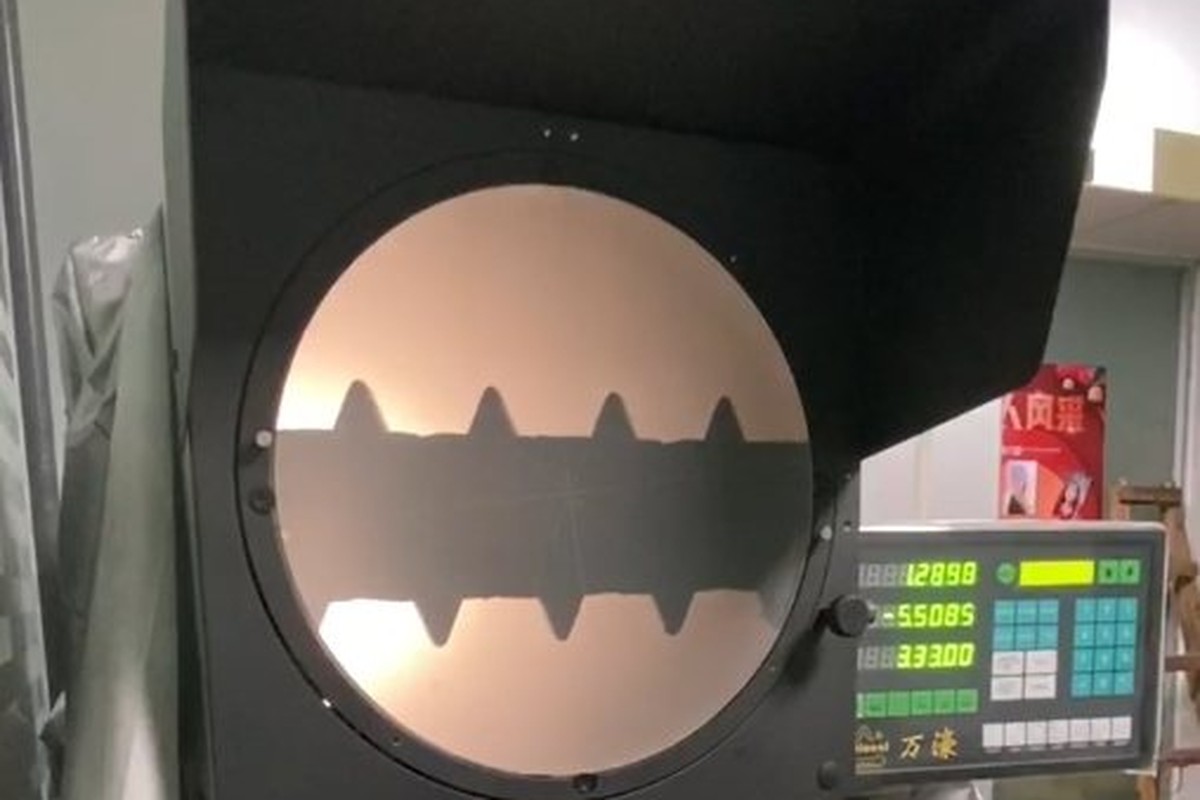
Head and knurl on the projector |
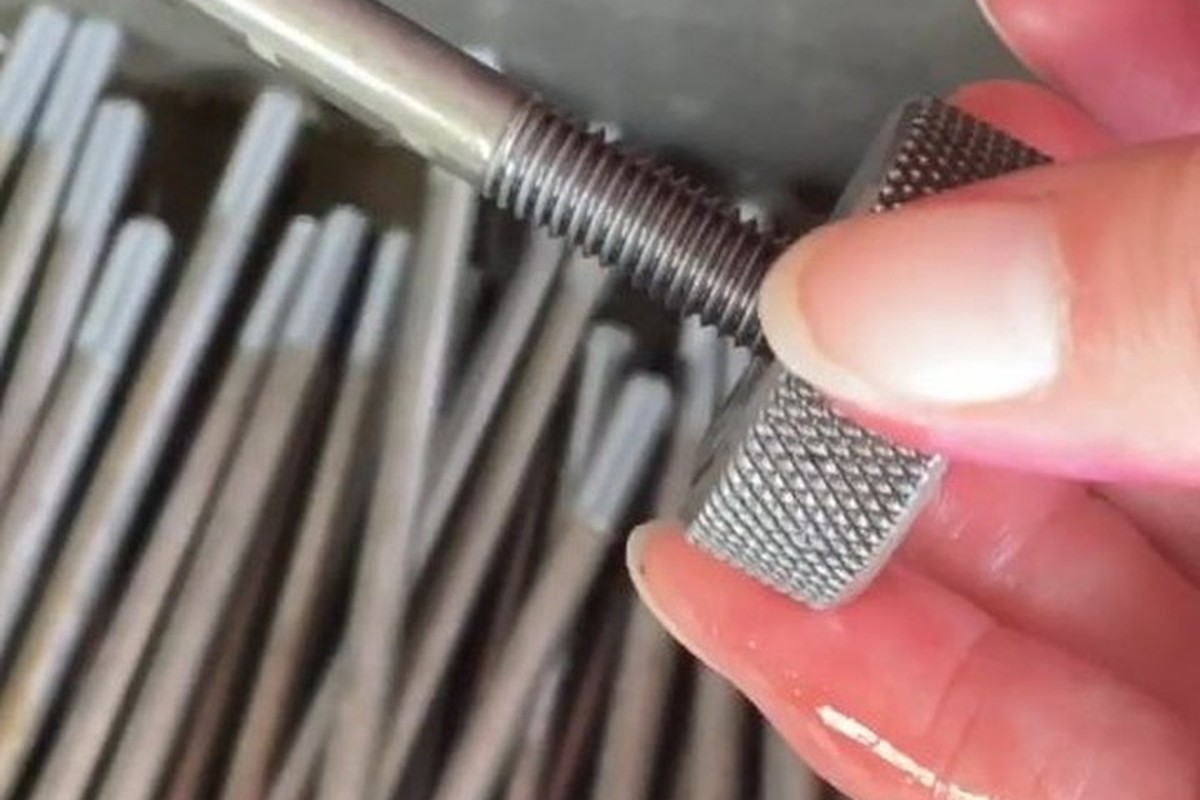
Thread gauged per batch |
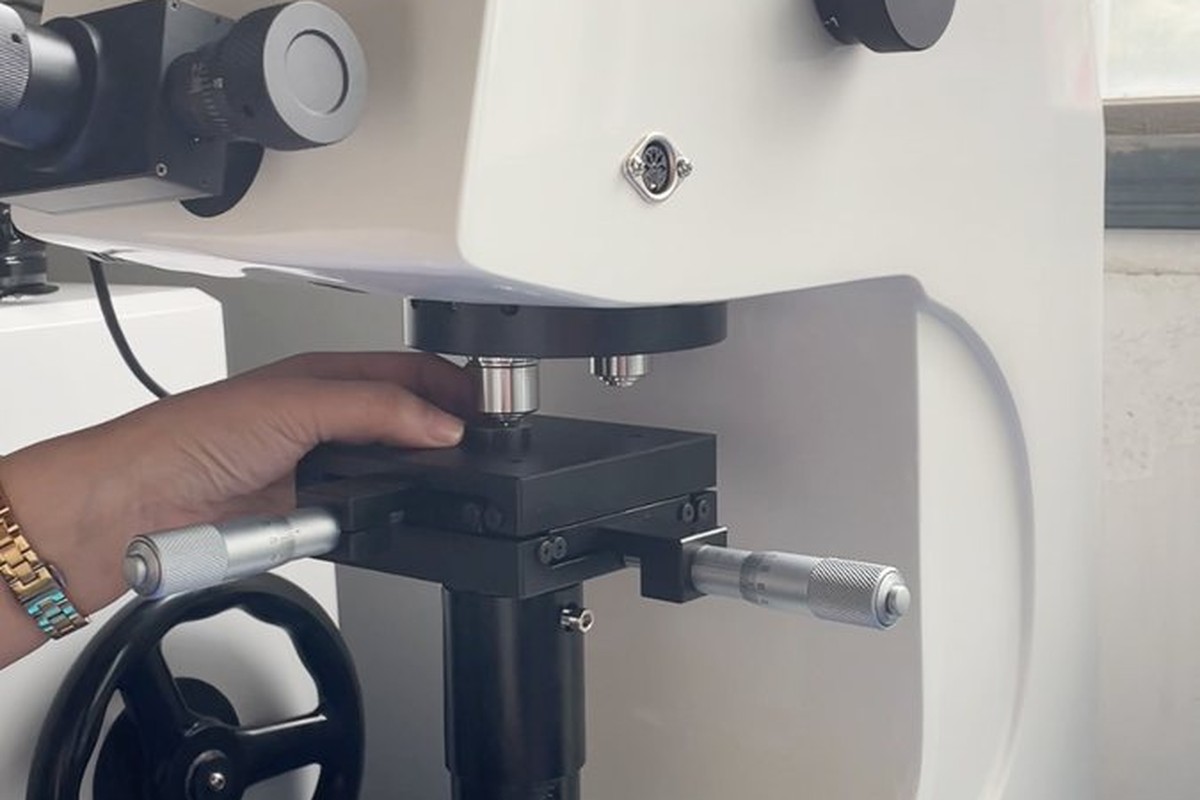
Hardness checked on the bar |
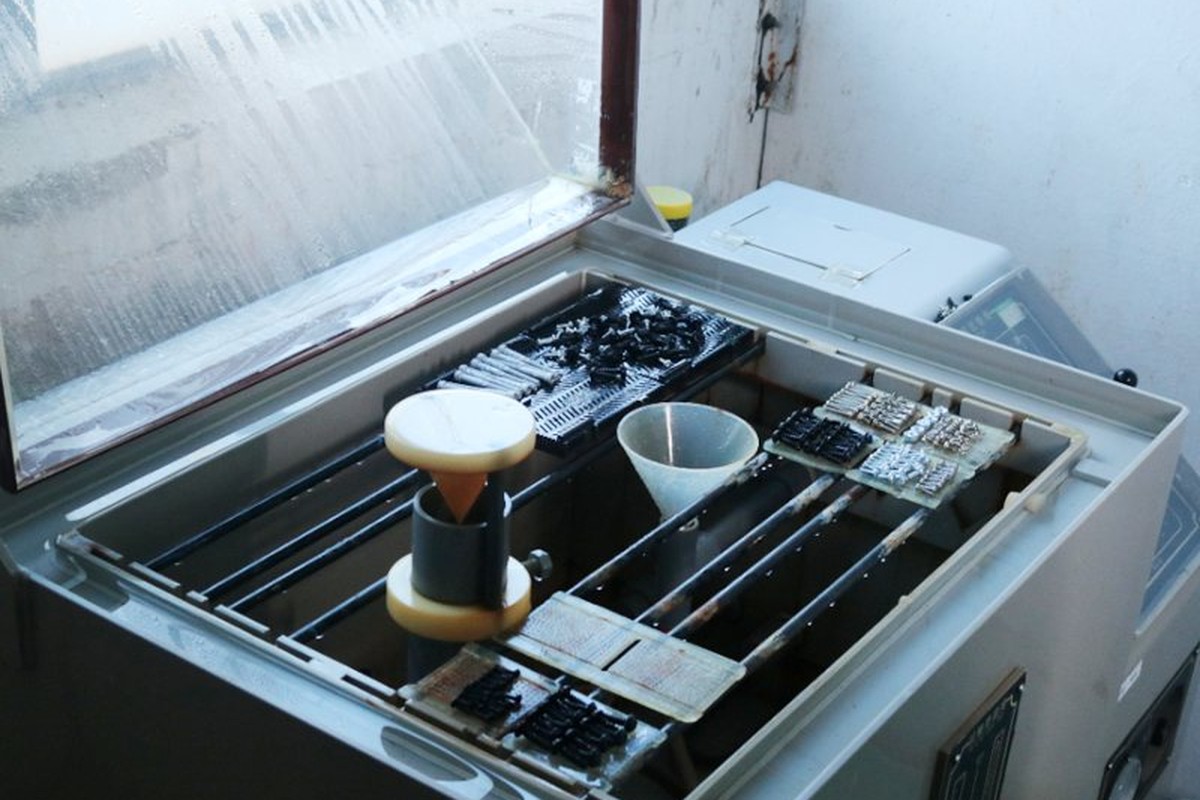
Salt-spray testing of the grade |
The knurl is checked for pitch, depth and crest condition under magnification, the head for diameter and height, and the shoulder for diameter and length. The thread is gauged per batch, and the finish is checked for whether passivation has rounded the crests.
The first article is turned by hand in its joint. That is the only test that shows whether the knurl grips, and it is quick enough to run on every batch instead of only on the first.
Every shipment of shoulder thumb screws is traceable to the bar it was made from and to the passivation batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.
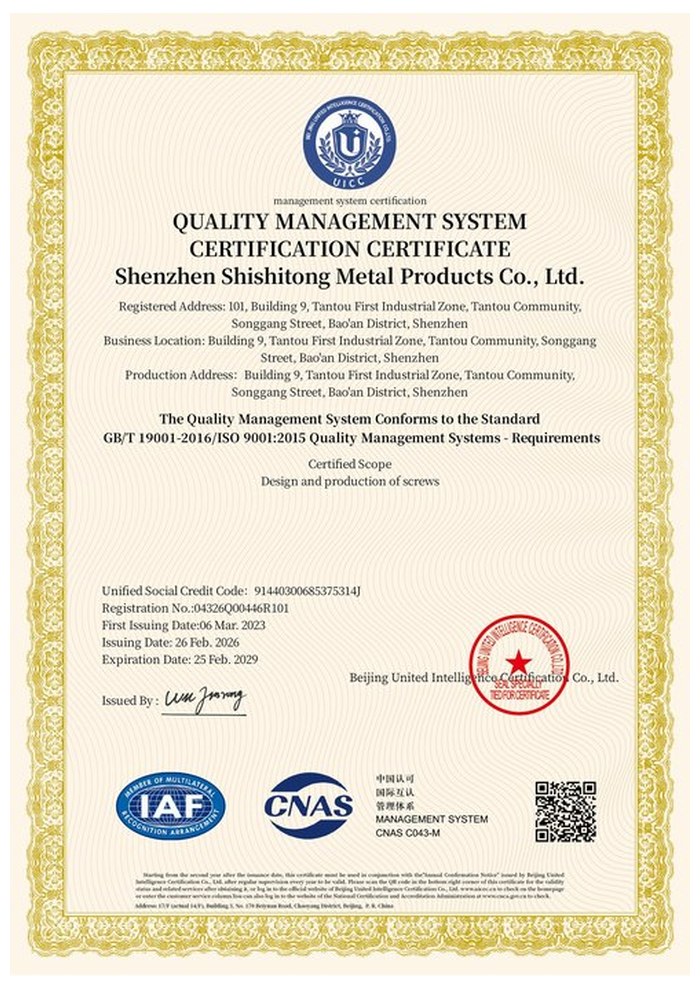
ISO 9001:2015 |
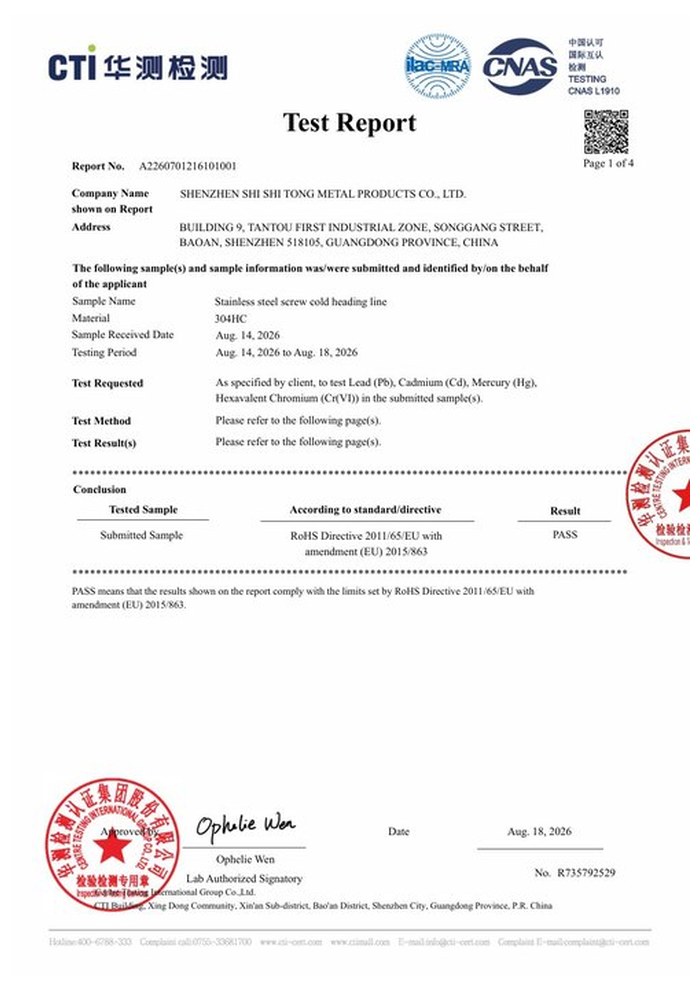
RoHS test report |
Registered trademark |
Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the grade. The documents carry the drawing revision and the batch number, so a repeat order keeps the same knurl and shoulder tolerance.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a shoulder thumb screw the first article is fitted and turned by hand, because the grip is the function. Buyers visit during the process to review samples and to see how the parts are turned.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the lathes and the passivation line can be seen on the day the parts run.
Customer group visit – sample review |
Customer group visit – process discussion |
Customer group visit – factory tour |
Customer visit – project kick-off |
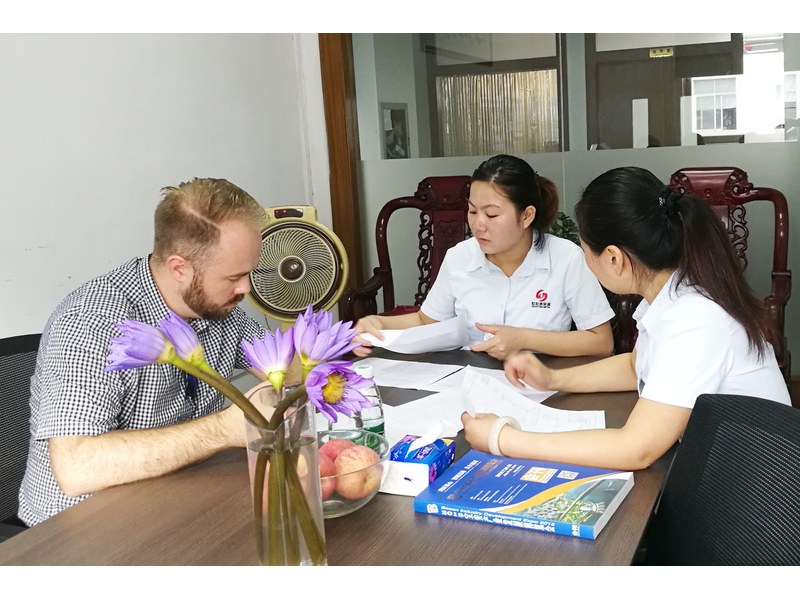
Danish customer – drawing review |
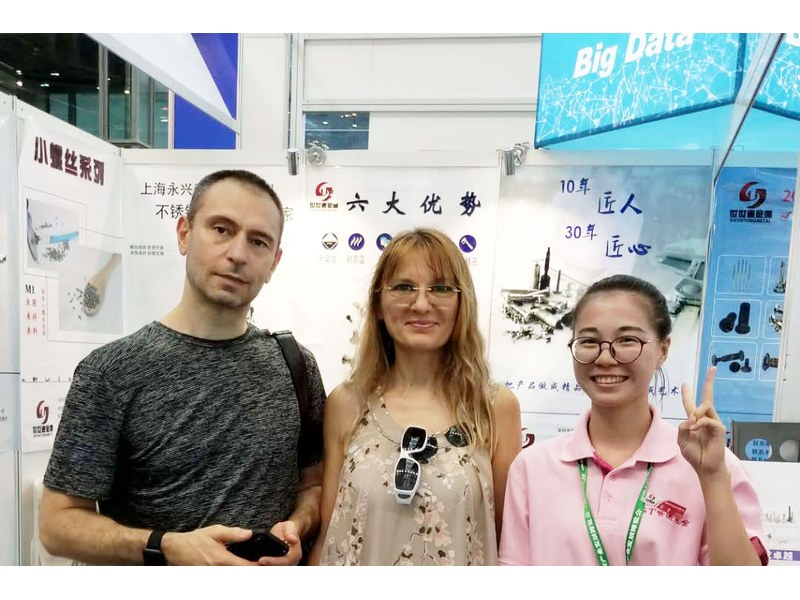
Industry exhibition – meeting customers |
No. The knurled head is the drive, and the part is turned by hand.
Only what a hand can give through the knurl. The joint should be held by fit and by preload set by hand, not by a torque figure.
It machines cleanly and takes a sharp knurl. 304 and 316 tear at the crest and need more finishing.
The knurl. A worn tool leaves shallow crests that look right and stop biting.
Shoulder length for the bearing, and thread length from the shoulder end.
Head diameter and height, knurl pitch and depth, shoulder diameter and length, thread and the grade.
How a shoulder thumb screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the part it adjusts
|
→ |
2
Knurl, head and shoulder agreed
|
→ |
3
First article fitted and turned by hand
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the head diameter and height, knurl pitch and depth, shoulder diameter and length, thread and the grade.
|
Head diameter
|
Head height
|
Knurl pitch
|
|
Shoulder diameter
|
Shoulder length
|
Thread
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.
 +86 13143444311
 sst@szsst88.com