Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
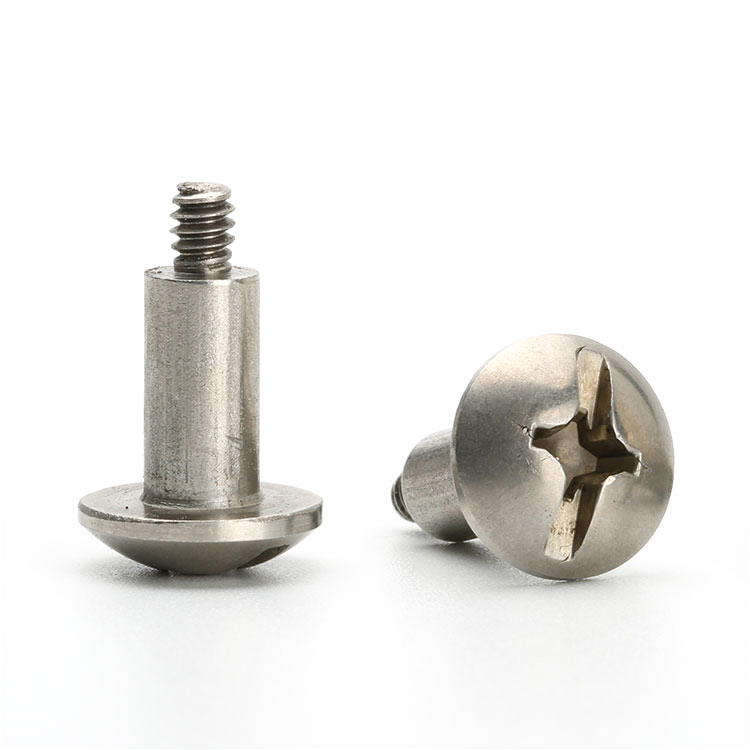
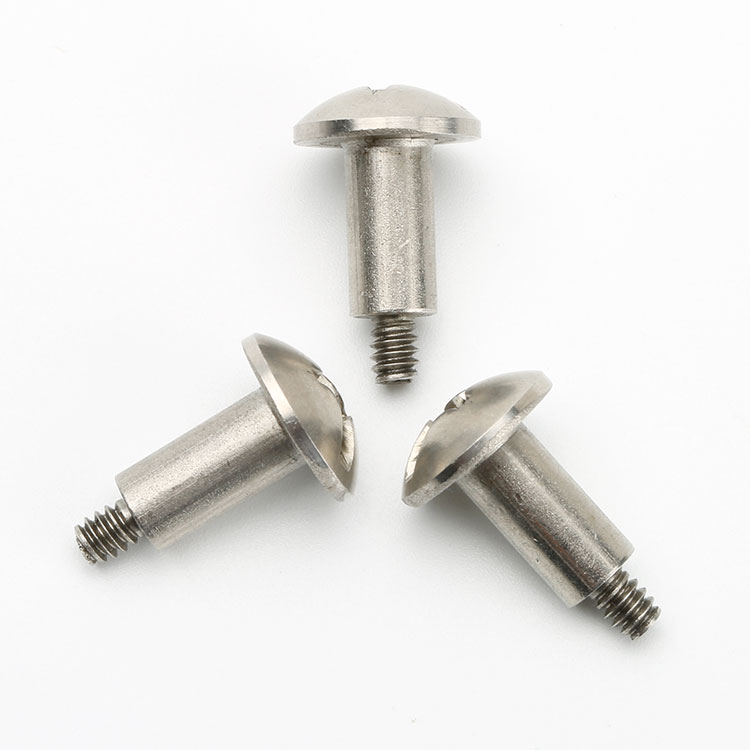
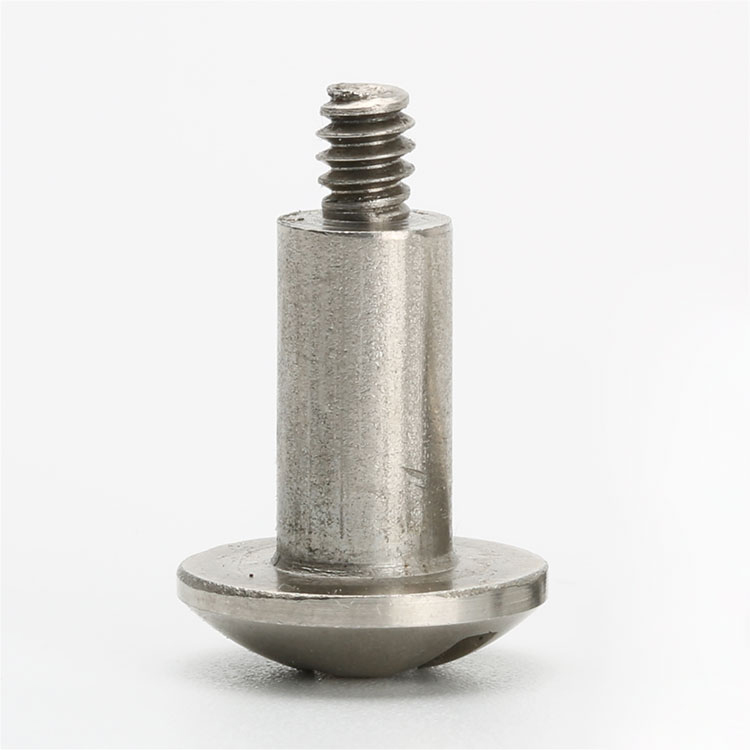
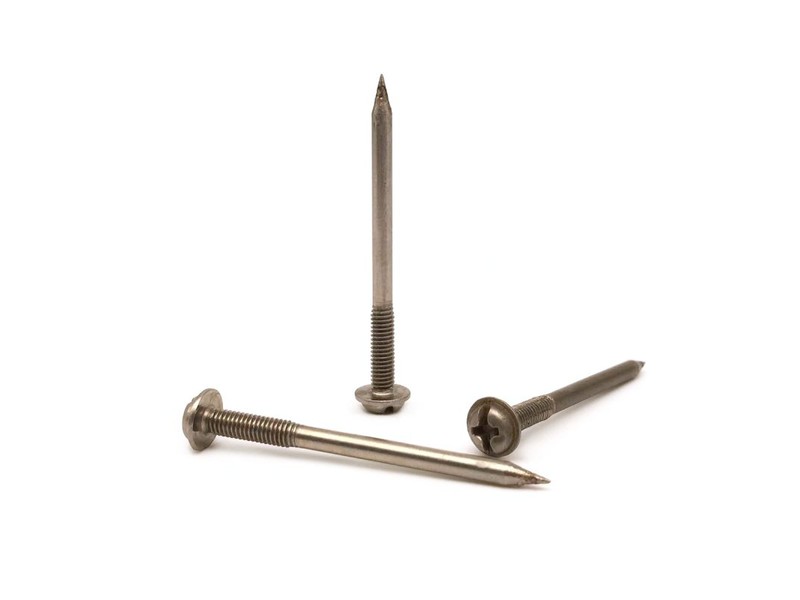
Type:Truss Head Shoulder Screw Stainless Steel
Materials:Stainless Steel
Surface treatment:Plain
Head Type:Truss Head
Drive:Phillips and slot (combined)
Thread:Machine thread
Point:Blunt
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:590
We make truss head shoulder screws in passivated A2 stainless with a wide low head, a combined Phillips and slot drive, a plain shoulder and a machine thread, quoting them from M1 to M14. Head diameter, both recess depths, shoulder tolerance and thread come from your drawing.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A truss head shoulder screw is a stainless fastener with a wide, shallow head, a combined Phillips and slot drive, a plain shoulder and a machine thread, quoted here from M1 to M14 with Number 590. The truss head has the largest bearing diameter and the lowest height of the standard head forms, so it spreads the clamp load over more area than a pan head while standing only a little above the surface.
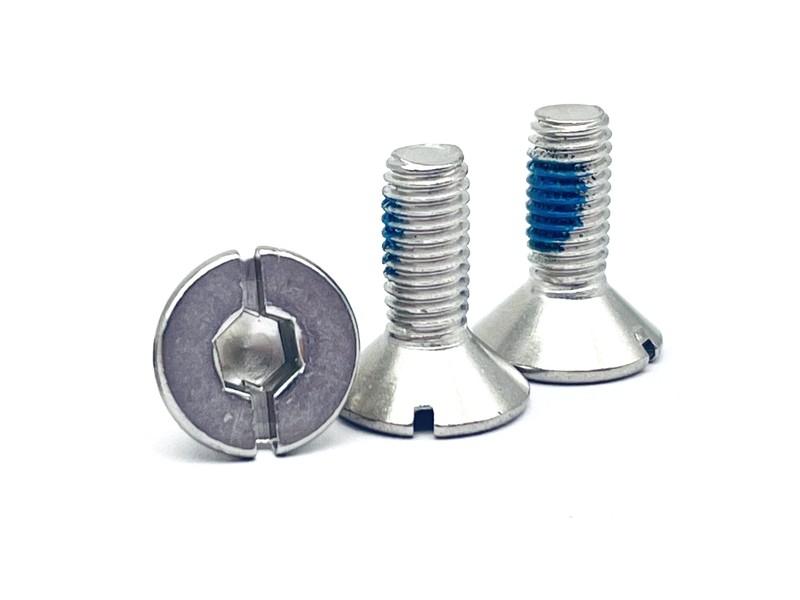
Truss head. A broad, low head with a thin edge, made to spread load on thin or soft material without a washer.
Phillips and slot. A cross and a straight slot cut into the same face, so the screw can be driven with a bit or a blade.
Shoulder. A plain section that runs in a bore and carries the radial load of the joint.
Passivated stainless. A2 grade, uncoated, so the head, both recesses and the shoulder are as made.
A truss head is defined by its ratio: wide relative to its height, with a thin rim that curves down to a flat bearing face. That shape is chosen for one reason — to spread a clamp load over as much area as possible on material that would otherwise be marked or dimpled. On a thin panel or a moulded cover, a truss head is the difference between a tight screw and a dished hole.
The thin rim is also the head’s weakness. Because the head has little height, it flexes if the surface under it is not flat. A truss head tightened onto a rough casting bends at the rim, and the bearing area that was supposed to spread the load is partly lost; the screw still looks seated and the panel is still marked.
The drive is a compromise forced by the head height. A truss head cannot carry a deep cross, so these screws often have a combined Phillips and slot recess: the cross for a driver and the slot for a blade, both cut shallow. The two recesses share a few tenths of a millimetre, and the metal between them is thin — the same limitation as any combined drive in a shallow head.
The shoulder below is what the part is really for. Truss head shoulder screws exist where a wide head and a locating journal are needed at once: a cover that must not be marked, sitting on a screw whose shoulder keeps it in line. The head does the spreading, the shoulder does the locating, and the thread only pulls the two together.
Stainless is the natural material for this combination. There is no plating to add to a thin head or to narrow a shallow recess, and the shoulder is left as made, which on a locating journal is exactly what the drawing needs.
The recorded range is M1 to M14, with the small and medium sizes used on instrument covers and thin panels. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For a truss head shoulder screw the quotation carries head diameter and height, both recess depths, shoulder diameter and length, and the thread.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Truss, wide and low | Head diameter, height and rim form |
| Recess | Phillips cross plus slot | Both depths and the metal between |
| Shoulder | Plain bearing section | Diameter, tolerance and length |
| Thread | Machine thread | Pitch, length and gauging |
| Edge | Thin rim | Edge condition and burr |
| Material | A2 stainless | Grade and heat number on the certificate |
| Finish | Passivated | Surface condition and film |
Head diameter is the functional number on a truss head. It is quoted against the panel it bears on, because the point of the head is the area; a truss head supplied one size down no longer spreads the load the drawing intended.
Edge condition matters as much as diameter. A truss head has a thin rim, and a burr or a rolled edge on it will mark the panel it is supposed to protect.
Three features define the part: the wide head, the thin rim and the shallow combined drive. The first spreads the load, the second is the limit on how much the head can take, and the third is what fits inside it.
| Feature | What it gives | What it costs |
|---|---|---|
| Wide head | The largest spread of any standard head | Needs clearance around the hole |
| Thin rim | Low profile on a wide head | Flexes on an uneven seat |
| Combined drive | Bit or blade will turn it | Shallow recesses, thin webs |
| Shoulder | Locates the joint | Fit must be held |
| Passivated A2 | No build on head or recess | Softer than steel; galls dry |
The spreading is the whole reason for the head. On a panel that has no room for a washer, or where a washer would be lost in service, a truss head is a permanent washer formed onto the screw.
The thinness is the reason for the drive compromise. A driver bit in a shallow cross can cam out, so on these parts the torque has to be set to what the recess will take rather than to what the thread could carry.
The recorded finish is passivation with no coating on A2 stainless. On a truss head that is the only sensible finish: the rim is thin enough that a coating’s edge would show, and the recesses are shallow enough that a deposit would change the driver fit.
| Option | How it protects | Effect on head and shoulder | Typical use |
|---|---|---|---|
| A2 stainless, passivated | Passive chromium oxide film | Head and shoulder as made | Instrument covers and panels |
| A4 stainless, passivated | Passive film with molybdenum | Head and shoulder as made | Marine and medical |
| Steel, nickel plated | Hard barrier deposit | Recess narrowed; re-checked | Indoor consumer products |
| Steel, black oxide | Conversion film, oiled | No measurable build | Internal mechanisms |
| Brass, plain | No coating needed | Softer rim; dents easily | Decorative and electrical |
Where the head is visible and the panel is soft, stainless is the better choice than a plated steel: the rim cannot chip, and a chip on a thin rim is exactly what marks a panel.
Where the joint is wet, A4 is the grade to specify. A thin head with a thin rim has very little material to lose to corrosion before the edge goes.
Three assemblies where a truss head shoulder screw is the fixing:
| Where it sits | The screw holds a cover where there is no room for a washer and the panel would dish under a narrower head. |
| When it goes wrong | The panel dimples anyway, because the head is bearing on a rough or uneven face. |
| Why it happens | The panel is thin, the head is wide, and the seat is not machined. |
| What we control | Head diameter and rim condition checked; first article fitted on the panel. |
| Where it sits | The screw fixes a faceplate where the head must be wide enough to spread load and low enough not to stand out. |
| When it goes wrong | A shallow recess rounds, and a thin rim marks the plate when the bit slips. |
| Why it happens | The joint is visible, the plate is coated, and the head is driven by hand. |
| What we control | Both recess depths checked; first article driven with a driver and a blade. |
| Where it sits | The screw locates a part on a moulded boss where a wide bearing face is the only way to avoid crushing the material. |
| When it goes wrong | The boss crushes, because even a truss head cannot spread a load beyond its diameter. |
| Why it happens | The part is soft, the boss is small, and the clamp is light. |
| What we control | Head diameter matched to the boss; torque agreed with the customer. |
Four reasons that matter on a wide thin head, each tied to what the drawing has to prove:
|
Head diameter and depth agreed
Head diameter, rim form, both recess depths and the shoulder are agreed as one set, because on a truss head shoulder screw they compete for the same height. Basis: Head and recess depths agreed. |
Formed, recessed, passivated in one route
The wide head is formed, both recesses are cut, the shoulder is sized and the thread rolled within one route before passivation. Basis: One route from wire to passivated screw. |
|
Rim checked for burr
The rim is checked for burr and for edge condition under magnification, because a thin rim is what marks the panel it protects. Basis: Rim checked for burr. |
Head form recorded
The head diameter and rim form are recorded from the first article, so a repeat order spreads the load the same way. Basis: Head form recorded. |
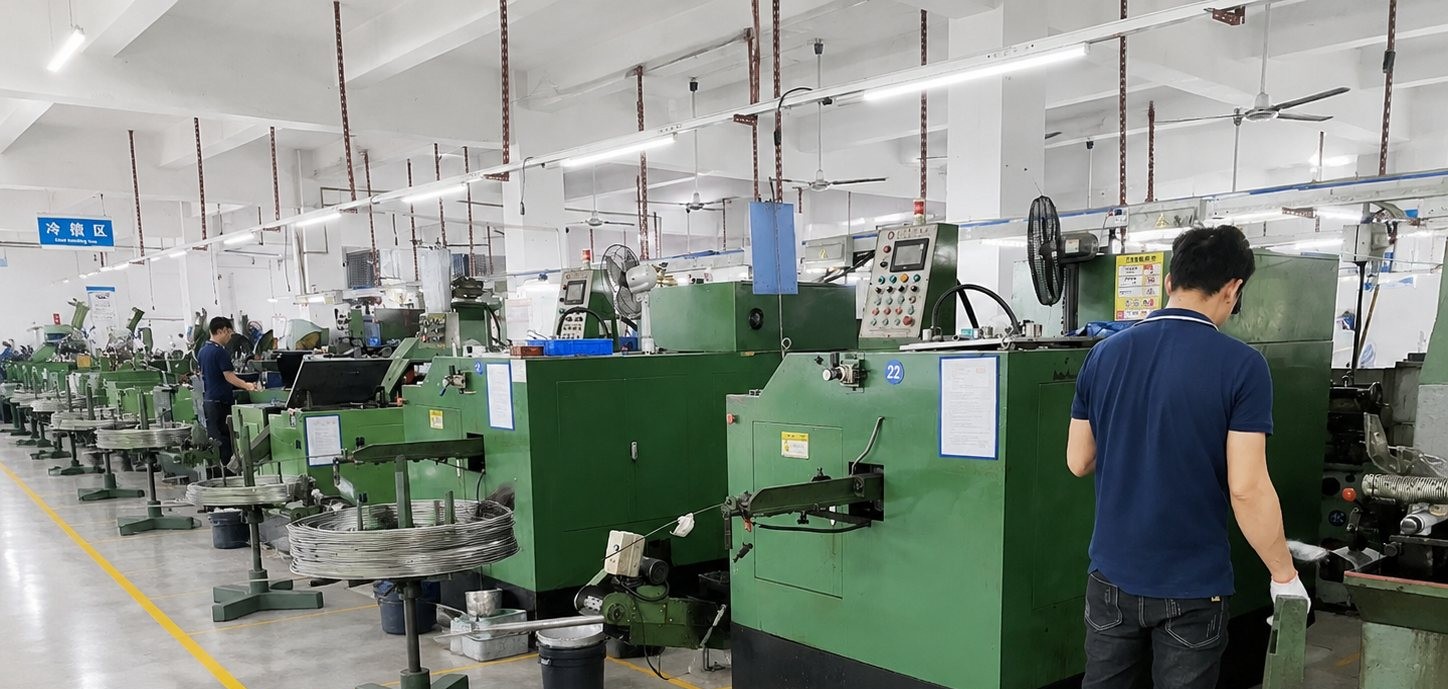
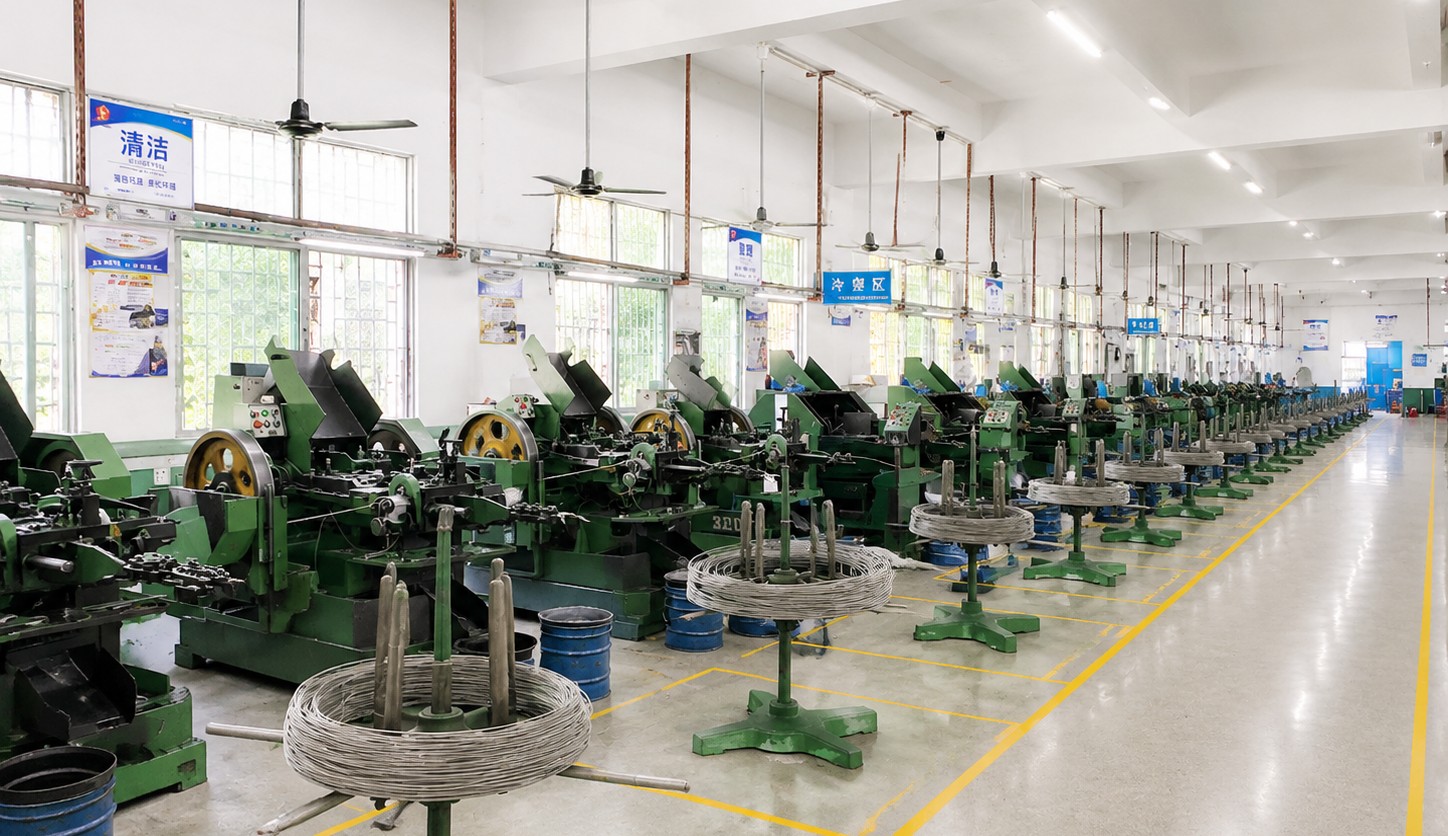
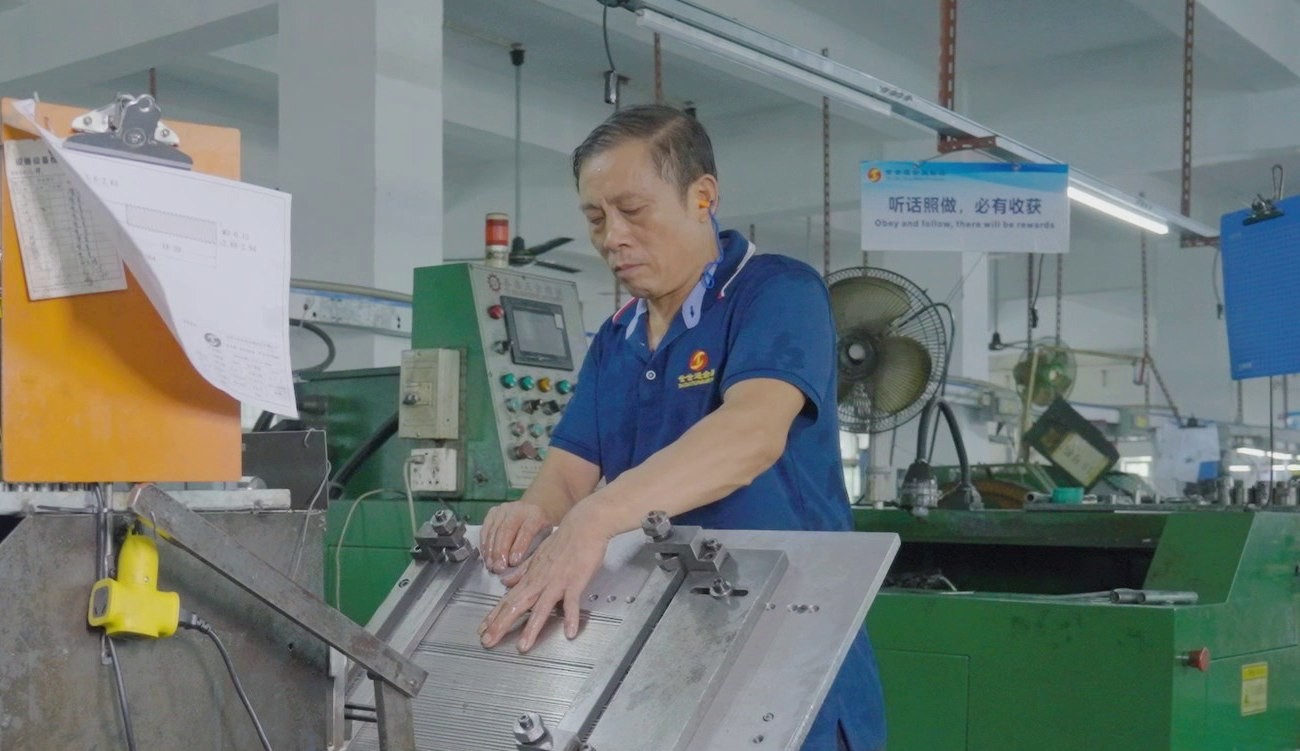
Shi Shi Tong forms truss head shoulder screws on single-die headers that upset the wide head and cut the combined Phillips and slot recess, then size the shoulder and roll the machine thread before passivating the parts. The first part of every run is measured on head diameter, head height, both recess depths, shoulder diameter and length before the batch continues.
|
|
Forming a thin, wide rim is the hardest part of a truss head. The metal has to be pushed outward to the diameter without tearing at the edge, and the rim that results is a fraction of a millimetre thick; a punch that is slightly worn leaves a rim that is thick on one side and thin on the other, and the head flexes unevenly.
What decides whether truss head shoulder screws pass is the head diameter and height, the rim, both recesses, the shoulder and the thread. The inspection agreement covers those, and the criteria come from the drawing.
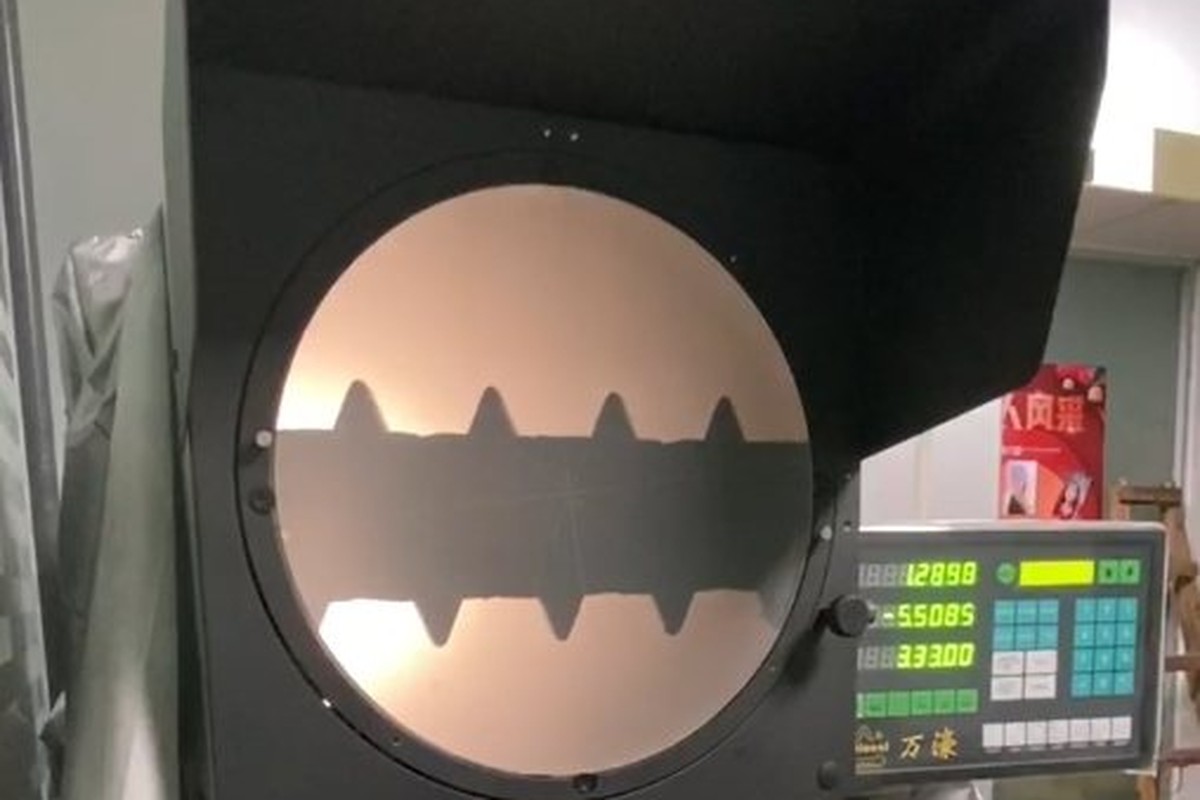
Head and rim on the projector |
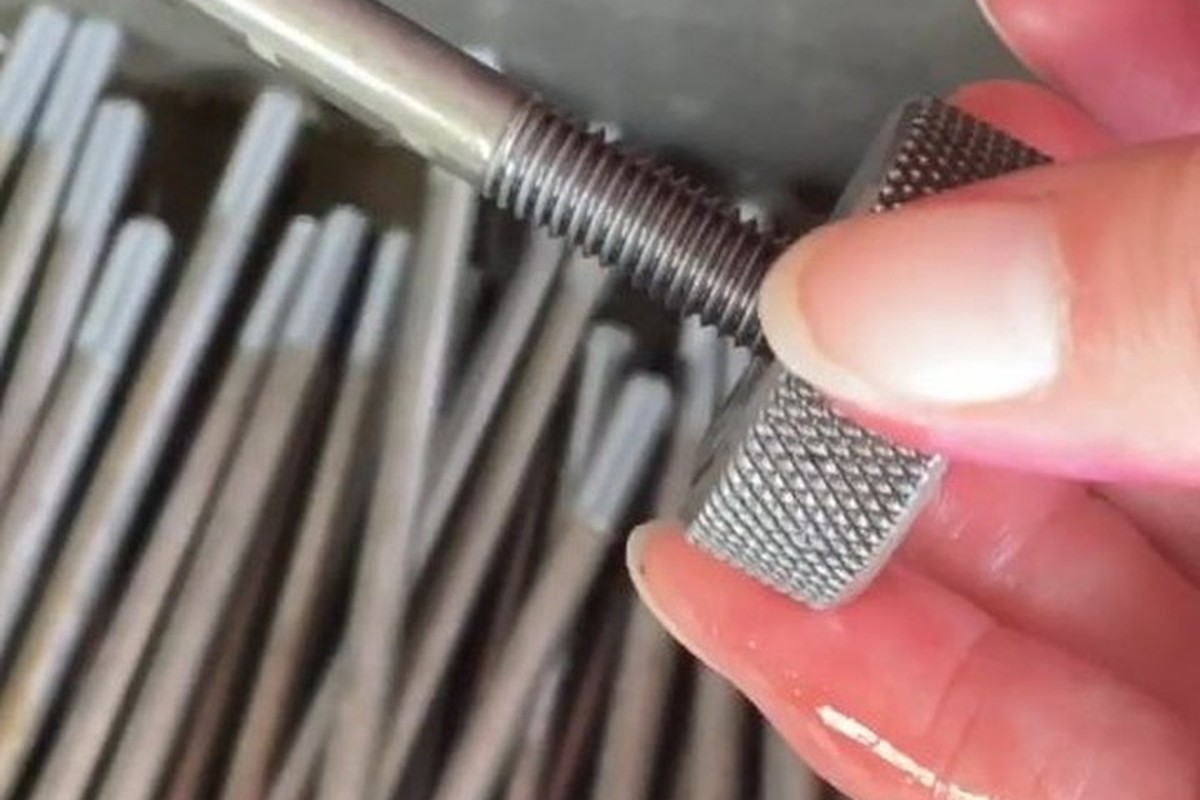
Thread gauged per batch |
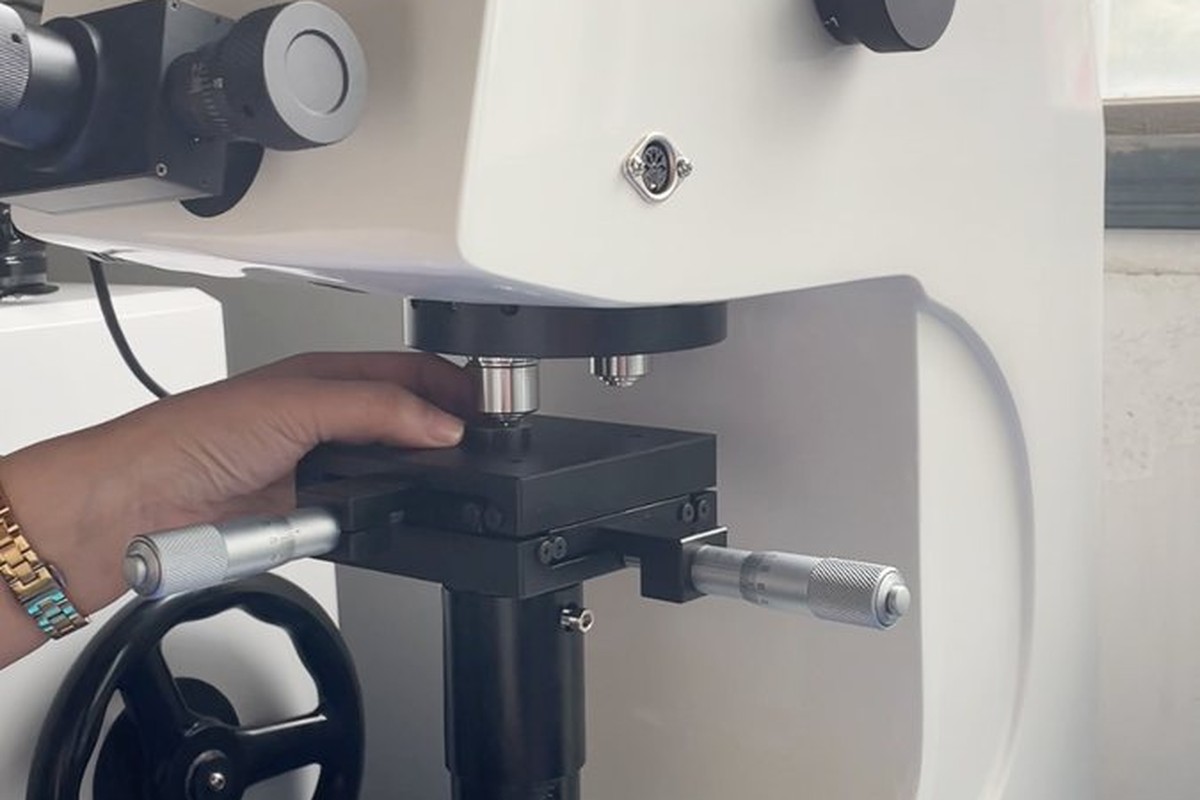
Hardness checked on the wire |
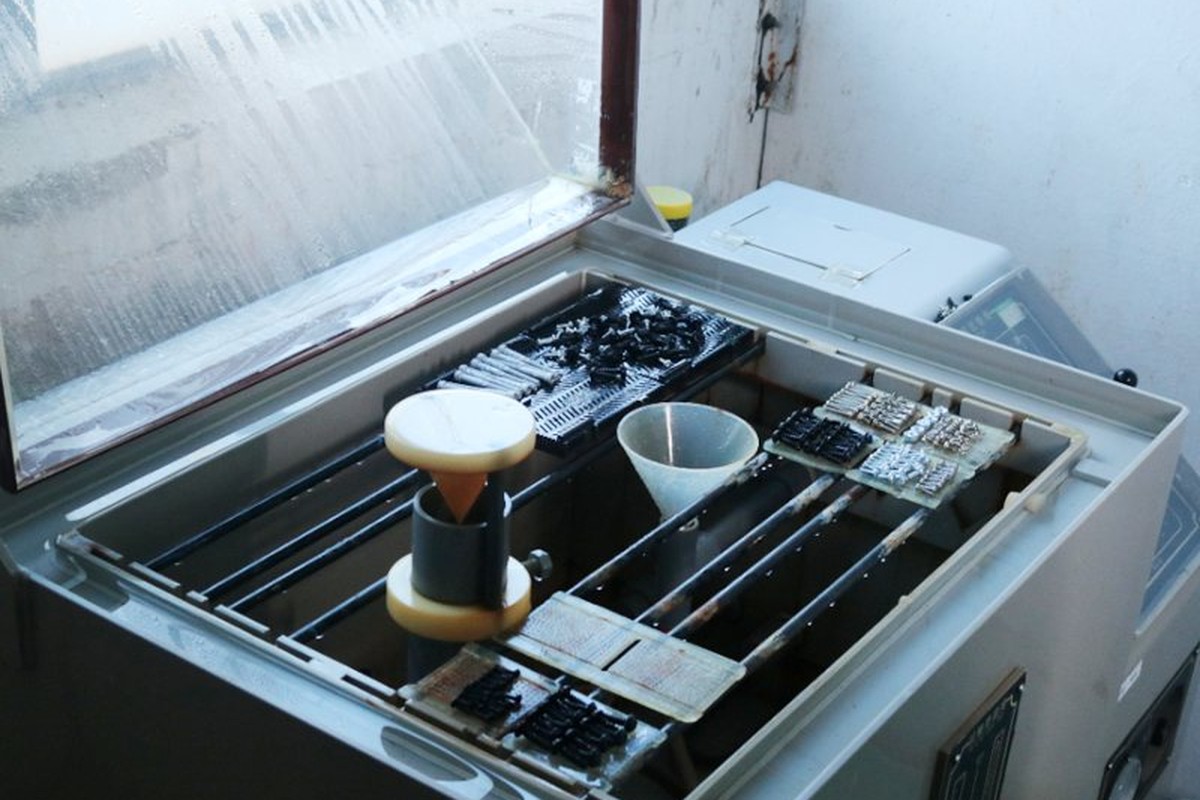
Salt-spray testing of the grade |
The head is measured for diameter and height, the rim for thickness and for burr, and both recesses for width and depth. The shoulder is measured for diameter and length, and the thread is gauged per batch.
The first article is seated on the customer panel and checked for whether the rim sits flat. A truss head that is slightly domed at the rim will mark a soft panel even when the head measures correctly.
Every shipment of truss head shoulder screws is traceable to the wire it was made from and to the passivation batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.
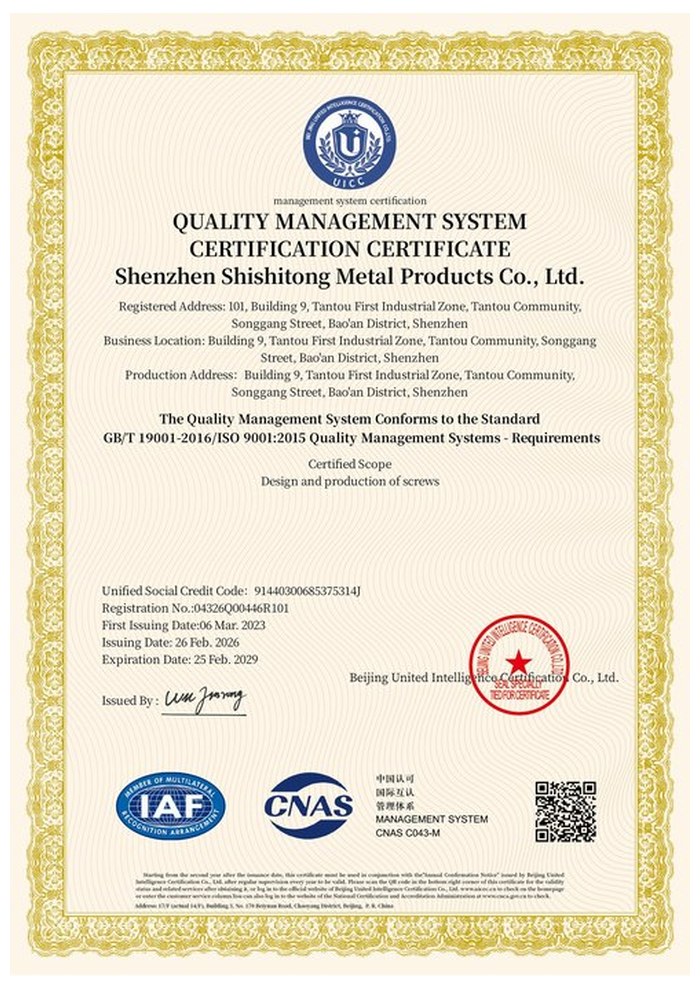
ISO 9001:2015 |
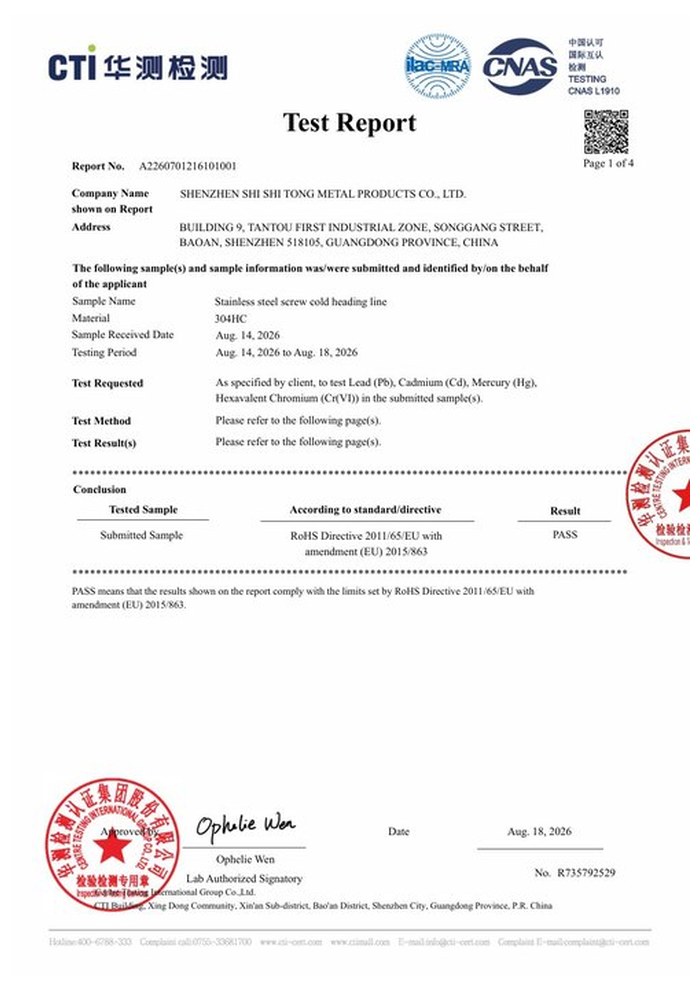
RoHS test report |
Registered trademark |
Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the grade. The documents carry the drawing revision and the batch number, so a repeat order keeps the same head diameter and shoulder tolerance.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a truss head shoulder screw the first article is fitted on the customer panel, because the spread of the head is the function. Buyers visit during the process to review samples and to see how the heads are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the passivation line can be seen on the day the parts run.
Customer group visit – sample review |
Customer group visit – process discussion |
Customer group visit – factory tour |
Customer visit – project kick-off |
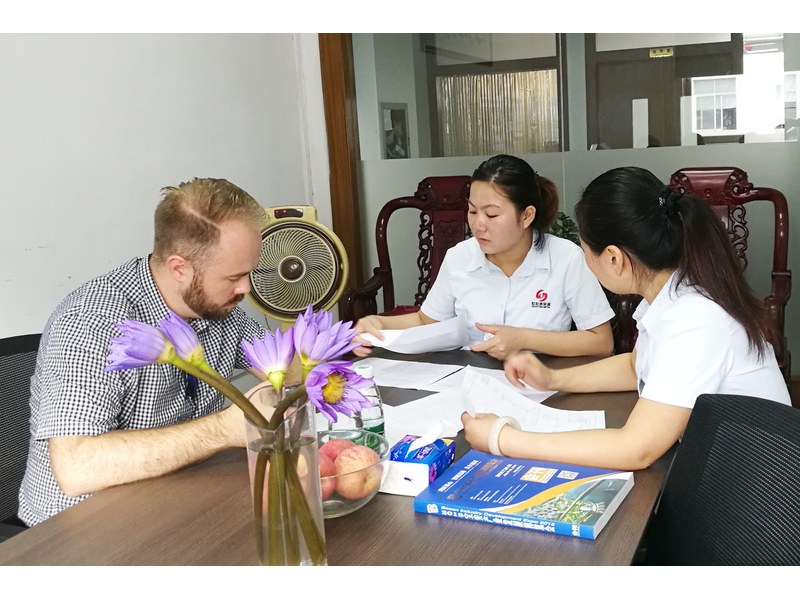
Danish customer – drawing review |
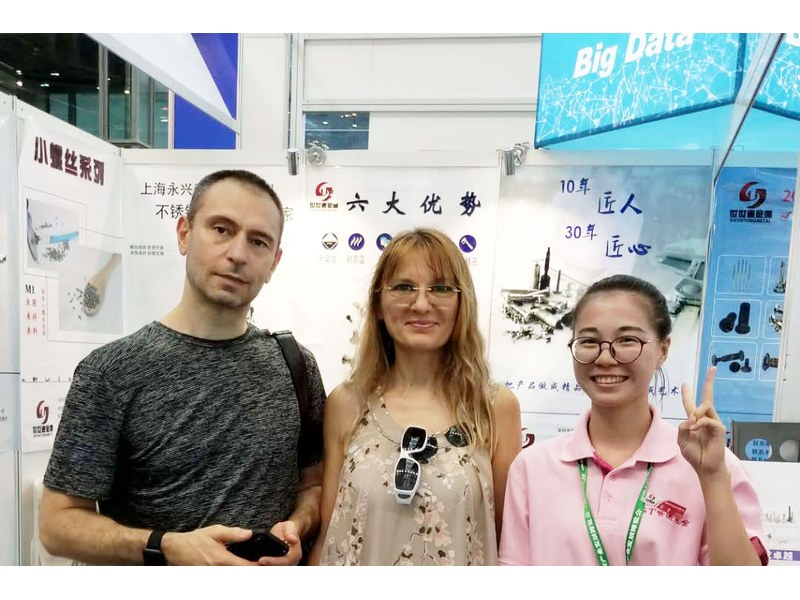
Industry exhibition – meeting customers |
The truss head is wider and lower, so it spreads the same clamp over more area. On a thin or soft panel that is what stops the hole dishing.
A truss head is too thin for a deep cross, so a slot is added as well. Either a bit or a blade will turn it.
Yes. The rim is thin and flexes on an uneven seat, so the torque is set to the head and to the panel, not to the thread.
It is checked for thickness and for burr. A burr on a thin rim marks the panel the head is meant to protect.
Shoulder length for the bearing, and thread length from the shoulder end.
Head diameter and height, rim form, both recess sizes and depths, shoulder diameter and length, thread and the grade.
How a truss head shoulder screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the panel it bears on
|
→ |
2
Head, recesses and shoulder agreed
|
→ |
3
First article fitted on your panel
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the head diameter and height, rim form, both recess sizes and depths, shoulder diameter and length, and the thread.
|
Head diameter
|
Head height
|
Recess depths
|
|
Shoulder diameter
|
Shoulder length
|
Thread
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.
 +86 13143444311
 sst@szsst88.com