Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
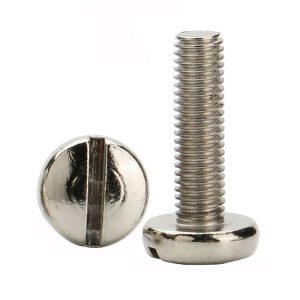
Type:Cheese Head Machine Screw
Materials:Steel, Brass
Surface treatment:Plain, White Zinc Plated
Head Type:Cheese Head
Drive:Slotted
Thread:Machine Thread
Point:Rounded End
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:443-1
We make cheese head machine screws in carbon steel with white zinc or copper finish, and in brass, with a single slot and a rounded end, quoting them from M1 to M14. Slot width, head height, thread and end form come from your drawing, and the first article is driven with your own blade.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A cheese head machine screw has a cylindrical head with a slightly domed top and a straight wall, taller than a pan head and flatter on top, driven by a single slot. The form is one of the oldest in the catalogue: it is the screw that a flat blade was designed for. This family is quoted from M1 to M14 with Number 443-1 in carbon steel with a white zinc or copper finish, and in brass, with a machine thread and a rounded end.
Cheese head. A cylinder with a domed top face, a straight wall and a flat bearing face underneath. The height gives the slot depth.
Single slot. One straight slot across the whole head. A flat blade sits in it and turns the screw.
Machine thread. A rolled thread for a tapped hole or a nut.
Rounded end. A rounded, chamfered point that will not cut into anything it passes on the way to its thread.
A cheese head machine screw is defined less by its head than by its drive. A slot is a single cut across the entire diameter of the head, so the drive is as wide as the screw and takes torque on two straight walls. That gives it an advantage and a weakness at once: the blade can apply more torque than a cross bit of the same size, and it can slide sideways out of the slot without warning.
The geometry of a cheese head machine screw exists to make the slot work. The head is tall enough for a slot with real depth, the top is domed so that a blade dropped on it finds the slot, and the wall is straight so the blade can be seen from the side while it is being driven. On a lower head the same slot would be shallow and would open up at the ends under load.
The slot’s failure mode is different from a cross. A cross cams the driver out vertically; a slot lets the blade rotate out of alignment and run across the top of the head, which marks the head and can cut into the wall. That is why slotted screws are driven with the blade held down as well as turned, and why a hand driver with a good blade is kinder to them than a powered one.
The rounded end is a small detail with a practical job. Where the screw passes through a clamped component before engaging its thread — a bush, a link, a hole in a plate — a rounded end slides through without cutting the bore or picking up a burr. A sharp point would start a thread in the wrong place, which on a machine screw means the screw jams before it reaches the nut.
Two materials are offered on this part for a reason that is mostly about appearance and conductivity. White zinc steel is the working version, and copper-finished steel is the decorative one; brass is the version that carries current, does not rust and turns into a clean slot. In each case the geometry is identical, so the choice is made on what the joint has to do rather than on how it is driven.
The recorded range is M1 to M14, covering M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For a cheese head machine screw the quotation carries head diameter, head height, slot width and depth, the thread and the end form, because the slot is the drive and its width is what a blade has to fit.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Cheese head, domed top | Head diameter and height |
| Slot | Single straight slot | Slot width, depth and burr |
| Thread | Machine thread | Pitch and length, gauged per batch |
| End | Rounded, chamfered | End radius and full thread length |
| Finish | White zinc or copper | Deposit thickness and adhesion |
| Length | Under the head | Measured on the shop plate |
Slot width is worth a number on the drawing even though a blade will fit almost anything. A slot that is too narrow binds the blade and lifts a burr at the edge; one that is too wide lets the blade rock, which rounds the slot floor and marks the head. The blade width matters as much as the slot, and both should be fixed together.
Head height has to support the slot. On a cheese head the two are linked: a taller head allows a deeper slot, and a deeper slot spreads the load over more of the blade. Where the head is reduced for clearance, the slot depth comes down with it, and the screw becomes harder to drive without damage.
Three features define this part: the slot, the tall head and the material choice. The first carries the torque, the second gives the slot somewhere to live, and the third is where the appearance and the conductivity are decided.
| Feature | What it gives | What it costs |
|---|---|---|
| Single slot | High torque from a flat blade | Blade can slide sideways |
| Tall cheese head | Deep slot, easy to see | Stands proud of the panel |
| Straight wall | Blade can be watched while driving | Nothing to stop over-drive |
| Rounded end | Passes a bore without cutting | Not suitable for self-tapping holes |
| Steel or brass | Cost or conductivity and finish | Two routes to keep separate |
The torque the slot takes is the reason cheese head machine screws have survived. A flat blade in a straight slot has a long contact length, so the load per unit area is low and the head can be tightened hard for its size. What it does not have is any self-limiting behaviour: the screw will keep taking torque until the head or the thread gives way, with no slip to warn the operator.
The two materials behave differently at the slot. White zinc steel holds its edge and takes torque until the driver slips; brass cuts a cleaner slot, turns more smoothly and looks better, but is softer and marks more easily. Where the screw is on show, brass is the traditional answer; where it is structural, steel is.
The recorded finishes are white zinc and copper on steel, and plain brass. Each is applied to the same geometry, so the slot and the thread are the same part in every version; only the surface changes, and with it the way the head looks and the way it survives moisture.
| Option | How it protects | Effect on slot and head | Typical use |
|---|---|---|---|
| Steel, white zinc | Sacrificial zinc | A few microns; slot re-checked | Indoor assembly and panels |
| Steel, copper finish | Decorative plate over steel | Thin; warm tone | Visible decorative fixings |
| Brass, plain | Alloy resists corrosion | Clean slot; softer metal | Electrical and instrument work |
| Stainless, plain | Passive chromium oxide film | Slot as cut | Damp and outdoor joints |
| Steel, black oxide | Conversion film, oiled | No measurable build | Internal mechanisms |
On a cheese head machine screw the white zinc version is the working finish and the one most slotted screws are bought in. The copper finish is there for appearance: it gives a warm tone on a decorative panel without the cost of brass, and it is a plate rather than a solid metal, so it should not be expected to last outdoors.
Brass is the one version that is the material all the way through. It will not rust, it conducts, it is not magnetic, and its slot stays clean after repeated use. Where the screw is part of an electrical path or a visible fitting on an instrument, that is the version to specify.
Three assemblies where cheese head machine screws are the fixing:
| Where it sits | The screw clamps a wire or a lug in a terminal block where the head is visible, the joint is adjusted with a flat blade and the metal may be in the circuit. |
| When it goes wrong | A soft or plated head deforms at the slot, and a rusted screw seizes in the block. |
| Why it happens | The joint is electrical, it is adjusted periodically, and the head shows. |
| What we control | Slot width and depth checked, alloy confirmed, first article fitted to the block. |
| Where it sits | The screw closes a cover where the fastener is part of the finish and a slotted head reads as traditional hardware. |
| When it goes wrong | An over-driven screw marks the head, and a wide slot lets the blade rock and cut the wall. |
| Why it happens | The fixing is on show, it is driven by hand, and the panel is painted. |
| What we control | Slot width matched to the blade, plating checked for thickness and adhesion. |
| Where it sits | The screw replaces a slotted fastener on equipment built when the slot was the standard drive, where the head form has to match the original. |
| When it goes wrong | A cross or hex head looks wrong on the panel, and a slot that is too wide will not hold a period blade. |
| Why it happens | The part is a replacement, the head form matters, and the tool is a flat blade. |
| What we control | Head and slot compared with the original sample, first article reviewed on the panel. |
Four reasons that matter on a slotted screw, each tied to what the drawing has to prove:
|
Slot width and blade agreed
The slot width and the blade that will be used are confirmed together, because a slot that is right on paper can still bind or rock in the customer’s driver. Basis: Slot width and blade agreed in writing. |
Head, slot and thread in one route
The domed head and the slot are formed in the heading stroke, the thread is rolled and the parts are plated in the same route. Basis: One route from wire to finished screw. |
|
Slot driven with the production blade
The first article is driven with the production blade at the joint torque, because the slot is the drive and a burr at its edge is a reject on a visible screw. Basis: First article driven with the blade. |
First article fixes the setting
The first article fixes the wire, the slot cutter and the plating; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these cheese head machine screws from wire on single-die headers that form the domed head and cut the slot in one stroke, roll the machine thread and form the rounded end, then finish the parts in white zinc, in copper or in plain brass as the drawing specifies. The first part of every run is measured on the head and slot, driven with the production blade and entered into a thread gauge before the batch continues.


|

|
A slot is a simple cut and an unforgiving one: it runs the full width of the head, so the two ends of the slot are open at the wall, and a cutter that is slightly dull tears the edge there. That torn edge is where a blade catches, where plating builds unevenly, and where the head begins to look worn after a couple of assemblies.
What decides whether cheese head machine screws pass is the slot, the head, the thread and the finish. The inspection agreement covers those, and the criteria come from the drawing.

Head and slot on the projector |

Thread gauged per batch |

Hardness checked on the wire |

Salt-spray testing of the plate |
On cheese head machine screws the slot is checked for width, depth and for burrs at its open ends, and then driven with the production blade. The head is checked for diameter and height on the projector, and the rounded end is checked for radius and for the length of full thread — a screw that has thread into the rounded end will not pass a bore cleanly.
The thread is gauged per batch and the finish is checked for thickness and adhesion, with attention to the slot where a deposit changes the fit of the blade. On a brass part the alloy is confirmed on the certificate rather than assumed from the colour.
Every shipment of cheese head machine screws is traceable to the wire it was made from and to the plating batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the plating. Where the order mixes steel and brass parts, each material is packed and recorded separately so the paperwork follows the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a slotted screw the first article is driven with the blade the customer uses, because the slot is the drive. Buyers visit during the process to review samples and to see how the heads and slots are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the plating line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
It takes high torque from a simple blade, it is easy to see while driving, and it matches equipment built when the slot was the standard drive.
The blade slides sideways rather than camming out, so it can mark the head or cut into the wall. A blade of the right width, held down while turning, is what prevents it.
To give the slot depth. A shallow slot opens up at the ends under load and the blade rocks in it.
It passes through a bore without cutting or burring it. A sharp point would start a thread where none is wanted.
Steel for cost and strength, brass for conductivity, appearance and a slot that stays clean. The geometry is the same; the choice is about the joint.
Head diameter and height, slot width and depth, thread size and length, the end form, the material and the finish.
How a cheese head machine screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the blade you use
|
→ |
2
Slot width, head height and thread agreed
|
→ |
3
First article driven with your blade
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the head diameter and height, the slot width and depth, the thread size and length, the end form, the material and the finish.
|
Head diameter
|
Head height
|
Slot width
|
|
Thread size
|
End form
|
Material
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com