Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
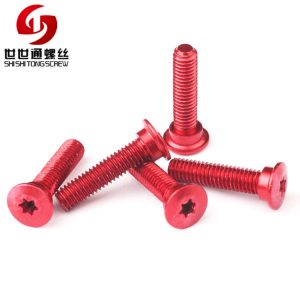
Type:Torx Truss Head Machine Screw
Materials:Carbon Steel
Surface treatment:Plain
Head Type:Truss Head
Drive:Torx Recess
Thread:Machine Thread
Point:Blunt
Forming:Single Die Heading + Serrated Face
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:37
We make torx truss head machine screws in plain carbon steel, a wide head with a ring of teeth under the rim and a six-lobe recess, quoting them from M1 to M14. Tooth depth, torque, recess and thread come from your drawing, and the first article is driven to torque on your own panel.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A torx truss head machine screw is a machine screw with a wide, shallow truss head carrying a ring of small teeth under the rim and a six-lobe star recess on top. The teeth press into the panel and key the head against rotation; the star drive turns the screw without climbing out, so the teeth can be brought to bear. This family is made in plain carbon steel, quoted from M1 to M14 with Number 37 and filed as an anti-slip screw.
Truss head. A wide, shallow dome with a flat bearing face, spreading the clamp load further than any other low head.
Serrated face. A ring of shallow teeth under the rim that bites into the surface when the screw is tightened.
Torx recess. A six-lobe star recess whose bit stays seated under load, so the head can be driven until the teeth bite.
Machine thread. A rolled thread for a tapped hole or a nut, ending in a blunt chamfer.
A serrated head is a mechanical lock, and it is only as good as the torque that seats it. The teeth are shallow; they need to be pressed into the surface to key, and that means the screw has to be driven to a real torque without the driver slipping. If the drive cams out early — as a cross recess is designed to do — the teeth never seat, and the part arrives with a locking feature that does nothing.
That is the reason a star recess belongs on this head. A Torx bit holds the recess walls under increasing torque, so the operator can keep turning until the head face meets the panel and the teeth bite. The drive and the lock are a pair: neither is much use without the other on this part.
The truss head does a second job here. Its wide face means the teeth are spread over a large circle rather than concentrated at a small rim, so each tooth carries less load and the panel sees a distributed pattern instead of a ring of dents. On a thin panel that matters, because a concentrated ring of teeth will dent the sheet and the joint loses preload.
The cost is the panel. Every tooth that bites leaves a mark, and the marks are permanent. On a painted or anodised panel a serrated head is a decision to damage the finish at every fixing; on a hidden joint or a bare metal surface it is free. That difference decides where the form can be used, not the torque capability.
The fourth element is the thread. Because the head is locked to the panel, the joint’s resistance to loosening now depends on the thread staying put, which a machine thread in a tapped hole does by friction alone. The teeth stop the head rotating; they do not stop the screw from losing preload through the thread. That is why the form is used with a defined assembly torque rather than an operator’s judgement.
The recorded range is M1 to M14, covering M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For a torx truss head machine screw the quotation carries head diameter, head height, tooth depth and count, recess size and the thread, because the teeth are the function and their depth is limited by the head.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Truss head, wide and shallow | Head diameter and height |
| Teeth | Ring of teeth under the rim | Tooth depth, count and sharpness |
| Recess | Torx, six-lobe star | Recess size and depth |
| Thread | Machine thread | Pitch and length, gauged per batch |
| End | Blunt, chamfered | Chamfer cut, not deburred |
| Finish | Plain carbon steel, oiled | Surface condition and rust prevention |
Tooth depth is the number to argue about. Deeper teeth hold better and mark the panel more; shallow teeth are gentle and rely on the drive to reach the torque that makes them work at all. On a painted panel the shallow version is the sensible one, and on a bare steel or aluminium joint the deeper tooth is worth the marks.
Recess size should be written out rather than implied, because the drive is what makes the lock work. A recess one size small on a small head is harder to drive and more likely to be damaged before the teeth bite; one size large loses head material the truss dome cannot spare.
Three features define this part: the serrated face, the star recess and the wide head. The first is the lock, the second is what lets the lock be engaged, and the third spreads the load and the tooth pattern.
| Feature | What it gives | What it costs |
|---|---|---|
| Serrated face | Mechanical key at the head | Marks paint and soft panels |
| Torx recess | Drive that does not cam out | Exact bit required |
| Wide truss head | Distributed tooth pattern | Thin rim, easily bent |
| Machine thread | Repeatable clamp in a tapped hole | Needs a tapped hole or nut |
| Plain steel | Cost and strength | Rusts if stored damp |
The combination is unusually well matched. A locking head needs torque, a star drive supplies it, and a wide head keeps the result gentle on the panel. Where a designer chooses one of these features it is usually because the others came with it — a serrated head with a cross recess, for example, is a part whose lock cannot be relied on.
The weakness is that none of it is adjustable. Once the teeth have bitten, the joint is at one depth; backing it off leaves a ring of marks and a looser joint. That is acceptable on an assembly that is set once, and a poor choice on one that is adjusted in service.
The recorded finish is plain carbon steel, oiled. A serrated face removes its own coating as it bites, so plating a toothed head is a partial exercise: the teeth scrape through the deposit and expose steel anyway. Plain steel accepts that and relies on the oil film and the assembly environment.
| Option | How it protects | Effect on teeth and head | Typical use |
|---|---|---|---|
| Plain steel, oiled | Oil film only | Teeth as formed | Painted or plated assemblies |
| Black oxide | Conversion film, oiled | No measurable build | Internal mechanisms |
| White zinc | Sacrificial zinc | Zinc protects beside the scraped teeth | Indoor general work |
| Black zinc | Sacrificial zinc, dark | Zinc protects beside the scraped teeth | Dark equipment |
| Stainless, plain | Passive chromium oxide film | Teeth as cut; no plate to lose | Damp and outdoor joints |
Where a coating is used, zinc is the better choice than nickel on a toothed head, because zinc protects sacrificially around the scraped area. A barrier coating on the same part gives no protection at the teeth at all, which is where the damage happens on every assembly.
Stainless is the answer where the joint is exposed, and on this form it has a practical advantage: there is no plate to lose, so the teeth stay as cut and the appearance of the head does not change between the first assembly and the tenth.
Three assemblies where torx truss head machine screws are the fixing:
| Where it sits | The screw clamps a bracket or a plate on equipment that runs continuously, where the head must not work loose between services. |
| When it goes wrong | A plain head rotates under vibration, and a cross recess cannot be driven hard enough to seat a locking face. |
| Why it happens | The joint vibrates, it is assembled once, and the head sits on a hard surface. |
| What we control | Tooth depth and count checked, first article driven to the specified torque. |
| Where it sits | The screw fixes a panel where the material is hard enough to accept the teeth and the fixing is hidden from view. |
| When it goes wrong | Shallow teeth never bite, and over-driving bends the truss rim. |
| Why it happens | The panel is metal, the fixing is not on show, and the joint is set once. |
| What we control | Teeth inspected, first article trialled on the panel material. |
| Where it sits | The screw locates a plate or a bracket where a plain head would allow the part to creep over time. |
| When it goes wrong | A damaged recess leaves a screw that cannot be removed, and a painted chassis shows every tooth mark. |
| Why it happens | The joint is internal, the panel is painted, and the fixing is at a defined torque. |
| What we control | Recess driven with the production bit, tooth depth matched to the finish. |
Four reasons that matter on a toothed locking screw, each tied to what the drawing has to prove:
|
Teeth and torque agreed
The tooth depth and the assembly torque are confirmed together, because a serrated head that is never driven to its torque has no locking effect at all. Basis: Tooth depth and torque agreed in writing. |
Head, teeth and recess in one route
The truss head, the teeth under the rim and the star recess are formed in the heading stroke, and the thread is rolled below. Basis: One route from wire to finished screw. |
|
Driven to the torque, not just measured
The first article is driven to the specified torque with the production bit and then checked for tooth engagement, because that is what the part is for. Basis: First article driven to torque. |
First article fixes the setting
The first article fixes the wire, the tooth die and the recess punch; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these torx truss head machine screws from carbon steel wire on single-die headers that form the wide head, the ring of teeth under the rim and the six-lobe recess in one stroke, then rolls the machine thread to a blunt chamfered end. The first part of every run is measured on the head and teeth, driven with the production bit at the specified torque and entered into a thread gauge before the batch continues.


|

|
The tooth die is the tool that decides the part. The teeth are shallow ribs around the underside of a wide head, and they have to come out sharp and even, because a tooth that is rounded by wear slides instead of biting. A worn tooth die produces a head that looks correct from above and behaves like a plain truss head in service.
What decides whether torx truss head machine screws pass is the teeth, the head, the recess and the thread. The inspection agreement covers those, and the criteria come from the drawing.

Head and teeth on the projector |

Thread gauged per batch |

Hardness checked on the wire |

Salt-spray testing where a finish is used |
The tooth ring is checked for depth, count and evenness on the projector and inspected at magnification for rounded crests. The head is checked for diameter, height and face flatness, and the recess is driven with the production bit at the torque the joint will use.
The thread is gauged per batch, and the first article is driven into a test plate and checked for the tooth marks it leaves — the pattern tells you whether all the teeth engaged or only part of the ring. Where the customer sends a panel sample, the test is done on that panel rather than on a generic plate.
Every shipment of torx truss head machine screws is traceable to the wire it was made from. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the coating. The documents carry the drawing revision and the batch number, so a repeat order is made to the same tooth geometry that was approved.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a locking part the first article is driven to the customer’s torque on their panel, because the tooth engagement is the function. Buyers visit during the process to review samples and to see how the heads and teeth are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
They press into the panel and key the head against rotation, so the joint resists loosening from the head side without a washer or an adhesive.
Because the teeth only work when the screw is driven to a real torque. A star drive stays seated under load, so the head can be brought down until the teeth bite.
Yes. The teeth leave a ring of marks, and on painted or anodised panels that is permanent. Where the face is visible, use a smooth head instead.
Deep enough to key on the panel and shallow enough not to cut it. On soft or painted panels the shallow version is the right choice.
The screw can be, but the marks remain and the second seating is at a different depth. Treat it as a once-set joint.
Head diameter and height, tooth depth and count, Torx recess size, thread size and length, the finish and the assembly torque.
How a torx truss head machine screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the panel it locks against
|
→ |
2
Tooth depth, torque and thread agreed
|
→ |
3
First article driven to torque on your panel
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the head diameter and height, the tooth depth and count, the Torx recess size, the thread size and length, and the assembly torque.
|
Head diameter
|
Head height
|
Tooth depth
|
|
Torx size
|
Thread size
|
Torque
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com