Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
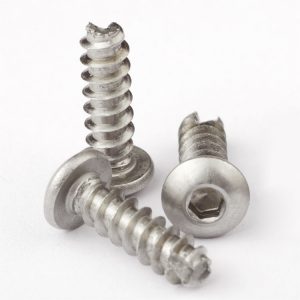
Type:Self Tapping Allen Screws
Materials: Steel
Surface treatment:Zinc Plated
Head Type:Cap Head
Drive:Hexagon socket, Allen key driven
Thread:Coarse single-lead self-tapping thread, rolled with allowance for hot-dip coating
Point:Sharp tapered point; no drill point
Forming:Single-die heading with socket punch, thread rolling, hot-dip galvanizing, sorting
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:432
We manufacture self tapping Allen screws with a cap head, a hexagon socket, a coarse self-tapping thread and a sharp point, in steel with a hot-dip galvanized finish. Thread and socket allowances, head, point and length are taken from your drawing and checked after dipping.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Self tapping Allen screws are screws that cut or form their own thread in a prepared hole, driven with an internal hexagon rather than a cross. The recorded item on this page is steel with a hot-dip galvanized finish, a cap head and a sharp point, quoted from M1 to M14 with Number 432.
Allen drive. A hexagon sunk in the head, driven with a key. The socket takes torque without cam-out, which on a tapping screw matters because the torque peaks while the thread is cutting.
Cap head. A short cylinder with a flat top and a full flat bearing face. It sits in a counterbore and spreads load over the whole head width, and the flat top is where the socket is punched.
Self tapping thread with a sharp point. A coarse thread that forms its own mating thread, with a tapered point that starts in the hole. No nut and no tapped hole are needed.
Hot-dip galvanized. A zinc coating applied by dipping the finished part in molten zinc. It is much thicker than electroplated zinc and far more durable outdoors — and on a small thread it is thick enough to matter, which is what decides how the part is made.
Where it belongs. Outdoor frames, machine guards, agricultural and construction hardware: joints that are made once and then left in the weather, where a thin electroplate would rust through at the first scratch.
The cap head and the hexagon socket are formed in one heading stroke, so the socket stays concentric with the shank. On a tapping screw that concentricity matters: a socket off centre makes the key push the head sideways while the thread is cutting, and the screw goes in at an angle.
The thread is rolled from under the head to the point with a sharp crest, because the crest is what forms the thread in the hole. Rolling work-hardens the flank and leaves a surface that cuts cleanly instead of tearing.
The point is formed after rolling, so it has a clean taper and a lead-in. A point that is blunt skates across a hole instead of entering it, and on a galvanized part the skate takes the zinc off the tip before the screw has done anything.
Then comes the difference from a plated screw. Hot-dip galvanizing leaves a coating measured in tens of microns, and on a small thread that closes the gap between the flanks. Parts for hot-dip are therefore made with a thread allowance — the thread is rolled slightly under size so that the coated part gauges correctly. The socket is affected the same way: a hexagon that measures right before dipping will not take the key afterwards.
The coating is duller and slightly uneven compared with electroplate, and that is normal. What matters is that the thread still takes its mating thread and the key still seats, and both are checked on the dipped part rather than before.
The family is quoted from M1 to M14, with M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14 in the recorded range. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission; self tapping Allen screws run short to medium, because the thread works in a panel or a frame rather than through a stack.
| Item | How it is defined | What we control |
|---|---|---|
| Thread | Coarse self-tapping, rolled with a coating allowance | Gauged after galvanizing |
| Socket | Hexagon, sized with an allowance for the coating | Checked with the key after dipping |
| Head | Cap head, flat top, chamfered edge | Diameter and height on the projector |
| Point | Sharp tapered point | Checked on the first article |
| Length | From under the head to the point | Measured on the shop plate |
| Hole | Set by the thread and the material | Confirmed in a sample of the customer’s part |
The coating allowance is the dimension that is invisible on the drawing and decides whether the part works. A thread rolled to nominal and then hot-dipped will not enter its own tapping hole, because the coating has grown it; a thread rolled under size and gauged after dipping will. That is why the first article is gauged in the galvanized condition.
The socket has the same problem in miniature. A key that fits before dipping will not reach the bottom afterwards, and a key that does not seat will round the hexagon on the first hard turn. The socket is checked with the key the customer uses, on the dipped part.
The combination of an internal hexagon and a cutting thread is chosen where the joint has to be tightened hard and there is no room for a driver to stand off.
| Feature | What it gives | What it costs |
|---|---|---|
| Hexagon socket | High torque, no cam-out, works in a recess | Needs the matching key |
| Cap head | Wide flat bearing face | Taller than a pan or countersunk head |
| Self-tapping thread | Holds without a nut or tapped hole | Hole size is critical |
| Sharp point | Clean start in a prepared hole | Not for undrilled sheet |
| Hot-dip galvanizing | Heavy zinc, durable outdoors | Thick coating; thread and socket allowance needed |
The socket is the reason to choose this over a cross-head tapping screw. A tapping screw spends its travel cutting and the torque peaks during the cut, which is exactly where a cross recess cams out and rounds the head. A hexagon socket sits inside the head, so it also fits where a driver cannot stand off the surface.
The galvanizing is the reason to choose this over a plated screw, and it is a different kind of decision. Hot-dip gives a coating heavy enough to survive long service in weather and abrasion, which an electroplate does not. The cost is that the coating changes the thread and the socket, so the part has to be designed around it rather than plated afterwards.
The recorded finish is hot-dip galvanizing. It is applied by dipping the finished part in molten zinc, which leaves a metallurgically bonded layer measured in tens of microns — far heavier than an electroplate, and the reason this part is specified for outdoor work.
| Finish | How it protects | Effect on thread and socket | Typical use |
|---|---|---|---|
| Hot-dip galvanized | Heavy zinc layer, bonded to the steel | Thick; thread and socket made with allowance | Outdoor frames and hardware |
| White zinc | Sacrificial zinc, blue-white passivation | A few microns; gauged after | Indoor general assembly |
| Dacromet | Zinc-aluminium flake layer, cured | Thin film; thread re-checked | Outdoor and wet assemblies |
| Zinc nickel | Alloy layer, higher corrosion resistance | Thicker; socket re-checked | Industrial and wet service |
| Stainless (equivalent part) | Alloy provides protection | No coating | Wash-down and coastal work |
The rule with hot-dip is that the part is designed for the coating. Thread allowance, socket allowance and a point that stays sharp enough to start are all decided before dipping, because nothing can be corrected afterwards — you cannot machine a galvanized thread without exposing bare steel.
The appearance is duller and slightly grainy compared with electroplate, and that is not a defect. What would be a defect is a thread that does not take its hole or a socket that does not take the key, which is why both are checked on the dipped part rather than on the bare one.
Three assemblies where a socket drive and a heavy zinc coating are both needed:
| Where it sits | The screw fixes a guard, a bracket or a panel to a steel frame that stands outside, where the fixing is tightened with a socket and left in the weather. |
| When it goes wrong | A thin electroplate rusts at the point and the socket within a season, and a cross recess cams out while the thread is cutting. |
| Why it happens | The joint is exposed, it is tightened hard, and it is not opened often. |
| What we control | Thread and socket gauged after dipping, point checked on the first article. |
| Where it sits | The screw holds a plate or a fitting on equipment that is used in mud and rain, with the head in a recess and the key easy to reach. |
| When it goes wrong | A plated screw seizes in the hole after a season, and a socket that filled with zinc will not take the key at all. |
| Why it happens | The joint is dirty, it is serviced, and the fixing is repeated. |
| What we control | Key fit checked on the dipped part, thread gauged per batch. |
| Where it sits | The screw fixes a cover or a bracket into a tapped or formed hole where the head has to sit in a counterbore. |
| When it goes wrong | A head that is too tall fouls the cover, and a shallow socket rounds under torque. |
| Why it happens | The frame is heavy, the joint is tightened hard, and the fixing is serviced. |
| What we control | Socket depth and head height checked on the section, thread gauged. |
Four reasons that matter on a galvanized socket tapping screw, each tied to what the drawing has to prove:
|
Coating allowance reviewed with the thread
The thread size, the socket size and the coating weight are reviewed as one set, so a thread that will not take its hole after dipping is raised before tooling. Basis: Coating allowance reviewed with the thread. |
Head, socket and thread in one route
The cap head and the hexagon socket are formed in one stroke, the thread is rolled with allowance, and the point is formed before dipping. Basis: One route from wire to galvanized screw. |
|
Thread and socket checked after dipping
The thread is gauged in the galvanized condition and the socket is checked with the production key on the dipped part. Basis: First article checked after dipping. |
First article to repeat production
The first article fixes the drawing revision, wire heat, die set, thread roll and coating weight; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these self tapping Allen screws on a single-die header that upsets the cap head and punches the hexagon socket in one stroke, rolls the coarse thread with the allowance the coating needs, and forms the point. The parts are then hot-dip galvanized and sorted. The first part of every run is gauged on the thread and checked with the key in the galvanized condition, and driven into a sample of the material, before the batch continues.


|

|
The dipping step is where a good screw can be ruined. The coating grows the thread and narrows the socket, so the parts are jigged to let the zinc drain out of the recess and the thread is checked afterwards rather than before. A bolt that is perfect before dipping and will not take its hole is the classic failure on this part, and it is caught only by gauging after the coating.
What decides whether self tapping Allen screws pass is the thread, the socket, the head, the point and the coating. The inspection agreement covers those, and the criteria come from the drawing.

Head and socket on the projector |

Thread gauged after dipping |

Hardness testing against the property class |

Salt-spray testing of the galvanized part |
The socket is checked with the key on the galvanized part, at the joint torque. That is the check that catches a socket that has been closed by the coating, and it is also the one that shows whether the zinc has bridged the corners of the hexagon.
The point is checked in the customer’s material. A point that has been rounded by the coating will not enter the hole, and on a galvanized part the damage shows as bare steel at the tip rather than as a mark on the panel.
Every shipment of self tapping Allen screws is traceable to the wire it was made from and to the galvanizing batch. The grade and heat number are recorded on the material certificate supplied with the parts, the coating weight is recorded per batch, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the coating. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a galvanized screw the first article is gauged after dipping and driven into a sample of the material, because the coating changes both the thread and the socket. Buyers visit during the process to review samples and to see how the heads are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header and the galvanizing line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
Self-tapping joints that stand outside or see abrasion, where the fixing is tightened with a socket key and left in place.
A tapping screw cuts for its whole travel and the torque peaks during the cut. A hexagon socket takes that without cam-out, and it fits in a recess where a driver cannot stand off.
The coating is much thicker than an electroplate, so the thread and the socket are made with an allowance and gauged after dipping. A thread rolled to nominal will not take its hole once it is galvanized.
It is checked with the key on the dipped part. Zinc can bridge the corners of the hexagon, and a socket that is tight will round on the first hard turn.
A few times at most. The thread it forms in the hole wears with each removal, and the socket wears with each key.
Thread size, socket size, head diameter and height, point form, length and datum, hole size, coating specification and weight.
How a self tapping Allen screw project runs from drawing to repeat delivery:
|
1
Send the drawing and a material sample
|
→ |
2
Coating allowance review
|
→ |
3
First article gauged after dipping
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size, socket size, head diameter and height, point form, length and datum, hole size, and the coating specification and weight.
|
Thread size
|
Socket size
|
Head diameter and height
|
|
Point form
|
Length and datum
|
Coating weight
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com