Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
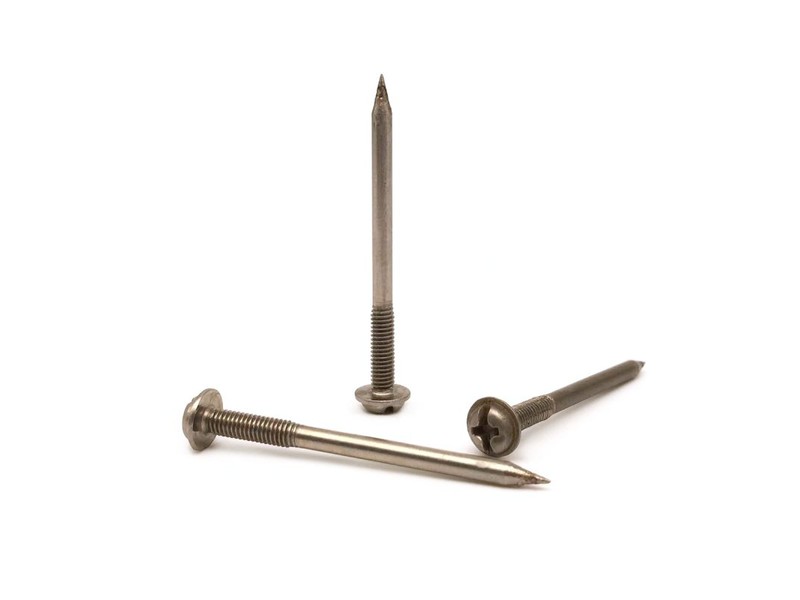
Type:Phillips Head Self Tapping Screws
Materials:Carbon Steel
Surface treatment:White Zinc Plated
Head Type:Pan Head
Drive:Phillips cross recess (PH2 on M4 to M6 sizes)
Thread:Coarse single-lead self-tapping thread, rolled, full to the head bearing face
Point:Sharp gimlet point for wood, board and plastics; drill point for sheet metal on request
Forming:Single-die heading, thread rolling, white zinc plating, sorting
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:520
We manufacture phillips head self tapping screws in the baseline form: a pan head, a coarse self-tapping thread over the full length, a sharp gimlet point and a bright white zinc finish. Head, point, thread and length are taken from your drawing, and the variants in the family are quoted from the same route.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Phillips head self tapping screws are self-tapping screws driven with a cross recess: the thread forms or cuts its own mating thread in a prepared hole, so no nut or tapped hole is needed. The recorded item on this page is the baseline form — a pan head, a coarse thread over the full length, a sharp gimlet point and a bright white zinc finish, in carbon steel, quoted from M1 to M14 with Number 520.
Pan head. A low dome on a flat annular bearing face. It is the default head for general work: enough bearing area for a thin panel, low enough to sit under a cover, and no flange to take up space.
Cross recess. Four tapered wings and a pointed centre. The bit centres itself and the wings cam out before the head tears open, which is why a Phillips screw tolerates a line where the driver torque varies.
Coarse thread, full length. A single-lead thread rolled from under the head to the point. Coarse pitch gives grip in soft materials, and running it the full length means the whole shank below the head engages.
Gimlet point. A sharp taper that starts in the hole and leads the thread in. It suits timber, board and plastics; for sheet metal the hole is drilled first and the point only enters it.
White zinc. A bright blue-white electroplate. It is the standard indoor finish for this family: thin, bright, sacrificial, and it does not fill the recess.
The pan head and the Phillips recess are formed in one heading stroke, which keeps the recess concentric with the shank. On the small sizes the wall between the recess and the outside of the head is only a few tenths of a millimetre, so the recess is formed rather than machined.
The thread is rolled from under the head to the point. Rolling work-hardens the steel and forms a continuous grain through the thread root, and it leaves a flank that cuts or forms the hole wall cleanly instead of tearing it.
The point is formed after rolling, which gives it a clean taper and a lead-in. A gimlet point that is blunt will skate across a hole rather than enter it, and on a thin panel that skate marks the surface before the screw has done anything.
White zinc is applied last, over the head, the recess and the thread. It adds a few microns, so the thread is gauged after plating and the recess is driven with the production bit in the plated condition — the only condition the customer ever sees.
The parts are sorted and packed dry. White zinc holds a thin oil film well and does not need more; heavy oil on a bright zinc part collects dust and makes the recess look dirty on a visible panel.
The family is quoted from M1 to M14, with M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14 in the recorded range. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission; on phillips head self tapping screws the size is chosen from the panel, not from the screw, and the drawing should carry both.
| What to decide | How it is set | What goes wrong if it is not |
|---|---|---|
| Thread size | Panel thickness and load | Too small strips; too large splits thin material |
| Head diameter | About twice the thread; covers the hole | A head that is too small pulls through |
| Length | Panel thickness plus engagement | Too short holds nothing; too long breaks out |
| Point form | Gimlet for wood, board and plastics | A gimlet point on sheet metal wanders |
| Pilot hole | Set by the thread and the material | Wrong hole strips or splits |
| Finish | Indoor: white zinc | Zinc outdoors gives way slowly |
Length is measured from under the head, and with a full thread the usable length is the whole shank. In a blind hole the thread depth has to be at least the length minus the panel thickness; in a through hole the length only has to be long enough to engage, but too long a screw breaks out of a visible face.
The head diameter is the quiet variable. At about twice the thread it covers a normal clearance hole with margin, and on a soft panel it spreads the load enough not to dish. Where the hole is oversized or the material is soft, the next size up or a washer head does the job better than pushing this head.
Phillips head self tapping screws are a family, not a single part: the head, the point and the finish each vary, and the combinations suit different joints. The recorded item on this page is the baseline — pan head, gimlet point, white zinc — and it is worth knowing what the alternatives buy.
| Variant | What it changes | When it is the right choice |
|---|---|---|
| Pan head (recorded) | General bearing area, low profile | Most panel and board joints |
| Washer head | Wider flange, more bearing area | Thin or soft panels, oversized holes |
| Countersunk head | Flush finish | Faces that are seen or slid over |
| Gimlet point (recorded) | Starts in wood, board and plastics | Soft materials with a pilot hole |
| Drill point | Cuts its own hole in sheet | Sheet metal without pre-drilling |
| White zinc (recorded) | Bright, thin, sacrificial | Indoor and general assembly |
The point is the decision that most often goes wrong. A gimlet point on sheet metal will not start, and a drill point on board will split it; the same head and thread can be supplied with either, and the drawing has to say which material the screw is going into rather than leaving it to the default.
The drive is the constant. Every variant in this family takes the same cross bit, which is why the family survives on lines that do not want to stock special drivers — and why a worn bit shows up as a rounded head on the smallest sizes first.
The recorded finish is bright white zinc with a blue-white passivation. It is the baseline finish for steel self-tapping screws: thin enough not to disturb the thread, bright enough to look clean, and sacrificial so a scratch is protected by the zinc around it.
| Finish | How it protects | Effect on thread and recess | Typical use |
|---|---|---|---|
| White zinc | Sacrificial zinc, blue-white passivation | A few microns; gauged after | Indoor general assembly |
| Yellow zinc | Sacrificial zinc, yellow passivation | A few microns; gauged after | Warm-tone indoor hardware |
| Black zinc | Zinc with black passivation | A few microns; recess re-checked | Dark panels |
| Dacromet | Zinc-aluminium flake layer, cured | Thin film; thread re-checked | Outdoor and wet assemblies |
| Stainless (equivalent part) | Alloy provides protection | No coating | Wash-down and coastal work |
White zinc is the right default because it is cheap, bright and doesn’t change the part. It is also the finish that fails first outdoors: the zinc gives way slowly in rain and salt air, and the screw then rusts at the recess and the point, which are the two places where the coating is thinnest.
The step up is Dacromet, which is a flake coating rather than a plated layer and holds up far better in wet service. It is also thicker and duller, so it is specified when the joint is outdoors rather than when the part is on show — and on phillips head self tapping screws the finish should be chosen by the environment, not the other way round.
Three assemblies where the baseline screw does the job without modification:
| Where it sits | The screw fixes a cover, a bracket or a trim to a panel where the material takes a thread and no nut is available behind. |
| When it goes wrong | A screw with the wrong point wanders or splits, and a bright zinc part left outdoors rusts at the recess. |
| Why it happens | The panel is thin or soft, the joint is made from one side, and the assembly is indoor. |
| What we control | Point form and pilot hole confirmed in a material sample, thread gauged after plating. |
| Where it sits | The screw closes a cover or fixes a gland plate where a cross driver is the only tool on the bench. |
| When it goes wrong | A head that is too small pulls through a thin lid, and a screw that is too long breaks into the wiring space. |
| Why it happens | The enclosure is thin, the fixing is small, and the joint is serviced. |
| What we control | Length against panel thickness checked, head diameter against the hole. |
| Where it sits | The screw fixes a bracket, a back panel or a hinge plate into board where the thread forms its own grip. |
| When it goes wrong | A drill point splits the board, and a head without a flange sinks into a soft face. |
| Why it happens | The material is board or MDF, the fixing is hidden or glanced, and the joint is made on a line. |
| What we control | Point checked on a board sample, head diameter checked against the face. |
Four reasons that matter on a baseline screw, each tied to what the drawing has to prove:
|
Material and point reviewed together
The material being fixed, the point form and the pilot hole are reviewed as one set, so a screw that will not start or will split is raised before tooling. Basis: Material, point and hole reviewed as one set. |
Head, thread and point in one route
The pan head and the recess are formed in one stroke, and the thread is rolled to a gimlet point on the same route. Basis: One route from wire to plated screw. |
|
Recess and thread checked after plating
The recess is driven with the production bit and the thread is gauged in the plated condition, because the deposit changes both. Basis: First article checked after plating. |
First article to repeat production
Drawing revision, wire heat, die set, thread roll and plating are set at the first article and kept as the reference for later batches. Basis: First article signed off before the batch is released. |
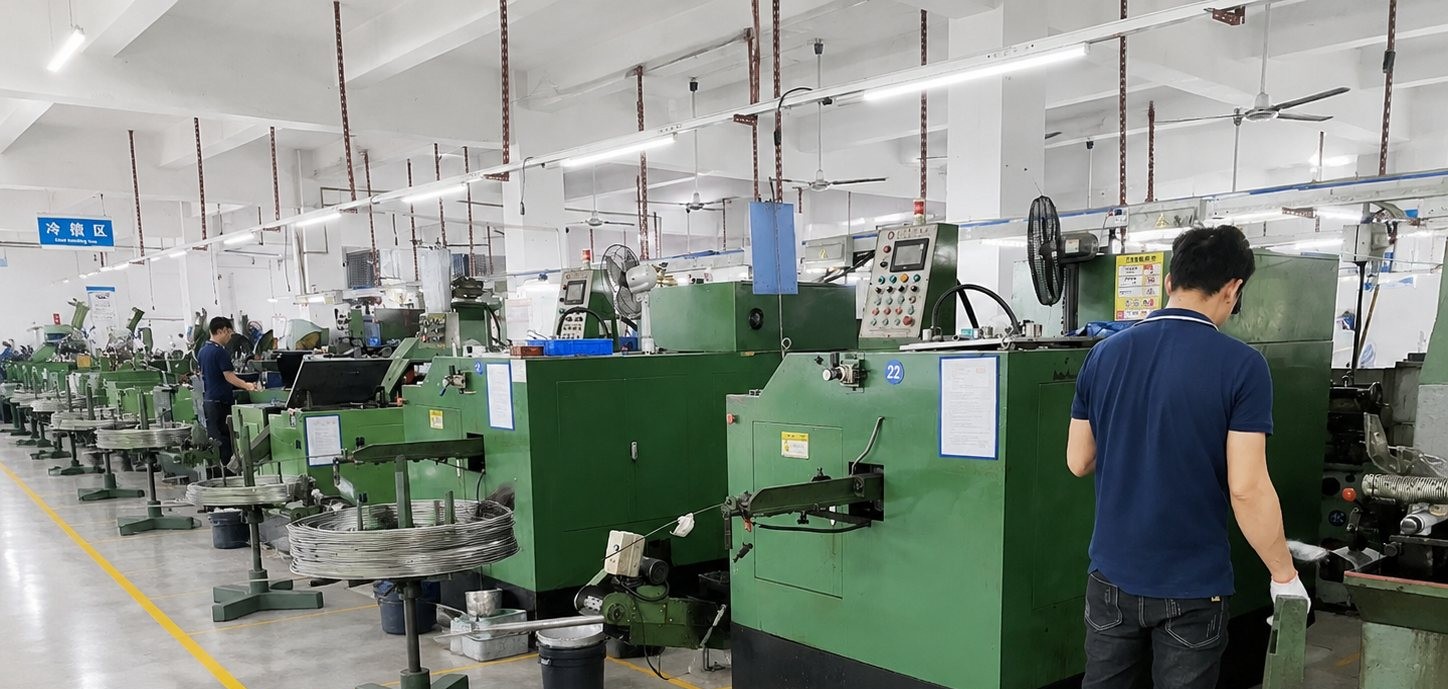
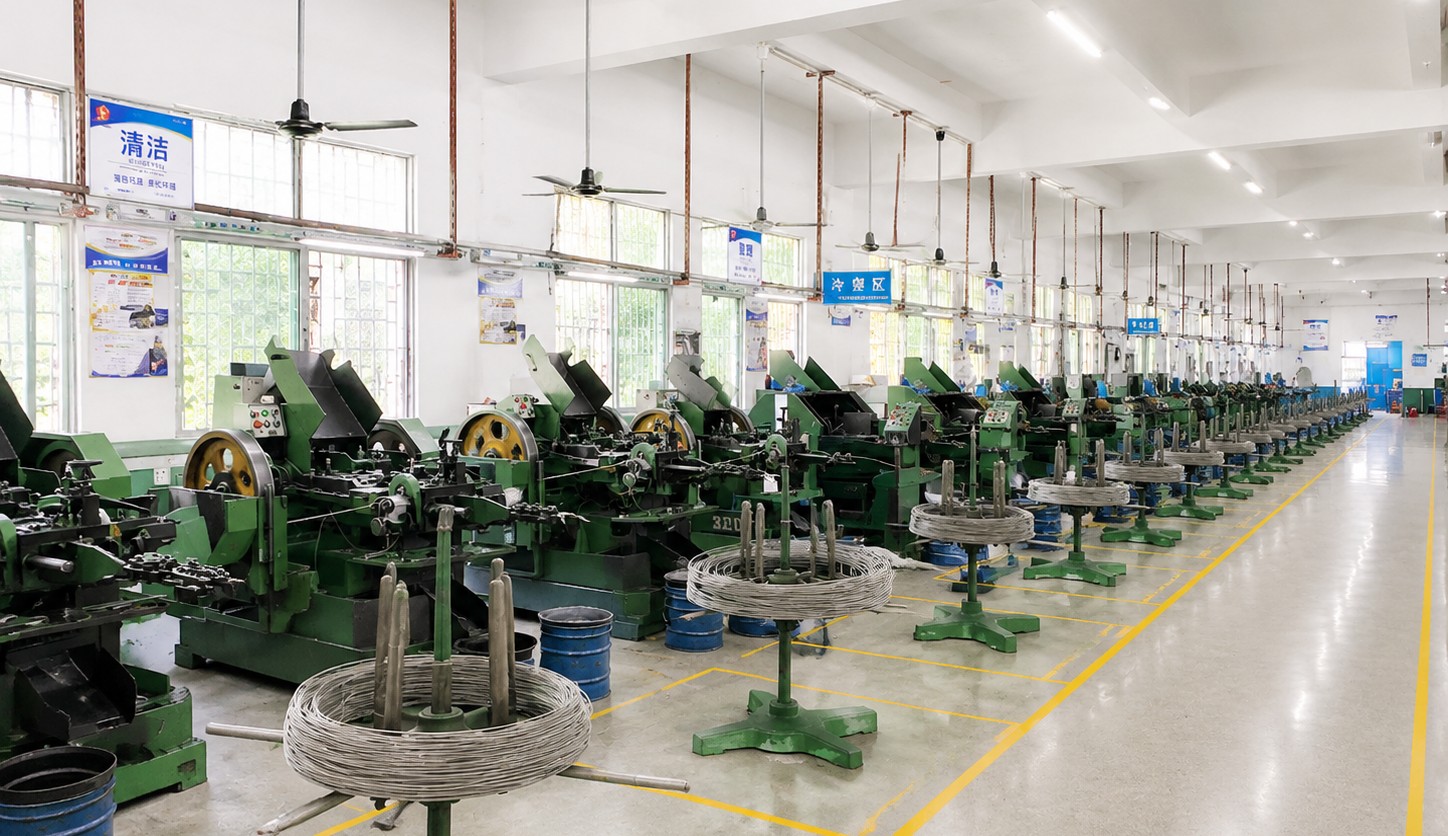
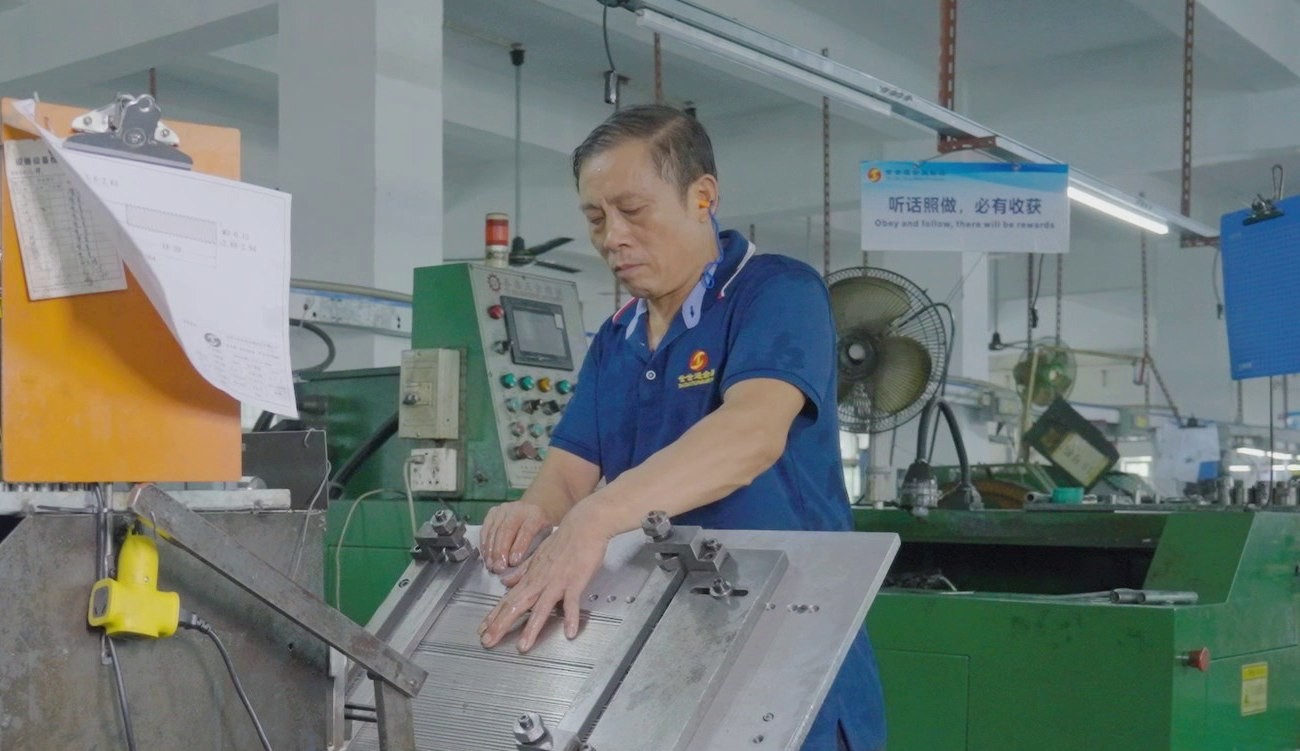
Shi Shi Tong forms these phillips head self tapping screws on a single-die header that upsets the pan head and the Phillips recess in one stroke, rolls the coarse thread over the full length and forms the gimlet point. The parts are white zinc plated and sorted. The first part of every run is measured on the head, gauged after plating and driven into a sample of the material, before the batch continues.
|
|
The point is where a baseline screw is usually won or lost. A gimlet point that is slightly blunt will skate on a painted panel and mark it before the thread catches, and the mark is on the customer’s product rather than on the screw. The point is therefore checked on the first article and sampled through the run, not assumed from the roll.
What decides whether phillips head self tapping screws pass is the head, the recess, the thread, the point and the plating. The inspection agreement covers those, and the criteria come from the drawing.
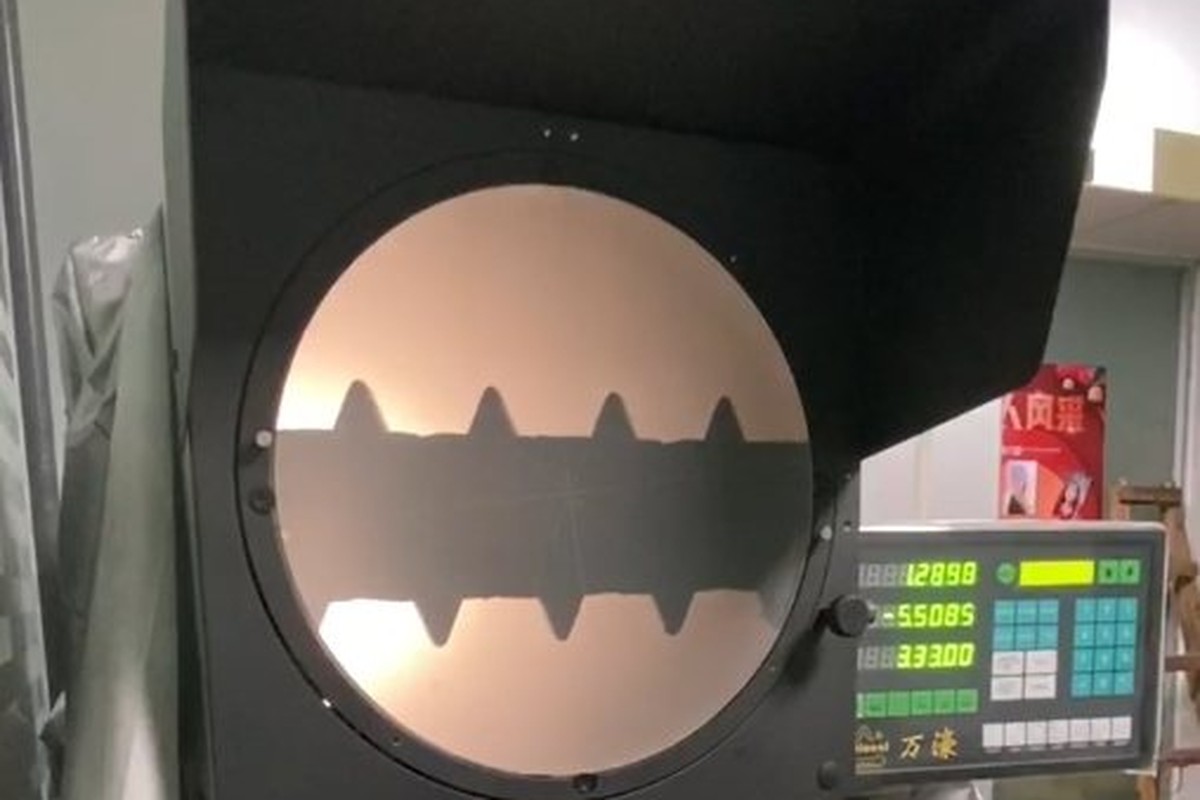
Head profile on the projector |
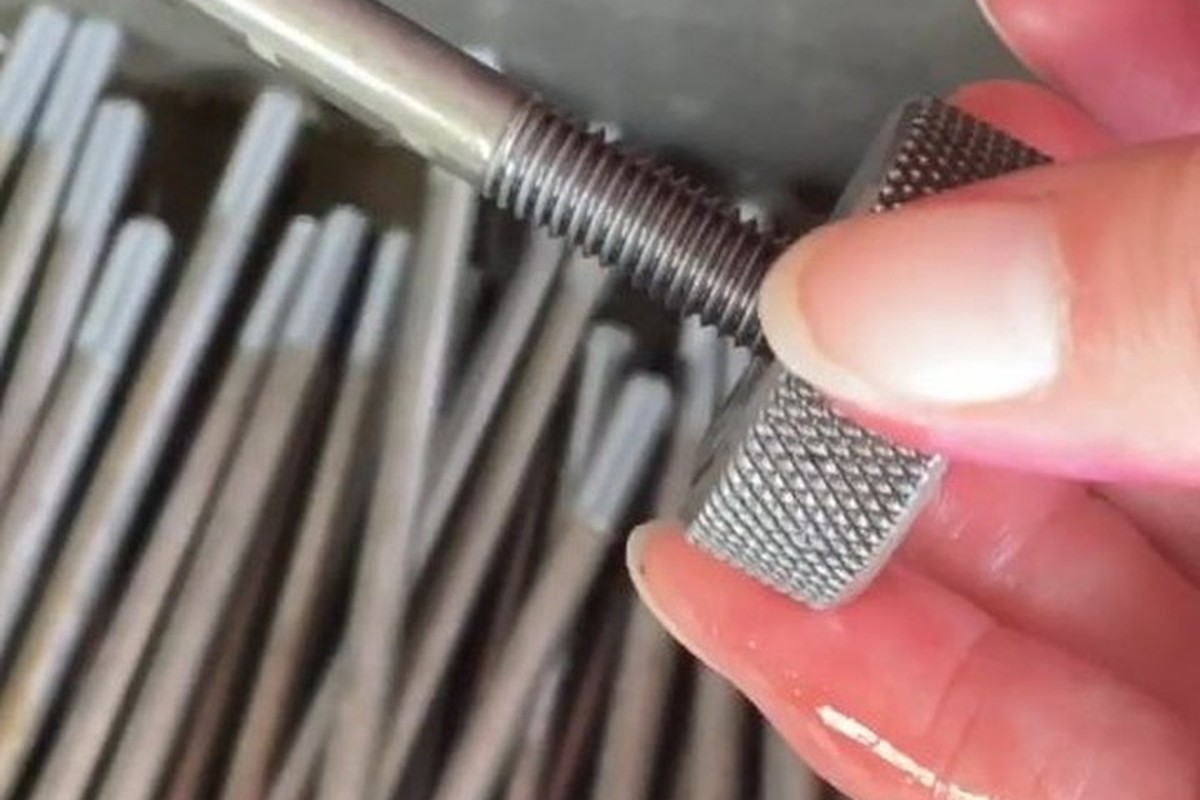
Thread gauged after plating |
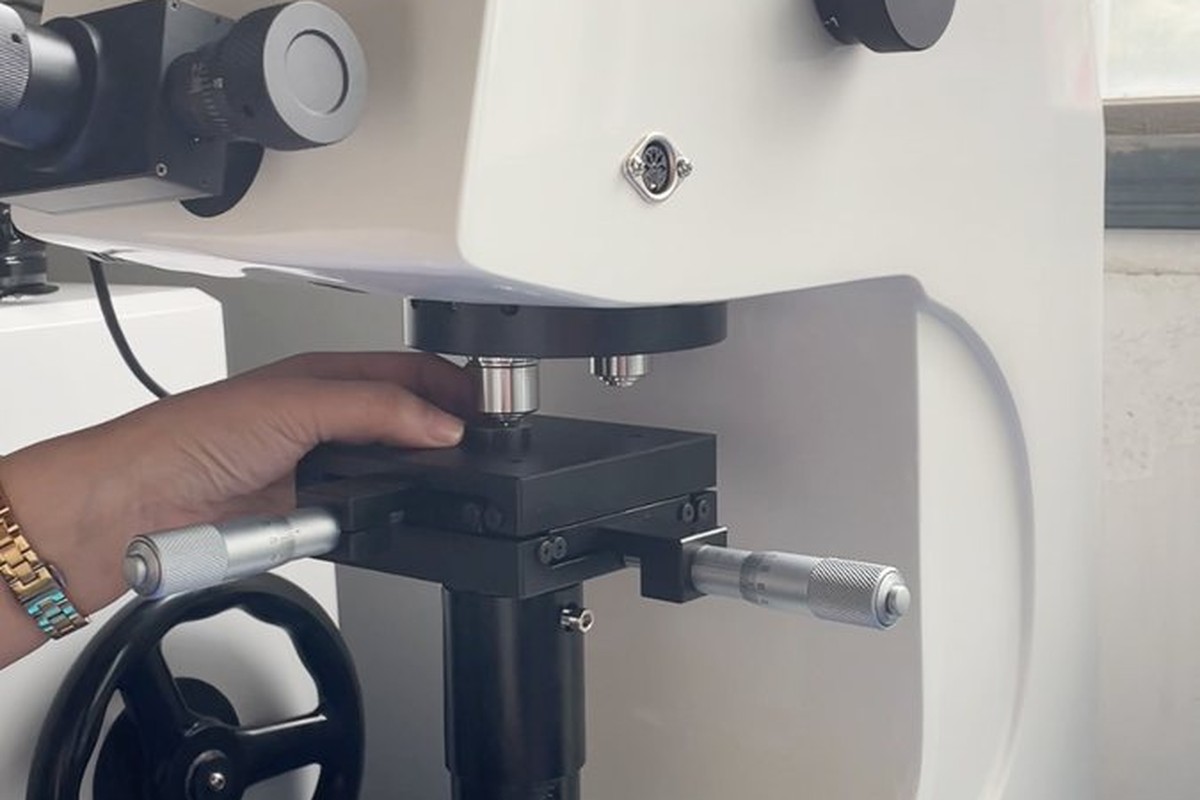
Hardness testing against the property class |
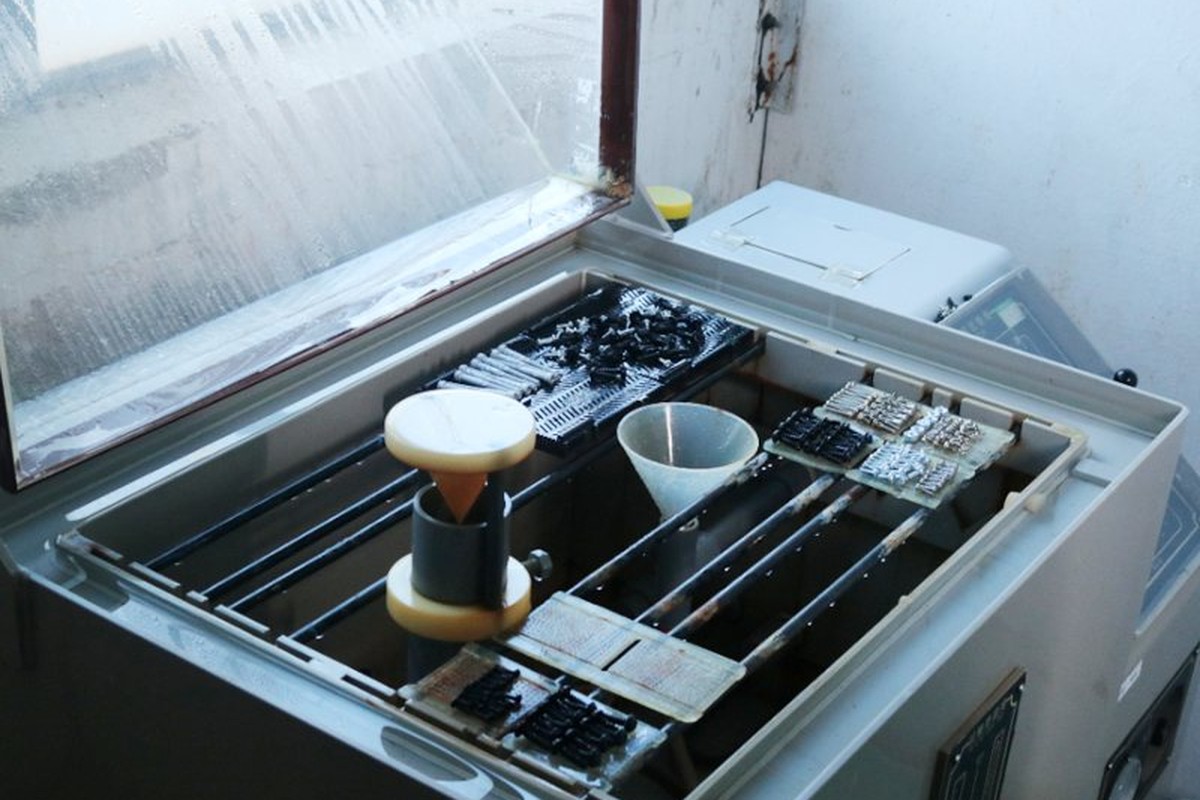
Salt-spray testing of the white zinc plate |
The recess is checked by driving with the production bit and looking for bright zinc on the wings. That bright mark is the earliest sign that the recess is too tight after plating, and it appears before the head strips — so it is a check that saves a line stoppage rather than one that documents a failure.
The point is checked on a sample of the actual material. A gimlet point that suits board will skate on thin sheet, and the test that settles which part has been made is the one that drives it into the customer’s material.
Every shipment of phillips head self tapping screws is traceable to the wire it was made from and to the plating batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.
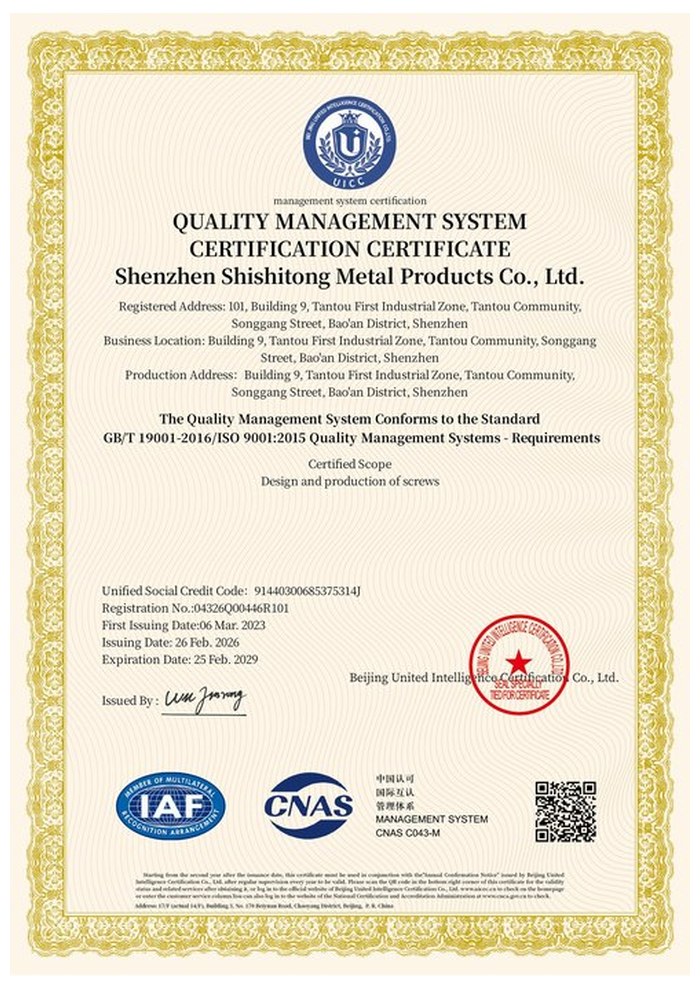
ISO 9001:2015 |
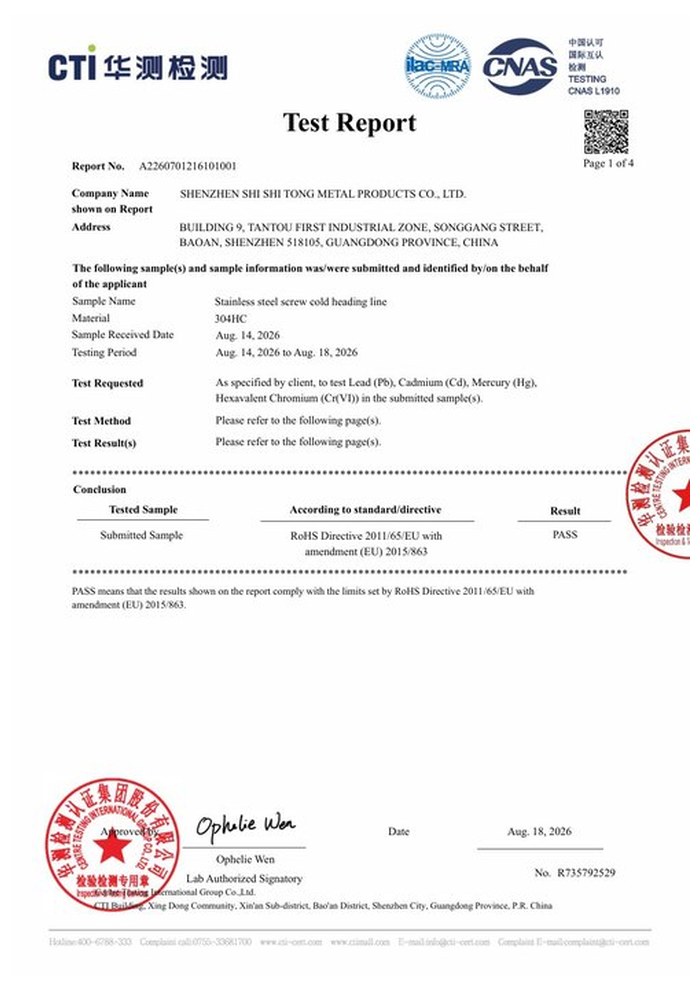
RoHS test report |
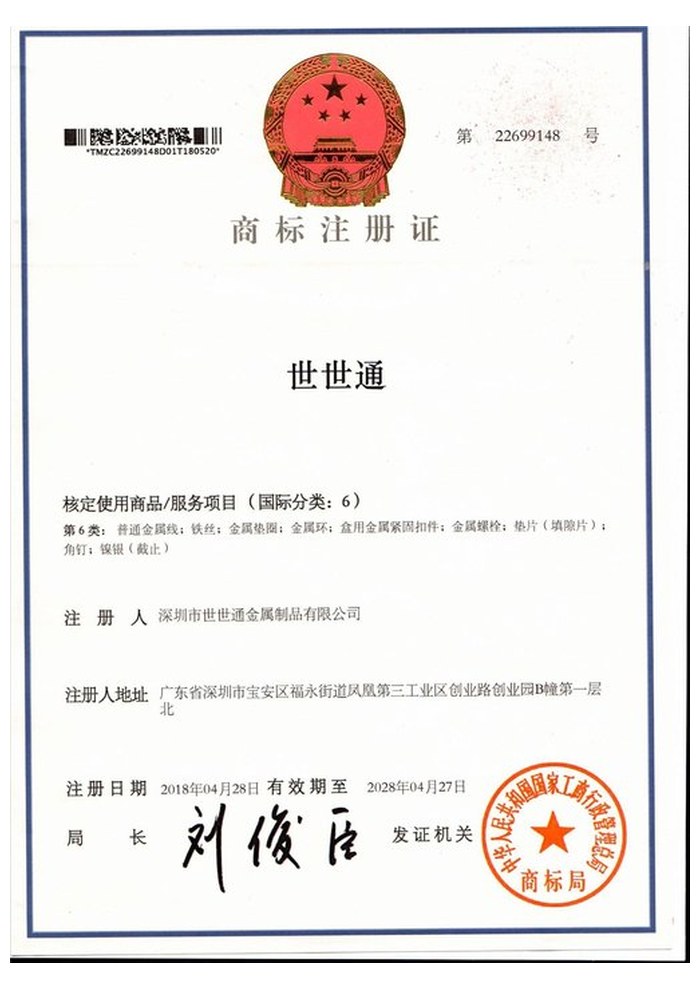
Registered trademark |
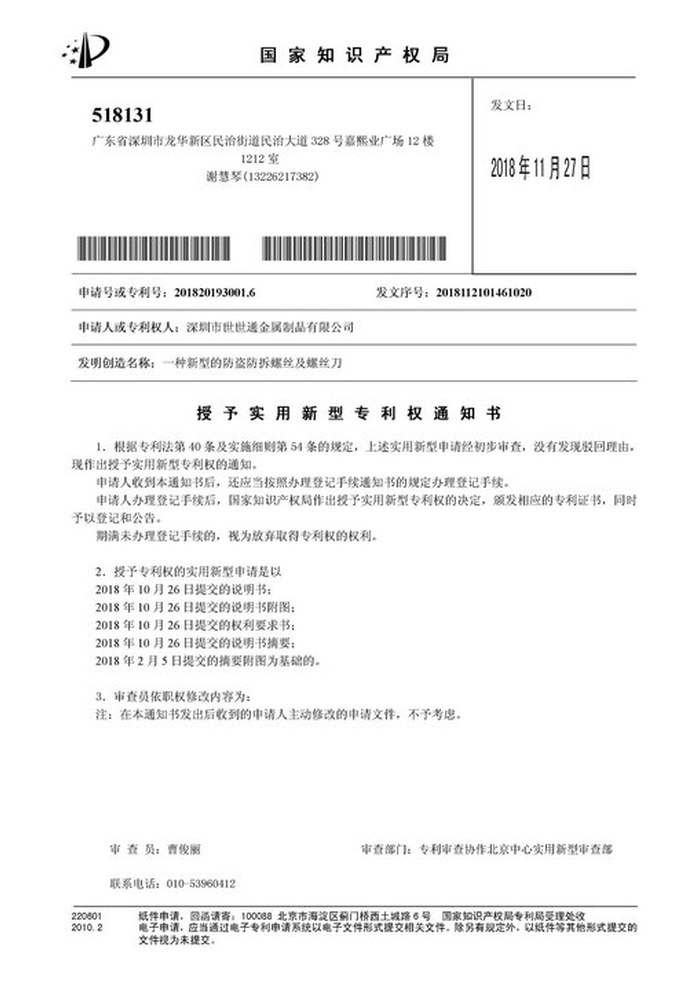
Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the plating. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a baseline screw the first article is driven into a sample of the material, because the point and the thread only prove themselves in the material they were specified for. Buyers visit during the process to review samples and to see how the heads are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header and the plating line can be seen on the day the parts run.
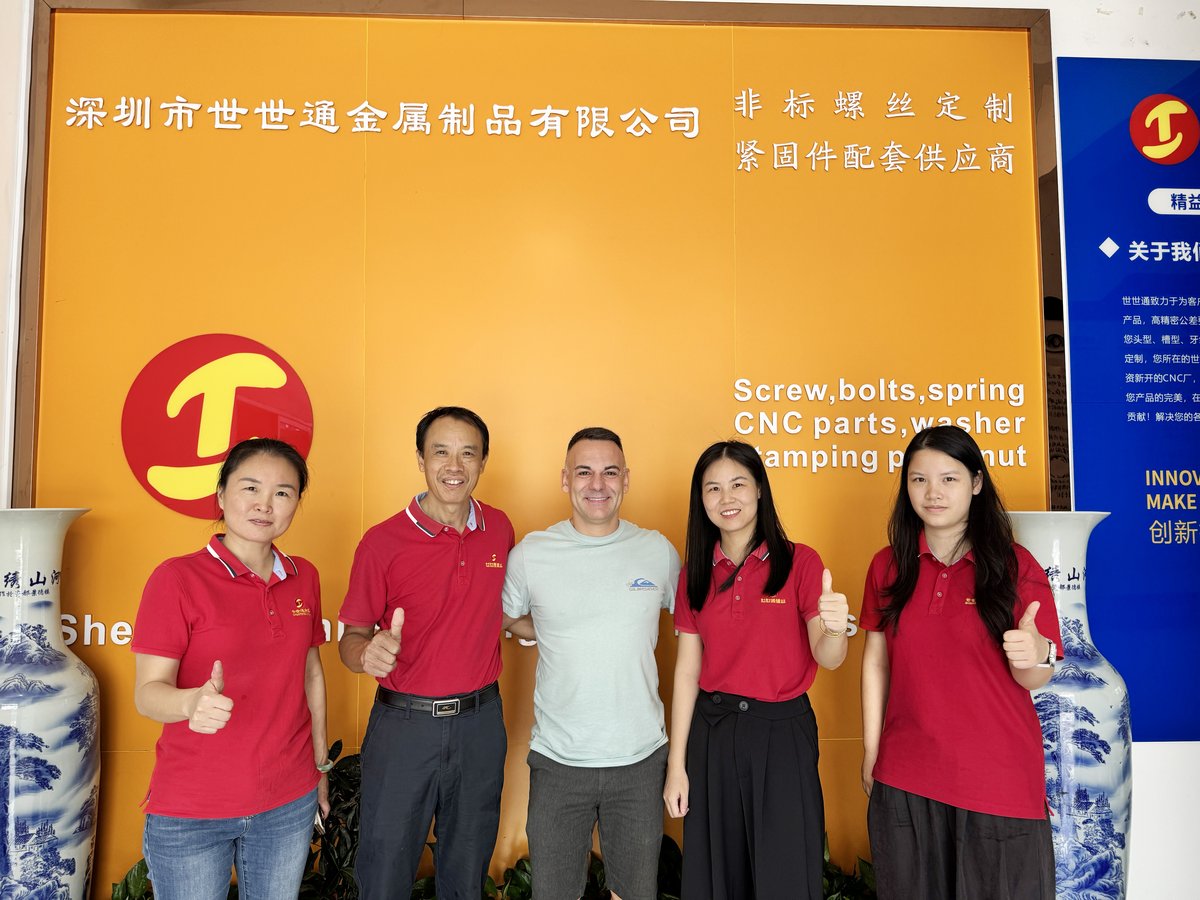
Customer group visit – sample review |
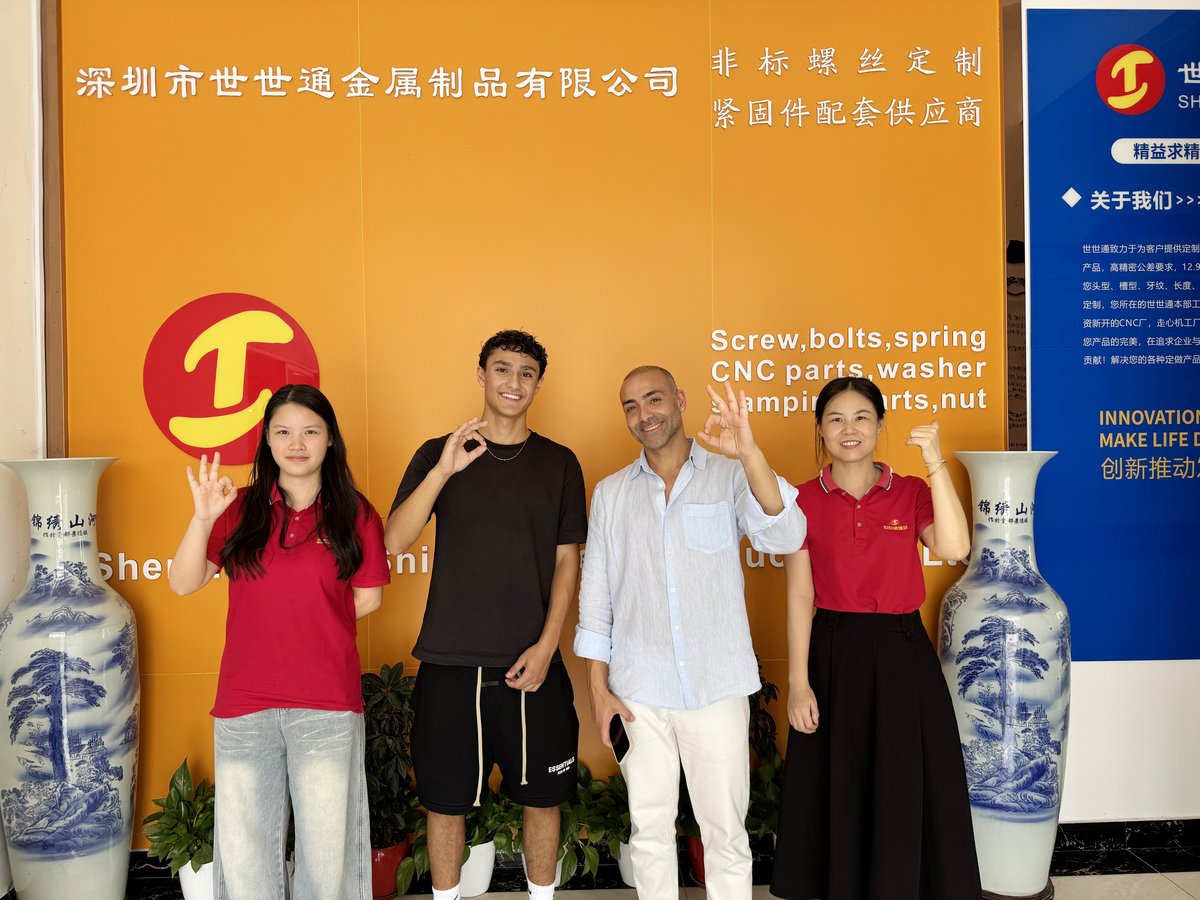
Customer group visit – process discussion |
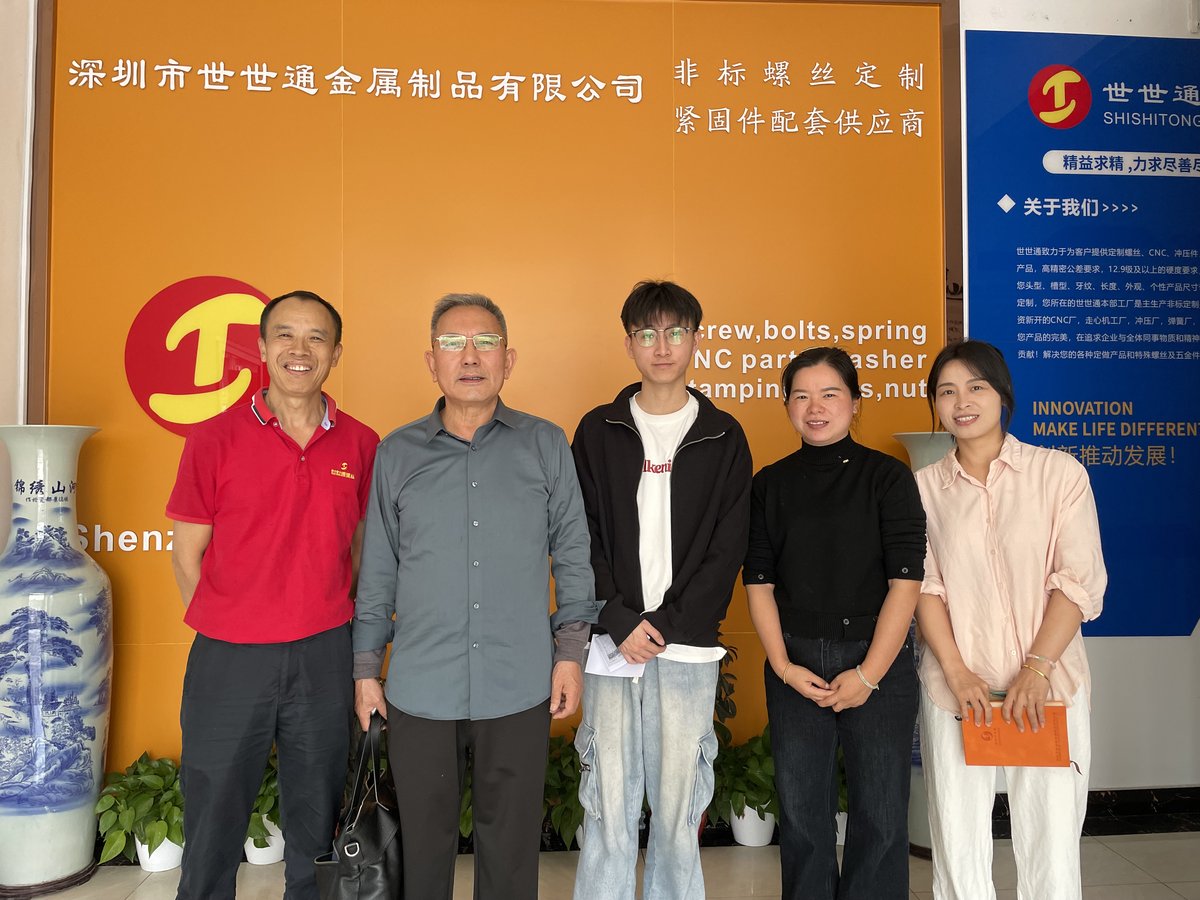
Customer group visit – factory tour |
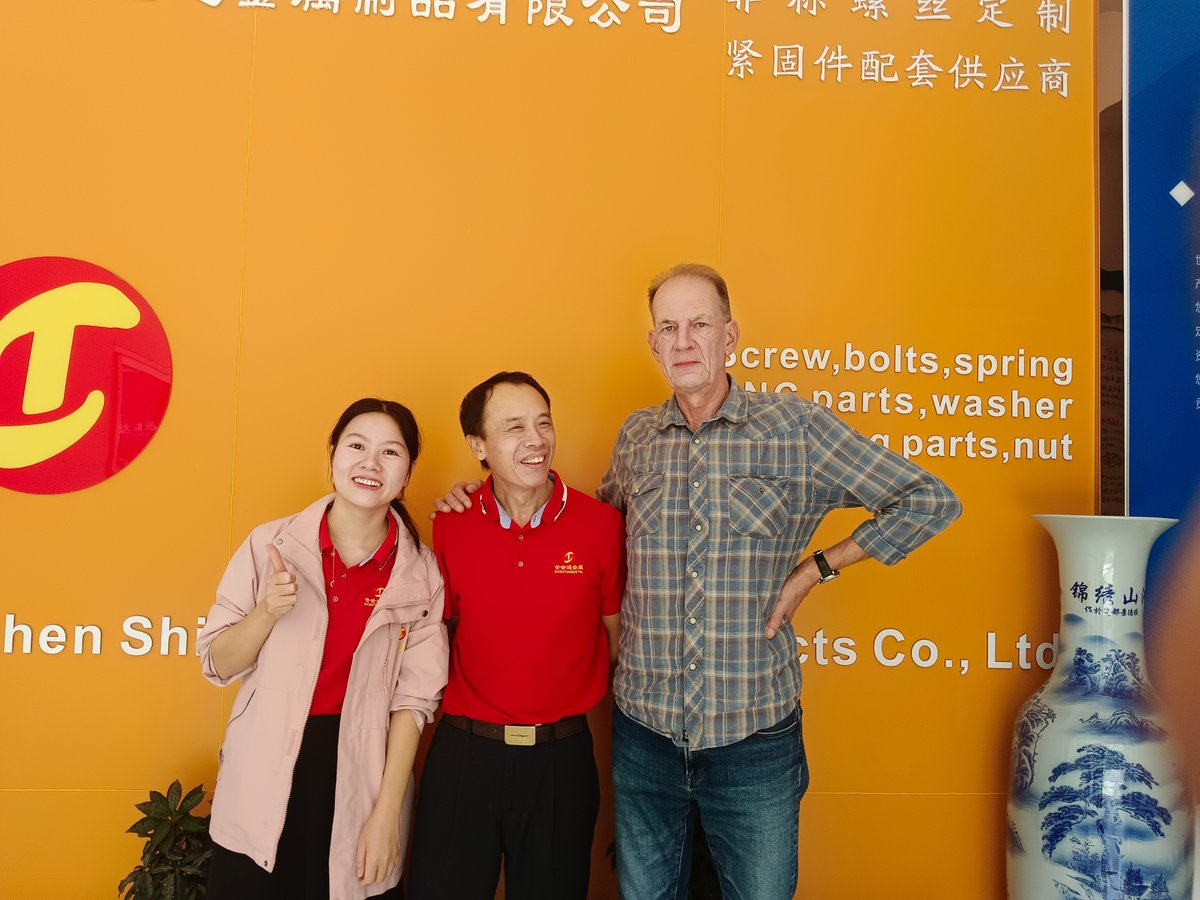
Customer visit – project kick-off |
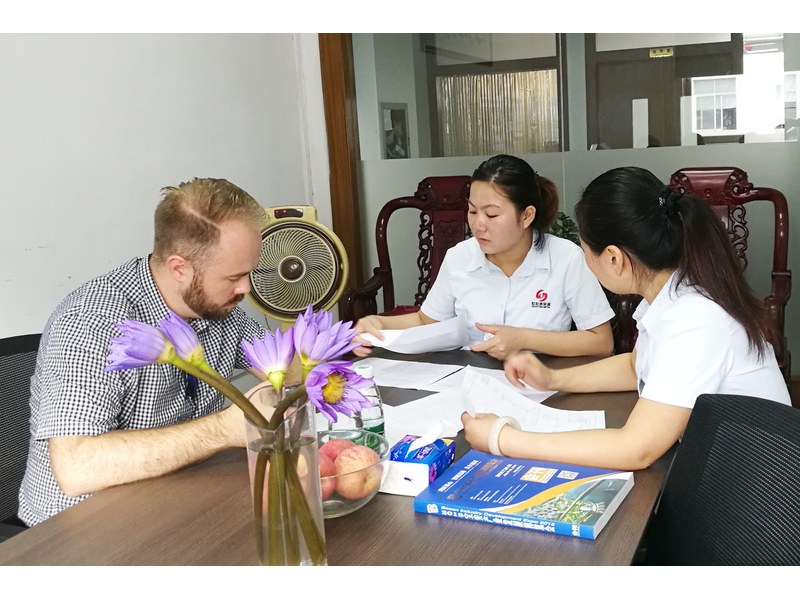
Danish customer – drawing review |
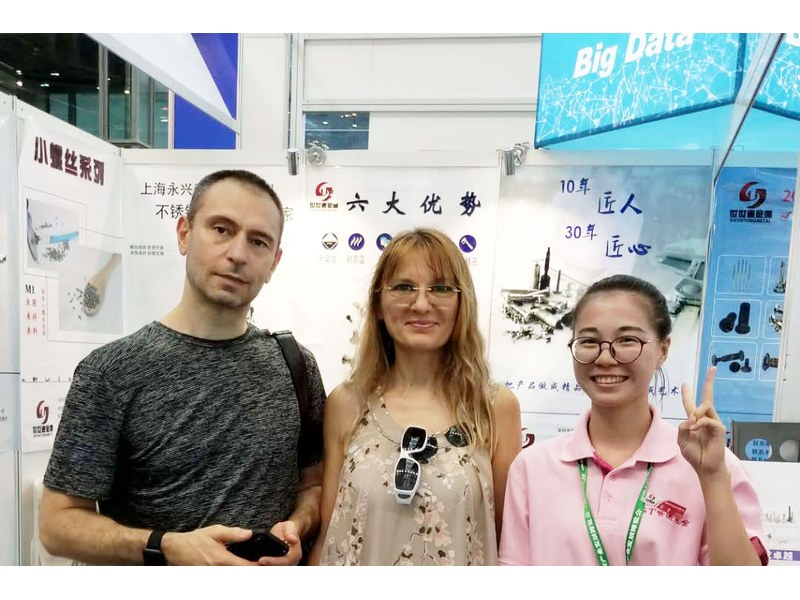
Industry exhibition – meeting customers |
Self-tapping screws driven with a cross bit. They form their own mating thread in a prepared hole, so no nut or tapped hole is needed.
A gimlet point for timber, board and plastics; a drill point for sheet metal. The two are different parts and the material decides which.
Panel thickness plus engagement, measured from under the head. In a blind hole the thread depth has to be at least the length minus the panel thickness.
Only briefly. It is the standard indoor finish and gives way slowly in rain and salt air. For outdoor joints a Dacromet or stainless part is the right choice.
The deposit narrows the cross and the wall around it is thin on small sizes. The bit has to fit, and the recess is checked after plating for exactly that reason.
Thread size and pitch, head diameter and height, point form, length and datum, material, finish and the material being joined.
How a phillips head self tapping screw project runs from drawing to repeat delivery:
|
1
Send the drawing and a material sample
|
→ |
2
Point and length review
|
→ |
3
First article driven in the sample
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size and pitch, head diameter and height, point form, length and datum, material, finish and the material being joined.
|
Thread and pitch
|
Head diameter and height
|
Point form
|
|
Length and datum
|
Material and finish
|
Panel material
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.
 +86 13143444311
 sst@szsst88.com