Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
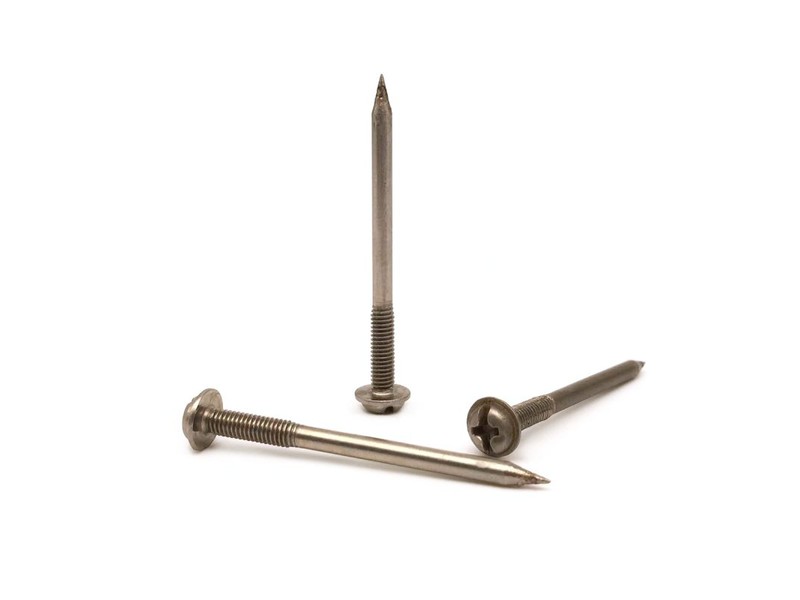
Type:Low Profile Self Tapping Screws
Materials:Carbon Steel
Surface treatment:Nickel Plated
Head Type:Ultra Profile Head
Drive:Phillips
Thread:Self Tapping
Point:Blunt
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:632
We head low profile self tapping screws from carbon steel with an ultra low head, a shallow cross recess and a coarse thread, bright nickel plated and quoted from M1 to M14. Head height, recess depth, thread and plating come from your drawing, and the first article is fitted under the cover the screw has to clear.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Low profile self tapping screws are screws whose head is deliberately shallower than a standard pan head, so the fixing barely stands above the surface it sits on, with a coarse thread that forms its own way into the material. The recorded item on this page is nickel plated carbon steel with an ultra profile head, quoted from M1 to M14 with Number 632.
Ultra profile head. A pan form that has been flattened: a low dome, a wide flat bearing face and a head height of a small fraction of its diameter. It covers the hole and bears on the part, but it does not stand proud of the surface the way a pan head does.
Cross recess. A Phillips cross, but a shallow one. On a low head there is very little material above the bearing face, so the recess cannot be as deep as on a standard head and has to be cut within the height that exists.
Self-tapping thread. A coarse thread with a sharp crest, rolled over the full length, that forms its own thread in sheet, board or a moulded boss. The joint needs no nut and no pre-tapped thread.
Blunt point. A short taper to a flat tip. The hole is drilled, punched or moulded first, and the first thread starts in that hole rather than piercing the material.
Nickel plate. A hard, bright, barrier deposit applied after the thread is rolled. It does not sacrifice itself the way zinc does; it protects by keeping the atmosphere off the steel, which is what a visible low head on a handled product needs.
The head is formed in one heading stroke and then flattened to the drawing height, and the recess is formed in the same stroke. On a low profile head the two are in competition: the recess and the material under it have to fit inside the head height, and every tenth taken off the head comes out of the wall below the cross.
That wall is what carries the torque. A standard pan head has the depth to put a full cross in and still leave material under it; a low head does not, so the recess is shallower, the driver engages less of it, and the head will cam out at a lower torque. The design decision on a low profile screw is therefore not only how low the head can be, but how much torque the joint actually needs once the head is that low.
The low head also changes the bearing face. Flattening a dome widens the flat area but shortens the radius that stiffens it, so a very low head can dish under a hard driver if the punch is not supported at the rim. A dished head shows as a bright ring on the part and a joint that rocks.
The thread is rolled full length from under the head to the blunt point. On a screw with this head the thread is proportionally large: the head is small, so the thread and the panel do most of the work, and the crest has to stay full after plating because the crest is what forms the thread in the material.
Nickel is plated over the finished screw, head, recess and thread. It builds a few microns in the recess, which matters more here than on a pan head because the recess is already shallow: the first article is driven with the production bit in the plated condition, and the bit is checked for wear at the same time.
The family is quoted from M1 to M14, with M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14 in the recorded range. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission; on a self tapping screw the working length is the thread length, because that is what forms in the panel.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Ultra profile, pan form | Height, diameter and face flatness |
| Recess | Phillips cross, shallow | Depth within the head height, bit tried after plating |
| Thread | Coarse single-lead self-tapping, full length | Gauged per batch after plating |
| Point | Short taper, blunt tip | Checked on the first article |
| Plating | Nickel, bright | Thickness range and adhesion sample |
| Length | From under the head to the point | Measured on the shop plate |
Head height is the dimension that has to be agreed first, because it fixes everything else. It decides the depth of the counterbore, the depth of the recess, and the torque the driver can put in. A drawing that quotes a head diameter and a length but leaves the height to the standard will come back with a head that is too tall for the counterbore it was designed around.
Length is measured from under the head, because that face bears on the panel. On a low head the difference from measuring at the top of the dome is small, which is exactly why it is worth writing down: a small difference is easy to absorb in a tolerance and hard to detect in a finished assembly.
Three features define this part: the low head keeps the fixing out of the way, the cross drives it with the standard bit, and the self-tapping thread works without a nut. The head height is the feature that everything else has to be traded against.
| Feature | What it gives | What it costs |
|---|---|---|
| Low head | Sits under a cover, a label or a sliding part | Less material for the recess and less torque |
| Wide flat face | Bears on thin sheet without a washer | A dished face shows as a bright ring |
| Shallow cross | Drives with a standard bit | Cams out earlier than a deep recess |
| Self-tapping thread | No nut, no tapped hole | Needs the right pilot hole |
| Nickel plate | Hard, bright, holds up to handling | Not sacrificial; a scratch exposes steel |
The reason to accept the torque loss is usually clearance. A low profile self tapping screw goes where a pan head would foul a cover, catch a sliding part, sit under a printed label or lift a stack of boards apart. In those places the joint is not highly loaded — it holds a trim, a panel or a housing — so the lower cam-out torque is not the limit; the clearance is.
The place it goes wrong is where a low head is specified for a joint that needs a full pan head’s torque. The screw looks right, the driver cam-outs before the joint is tight, and the answer is not a bigger driver but a head that is one step taller. That conversation is worth having at drawing review, when the head height can still be changed.
The recorded finish is bright nickel, applied after the thread is rolled. Nickel is a barrier coating rather than a sacrificial one: it does not corrode to protect the steel around a scratch, it keeps the atmosphere away from the steel for as long as the film is intact. On a visible low head that shows a lot of flat surface, that is the right trade, because a bright even tone is what the part is for.
| Finish | How it protects | Effect on the shallow recess | Typical use |
|---|---|---|---|
| Bright nickel | Hard barrier deposit | A few microns; bit tried after plating | Visible, handled assemblies |
| White zinc | Sacrificial zinc | A few microns; recess re-checked | Indoor, cost-driven work |
| Black nickel | Dark nickel deposit | A few microns; recess re-checked | Dark visible equipment |
| Black oxide | Thin conversion film, oiled | Almost no change | Unseen joints, tool-room work |
| Dacromet | Zinc-aluminium flake layer | Film builds; recess re-checked | Outdoor and wet service |
On a shallow head the plating has less room than usual. A recess that is already only a little deeper than the driver tip cannot afford a coating that fills it, which is why the recess is re-checked after plating and why a thick decorative deposit is a poor choice on a low head even when it looks better in the sample bag.
Nickel also has an honest limit. Where the coating is broken — a slipped driver, a ding at the rim, a scratch across the flat — there is no zinc to protect the edges and the steel rusts from that point. On a wet or washed assembly the answer is stainless or a flake coating, not a thicker nickel.
Three assemblies where a low profile self tapping screw solves a clearance problem rather than a strength problem:
| Where it sits | The screw closes a housing where the head has to sit under a cover, a label or a sliding battery door and a pan head would stand proud of the seam. |
| When it goes wrong | A proud head rubs the cover, wears the print and stops the door sliding; a tall head shows through a gap. |
| Why it happens | The head must clear a moving part, the housing is thin, and the fixing is visible only in its recess. |
| What we control | Head height and face flatness checked, recess driven with the production bit after plating. |
| Where it sits | The screw fixes a trim, a bracket or a plate where the sheet is too thin to countersink and the surface has to stay close to flush. |
| When it goes wrong | A countersunk head would thin the sheet past its limit, and a pan head leaves a bump that the next layer sits on. |
| Why it happens | The sheet is thin, the surface is stacked against another part, and the fixing repeats. |
| What we control | Head height held to the drawing, thread gauged after plating, pilot hole agreed on the sheet. |
| Where it sits | The screw fixes a fitting where the head sits under a laminate edge, a slide or a trim strip and any bump is felt. |
| When it goes wrong | A proud head tents the laminate, and a head that is too small pulls through a soft board. |
| Why it happens | The fixing is under a surface, the material is soft, and the assembly is handled. |
| What we control | Head diameter matched to the spacing, face flat checked, point form tested on the board. |
Four reasons that matter on a shallow head, each tied to what the drawing has to prove:
|
Head height reviewed before the die
The head height, the recess depth and the joint torque are reviewed as one set, so a head that is too low to take the driver or too high for its counterbore is raised before the die is cut. Basis: Head height and recess reviewed together. |
Heading, rolling and plating in one route
The low head and the shallow cross are formed in one stroke, the thread is rolled to a blunt point and the parts are nickel plated in the same route. Basis: One route from wire to plated screw. |
|
Recess judged in the plated state
The recess is driven with the production bit after plating, and the head face is checked for flatness on the first article, because a shallow head shows a dish at once. Basis: First article checked after plating. |
First article fixes the setting
The first article fixes the wire heat, die set, thread roll and plating; repeat orders are compared against that record rather than re-read from the drawing. Basis: First article signed off before the batch is released. |
Shi Shi Tong heads these low profile self tapping screws from carbon steel wire on single-die headers that form the flattened head and the shallow cross in one stroke, rolls the coarse thread full length to a blunt point and plates the parts bright nickel. The first part of every run is measured on the head height and face, driven with the production bit and driven into a sample of the customer’s material before the batch continues.


|

|
A low head is harder to head than a pan head, because the punch has to form a flat disc without thinning the rim. When the die is worn the rim comes out rounded and slightly thicker, the head looks domed rather than flat, and the recess ends up shallower than the drawing because the material has flowed outwards instead of staying under the punch. That is why the head profile is checked on the section and not only across the top.
What decides whether low profile self tapping screws pass is the head height, the face, the recess, the thread and the plating. The inspection agreement covers those, and the criteria come from the drawing.

Head height and recess on the projector |

Thread gauged after plating |

Hardness testing against the property class |

Salt-spray testing of the nickel plate |
The head is checked for height and diameter on the projector and for flatness on the first article. Height is checked at the rim and at the centre, because a low head that is thicker at the rim is a head that has lost recess depth, and that is the failure the customer feels as cam-out rather than sees.
The recess is driven with the production bit after plating. On a shallow cross this is the decisive check: the bit reaches the bottom with almost no margin, so a coating that fills a few microns or a punch that has worn a few microns both show up as a bit that sits high and rocks.
The thread is gauged after plating and the driving torque is measured in a sample of the customer’s material. On a self tapping screw the strip torque is read with it, because a low head that strips the panel and a low head that cams out look the same to an operator and have completely different causes.
Every shipment of low profile self tapping screws is traceable to the wire it was made from and to the plating batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the plating. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a low head the first article is also the clearance sample, so the customer checks it under the cover or the label it has to sit beneath before the batch is released. Buyers visit during the process to review samples and to see how the heads are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the plating line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
A head height well below a standard pan head of the same diameter, usually a flattened disc rather than a dome. The number is on the drawing; there is no single figure that covers the family.
The same cross bit, but the recess is shallower because the head is shallower. A worn bit shows up here first, and the first article is driven with the production bit.
Less than a pan head of the same size, because there is less material under the cross. Where the joint needs more, the answer is a taller head rather than a harder driver.
A blunt point for a drilled, punched or moulded hole. It starts in the hole and forms its own thread; it does not pierce the material first.
Nickel is harder, brighter and better on a visible handled part, but it is a barrier rather than a sacrificial coating. Once it is scratched the steel at the scratch rusts.
Head diameter and height, recess size, thread size and type, point form, length and datum, material, plating thickness and the pilot hole reference.
How a low profile self tapping screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the clearance envelope
|
→ |
2
Head height and recess review
|
→ |
3
First article fitted under the cover
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the head diameter and height, the recess size, the thread size and type, the point form, the length and datum, the material and plating.
|
Head height
|
Head diameter
|
Recess size
|
|
Thread and type
|
Point form
|
Length and plating
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com