Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
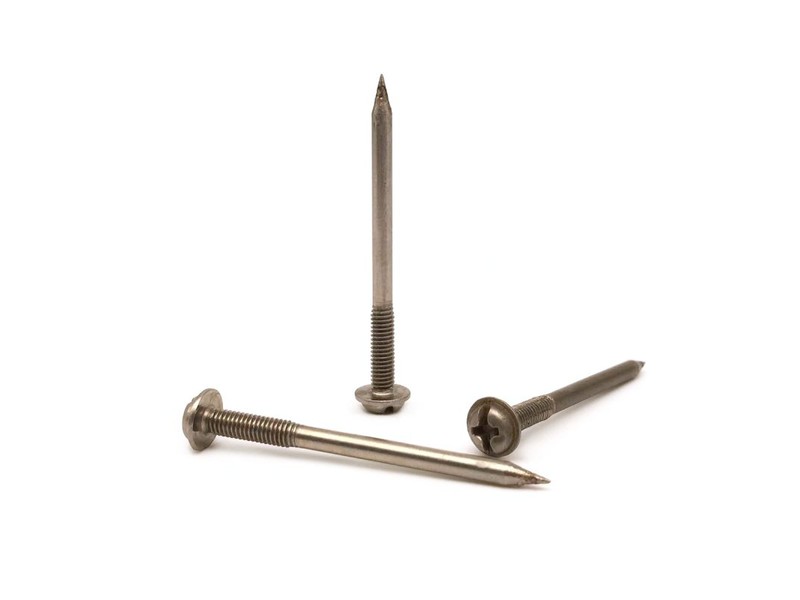
Type:Countersunk flat head self tapping screw with a Phillips cross recess, a full length coarse thread and a flat blunt point (Non-Standard)
Materials:Carbon Steel
Surface treatment:Nickel Plated; bright silver white electroplated film over the cone, the recess and the thread crests
Head Type:Countersunk flat head, 90 degree cone on the underside, flat top face with a slight crown, head diameter about 2 times the thread diameter, head height about 0.5 times the head diameter; no washer, no flange
Drive:Phillips cross recess, four tapered wings with a pointed centre; no straight slot, no hexagon socket, no Torx
Thread:Coarse single-lead self tapping thread, sharp crest, rolled, full length from the root of the head cone; no plain shank
Point:Flat blunt end with a small chamfer; no gimlet taper, no sharp point, no drill point, no cutting slot
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Forming:Single-die cold heading, thread rolling, nickel plating, sorting
Number:646
We manufacture csk phillips head self tapping screws with a 90-degree countersunk head, a full coarse thread and a flat blunt point, in carbon steel with a bright nickel finish. Cone angle, head proportions, point, length and finish are taken from your drawing.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A csk phillips head self tapping screw is a self-tapping screw with a countersunk head — csk is the trade shorthand for countersunk — a Phillips cross recess, and a thread that forms its own path in a prepared hole. The recorded item on this page is carbon steel with a bright nickel finish and a flat blunt point, quoted from M1 to M14 with Number 646.
Countersunk head. A 90-degree cone on the underside and a flat top face with a slight crown. The head seats in a countersink and finishes flush, with the diameter at about twice the thread and the height about half the head diameter.
Phillips recess. Four tapered wings with a pointed centre. There is no slot and no socket, so the drive is the standard cross bit — which on a flush head matters, because a bit that wanders crushes the countersink edge before the screw has started.
Coarse self-tapping thread. A single-lead thread with a sharp crest, rolled over the full length from the root of the cone. There is no plain shank, so the whole length below the surface is working length.
Flat blunt point. This is the feature that distinguishes this part from most countersunk self-tapping screws: the end is flat with a small chamfer and no taper. It does not start its own hole, it does not skate, and it stops when the hole ends rather than driving on.
Bright nickel. A thin electroplated finish that reads silver-white over the cone, the recess and the thread crests. It protects the steel and keeps a flush fixing looking clean on a visible face.
The cone and the Phillips recess are formed in one heading stroke, so the recess stays concentric with the shank and square to the cone. On a countersunk head that squareness is what decides whether the screw seats evenly or bites one side of the countersink first.
The 90-degree cone angle has to match the countersink in the panel. A cone that is steeper sits on a narrow ring and crushes the edge of the countersink; one that is shallower bottoms before the head reaches the surface. Both show as a ring of torn material around a head that stands slightly proud.
The thread is rolled from the root of the cone to the point, with no plain shank, so the whole length below the surface engages. On a csk phillips head self tapping screw with a blunt end that matters more than usual: the thread has to start cutting at the hole entry, because there is no tapered point to lead it in gently.
The point is left flat with a small chamfer rather than tapered. A flat point cannot make its own hole and cannot wander, so the hole position is exactly the one that was drilled. It also stops the screw at the far face of a panel instead of letting the tip break through.
Nickel plating follows rolling and covers the cone, the recess and the crests. It adds a few microns, so the thread is gauged in the plated condition and the head is checked in a countersink sample after plating rather than on a bare part.
The family is quoted from M1 to M14, with M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14 in the recorded range. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission; a csk phillips head self tapping screw is normally short, because the head is buried and the thread only has the panel thickness to work in.
| Item | How it is defined | What we control |
|---|---|---|
| Cone angle | 90 degrees, to match the countersink | Checked on the projector |
| Head diameter | About twice the thread diameter | Measured on the first article |
| Head height | About half the head diameter | Checked on the section |
| Recess | Phillips cross | Driven with the production bit |
| Thread | Coarse single-lead self-tapping, full length | Gauged per batch after plating |
| Point | Flat with a small chamfer | Checked on the first article |
| Length | Overall, top of head to point | Measured on the shop plate |
Length on a countersunk screw is measured overall, from the top of the head to the point. The working length is that figure minus the countersink depth, and on this part the countersink depth is roughly the head height — so a screw quoted as 12 mm overall in a 2.4 mm countersink has about 9.6 mm of thread in the panel, not 12.
The head proportions are worth checking against the hole before ordering. At twice the thread diameter the head covers a normal clearance hole; where the hole is oversized or the countersink is wide, the next size up is the honest answer rather than pushing this head beyond its diameter.
A flat point on a self-tapping screw is a deliberate restriction, and it changes where the part can be used.
| Feature | What it gives | What it costs |
|---|---|---|
| Flat blunt point | No wandering, no breakthrough, stops at the hole end | Cannot start its own hole |
| Countersunk head | Flush finish, nothing to catch | Cone must match the countersink |
| Full thread to the cone | Engagement over the whole working length | No lead-in taper to guide the first turn |
| Phillips recess | Standard bit, cams out before damage | Less torque than a socket of the same size |
| Bright nickel | Clean silver finish | Thin coating can be worn at the crests |
The point is the reason to specify this version. A gimlet point will centre itself in a hole and lead the thread in, which is convenient on timber and board; a flat point will not, so the hole has to be there and it has to be the right size. What you get in exchange is position accuracy: the screw goes where the hole is, not where the point decides.
The blunt end also stops the screw. In a panel of known thickness the tip reaches the far face and stops, rather than breaking through and leaving a sharp point inside a housing. On a csk phillips head self tapping screw used in an enclosure that is a practical advantage rather than a restriction.
The trade is the entry. Without a taper, the first thread has to cut its way in from a flat face, so the hole must be chamfered or deburred and the driving torque at the start is higher. That is a process decision on the customer’s line, and it belongs on the drawing next to the hole size.
The recorded finish is bright nickel, applied after the thread is rolled. The deposit is thin and bright, and on a countersunk head the cone is the surface that shows it most: a flush fixing is judged by the ring of cone visible in the panel.
| Finish | How it protects | Effect on cone and thread | Typical use |
|---|---|---|---|
| Bright nickel | Hard metallic deposit | A few microns; seat checked after plating | Visible flush fixings |
| White zinc | Sacrificial zinc, blue-white passivation | Thin; thread gauged after | General indoor assembly |
| Black zinc | Zinc with black passivation | A few microns; recess re-checked | Dark panels |
| Dacromet | Zinc-aluminium flake layer, cured | Thin film; seat re-checked | Outdoor and wet assemblies |
| Stainless (equivalent part) | Alloy provides protection | No coating | Wash-down and coastal work |
The seat is where plating matters on this part. A deposit on the cone changes its fit in the countersink very slightly, and on a flush head that is enough to move the contact ring from the middle of the cone to its edge — a head that looks sunk or proud depending on the light. The first article is therefore seated in a countersink sample after plating.
Nickel over steel is a hard coating on a softer body, so a screw driven hard can crack the deposit at the thread crests and let the steel corrode underneath. On a csk phillips head self tapping screw used indoors that is a cosmetic issue; outdoors it is a reason to specify a different finish.
Three assemblies where a flush head and a prepared hole are both normal:
| Where it sits | The screw fixes a panel or a cover into a punched or drilled hole, with the countersunk head finishing flush on the outside face. |
| When it goes wrong | A pointed screw wanders off the hole and marks the paint, and a cone that does not match the countersink leaves the head proud. |
| Why it happens | The sheet is thin and coated, the face is seen, and the holes are punched in a flat pattern. |
| What we control | Cone angle against the countersink sample, point checked as flat, plating seat checked after plating. |
| Where it sits | The screw fixes a hinge plate, a bracket or a connector into a drilled hole where the head has to sit below the surface. |
| When it goes wrong | A head that stands proud catches on whatever slides over it, and a gimlet point splits a brittle board where a flat point would not. |
| Why it happens | The material is board or a composite, the fixing is flush, and the joint is made on a bench. |
| What we control | Point form and hole size checked against the board sample, head seat checked. |
| Where it sits | The screw holds a plate or a bezel where the fixing is flush and the panel face has to stay readable. |
| When it goes wrong | A proud head breaks the plane of the panel, and a bright head that has worn at the crests reads as damage. |
| Why it happens | The panel is machined or punched, the face is visible, and the fixings are in rows. |
| What we control | Cone and recess checked, finish tone matched to the panel, thread gauged per batch. |
Four reasons that matter on a flush self-tapping screw, each tied to what the drawing has to prove:
|
Cone and point reviewed together
The cone angle, the head proportions and the flat point are reviewed against the countersink and the hole, so a screw that will not seat or will not start is raised first. Basis: Cone and point reviewed as one set. |
Head, recess and thread in one route
The 90-degree cone and the Phillips recess are formed in one stroke, and the coarse thread is rolled from the cone root to a flat chamfered point. Basis: One route from wire to plated screw. |
|
Seat and recess checked after plating
The head is seated in a countersink sample and the recess is driven with the production bit, both in the plated condition. Basis: First article seated in a countersink sample. |
First article to repeat production
Repeat orders are checked against the first article, which records the drawing revision, wire heat, die set, thread roll and plating. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these csk phillips head self tapping screws on a single-die header that upsets the 90-degree cone and the Phillips recess in one stroke, rolls the coarse thread from the cone root and finishes the point flat with a small chamfer. The parts are nickel plated. The first part of every run is seated in a countersink sample, driven into a sample of the material and gauged after plating, before the batch continues.


|

|
The flat point is the operation that has to be controlled carefully on this part. It is made by trimming rather than tapering, and a trim that is not square leaves a burr on one side of the end — which drags in the hole and makes the screw start crooked. The end is checked on the magnified first article for squareness as well as for diameter.
What decides whether csk phillips head self tapping screws pass is the cone, the head proportions, the flat point, the recess, the thread and the plating. The inspection agreement covers those, and the criteria come from the drawing.

Cone angle on the projector |

Thread gauged after plating |

Hardness testing against the property class |

Salt-spray testing of the nickel plate |
The seat is checked by driving the first article into a countersink sample and looking at the contact ring. An even ring is a pass; a partial ring means the cone is not seating flat, which on a flush fixing is visible from across a room as a head that is slightly out of plane.
The point is checked for squareness and for the chamfer. A flat end is only an advantage if it is square, and a square end with no chamfer drags on the hole entry and raises the starting torque above what the line expects.
Every shipment of csk phillips head self tapping screws is traceable to the wire it was made from and to the plating batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the plating. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a flush fixing the first article is seated in the customer’s countersink, because the seat is decided by the panel and not by the screw alone. Buyers visit during the process to review samples and to see how the heads are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header and the plating line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
Countersunk. The head is a 90-degree cone that sits in a countersink and finishes flush with the surface.
A flat point cannot wander or break through, and it stops at the end of the hole. The hole has to be drilled or punched first; the screw will not make one.
Overall, from the top of the head to the point. The working length is that minus the countersink depth, which is roughly the head height.
Only if the countersink angle matches the cone. A mismatch leaves the head proud or sunk, and the countersink edge gets crushed.
Slightly. The deposit on the cone moves the contact ring, so the head is checked in a countersink sample after plating.
Thread size and pitch, head diameter and height, countersink angle, recess, point form, overall length, material and finish.
How a csk phillips head self tapping screw project runs from drawing to repeat delivery:
|
1
Send the drawing or a countersink sample
|
→ |
2
Cone and point review
|
→ |
3
First article seated and driven
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size and pitch, head diameter and height, countersink angle, recess, point form, overall length, material and finish.
|
Thread and pitch
|
Head diameter and height
|
Countersink angle
|
|
Point form
|
Overall length
|
Finish
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com