Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
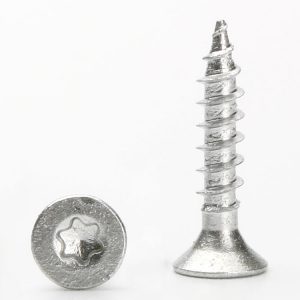
Type:Flat Head Tapping Screw Black Phosphate Screws
Materials:Carbon Steel
Surface treatment:Black Phosphate Plated
Head Type:Flat Countersunk Head
Drive:Pozi
Thread:Half Thread Self Tapping
Point:Gimlet Point
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:793
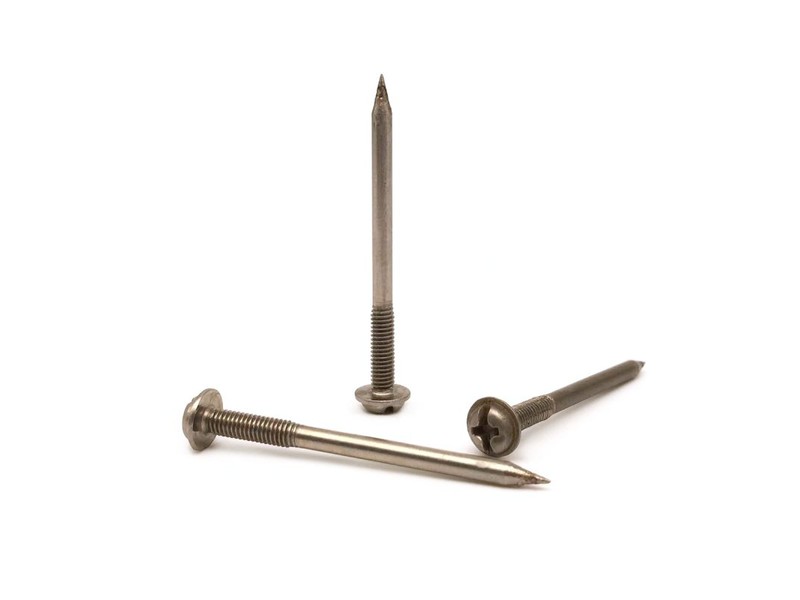
We make flat head tapping screws in carbon steel with a countersunk cone, a Pozi drive, a half thread and a sharp point, finished in black phosphate and oiled. Cone angle, Pozi size, point and finish come from your drawing, and the first article is seated in your panel and driven with a Pozi bit.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A flat head tapping screw seats flush on a countersunk cone and forms its own thread in the material, and the recorded item adds a black phosphate finish and a Pozi drive. It is carbon steel with a flat countersunk head, a half thread and a sharp point, quoted from M1 to M14 with Number 793.
Flat countersunk head. A cone that seats in a matching countersink and leaves the surface unbroken. It centres the screw as it turns and carries the clamp load over the whole cone.
Pozi drive. A cross with four extra ribs set between the wings. The bit engages the ribs as well as the cross, so the drive carries more torque before it slips — and it still slips when the torque is too high, which is the warning.
Half thread, sharp point. Thread from the point to a defined position with a plain shank under the head, and a gimlet tip that bites and starts its own hole in soft material.
Black phosphate. A conversion coating: the steel surface becomes a dark phosphate crystal that holds oil. It adds no measurable thickness, so the cone and the drive are exactly as formed.
The Pozi recess is a cross with four additional ribs at forty-five degrees, and the ribs do two things. They let the bit transmit more torque before the wings cam out, and they make the screw noticeably less prone to the bit climbing out under a powered driver. A Phillips bit will enter a Pozi recess, which is exactly the problem: it sits on the ribs, never reaches the bottom, and rounds the wings.
For a flat head tapping screw that matters because the drive is the only access. Once the head is flush there is nothing to grip, so a recess that has been damaged by the wrong bit cannot be recovered — the screw has to be drilled out of a hole that was meant to be invisible. The first thing to check on any Pozi screw is that the driver is a Pozi.
On flat head tapping screws the cone and the drive share the head height. The cone takes the lower part, and on a small head the recess is shallow, so the Pozi ribs are short and the bit has to be the right size and in good condition to reach them. That is the practical limit of the part: the drive carries more torque than a Phillips, but not more than its own depth allows.
On flat head tapping screws the half thread and the sharp point are the other end. In a two-member stack the plain shank passes the top member without cutting it, and the gimlet tip starts its own hole in wood, board or a soft polymer. On a flush fixing those two features are what let the joint close from one side.
Black phosphate is applied after the thread and the cone are formed, and it is a conversion rather than a deposit. The cone is the surface that seats against the countersink, so a coating that added thickness would change where the head stops; phosphate does not, and the head sits exactly where the geometry says.
The family is quoted from M1 to M14, with M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14 in the recorded range. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission; on flat head tapping screws the cone angle, the drive size and the thread length are quoted with the length, because all four are read against the panel.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Countersunk cone, flush top | Cone angle, diameter and concentricity |
| Drive | Pozi, cross with four ribs | Depth and width, Pozi bit tried on the part |
| Thread | Self-tapping, half length | Thread length and position from the end |
| Point | Gimlet, sharp tip with a threaded lead | Point angle and lead length |
| Finish | Black phosphate, oiled | Coating depth and oil film |
| Length | From the top of the head to the point | Measured on the shop plate |
The cone angle has to match the countersink, and on thin sheet the countersink is often formed rather than cut, which leaves it a degree or two off. The first article is seated in a sample of the customer’s panel for that reason rather than judged against the drawing.
Length is measured from the top of the head, because a countersunk head finishes flush and the top face is the datum that shows. From the start of the cone instead, the screw measures short by the head depth, which in a thin panel is the whole engagement on the far side.
Three features define this part: the Pozi drive, the countersunk head and the phosphate finish. The first two are what make a flush joint reliable, and the third is what keeps it looking like a black machine part rather than an unfinished screw.
| Feature | What it gives | What it costs |
|---|---|---|
| Pozi drive | More torque without slipping | A Phillips bit will damage it |
| Flush cone | Unbroken surface, self-centring | Bears on the panel; the panel is the limit |
| Pozi ribs | A clear cam-out point at high torque | Ribs wear before the wings do |
| Half thread | Plain shank passes the top member | Thread length must be specified |
| Black phosphate | Matte black, holds oil, no build | Not sacrificial; rusts at a scratch |
The practical difference between Pozi and Phillips is felt at the driver rather than read on the drawing. A Phillips screw that is driven hard climbs out; a Pozi screw keeps driving until the ribs lose engagement, and then it lets go. On a flush head that difference is the difference between a joint that stays tight and a cone with a bright starburst on it.
The phosphate finish is chosen for the look and for the oil. It is a matte black that does not reflect and does not read as a plated part, and the crystal holds a film of oil that makes it feel dry and slightly absorbent rather than slick. On equipment that is meant to look like machinery, that is the right tone.
The recorded finish is black phosphate. It is a conversion coating: the surface of the steel is turned into a dark phosphate layer, which is porous and holds oil, and it adds no measurable thickness. The protection is the oil film in the crystal, not the crystal itself.
| Finish | Build | How it protects | Where it fits |
|---|---|---|---|
| Black phosphate | None measurable | Oil held in a porous conversion layer | Dry indoor parts that should look unplated |
| Black zinc | A few microns | Sacrificial zinc with a dark passivation | Dark joints that see damp |
| Black oxide | None measurable | Oil film on a thin conversion layer | Tool-room and machine internals |
| Black nickel | A few microns | Hard barrier deposit | Visible handled parts |
| Dacromet | Thin flake layer | Zinc-aluminium barrier | Outdoor and automotive |
The difference that matters in service is sacrificial behaviour. A black zinc screw corrodes in place of the steel and protects the joint even after the oil has gone; a black phosphate screw does not, and once the oil film is washed off the steel at the cone and in the drive starts to rust. That is why the two finishes appear on different products even though they look similar in a box.
Phosphate has one advantage zinc does not: it is a good base for paint and for a subsequent oil or wax, and it does not build in a recess. A driven flush head with a phosphate finish keeps its drive exactly as formed, while a plated one can tighten the ribs enough to make the bit sit high.
Three assemblies where flat head tapping screws in black phosphate are the fixing:
| Where it sits | The screw closes a cover or fixes a plate where the surface must be flush, the part is inside a machine, and the finish must not be a bright plating. |
| When it goes wrong | A proud head fouls a sliding cover, and a plated head shows through a gap as a bright point. |
| Why it happens | The joint is flush, the part is dark and internal, and the fixing repeats. |
| What we control | Cone and drive checked, first article seated in a sample panel. |
| Where it sits | The screw fixes a panel or a module onto a dark casing where the fixing sits flush and reads as part of the product. |
| When it goes wrong | A bright screw on a matte black face reads as a repair, and a flush head that rocks shows a crescent of light. |
| Why it happens | The face is dark, the head is flush, and the joint is serviced. |
| What we control | Drive driven with the Pozi bit, cone seated, tone held to the sample. |
| Where it sits | The screw joins a bracket or a fitting into board or a soft composite where the head must sit flush and the screw starts its own hole. |
| When it goes wrong | A screw that does not start skates and tears the surface, and a head that stands proud is felt through a veneer. |
| Why it happens | The material is soft, the face is finished over, and the fixing repeats. |
| What we control | Point and thread tested on a sample board, cone angle matched. |
Four reasons that matter on a flush Pozi screw, each tied to what the drawing has to prove:
|
Drive, cone and point reviewed together
The Pozi size, the cone angle and the point are reviewed as one set, so a drive that would be too shallow or a cone that would not seat is raised before the die is cut. Basis: Drive, cone and point reviewed as one set. |
Heading, rolling and phosphating in one route
The countersunk head and the Pozi recess are formed in one stroke, the thread is rolled and the parts are phosphated and oiled in the same route. Basis: One route from wire to oiled screw. |
|
Pozi bit tried on the part
The drive is checked for depth and width with a Pozi bit rather than a Phillips one, and the cone is seated in a sample panel. Basis: Pozi bit tried on the first article. |
First article fixes the setting
The first article fixes the wire heat, the drive punch, the cone and the phosphate bath; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these flat head tapping screws from carbon steel wire on single-die headers that cut the countersunk cone and the Pozi recess in one stroke, rolls the half thread and forms the gimlet point, then phosphates and oils the parts. The first part of every run is measured on the cone, driven with a Pozi bit and seated in a sample panel before the batch continues.


|

|
The drive punch is what separates a good Pozi from a screw that will not be opened. The ribs stand in the gaps between the wings and are the smallest features in the head; a punch that is worn leaves them short, and a short rib is a screw that behaves like a Phillips — it cams out early and the user blames the driver. The ribs are checked on the section of the first article.
What decides whether flat head tapping screws pass is the cone, the drive, the thread, the point and the finish. The inspection agreement covers those, and the criteria come from the drawing.

Cone and drive on the projector |

Thread gauged per batch |

Hardness testing against the property class |

Salt-spray testing of the phosphated finish |
The cone is checked for angle, diameter and concentricity, and the drive for depth and rib condition, then turned with a Pozi bit. Using a Phillips bit in the check would measure nothing useful: the two drives accept the same bit at the entrance and behave differently under load.
Seating is checked with a light behind the head, which is the customer’s acceptance test on a flush joint. The thread is gauged per batch, the point is checked for its threaded lead, and the phosphate is read on the batch sample for colour and oil rather than by thickness.
Every shipment of flat head tapping screws is traceable to the wire it was made from and to the phosphate batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the finish. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a flush dark head the first article is also the tone sample, since the whole cone is visible at once. Buyers visit during the process to review samples and to see how the heads are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the phosphating line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
No. Pozi has four extra ribs between the wings, so the bit carries more torque before it slips. A Phillips bit will enter a Pozi recess but rides on the ribs and rounds them.
It gives a matte black that does not build in the cone or the drive, and it holds oil. It is not sacrificial, so it relies on the oil film for protection.
Indoors and oiled, no. Once the oil is washed off or the part is degreased, the steel at the cone and in the drive rusts, even though the part still looks black.
A gimlet point with a threaded lead, for wood, board and soft polymers. It will skate on hard or thin sheet.
From the top of the head, since the head finishes flush. From the start of the cone would give a screw short by the head depth.
Cone angle and diameter, Pozi size, thread size with its length and datum, point form, overall length and the finish.
How a flat head tapping screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the countersink sample
|
→ |
2
Cone, Pozi size and point review
|
→ |
3
First article seated and driven
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the cone angle and diameter, the Pozi size, the thread size with its length and datum, the point form, the overall length and the finish.
|
Cone angle
|
Head diameter
|
Pozi size
|
|
Thread and datum
|
Point form
|
Finish
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com