Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
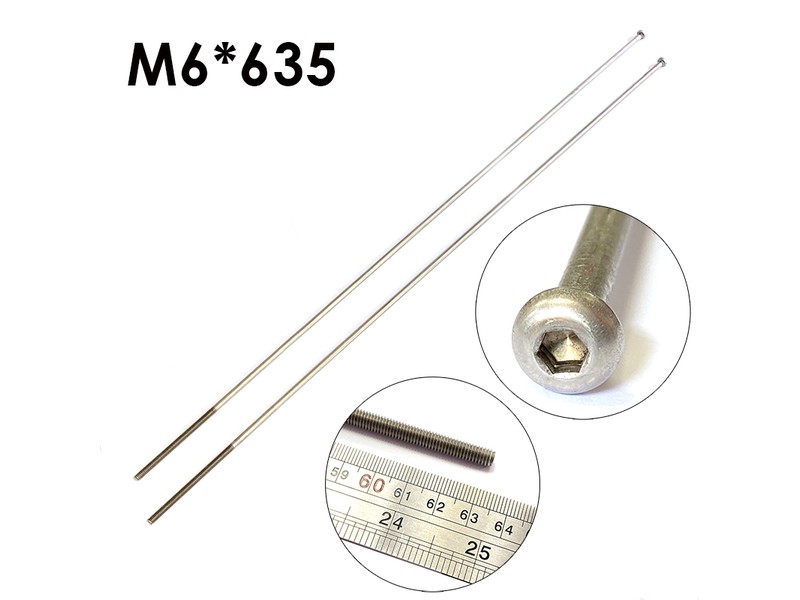
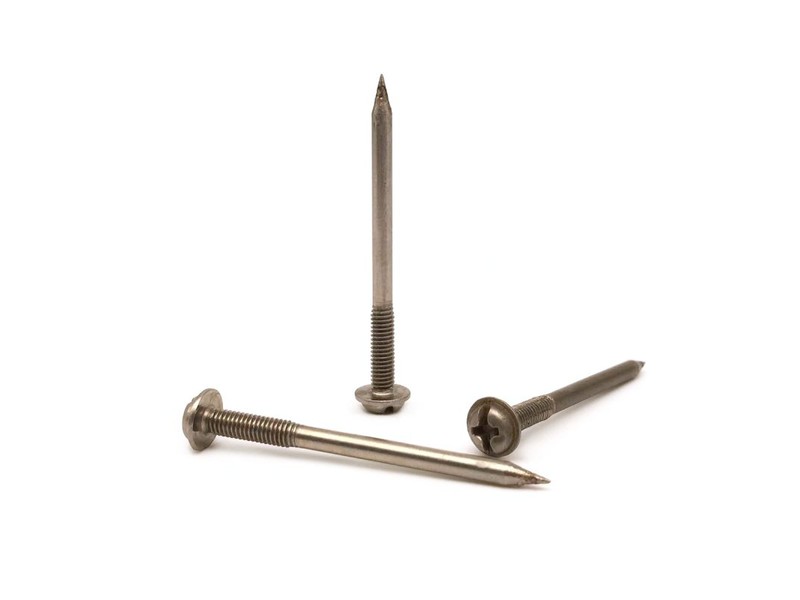
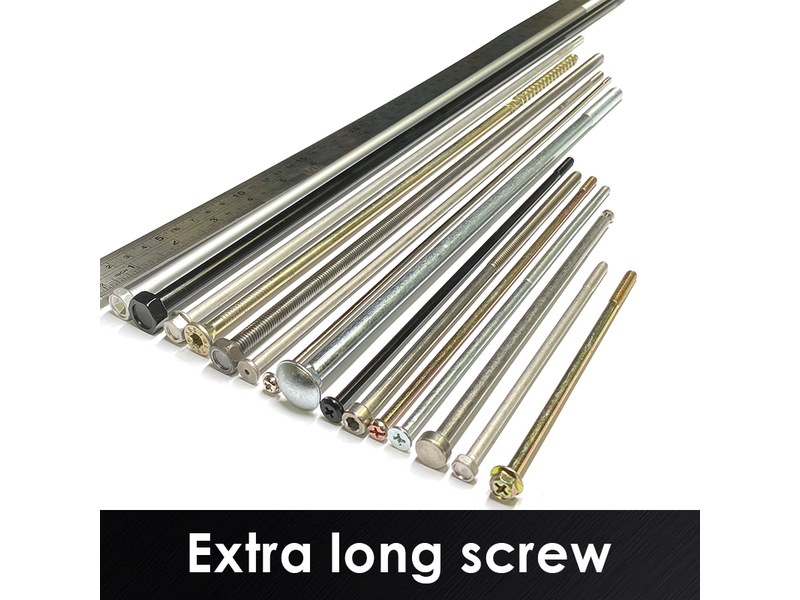
Type:Thin Long Screws Pan Head Cross Phillips
Materials:Steel
Surface treatment:White Zinc Plated
Head Type:Pan Head
Drive:Phillips (cross)
Thread:Self-tapping, half thread
Point:Flat, blunt
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:86
We make thin long screws in white zinc plated steel with a pan head, a Phillips recess, a half thread and a flat self-tapping point, quoting them from M1 to M14. Point type, lengths, shank diameter and pilot hole come from your drawing, and the first article is driven into your material.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Thin long screws are slender fasteners whose diameter is small relative to their length, used where the joint has to reach through a thin wall or a spacer without adding bulk. This one has a pan head, a Phillips recess, a half thread with a flat self-tapping point and a white zinc finish, quoted from M1 to M14 with Number 86.
Thin shank. A small diameter over a long length, so the screw takes little room in the joint.
Half thread. The plain shank runs through the front part and the thread occupies only the last section.
Flat self-tapping point. A blunt, thread-forming end, so the screw does not pierce the material it enters.
White zinc. A bright sacrificial zinc deposit over steel, the general indoor finish.
Thin long screws are used where a joint has to reach through a slim sleeve or a thin wall and there is no room for a larger diameter: instrument covers, small housings, thin plates with a soft part behind. The slenderness is the point of the part, and it is also its limit.
On thin long screws the diameter is the limiting dimension, above the thread and above the head. A thin shank has a small polar section, so it twists more under the same torque and it bends more easily in handling; both mean the driving torque is set by the shank rather than by the joint. The thread at the end is the same size as the shank it grows out of, so it also carries less.
The flat point is a part of the same design. A pointed self-tapping end is made to enter by piercing or by locating in a drilled hole; a flat ended one is made to start in a drilled pilot and to form its thread without piercing anything. On a thin screw that is a deliberate choice, because a point that pierces concentrates force at the tip and can split a small boss.
The half thread follows from the length. The plain shank passes through the front part, which is often a thin panel or a sleeve, and only the last section forms a thread in the far part. That keeps the front bore smooth and puts the clamp where the design wants it, and on a thin screw it also means the plain section is most of the part.
The pan head closes the joint. It is wider than a cheese head and lower than a fillister, so it spreads the clamp on a thin panel without standing far above it. On a thin long screw the head is the only part that touches a visible surface, so its diameter and its flat bearing ring do the work a washer would do on a larger fastener.
White zinc is the finish over all of it. It is thin enough to keep the small thread usable and bright enough to look like a finished part, and it is sacrificial, so a scratch on a thin shank does not immediately become a rust point. On a screw this small the coating is a real fraction of the thread depth, which is why the thread is gauged after plating.
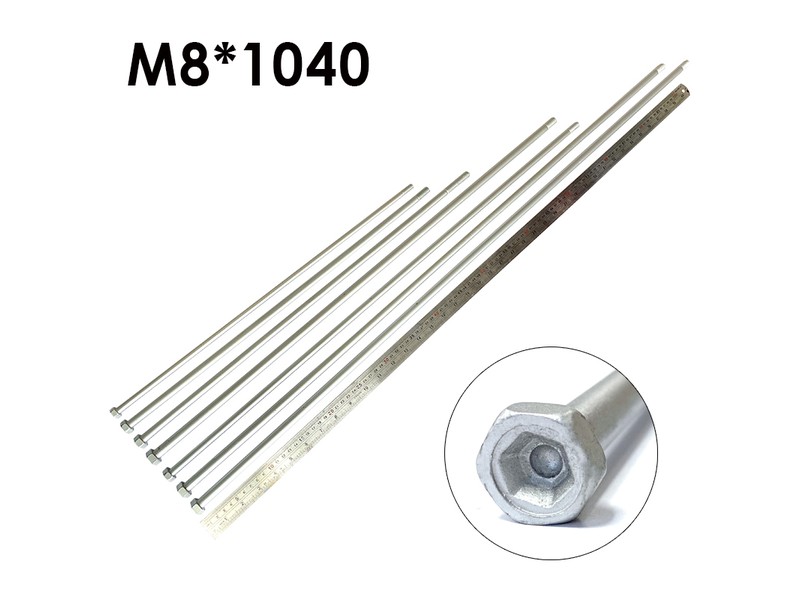
The recorded range is M1 to M14, with thin long lengths made to the drawing. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For thin long screws the quotation carries overall length, threaded length, shank diameter, head diameter and height, point type and the pilot hole.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Pan head, Phillips | Head diameter, height and recess depth |
| Shank | Thin plain section | Diameter and length |
| Thread | Self-tapping, half thread | Thread form, length and crest |
| Point | Flat, blunt | Point diameter and squareness |
| Material | Carbon steel | Grade and heat number on the certificate |
| Finish | White zinc plated | Thickness and gauging after plating |
| Pilot hole | In the far part | Diameter advised per material |
Point type belongs on the drawing as an explicit choice. A flat point starts in a drilled pilot and forms a thread without piercing; a sharp point will pierce thin sheet but concentrates force at the tip, which on a thin screw is where a small boss splits.
Threaded length is quoted from the point end and plain length from the head. On thin long screws the plain section is most of the length, so the division between them is what decides whether the screw clamps the far part or threads the front one.
Three features define the part: the thin shank, the self-tapping half thread and the pan head. The first keeps the joint compact, the second forms its own thread at the far end, and the third spreads the clamp without a washer.
| Feature | What it gives | What it costs |
|---|---|---|
| Thin shank | Little room needed in the joint | Low torque limit; bends in handling |
| Half thread | Front part stays unthreaded | Both lengths must be specified |
| Flat point | Starts in a pilot without piercing | Needs a drilled hole to locate |
| Pan head | Load spread on a thin panel | Stands above the surface |
| White zinc | Bright, sacrificial, gauged after plating | Thin; thread tolerances affected |
The slender shank is the reason the part exists. A joint that has to reach through a slim sleeve or a thin wall has no room for a larger diameter, and a thin screw with a small head is the only way to close it without adding a boss.
The cost is paid in torque. A thin shank twists and a small thread strips, so the driving torque has to be set for the screw, and the joint should be one where a light clamp is enough.
The recorded finish is white zinc plating over carbon steel. It is a thin, bright, sacrificial deposit: thin enough that a small thread still gauges, bright enough to look finished, and sacrificial so that damage to the coating protects the steel around it rather than becoming a rust point immediately.
| Option | How it protects | Effect on thread and head | Typical use |
|---|---|---|---|
| White zinc plated | Sacrificial zinc, bright | Thin build; gauged after plating | Indoor general assemblies |
| Black zinc plated | Sacrificial zinc, dark | Thin build; wear visible | Dark housings |
| Nickel plated | Barrier deposit, bright | Build on a small thread; gauged | Visible consumer parts |
| Black oxide | Conversion film, oiled | No measurable build | Internal mechanisms |
| Stainless alternative | Passive film, no build | Thread as made | Wet and food service |
Where the joint is damp, the coating on a thin screw is not enough: the shank is thin, the coating is thin, and the part that corrodes first is the thread at the far end where nothing can be seen. A stainless body is the specification that changes the outcome.
Where the part is visible and decoratively important, nickel is a harder and brighter finish, but on a thin thread its build has to be allowed for. The thread is gauged after plating, and a small thread with a heavy deposit is a thread that no longer forms properly in the material.
Three assemblies where thin long screws are the fixing:
| Where it sits | The screw reaches through a thin wall or a sleeve into a boss at the far end, where a larger diameter would not fit. |
| When it goes wrong | A shank that is a few hundredths over binds in the sleeve, and the joint cannot be closed. |
| Why it happens | The joint is slim, the parts are thin, and the clamp is light. |
| What we control | Pilot hole agreed; first article assembled through the sleeve. |
| Where it sits | The screw holds a cover on a thin panel where the head must spread load without a washer and the reach is set by the case depth. |
| When it goes wrong | The panel dishes at a narrow head, or the screw strips in the far boss before it is tight. |
| Why it happens | The panel is thin, the head is visible, and the far part is soft. |
| What we control | Head diameter and thread form checked; first article fitted. |
| Where it sits | The screw passes through a thin plate and forms a thread in a plastic or light-alloy part behind it. |
| When it goes wrong | The float-ended point does not start, and the screw cross-threads instead of forming. |
| Why it happens | The joint is small, the far part is soft, and the point has to locate in a pilot. |
| What we control | Point diameter and pilot hole checked; first article driven. |
Four reasons that matter on a slender part, each tied to what the drawing has to prove:
|
Point, lengths and pilot agreed
Point type, threaded length, plain length, shank diameter and pilot hole are agreed as a set, because on thin long screws each one changes the joint. Basis: Point, lengths and pilot agreed. |
Headed, threaded, plated in one route
The pan head is formed, the half self-tapping thread rolled and the flat point cut, then the parts are white zinc plated within one route. Basis: One route from wire to plated screw. |
|
Shank and point measured
The shank is checked for diameter along its length and the point for diameter and squareness, because both are fits on a thin part. Basis: Shank and point measured. |
Driving torque recorded
The driving torque into the customer material is recorded from the first article, so a repeat order does not strip at assembly. Basis: Driving torque recorded. |
Shi Shi Tong forms thin long screws on single-die headers that form the pan head and cut the Phillips recess in one stroke, draws the thin shank, rolls the half self-tapping thread and cuts the flat point before white zinc plating. The first part of every run is measured on head, shank diameter, overall length, thread length and point before the batch continues.


|

|
A thin long blank is the least forgiving thing on a heading line. It has to be held over most of its length with very little material to grip, and any misalignment shows as a head that runs off the axis or a shank that is pushed into a slight set; the screw then measures correctly and will not pass the sleeve.
What decides whether thin long screws pass is the point, the thread, the shank and the head. The inspection agreement covers those, and the criteria come from the drawing.

Point and thread on the projector |

Thread and point checked |

Hardness checked on the wire |

Coating proved by salt spray |
The point is checked for diameter and for squareness to the axis, the thread for form and length, and the shank for diameter along its length. The head is measured for diameter, height and recess depth, and the coating for thickness.
The first article is driven into the customer material with the driving torque recorded. A thin screw that needs more torque than the assembly station can give will twist or strip in production, and only the drive test shows it.
Every shipment of thin long screws is traceable to the wire it was made from and to the plating batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the coating. The documents carry the drawing revision and the batch number, so a repeat order keeps the same point, lengths and finish.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On thin long screws the first article is driven into the customer material, because the thread is formed there and nowhere else. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the point grinding station can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
A flat point starts in a drilled pilot and forms a thread without piercing; a sharp point pierces thin sheet but concentrates force at the tip.
The shank has little material, so it takes part of the driving torque as twist. The joint torque is set by the shank, not by the material.
The plain shank passes through the front part, so a thin sleeve or panel is not threaded on the way to the far part.
It is thin and sacrificial, which is right indoors. Outdoors the thread corrodes first because nothing can reach it.
Yes, if the shank diameter is a sliding fit. A few hundredths over is a screw that binds halfway through.
Overall length, threaded length, shank diameter, head diameter and height, point type, the grade and the finish.
How a thin long screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the material it enters
|
→ |
2
Point, lengths and pilot hole agreed
|
→ |
3
First article driven with recorded torque
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the overall length, threaded length, shank diameter, head diameter and height, point type, the grade and the finish.
|
Overall length
|
Threaded length
|
Shank diameter
|
|
Head height
|
Point type
|
Pilot hole
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com