Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
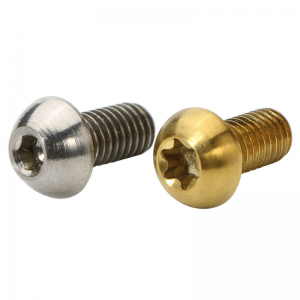
Type:Pan Head Torx Screws
Materials:Steel
Surface treatment:Dacromet
Head Type:Pan Head
Drive:Torx Recess
Thread:Self Tapping Thread
Point:Blunt Flat Point
Forming:Single Die Heading + Serrated Face
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:516
We make pan head Torx screws in Dacromet coated steel, a self-tapping screw with a serrated head face, a six-lobe recess and a blunt point, quoting them from M1 to M14. Coating, thread, teeth and pilot hole come from your drawing, and the first article is driven into your own sheet.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Pan head Torx screws are self-tapping screws with a domed head, a ring of teeth under the rim, a six-lobe star recess and a Dacromet coating. The thread forms its own thread in the hole, the teeth key the head against loosening, and the coating is there for a steel joint that will see weather. This family is quoted from M1 to M14 with Number 516.
Pan head with teeth. A low dome and a wide bearing face, with shallow serrations that press into the panel.
Torx recess. Six lobes that hold the bit under load, so the teeth can be driven into contact.
Self-tapping thread. A coarse thread with a sharp crest, forming its own thread in a drilled or punched hole.
Dacromet. A zinc-aluminium flake coating, thicker than zinc plating and made for outdoor steel joints.
In use pan head Torx screws are chosen for a steel joint that will sit outdoors and be assembled once, where the coating has to outlast the paint and the head must not work loose.
Zinc plating is a few microns thick. Dacromet — a zinc-aluminium flake layer applied and cured — is several times that, and on a self-tapping screw the difference matters because the thread has to fit a hole it has not yet formed. The coating sits on the crest of every thread, which is exactly the part that does the cutting, so a Dacromet screw starts life with a thicker crest than the same screw in zinc.
On pan head Torx screws the consequence is straightforward: a coated self-tapping screw needs a slightly larger pilot hole, or it needs more torque to drive. If the hole was developed on a zinc-plated screw, the Dacromet version will feel tight, and in a thin panel or a brittle material it will distort the hole instead of forming a thread. That is a design change dressed as a finish change.
On pan head Torx screws the coating is worth that complication where the joint is outside. It resists weather far better than zinc plating and it does not produce the white corrosion product that zinc does, which matters on a visible steel structure. On an indoor assembly it is usually more coating than the job needs, and the standard zinc version is cheaper and easier to drive.
The serrated face is the second locking element. The teeth are shallow, and they only key if the screw is driven until the head face meets the panel — which in turn depends on the torque being enough to seat the head without stripping the sheet. That is why a star recess belongs on this part: it lets the head be driven to contact without cam-out, so the teeth do the job they were formed for.
The blunt flat point says the hole is formed, not found. A screw with this point is not going to start on a mark by hand; it is driven into a punched or drilled hole, usually in a jig or on a line. That is a reasonable trade, because the same geometry that will not self-start also will not wander, and the thread goes in square.
The recorded range is M1 to M14, covering M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For pan head Torx screws the quotation carries head diameter and height, tooth depth, recess size, thread and length, and the coating, because the coating thickness is part of the fit.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Pan head with serrated face | Head diameter, height, tooth depth |
| Recess | Torx, six-lobe star | Recess size and depth |
| Thread | Self-tapping, coarse pitch | Pitch and major diameter, gauged |
| Point | Flat, blunt with chamfer | Point diameter and chamfer |
| Coating | Dacromet, zinc-aluminium flake | Coating thickness and adhesion |
| Length | Under the head | Measured on the shop plate |
The pilot hole has to be quoted with the coating. A hole that suits a zinc-plated screw is too small for the Dacromet version of the same screw, and the symptom is a joint that drives hard and then strips when the operator pushes. Where the customer has an existing hole, the first article is driven into it before the batch is made.
Tooth depth is a smaller trade but worth writing down. Deeper teeth hold better and mark a painted panel; shallow teeth are gentler and rely on the torque reaching the seat. On a visible panel the shallow version is the sensible one.
Three features define this part: the Dacromet coating, the serrated face and the star recess. The first is why the part exists outdoors, the second stops it coming loose, and the third is what lets the second work.
| Feature | What it gives | What it costs |
|---|---|---|
| Dacromet coating | Weather resistance on steel | Thicker on the thread; hole must suit |
| Serrated face | Mechanical key at the head | Marks paint and soft panels |
| Torx recess | Drive to the seat without cam-out | Exact bit required |
| Self-tapping thread | No nut or tapped hole | Higher torque than a machine screw |
| Blunt point | Square entry into a formed hole | Will not start without one |
On pan head Torx screws the combination is aimed at one job: a steel or sheet joint that lives outside, assembled once, and expected to stay tight. Each feature does a part of that, and none of them is decorative. On an indoor joint the same screw works, but it is more than the job needs and it drives harder than a plain zinc part.
The limit is the sheet. A serrated head bites into whatever is under it, and in thin material the bite reduces the clamp area. Where the panel is thin, a flanged or a washer-faced head spreads the load better; where it is thick enough to take the teeth, the locking is a genuine benefit.
The recorded coating is Dacromet, a zinc-aluminium flake layer cured onto the steel. It is thicker than zinc plating, free of the white corrosion product that zinc produces, and it survives weather that would take a plated screw apart in a season. The cost is the thickness itself: it has to be allowed for in the thread and in the recess.
| Option | How it protects | Effect on thread and recess | Typical use |
|---|---|---|---|
| Dacromet | Zinc-aluminium flake layer | Thicker; hole and torque adjusted | Outdoor steel structures |
| White zinc | Sacrificial zinc, trivalent | Thin; thread as plated | Indoor general work |
| Blue zinc | Sacrificial zinc | Thin; bright appearance | Cost-driven indoor |
| Black zinc | Sacrificial zinc, dark | Thin; marks dark panels less | Dark equipment |
| Stainless, plain | Passive chromium oxide film | Thread as cut | Washdown and coastal |
Where the joint is outdoors, Dacromet is the right choice on steel because it neither rusts through nor stains the surrounding surface. Where the joint is stainless, the stainless screw is the answer and the coating question disappears — there is nothing to protect.
The coating also affects the recess, since the flake layer is thicker on the lobes than a zinc deposit would be. The recess is checked on the coated part, because a socket that accepts the bit before coating may need a push afterwards.
Three assemblies where pan head Torx screws are the fixing:
| Where it sits | The screw closes a panel or fixes a bracket where the joint is exposed to weather and the coating has to survive without regular attention. |
| When it goes wrong | A zinc-plated screw produces white corrosion, and a plain head works loose on a vibrating frame. |
| Why it happens | The joint is outside, it is assembled once, and the panel is steel. |
| What we control | Coating thickness and adhesion checked, first article driven into the panel. |
| Where it sits | The screw fixes a plate or a rail where the thread forms in the sheet and the head must not work loose under load. |
| When it goes wrong | A plain screw backs out under vibration, and an over-driven screw strips the sheet. |
| Why it happens | The joint vibrates, the sheet is thin, and the fixing is not adjusted. |
| What we control | Tooth depth and thread checked, first article tightened to the specified torque. |
| Where it sits | The screw locates a component where the head sits on a painted surface and the joint is set once in production. |
| When it goes wrong | Deep teeth cut through the paint and start a rust point, and a shallow recess strips at the set torque. |
| Why it happens | The panel is painted, the fixing is hidden, and the torque is defined. |
| What we control | Tooth depth matched to the paint, recess driven with the production bit. |
Four reasons that matter on a coated self-tapping screw, each tied to what the drawing has to prove:
|
Coating and pilot hole agreed
The coating, the thread and the pilot hole are confirmed together, because a Dacromet thread is thicker than a plated one and the hole has to suit the coating that will be delivered. Basis: Coating, thread and hole agreed. |
Head, teeth, thread and coating in one route
The serrated head and the star recess are formed in one stroke, the thread is rolled and the coating is applied as the last step. Basis: One route with the coating last. |
|
Driven into the actual sheet
The first article is driven into a sheet of the customer thickness and pulled, because a coated self-tapping joint behaves differently from a plated one. Basis: First article driven into the sheet. |
First article fixes the setting
The first article fixes the wire, the tooth die and the coating; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these pan head Torx screws from carbon steel wire on single-die headers that form the pan head with its serrated face, cut the six-lobe recess and form the blunt point, roll the self-tapping thread and apply the Dacromet coating as the last step. The first part of every run is measured on the head and thread, driven into a panel and entered into a thread gauge before the batch continues.


|

|
On pan head Torx screws the coating is applied after the thread is rolled, and the flake layer lands on the crest as well as the root. That is why the crest diameter is measured on the finished part rather than on the bare screw: a change in coating thickness from one batch to the next is a change in the fit, and the customer’s panel is the place where it shows.
What decides whether pan head Torx screws pass is the coating, the thread, the teeth and the recess. The inspection agreement covers those, and the criteria come from the drawing.

Thread and teeth on the projector |

Thread gauged per batch |

Hardness checked on the wire |

Salt-spray testing of the coating |
On pan head Torx screws the coating is checked for thickness and adhesion, with attention to the crest of the thread and the inside of the recess, since those are the two places the flake layer decides the fit. The thread is gauged per batch, the teeth are inspected for depth and evenness, and the recess is driven with the production bit.
Every first article is driven into a sheet of the customer thickness. On a coated self-tapping screw that test is the one that catches the real problem: a thread that measures correctly in the gauge room and drives too hard in the panel.
Every shipment of pan head Torx screws is traceable to the wire it was made from and to the coating batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the coating record is kept with the inspection file.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the coating. The documents carry the drawing revision and the batch number, so a repeat order is made to the same coating thickness that was approved.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a coated self-tapping part the first article is driven into the customer’s own sheet, because the coating and the hole decide the joint. Buyers visit during the process to review samples and to see how the parts are formed and coated.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the coating line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
Yes. Dacromet is thicker than zinc plating and sits on the thread crest, so the pilot hole and the driving torque have to suit the coated screw.
On steel joints that live outside. It resists weather far better than zinc plating and does not produce white corrosion.
They press into the panel and key the head against loosening, which is why the screw has to be driven until the face meets the surface.
Because the head must be driven to contact without cam-out for the teeth to work, and because the torque to form a thread in steel is high.
No. The point is blunt, so it needs a punched or drilled hole. What it will not do is wander, which is why it suits jigged assembly.
Thread size and length, point form, head diameter and height, tooth depth, Torx recess size, coating thickness and the pilot hole.
How a pan head Torx screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the sheet it goes into
|
→ |
2
Coating, thread and pilot hole agreed
|
→ |
3
First article driven into your sheet
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size and length, the point form, the head diameter and height, the tooth depth, the Torx recess size and the coating specification.
|
Thread size
|
Length
|
Head diameter
|
|
Tooth depth
|
Torx size
|
Coating
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com