Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
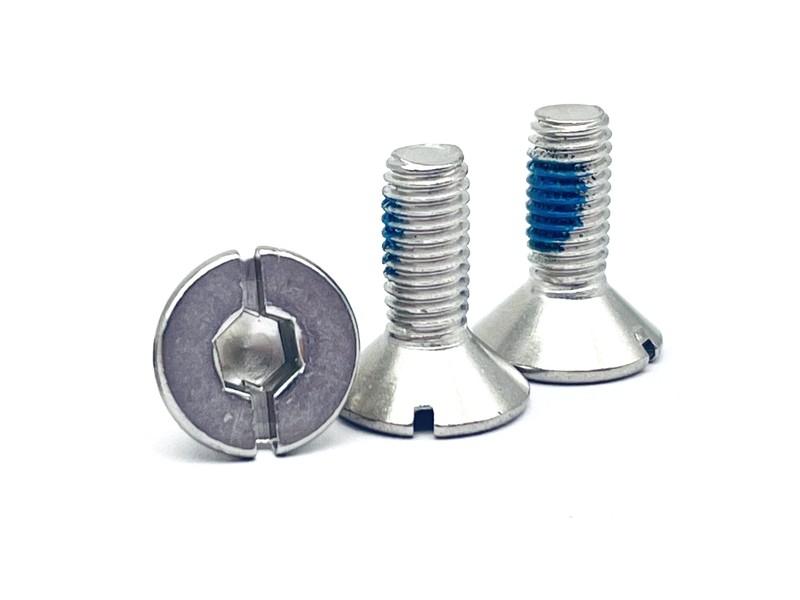
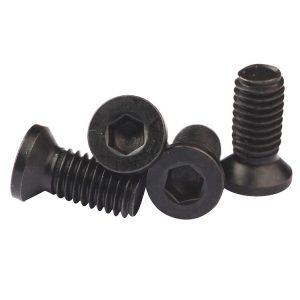
Type:Countersunk Allen Screw
Materials:Aluminum
Surface treatment:Anodized
Head Type:Flat Head
Drive:Allen Socket
Thread:Machine Thread
Point:Blunt
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:801
We make countersunk Allen screws in anodised 6000-series aluminium, a flush head with a hexagon socket and a machine thread, quoting them from M1 to M14. Alloy, thread, torque, cone and finish colour come from your drawing, and the first article is driven into your own thread.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A countersunk Allen screw is a machine screw with a countersunk head and an internal hexagon socket, made here in aluminium with an anodised finish. The head sits flush in a panel, the socket takes the key, and the machine thread runs in a tapped hole or a nut. The alloy is a 6000-series aluminium, and the family is quoted from M1 to M14 with Number 801.
Countersunk head. A 90-degree cone under a flat face, seating in a countersink cut in the panel.
Hexagon socket. An internal hexagon for a key, cut into the head.
Machine thread. A rolled thread for a tapped hole or a nut, ending in a blunt chamfer.
Anodised aluminium. A hard oxide layer grown from the metal itself, which can be dyed, and which does not conduct.
In use countersunk Allen screws in aluminium are chosen where weight or colour drives the design, and the joint they go into is light enough for a soft thread to hold.
Aluminium fasteners are chosen for weight first and for appearance second. A 6000-series screw is roughly a third the weight of a steel one and can be anodised in a colour that matches the panel, which is why it appears on equipment where every gram or every shade matters. What it is not is strong, and the two ways that shows up are both worth designing around.
On a countersunk Allen screw the first is the thread. Aluminium strips at a fraction of the torque a steel screw of the same size will take, and once stripped there is nothing to repair — the boss or the tapped hole is gone. That is why aluminium screws go into joints that are lightly loaded, or into threads that carry a steel or a captive insert, and why the torque on the drawing is the number that matters most.
On a countersunk Allen screw the second is the anodised layer. Anodising is a hard, brittle oxide grown out of the aluminium; it resists wear and corrosion well, but it does not stretch. When the head seats and the cone deforms slightly, the oxide cracks in fine lines, and bare aluminium is exposed at exactly the place where the joint holds water. On a plain aluminium part that is a cosmetic mark; on an anodised one it is a corrosion start.
On a countersunk Allen screw there is also a galvanic consequence. Aluminium is anodic to steel and to stainless, so in a wet joint with a steel panel the aluminium screw or the aluminium panel will corrode first, depending on which is the smaller area. On indoor equipment this never matters; outdoors, the pairing is a decision to make deliberately.
The colour is the other reason the part exists, and it is a legitimate one. Anodising takes a dye in the same process that grows the oxide, so the head can be black, natural satin, or matched to a coloured housing. That is impossible to do convincingly with plating on steel, and it is why anodised aluminium hardware appears on products where the fixings are part of the finish.
The recorded range is M1 to M14, covering M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For a countersunk Allen screw the quotation carries head diameter and height, cone angle, socket size and depth, the thread and the anodising specification, because the coating thickness enters both the cone and the socket.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Countersunk, 90-degree cone | Head diameter, height and cone angle |
| Socket | Internal hexagon | Socket across flats and depth |
| Thread | Machine thread | Pitch and length, gauged per batch |
| End | Blunt, chamfered | Chamfer cut, not deburred |
| Finish | Anodised | Oxide thickness, colour and sealing |
| Length | Overall, head included | Measured on the shop plate |
Anodising thickness matters more than it would on a plated part, because the oxide grows into the surface as well as out of it: a heavy coating changes the cone and narrows the socket by more than a zinc deposit would. On a small screw that is the difference between a key that fits and one that has to be pushed.
Head height follows the head standard for the thread, and the socket depth follows the head height. Because aluminium cannot take the torque of steel anyway, a shallower socket on this part is less of a limitation than it would be on a steel screw — the thread gives first in almost every case.
Three features define this part: the aluminium body, the anodised finish and the flush countersunk head. The first is the weight, the second is the colour, and the third is the reason it is used on visible panels.
| Feature | What it gives | What it costs |
|---|---|---|
| Aluminium body | About a third the weight of steel | Thread strips at low torque |
| Anodised finish | Hard, coloured, non-conductive | Brittle; cracks at the cone |
| Countersunk head | Flush line, self-centring | Needs a matching countersink |
| Hexagon socket | Compact drive with a common key | Shallow socket in a thin head |
| Machine thread | Repeatable clamp in a tapped hole | Needs a nut or a tapped insert |
On a countersunk Allen screw the non-conductive property of anodising is worth noting, because it is sometimes the reason for the part and sometimes a surprise. An anodised screw does not make an electrical connection through its head; where the joint is meant to earth through the fastener, the anodised layer has to be removed at the contact or a different material used.
The soft thread is the feature that sets the assembly. A short key and a hand are usually enough, a torque setting is better, and a power driver with no clutch is how aluminium threads are destroyed. Where the joint has to take real load, the aluminium screw is the wrong fastener and a steel or stainless one is the right answer, whatever the weight budget says.
The recorded finish is anodised aluminium. The oxide is grown from the metal, is harder than the base alloy, and takes a dye, so the finish can be a specific colour rather than a generic grey. It is also brittle and non-conductive, and it is a surface conversion rather than an added layer, which means a deep scratch has taken the protection with it.
| Option | How it protects | Effect on cone and socket | Typical use |
|---|---|---|---|
| Anodised, clear | Hard oxide, natural tone | Thin build; socket as cut | Visible natural aluminium |
| Anodised, black | Hard oxide with dye | Thin build; colour throughout | Dark panels and housings |
| Anodised, colour | Hard oxide with dye | Colour matched to the housing | Consumer and display products |
| Chromate conversion | Thin conductive film | No measurable build | Joints needing conductivity |
| Aluminium, plain | Bare alloy | As machined | Internal, non-visible parts |
On a countersunk Allen screw the choice between anodising and a conversion coating is often made on conductivity rather than on corrosion. An anodised part insulates; a chromate conversion coat leaves the surface conductive and is the finish to use where the fastener is part of an earth path or a heatsink joint.
Whatever is chosen, the finish on an aluminium screw should not be expected to protect the thread. Once the thread is stripped or the cone cracked, the oxide is gone at that point, and there is no sacrificial metal behind it to help.
Three assemblies where countersunk Allen screws are the fixing:
| Where it sits | The screw closes a panel or fixes a bracket where weight matters and the joint is lightly loaded. |
| When it goes wrong | An aluminium thread strips at a torque a steel one would take, and the boss cannot be repaired. |
| Why it happens | The joint is light, the weight budget is tight, and the thread is short. |
| What we control | Thread gauged per batch, first article driven to the specified torque. |
| Where it sits | The screw fixes a panel where the fixing is visible and the colour has to match the housing. |
| When it goes wrong | A deep scratch takes the oxide with it, and a head that is not flush leaves a bright ring. |
| Why it happens | The finish is decorative, the panel is anodised, and the fixing is on show. |
| What we control | Colour matched to a sample, cone and head checked after coating. |
| Where it sits | The screw fixes a board or a heatsink where the fastener is non-magnetic and must not add weight. |
| When it goes wrong | An anodised screw insulates a joint that was meant to conduct, and aluminium against steel corrodes in damp air. |
| Why it happens | The joint is electrical or thermal, the part is light, and the environment is dry. |
| What we control | Finish conductivity confirmed, first article fitted to the assembly. |
Four reasons that matter on a soft metal fastener, each tied to what the drawing has to prove:
|
Torque and thread agreed
The alloy, the thread and the torque are confirmed together, because an aluminium thread strips well below the torque a steel screw of the same size would accept. Basis: Torque set from the thread, not the head. |
Head, socket and thread in one route
The countersunk head and the hexagon are formed in the heading stroke, the thread is rolled and the anodising is applied as the last step. Basis: One route with anodising last. |
|
Cone and socket checked after anodising
The first article is checked on the anodised part, because the oxide grows into the surface and changes both the cone and the socket. Basis: First article checked after anodising. |
First article fixes the setting
The first article fixes the wire, the die and the anodising bath; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these countersunk Allen screws from aluminium wire on single-die headers that cut the countersunk head and the hexagon in one stroke, rolls the machine thread to a blunt chamfered end and anodises the finished parts. The first part of every run is measured on the head and socket on the anodised screw and driven with the production key before the batch continues.


|

|
On countersunk Allen screws aluminium is a different working material from steel or brass, and the thread rolling shows it. It is soft enough that a thread roll can leave a smeared crest if the lubrication is wrong, and hard enough after cold working that a second pass is not possible. The roll setting is found once per alloy lot and then held, and the first article is checked for a clean crest before the batch runs.
What decides whether countersunk Allen screws pass is the socket, the cone, the thread and the anodising. The inspection agreement covers those, and the criteria come from the drawing.

Head and socket on the projector |

Thread gauged per batch |

Hardness checked on the alloy |

Corrosion testing of the finish |
On countersunk Allen screws the cone is checked for angle and the head for diameter and height after anodising, because the oxide changes both. The socket is checked across flats and for depth and driven with the production key, and the thread is gauged per batch, with the strip torque recorded on the first article rather than a bare dimensional pass.
The anodising is checked for thickness, colour and sealing, with attention to the cone, where the oxide is most likely to crack when the head seats. Where the part is meant to conduct, the finish is specified as a conversion coating instead and the conductivity of the face is part of the acceptance.
Every shipment of countersunk Allen screws is traceable to the aluminium wire it was made from and to the anodising batch. The alloy and the lot number are recorded on the mill certificate supplied with the parts, and the anodising record is kept with the inspection file.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the mill certificate for the wire, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the anodising. The documents carry the drawing revision and the batch number, so a repeat order is made from the same alloy and the same finish.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On an aluminium part the first article is driven at the joint torque into the customer’s own thread, because the thread is the limit. Buyers visit during the process to review samples and to see how the parts are formed and finished.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the anodising line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
Weight and colour. An aluminium screw is about a third the weight, and it can be anodised to a specific shade. It is not a strength substitution.
Much less than a steel screw of the same size, and the exact figure belongs on the drawing. A thread that strips cannot be repaired.
The oxide is hard but brittle. When the cone deforms as the head seats, fine cracks open and expose bare aluminium where water collects.
Dry and indoors, yes. Outdoors, aluminium is anodic to steel and will corrode first, so the pairing needs a coating or an isolating washer.
No. The oxide insulates. Where the joint has to earth through the fastener, use a conversion coating or remove the oxide at the contact.
Head diameter and height, cone angle, socket size and depth, thread size and length, the alloy, and the finish with its colour and thickness.
How a countersunk Allen screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the joint torque
|
→ |
2
Alloy, thread, cone and colour agreed
|
→ |
3
First article driven into your thread
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size and length, the head diameter and height, the cone angle, the socket size, the alloy and the finish with its colour.
|
Thread size
|
Length
|
Head diameter
|
|
Cone angle
|
Alloy
|
Finish colour
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com