
Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
Type:Custom titanium screws
Materials:TA1 / Grade 1, TA2 / Grade 2, TC4 / Grade 5
Surface treatment:Finish selected for titanium grade and application
Head Type:Custom head and drive geometry, subject to drawing review
Diameter:M1.6–M12; length and geometry assessed separately
Thread:Per drawing - rolled or cut to suit the geometry
Forming:Per drawing - turning, heading and thread production
Shi Shi Tong is a titanium screw manufacturer producing custom titanium screws in TA1 (Grade 1), TA2 (Grade 2) and TC4 (Grade 5), from M1.6 to M12, machined at titanium-specific speeds and finished natural, passivated or anodized to a colour sample. Grade, thread, head geometry and finish are made to your drawing.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A titanium screw manufacturer produces fasteners in titanium alloys rather than steel, for joints where weight, corrosion or a non-magnetic material decide the choice. Titanium is about half the weight of steel at similar strength, it resists chlorides and seawater, and it does not take a magnetic signature — but it also galls, machines slowly and costs more, so the part has to be designed around those limits.
Weight where it is carried. On a titanium screw manufacturer’s drawing, weight shows up as a smaller head, a thinner shank or a hollow feature that would be impossible in steel. The saving is real only when the screw is part of a moving assembly or a component that is carried, which is why titanium parts usually appear in clusters.
Corrosion and non-magnetic service. Titanium keeps its oxide film in seawater and in many chemical environments, and it is effectively non-magnetic. That is why titanium screws turn up on marine equipment, in medical instruments and in equipment that has to pass a magnet check.
What titanium changes in the shop. Titanium work-hardens, conducts heat poorly and galls against itself, so thread rolling, thread cutting and even deburring are slower than in stainless. A titanium screw manufacturer plans the route around heat, tool wear and galling, not only around the drawing.
Together these decide whether a titanium part is worth it: the weight and corrosion have to matter enough to pay for the slower route, and the joint has to be designed so the screws are not over-torqued or repeatedly re-driven.
The grade is the first line on the drawing. TA1 (Grade 1) is commercially pure, soft and highly formable, used where corrosion resistance matters more than strength. TA2 (Grade 2) is the common general-purpose pure grade. TC4 (Grade 5) is the alpha-beta alloy with much higher strength, and it is the grade most structural titanium screws are made from.
A titanium screw manufacturer changes the process as well as the strength when the grade changes. TA1 and TA2 form and roll more easily; TC4 is harder, springier and more abrasive on tooling, so a titanium screw manufacturer will plan more passes, more cooling and shorter tool life for the same geometry. A drawing that names the alloy but not the grade leaves the shop to choose between a part that forms and a part that holds load.
Titanium also galls against itself and against stainless. Threads that will be assembled and disassembled repeatedly are often specified with a dry-film lubricant, a different coating or a controlled thread class, and the drawing says which. That is a joint decision, not a finishing detail.
Custom titanium screws are quoted from M1.6 to M12, with length and geometry assessed part by part. Where a long titanium screw is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission, because the machining route and the material cost change with length.
| Item | How it is defined | What we control |
|---|---|---|
| Diameter and thread | M1.6 to M12, metric or per drawing | Thread gauged per batch; class per drawing |
| Length | Overall and thread length from a stated datum | Datum agreed on the drawing; checked on the first article |
| Head and drive | Custom geometry reviewed against the drawing | Recess checked with the matching driver |
| Concentricity | Head and shank on one axis | Turned in one set-up where the drawing requires it |
| Surface | Natural, anodized colour or specified finish | Finish checked against the accepted sample |
Every combination of diameter, length and head form is checked against the drawing before a quotation is issued. That is how a titanium screw manufacturer prices a part: route first, then the part. A titanium screw manufacturer quotes the route as well as the part, because the same screw in TA2 and in TC4 will not cost the same or run at the same speed.
Length and thread position are measured from the same datum, and the recess is checked with the matching driver. The first article is measured on every dimension before the batch continues.
Titanium is machined slowly for a reason. It conducts heat poorly, so heat stays at the cutting edge instead of going into the chip; it work-hardens, so a dull tool makes the next pass harder; and it galls, so a thread rolled too fast can tear instead of forming. A titanium screw manufacturer sets speeds, feeds and coolant around those three facts.
For a titanium screw manufacturer, threads are the most sensitive feature. Rolling is preferred where the geometry allows, because it forms the thread instead of cutting it and leaves a better root; cutting is used where the thread has to run out into a relief or where the diameter is small. In both cases the thread is checked after the finish, because coatings and anodizing change a titanium thread by a few microns.
Deburring is not cosmetic on titanium. A burr at a recess edge or a thread start will gall the mating part on the first assembly, and titanium burrs are tougher than steel ones. The part is deburred as a process step, then cleaned and finished before the gauges.
Titanium can be supplied natural, with the oxide film it forms in air, or anodized to a colour. Titanium anodizing is a thin oxide layer grown at low voltage; the colour comes from the film thickness rather than a dye, and it can shift with voltage and surface condition, so the colour is matched to a physical sample.
| Finish | How it protects | Effect on thread and recess | Typical use |
|---|---|---|---|
| Natural titanium | Air-formed oxide film | No dimensional change | Industrial joints where colour is not required |
| Anodized colour | Thin oxide layer, colour by film thickness | Builds a few microns; thread re-checked | Visible parts and colour-coded assemblies |
| Passivated / cleaned | Surface cleaned, oxide restored | No dimensional change | Parts stored or handled before assembly |
| Dry-film lubricant | Bonded lubricating layer | Adds a thin film; thread gauged after | Threads that are assembled repeatedly |
| Black oxide (steel) | Conversion coating on steel equivalents | Minimal build-up | Steel parts in the same assembly |
Salt-spray and corrosion testing are agreed per project and written on the drawing; titanium is usually tested for the environment it will see, not for a generic rating. On a titanium screw the finish is chosen with the galling behaviour of the mating part in mind, because a coating that looks right but increases friction in the thread can make the joint worse.
Packing protects the head and the thread. Screws are packed in layers with the heads up, and the label carries the batch, grade and finish reference.
Three environments where a titanium screw manufacturer is asked for weight, corrosion or a non-magnetic part — and where a titanium screw manufacturer has to prove the joint still works — with what the screw has to do instead:
Marine and offshore equipment
|
Offshore equipment – titanium hardware in salt air |
Medical and laboratory instruments
|
Instruments – non-magnetic hardware near sensors |
Chemical processing and semiconductor equipment
|
Process equipment – titanium hardware in aggressive chemistry |
Four reasons that matter when you choose a titanium screw manufacturer, each tied to what the drawing has to prove:
|
Grade and route reviewed first
The grade, the geometry and the assembly torque are reviewed together before tooling, so a part that would gall or over-stress its thread is raised before the first bar is cut. Basis: Drawing, grade and joint reviewed before machining. |
Slow speeds, controlled thread production
Titanium is machined at speeds set for heat and tool wear, and threads are rolled or cut according to the geometry rather than the default route. Basis: Titanium-specific speeds, feeds and thread route. |
|
Threads and recess gauged after finishing
The thread is checked after anodizing or coating and the recess with the matching driver, so the part that arrives can be assembled without re-cutting. Basis: Thread and recess gauged in the finished condition. |
First article to repeat production
The first article fixes the drawing revision, grade and heat, set-up and finish reference; repeat orders are compared against that record. Basis: First article and finish reference signed off before the batch. |
As a titanium screw manufacturer, Shi Shi Tong produces these parts from titanium bar or wire through turning, heading and thread production chosen for the geometry and grade. TC4 parts take more passes and shorter tool life; TA1 and TA2 form more easily. The first part of every run is checked against the drawing and the driver before the batch continues.
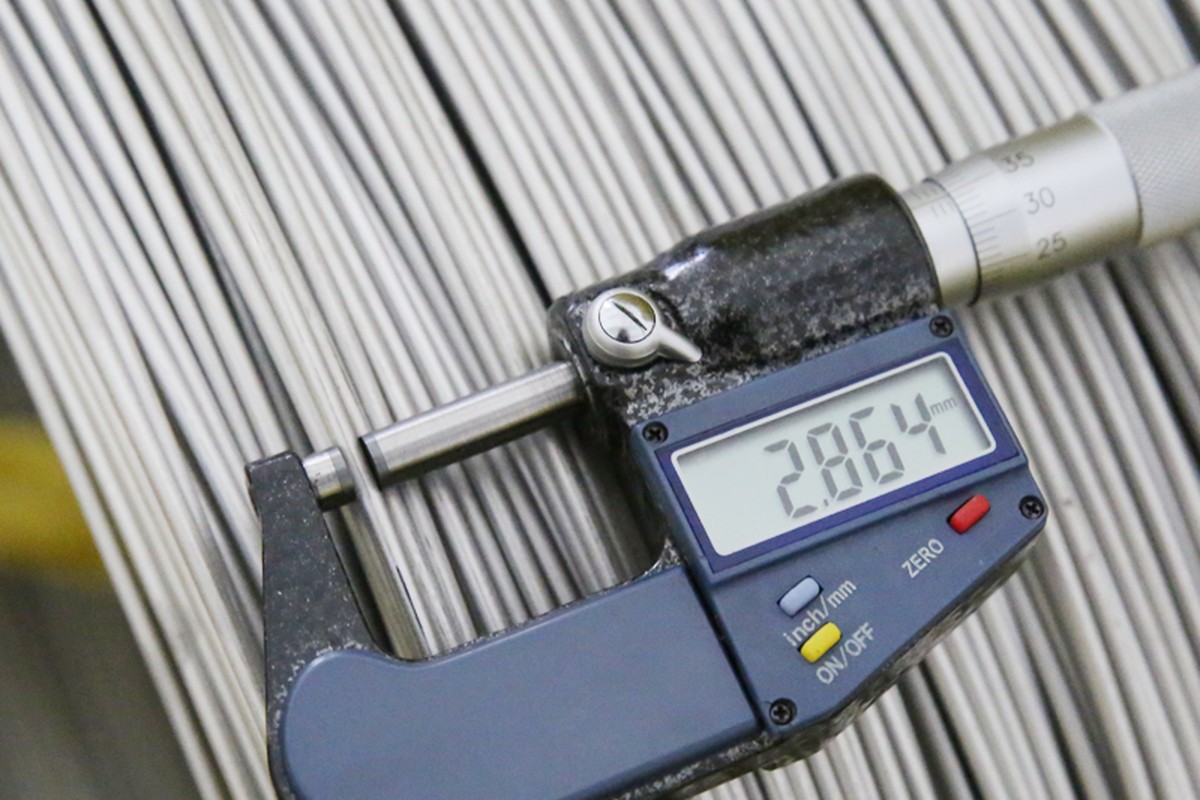
Material checked before the bar is cut |
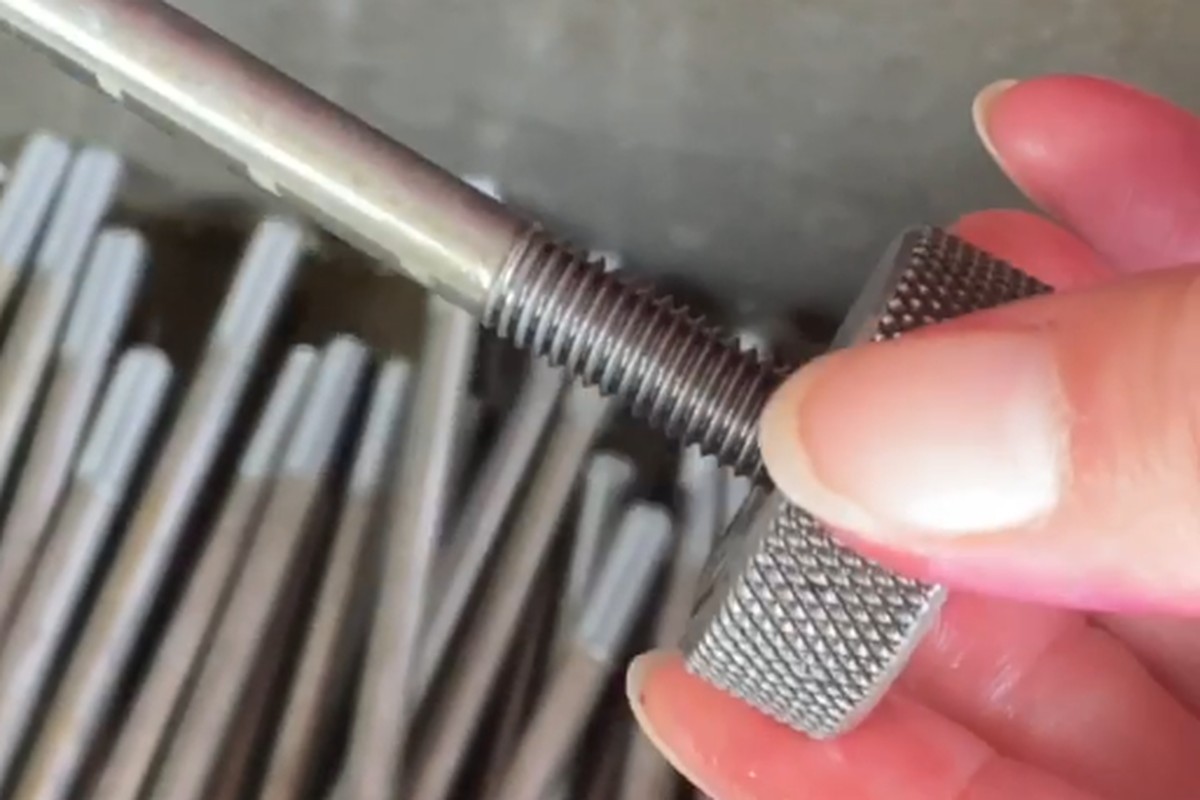
Threads gauged after finishing |
Between runs the machine is set to the drawing; the set-up and the grade are recorded with the first article, which is how a titanium screw manufacturer keeps a repeat order identical to the sample. Finished parts are checked again after anodizing or coating, so the record covers both the machined and the finished condition, and a repeat order can be compared with what was approved.
What decides whether a titanium screw passes is not its colour or its weight: it is the diameter and length on the drawing, the thread class, the recess fit against the driver, and the finish in the condition it ships in. The inspection agreement covers those, and the criteria come from the drawing.

Thread gauging after finishing |

Head and recess profile on the projector |

Hardness testing where the grade requires it |

Corrosion testing of the agreed finish |
Each batch is recorded against the drawing revision: dimensions and thread from the first article, the recess checked with the driver, and the finish checked against the accepted sample. If a gauge or the finish check fails, the parts back to the last good setting are held and re-checked before anything ships.
Any outside test the drawing calls for is commissioned with the batch, and the report is filed under the same number as the inspection record.
Every titanium screw shipment from this titanium screw manufacturer is traceable to the bar or wire it was made from. The grade, heat number and standard are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the finish. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing and grade review, first-article approval, then batches checked against that sample. Buyers visit during the process to review samples and to see the machining and finishing steps their parts will go through.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
As a titanium screw manufacturer working from drawings, we invite buyers and quality engineers for sample review, process discussion and supplier audits; the visit is arranged around production so the turning cells and the finishing line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
TA1 (Grade 1), TA2 (Grade 2) and TC4 (Grade 5) are the grades quoted on this page, from M1.6 to M12. The grade comes from the drawing, and it changes the machining route as well as the strength.
Titanium machines slowly, work-hardens and galls, so a titanium screw takes more passes, more cooling and shorter tool life than the same screw in steel. The material cost is higher as well, and the route is planned around that.
Titanium can gall against itself and against stainless when a joint is assembled and taken apart repeatedly. The drawing can specify a dry-film lubricant, a coating or a controlled thread class to manage it.
Yes. Titanium anodizing grows a thin oxide layer whose thickness sets the colour; it is matched to a physical sample because the colour shifts with voltage and surface condition.
Custom titanium screws are quoted from M1.6 to M12, with length and geometry assessed part by part. Where a long screw is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
Grade, thread size and class, length and datum, head and drive geometry, finish or colour, assembly torque, and whether the joint is assembled repeatedly.
How a titanium screw manufacturer takes your drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
Grade and DFM review
|
→ |
3
First article approval
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a custom titanium screw quotation, send the drawing with the grade, thread size and class, length and datum, head and drive geometry, finish or colour, and the assembly torque. Grade and routing are confirmed with you before production.
|
Titanium grade
|
Thread size and class
|
Length and datum
|
|
Head and drive geometry
|
Finish or colour
|
Assembly torque and quantity
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com













