Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
Type:slotted truss head machine screws
Materials:Titanium
Surface treatment:Plain
Head Type:Truss head
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
Drive type:Slotted
Thread:Machine thread
Forming:Single-die cold heading
Number:1618
We manufacture slotted truss head machine screws in titanium with a wide low head and a single slot, from M1 to M10, plain and made to drawing. Head diameter, slot width and depth, thread class and grade are checked before the batch runs.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
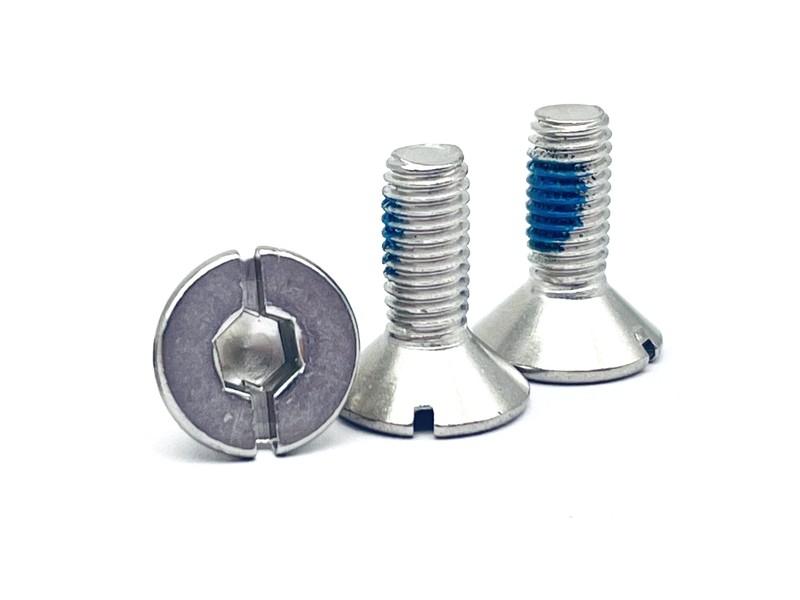
A slotted truss head machine screw is a machine screw with a wide, low head and a single slot driven by a flat blade. The one on this page is made in titanium, supplied plain, in sizes M1 to M10, so it is chosen where the joint has to stay light and corrosion resistant and the head has to spread its load over a thin panel.
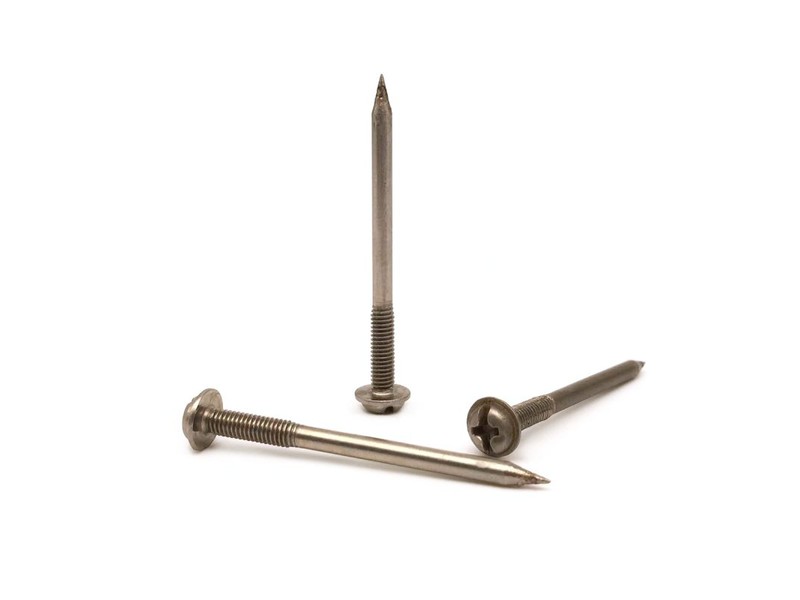
Truss head. The head is wide relative to its height, with a large bearing face that sits on the panel. It spreads the clamp load over thin sheet, plastic or a soft gasket, and it keeps the profile low where a taller head would foul the assembly.
Slotted drive. A single slot takes a flat blade. It is the simplest drive to make and to inspect, and on a small screw it is fast to use; the trade-off is that a blade that is too narrow or too thick cams out and damages the slot.
Titanium body. Titanium is light and resists corrosion without a coating, but it is also softer at the surface than steel. The slot is the feature that shows the difference: a poorly fitting blade deforms the slot edges faster on titanium than on steel.
Together these decide the joint: the truss head bears on the panel, the slot takes the blade, and the titanium body keeps the part light and corrosion resistant.
This screw is formed from titanium wire on a single-die header, thread rolled and supplied plain. The grade comes from the drawing, with TA1 and TA2 the common choices where corrosion resistance matters and TC4 where the screw carries load.
The truss head is formed in the die with its wide bearing face and low profile. Titanium is harder to head than steel, so the die and the press load are set for the grade, and the head is checked for laps or cracks that a steel part would not show.
The slot is cut into the head after heading. Its width and depth are set to the blade on the drawing: a slot that is too narrow will not take the blade, and one that is too wide lets the blade rock and rounds the edges.
Plain titanium keeps the dimensions the process produced. The passive oxide film forms in air without adding measurable thickness, so the thread and the slot stay as they were measured and the part can be assembled without re-checking the blade fit.
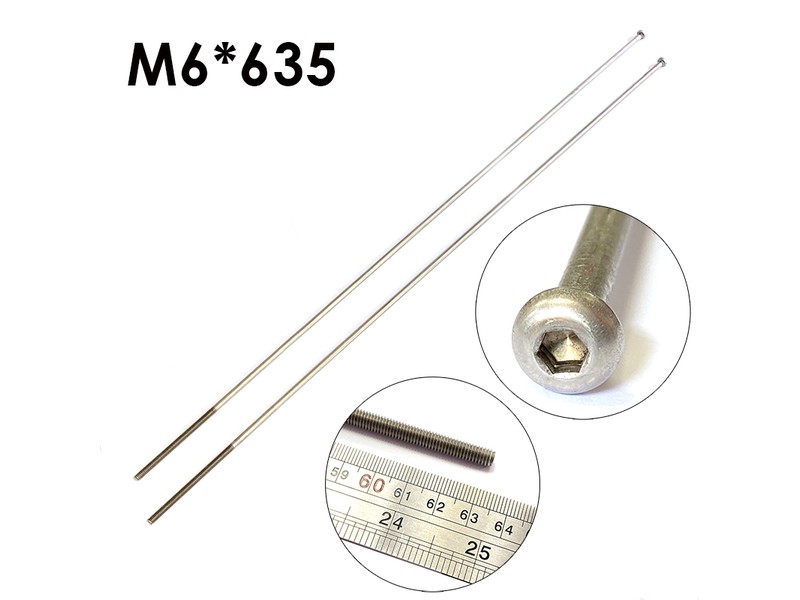
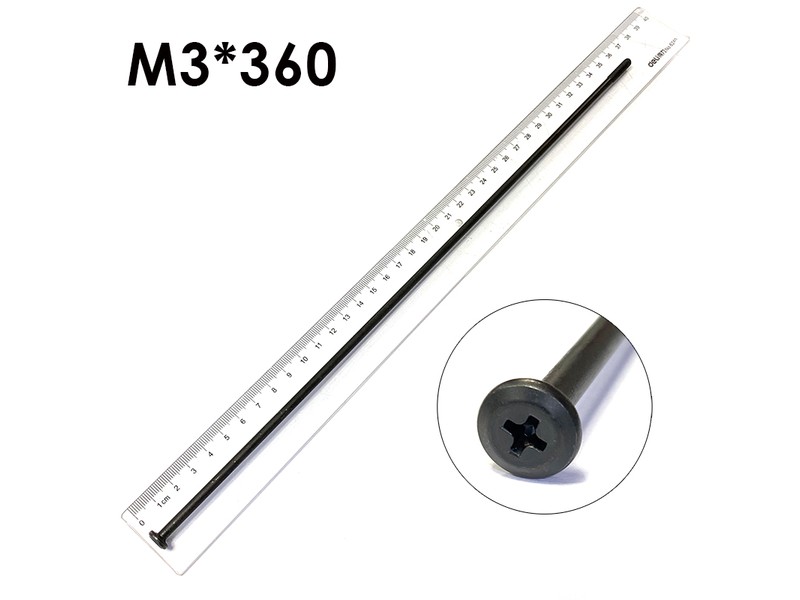
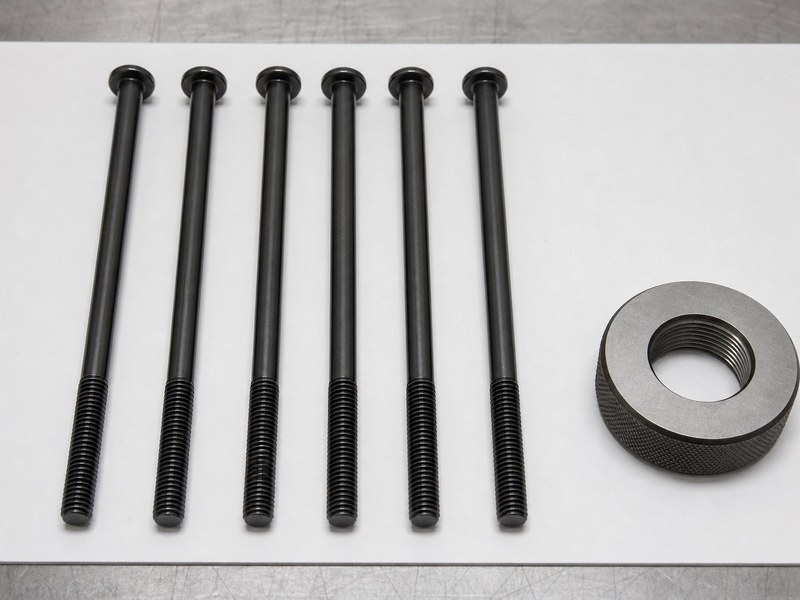
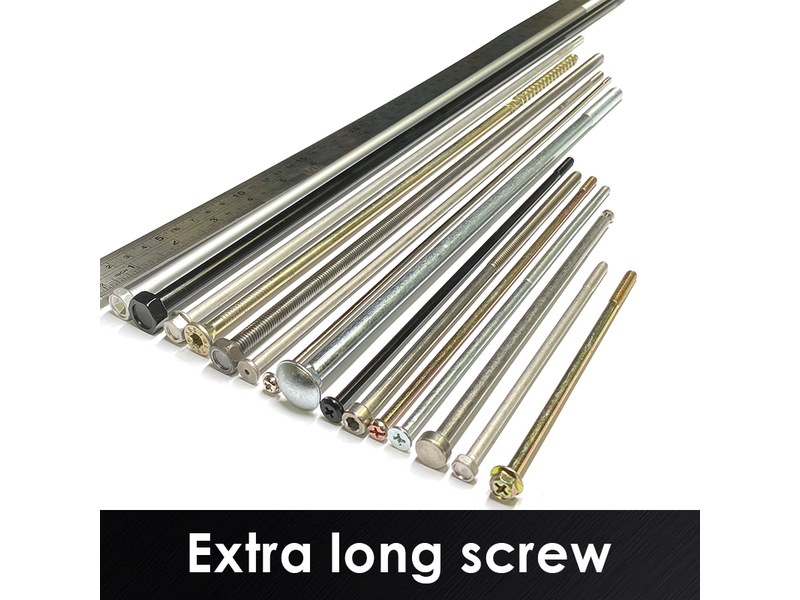
Screws of this type are quoted from M1 to M10 and in lengths to suit the drawing, with the head and slot measured on the projector and the thread gauged. Where a long version is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
| Item | How it is defined | What we control |
|---|---|---|
| Head diameter | The wide truss bearing face | Checked on the projector on the first article |
| Head height | The low profile above the panel | Checked against the drawing |
| Slot width and depth | The blade that drives the screw | Checked with the blade and on the projector |
| Thread size and length | Machine thread to the drawing | Gauged per batch |
| Head edge | The rim that sits on the panel | Checked for burrs on the first article |
| Total length | From the top of the head to the tip | Datum stated on the drawing; measured on the shop plate |
Each size is quoted against the joint it closes. On a thin panel the truss head is what keeps the sheet from denting, and the slot depth is what keeps the blade engaged, so head diameter and slot depth are reviewed together.
Head height is measured from the bearing face and the total length from the top of the head. The batch is checked on the features the process can drift on: slot depth, head diameter and thread class.
The slot is the drive of a slotted truss head machine screw. It is a single straight recess, and it takes a flat blade of a stated width and thickness. The blade has to fill the slot in width and sit on the bottom; a blade that is too narrow cams out, and one that is too thick sits on the edges and rounds them.
On a small screw the slot is also a strength feature. Cutting it removes material across the head, and on a truss head that material is what carries the driving torque. The slot depth is set so the blade engages without the head opening through the top face.
Titanium makes the fit more important. The metal is softer at the surface than steel, so a blade that rocks will deform the slot edges after a few assemblies, and the damage is not visible until the screw is removed and re-driven. The first article is driven with the blade that will be used.
The truss head works with the slot rather than against it. Its wide face gives the blade room to sit flat and its low profile keeps the screw out of the way; the bearing face spreads the load so the head does not dish when the joint is tightened.
This slotted truss head machine screw is supplied plain. Titanium forms its own passive oxide film in air, so the part resists corrosion without plating, and there is no coating to build in the slot or on the thread. The finish is therefore the metal itself, and the inspection is about the surface and the slot rather than about a colour.
| Finish | How it protects | Effect on slot and thread | Typical use |
|---|---|---|---|
| Plain titanium | Passive oxide film forms in air | No build-up; blade fit unchanged | Medical, marine and chemical parts |
| Colour anodized | Thin oxide layer, dyed and sealed | Negligible build-up; blade re-checked | Colour-coded and visible parts |
| Bead blasted | Uniform matte surface | No dimensional change | Parts where glare matters |
| Dry film lubricant | Bonded film that reduces galling | Thin film; thread checked over it | Titanium-to-titanium joints |
| Zinc plated (steel equivalent) | Sacrificial zinc layer | Build-up in slot; blade checked after | Steel parts where weight is not critical |
Salt-spray exposure is agreed per project and written on the drawing; plain titanium is tested in the condition it ships in. Colour anodizing is matched to an accepted sample, because the shade shifts with voltage and alloy.
Packing protects the head and the slot. Titanium parts are light and can rub in a bag, so they are packed in layers, and the label carries the batch, the grade and the finish reference.
Three assemblies where slotted truss head machine screws are chosen for the wide head and the simple drive, and what the screw has to do instead:
| Where it sits | The screw closes a cover where the head has to spread its load over a thin panel and the blade is the tool on the bench. |
| When it goes wrong | A head that is too small dents the cover, and a slot that is too shallow lets the blade slip. |
| Why it happens | The panels are thin, the parts are small, and the screws are driven by hand. |
| What we control | Head diameter and slot depth checked, and the blade tried on the first article. |
| Where it sits | The screw holds a painted panel where the wide head protects the coating and the slot is quick to use. |
| When it goes wrong | A head edge burr marks the paint, and a slot that is too tight splits under the blade. |
| Why it happens | The panel is coated, the screws are visible, and the joint is assembled once. |
| What we control | Head edge and slot checked, and the thread gauged per batch. |
| Where it sits | The screw fixes a cover in a damp or chemical environment where the body has to resist without a coating. |
| When it goes wrong | A steel screw rusts at the slot, and a titanium slot that is deformed by a poor blade seizes at the next service. |
| Why it happens | The environment is wet or aggressive, the parts are light, and the joint is opened for service. |
| What we control | Grade recorded, slot checked with the blade, and the surface inspected before packing. |
Four reasons that matter on a slotted truss head machine screw in titanium, each tied to what the drawing has to prove:
|
Head and slot reviewed together
The truss head diameter, the slot depth and the blade width are reviewed before the die is cut, so a head that would dish or a slot that would round is raised first. Basis: Head and slot reviewed before tooling. |
Headed and threaded for the grade
The head and thread are formed with the parameters set for titanium, so the head is not cracked and the slot is not smeared. Basis: Parameters set for the titanium grade. |
|
Slot checked with the blade
The slot is checked with the flat blade and the head on the projector, and the thread is gauged, on the first article and per batch. Basis: Blade fit and head checked on the first article. |
First article to repeat production
The first article fixes the drawing revision, grade and heat, die set and finish; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these slotted truss head machine screws on a single-die header: the truss head is struck in the die, the slot is cut, the thread is rolled, and the parts are supplied plain. The first part of every run is measured on the head, checked with the flat blade and gauged on the thread before the batch continues.


|

|
Between runs the die insert is changed to the drawing head and the slot tool to the blade width; the first parts go to the projector and the blade check before the run continues, and the setting is recorded. The grade is recorded with the batch so the part can be traced to its certificate.
What decides whether a slotted truss head machine screw passes is not the shine of the metal: it is the head diameter and height, the slot width and depth, the head edge and the thread class. The inspection agreement covers those, and the criteria come from the drawing.

Head, slot and edge on the projector |

Thread gauging against GO/NO-GO gauges |

Hardness testing where the drawing requires it |

Salt-spray testing of the agreed finish |
Each batch is recorded against the drawing revision: head and slot from the first article, the blade fit checked, and the thread gauged per batch. If a gauge or the slot check fails, the parts back to the last good setting are held and re-checked.
A third-party test report, where the drawing calls for one, travels with the shipment and is filed under the same batch number as the inspection record.
Every shipment is traceable to the bar or wire it was made from. The grade, heat number and standard are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the finish. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. Slotted parts are approved with the blade, so the slot and the tool are signed off as a pair. Buyers visit during the process to review samples and to see how the heads and slots are made.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header and the slot cell can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
It is a machine screw with a wide, low head and a single slot driven by a flat blade. This one is titanium, plain, from M1 to M10.
The wide bearing face spreads the clamp load over a thin panel, so the sheet does not dent. The low profile keeps the head out of the way where a taller head would foul the assembly.
Titanium is softer at the surface than steel. A blade that rocks deforms the slot edges after a few assemblies, and the damage is not visible until the screw is removed and re-driven.
Screws of this type are quoted from M1 to M10 and in lengths to suit the drawing. Where a long version is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
No. Titanium forms its own passive oxide film in air and resists corrosion without plating. Colour anodizing is optional and is thin enough not to change the slot or the thread.
Head diameter and height, slot width and depth, thread size and length, total length and datum, titanium grade, finish and the blade used at assembly.
How a slotted truss head machine screw project runs from drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
Head and slot review
|
→ |
3
First article approval
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a slotted truss head machine screw quotation, send the drawing with the head diameter and height, slot width and depth, thread size and length, total length and datum, titanium grade, finish and the blade used at assembly.
|
Head diameter and height
|
Slot width and depth
|
Thread size and length
|
|
Total length and datum
|
Titanium grade
|
Finish and blade
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com