Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
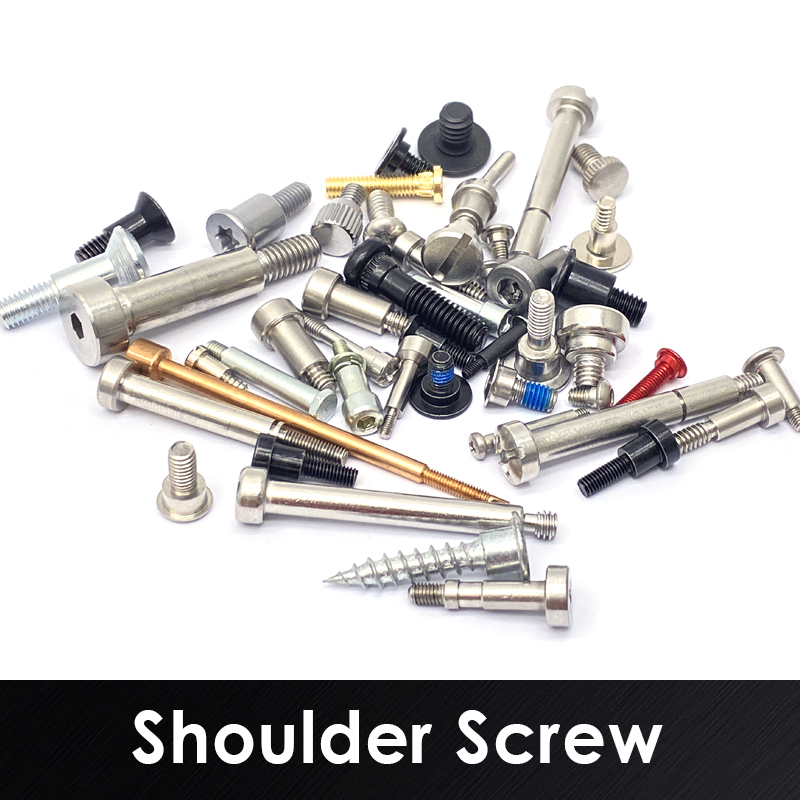
Type:Custom shoulder screws
Materials:Stainless steel / carbon steel / aluminum / titanium / copper — per drawing
Surface treatment:Per drawing — plain, zinc plating, black oxide, electrophoresis, …
Head Type:Per drawing — cap, flat, pan, countersunk, …
Drive type:Per drawing — hex socket, Phillips, slotted, Torx, none, …
Thread:Per drawing - thread independent of the shoulder
Forming:Per drawing - turning, grinding or cold heading
Shi Shi Tong is a shoulder screw manufacturer producing custom shoulder screws to joint drawings: shoulder diameter and length held to the bore fit, thread independent of the shoulder, and head form set by the clearance. Stainless, carbon steel, aluminium and titanium, from M3 to M16 shoulders, with the first article checked against the joint.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A shoulder screw manufacturer produces screws where the unthreaded shoulder is a locating feature, not just a spacer: the shoulder is ground or turned to a controlled diameter, the thread is smaller and sits at one end, and the head pulls the shoulder into the bore. The joint turns or slides on the shoulder, and the thread only clamps it.
The shoulder is the working surface. On a custom shoulder screw the shoulder diameter and length set the fit in the bore, the clearance in the linkage and the pivot height. When you buy from a shoulder screw manufacturer, the dimension you are paying for is that shoulder, not the thread.
Thread independent of the shoulder. The thread is usually one size smaller than the shoulder and is specified separately, so the same shoulder can carry different thread sizes for different joints. That independence is what makes a shoulder screw different from a machine screw with a long shank.
Head as the stop. The head stops the shoulder at the right depth and gives the drive. It can be a socket cap, a slotted or Phillips pan head, a countersunk head or a low-profile head, depending on how the joint is assembled and what clearance it has.
Together these decide whether the joint pivots freely, clamps without slop, and can be serviced. A shoulder screw manufacturer who can hold the shoulder tolerance is the difference between a linkage that moves and one that binds.
The shoulder is the first dimension: its diameter has to match the bore fit and its length has to match the stack it passes through. A shoulder that is a few hundredths oversize will not enter the bore; one that is undersize lets the linkage rattle and wear the bore.
The thread is the second: its size, length and position decide how the joint is clamped, and the thread must not run into the shoulder or into the parts that pivot on it. On a custom shoulder screw the thread length is short by design, so the shoulder stays fully cylindrical.
The head is the third: it seats against the outer part and sets the shoulder depth. As a shoulder screw manufacturer, the shop has to hold all three on one part, because a correct shoulder with the wrong head height still will not assemble. On a countersunk or low-profile head the head height is also a clearance dimension. A shoulder screw manufacturer has to hold all three on one part, because a correct shoulder with the wrong head height still will not assemble.
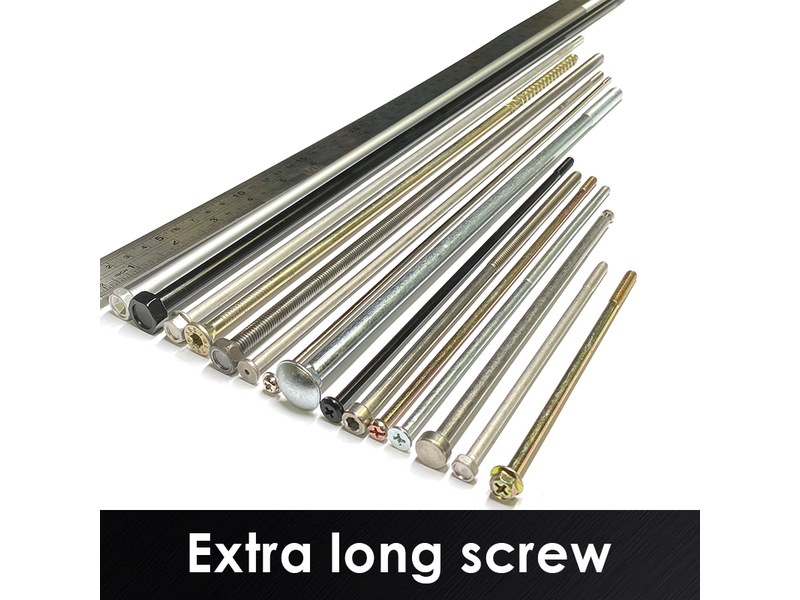
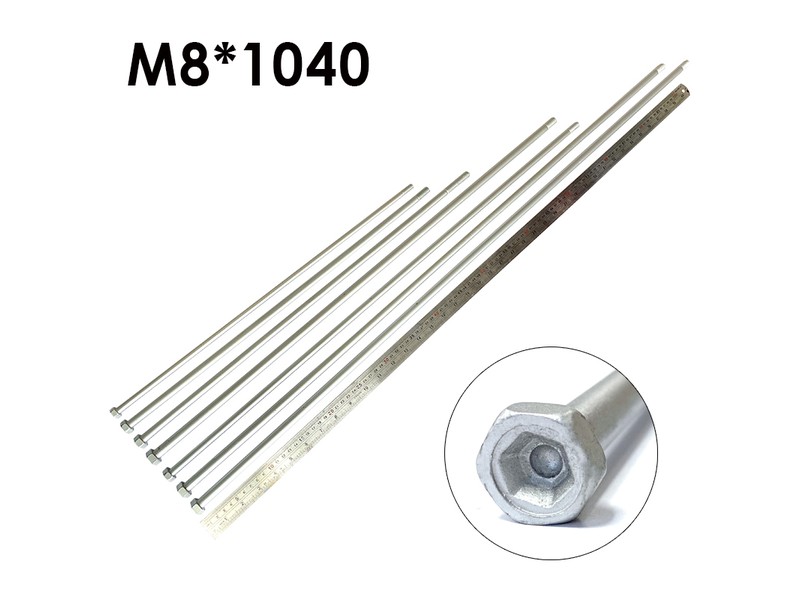
Shoulder screws are produced from M3 to M16 shoulder diameters, with shoulder lengths from a few millimetres up to 200 mm, and threads from M2.5 to M12. Longer versions are quoted on review: where a long shoulder is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
| Item | How it is defined | What we control |
|---|---|---|
| Shoulder diameter | The locating diameter in the bore | Turned or ground to the drawing band; checked on the first article |
| Shoulder length | The pivot height between head and thread | Length from the head datum, checked on the first article |
| Thread size and length | The clamping thread at one end | Thread gauged per batch; length from the drawing |
| Head form and height | The stop and the drive | Head diameter, height and recess checked against the drawing |
| Run-out between shoulder and thread | The two axes have to align | Checked between centres on the first article |
Every combination of shoulder diameter, shoulder length and thread is quoted against the drawing. A shoulder screw manufacturer quotes the joint, not the size: the bore, the stack and the thread all have to fit together. A shoulder screw manufacturer works from the joint: the bore, the stack and the thread all appear on the drawing, and the screw is checked against them rather than against a catalogue size.
Shoulder diameter and length are measured at the same datum as the thread, and the head height is read from the outer face. The first article is checked on every dimension before the batch is released.
Custom shoulder screws are quoted against the fit on the drawing. Shoulder diameters are typically held to h9 or a fit band stated by the customer, with tighter bands ground rather than turned. Surface roughness on the shoulder matters because the shoulder is a bearing surface in many joints.
| Feature | Why it matters in the joint | What we control |
|---|---|---|
| Shoulder diameter | Sets bore fit and play | Held to the fit band; ground where the band is tight |
| Roundness | A lobed shoulder wears the bore | Checked on the projector and with a micrometer |
| Surface roughness | Bearing surface finish | Checked with a roughness tester |
| Thread-to-shoulder run-out | Off-axis thread tilts the joint | Checked between centres |
| Head squareness | Head has to seat flat | Checked on the surface plate |
A shoulder screw manufacturer reads the fit band with the coating in mind. A plated shoulder grows by the coating thickness, so a shoulder that has to slide in a bore is either masked during plating or machined undersize before the coating, and the first article confirms which route the drawing requires.
Inspection follows the drawing: the shoulder is measured in two directions for roundness, the head is checked for squareness, and the thread is gauged. The results are recorded against the batch, so a repeat order can be compared with the approved sample.
As a shoulder screw manufacturer we machine shoulder screws in stainless steel, carbon steel, aluminium, titanium and copper alloys, chosen for the joint: stainless for corrosion, carbon steel for strength and cost, aluminium for weight, titanium for weight and corrosion together. The material is part of the drawing, and the certificate follows the batch.
| Finish | How it protects | Effect on the shoulder fit | Typical use |
|---|---|---|---|
| Passivated stainless | Free iron removed, passive film restored | No dimensional change | Stainless joints, indoor and damp |
| Zinc plated (carbon steel) | Sacrificial zinc layer | Shoulder grows; masked or machined undersize | Carbon steel joints in dry service |
| Black oxide | Conversion coating, minimal thickness | No measurable build-up | Indoor joints where black is required |
| Dacromet flake | Zinc-aluminium flake layer | Thin film; shoulder checked over the coating | Outdoor carbon steel joints |
| Anodized aluminium | Oxide layer, dyed if required | Builds a few microns; bore fit re-checked | Lightweight visible joints |
The finish is chosen with the fit, not after it. On a shoulder screw the coated diameter is the working diameter, so the drawing states whether the shoulder is masked, machined to a pre-plate size or accepted at the coated dimension, and the first article confirms it.
Packing protects the shoulder. Screws are packed so the shoulder does not rub against the carton or against each other, and the label carries the batch and the material heat.
Three joints where the shoulder does the work and the thread only clamps — the cases a shoulder screw manufacturer is asked about most often — and what the shoulder has to do instead:
Hinges, pivots and access covers
|
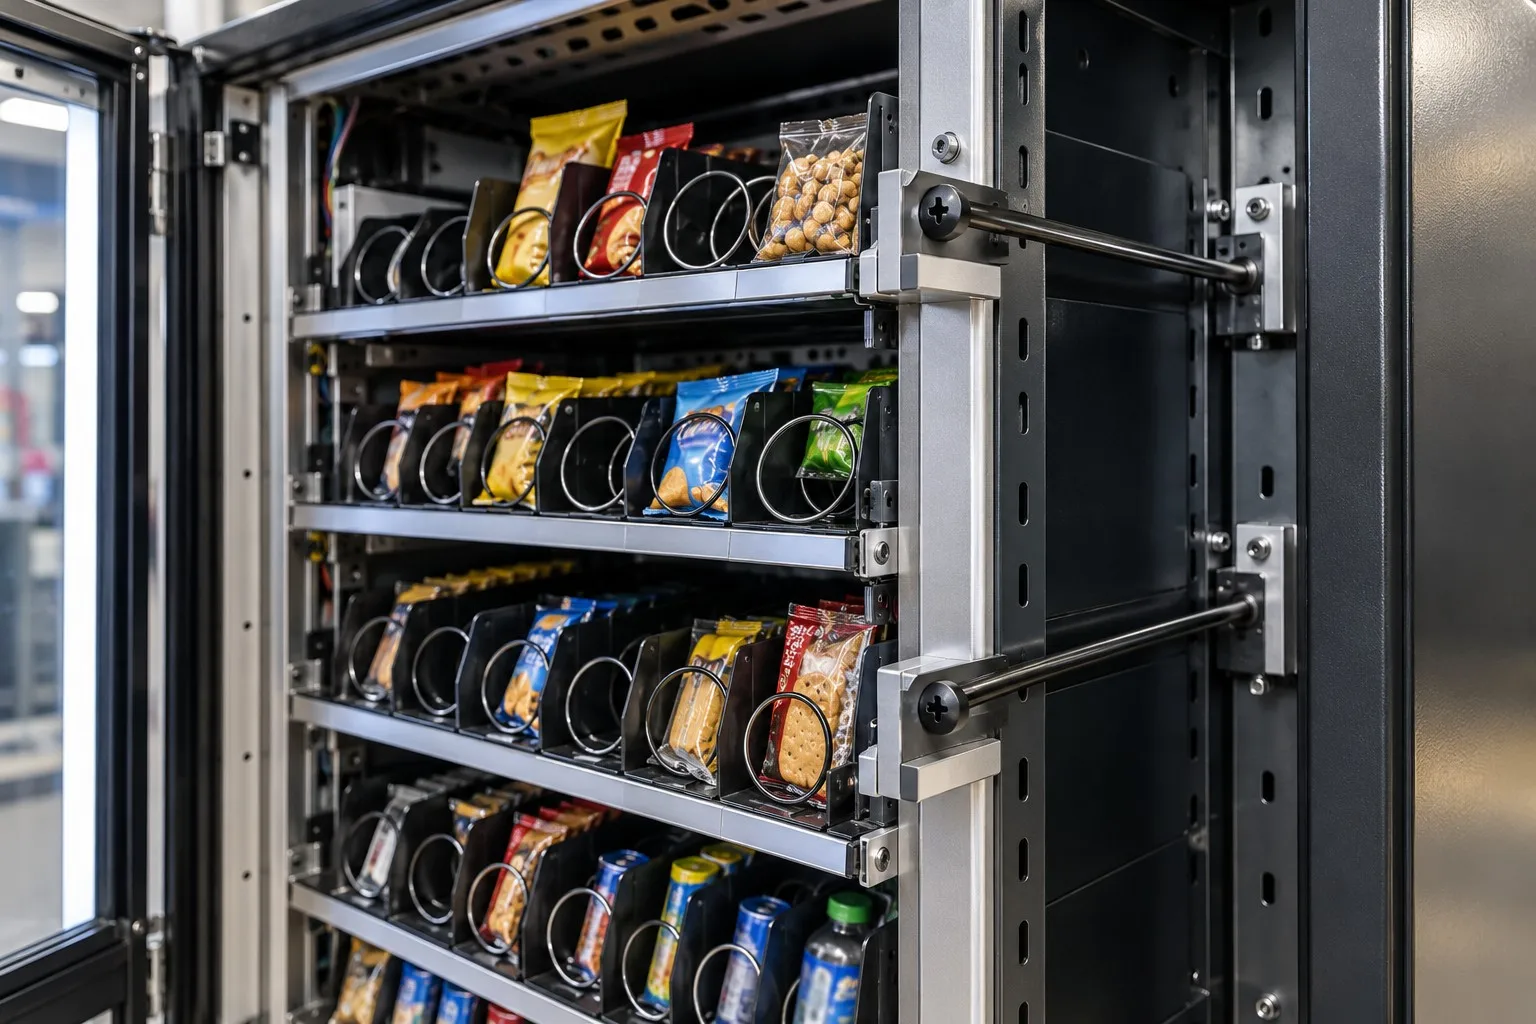
Hinges and covers – shoulder screws as pivots |
Automation linkages and pivoting arms
|
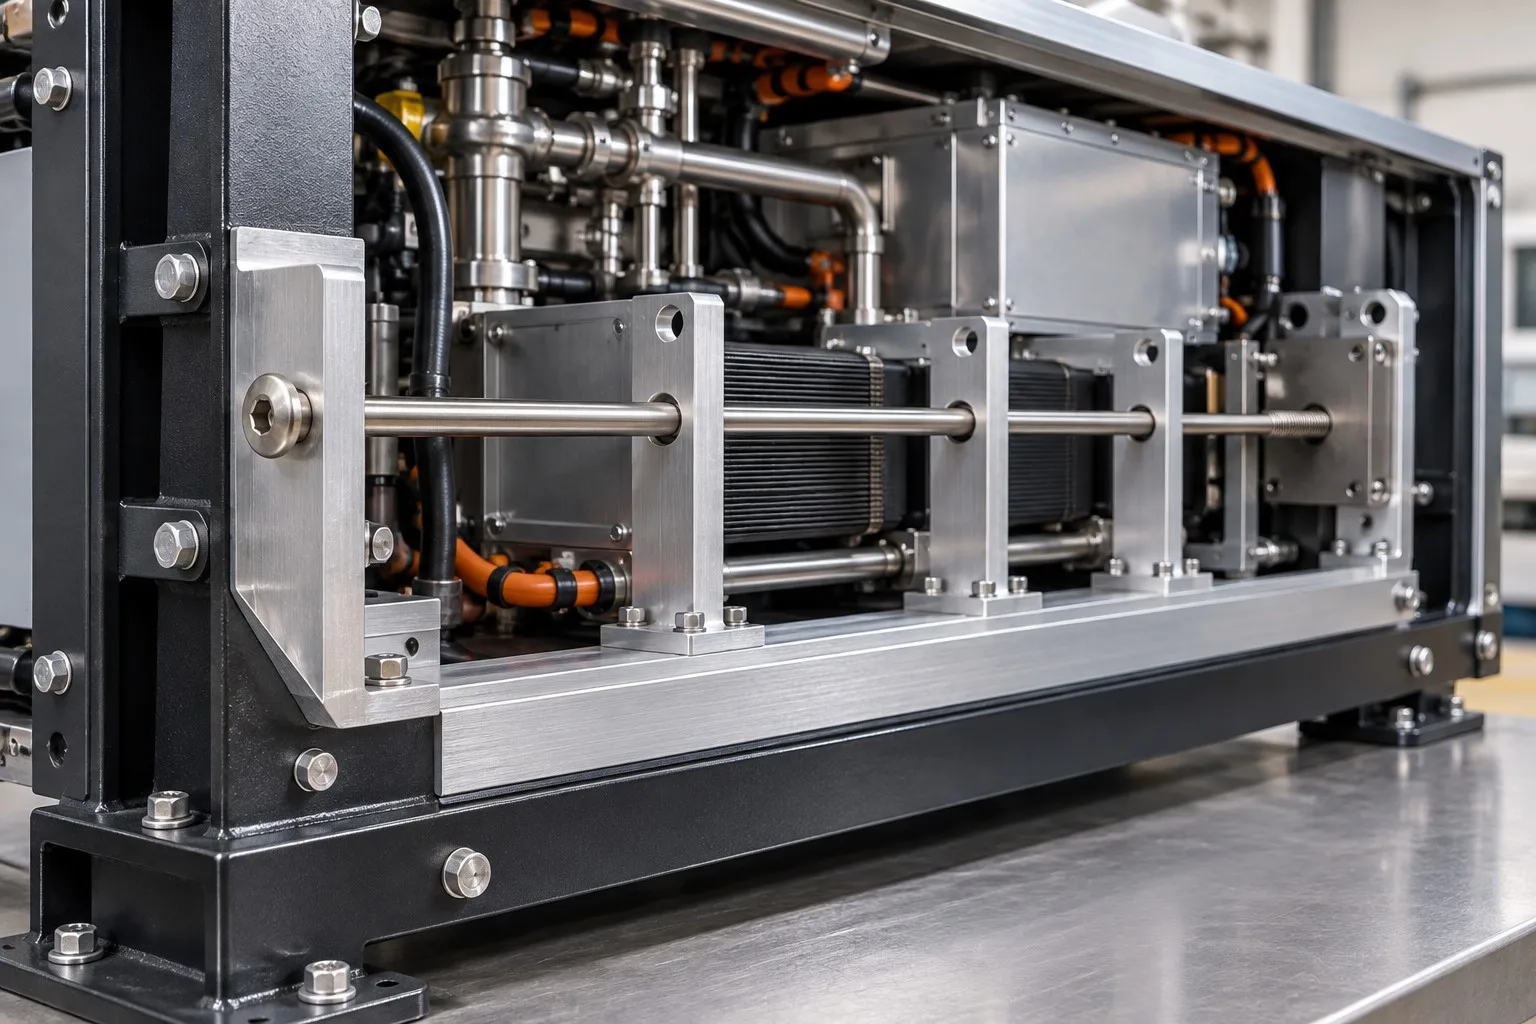
Automation – shoulder screws as pivot bearings |
Instrument and enclosure hardware
|
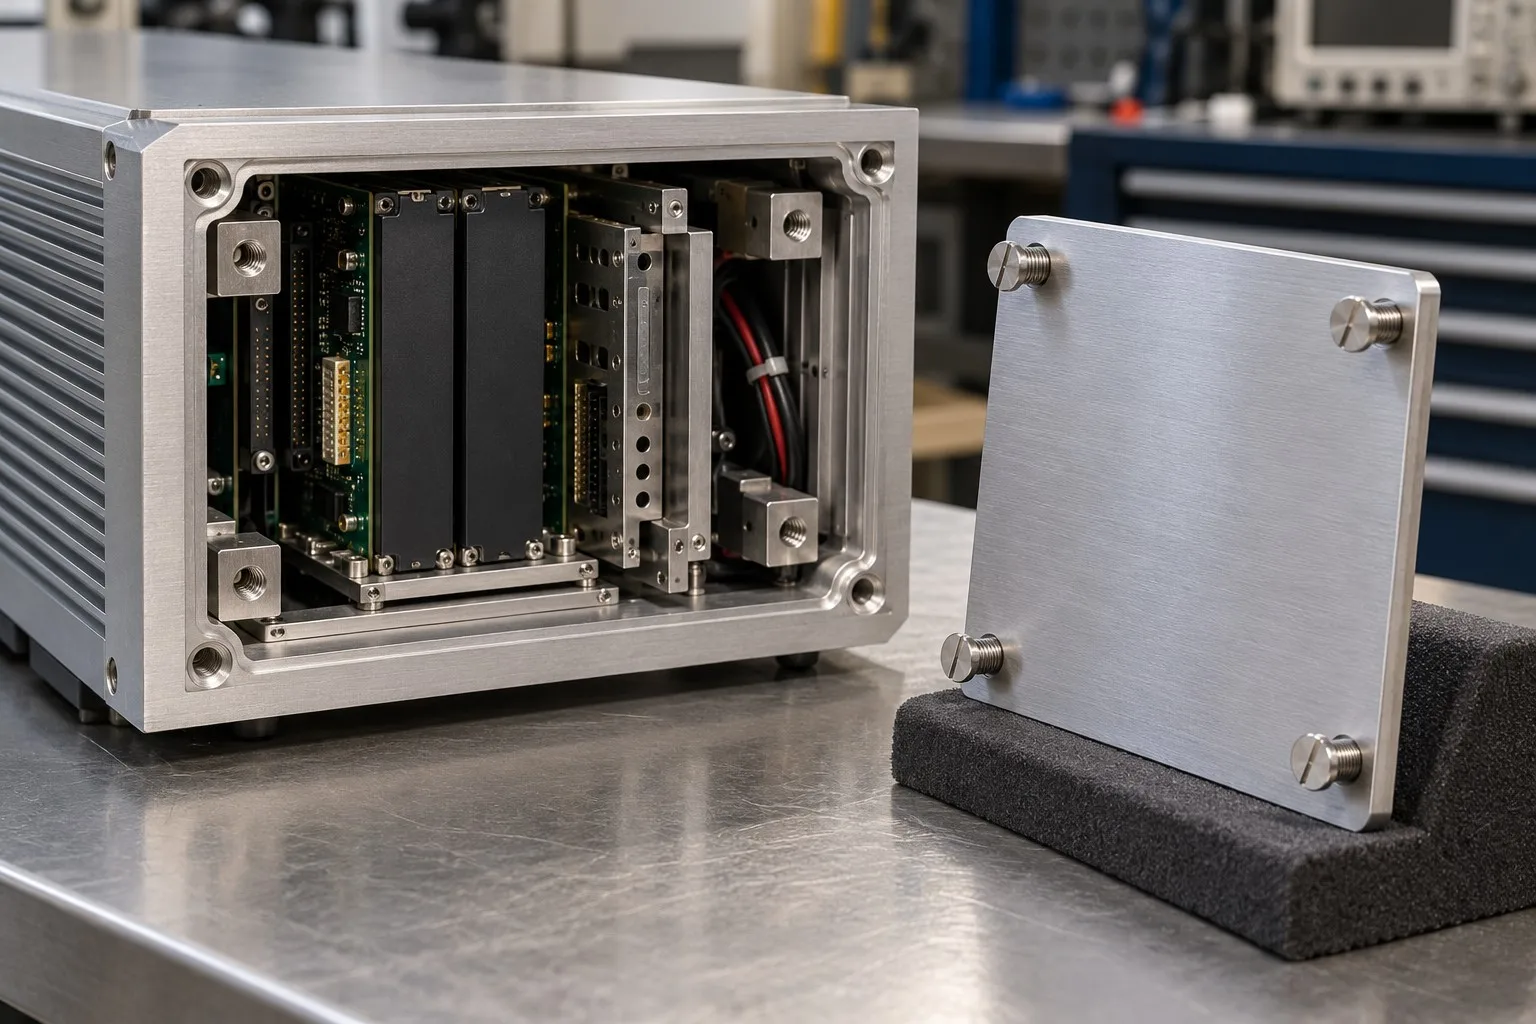
Instruments – shoulder screws locating a cover |
Four reasons that matter when you choose a shoulder screw manufacturer, each tied to what the joint drawing has to prove:
|
Joint review before tooling
The bore, the stack and the thread are reviewed together before a die or a turning programme is released, so the shoulder is dimensioned against the joint and not against a catalogue size. Basis: Joint drawing reviewed before tooling or programming. |
Turned, ground or headed to the fit
Shoulders that need a tight band are turned and, where required, ground; shoulders that suit a formed route are headed. The route is chosen to hold the fit on the drawing. Basis: Route chosen to hold the shoulder fit band. |
|
Shoulder and run-out measured
The shoulder is measured for diameter and roundness, and the thread-to-shoulder run-out is checked between centres, so the pivot runs true. Basis: Shoulder and run-out checked on the first article. |
First article to repeat production
The first article fixes the drawing revision, material heat, set-up and finish batch; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
A shoulder screw manufacturer has to choose the route from the fit: custom shoulder screws run from bar or wire through turning, heading and thread production, depending on the shoulder fit the drawing asks for. Tight shoulders are turned and ground; formed shoulders are headed and then thread-rolled. In every case the head datum, the shoulder and the thread are produced in one route so the axes stay together.


|

|
Between runs the tooling is changed to the drawing shoulder and thread dimensions; the first part goes to the gauges before the run continues, and the setting is recorded. A repeat order starts from that record, so the shoulder that fitted on the sample is the shoulder that arrives on the reorder.
At a shoulder screw manufacturer, what decides whether a custom shoulder screw passes is not its appearance: it is the shoulder diameter and length, the roundness of the shoulder, the thread-to-shoulder run-out, and the head seating flat. The inspection agreement covers those, and the criteria are the ones written on the joint drawing.

Thread gauging against GO/NO-GO gauges |

Shoulder and head profile on the projector |

Hardness testing where the drawing requires it |

Salt-spray testing of the finish |
Each batch is recorded against the drawing revision: shoulder diameter and length from the first article, roundness and run-out between centres, thread gauging per batch, and the finish checked in the condition it ships. If a gauge or the run-out check fails, the parts back to the last good setting are held and re-checked.
Where a third-party report is required for the material or the finish, it is listed on the drawing so the paperwork ships with the parts, and the batch number on the label matches the record used for the gauge.
Every custom shoulder screw shipment from this shoulder screw manufacturer is traceable to the bar or wire it was made from. The grade, heat number and standard are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the finish. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
As a shoulder screw manufacturer working from joint drawings, Shi Shi Tong has supplied more than 8,678 customers in 89 countries and regions; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: joint drawing review, first-article approval, then batches checked against that sample. Buyers visit during the process to review samples and to see the turning, heading and finishing steps their parts will go through.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the turning cells, the heading floor and the finishing line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
Screws where the unthreaded shoulder is the working surface: it locates in a bore, sets the pivot height and carries the moving joint, while the smaller thread at one end only clamps the stack. Holding that independence is what a shoulder screw manufacturer is asked to do.
On a machine screw the shank is just a carrier for the thread. On a shoulder screw the shoulder diameter and length are held to a fit, and the thread is independent of the shoulder and sits at one end.
Shoulder diameters are typically held to h9 or a fit band on the drawing, with tighter bands ground rather than turned. The band is read with the coating in mind where the part is plated.
Stainless steel, carbon steel, aluminium, titanium and copper alloys, chosen for corrosion, strength or weight. The material and heat number are recorded on the certificate.
Shoulder diameters from M3 to M16, shoulder lengths from a few millimetres to 200 mm, and threads from M2.5 to M12. Where a long shoulder is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
Shoulder diameter and fit band, shoulder length, thread size and length, head form and height, material and finish, and the datum for the shoulder length.
How a shoulder screw manufacturer takes a joint drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
Joint and DFM review
|
→ |
3
First article approval
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a custom shoulder screw quotation, send the drawing or the joint drawing with the bore, the stack and the thread: shoulder diameter and fit band, shoulder length, thread size and length, head form and height, material and finish. The joint is reviewed with you before production.
|
Shoulder diameter and fit band
|
Shoulder length
|
Thread size and length
|
|
Head form and height
|
Material
|
Finish and quantity
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com