Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
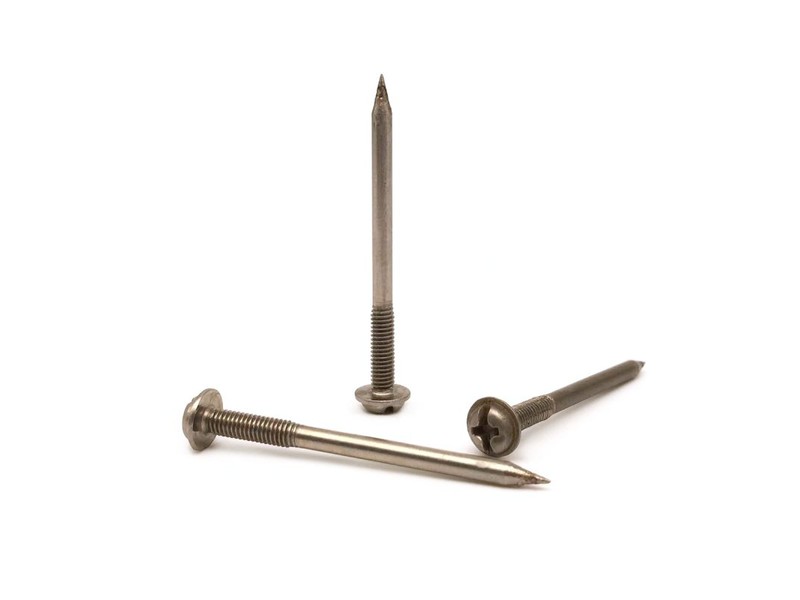
Type:Red copper screw | ultra low head screw
Materials:Red copper
Surface treatment:Plain
Head Type:Ultra low head
Drive type:None (no slot; plain dished head face)
Thread:Partial machine thread, rolled at the tip
Forming:Single-die cold heading
Number:1679
We manufacture red copper ultra-low head screws with a dished contact face, no drive recess, a small shank and a partial machine thread, from M2 to M8, formed on a single-die header and supplied plain or finished to the drawing. Head face, shank, thread and the assembly method are agreed before production.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
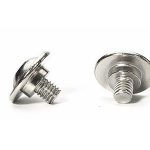
A red copper screw is a fastener made in pure copper, chosen for conductivity, thermal transfer or a soft contact face. This one is an ultra-low head screw with no slot: the head is a shallow dished face, almost flat, with no recess at all, and the thread runs over part of a small shank. The head is a contact surface rather than a place to put a driver.
Ultra-low head. The head height is kept to a minimum so the screw sits almost flush in a recess, or so the head can act as a flat contact pad without standing proud. On a red copper screw that matters because copper is often chosen for a face that carries current or heat, not for a head you turn.
No slot, no recess. A head with no slot cannot be turned with a driver. The part is assembled from the thread end, with a nut, or with a tool that grips the shank; the drawing review settles which, because the assembly method is part of the joint. A screw with no drive and no assembly method is a drawing that has not been finished.
Soft metal, small shank. Red copper is soft and conducts well, so the thread strips early and the shank deforms if it is over-tightened. The thread is partial, the shank is small, and the drawing states the torque the joint can take.
Together these decide whether the part works: it sits flat, it carries the current or the heat, and it can be installed without a drive recess.
The head face on a red copper screw is dished: slightly concave or chamfered at the rim, so the contact ring bears on the mating surface. That shape is a contact face, not a driver recess, and its form is checked on the first article because a contact face that is not flat enough raises the resistance of the joint.
The small shank under the head is what the part is held by during assembly. It has to be strong enough to take the turning or pressing force and small enough to pass through the clearance in the joint, so its diameter and length are dimensioned with the assembly method in view.
The thread is partial and sits at the far end. On a red copper screw the thread is the clamping feature; the plain shank is what locates and what the assembly tool can grip. Keeping the thread away from the head also keeps the head face from being distorted by the thread rolling step.
Red copper screws are quoted from M2 to M8 and up to 100 mm, with length measured from the head face to the tip. Where a long version is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
| Item | How it is defined | What we control |
|---|---|---|
| Total length | From the head face to the tip | Datum stated on the drawing; length measured on the shop plate |
| Head diameter and height | The ultra-low head and its dished face | Head height and face form checked on the first article |
| Shank diameter | The small shank the part is held by | Shank diameter held to the drawing |
| Thread length and position | The partial thread at the tip | Thread start taken from the drawing, not a sample |
| Face flatness | The contact face on the head | Checked on the surface plate and the projector |
Each diameter and length combination is checked against the drawing before a quotation is issued. On a part with no drive recess the assembly method is reviewed first, because a head that cannot be turned changes how the whole joint is built.
Length and thread position are measured from the head face, and the head face is checked for flatness and height on the first article before the batch continues.
For a red copper screw the drawing fixes the thread and the shank, and it also has to fix how the part is installed: thread size and class, thread length, the small shank, the head face and the assembly method. Without the last item the part cannot be planned, because the copper will not take the torque a steel screw of the same size would.
| Parameter | Why it matters on a no-slot copper screw | What we control |
|---|---|---|
| Thread class | The thread is the only clamping feature | Gauged per batch; class per drawing |
| Shank diameter | It is what the assembly tool grips or the joint clears | Held to the drawing; checked on the first article |
| Head face | It is the contact surface | Flatness and height checked on the first article |
| Assembly method | No recess means the part is turned from the thread side or pressed | Reviewed with the customer before tooling |
Red copper is usually supplied plain: the metal is the finish and the contact surface. Copper tarnishes in air, and a tarnished face has a different contact resistance, so the drawing states whether the part is cleaned and sealed, used bare, or plated where a stable surface is needed.
| Finish | How it protects | Effect on the contact face | Typical use |
|---|---|---|---|
| Plain, cleaned | Oxide removed before packing | Clean copper face; tarnishes in service | Internal conductive joints |
| Cleaned and sealed | Thin sealing film | Slower tarnish; film considered in the contact | Stored or visible copper parts |
| Nickel plated | Hard plated layer | Stable face; higher resistance than bare copper | Parts that must stay bright |
| Tin plated | Soft, solderable layer | Solderable face; low oxide growth | Terminals and solder joints |
| Silver plated | Noble high-conductivity layer | Low resistance; tarnish-resistant | High-current contacts |
Salt-spray and contact-resistance testing are agreed per project and written on the drawing. On a red copper screw the finish is part of the electrical design, so it is chosen with the joint rather than applied at the end.
Packing protects the head face and the thread. Parts are packed so the dished face does not rub and the copper does not pick up marks, and the label carries the batch and the material grade.
Three joints where a red copper screw is chosen for conductivity or a soft contact face, and what the screw has to do instead:
Electrical contacts and terminals
|
Electrical contacts – flat copper face on the conductor |
PCB and busbar assemblies
|
Busbars – copper screws as contact hardware |
Thermal and RF assemblies
|
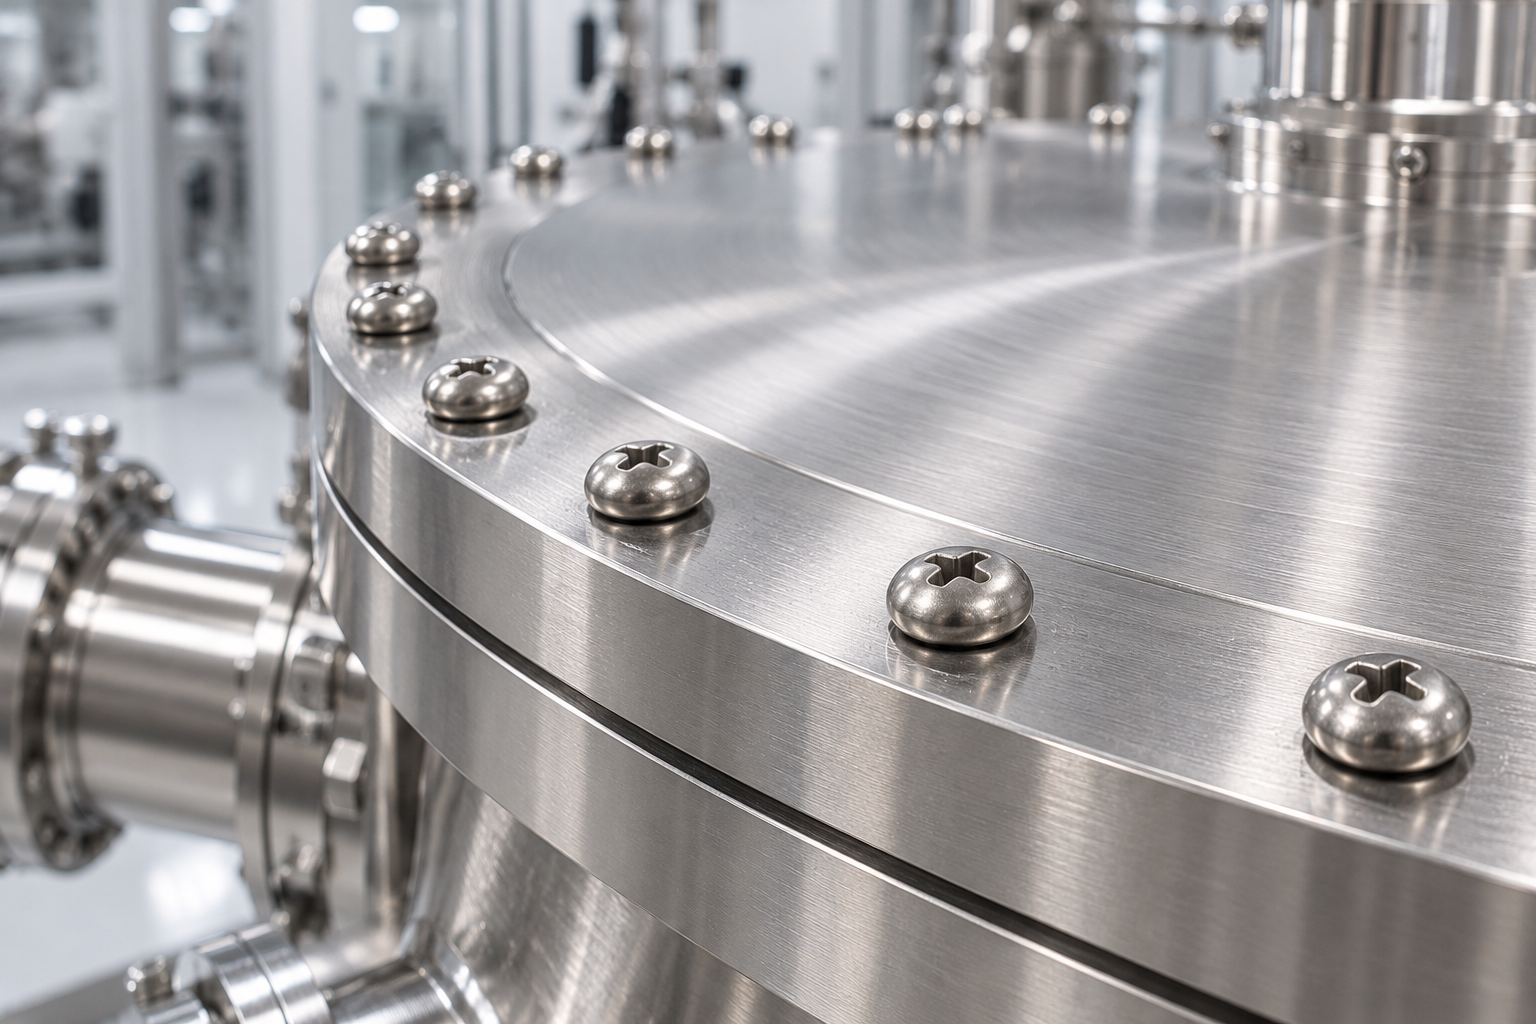
Thermal and RF – copper hardware at a contact interface |
Four reasons that matter on a red copper screw, each tied to what the drawing has to prove:
|
Face and assembly reviewed first
The head face, the small shank, the thread and the assembly method are reviewed together before tooling, so a part with no drive recess is not made without knowing how it goes in. Basis: Drawing and assembly method reviewed before tooling. |
Soft metal, formed with care
Copper is headed at speeds and with tooling set for a soft, gummy metal, so the dished face forms cleanly and the small shank is not deformed by the heading step. Basis: Soft-metal tooling and forming. |
|
Face and thread measured
The head face is checked for flatness and height, and the thread gauged after finishing, so the contact face that conducts is the face that was approved. Basis: Face and thread checked on the first article. |
First article to repeat production
The first article fixes the drawing revision, copper grade, die set and finish condition; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
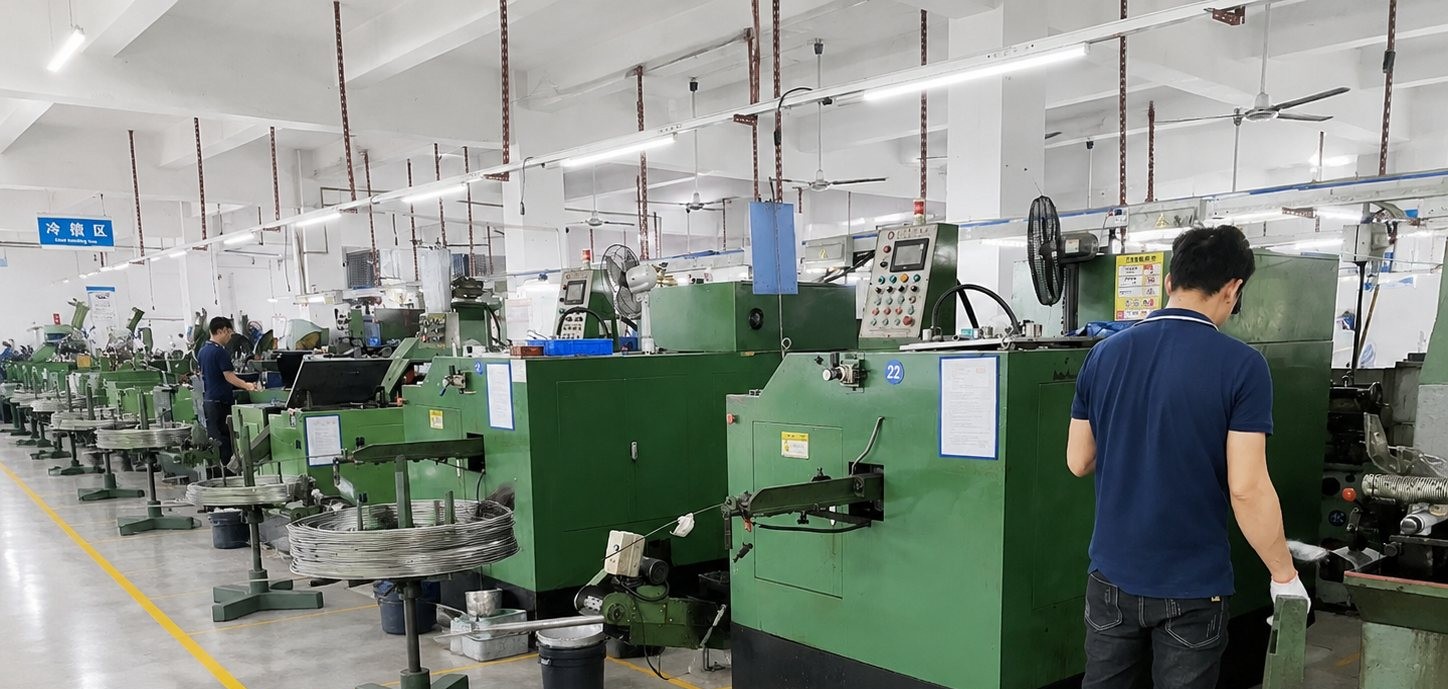
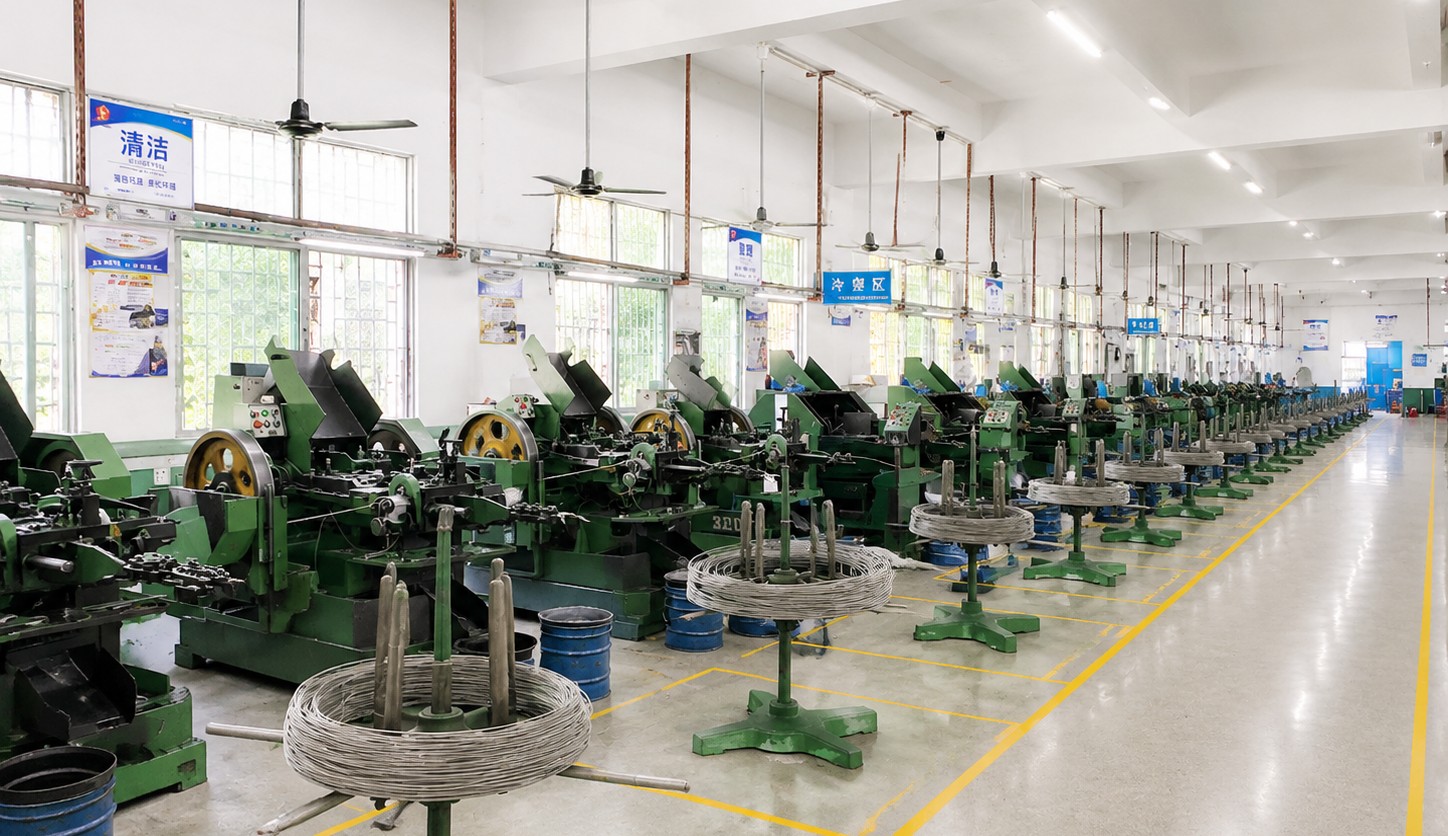
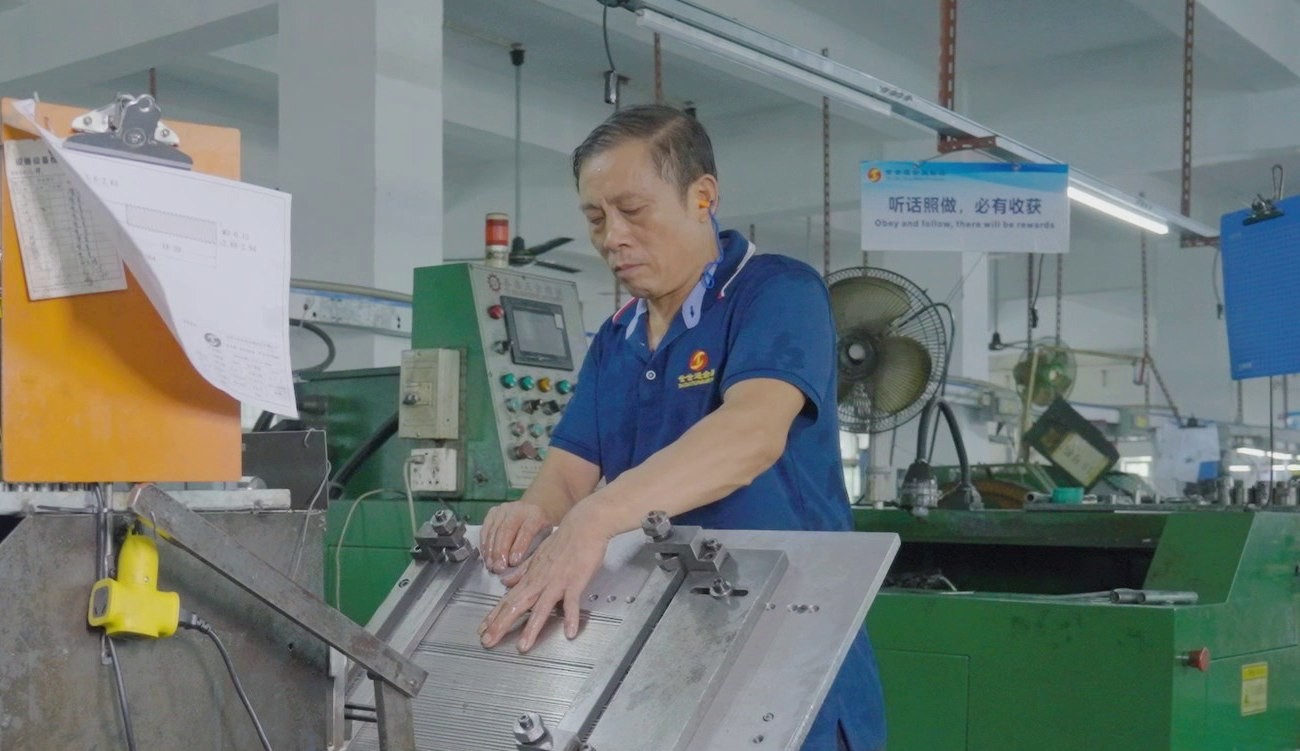
Shi Shi Tong forms these red copper screws on a single-die header: the ultra-low dished head and the small shank are formed in the die, the partial thread is rolled at the tip, and the parts are cleaned before packing. The first part of every run is checked for head height, face form and thread before the batch continues.
|
|
Between runs the die insert is changed to the drawing head form and shank diameter; the first parts go to the gauges before the run continues, and the setting is recorded. The copper parts are packed by the face up, so the dished surface is not marked before it reaches the assembly.
What decides whether a red copper screw passes is not its colour: it is the head height and the flatness of the dished face, the small shank diameter, and the thread class in the condition it ships. The inspection agreement covers those, and the criteria come from the drawing.
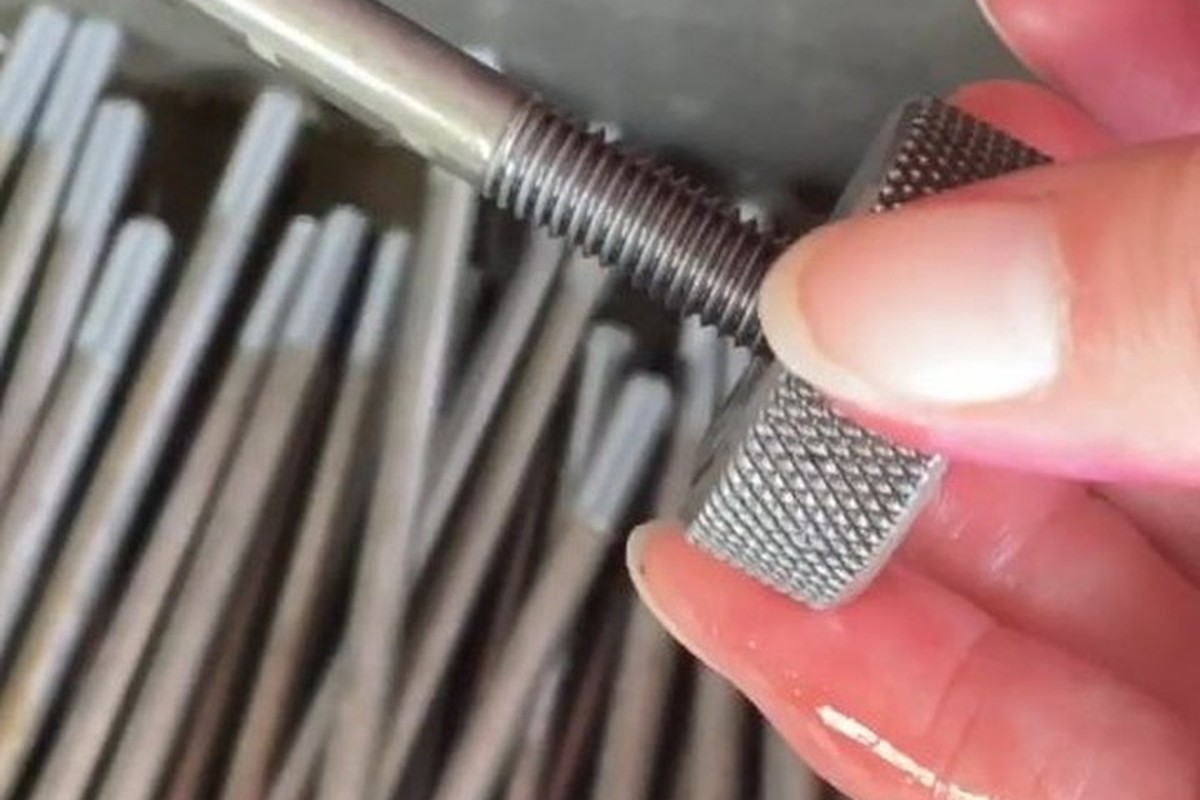
Thread gauging after finishing |
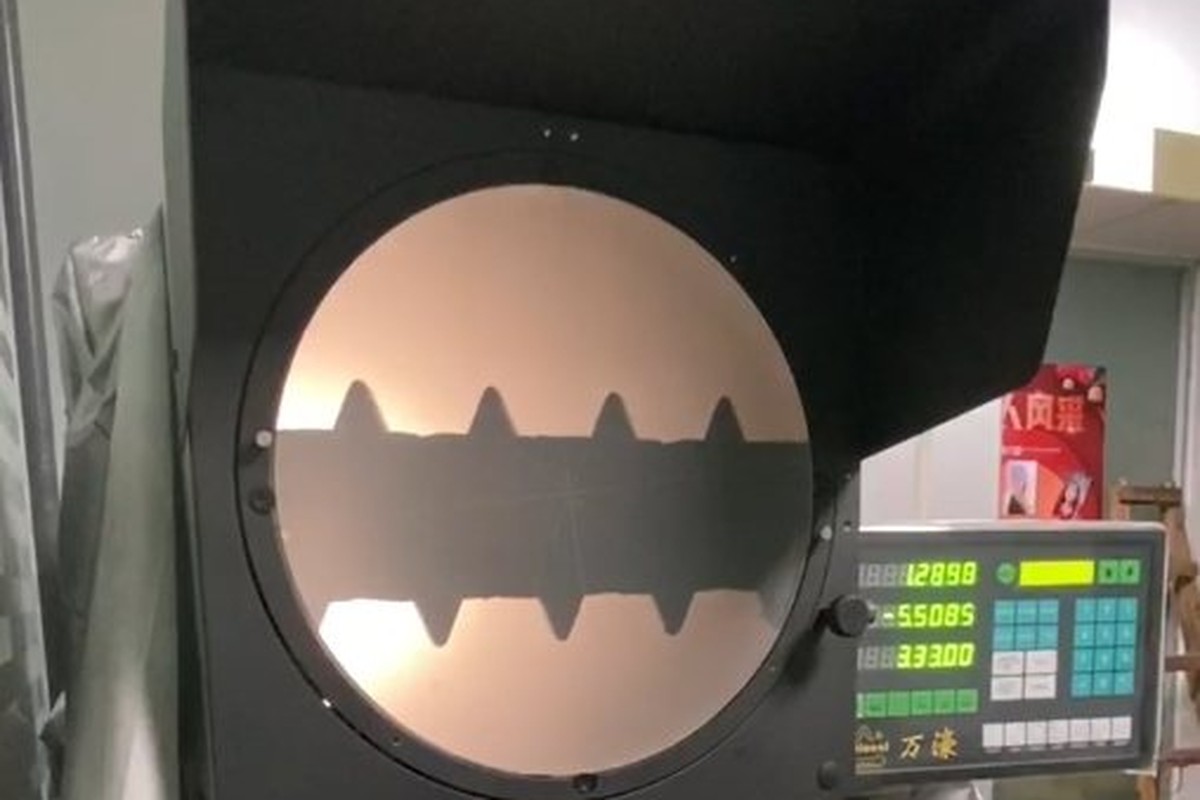
Head face and shank profile on the projector |
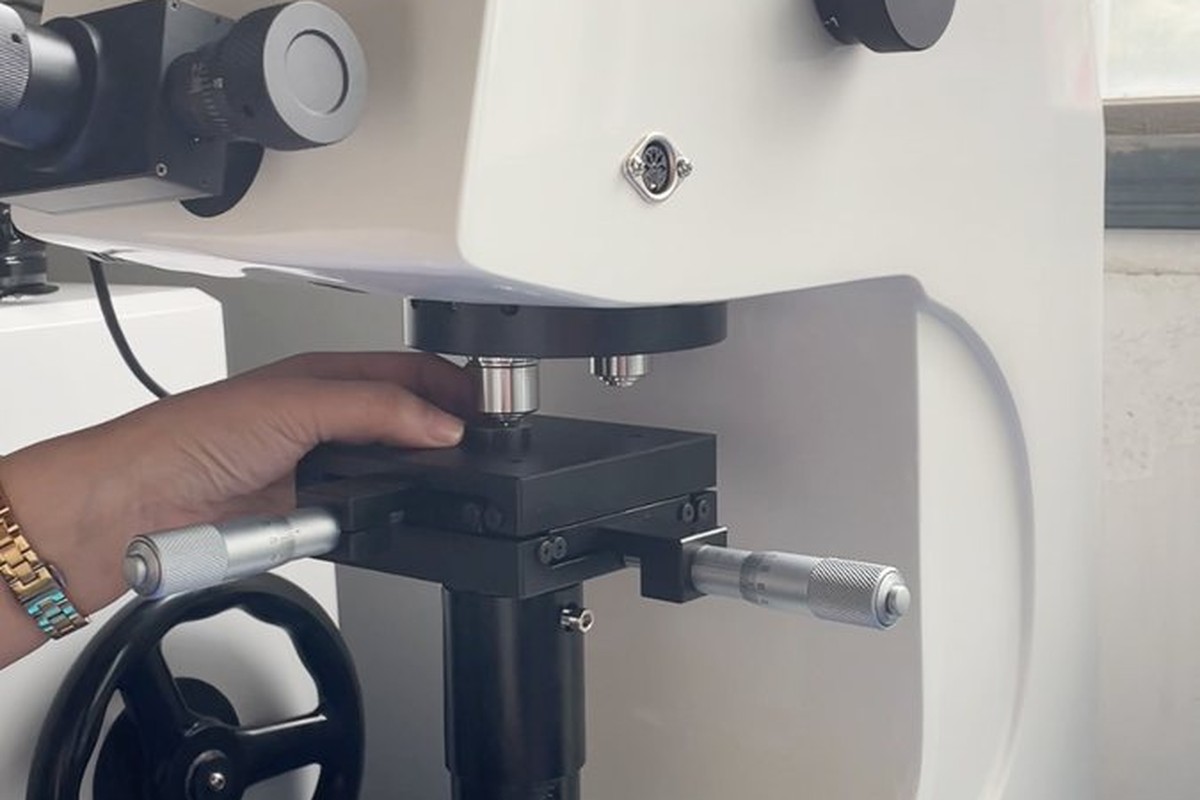
Hardness testing of the copper |
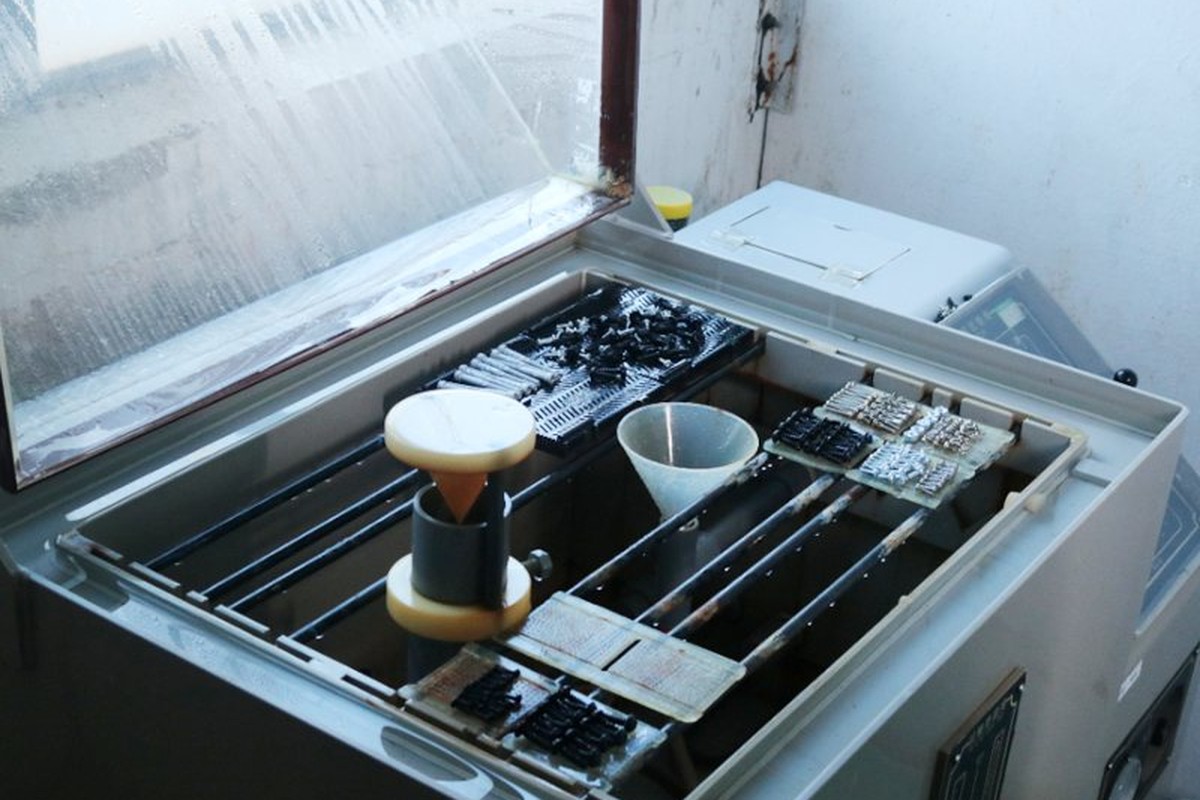
Corrosion testing of the agreed finish |
Each batch is recorded against the drawing revision: head face and shank from the first article, thread gauging per batch, and the finish checked against the sample. If a gauge or the face check fails, the parts back to the last good setting are held and re-checked.
If the material or finish needs an outside test, the request is set at the drawing stage, and the report ships with the parts under the batch number.
Every red copper screw shipment is traceable to the wire it was made from. The grade, heat number and standard are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.
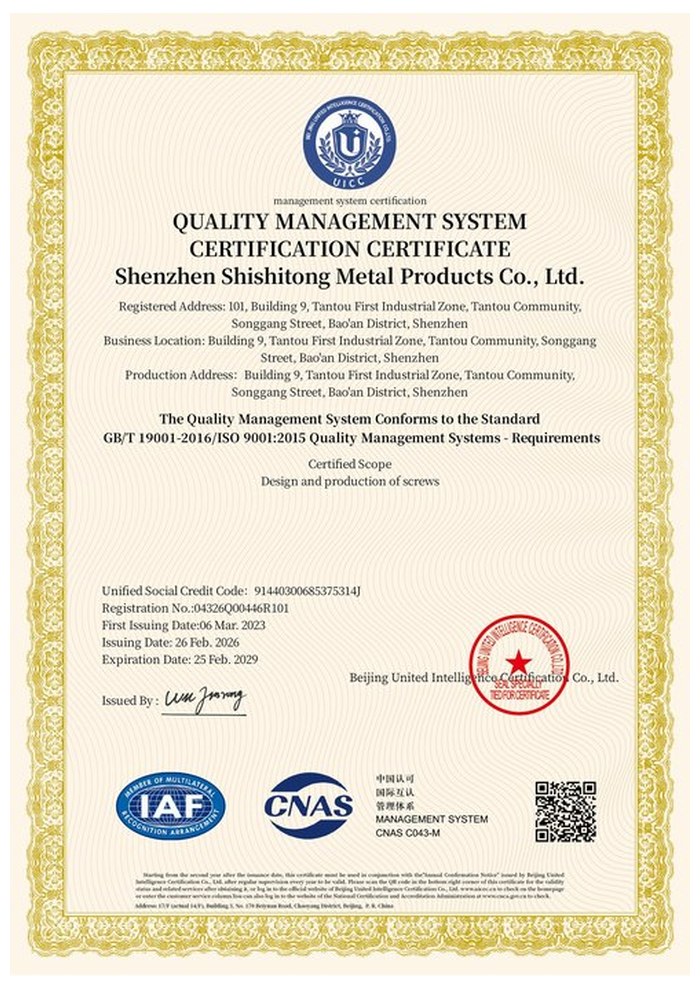
ISO 9001:2015 |
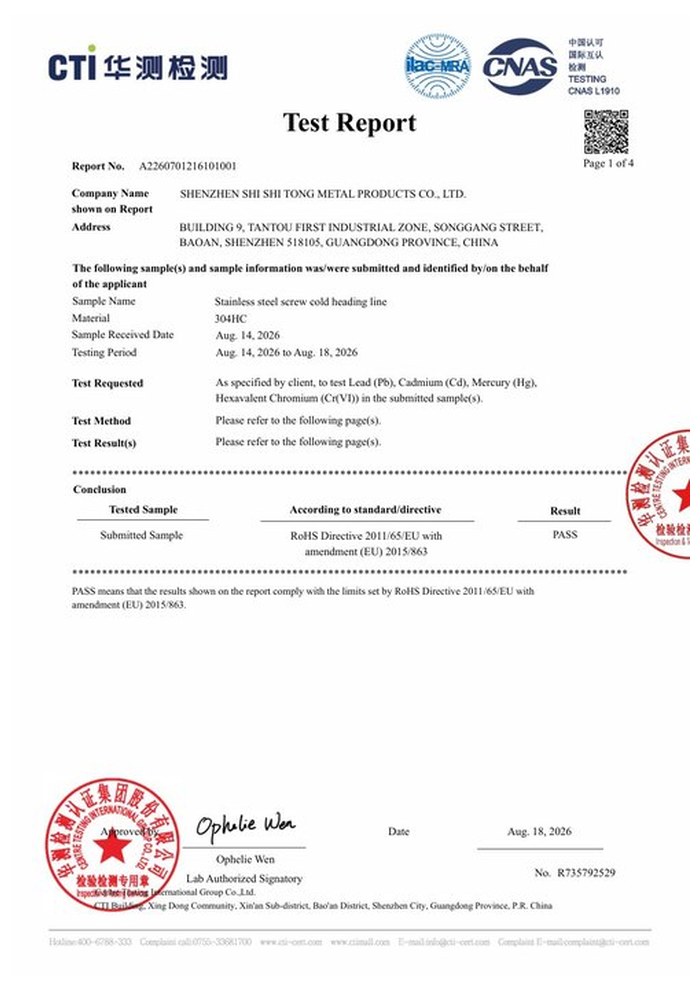
RoHS test report |
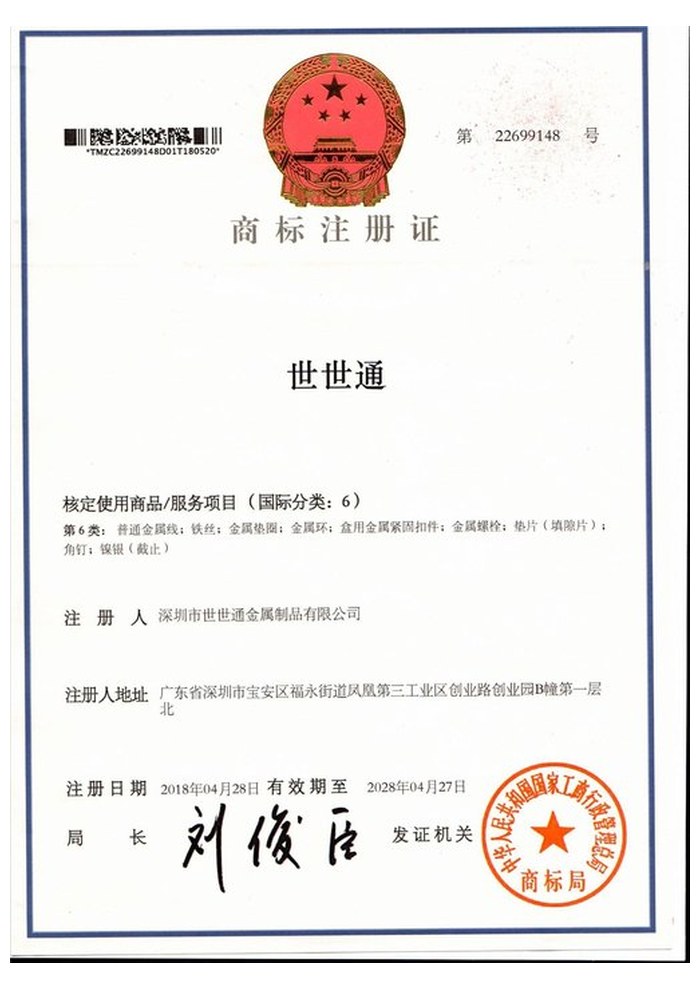
Registered trademark |
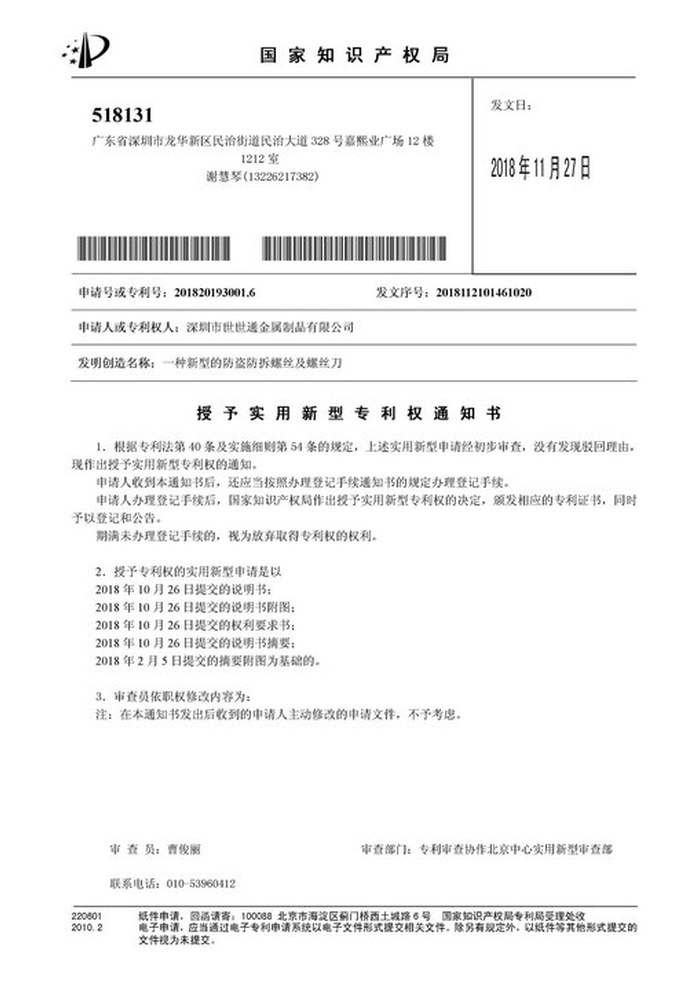
Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the finish. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing and assembly review, first-article approval, then batches checked against that sample. Buyers visit during the process to review samples and to see how the heads and threads are formed, and conductive parts are approved on a physical sample rather than a drawing alone.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the heading floor and the finishing line can be seen on the day the parts run.
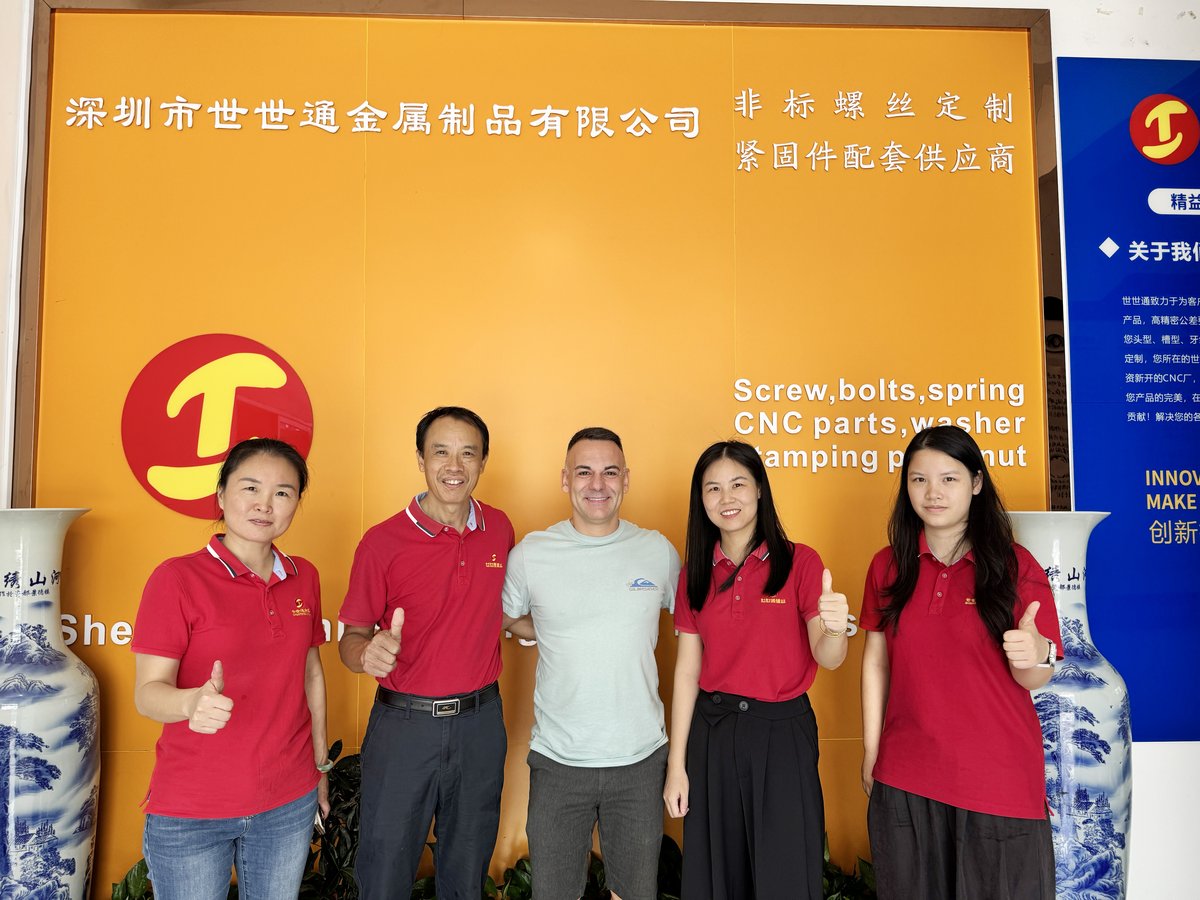
Customer group visit – sample review |
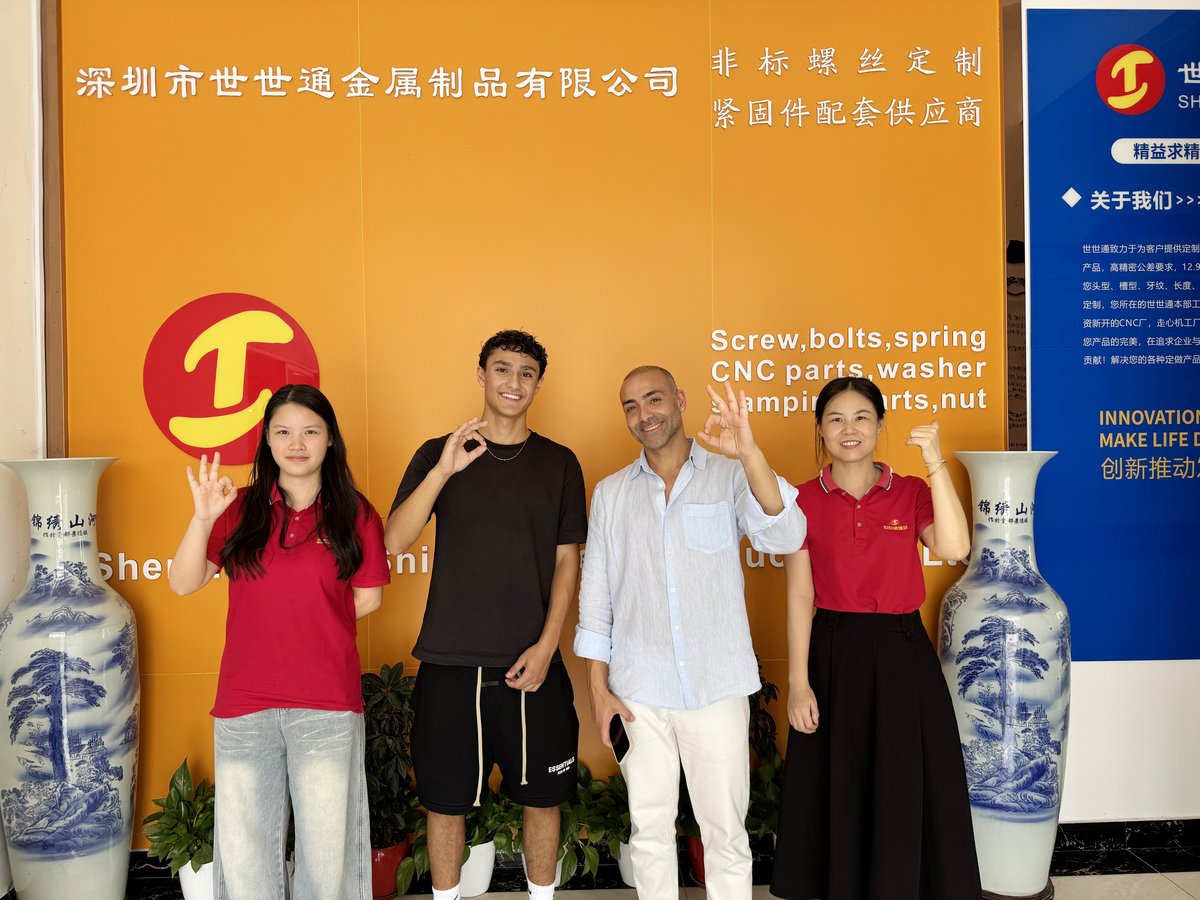
Customer group visit – process discussion |
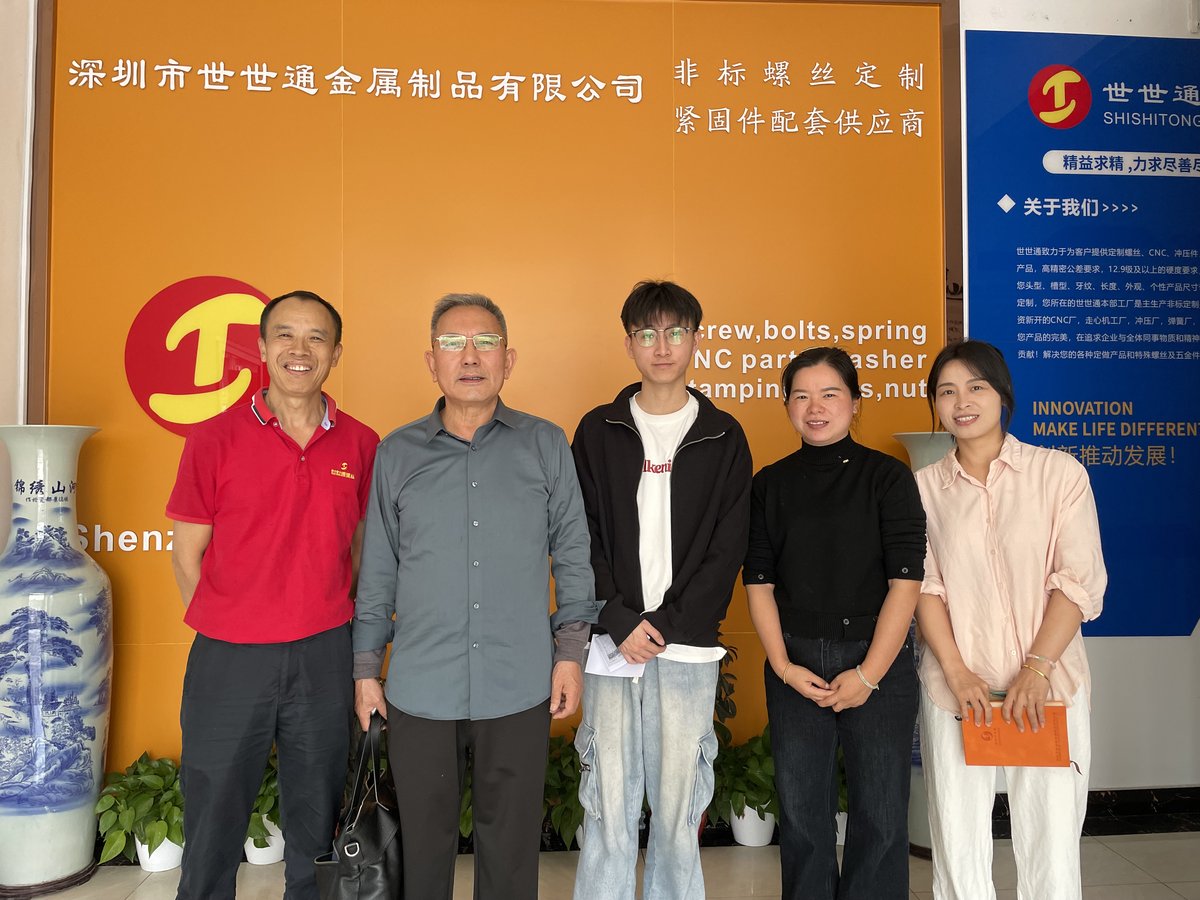
Customer group visit – factory tour |
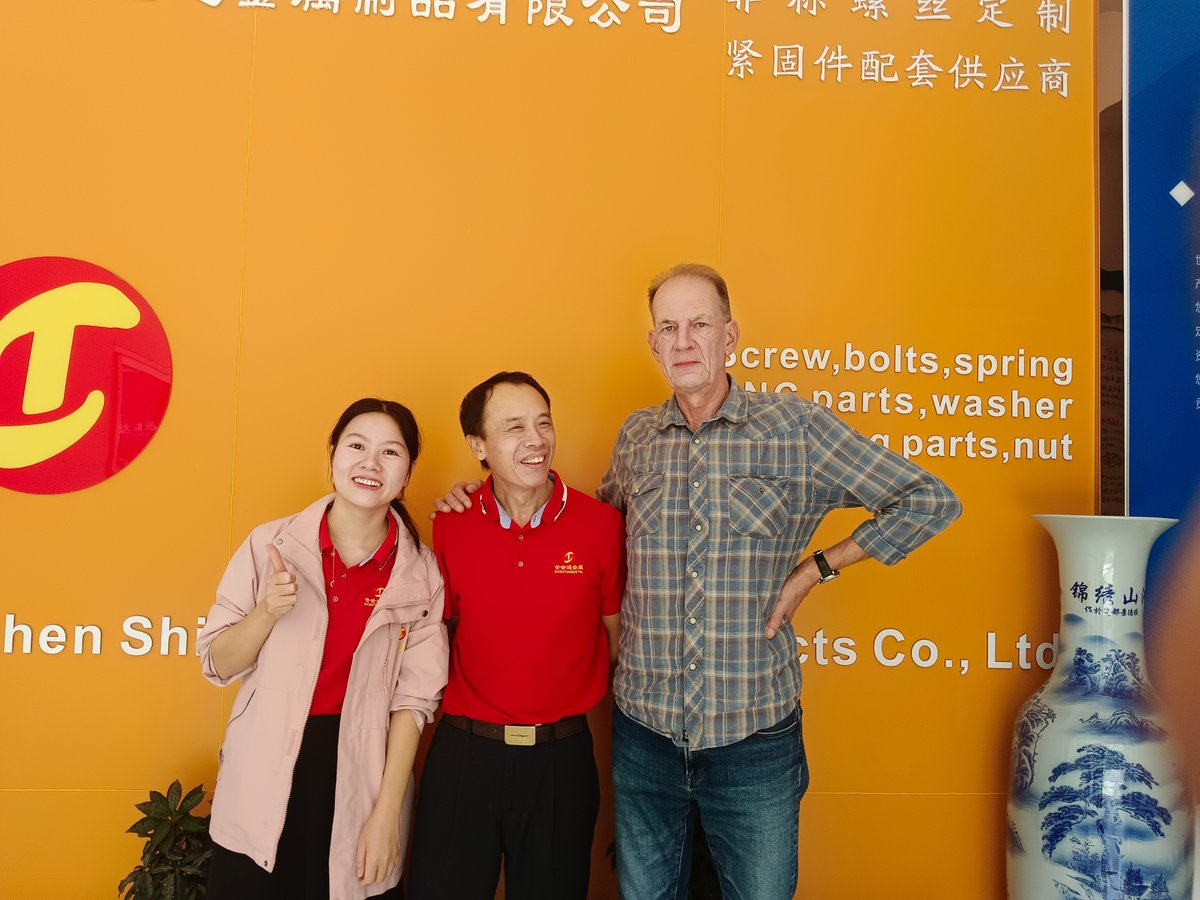
Customer visit – project kick-off |
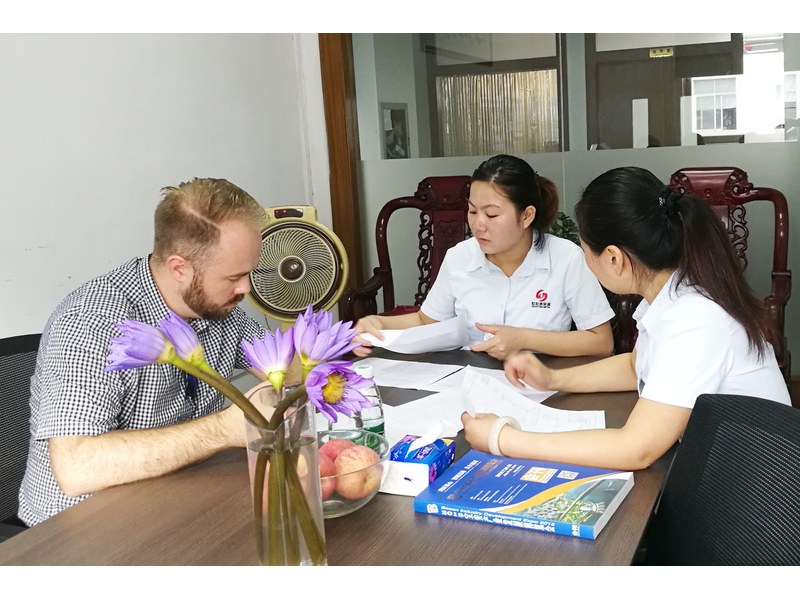
Danish customer – drawing review |
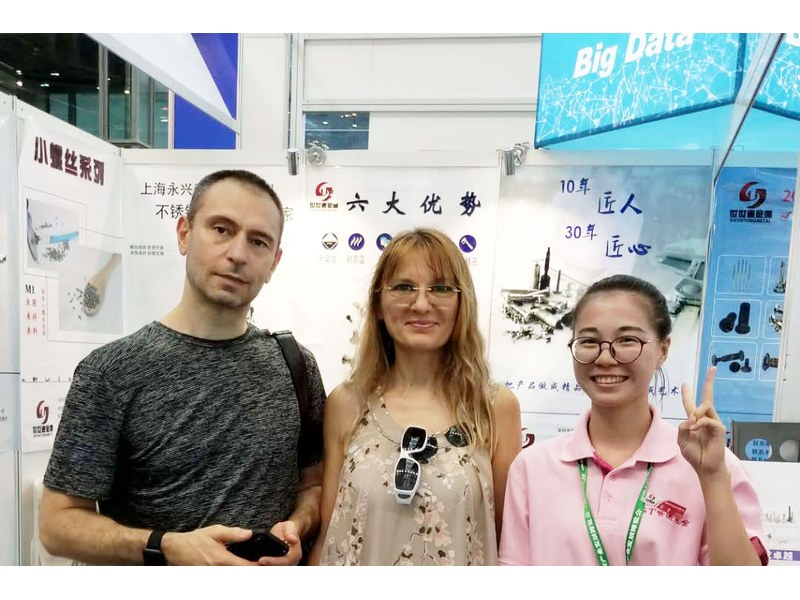
Industry exhibition – meeting customers |
A fastener made in pure copper, chosen for conductivity, thermal transfer or a soft contact face. Copper is soft and tarnishes, so the finish and the assembly method are part of the specification.
It is not turned from the head. The part is installed from the thread end, with a nut, or with a tool that grips the small shank; the drawing review fixes which method before the part is made.
The head sits almost flush in a recess, or the dished face acts as a flat contact pad. Head height and face form are checked on the first article, because the face is the working surface.
Red copper screws are quoted from M2 to M8 and up to 100 mm, measured from the head face. Where a long version is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
Not always. Bare copper has the highest conductivity and tarnishes; plating such as nickel, tin or silver gives a stable or solderable surface at some cost in resistance. The drawing decides.
Thread size and class, thread length, shank diameter, total length from the head face, head diameter, height and face form, material, finish and the assembly method.
How a red copper screw project runs from drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
Face and assembly review
|
→ |
3
First article approval
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a red copper screw quotation, send the drawing with the thread and class, thread length, shank diameter, total length from the head face, head diameter, height and face form, material, finish, and the assembly method.
|
Thread size and class
|
Thread and shank
|
Total length from head face
|
|
Head diameter, height and face form
|
Copper grade and finish
|
Assembly method and quantity
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.
 +86 13143444311
 sst@szsst88.com