Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
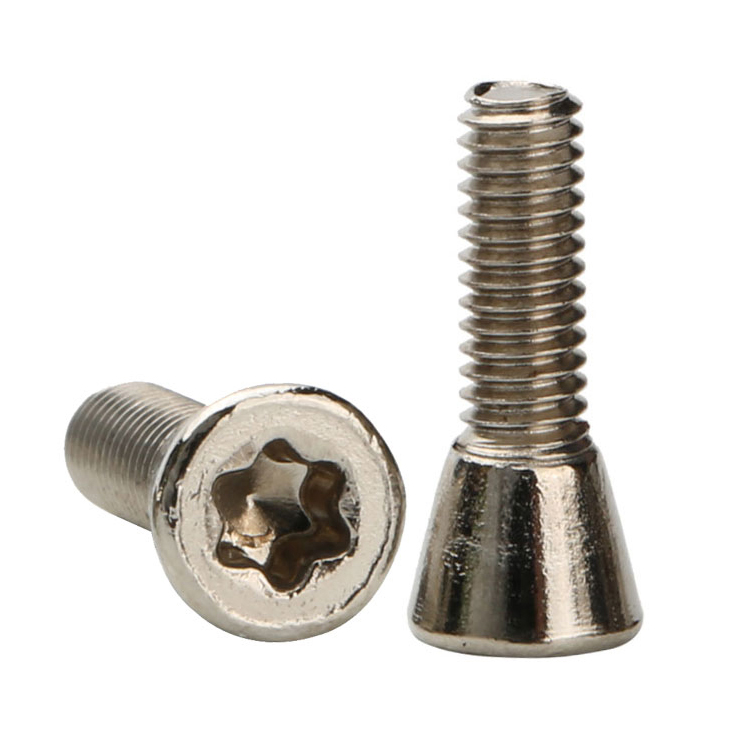
Type:Metric Torx Flat Head Screws
Materials:Carbon Steel
Surface treatment:Nickel
Head Type:Flat Head
Drive:Torx six-lobe recess (T-size matched to the thread)
Thread:Metric machine thread, rolled 60 degrees, full to the head cone
Point:Blunt end with a small chamfer; no taper, no drill point
Forming:Single-die heading, thread rolling, nickel plating, sorting
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:840
We manufacture metric torx flat head screws with a 90-degree countersunk head, a six-lobe star recess and a rolled machine thread, in carbon steel with a bright nickel finish. Head and cone, recess size, thread and length are taken from your drawing.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Metric torx flat head screws are machine screws with a countersunk head and a six-lobe star recess, sized to the metric thread system. The recorded item on this page is carbon steel with a bright nickel finish, and the six-lobe drive is what separates it from the cross-recess screws in the same family, quoted from M1 to M14 with Number 840.
Metric sizing. Diameter and pitch in millimetres, so M3 × 0.5 or M4 × 0.7 — the pitch is part of the size and does not interchange with a fine pitch of the same diameter.
Flat head. A 90-degree cone under the crown that seats in a countersink and finishes flush. The head is not domed above the surface; it is meant to disappear into it.
Torx recess. Six lobes with straight walls, driven with a matching star bit. The bit engages on six faces rather than four tapered ones, so it does not cam out in the way a cross does and it transfers more torque into a flush head.
Machine thread. A rolled thread for a tapped hole or a nut, with a blunt end. This is not a self-tapping part — the thread it engages is already there.
Nickel finish. A bright, hard deposit that protects the steel and keeps the cone face clean where the fixing meets the panel.
The 90-degree cone and the six-lobe recess are formed in one heading stroke. On a flat head that concentricity matters: the cone is the bearing surface and the recess is the only place the tool can act, so a recess formed off centre makes the bit push the head sideways and the cone bites the countersink on one side.
The lobes are cut to the standard star series that matches the thread size. A recess that is a size small will take the bit only part way and cam out at a fraction of the intended torque; one that is a size large will not drive the screw at all.
The thread is rolled and runs to the underside of the cone. Rolling work-hardens the flank, which is what gives the thread its wear resistance in a joint that is opened more than once, and it leaves a surface that gauges consistently.
The end is blunt with a small chamfer. It cannot start a hole of its own, and the chamfer is what lets the first thread enter a tapped hole without catching on the lead-in.
Nickel plating follows rolling. It covers the cone, the recess walls and the thread crests, and it adds a few microns — so metric torx flat head screws are gauged after plating and the recess is checked with the production bit in the same condition.
The family is quoted from M1 to M14, with M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14 in the recorded range. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission; on metric torx flat head screws the length is quoted overall because the head sits below the surface, and the countersink depth is what has to be subtracted.
| Item | How it is defined | What we control |
|---|---|---|
| Thread | Metric machine thread, rolled | Gauged per batch after plating |
| Cone angle | 90 degrees, to match the countersink | Checked on the projector |
| Head diameter | About twice the thread diameter | Measured on the first article |
| Recess | Six-lobe star, sized to the thread | Checked with the production bit |
| End | Blunt with a small chamfer | Checked on the first article |
| Length | Overall, top of head to end | Measured on the shop plate |
The head diameter is what covers the countersink, and it is worth checking against the panel before ordering. At about twice the thread the head covers a normal hole with margin; where the countersink is wide or the hole has opened up, the next size up is the honest answer.
The recess size is what the assembly depends on. A star bit that is the right size lasts a long time in a flush head because it does not cam out; a bit that is one size small will round the lobes, and on a recessed head the damage is hidden until the screw has to come out again.
A flat head has no material to spare above the surface, so the drive has to look after itself. That is the argument for the star recess on this part.
| Feature | What it gives | What it costs |
|---|---|---|
| Six-lobe recess | High torque, no cam-out, long bit life | Needs the matching star bit |
| Flat head | Flush finish, nothing to catch | Cone must match the countersink |
| Metric thread | Standard worldwide | Fine and coarse pitches do not interchange |
| Full thread to the cone | Engagement over the whole working length | No plain shank to centre the screw |
| Nickel finish | Hard, bright, even cone face | A few microns; recess re-checked |
A cross recess in a countersunk head has a problem that a domed head does not: when the bit cams out, it lifts and the wings scrape the recess, and there is no head material around it to absorb the damage. A star bit pushes down the axis of the screw rather than wedging, so the head stays seated while the torque goes into the thread.
The trade is tooling. A star bit is not the driver most benches already have, so a line that converts to torx has to change its bits and its torque settings. On a joint that is assembled a few times and then left alone, that is a small cost; on a maintenance joint opened weekly, it is worth checking that the bit is available where the work happens.
The recorded finish is bright nickel, applied after the thread is rolled. Nickel is harder than zinc and takes a polish, which matters on a countersunk head because the visible surface is a ring of cone set into the panel.
| Finish | How it protects | Effect on cone and recess | Typical use |
|---|---|---|---|
| Bright nickel | Hard metallic deposit | A few microns; seat checked after plating | Visible flush fixings |
| White zinc | Sacrificial zinc, blue-white passivation | Thin; gauged after | General indoor assembly |
| Black zinc | Zinc with black passivation | A few microns; recess re-checked | Dark panels |
| Dacromet | Zinc-aluminium flake layer, cured | Thin film; seat re-checked | Outdoor and wet assemblies |
| Stainless (equivalent part) | Alloy provides protection | No coating | Wash-down and coastal work |
The cone is where plating is judged. A deposit changes its fit in the countersink by a few microns, which is enough to move the contact ring and make a flush head look sunk or proud depending on the light. That is why the first article is seated in a countersink sample after plating rather than measured on a bare part.
The recess is the second surface to watch. Nickel throws into a recess less evenly than onto a flat face, and a star recess that is slightly tight after plating is harder to seat than a cross. The first article is driven with the production bit, and the batch follows that sample.
Three assemblies where a flush head and a non-cam-out drive are both useful:
| Where it sits | The screw holds a plate or a bezel down in a countersink where the face has to stay flush and the fixing is tightened without a hand steady on the driver. |
| When it goes wrong | A cross recess cams out on a flush head and marks the face, and a proud head breaks the plane of the panel. |
| Why it happens | The face is visible, the fixing is flush, and the assembly is tightened to a setting. |
| What we control | Cone seated in a countersink sample, recess driven with the production bit after plating. |
| Where it sits | The screw fixes a trim plate, a cover or a bracket where the head must not stand above the surface and the joint sees vibration. |
| When it goes wrong | A cam-out on a cross recess leaves a bright scar on a dark finish, and a loose flush head rattles. |
| Why it happens | The joint vibrates, the face is finished, and the head is flush. |
| What we control | Seat and recess checked, thread gauged per batch. |
| Where it sits | The screw fixes a hinge plate, a connector or a bracket where the head sits below the surface and the drive has to work without a pilot hole in a soft material. |
| When it goes wrong | A cross recess rounds in a hard-plated head, and a head that is not flush catches on whatever slides over it. |
| Why it happens | The material is board or a composite, the fixing is flush, and the joint is made on a bench. |
| What we control | Point and length checked against the board sample, seat checked. |
Four reasons that matter on a star-drive flush screw, each tied to what the drawing has to prove:
|
Recess and cone reviewed together
The recess size, the cone angle and the head diameter are reviewed as one set, so a drive that will not seat the head is raised before tooling. Basis: Recess and cone reviewed as one set. |
Head, recess and thread in one route
The 90-degree cone and the six-lobe recess are formed in one stroke, and the thread is rolled to the underside of the cone. Basis: One route from wire to plated screw. |
|
Seat and drive checked on the part
The head is seated in a countersink sample and the recess driven with the production bit, both after plating. Basis: First article seated and driven. |
First article to repeat production
The first article fixes the drawing revision, wire heat, die set, thread roll and plating, and repeat orders are compared with that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these metric torx flat head screws on a single-die header that upsets the 90-degree cone and the six-lobe recess in one stroke, then rolls the machine thread to a blunt chamfered end. The parts are nickel plated and sorted. The first part of every run is seated in a countersink sample, driven with the production bit and gauged after plating, before the batch continues.


|

|
The star recess punch is the tool that has to be right. A worn punch leaves lobes that measure close and still allow the bit to lift, and on a flush head a lifting bit scars the crown of the screw and the face around it. The recess is therefore checked by driving rather than by gauging, and the punch is changed on that evidence.
What decides whether metric torx flat head screws pass is the cone, the head, the recess, the thread and the plating. The inspection agreement covers those, and the criteria come from the drawing.

Cone angle on the projector |

Thread gauged after plating |

Hardness testing against the property class |

Salt-spray testing of the nickel plate |
The seat is checked by driving the first article into a countersink sample and reading the contact ring. An even ring is a pass; a partial ring means the cone is not seating flat, which on a flush fixing is visible from across a room.
The recess is checked with the bit and inspected at the lobe corners. A star recess that has been damaged shows as a polished line along one flank rather than as a missing corner, and that line appears before the bit actually slips.
Every shipment of metric torx flat head screws is traceable to the wire it was made from and to the plating batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the plating. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a flush fixing the first article is seated in the customer’s countersink, because the seat is decided by the panel and not by the screw alone. Buyers visit during the process to review samples and to see how the heads are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header and the plating line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
A six-lobe star recess driven with a matching star bit. It engages on six faces, does not cam out like a cross, and transfers more torque into the head.
A flush head has no material to spare above the surface, so a bit that lifts scars the crown and the face around it. A star bit pushes along the axis instead.
Overall, from the top of the head to the end, because the head sits below the surface. The working length is that minus the countersink depth.
The star size that matches the thread; it is stated on the drawing. A bit one size small will round the lobes and the damage is hidden in the recess.
No. It has a blunt end and a machine thread, so it goes into a tapped hole or a nut rather than forming its own thread.
Thread size and pitch, head diameter and height, countersink angle, recess size, length and datum, material and finish.
How a metric torx flat head screw project runs from drawing to repeat delivery:
|
1
Send the drawing or a countersink sample
|
→ |
2
Cone and recess review
|
→ |
3
First article seated and driven
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size and pitch, head diameter and height, countersink angle, recess size, length and datum, material and finish.
|
Thread and pitch
|
Head diameter and height
|
Countersink angle
|
|
Recess size
|
Length and datum
|
Finish
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com