Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
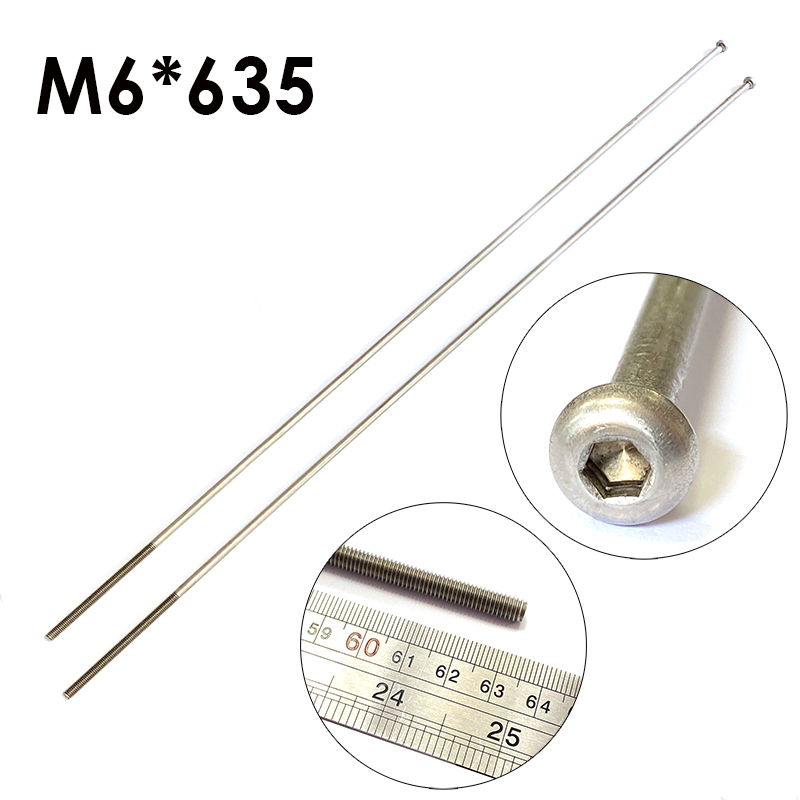
Type:Extra long hexagon socket pan head machine screw
Materials:Stainless steel
Surface treatment:Plain
Head Type:Pan head
Drive type:Socket
Thread:Partial (half) machine thread
Forming:Split-die cold heading (one-piece)
Number:1044
We manufacture extra-long M6 pan head machine screws in stainless steel, with a hex socket drive and a partial (half) machine thread, from M1.4 to M12 and up to 2,000 mm, formed one-piece by split-die cold heading and supplied plain or passivated. Head diameter, socket depth, thread start and material grade are made to your drawing.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
An M6 pan head machine screw combines three features that have to agree with each other: a 6 mm metric thread, a pan head with a rounded top and a flat bearing face, and a hex socket recess that takes an Allen key instead of a screwdriver. Make the screw extra long and a fourth condition appears: the shank has to carry the head through a long stack while the thread only bites at the far end.
Pan head bearing area. The pan head spreads load over a wider face than a cheese or fillister head of the same thread, and the rounded top keeps the head from catching on a moving part. On an M6 pan head machine screw the head diameter and the bearing face are dimensioned together, because the face is what clamps the plate, not the thread.
Hex socket and torque. The socket drives from inside the head, so the head can sit close to a wall or inside a bore where a Phillips driver cannot reach. A long screw driven from a socket needs the recess to be cut concentric with the shank; if the socket is off centre the key cocks over and the head walks sideways as it tightens.
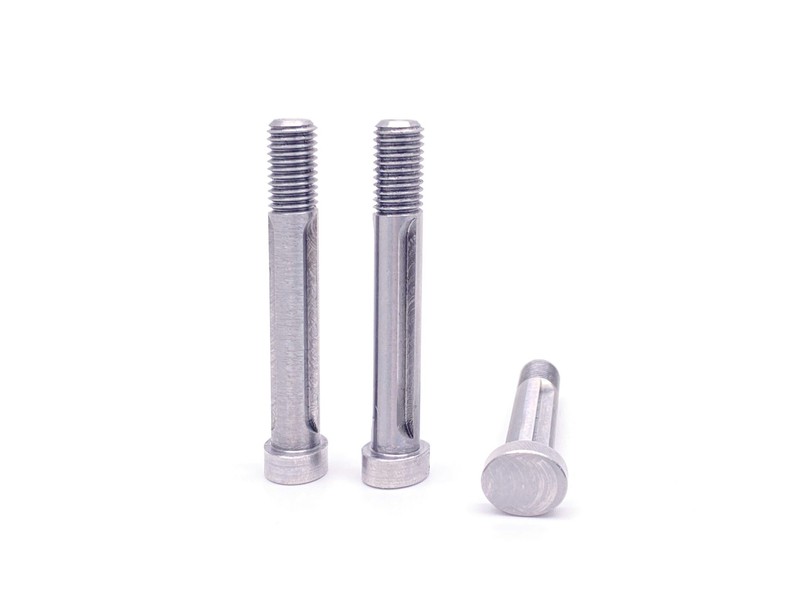
Partial thread on a long shank. The plain shank passes through the plates or spacers and the thread engages only in the last section, which keeps the thread out of the shear plane and lets the stack slide into place before the screw is turned.
On a stainless M6 pan head machine screw the finish is the metal, so a burr left at the socket or under the head cannot be hidden by plating. Deburring and a clean passivated surface are part of the part, not an afterthought.
A long M6 pan head machine screw is formed in one piece on a split-die header. The die opens along the shank, so the head and the first part of the shank are headed from the same billet even when the finished length is far beyond a standard heading window. A welded or brazed shank is not the default for this part, and for stainless work it is not used at all.
The reason is not cost. A joint under the head or down the shank is a corrosion cell in stainless steel and a fatigue origin in any steel; it also sits under the same passivation as the rest of the screw, so nothing about it looks different until it fails. Forming the shank in one piece removes that risk from the drawing review stage.
The die set fixes head form, socket position and thread start together. The thread is rolled after forming, because rolling moves material rather than cutting it and leaves an uninterrupted grain flow at the thread root. When the length or the head changes, the die insert and the thread rolls change with it, and the first parts of each run go to the gauges before the run continues.
M6 pan head machine screws are quoted as part of a family that runs from M1.4 to M12 and up to 2,000 mm. Length is normally held to +0/-2 mm on the drawing, and custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
| Item | How it is defined | What we control |
|---|---|---|
| Total length | From the bearing face under the head to the tip | Datum stated on the drawing; length measured on the shop plate |
| Head diameter and height | Pan head envelope and the face that clamps the plate | Head diameter and bearing face checked against the drawing |
| Socket size and depth | The hex recess that takes the Allen key | Socket cut concentric with the shank, checked with the matching key |
| Thread length and position | Where the thread starts and how far it runs | Thread start position taken from the drawing, not from a sample |
| Plain shank length | The unthreaded span through the stack | Shank diameter and length held to the stack it passes through |
Diameter and length are quoted per part, and each M6 pan head machine screw combination is checked against the drawing before a quotation is issued. A long M6 and a short M6 in the same thread class take different routes through heading and rolling, so the check confirms that the route can hold both the length and the thread start.
Length is measured from the bearing face, not over the thread, and the thread length is read as a position from the same datum. Head diameter, socket depth and thread start are gauged on the first article before a batch is released, because those three dimensions decide whether the screw clamps the stack or bottoms out before it does.
For an M6 pan head machine screw the drawing fixes five things: thread size and pitch (M6x1.0 unless the drawing says otherwise), thread length and position, plain shank length, total length and its datum, and right- or left-hand direction. A sixth line matters on stainless parts: the grade and the surface condition the parts are supplied in.
| Parameter | Why it matters on a long M6 screw | What we control |
|---|---|---|
| Thread start position | It sets where the plain shank ends and where the clamped stack sits | Start dimension checked on the first article and per batch |
| Engaging length | Too short leaves the joint weak; too long runs the thread into the stack | Thread length and position taken from the drawing |
| Socket size and depth | The Allen key must seat fully without bottoming in the recess | Socket gauged with the matching hex key after finishing |
| Handedness | A left-hand thread on a right-hand assembly will not pull the joint closed | Direction marked on the part and on the packing |
A stainless M6 pan head machine screw is supplied with the metal as the finish. There is no plated layer to build up the thread or fill the socket, so the thread fits at nominal size and the socket keeps the dimensions it was cut to. What the part does need is a clean, burr-free surface and passivation where the drawing calls for it, because free iron left on the surface is what starts corrosion, not the alloy itself.
| Finish | How it protects | Effect on thread and socket | Typical use |
|---|---|---|---|
| Plain / passivated stainless | Clean alloy surface, oxide film restored by passivation | No added thickness; thread stays at nominal size | Stainless assemblies, indoor and damp service |
| Electropolished stainless | Surface levelled and enriched in chromium | Slightly brighter, burrs removed, no dimensional change | Laboratory, hygienic and instrument equipment |
| Passivated plus light oil | Passive film plus a temporary barrier for transit | No dimensional change; oil is cleaned before use | Parts that ship or store before assembly |
| Zinc electroplated (carbon steel) | Sacrificial zinc layer | Build-up on the flank; socket may need masking | Carbon steel parts in dry indoor service |
| Dacromet flake (carbon steel) | Zinc-aluminium flake layer | Thin and even; a few microns in the thread | Wet or outdoor carbon steel assemblies |
Plain stainless parts are checked for finish and cleanliness rather than salt spray; salt-spray exposure is agreed only where the drawing specifies a coating. Parts are degreased and deburred before passivation, and the socket is cleaned after deburring so no cutting compound is left in the recess where a key will sit.
Packing protects the head and the thread in transit. Long screws are packed in layers with the heads supported, so the shank cannot take a set under its own weight, and the thread section is kept away from the carton wall. Batch and material information go on the label, so the part that arrives matches the record used for gauging.
Three assembly conditions where a long M6 pan head machine screw has to hold a stack together, and what it has to do instead:
Automation and robot gantry frames
|
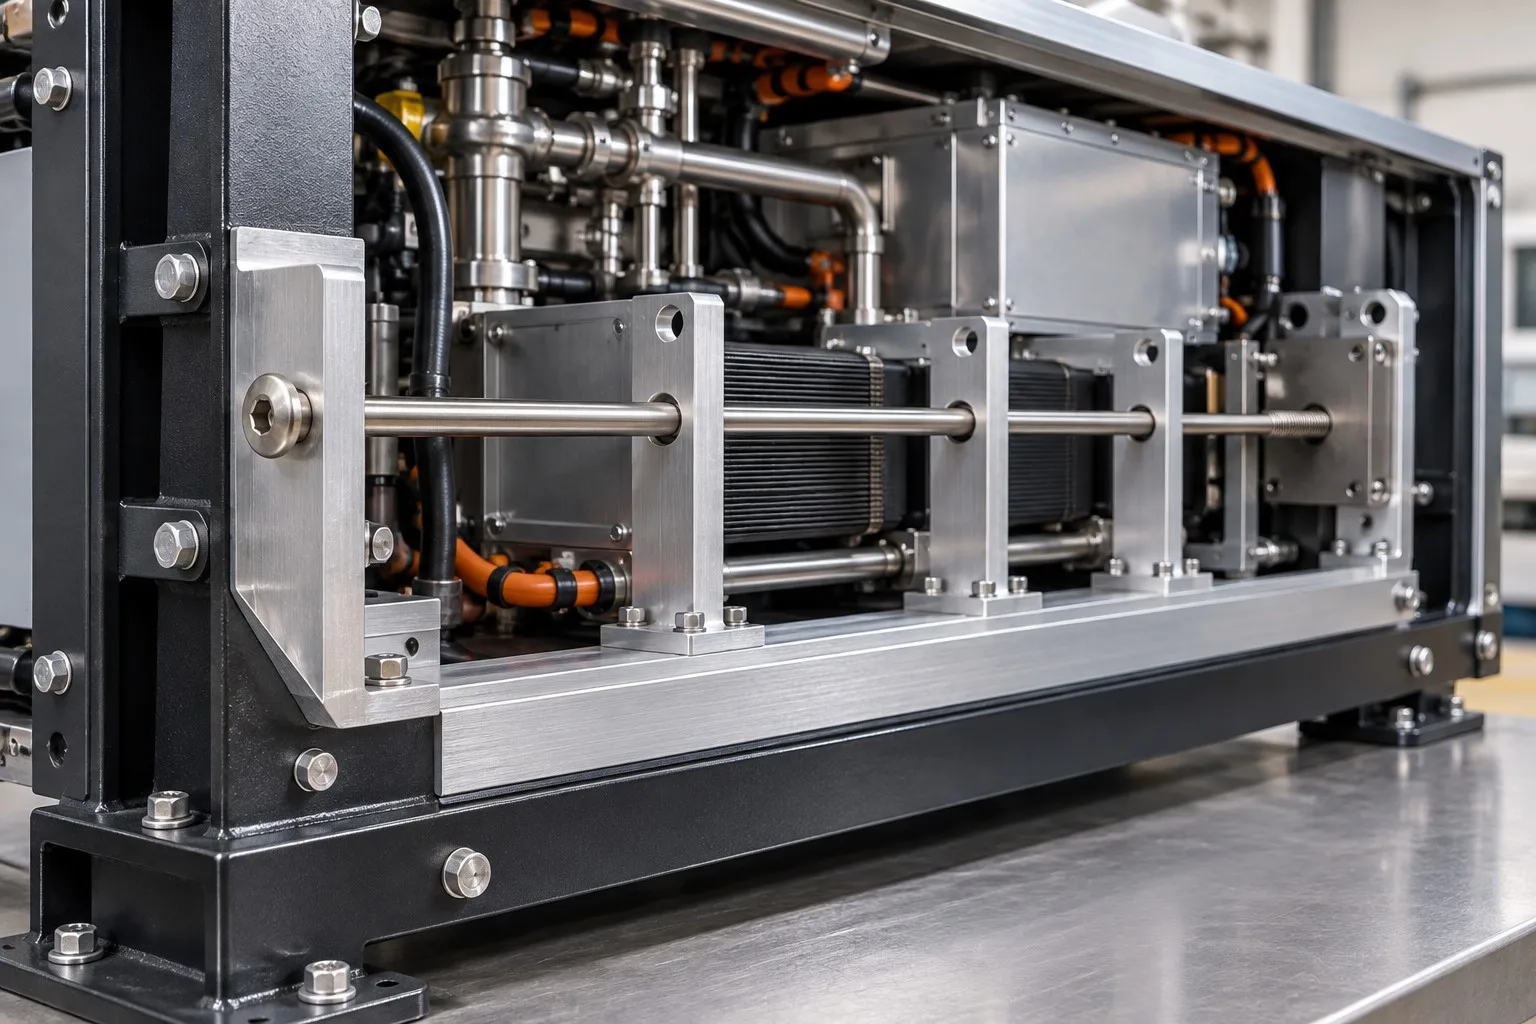
Robot gantry – long screws through machined blocks |
Battery module and pack racks
|
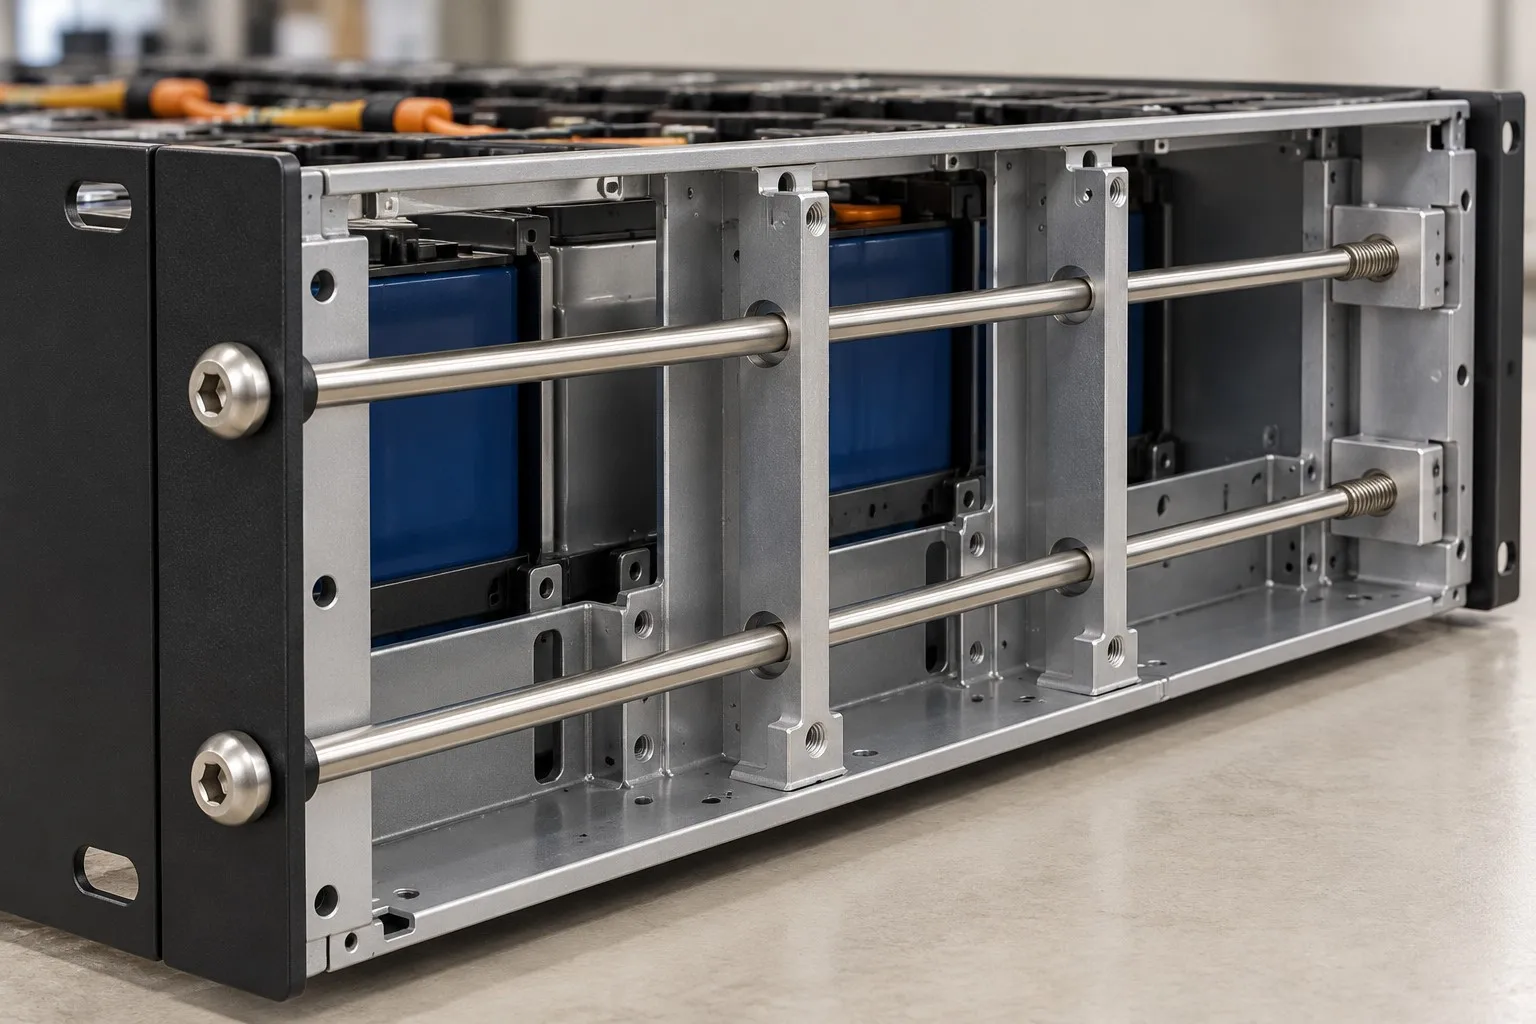
Battery module – screws clamping the pack frame |
Chemical process skids and instrument racks
|
Chemical skid – stainless hardware on instrument frames |
Four reasons that matter specifically on a long M6 pan head machine screw, each tied to what the drawing has to prove:
|
Engineering review before tooling
Head diameter, socket depth and thread start are settled before a die is cut, so the first sample is measured against the drawing instead of against a guess. Basis: Drawing or sample reviewed before tooling is released. |
One piece, formed in a split die
A long M6 pan head machine screw is headed in one piece on a split-die header. A welded shank is never the default, so no joint can hide under the passivation. Basis: One-piece split-die heading route, no welded shank. |
|
Socket and thread gauged on the part
The hex recess is checked with the matching key and the thread with GO/NO-GO gauges, so the key that reaches the recess on the bench is the key the customer uses. Basis: Socket checked with the matching hex key; thread gauged GO/NO-GO. |
From approved sample to repeat production
The first article fixes the drawing revision, material heat, die set and thread rolls; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
These M6 pan head machine screws are formed, not assembled. Stainless wire goes through the heading aisle; on a split-die header the die opens along the shank so the head and the first part of the shank come from the same billet, and the operator sets the die and checks the first parts against the drawing before the run is released. The thread is rolled after forming, the socket is formed with the head, and the parts are deburred and passivated before final gauge.


|

|
Between runs the die is changed to the drawing length and head form; the first parts go to the gauges before the run continues, and the setting is recorded. Parts that pass the bench checks are packed in layers so a long shank is supported over its length rather than hanging from the head.
What decides whether an M6 pan head machine screw passes is not its appearance: it is the head and bearing face against the clamped part, the socket fit against the key in service, and the thread fit in the condition it ships in. The inspection agreement covers those, and the criteria are the ones written on the drawing rather than a generic standard.

Thread gauging against GO/NO-GO gauges |

Head diameter and profile on the optical projector |

Hardness testing of the base material |

Salt-spray testing where a coating is specified |
Each batch is recorded against the drawing revision: head diameter and height from the first article, the socket checked with the matching hex key, thread gauging per batch, and the material heat number on the certificate. If a gauge or the key fit fails, the parts back to the last good setting are held and re-checked before anything ships.
An outside report on the material, where the drawing asks for one, is filed with the batch so the paperwork and the parts share one batch number.
Every M6 pan head machine screw shipment is traceable to the material it was made from. The grade, heat number and standard are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. Buyers visit during the process to review samples and to see the forming, threading and finishing steps their parts will go through.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header, the thread rolling and the finishing line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
An M6 pan head machine screw is a 6 mm metric machine screw with a pan-shaped head, a flat bearing face and a hex socket recess for an Allen key. On long parts the head, socket and thread start are dimensioned together so the shank carries the head through the stack.
M6 pan head machine screws are quoted from M1.4 to M12 and up to 2,000 mm, with length usually held to +0/-2 mm. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
This part is specified with a partial (half) machine thread: the plain shank passes through the stack and the thread engages only at the far end. Thread length and start position come from the drawing.
The grade is the one written on your drawing, and the material certificate records the grade, heat number and standard that were used for the batch.
With the matching hex key after finishing: the key must seat to the recess depth without bottoming, and the socket is formed concentric with the shank so the key does not cock over under torque.
Thread size and pitch, thread length and position, plain shank, total length and datum, head diameter and height, socket size and depth, material grade, surface condition, and quantity.
How an M6 pan head machine screw project runs from drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
DFM review and quotation
|
→ |
3
First article approval
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For an M6 pan head machine screw quotation, send the drawing with thread size and position, plain shank and total length with its datum, head diameter and height, socket size, material grade and surface condition. Head, socket and thread start are confirmed with you before production.
|
Thread size, pitch and length position
|
Plain shank length
|
Total length and datum
|
|
Head diameter and height
|
Socket size and depth
|
Material grade and quantity
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com