
Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
Type:High-low screw for plastic, ultra-low Torx head
Materials:Carbon steel
Surface treatment:White zinc plated
Head Type:Ultra low head
Drive type:Torx (internal)
Thread:High-low thread for plastics
Forming:Single-die cold heading
Number:1830
We manufacture high-low screws for plastic in carbon steel, white zinc plated, with a high crest that cuts the thread in the plastic and a low crest that follows in the same groove, under an ultra-low Torx head, from M2 to M8. Crest diameters, phase, head height, Torx size and plating are made to your drawing.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
This is a thread-forming screw with two thread starts: one series of high crests and one of low crests, alternating around the shank. The high thread cuts the path into the plastic, and the low thread follows in the same groove, so the screw drives with less torque and holds with more thread contact than a single-start screw of the same size.
Two threads, one groove. The high crest leads and forms the thread in the boss; the low crest sits inside the same groove behind it. Because the low crest does not cut new material, the driving torque drops, and because both crests bear on the formed thread, the pull-out and strip resistance rise.
Ultra-low head. The head is turned down to an ultra-low profile with a small shoulder, so it sits almost flush in a plastic housing without a deep counterbore. A standard pan head would stand proud of a thin wall and catch on the mating part.
Torx recess. The Torx recess takes the driving torque that a small head can carry, without the cam-out that a Phillips recess shows when the head is this low. The recess is formed with the head, so the driver axis and the thread axis stay together.
White zinc on carbon steel. The zinc layer protects the carbon steel and the Torx recess. It also adds thickness to the high and low threads, so the thread form is gauged after plating, in the condition the screw is driven in.
The thread is not a machine thread. It is a double-start, asymmetric form: two crest heights, one lead, and a flank angle chosen for the plastic being joined. The screw forms its own thread in a moulded boss or a pilot hole, and it can be removed and re-driven a limited number of times before the formed thread strips.
The high crest does the cutting. Its diameter is larger than the pilot hole, so it displaces and shears a thread into the plastic; the low crest is smaller and rides in the groove the high crest has just cut. If the two crests are out of phase, the low thread cuts its own path and the driving torque doubles.
The pilot hole and boss are part of the joint, not the screw. The screw is specified with a pilot diameter and a boss wall thickness, and the drawing review checks those against the thread form. The same screw in an undersized hole will strip the boss, and in an oversized hole it will not hold.
High-low screws for plastic are quoted from M2 to M8 and in lengths from a few millimetres to 50 mm, with length usually held to +/-0.1 mm on the drawing. Where a longer version is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
| Item | How it is defined | What we control |
|---|---|---|
| Total length | From the top of the head to the tip | Datum stated on the drawing; length measured on the shop plate |
| Head diameter and height | The ultra-low head and its small shoulder | Head height held so the head sits near flush |
| High and low thread diameters | The two crest heights | Both crests checked after plating |
| High-low pitch and phase | How the two starts line up | Thread form checked on the optical projector |
| Torx recess size | The recess that takes the T driver | Recess checked with the matching bit after coating |
Each thread size and length combination is checked against the drawing before a quotation is issued. On this screw the two crest diameters and their phase are the dimensions that decide whether the screw drives, so both are gauged on the first article and again after plating.
Length is measured from the top of the head, and head height is read from the same datum. The recess is checked with the Torx bit after the zinc line, because the coating builds up in the recess and a bit that fits before plating may not seat after it.
The ultra-low head on this high-low screw for plastic is formed in the heading die together with the shoulder and the Torx recess. Head height is kept low enough that the head disappears into a shallow counterbore, while the shoulder keeps a bearing face wide enough to clamp the plastic without cracking it.
A head this low leaves little material over the recess. The Torx punch has to be set so the recess depth leaves a full-driving section under the head without breaking through; the drawing pairs head height and recess depth, and the pair is checked on the first article.
Because the recess is the only place the driver can grip, it is gauged with the matching T bit after the white zinc is applied. A recess that looks deep enough can still be a few tenths shallow, and the bit will cam out on the first drive. The recess is therefore checked on the first article and again after plating, with the same bit the customer will use.
White zinc is an electroplated zinc layer applied after heading and thread rolling. On a high-low screw for plastic it protects the carbon steel and the formed threads, but it also changes the high and low crest diameters, so the thread form is specified with the plating and gauged after it.
| Finish | How it protects | Effect on thread and recess | Typical use |
|---|---|---|---|
| White zinc plated | Electroplated zinc layer | Build-up on both crests; gauged after plating | Appliance and electronic plastic housings |
| Blue zinc plated | Electroplated zinc layer | Same build-up; gauged after plating | General indoor assemblies |
| Black oxide | Conversion coating, minimal thickness | No measurable build-up | Dark plastic housings |
| Zinc-nickel | Zinc alloy with higher corrosion resistance | Thicker film; thread form re-checked | Damp service |
| Dacromet flake | Zinc-aluminium flake layer | Thin film; thread checked over the coating | Outdoor plastic assemblies |
Salt-spray exposure is agreed per project and written on the drawing. For a high-low screw for plastic the acceptance state is after plating, not after cleaning, because the joint is assembled with the plated thread and the plastic sees the coating as it forms its own groove.
Packing protects the head and the two thread crests. Screws are packed in layers or bags with the count stated, the ultra-low heads are kept apart so the shallow recess is not nicked, and the label carries the batch and the plating run.
Three assembly conditions where a high-low screw for plastic forms a thread in a moulded boss and holds it through service, and what it has to do instead:
Appliance and white goods housings
|
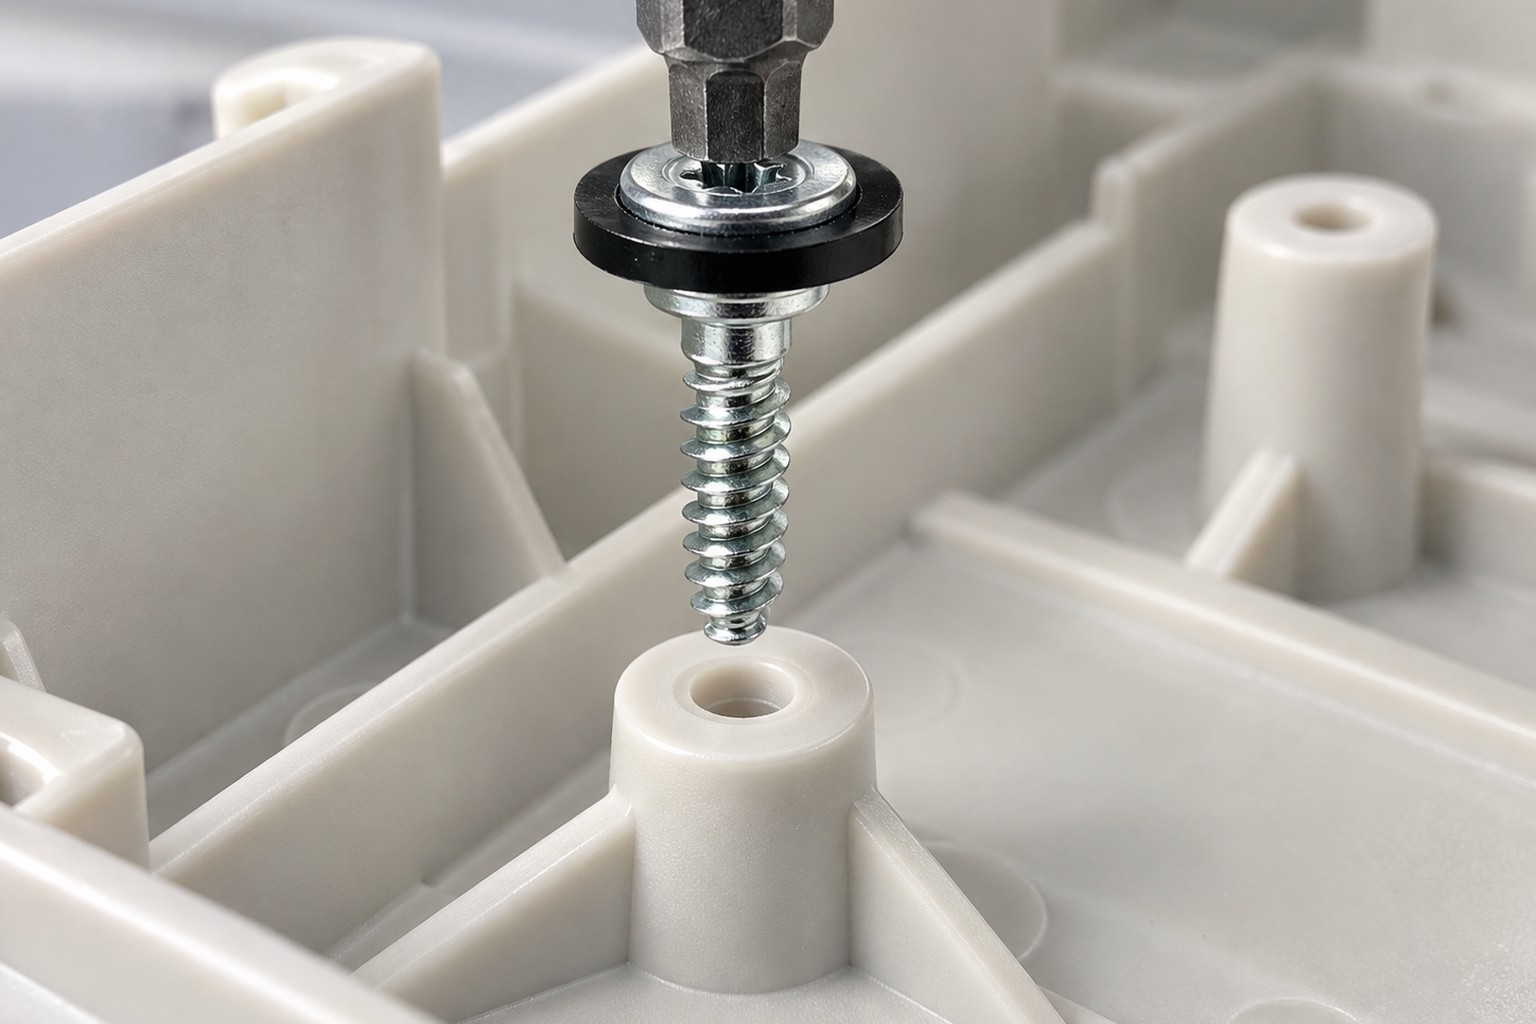
Appliances – thread formed into a moulded plastic boss |
Electric motors and small drive units
|
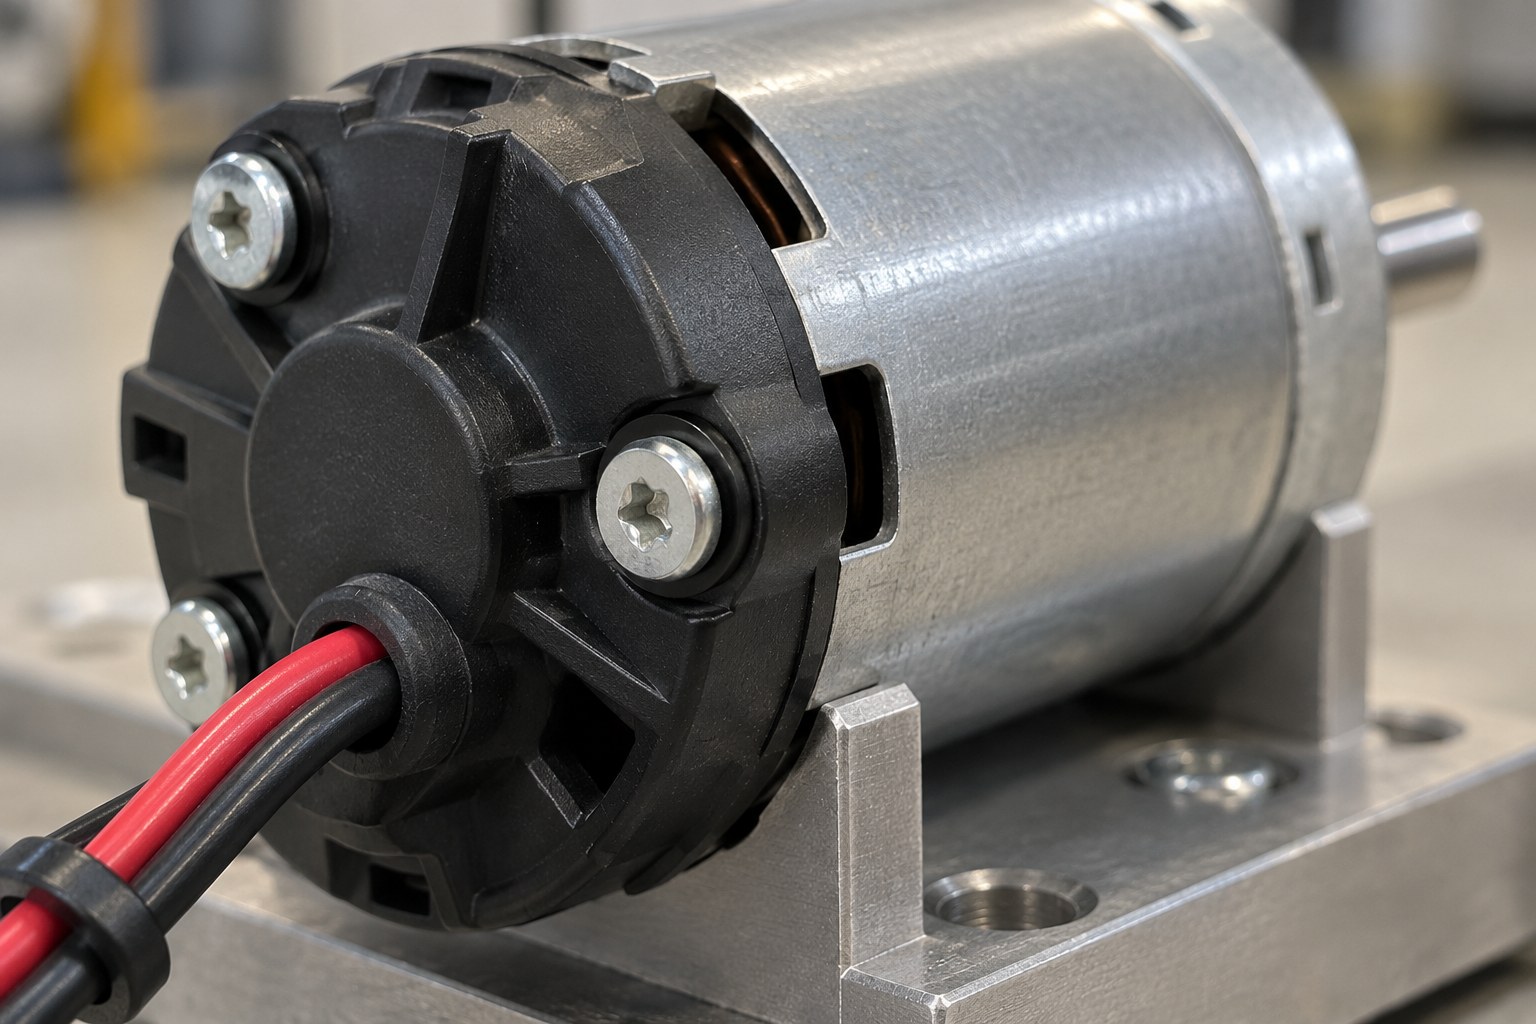
Motors – plastic covers held by high-low threads |
Self-service equipment plastic panels
|
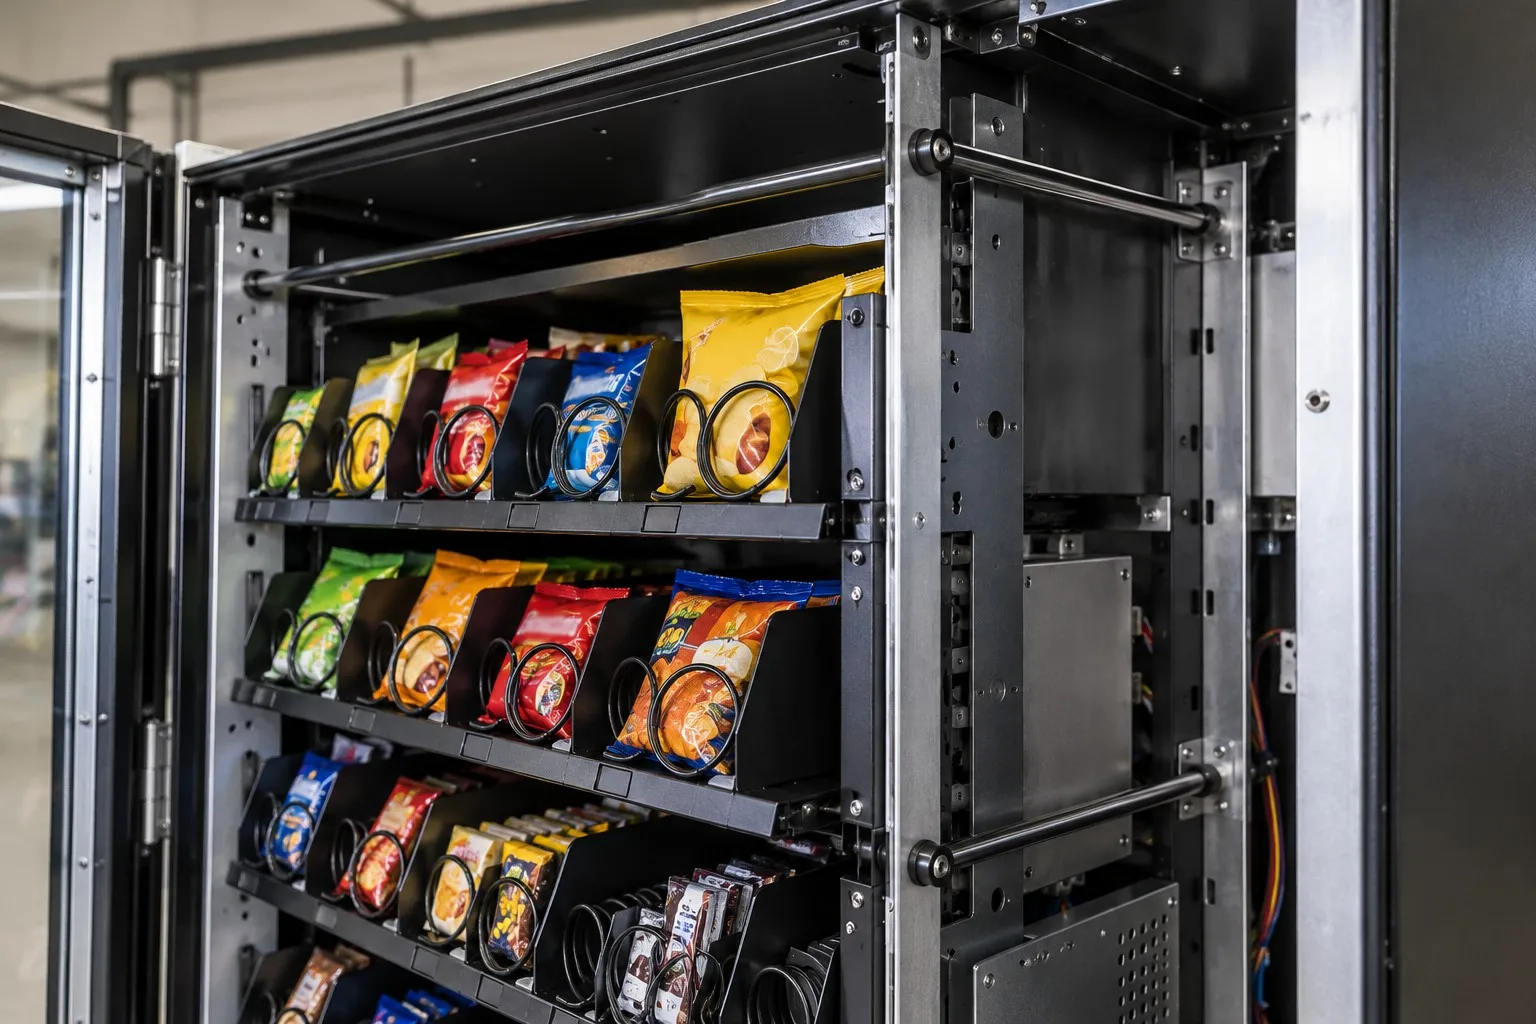
Kiosks – high-low screws in moulded plastic trim |
Four reasons that matter specifically on a high-low screw for plastic, each tied to what the drawing has to prove:
|
Engineering review before tooling
High and low crest diameters, phase, head height and recess depth are settled before a die is cut, so the first sample is measured against the drawing instead of against a guess. Basis: Drawing or sample reviewed before tooling is released. |
Both thread starts in one heading route
The high-low thread is produced on the heading and rolling route, so the two starts keep their phase and the head keeps its recess on the same axis. Basis: One-piece heading route, two thread starts in phase. |
|
Crests, phase and recess gauged
Both crest diameters and their phase are checked on the projector, and the recess with the matching Torx bit, so the screw drives as it was approved. Basis: High-low form and recess gauged on the first article. |
First article to repeat production
The first article fixes the drawing revision, material heat, die set and recess tooling; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
These high-low screws for plastic are formed on a single-die header. The ultra-low head, the shoulder and the Torx recess are formed in the die, the high-low thread is produced on the thread-rolling route, and the parts are then white-zinc plated and gauged. The operator checks the first parts of each run against the drawing before the batch continues.


|

|
Between runs the die insert is changed to the drawing head form and the thread rolls are set to the high-low pitch; the first parts go to the projector before the run continues, and the setting is recorded. Parts that pass the bench checks are packed so the ultra-low heads and the two crests are not damaged.
What decides whether a high-low screw for plastic passes is not its appearance: it is the two crest diameters and their phase, the head sitting in the counterbore, and the Torx recess taking the driver after plating. The inspection agreement covers those, and the criteria are the ones written on the drawing.

Thread gauging of the high-low form |

High and low crest profile on the optical projector |

Hardness testing of the carbon steel |

Salt-spray testing of the white zinc |
Each batch is recorded against the drawing revision: head height and recess from the first article, both crest diameters and their phase on the projector, and the coating thickness on the body. If a gauge or the phase check fails, the parts back to the last good setting are held and re-checked.
Where a third-party report is required for the material or the plating, it is listed on the drawing so the paperwork ships with the parts, and the batch number on the label matches the record used for the gauge.
Every high-low screw for plastic shipment is traceable to the wire it was made from. The grade, heat number and standard are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the plating. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. Buyers visit during the process to review samples and to see the forming, threading and plating steps their parts will go through.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header, the thread rolling and the plating line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
It is a thread-forming screw with two thread starts: a high crest that cuts the thread in the plastic and a low crest that follows in the same groove. It drives with less torque and holds with more thread contact than a single-start screw.
The low crest does not cut new material. It rides in the groove opened by the high crest, so driving torque drops while both crests bear on the formed thread and resist pull-out and strip.
The pilot diameter and boss wall are part of the joint. They are checked against the thread form on the drawing, because an undersized pilot cracks the boss and an oversized one will not hold.
High-low screws for plastic are quoted from M2 to M8 and up to 50 mm, usually held to +/-0.1 mm. Where a longer version is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
It depends on the plastic and the boss. Each re-drive cuts the formed thread again, and the drawing or the sample review fixes how many cycles the joint is expected to take.
Thread form and pitch, high and low crest diameters, total length and datum, head diameter and height, Torx size, material, plating, pilot hole and boss wall, and quantity.
How a high-low screw for plastic project runs from drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
DFM review and quotation
|
→ |
3
First article approval
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a high-low screw for plastic quotation, send the drawing with thread form and pitch, high and low crest diameters, total length and datum, head diameter and height, Torx size, material and plating, plus the pilot hole and boss wall if the joint is fixed.
|
Thread form and pitch
|
High and low crest diameters
|
Total length and datum
|
|
Head diameter and height
|
Torx size
|
Material, plating and quantity
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com














