Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
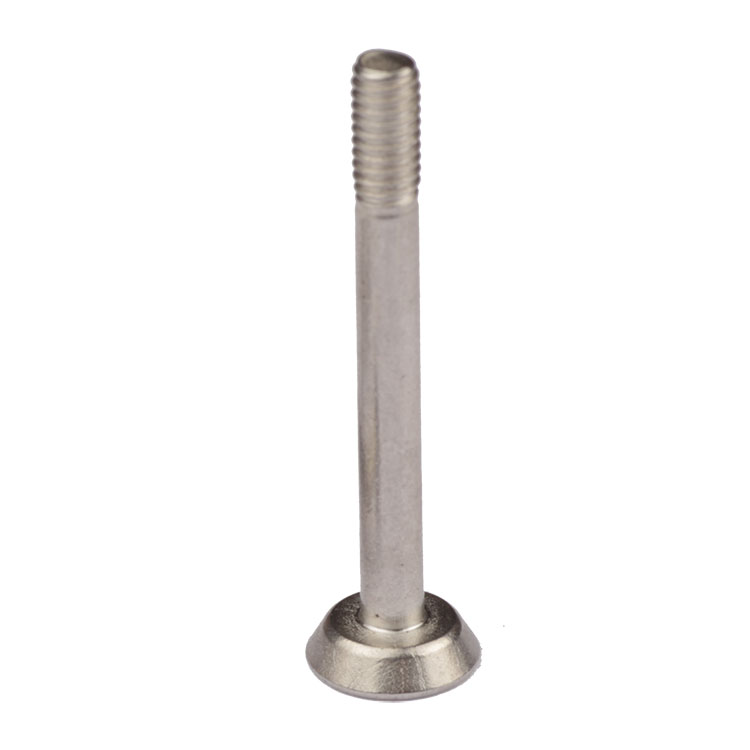
Type:Flat Undercut Screws
Materials:SUS
Surface treatment:Plain
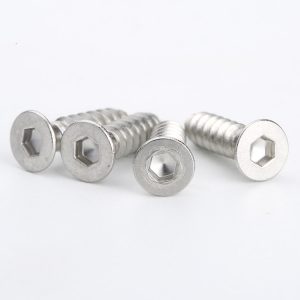
Head Type:Undercut Flat Head
Drive:Phillips
Thread:Machine Thread
Point:Blunt
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:522
We make flat undercut screws in stainless steel with a 90 degree countersunk head, a relief under the head and a cross recess, quoting them from M1 to M14. Cone angle, undercut depth, thread and grade come from your drawing, and the first article is seated in your own countersink.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Flat undercut screws are countersunk machine screws with a relief machined under the head, so the head can sit fully into a countersink instead of being held up by the fillet where the head meets the shank. The recorded item on this page is stainless steel with a plain finish, an undercut flat head and a cross recess, quoted from M1 to M14 with Number 522.
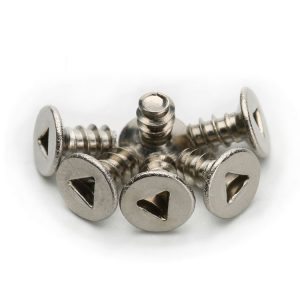
Flat head. A 90 degree countersunk cone with a flush top. It seats in a matching cone in the part, centres itself as it is tightened, and leaves the surface unbroken behind it.
Undercut. A turned relief between the bearing cone and the shank. Without it the radius left by the heading die sits right where the hole edge is, and the head stops a few hundredths short of flush; with it, the cone is the only part that touches, and it touches where the drawing says it should.
Cross recess. Four tapered wings around a pointed centre, driven with a Phillips bit. On a flush head the recess is the only access, so its depth and the bit that fits it decide how the joint is assembled and how it comes apart.
Stainless, plain. The alloy is the protection, and passivation restores the oxide film after the thread and the undercut are formed. There is no coating to chip at the flush edge, which on a countersunk head is the line the customer sees.
The head is a cone, and everything about the joint rests on the angle of that cone. On a flat undercut screw the head seats by matching surfaces: the cone on the screw presses on the cone in the part, and the load travels through the whole cone area rather than through a ring at the edge of a hole. That is why a flat undercut screw can hold a thin panel flush without a washer and without a raised head.
The undercut is what makes the seat complete. Heading leaves a radius at the junction of head and shank, and that radius has to go somewhere. Either it sits on the corner of the hole and holds the head proud — visible as a fine line of light under a flush head — or the hole has to be relieved to clear it. The undercut removes the argument: the radius is cut away, the cone seats on the countersink, and the joint is flush by construction.
The depth of the undercut is a drawing dimension, not a detail. Too shallow and the fillet still touches the hole edge; too deep and the cone loses bearing area near its inner diameter, which is where a countersunk head is thinnest. On a small screw the difference between the two is a few hundredths, which is why the undercut is checked on the section and not only on the outside.
The shank and thread follow the drawing as on any machine screw: blunt chamfered end, thread for a tapped hole or a nut. On a self-centring head the thread does not have to steer the screw, because the cone has already centred it — which is one reason these heads are used where a joint has to come apart and go back square.
Stainless is formed, threaded and passivated. Passivation matters more than usual on a countersunk head, because the cone is a large smooth surface and any free iron left on it by tooling shows as a rust bloom across the whole visible face rather than at a single spot.
The family is quoted from M1 to M14, with M1, M2, M3, M4, M5, M6, M7, M8, M9, M10 and M14 in the recorded range. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission; on a flat undercut screw the length is measured from the top face, which sits flush with the part, rather than from a bearing face above it.
| Item | How it is defined | What we control |
|---|---|---|
| Head | 90 degree countersunk cone, flush top | Cone angle, diameter and concentricity |
| Undercut | Relief between cone and shank | Depth and diameter, checked on the section |
| Recess | Phillips cross | Depth and width, driven with the production bit |
| Thread | Metric machine thread | Pitch and length, gauged per batch |
| End | Blunt, chamfered | Chamfer cut, not deburred |
| Length | From the top face to the end | Measured on the shop plate |
Cone angle and countersink angle have to be the same, and on flat undercut screws the drawing usually calls 90 degrees because that is what the tooling in the part produces. A cone that is a degree off seats on a line instead of a surface: the head looks flush, the joint feels tight, and the bearing area is a fraction of what was designed.
Length from the top face is the dimension that matters in a flush joint. Measuring from the start of the cone instead gives a screw that is short by the head depth, and in a thin panel that difference is the whole thread engagement on the far side.
Three features define a flat undercut screw: the flush head, the undercut that lets it seat, and the cross recess that drives it. The undercut is the one that is invisible when it is right and obvious when it is missing.
| Feature | What it gives | What it costs |
|---|---|---|
| Flush countersunk head | Unbroken surface, self-centring | Bears on a cone; less torque than a cap head |
| Undercut relief | Head seats fully in the countersink | Removes material near the cone root |
| Cross recess | Standard bit, cams out before damage | Depth limited by the head height |
| Stainless body | No coating to chip at the flush edge | Galls against stainless; needs care in chloride |
| Blunt end | Re-enters an existing thread cleanly | Needs a tapped hole or a nut |
The failure the undercut prevents is a small one that reads as poor workmanship. A head that stands two hundredths proud of a panel looks like a mistake, catches on a sliding part, and shows a shadow line that no amount of tightening removes. On a flush assembly that edge is the difference between a product that looks machined and one that looks assembled.
The cost is at the root of the cone. Material has to come out to make the relief, and the cone is already the thinnest part of the head at its inner end. That is why the undercut depth is specified rather than maximised, and why the first article is checked on the section: a deep undercut looks better on the bench and fails under torque.
Flat undercut screws are finished plain stainless and passivated. There is no coating thickness to upset the cone, which matters because a countersunk head seats on an angle: a few microns of plating on the cone changes where the head stops, and on a flush joint that is the visible dimension.
| Finish | How it protects | Effect on cone and recess | Typical use |
|---|---|---|---|
| Stainless, plain | Passive chromium oxide film | None; gauged as formed | General instrument and panel work |
| Stainless, passivated | Thicker passive film after acid passivation | None; film is angstroms | Cleaned or washed assemblies |
| Zinc plated steel | Sacrificial zinc | A few microns; recess and cone re-checked | Indoor, cost-driven work |
| Dacromet | Zinc-aluminium flake layer | Film builds; cone re-checked | Outdoor and wet panels |
| Black oxide | Thin conversion film, oiled | Almost no change | Unseen joints, dark assemblies |
On a flush head the finish also decides how the joint reads after service. A plated cone wears through at the seat and shows a bright ring; a stainless cone keeps its tone but can gall if it is driven into a stainless part without a lubricant. Either way the seat, not the top, is where the wear shows first.
Stainless in chloride is the honest limit. A 304 part in a coastal or chlorinated environment will pit at the cone, where moisture sits and air is excluded. Where that service is expected, the grade is the answer rather than the finish, and the drawing should say which grade rather than leaving it open.
Three assemblies where a flat undercut screw is chosen because the surface has to stay unbroken:
| Where it sits | The screw closes a panel or fixes a face plate where the head has to finish flush with the front surface and the countersink is cut into sheet or plate. |
| When it goes wrong | A head held proud by the fillet catches on a cover, shows a shadow line and lifts the plate off its gasket. |
| Why it happens | The surface is visible and stacked, and the countersink is shallow. |
| What we control | Cone angle, head diameter and undercut depth checked on the section. |
| Where it sits | The screw fixes a guide, a rail or a cover on a member that slides past another part, so nothing may stand above the surface. |
| When it goes wrong | A proud head scores the mating surface, and a head that is not square rides up and jams the slide. |
| Why it happens | The joint moves against another surface, and the head is in the wear path. |
| What we control | Head concentricity and cone angle checked, recess driven with the production bit. |
| Where it sits | The screw joins two thin members where the countersink is formed in the sheet and the joint has to be flat on both faces. |
| When it goes wrong | A fillet that lands on the hole edge splits the sheet at the countersink, and the joint loosens as the edge deforms. |
| Why it happens | The sheet is thin, the countersink is shallow, and the head has to be flush. |
| What we control | Undercut depth matched to the sheet, thread engagement checked on the far side. |
Four reasons that matter on a flat undercut screw, each tied to what the drawing has to prove:
|
Cone and undercut reviewed together
The cone angle, the head diameter, the undercut depth and the countersink in the part are reviewed as one set, so a head that would stand proud is raised before the tooling is set. Basis: Cone and undercut reviewed as one set. |
Forming, undercut and thread in one route
The head is formed, the undercut is machined and the thread is rolled in one route, so the cone stays concentric with the shank. Basis: One route from wire to finished screw. |
|
Seat checked on the section
The undercut and the cone are checked on the section of the first article and the head is checked for concentricity, because a flush joint fails on dimensions that a length gauge cannot see. Basis: Seat checked on the first-article section. |
First article fixes the setting
The first article fixes the wire heat, die set, undercut tool and thread roll; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these flat undercut screws from stainless wire: the countersunk head is formed in one stroke, the undercut is machined under the head, the thread is rolled to a blunt chamfered end, and the parts are passivated before packing. The first part of every run is cut and checked on the section for cone angle and undercut depth, driven with the production bit and entered into a thread gauge before the batch continues.


|

|
The undercut is where the process is won or lost. It is a small amount of metal removed in a place that is hard to see, and a tool that is dull will smear it rather than cut it, leaving a burr that lifts the head off the countersink by exactly the amount the undercut was meant to remove. That is why the undercut is checked with a section and a seating test rather than with a caliper.
What decides whether flat undercut screws pass is the cone, the undercut, the recess, the thread and the alloy. The inspection agreement covers those, and the criteria come from the drawing.

Cone and undercut on the projector |

Thread gauged per batch |

Hardness checked on the formed head |

Salt-spray testing of the stainless grade |
The cone of a flat undercut screw is checked on the projector for angle, diameter and concentricity, and the undercut on a section. Concentricity is the check that catches a head that would seat crooked: a cone that is off centre centres the screw off the hole, and on a flush joint the error shows as a crescent of light on one side.
Seating is checked by driving the first article into a countersunk sample and reading the gap with a light behind it. That is the customer’s acceptance test, whatever the drawing says, and it is the one that catches a burr at the undercut that a dimensional check passes.
The recess is driven with the production bit after passivation, and the thread is gauged per batch. On a countersunk head the recess is shallow relative to a pan head, so a worn bit shows here earlier than anywhere else on the part.
Every shipment of flat undercut screws is traceable to the wire it was made from and to the passivation batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the grade or the passivation. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a flat undercut screw the first article is also seated in the customer’s own countersink, so the gap is measured on the real joint rather than on a gauge. Buyers visit during the process to review samples and to see how the heads and undercuts are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers, the undercut tool and the passivation line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
The undercut on a flat undercut screw removes the fillet between head and shank so the cone seats on the countersink. Without it the head stops a few hundredths proud of a flush surface.
Deep enough to clear the fillet, shallow enough to keep bearing area near the cone root. It is a drawing dimension checked on the section, not a shop choice.
Because that is what the countersink tool in the part usually produces. The two angles have to match; a mismatch seats the head on a line instead of a surface.
Less than a cap head of the same size. A countersunk head bears on a cone, and in thin sheet the sheet distorts before the screw reaches its limit.
Yes, if the thread and the countersink are sound. A reused countersink that has been deformed will not seat the same head flush a second time.
Cone angle and head diameter, undercut depth and diameter, recess size, thread size and length, length from the top face, grade and finish.
How a flat undercut screw project runs from drawing to repeat delivery:
|
1
Send the drawing or the countersunk sample
|
→ |
2
Cone, undercut and thread review
|
→ |
3
First article seated in your part
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the cone angle and head diameter, the undercut depth and diameter, the recess size, the thread size and length, the length from the top face, the grade and the finish.
|
Cone angle
|
Head diameter
|
Undercut depth
|
|
Recess size
|
Thread and length
|
Grade and finish
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com