Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
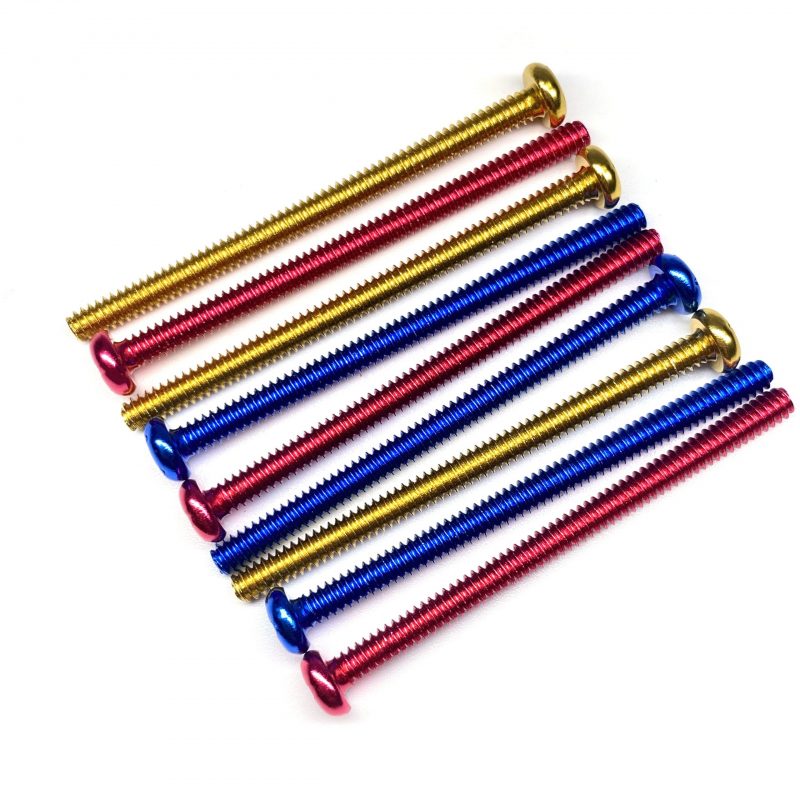
Type:Aluminium pan head screw, anodized colour
Materials:Aluminum
Surface treatment:Anodized (red, gold, blue)
Head Type:Pan head
Drive type:Phillips
Thread:Machine thread
Forming:CNC turning from bar
Number:1836
We manufacture aluminium pan head screws in anodized red, gold and blue, with a rounded pan head, a flat bearing face and a Phillips recess, from M2 to M8, turned from bar and anodized as a batch with a colour reference. Head diameter, head height, recess size, thread class and colour are made to your drawing and sample.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
An aluminum pan head screw is a machine screw with a rounded pan head and a Phillips cross recess, made in aluminium rather than steel. The pan head sits on the panel instead of sinking into it, so the bearing face and the head height matter as much as the thread, and the anodized colour is whatever the visible face of the assembly needs.
Pan head bearing face. The head has a flat underside and a domed top. The flat face spreads the clamping load over a washer-like area, which suits thin panels and plastic covers, while the dome keeps the head from catching on a hand or a moving part.
Phillips recess. The cross recess centres the driver and cams out at a set torque. On an aluminum pan head screw the recess is the part that fails first if the driver is the wrong size, because aluminium is softer than steel and the cross flanks round before the thread does.
Aluminium and anodizing. Aluminium keeps the part light and takes an anodic colour layer that is grown from the metal, dyed and sealed. Red, gold and blue parts are visible hardware: the colour has to hold through handling, and the thread and recess still have to gauge after the anodizing bath.
Together these decide how the part behaves on site: it sits on the panel with a wide bearing face, it matches the colour of the assembly, and the recess survives assembly with the correct PH driver.
On an aluminum pan head screw the head height is a design decision, not a by-product. A taller head carries more recess depth and more material over the bearing face; a lower head keeps the part out of the way but leaves less to drive against. The drawing fixes head height and recess depth as a pair.
The bearing face is flat and slightly larger than the shank, so the load spreads around the hole instead of concentrating at the head edge. On a thin panel that difference is what stops the head from pulling through or dimpling the surface when the screw is tightened.
The Phillips recess is formed with the head, so its axis stays on the shank axis. After anodizing the recess is checked with the matching PH bit, because the oxide layer adds a few microns to the flanks and a bit that fitted before the bath may feel tight after it.
Aluminum pan head screws are quoted from M2 to M8 and up to 100 mm, with length usually held to +/-0.1 mm on the drawing. Where a long version is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
| Item | How it is defined | What we control |
|---|---|---|
| Total length | From the top of the pan head to the tip | Datum stated on the drawing; length measured on the shop plate |
| Head diameter and height | The bearing face and the dome above it | Head diameter and height held to the drawing |
| Phillips recess size | The cross that takes the PH driver | Recess checked with the PH bit after anodizing |
| Thread size and length | Machine thread into the tapped part | Thread gauged after anodizing |
| Colour | Anodized colour against the accepted sample | Colour checked under agreed light per batch |
Each diameter and length combination is checked against the drawing before a quotation is issued. On a light part the head diameter and the panel hole are reviewed together, because a pan head that is too small for the hole will pull through long before the thread fails.
Length is measured from the top of the head, and the thread length is read as a position from the same datum. Head height, recess size and thread class are gauged after anodizing, in the condition the customer assembles.
For an aluminum pan head screw the drawing fixes six things: thread size and pitch, thread length, total length and its datum, head diameter and height, Phillips size, and right- or left-hand direction. A seventh line matters on aluminium: the driving torque, because an aluminium thread strips at a lower torque than a steel one of the same size. The driving torque is agreed together with the driver size, and both are written on the drawing that goes to the line.
| Parameter | Why it matters on an aluminium screw | What we control |
|---|---|---|
| Thread start position | It sets how much plain shank sits under the head | Start dimension checked on the first article |
| Thread class | Anodizing changes the thread by a few microns | Thread gauged after anodizing |
| Phillips size | A PH bit one size up rounds the cross | Recess checked with the PH bit and driver |
| Driving torque | Aluminium strips earlier than steel | Recess and thread form checked against the joint |
Anodizing grows an aluminium oxide layer out of the surface, dyes it and seals it. On an aluminum pan head screw the layer is the finish: the dome, the bearing face and the recess all take the same colour, with no paint edge to chip at the head rim.
| Finish | How it protects | Effect on thread and recess | Typical use |
|---|---|---|---|
| Anodized red | Oxide layer dyed and sealed | Thread builds a few microns; gauged after anodizing | Visible hardware on coloured assemblies |
| Anodized gold | Oxide layer dyed and sealed | Same build-up; gauged after anodizing | Warm-toned panels and trim |
| Anodized blue | Oxide layer dyed and sealed | Same build-up; gauged after anodizing | Blue anodized enclosures |
| Clear anodized | Oxide layer, no dye | Same build-up; gauged after anodizing | Parts that keep the metal look |
| Zinc plated (steel) | Sacrificial zinc layer | Thicker build-up on thread | Steel equivalents where colour is not required |
Salt-spray exposure is agreed per project and written on the drawing; anodized parts are tested in the condition they ship in. Colour is checked against the accepted sample on every batch under agreed light, because a shade shift is the defect that shows first on a visible screw.
Packing protects the anodized heads. Screws are packed in layers with the heads up so the domed surface does not rub, and the label carries the batch, alloy and colour reference.
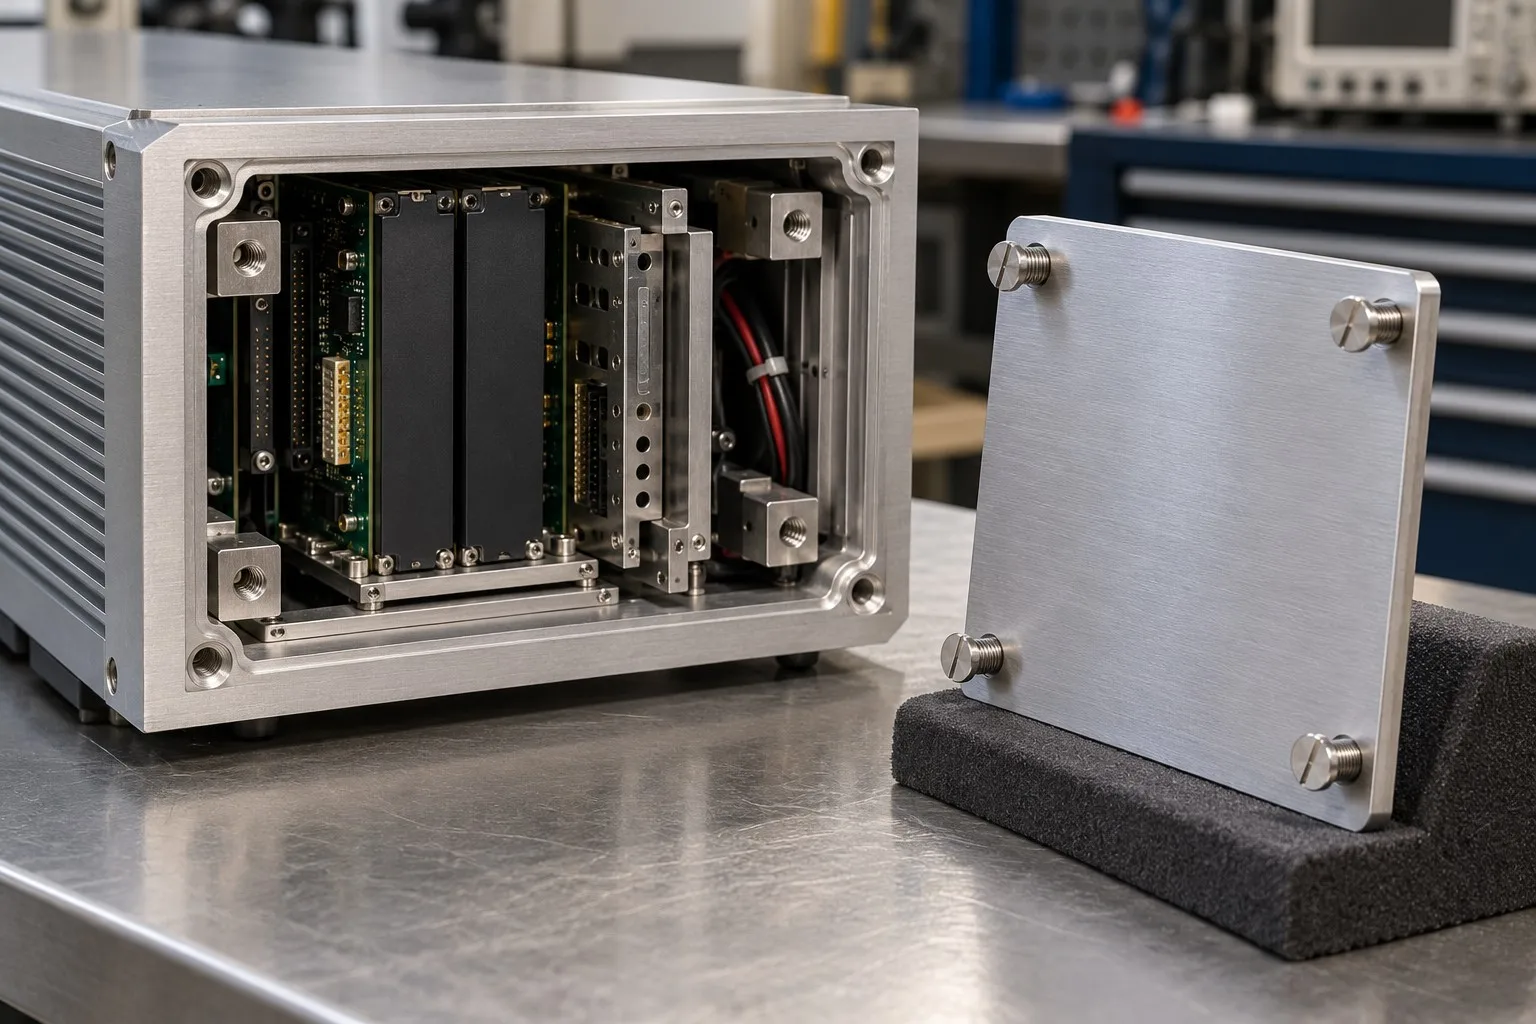
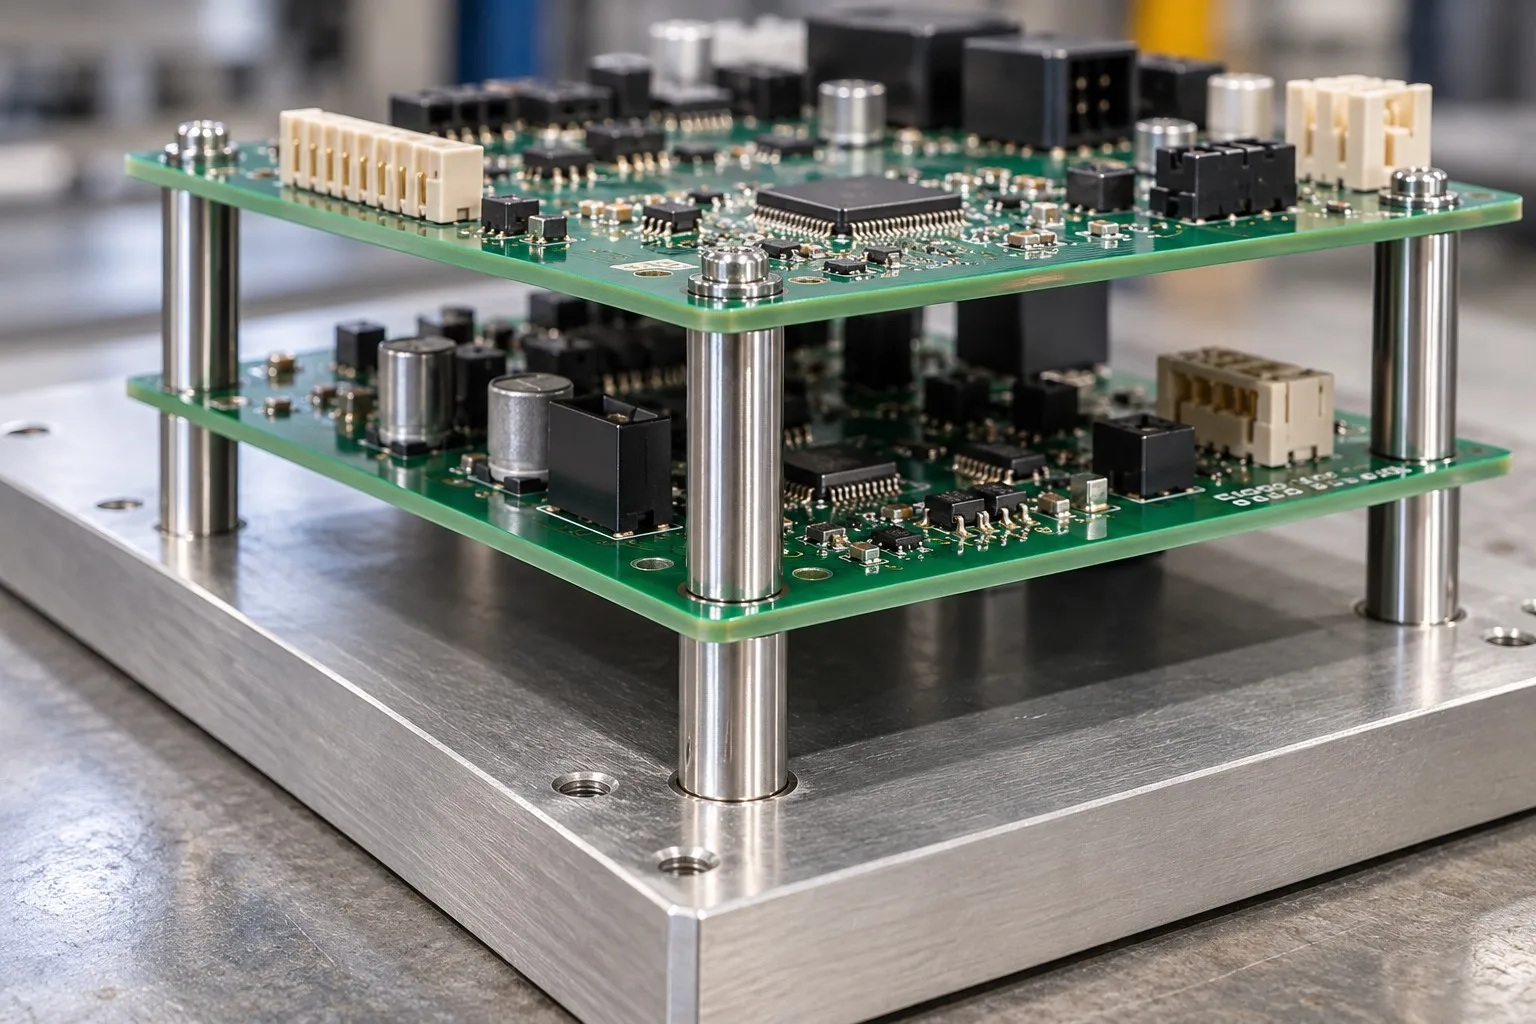
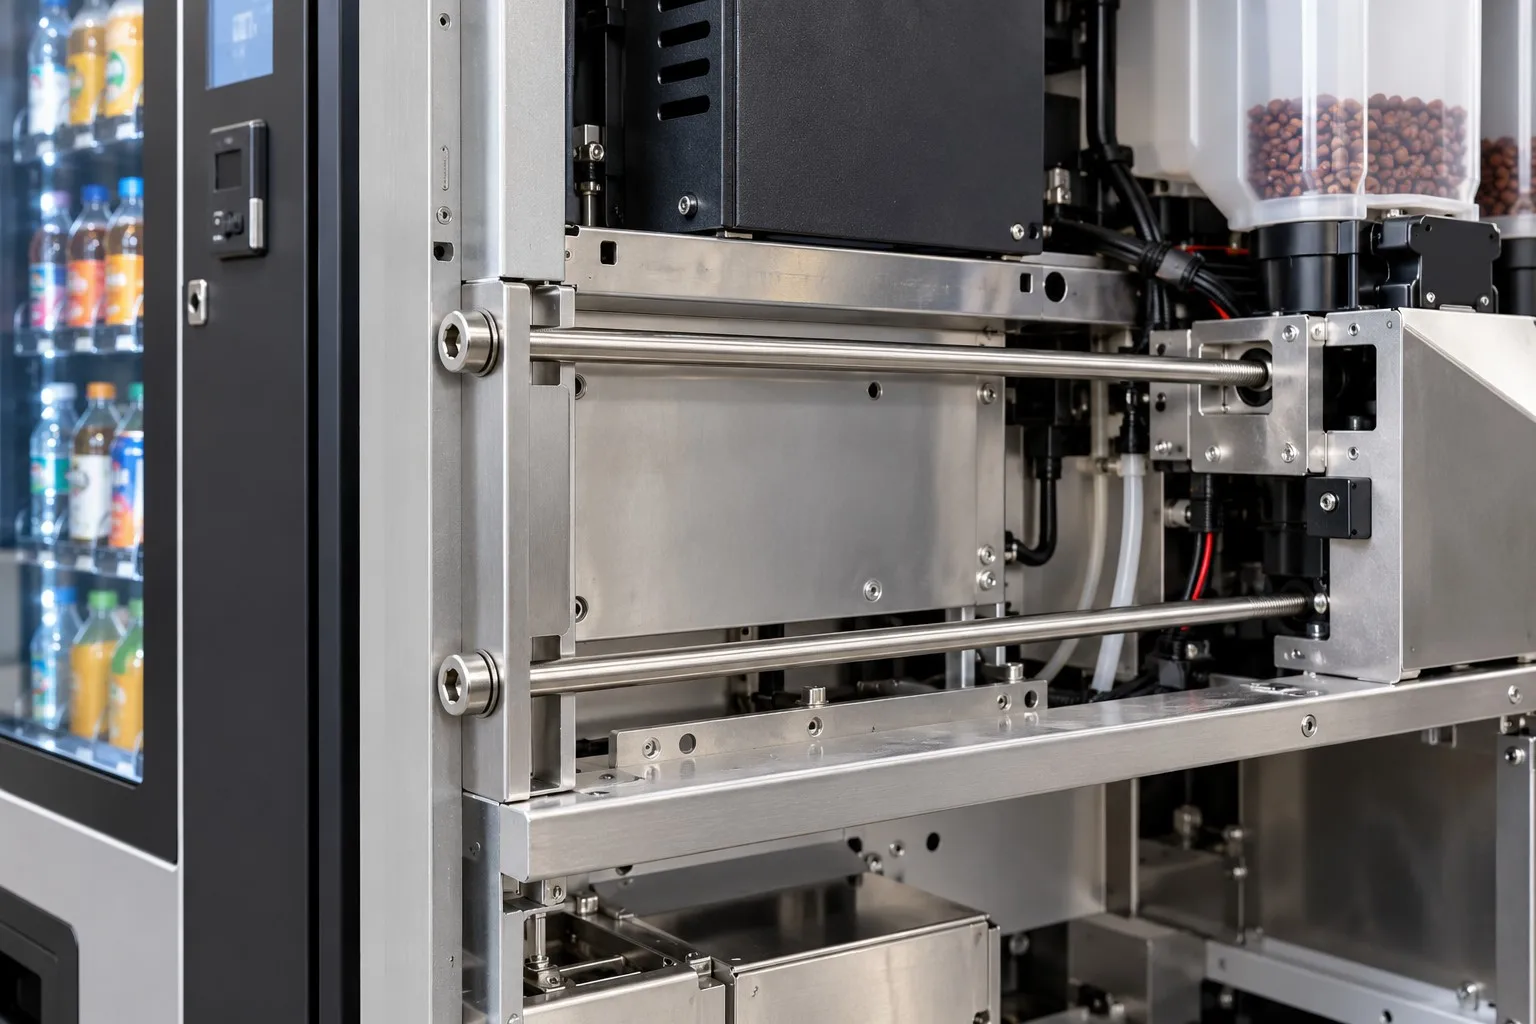
Three assembly conditions where an aluminum pan head screw sits on a panel with a wide bearing face and shows its colour, and what it has to do instead:
Audio and electronic enclosures
|
Electronics – colour-matched pan head screws |
Light PCB and bracket assemblies
|
PCB stacks – pan head screws on thin boards |
Kiosks and equipment trim
|
Kiosks – coloured pan head screws on trim |
These three conditions share one requirement: the head is seen and the joint is thin. That is why the drawing review starts from the panel hole and the colour sample rather than from the thread alone.
Four reasons that matter specifically on an aluminum pan head screw, each tied to what the drawing has to prove:
|
Engineering review before the bar is cut
Head diameter, head height, recess size and colour reference are settled before the first bar is cut, so the first sample is measured against the drawing and the colour card. Basis: Drawing and colour sample reviewed before production. |
Turned and anodized in one flow
The head and thread are produced on the turning route and the parts go to anodizing as a batch with the colour reference, so thread class and colour are read from the same run. Basis: Turning and anodizing recorded per batch. |
|
Thread and recess gauged after anodizing
The thread is gauged after anodizing and the recess checked with the PH bit, so the screw that arrives can be assembled without re-cutting the thread. Basis: Thread and recess gauged in the anodized condition. |
First article to repeat production
The first article fixes the drawing revision, alloy, turning set-up and colour reference; repeat orders are compared against that record. Basis: First article and colour sample signed off before the batch. |
These aluminum pan head screws are turned from aluminium bar. The bar is cut to length, the pan head and bearing face are turned, the thread is produced, and the parts go to anodizing as a batch with the colour reference. The operator checks the first parts of each run against the drawing before the batch continues.
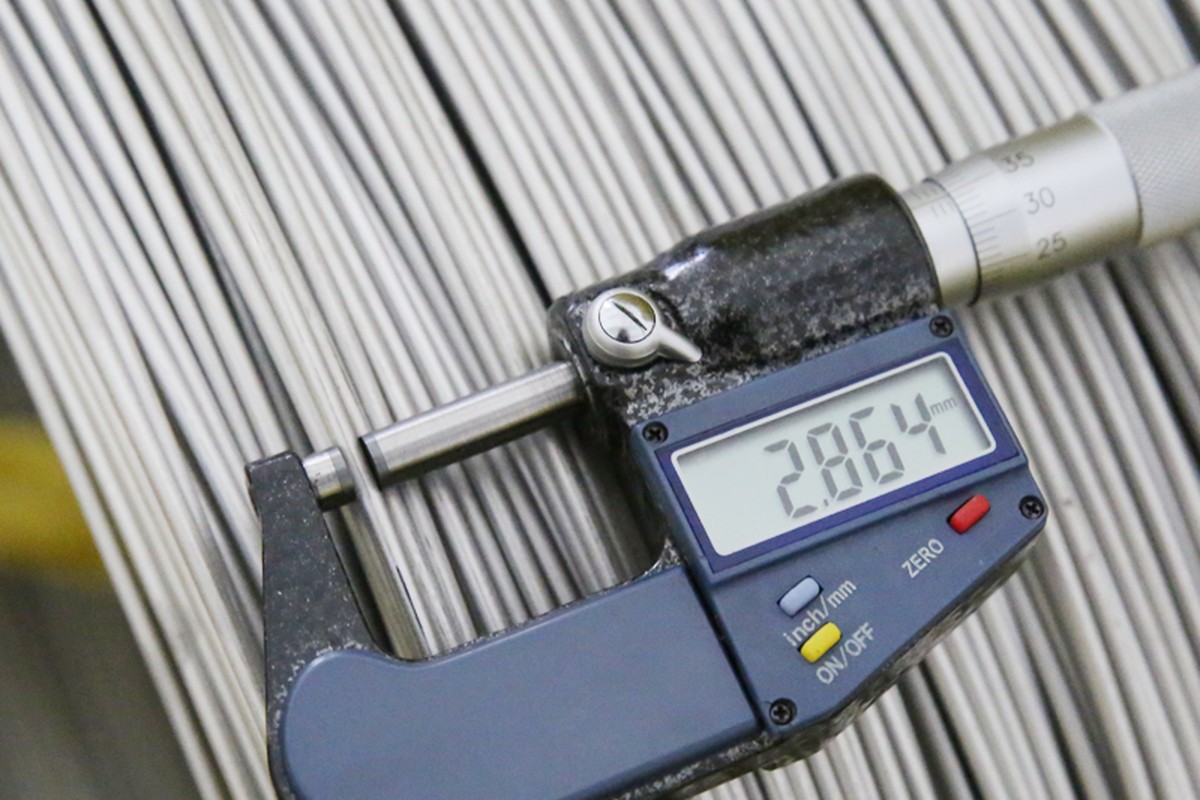
Material checked before the bar is cut |
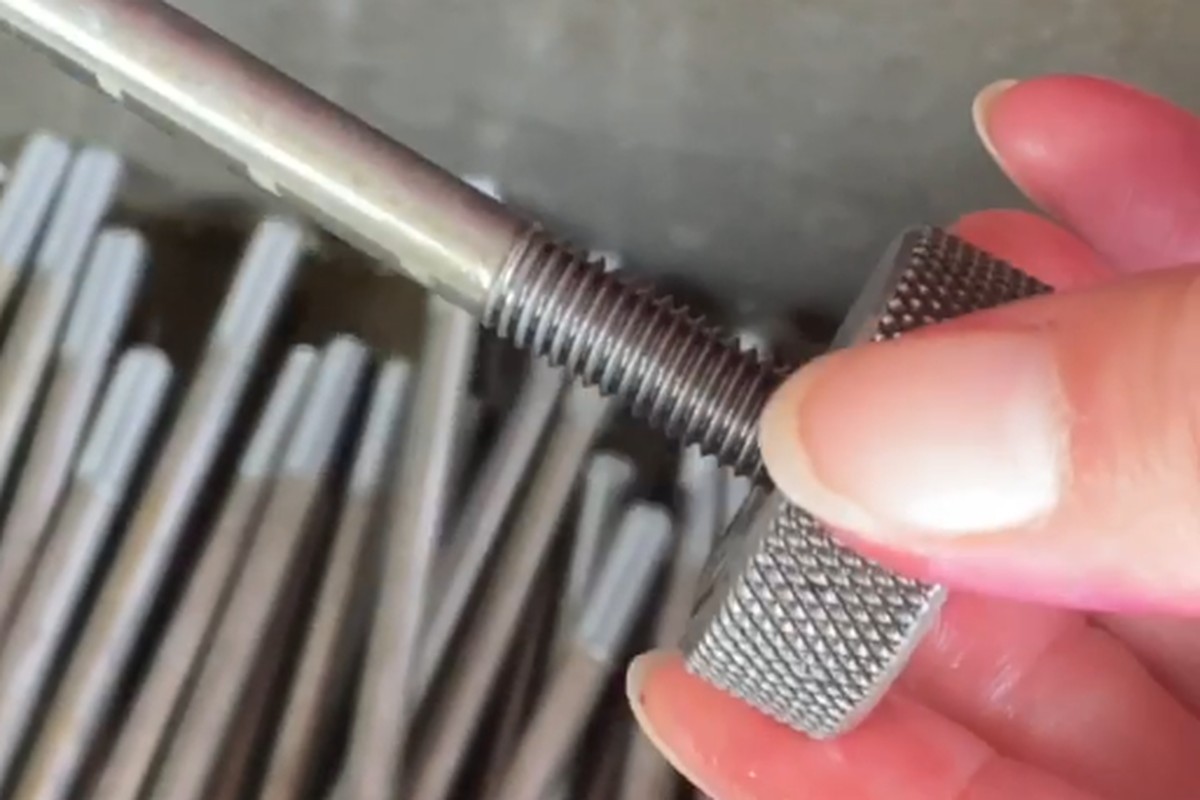
Threads gauged after anodizing |
Between runs the lathe is set to the drawing head height and thread size; the first part goes to the gauges before the run continues, and the setting is recorded. Anodized parts are checked again after the bath, so the record covers both the machined and the coloured condition.
What decides whether an aluminum pan head screw passes is not its colour alone: it is the head diameter against the panel hole, the recess taking the PH driver, the thread matching the tapped part after anodizing, and the colour matching the accepted sample. The inspection agreement covers all four.

Thread gauging after anodizing |

Head diameter and recess profile on the projector |

Hardness testing of the aluminium alloy |

Salt-spray testing of the anodized finish |
Each batch is recorded against the drawing revision: head diameter from the first article, the recess checked with the PH bit, the thread gauged after anodizing, and the colour checked against the sample under agreed light. If a gauge or the colour check fails, the parts back to the last good setting are held and re-checked.
Where a third-party report is required for the alloy or the anodized finish, it is listed on the drawing so the paperwork ships with the parts, and the batch number on the label matches the record used for the gauge.
Every aluminum pan head screw shipment is traceable to the aluminium bar it was made from. The alloy, heat or lot number and standard are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the alloy or the finish. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. Colour-critical parts are approved on a physical sample rather than a file, and buyers visit to see the turning and anodizing steps their parts will go through.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the turning cells and the anodizing line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
It is a machine screw with a rounded pan head, a flat bearing face and a Phillips cross recess, made in aluminium. The head sits on the panel rather than sinking into it, and the anodized colour becomes part of the visible finish.
A pan head sits proud and spreads load on a wide bearing face, which suits thin panels. A countersunk head sinks flush and needs a matching angle in the panel. The choice is driven by the panel and the visible line, not by the thread.
Yes. The anodic layer adds a few microns to the thread and the recess, so the thread class is read after anodizing and the recess is checked with the PH bit in the same condition.
Aluminum pan head screws are quoted from M2 to M8 and up to 100 mm, usually held to +/-0.1 mm. Where a long version is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
The colour is matched against an accepted sample under agreed light. Anodized batches shift with alloy, bath and dye lot, so the sample and the acceptance range are fixed before production.
Thread size and pitch, thread length, total length and datum, head diameter and height, Phillips size, alloy, anodized colour and finish, and quantity.
How an aluminum pan head screw project runs from drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
DFM review and quotation
|
→ |
3
First article approval
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For an aluminum pan head screw quotation, send the drawing with thread size and pitch, thread length, total length and datum, head diameter and height, Phillips size, alloy, anodized colour and finish. Head, recess and colour are confirmed with you before production.
|
Thread size and pitch
|
Thread length
|
Total length and datum
|
|
Head diameter and height
|
Phillips size
|
Alloy, colour and quantity
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com