Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
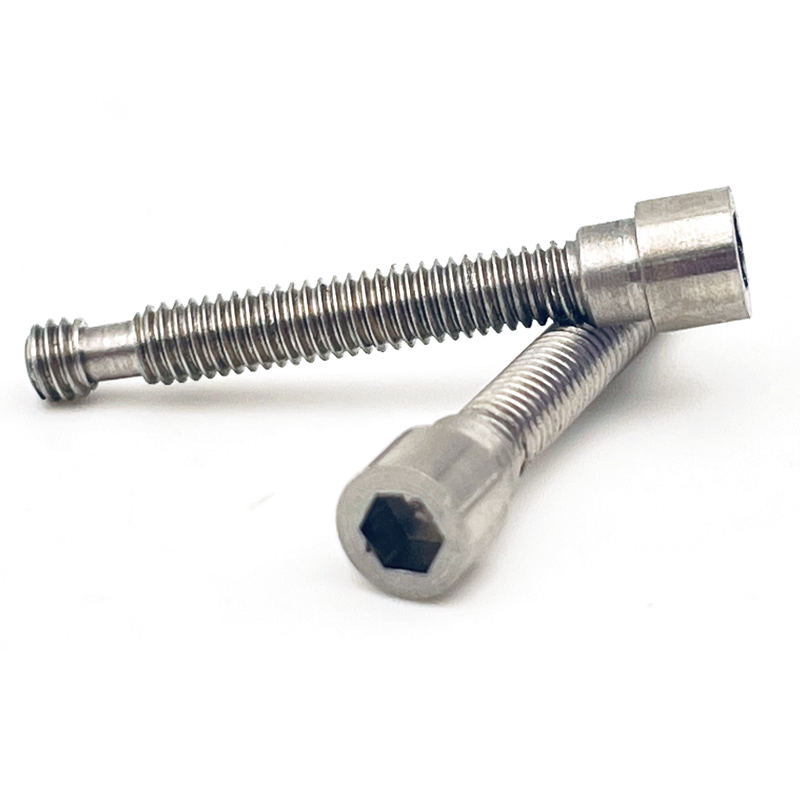
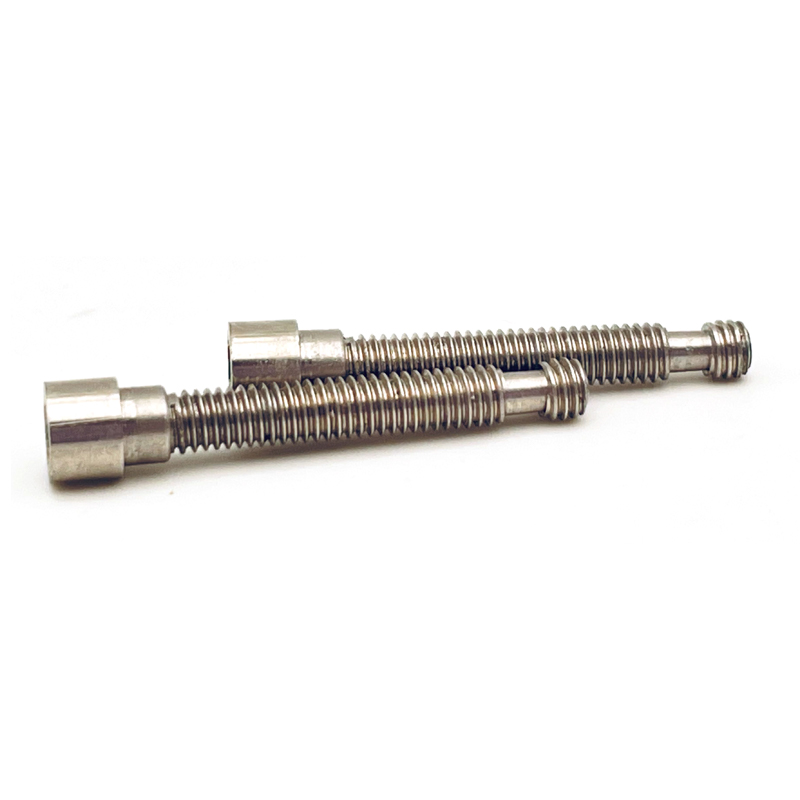
Type:Stainless steel socket head cap shoulder screws
Materials:Stainless steel
Surface treatment:Plain
Head Type:Cap head
Drive type:Hex socket (Allen)
Thread:Machine thread
Forming:Multi-station cold heading with shoulder
Number:1742
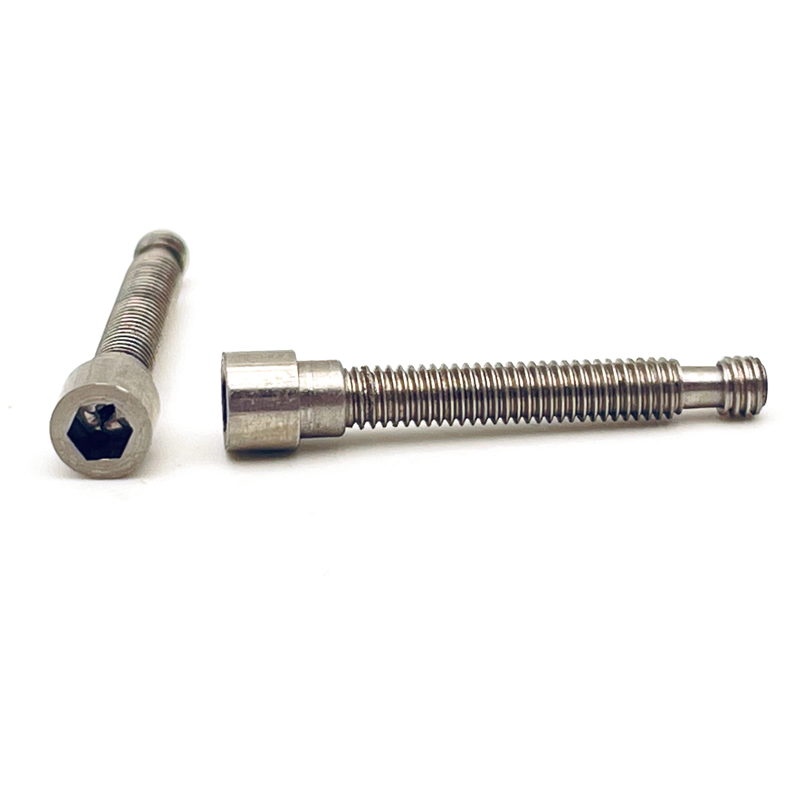
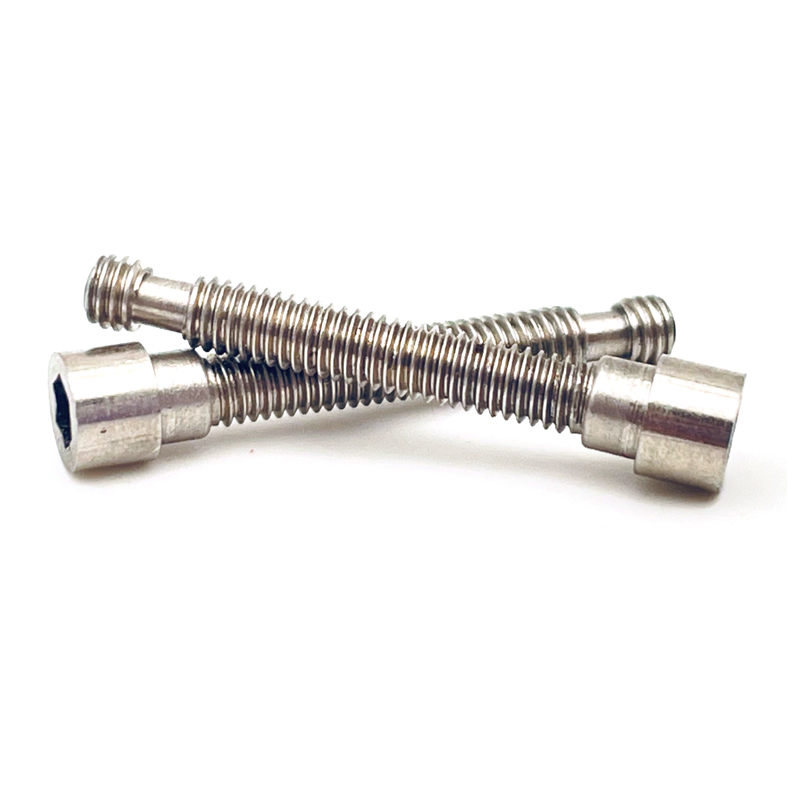
We manufacture stainless socket hex screws with a cap head, a hex socket and a precision shoulder above a smaller machine thread, plain and passivated, made to drawing. Shoulder diameter and length, step radius, thread class and finish are settled before the batch runs.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A socket hex screw is a cap head screw driven with an Allen key. The one on this page is a shoulder type: below the head sits an unthreaded shoulder that acts as a pivot or a guide, and the machine thread that holds the joint is smaller than that shoulder.
Cap head and hex socket. The head is a cylinder with a hexagon socket, so the screw takes a high clamp load from a small head and the key is the only tool needed. On a shoulder screw the head also sets the axial position: it stops the shoulder at the face it bears on.
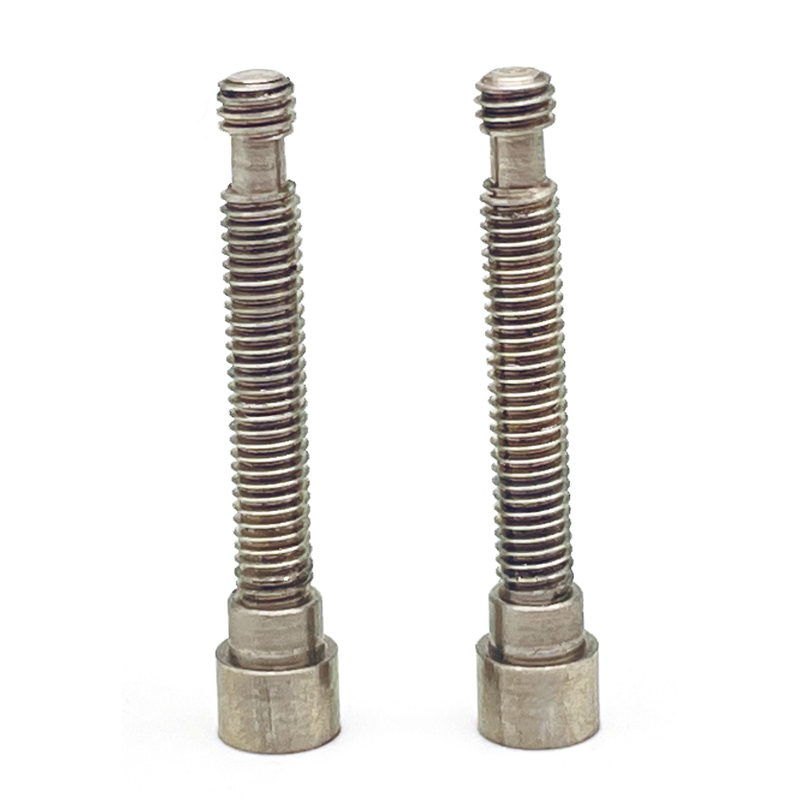
The shoulder. The shoulder is the working surface, not a spacer. Its diameter sets the fit in the pivot hole, and its length sets the stack height between the head and the thread. Both are held to the drawing, because a shoulder that is a few hundredths off changes the clearance in a linkage.
Thread below the shoulder. The thread is smaller than the shoulder and runs below it into the tapped part. That step is what stops the shoulder from being pulled into the hole and what keeps the pivot surface at the right height.
Together these decide the joint: the head clamps, the shoulder locates, and the thread holds the assembly without the shoulder ever carrying thread.
This socket hex screw is formed from stainless wire on a multi-station header, thread rolled and supplied plain and passivated. The grade comes from the drawing, with 303, 304 and 316 the common choices, and the wire heat number stays traceable to the material certificate.
The cap head and the hex socket are formed in the die, and the shoulder is produced behind the head. The shoulder diameter and length are the features that make the part a shoulder screw rather than a cap screw, and they are checked on the projector against the drawing.
The thread is rolled below the shoulder. The transition between the shoulder and the thread is where the load changes from a pivot to a clamp, and a sharp step there concentrates stress; the drawing sets the radius or undercut, and the first article is checked on that transition.
Plain stainless keeps every dimension the process produced. Passivation restores the chromium film without adding thickness, so the shoulder diameter that was measured is the diameter that fits the pivot hole.
Socket hex screws of this type are quoted from M4 to M10 shoulder sizes and in lengths to suit the drawing, with the head, the shoulder and the thread measured on the projector and with gauges. Where a long version is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
| Item | How it is defined | What we control |
|---|---|---|
| Head diameter and height | The cap head that clamps the joint | Checked on the projector on the first article |
| Hex socket | Key size and depth | Checked with the key and on the projector |
| Shoulder diameter | The fit in the pivot hole | Measured with micrometers on the first article |
| Shoulder length | The stack height under the head | Measured from the head face |
| Thread size and length | Machine thread below the shoulder | Gauged per batch |
| Step radius | The transition from shoulder to thread | Checked on the projector |
Each size is quoted against the joint it locates. The shoulder diameter and the pivot hole are a pair, and the shoulder length and the plate stack are another, so both are reviewed with the drawing rather than picked from a table.
Shoulder length is measured from the head face, and the total length from the top of the head. The batch is checked on the features the process can drift on: shoulder diameter, shoulder length and thread class.
The shoulder is the part of a socket hex screw that does the locating. It runs unthreaded through the pivot hole, and the clearance between the shoulder and the hole is what decides whether a linkage moves freely or binds. That clearance is set by the hole on the drawing and by the shoulder tolerance on the screw.
Shoulder length sets the stack. It has to equal the total thickness of the parts it passes through, plus the clearance the joint needs, and no more. A shoulder that is too long clamps the parts before the head seats; one that is too short lets the parts move under the head.
The thread below the shoulder is deliberately smaller. It passes through the pivot hole without touching the sides and engages the tapped part behind it, so the clamp load is carried by the thread and the pivot is carried by the shoulder. The step between them is what takes the difference in diameter.
Where the joint is a pivot, the shoulder is also a wear surface. Stainless on stainless can gall in a dry pivot, so the drawing states the fit and the first article is assembled and cycled before the batch is released.
This socket hex screw is supplied plain and passivated. There is no coating to build on the shoulder, the socket or the thread, so the pivot fit and the key fit stay as they were measured, and a coated shoulder cannot change the clearance in service.
| Finish | How it protects | Effect on shoulder and thread | Typical use |
|---|---|---|---|
| Plain, passivated stainless | Alloy resists corrosion; passive film restored | No build-up; pivot fit unchanged | Pivots, fixtures and wash-down areas |
| Electropolished | Surface levelled, chromium enriched | Shoulder smoothed; fit re-checked | Hygienic and visible assemblies |
| Black oxide (carbon steel) | Conversion coating, minimal thickness | No measurable build-up | Indoor carbon steel equivalents |
| Zinc plated (carbon steel) | Sacrificial zinc layer | Build-up on thread; gauged after | Carbon steel parts where cost matters |
| Dacromet flake (steel) | Zinc-aluminium flake layer | Thin film; thread checked over coating | Outdoor carbon steel parts |
Salt-spray exposure is agreed per project and written on the drawing; plain stainless is tested in the condition it ships in. On a shoulder screw the shoulder is the face that matters: a coating that builds there changes the pivot clearance even when the thread is correct.
Packing protects the shoulder and the socket. Screws are packed so the shoulders do not knock, and the label carries the batch, the material heat and the finish reference.
Three assemblies where socket hex screws with a shoulder are chosen to locate as well as clamp, and what the screw has to do instead:
| Where it sits | The shoulder runs through a lever or a link and acts as the pivot pin, while the thread holds the joint together. |
| When it goes wrong | A shoulder that is a few hundredths off makes the linkage bind or rattle, and a short shoulder lets the parts move under the head. |
| Why it happens | The joint moves, the hole is reamed, and the screw is assembled once and left. |
| What we control | Shoulder diameter and length checked, the pivot assembled and cycled on the first article, and the thread gauged. |
| Where it sits | The shoulder locates a plate or a stop against a hardened surface, and the thread pulls it down. |
| When it goes wrong | A shoulder that is too long holds the plate off the datum, and a thread that is out of class leaves the stop loose. |
| Why it happens | The fixture is set to a datum, the parts are hardened, and the joint is adjusted during set-up. |
| What we control | Shoulder length measured from the head face, diameter checked, and the thread gauged per batch. |
| Where it sits | The shoulder guides a jaw or a plate in a slot, and the thread fastens it to the frame. |
| When it goes wrong | A shoulder that is not round binds in the slot, and a step that is sharp cracks under repeated cycling. |
| Why it happens | The frame runs continuously, the joint cycles, and the parts are stainless. |
| What we control | Shoulder diameter and roundness checked, step radius reviewed, and the first article cycled. |
Four reasons that matter on a socket hex screw with a shoulder, each tied to what the drawing has to prove:
|
Shoulder and hole reviewed together
The shoulder diameter, the shoulder length and the pivot hole are reviewed before the die is cut, so a screw that would bind or hold a plate off its datum is raised first. Basis: Shoulder, hole and stack reviewed before tooling. |
Headed, threaded and shouldered in one route
The head and socket are formed, the shoulder is produced behind the head and the thread is rolled below it, so the shoulder stays on the screw axis. Basis: One route for head, shoulder and thread. |
|
Shoulder measured on the part
The shoulder diameter is measured with micrometers and the length from the head face, and the thread is gauged, on the first article and per batch. Basis: Shoulder diameter and length checked on the first article. |
First article to repeat production
The first article fixes the drawing revision, wire heat, die set and finish batch; repeat orders are compared against that record. Basis: First article signed off before the batch is released. |
Shi Shi Tong forms these socket hex screws on a multi-station header: the cap head and the hex socket are struck in the die, the shoulder is produced behind the head, the thread is rolled below it, and the parts are passivated. The first part of every run is measured on the shoulder and the head, checked with the key and gauged on the thread before the batch continues.


|

|
Between runs the die insert is changed to the drawing head and the socket punch to the key size, and the shoulder tool is set with the thread length; the first part goes to the projector and the gauges before the run continues. The setting is recorded, and the first article is assembled with the pivot hole before the batch is released.
What decides whether a socket hex screw passes is not only the thread: it is the head, the hex socket, the shoulder diameter and length, and the step between the shoulder and the thread. The inspection agreement covers those, and the criteria come from the drawing and the pivot hole.

Thread gauging against GO/NO-GO gauges |

Head, shoulder and step on the projector |

Hardness testing where the drawing requires it |

Salt-spray testing of the passivated part |
Each batch is recorded against the drawing revision: shoulder and head from the first article, the key fit checked, and the thread gauged per batch. If a gauge or the shoulder check fails, the parts back to the last good setting are held and re-checked.
Where the drawing asks for a third-party report, it is ordered alongside the batch and filed with the inspection record under one batch number.
Every socket hex screw shipment is traceable to the wire it was made from. The grade, heat number and standard are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the material or the finish. The documents carry the drawing revision and the batch number, so the paperwork can be matched to the parts.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. Shoulder screws are approved with the pivot hole, so the shoulder diameter and the stack are signed off as a pair. Buyers visit during the process to review samples and to see how the heads and shoulders are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the header and the passivation line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
It is a cap head screw driven with an Allen key. The one on this page is a shoulder type, with an unthreaded shoulder below the head that locates the joint and a smaller machine thread that holds it.
The shoulder runs unthreaded through the pivot or guide hole and sets the clearance and the stack height. The thread below it is smaller, so the shoulder is never pulled into the hole and never carries thread.
By the hole it runs in. The shoulder diameter and the pivot hole are reviewed together, and the first article is measured with micrometers and assembled with the mating part before the batch is released.
Socket hex screws of this type are quoted from M4 to M10 shoulder sizes and in lengths to suit the drawing. Where a long version is required, custom lengths up to 2,000 mm are subject to DFM review after drawing submission.
Stainless on stainless can gall in a dry pivot. The fit is agreed on the drawing, the first article is assembled and cycled, and any lubrication used at assembly is stated.
Head diameter and height, hex socket size and depth, shoulder diameter and length, the step radius, thread size and length, total length and datum, material and finish.
How a socket hex screw project runs from drawing to repeat delivery:
|
1
Send the drawing or sample
|
→ |
2
Shoulder and hole review
|
→ |
3
First article approval
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a socket hex screw quotation, send the drawing with the head diameter and height, hex socket size and depth, shoulder diameter and length, the step radius, thread size and length, total length and datum, material and finish.
|
Head diameter and height
|
Socket size and depth
|
Shoulder diameter and length
|
|
Step radius
|
Thread size and length
|
Material and finish
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com