Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
Type:Mini Screw, Ultra Stainless Screws
Materials:304 Stainless Steel
Surface treatment:Plain
Head Type:Low Profile
Drive:Phillips (cross)
Thread:Machine thread
Point:Blunt
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
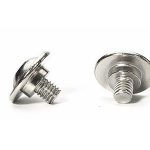
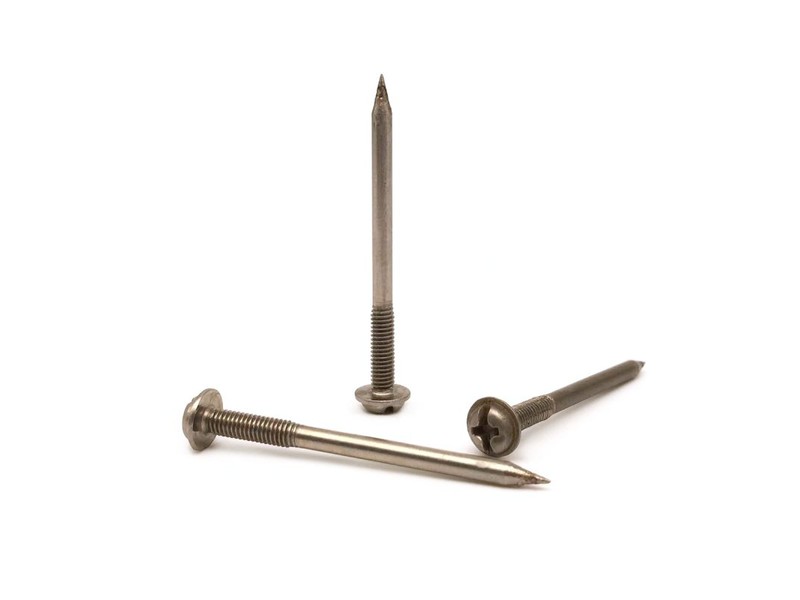
We make ultra low profile mini screws in 304 stainless, a thin pan head with a Phillips recess and a fine machine thread, quoted from M1 to M10. Head height, recess depth, thread and torque come from your drawing, and the first article is fitted into your pocket.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Ultra low profile mini screws are miniature machine screws with a head thin enough to sit almost level with the surface, a Phillips recess and a 304 stainless body, quoted here from M1 to M10 with the smallest sizes carrying most of the work. The head height is the defining number: on these parts it is a fraction of a standard pan head, which is what makes them fit where nothing else does.
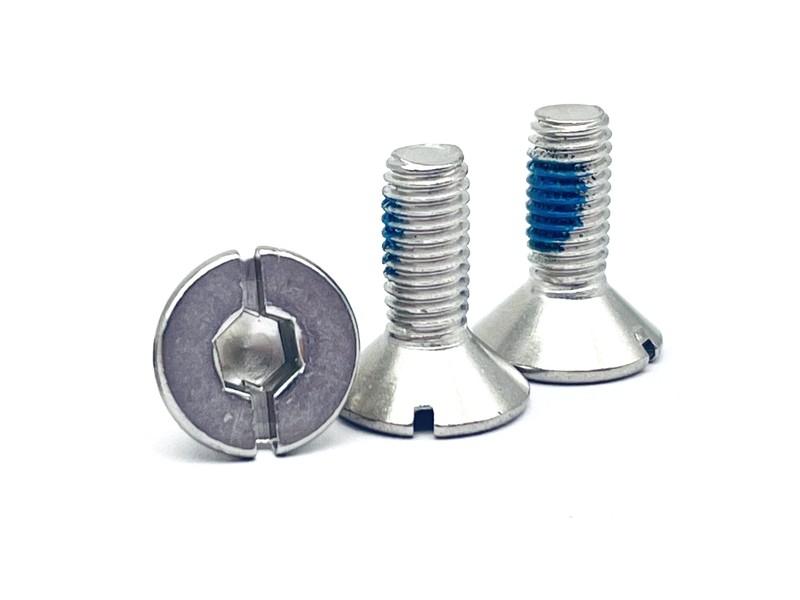
Thin head. A pan-shaped head pressed down to a low height, with a small flat bearing face underneath and a low dome on top.
Phillips recess. A cross recess cut into the thin head, driven with a PH000, PH00 or PH0 bit depending on size.
Machine thread. A rolled metric thread for a tapped hole or a nut, with a fine pitch at the small sizes.
304 stainless, plain. Passivated and uncoated, so the thin head and the recess are as formed and the alloy is the protection.
These are parts for assemblies that have no depth to spare: a hinge pocket, a sliding cover, a gearbox lid that has to sit inside a housing. Where a standard head would stand proud, a thin head disappears, and the joint keeps the same thread and the same load.
A thin head spends its height on the thread and the recess, not on the drive walls. On a standard pan head at M2 there is room for a recess deep enough to take the full bit tip; on an ultra low profile head of the same thread the recess is shallower, so the bit engages fewer tenths of a millimetre and the load per unit area goes up.
That is the trade the part is built on. The recess has to be shallow, and a shallow Phillips recess is where cam-out starts: the cross recess drives on inclined flanks, and the shallower the engagement the sooner the bit climbs out under torque. A PH000 bit in a shallow cross will slip before it strips, which marks the head and damages the driver tip.
The bearing face is the second consequence. A thin head has a small annulus under it, so the clamp load spreads over less area and the head can dish on a soft or uneven surface. On a metal pocket machined flat the face is fine; on plastic it needs a washer or a wider head, and the thin head is the wrong part for that joint.
The head is also the handling feature. At M1.2 the head is a couple of millimetres across and a fraction of a millimetre thick, so it deforms under a careless pick, and a burr at the recess edge is enough to stop the bit seating. Deburring is not cosmetic on these parts; it is what makes them usable.
What the form buys is depth. In a pocket that is 3 mm deep with a cover that has to sit flush, the difference between a 0.7 mm head and a 0.4 mm head is the difference between a cover that closes and one that does not. That is why the head height, not the thread, is the number that gets specified first.
The recorded range is M1 to M10, in the ten recorded sizes M1, M2, M3, M4, M5, M6, M7, M8, M9 and M10, with the M1 to M3 end being where the thin head matters most. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For ultra low profile mini screws the quotation carries head diameter, head height, recess size and depth with the thread, because those three head numbers are the part.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Pan form, low height | Head diameter and head height |
| Recess | Phillips cross | Recess size (PH000 to PH0) and depth |
| Bearing face | Small flat annulus | Flatness and edge condition |
| Thread | Machine thread, fine at small sizes | Pitch and length, gauged per batch |
| End | Blunt, chamfered | Chamfer cut, not deburred |
| Material | 304 stainless | Grade and heat number on the certificate |
| Finish | Passivated | Surface condition and film |
Head height should be quoted as a tolerance, not a nominal. On a part whose whole purpose is to fit a pocket, a head a few hundredths high is a cover that will not seat, and it is the first number a buyer checks on the sample.
Recess depth follows the head height. Where the design allows, a slightly deeper recess takes more torque; where the head is already at its minimum, the recess is shallow by necessity and the torque has to be set accordingly.
Three features define the part: the low head, the cross recess cut into it and the 304 body. The first two compete for the same fraction of a millimetre, and the third removes any coating from the recess, which at this depth would be the difference between a bit that seats and one that rocks.
| Feature | What it gives | What it costs |
|---|---|---|
| Low head | Sits flush in a shallow pocket | Little height for the recess |
| Shallow cross recess | Fits the thin head | Bit engagement short; cam-out starts sooner |
| Small bearing face | Low profile | Dishes on soft or uneven seats |
| 304 stainless | Corrosion resistance, no plating | Work-hardens; galls dry |
| Passivated finish | Recess as formed | Not a lubricant |
The flush fit is the reason the part exists. A cover, a hinge leaf or a bezel that has been designed to sit level needs a head that does not interrupt the surface, and a low profile head is the only screw form that does that without a counterbore.
The shallow recess is the tax on that fit, and it is paid at the assembly station. Drivers wear faster in a shallow cross, bits have to be changed before they round, and the torque figure in the work instruction has to be one the recess will take cold.
The recorded finish is passivation with no coating on 304 stainless. At a head thickness measured in tenths of a millimetre that is the right choice: a plating build would be a measurable share of the recess depth, and on a thin head the deposit also has to be controlled at the edge of the bearing face, where a rough plating bead would stop the head seating flat.
| Option | How it protects | Effect on the thin head | Typical use |
|---|---|---|---|
| 304 stainless, passivated | Passive chromium oxide film | None; head and recess as formed | Electronics and eyewear |
| 316 stainless, passivated | Passive film with molybdenum | None; head and recess as formed | Medical and marine |
| Brass, plain | No protection needed indoors | Softer head; recess wears sooner | Electrical and decorative |
| Carbon steel, nickel plated | Barrier deposit, bright | Build at recess and head edge | Visible consumer parts |
| Carbon steel, black oxide | Conversion film, oiled | No measurable build | Internal mechanisms |
The 304 and 316 choice follows the cleaning regime. 304 covers ordinary handling and indoor moisture; 316 is the grade where chlorides are present, which on a mini screw usually means a medical instrument or a marine sensor rather than a coastal structure.
Where the head is driven often, the recess wears before the thread. Passivated stainless wears more evenly than a plated head, because there is no soft deposit to rub through and leave a step at the lobes of the cross.
Three assemblies where ultra low profile mini screws are the fixing:
| Where it sits | The screw closes a hinge leaf or a temple joint where the head must not stand proud and the space around it is measured in tenths of a millimetre. |
| When it goes wrong | A standard head rubs against the mating part, and a shallow recess rounds when the hinge is adjusted. |
| Why it happens | The joint is a pocket, the head is flush, and the part is serviced. |
| What we control | Head height tolerance checked on the sample; recess driven with the specified bit. |
| Where it sits | The screw closes a housing or retains a bezel where the cover has to sit level and the fasteners are too small for a socket head. |
| When it goes wrong | The bit cams out of the shallow cross and marks the housing, or the thin head dishes on a plastic seat. |
| Why it happens | The joint is small, visible, and assembled in volume. |
| What we control | Recess depth and bit size agreed; first article driven at the production torque. |
| Where it sits | The screw retains a lid or a bearing plate inside a housing where a tall head would foul the gear train. |
| When it goes wrong | A proud head touches a rotating part, and a burr at the recess stops the bit seating during service. |
| Why it happens | The joint is inside a mechanism, it is oiled, and clearance is tight. |
| What we control | Head height and burr condition checked; stainless grade confirmed. |
Four reasons that matter on a thin-headed mini screw, each tied to what the drawing has to prove:
|
Head height and recess agreed
The head height tolerance and the recess depth are settled together, because a thin head leaves the recess nowhere to go. Basis: Head height and recess agreed. |
Headed, deburred, passivated in one route
The low head and cross recess are formed in one stroke, the thread is rolled and the parts are deburred and passivated in the same route. Basis: One route from wire to passivated screw. |
|
First article checked in the pocket
The first article is checked for head height against the pocket it fits, because the number that matters is clearance, not a nominal. Basis: First article checked in the pocket. |
Setting fixed by the first article
The first article fixes the punch height and the recess depth; repeat orders are measured against that record. Basis: First article signed off before the batch. |
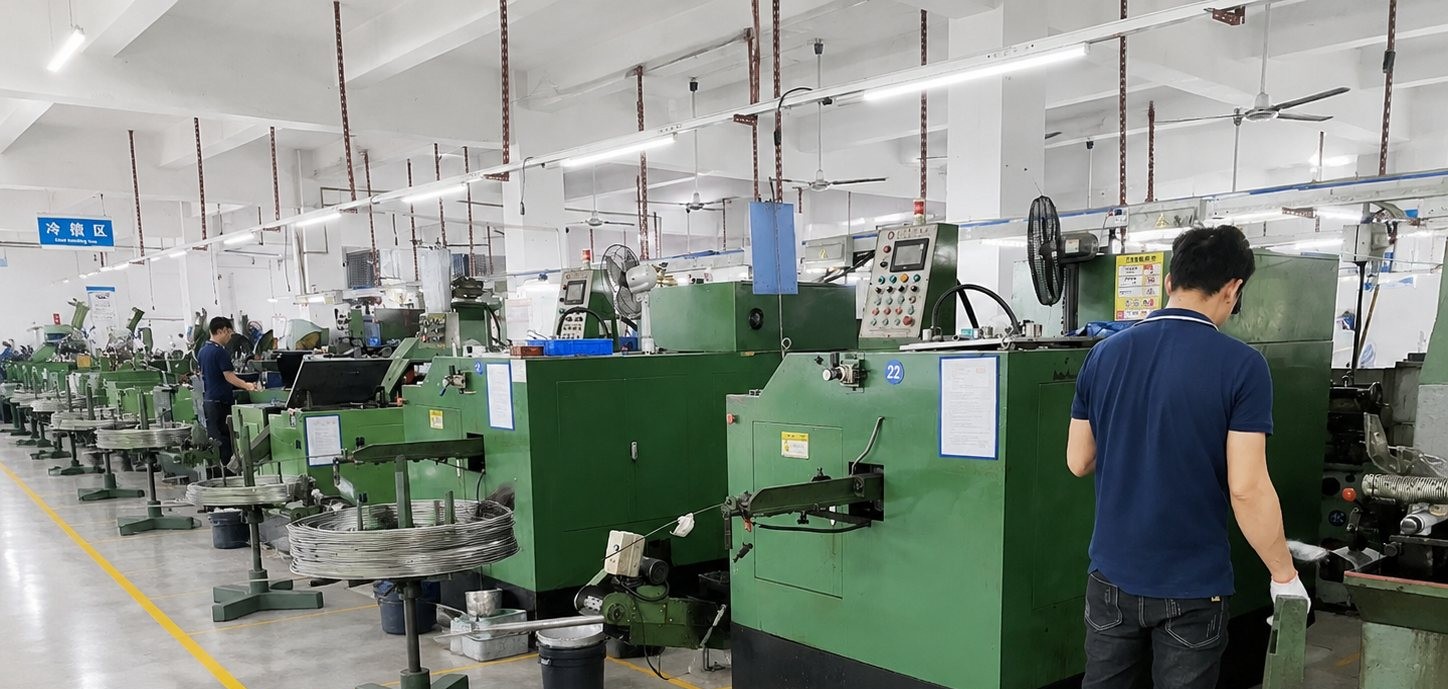
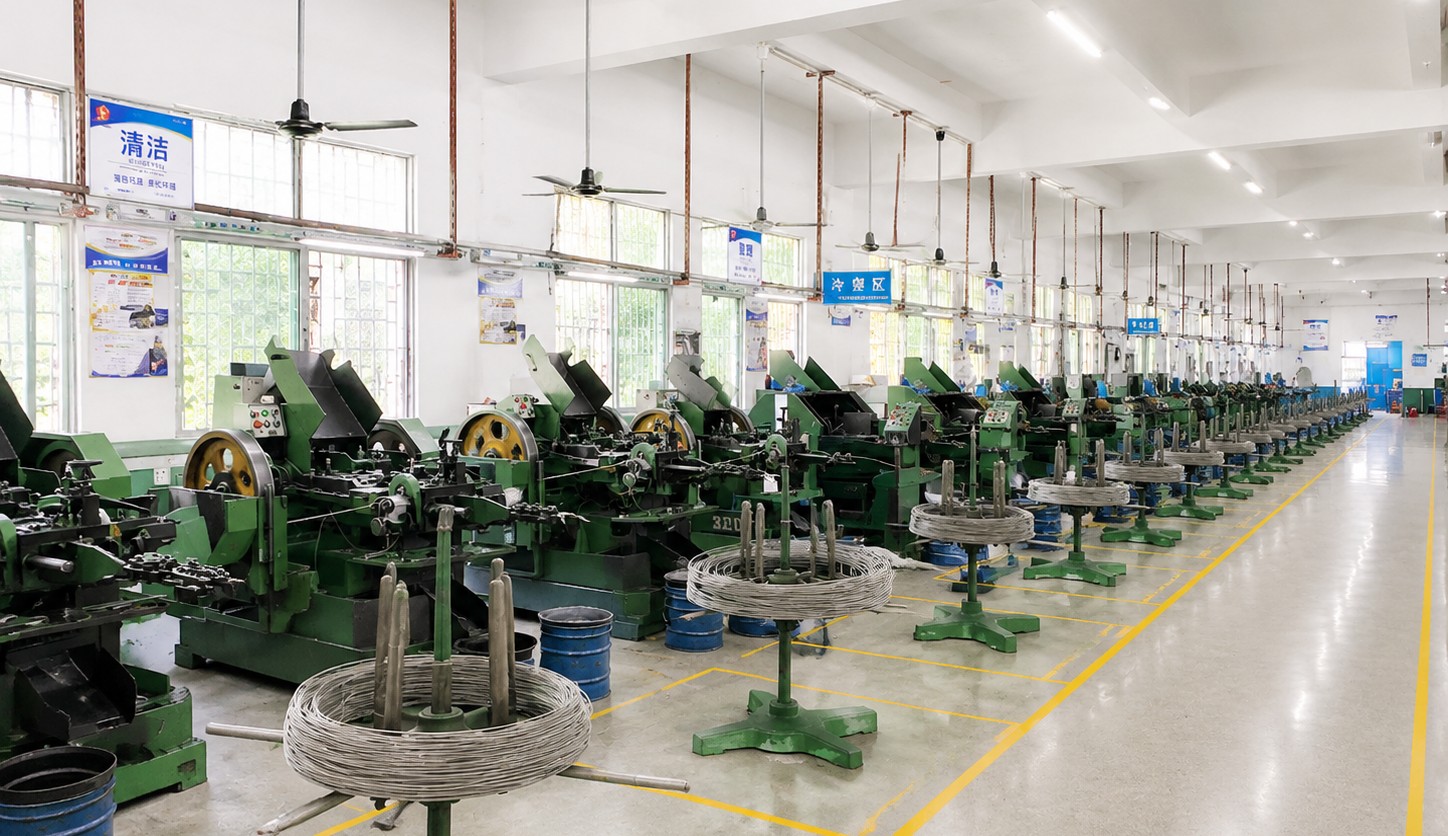
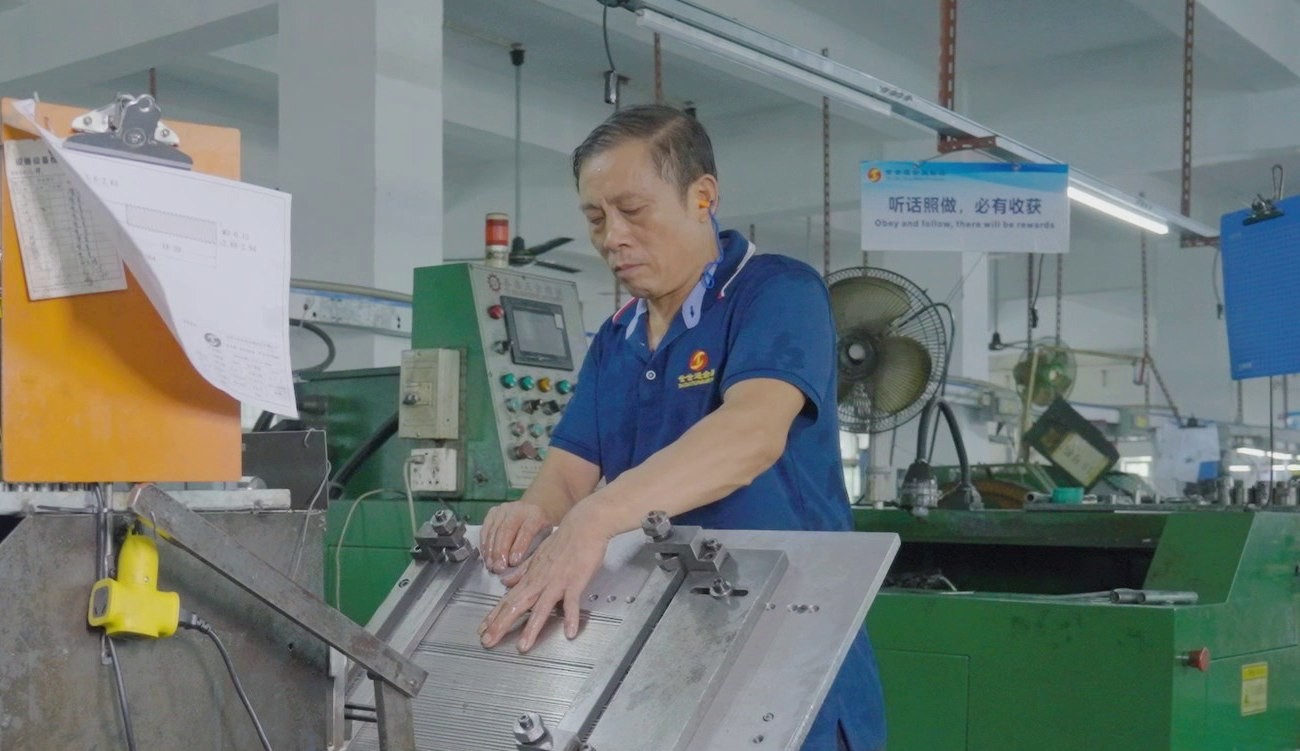
Shi Shi Tong forms ultra low profile mini screws from 304 stainless wire on single-die headers that form the low head and cut the cross recess in one stroke, rolls the fine machine thread to a blunt chamfered end, deburrs the recess edge and passivates the parts. The first part of every run is measured on head height, head diameter and recess depth before the batch continues.
|
|
A low head is the hardest head to form cleanly. The punch has to stop the metal at a height it would rather overshoot, and the cross recess is cut into a face that is already thin, so the metal has less room to flow. A worn punch shows up as a head that is slightly high in the middle, and a bit then seats on the high spot instead of in the recess.
What decides whether ultra low profile mini screws pass is the head height, the head diameter, the recess, the thread and the burr at the recess edge. The inspection agreement covers those, and the criteria come from the drawing.
Head height and recess on the projector |
Thread gauged per batch |
Hardness checked on the wire |
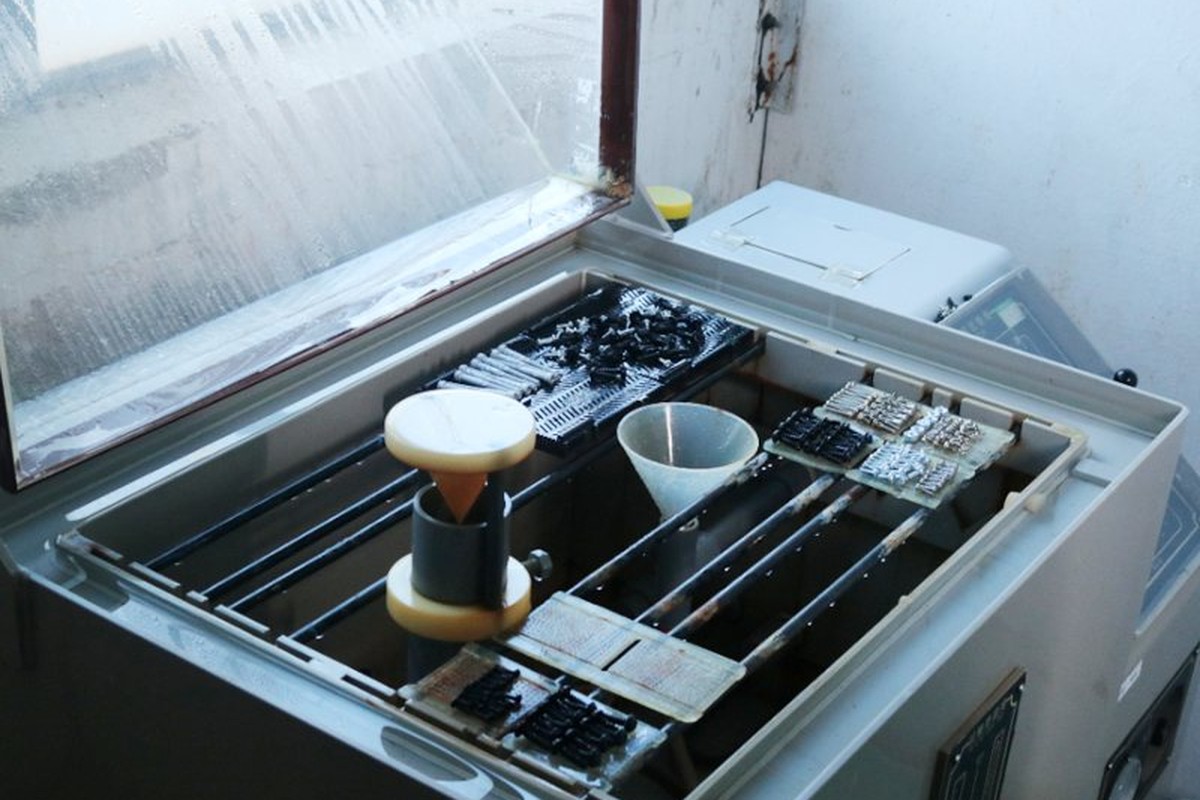
Salt-spray testing of the grade |
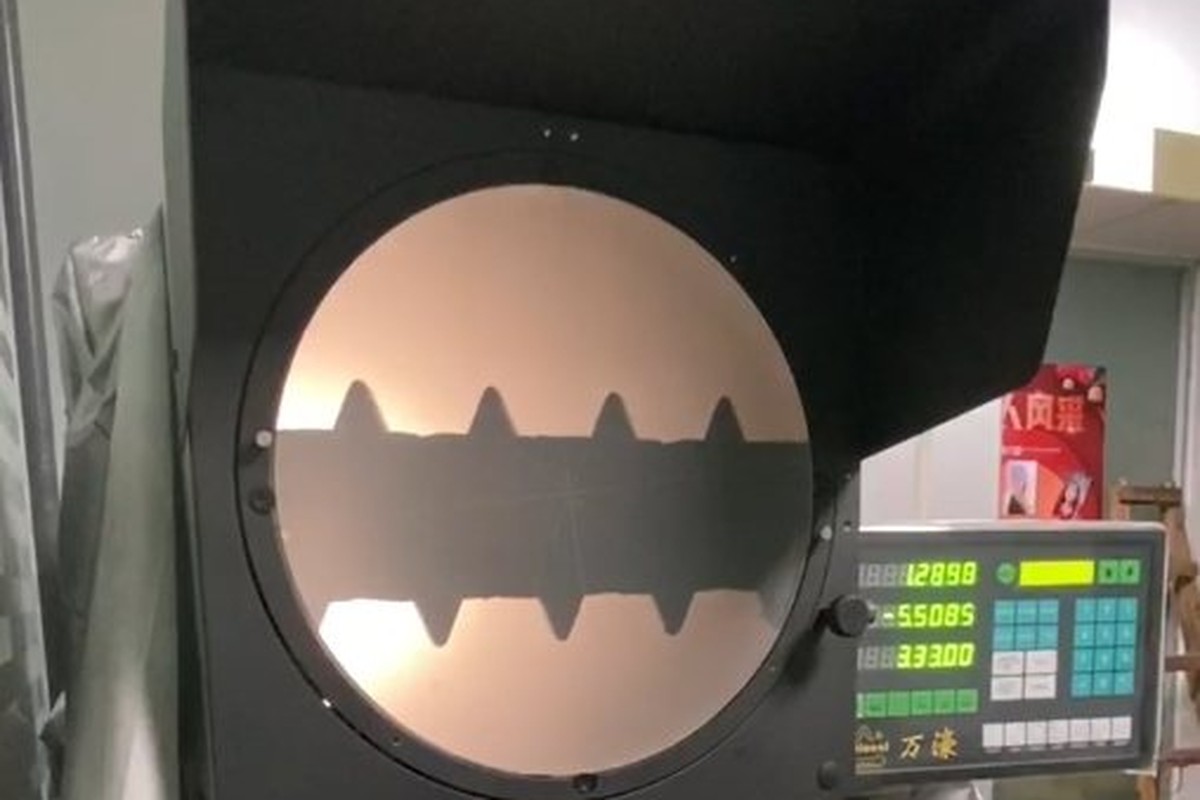
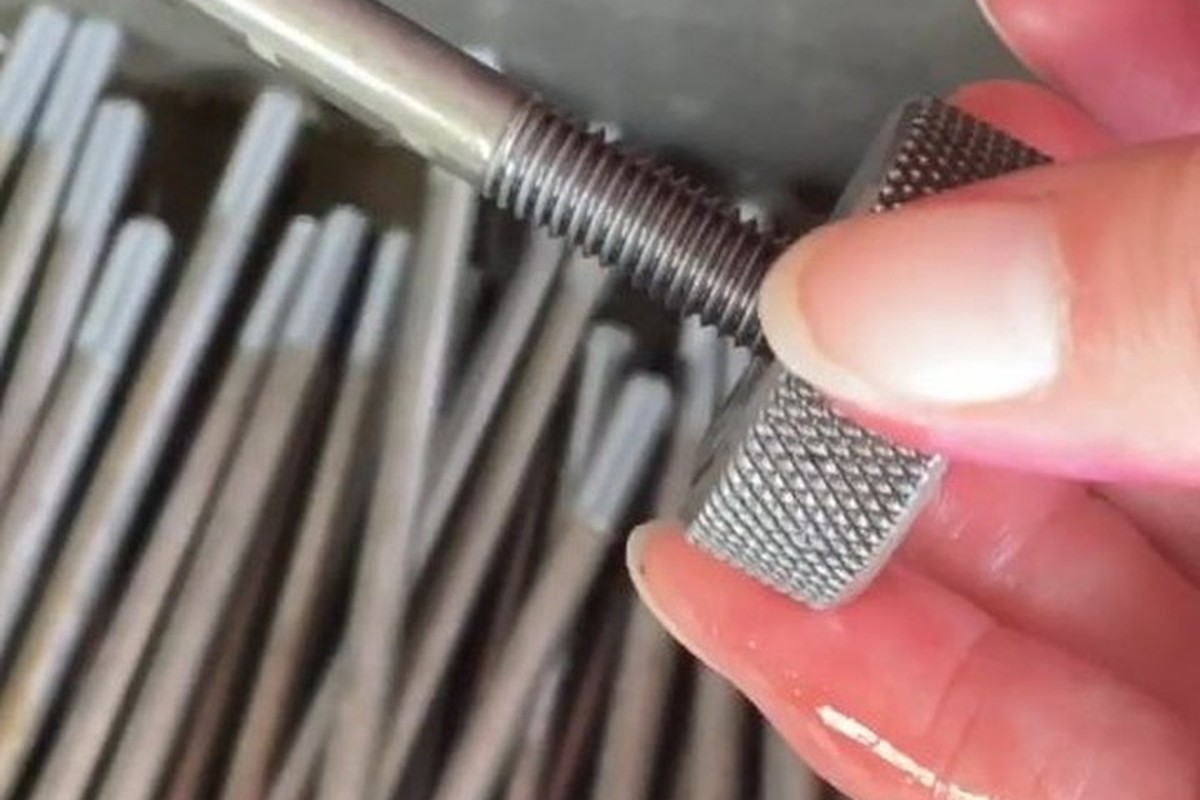
Head height is measured on the projector rather than with a caliper, because the top of the head is domed and a caliper reads the high point. The recess is checked for depth and for burr, the head diameter for the pocket fit, and the thread is gauged per batch at the small sizes.
Where the part goes into a moulded pocket, the first article is fitted into the customer’s cover and checked for flushness. That is a check the drawing cannot make, because the pocket is part of the customer’s part.
Every shipment of ultra low profile mini screws is traceable to the wire it was made from and to the passivation batch. The grade and heat number are recorded on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.
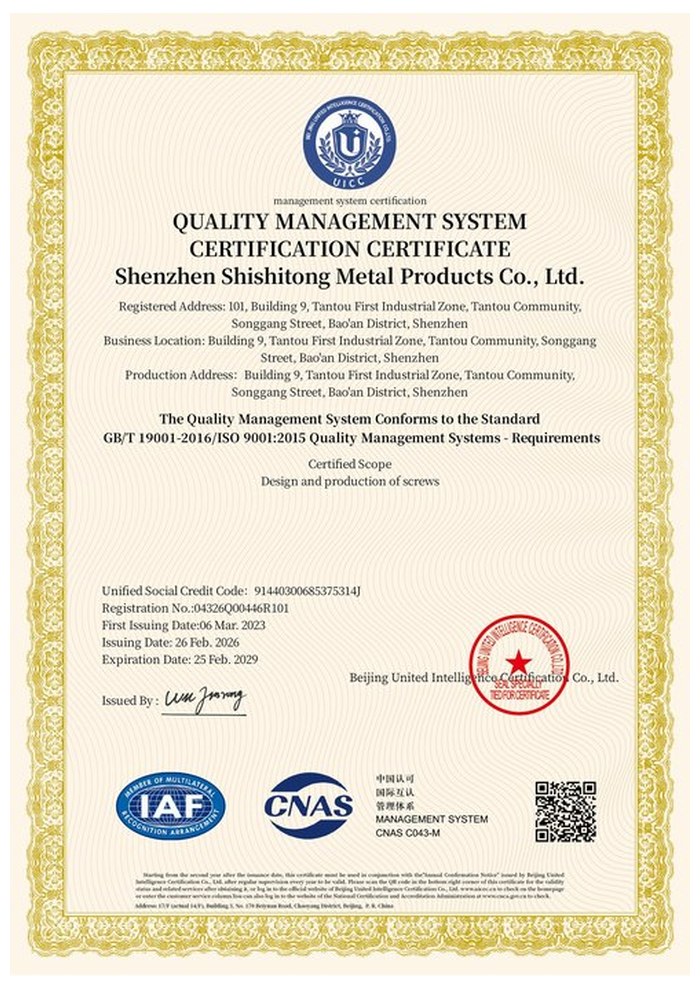
ISO 9001:2015 |
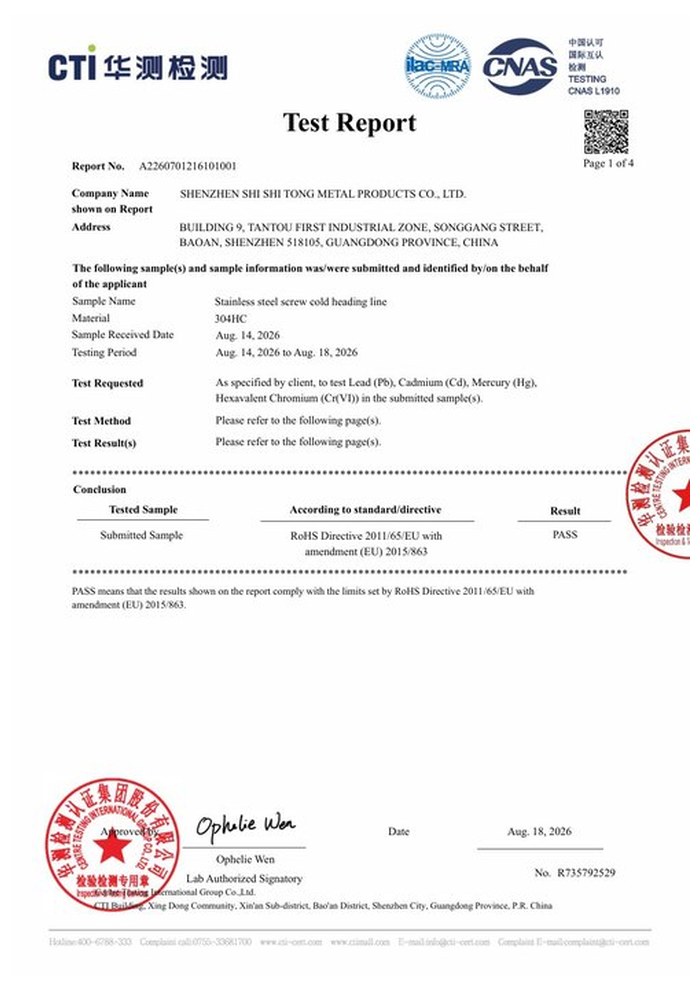
RoHS test report |
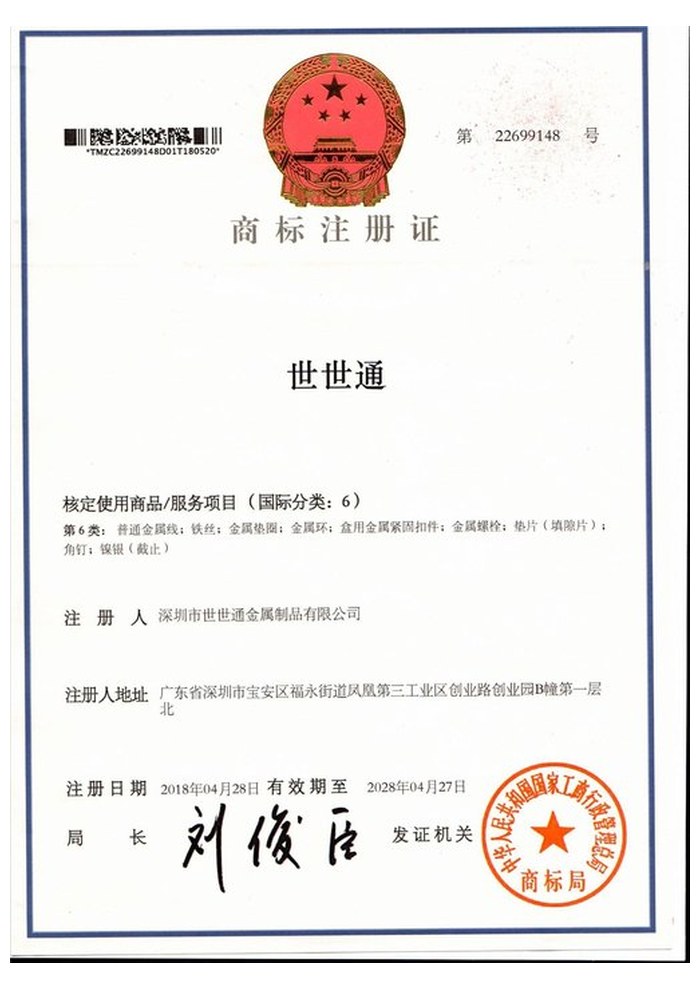
Registered trademark |
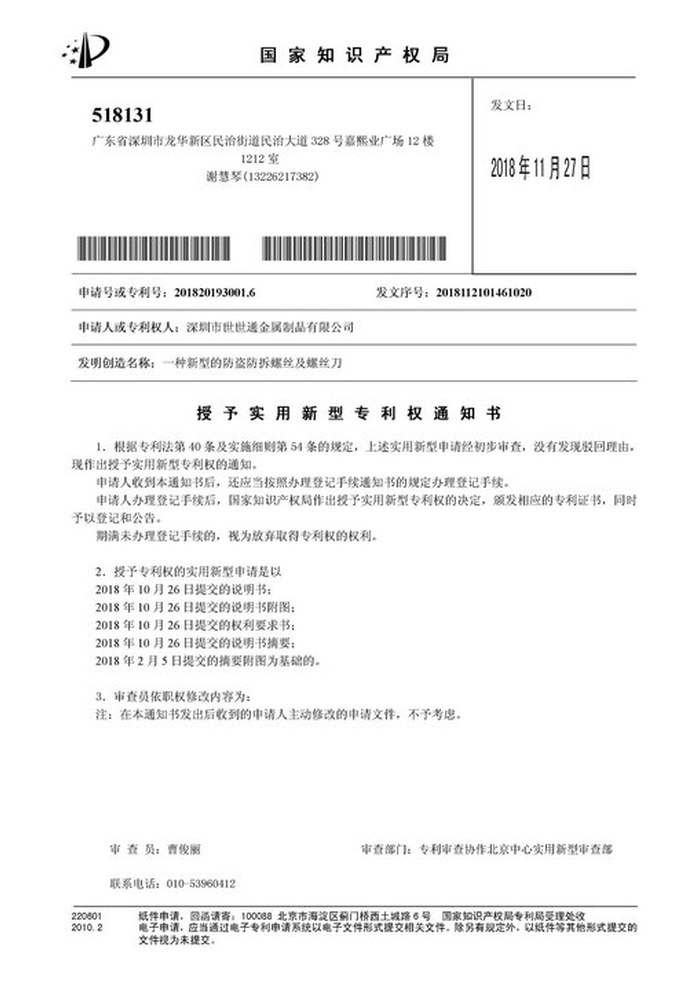
Patent: security screw and driver |
With each batch we supply the material certificate, the inspection record for the criteria on the drawing and, where it is listed, the third-party report for the grade or the passivation. The documents carry the drawing revision and the batch number, so a repeat order is made to the same head height that was approved.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a thin-headed mini screw the first article is fitted into the customer’s pocket, because clearance is what the part is for. Buyers visit during the process to review samples and to see how the heads are formed.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the passivation line can be seen on the day the parts run.
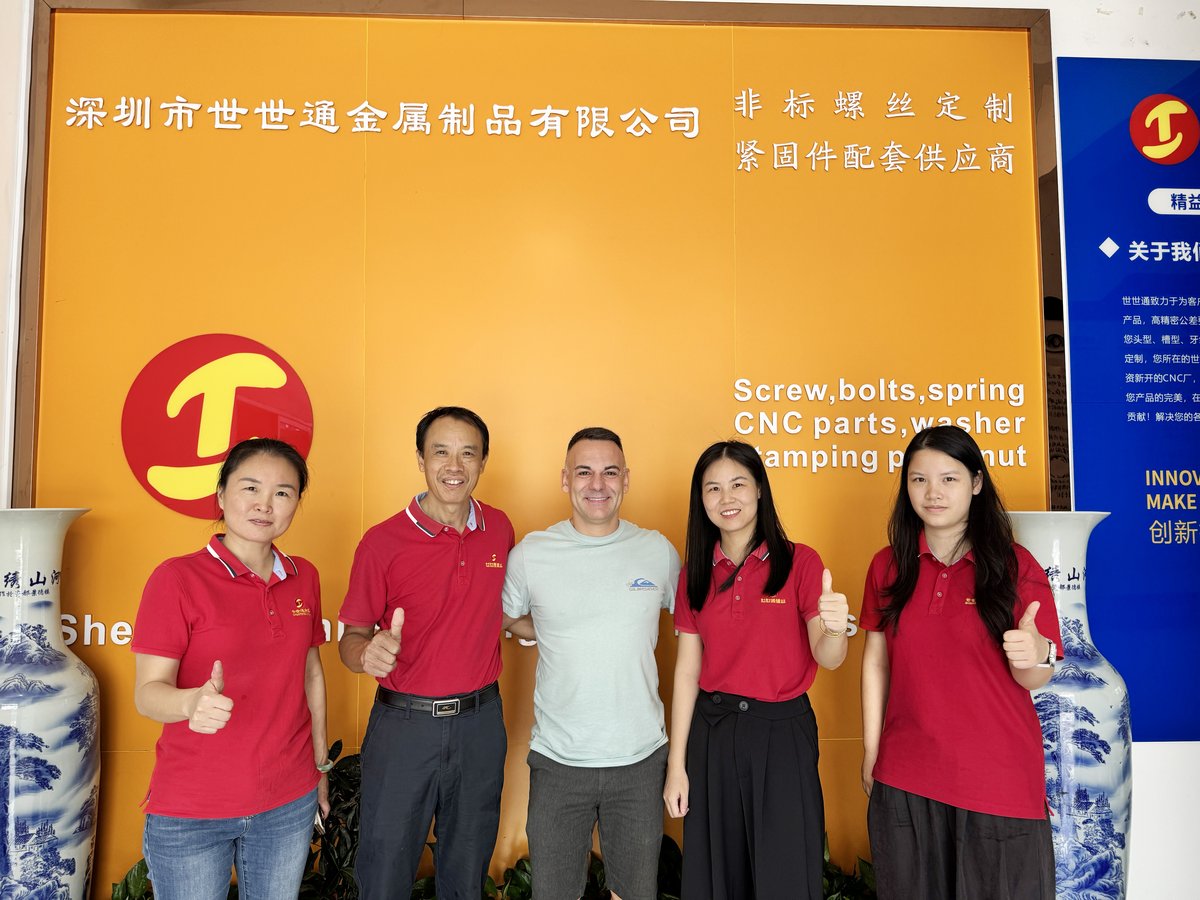
Customer group visit – sample review |
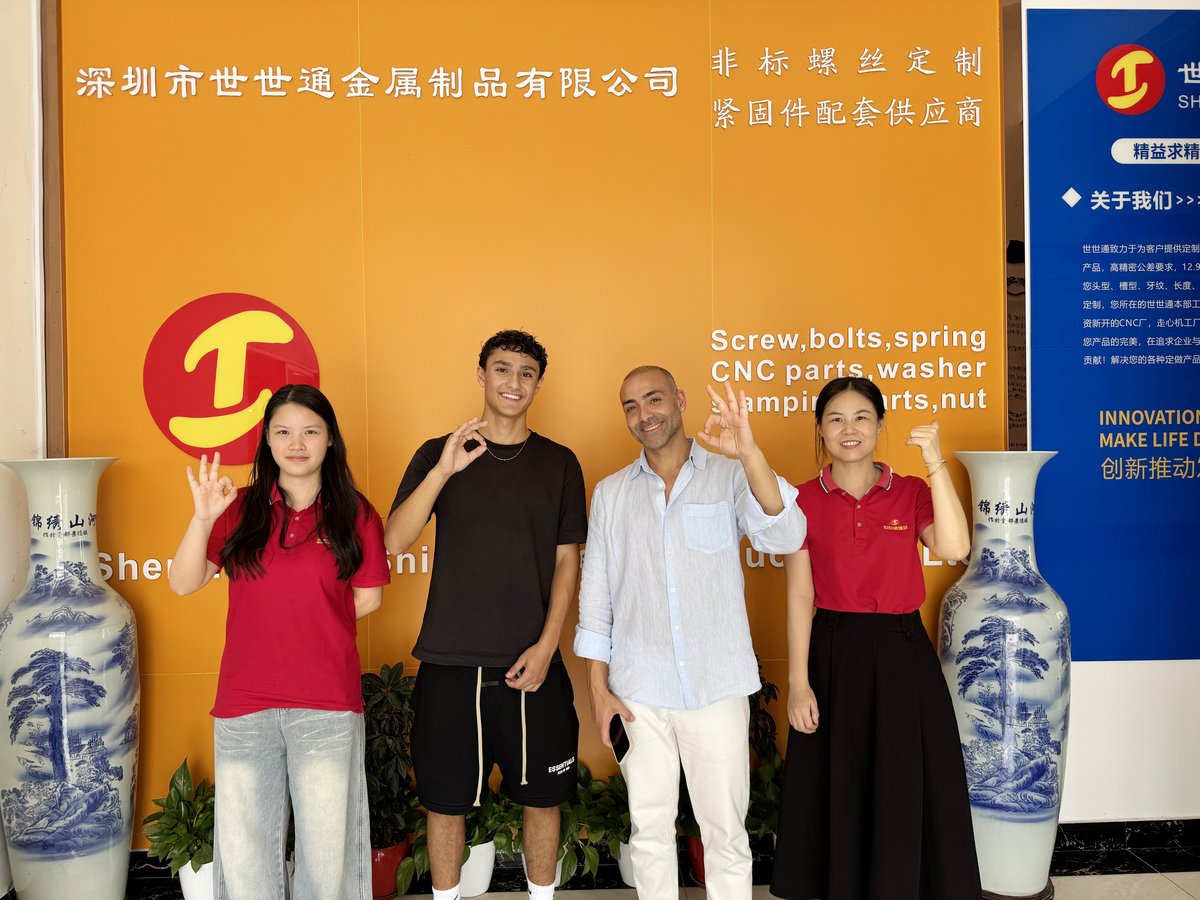
Customer group visit – process discussion |
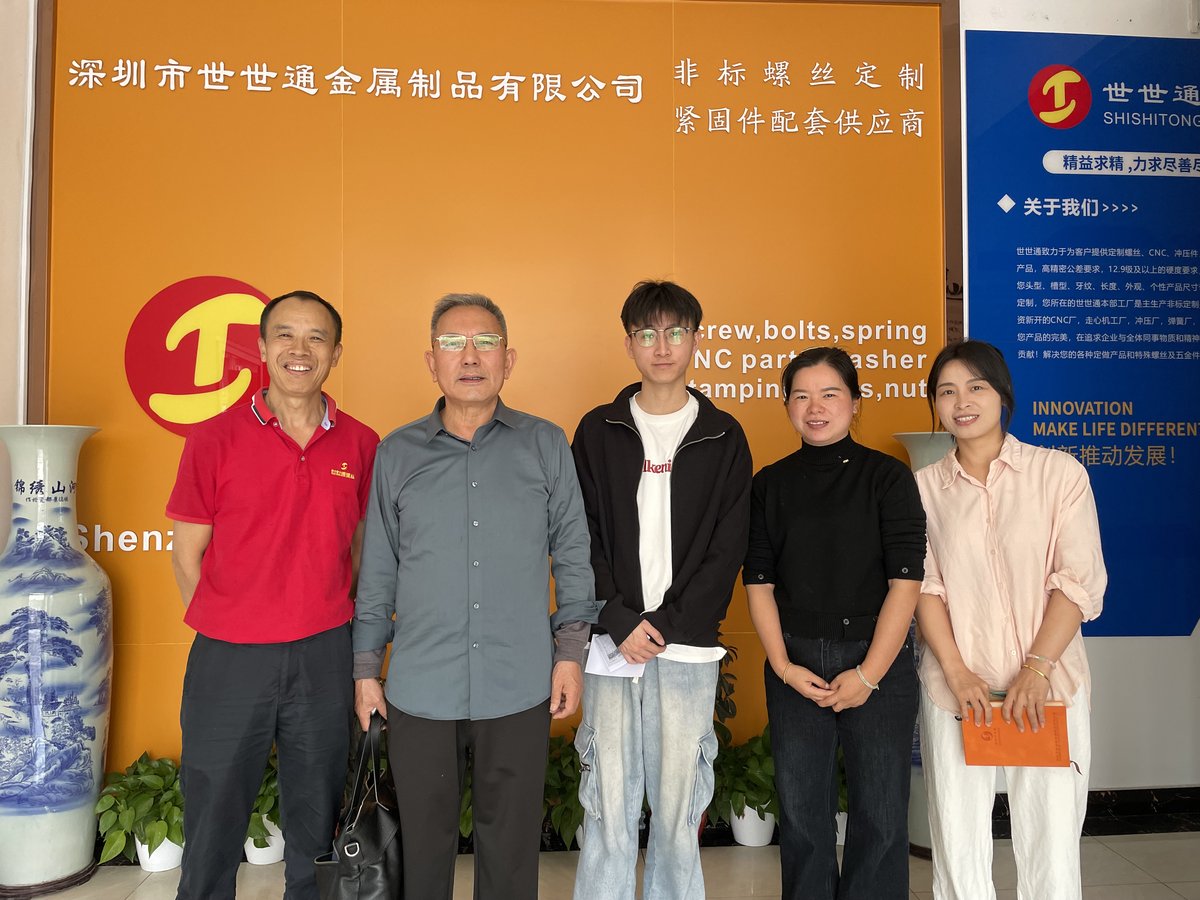
Customer group visit – factory tour |
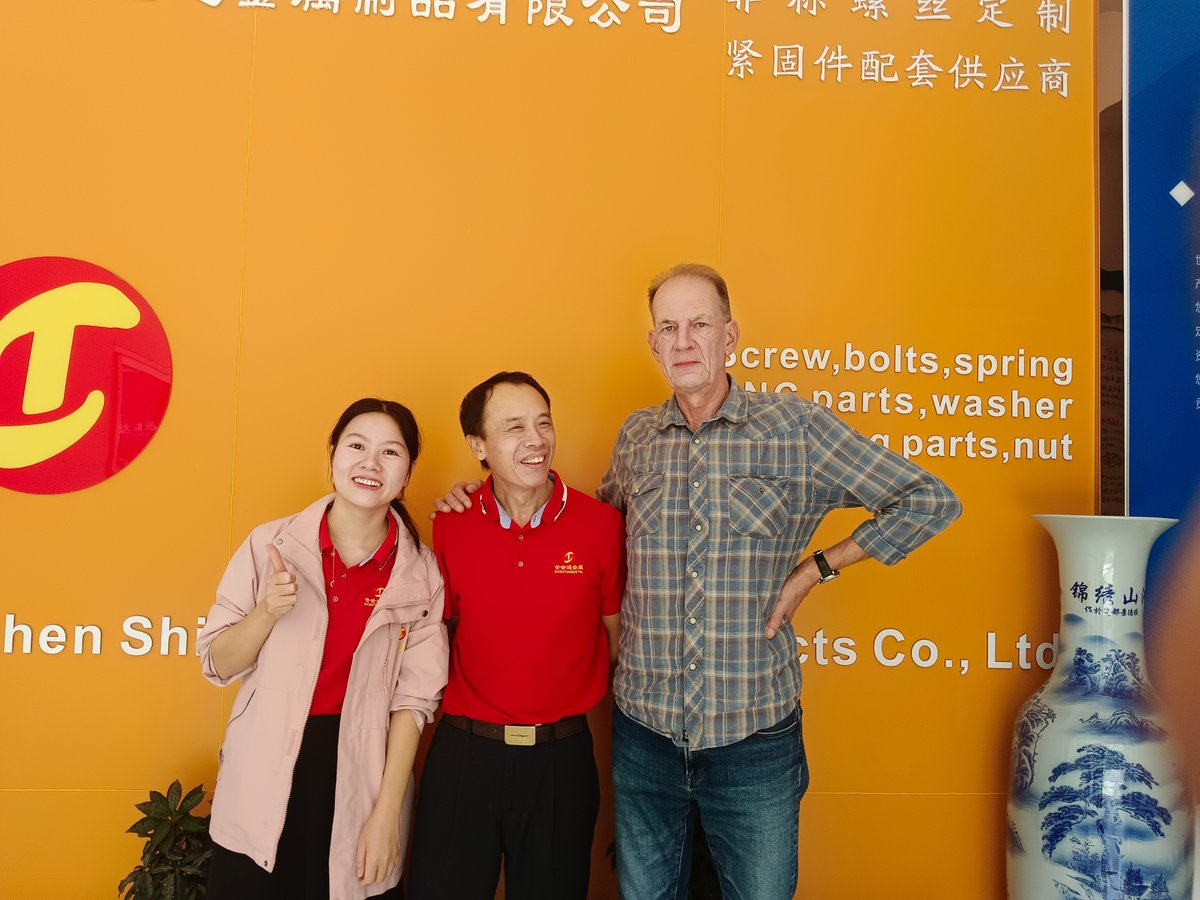
Customer visit – project kick-off |
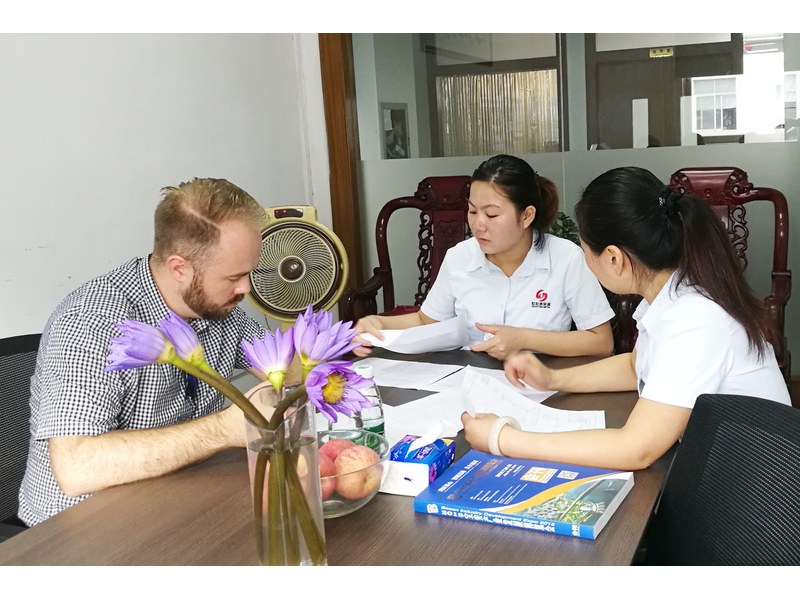
Danish customer – drawing review |
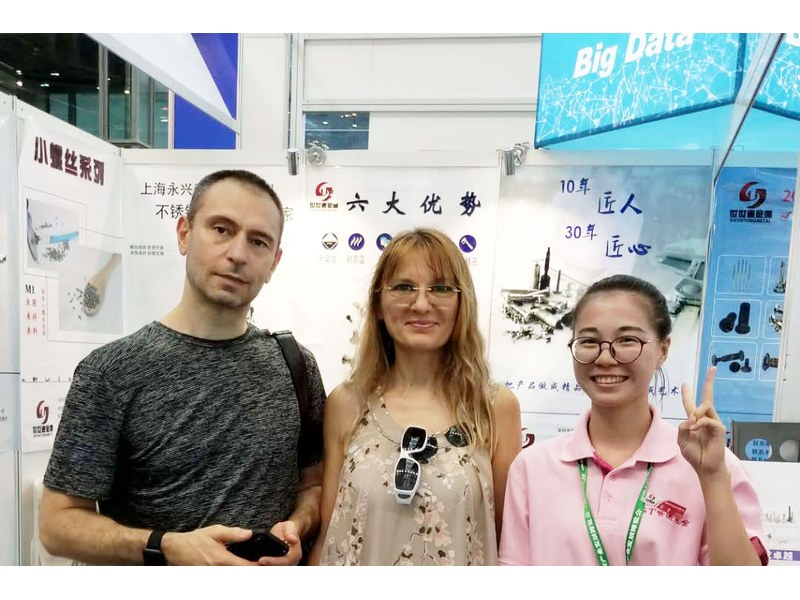
Industry exhibition – meeting customers |
The recess has to be shallow to fit a thin head, so the bit engages less. A torque the recess will take, and a bit in good condition, keep it seated.
It follows the thread size and the recess. The head height tolerance is quoted with the recess depth, because one sets the other.
It carries the same thread, but the bearing face is small. On a soft seat a washer or a wider head is the safer choice.
PH000, PH00 or PH0, depending on the screw. The bit has to match the recess exactly, and it has to be changed when it wears.
304 covers ordinary exposure. For chlorides, the grade to specify is 316.
Thread size and length, head diameter, head height with a tolerance, recess size and depth, the grade and the torque the joint will use.
How an ultra low profile mini screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the pocket it fits
|
→ |
2
Head height, recess and thread agreed
|
→ |
3
First article fitted into your pocket
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the thread size and length, the head diameter, the head height including tolerance, the recess size and depth, the grade and the torque the joint will use.
|
Thread size
|
Length
|
Head diameter
|
|
Head height
|
Recess size
|
Pocket depth
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.
 +86 13143444311
 sst@szsst88.com