Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
Type:Titanium Screws, Screw In China
Materials:Titanium
Surface treatment:Anodized
Head Type:Pan Head
Drive:Phillips cross recess
Thread:Machine thread
Point:Plain, chamfered
Forming:Machined and threaded
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
Number:353
We make anodized titanium screws in titanium with a pan head and a Phillips recess, quoting them from M1 to M10. Grade, head and recess, thread and colour come from your drawing, and the first article is checked against your colour reference.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
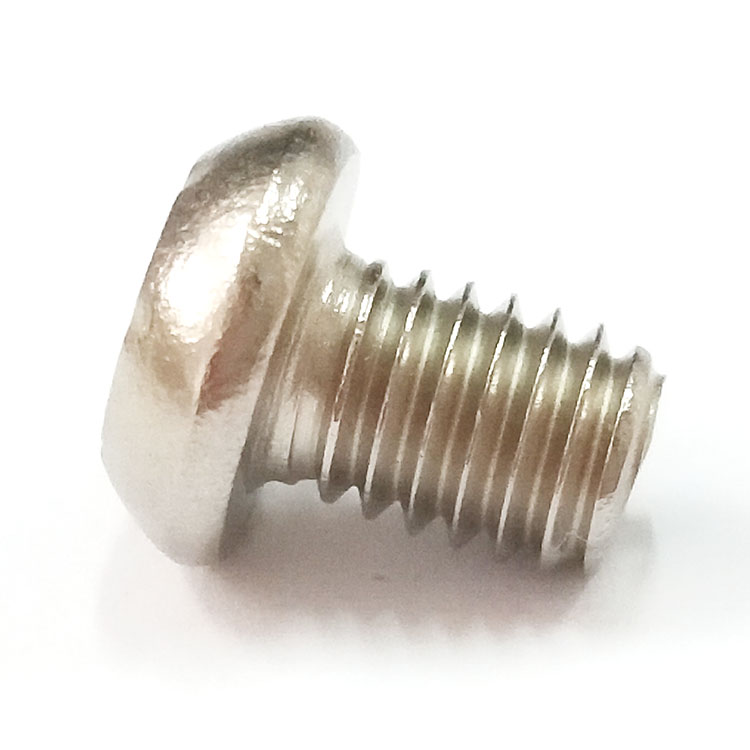
Anodized titanium screws are titanium fasteners whose surface oxide has been thickened and, in most cases, dyed by an anodising process, so the part takes a colour without any applied coating. The part recorded here is a pan head Phillips machine screw, quoted from M1 to M10 with Number 353.
Titanium body. A light, strong, non-magnetic metal that is about 57 percent of the density of steel.
Anodised finish. A thickened oxide grown from the metal itself, coloured by the anodising voltage rather than painted on.
Pan head. A rounded head with a wide bearing face, so the clamp spreads without a washer.
Phillips recess. Four tapered arms driven with a standard cross-tip bit.
Machine thread. A uniform thread for a tapped hole, a nut or an insert.
Anodized titanium screws are used in consumer hardware, medical and laboratory equipment, sports gear and marine fittings, where the colour of the fixing is part of the design, the joint has to stay non-magnetic, and a coated or plated part would wear through.
For anodized titanium screws the finish is not a coating. The process grows an oxide layer from the titanium surface itself, and it is the thickness of that layer — set by the voltage — that produces the colour, by interference rather than by pigment. The consequence is that the colour cannot flake off, because there is nothing sitting on top of the metal to flake; what happens instead is that the layer wears thin where it is rubbed, and the colour fades towards the natural grey of the metal.
That difference matters on anodized titanium screws. A plated screw in a joint that is opened repeatedly loses its plate at the recess first, and the bare steel underneath rusts. An anodised titanium screw loses oxide at the recess too, but what it reveals is titanium, which still does not rust; the joint keeps working and only the colour changes.
The weakness of anodized titanium screws is that the layer is thin and relatively soft. It survives handling and occasional service, but a Phillips recess driven by a worn bit will dull at the arms, and a threaded part run in and out of an aluminium insert will show bright wear on the crests. Where the appearance has to survive many assemblies, the answer is a drive with more contact area, not a thicker anodising.
The pan head is the right partner on anodized titanium screws. It gives a wide bearing face so the head does not sink into a soft panel, and its dome reads as a deliberate finish rather than as hardware. The Phillips recess keeps the cost down and matches the tooling most assembly lines already have.
The titanium underneath then decides the behaviour of anodized titanium screws. It is strong for its weight and it does not corrode in ordinary service, but its elastic modulus is about half that of steel, so it stretches more under the same load, and it galls against itself and against aluminium. An anodised layer helps a little with galling, which is one reason coloured titanium screws feel smoother to assemble than plain ones.
The recorded range is M1 to M10, with lengths made to the drawing. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For anodized titanium screws the quotation carries the grade, head diameter and height, PH size and recess depth, thread pitch, the anodising colour and the overall length.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Pan, rounded top | Diameter, height and bearing face |
| Recess | Phillips, PH size per diameter | Arm depth and floor thickness |
| Thread | Machine thread | Pitch, length and start position |
| Length | Overall, head included | Length tolerance and thread start |
| Grade | Commercially pure or alloy | Grade stated and traced |
| Finish | Anodised, coloured | Layer thickness, colour and uniformity |
The colour belongs on the drawing as a target rather than as a word. Anodised titanium colours depend on voltage and surface preparation, so two suppliers asked for “blue” can deliver two different blues; a sample or a colour reference avoids that.
PH size and head height are quoted together, because the recess is the feature that shows wear first on a coloured part. A deeper recess with a well-formed floor gives the bit more contact and keeps the colour intact longer.
Four features define anodized titanium screws, and each one is a trade:
| Feature | What it gives | What it costs |
|---|---|---|
| Titanium body | Light, strong for its weight, non-magnetic | Costly material and machining |
| Anodised colour | Integral colour that cannot flake | Layer is thin; wears at the recess |
| Pan bearing face | Clamp spread on thin panels | Stands above the surface |
| Phillips recess | Standard bit; low cost | Dulls at the arms with a worn driver |
| Machine thread | Repeatable joint | Galls in aluminium; lower preload than steel |
The value is a coloured fixing that behaves like metal rather than like paint. On a consumer product where the screws are part of the finish, an anodised titanium screw keeps its colour through handling and cleaning, and it does not produce the white flake a plated screw leaves when it fails.
The cost is concentrated in the recess and in the material. Titanium is expensive to buy and slow to machine, and the cross recess is the least durable drive for a coloured head, so the joint has to be treated as one that is assembled and left.
The recorded finish is anodising on titanium with no applied coating. It is the finish that suits titanium best: the colour lives in the oxide, the process does not change the dimensions measurably, and the part keeps its non-magnetic, corrosion-resistant behaviour.
| Option | How it protects | Effect on recess and thread | Typical use |
|---|---|---|---|
| Anodised, coloured | Thickened oxide, integral colour | No build; recess as formed | Visible consumer hardware |
| Plain, passivated | Native oxide | Recess and thread as machined | Medical and marine |
| Black PVD | Hard decorative layer | Harder than anodising; recess checked | Optical and tactical |
| Bead blasted, plain | Matte native oxide | Texture only | Matte visible parts |
| Gold plated | Decorative metal layer | Wears at recess edges | Jewellery-like hardware |
Where the screw is handled hard or opened often, PVD is the harder finish and keeps the colour longer, at the cost of a measurable build that has to be allowed for in the recess. Where the joint is static and the colour matters, anodising is the cheaper and more natural choice.
Where the part is medical or in salt water, plain passivated titanium is often preferred: the colour is decorative, and any finishing step is another thing to control.
Three assemblies where colour and material both matter:
| Where it sits | The screw fixes a case or a bezel where the head is visible and the colour has to match the housing. |
| When it goes wrong | The colour dulls at the recess and the fixing no longer matches the product. |
| Why it happens | The part is visible, handled daily, and assembled once. |
| What we control | Colour and recess checked; first article fitted and inspected as a set. |
| Where it sits | The screw holds a component where weight matters and the part is exposed to water and grit. |
| When it goes wrong | Plain titanium galls in the aluminium frame and the screw seizes. |
| Why it happens | The joint is light, exposed, and serviced occasionally. |
| What we control | Grade and thread checked; first article assembled with the agreed lubricant. |
| Where it sits | The screw holds a bracket inside equipment that is cleaned and must stay non-magnetic and corrosion free. |
| When it goes wrong | A steel screw is substituted and the instrument fails a magnetic or corrosion check. |
| Why it happens | The environment is aggressive, the part is small, and the finish is decorative. |
| What we control | Grade traced; first article cleaned as the process requires. |
Four reasons that matter on a coloured titanium part, each tied to something the drawing has to prove:
|
Colour and grade agreed
The titanium grade, the anodising colour and the recess size are agreed as a set, because colour and wear both depend on the surface preparation. Basis: Colour and grade agreed. |
Turned, threaded and anodised in one route
The part is machined, the thread cut or rolled, and the anodising applied as the last step so nothing disturbs the colour afterwards. Basis: One route from bar to anodised part. |
|
Recess and colour checked
The recess is proved with the production bit and the colour is checked against a reference, because both are what the customer sees. Basis: Recess and colour checked. |
First article in your joint
The first article is assembled in the customer part with the agreed lubricant, because titanium joints are decided by friction as much as by size. Basis: First article assembled in the joint. |
Small titanium screws are turned or headed, threaded, then cleaned and anodised. Anodising is done as the last operation, because the layer is thin and soft and any later handling would mark it; the first part of every run is measured on head, recess, thread and colour against the reference.


|

|
Anodising titanium is a voltage-controlled process rather than a dye bath. The colour comes from the thickness of the oxide, so the bath chemistry, the current and the surface preparation all decide the result, and a part that is handled or degreased unevenly takes an uneven colour. The process is run on batches of the same size and finish so that the colour stays consistent.
Handling after anodising is the second control. The layer marks if parts knock together in bulk, and a bright mark on a coloured head is the first thing an inspector sees. Parts are packed so they do not rub, and the recess is checked with the production bit before packing rather than on the line.
What decides whether anodized titanium screws pass is the head, the recess, the thread and the colour. The inspection agreement covers those, and the criteria come from the drawing.

Head and recess on the projector |

Thread and start checked |

Temper checked on the bar |

Salt-spray testing of the grade |
Head diameter and height are measured on a projector, the recess is proved with the production bit, and the colour is checked against a physical reference under the same light. Colour under a different lamp is not a comparison, which is why the reference is kept rather than described.
A sample from every batch is assembled into the customer’s part and removed. That cycle shows a recess that dulls on the first turn and a thread that galls, and neither is visible on a part that has only been measured.
Every batch is traceable to the bar it was made from and to the anodising batch that coloured it. The grade and heat number appear on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing and the anodising record. The documents carry the drawing revision and the batch number, so a repeat order keeps the same grade and the same colour.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On anodized titanium screws the first article is checked for colour against the customer’s reference, because colour is what the part is bought for. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the machining cells and the anodising line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
The colour is in the oxide, so it cannot flake. It dulls where it is rubbed, revealing titanium rather than bare steel.
Only by stripping and re-anodising, which also removes material and re-opens the recess. It is not a touch-up process.
For its weight, yes; for a given size, usually less stiff. Titanium has about half the modulus of steel.
Titanium galls. A lubricant at assembly and a slower drive are the practical answers.
Commercially pure for corrosion and formability, the alloy grade for strength. The two machine and behave differently.
Grade, head diameter and height, PH size, thread pitch, anodising colour reference and length.
How an anodized titanium screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the colour
|
→ |
2
Grade, recess and colour agreed
|
→ |
3
First article in your joint
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the titanium grade, head diameter and height, PH size, thread pitch, colour reference and overall length.
|
Grade
|
Head size
|
PH size
|
|
Thread pitch
|
Colour
|
Length
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com