Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
Materials:Titanium
Surface treatment:Anodized
Head Type:Flat Countersunk Head
Groove Type:Hexagon Socket
Thread Type:Machine
Point:Plain, chamfered
Forming:CNC turning from bar; socket machined; anodised
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
Number:192-1
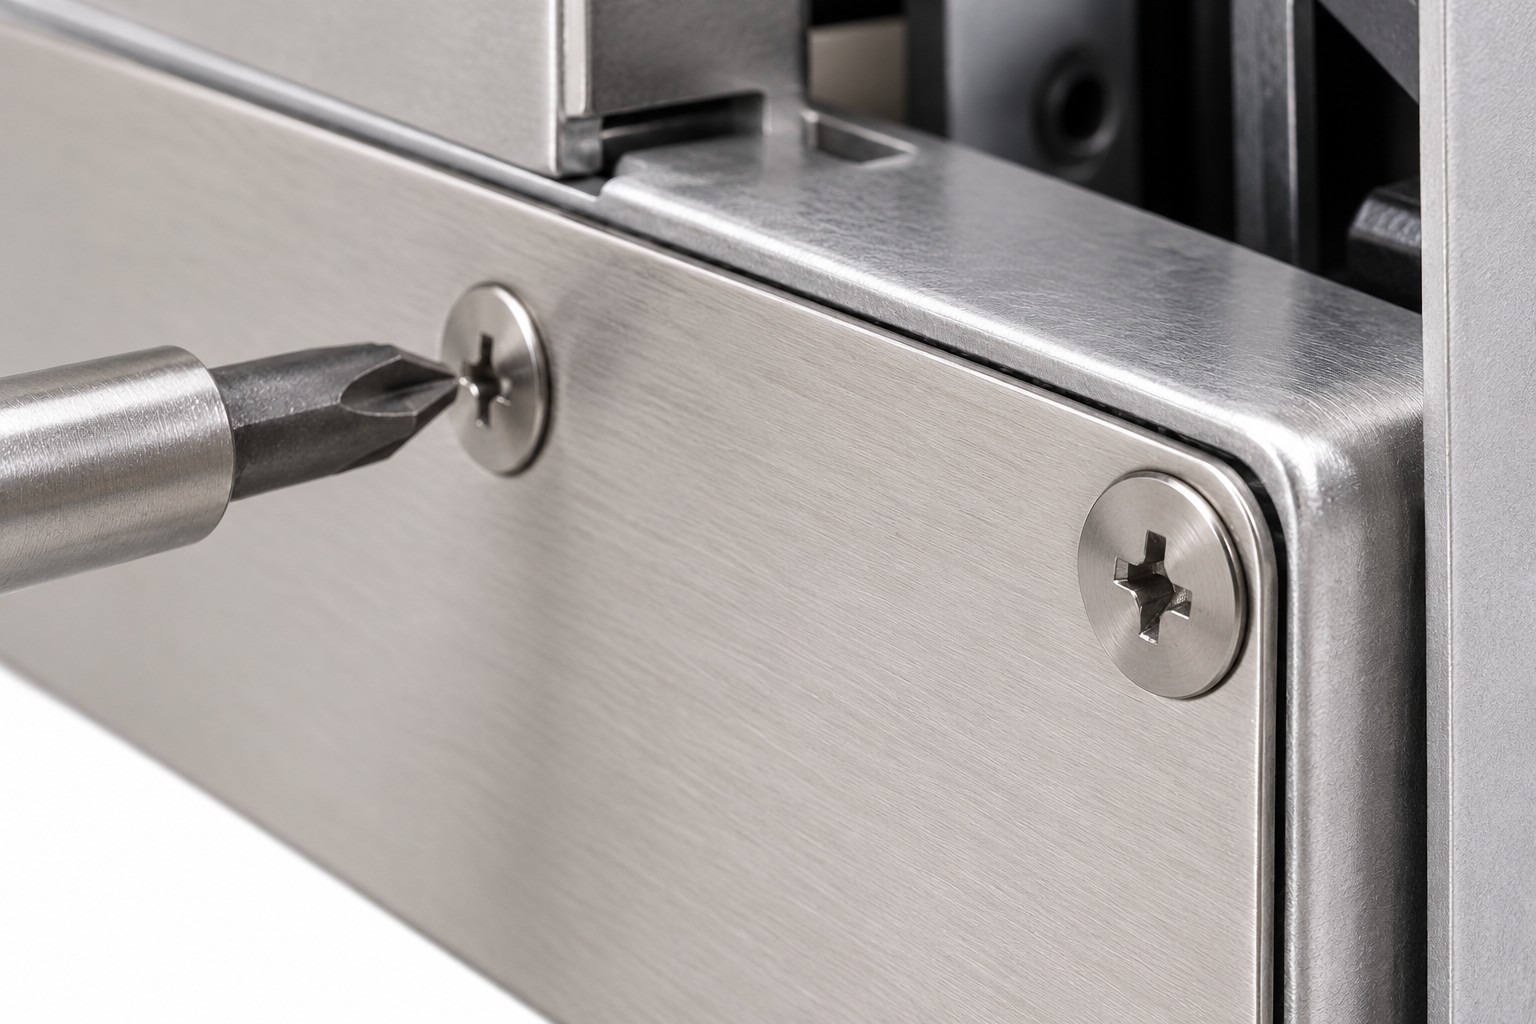
We make titanium flat head cap screws to the DIN 7991 proportion, anodised, with a countersunk seat and a hex socket, quoted from M1 upward to the drawing. The cone takes away the underside and the socket takes away the top, so the thin web between them is what carries the driving torque and sets the head’s ceiling.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
A titanium flat head cap screw is a countersunk socket screw made in titanium, with a conical underside and a hex socket in a flat top. This part is anodised, made to the DIN 7991 proportion, and is quoted from M1 upward with the head and the length made to the drawing.
Titanium body. Half the weight of steel, no rust, and no magnetism.
Countersunk head. A cone that seats into a matching countersink and finishes level with the surface.
Hex socket. Six flats in the top face, which is where the driving torque enters the part.
Anodised finish. Colour grown into the surface, adding no thickness to the cone or the socket.
They are used where a joint has to finish flush and stay light: instrument panels, marine fittings, drone and robotics frames, and any assembly where a socket head is preferred to a cross for the torque it carries.
A countersunk socket screw is a head with two hollows in it. The cone takes away the underside, the hex socket takes away the top, and what is left between them is a thin web of metal at the centre of the head. That web is the section that carries every bit of the driving torque from the key to the shank, and it is the thinnest part of the whole screw.
On a steel part that web is comfortable. On titanium it is where the margin goes first, because the material is stiffer and does not redistribute a local peak the way a softer head can. The failure, when it comes, is a crack starting at a corner of the socket and running down into the cone, and it appears under the driver rather than in service.
That is why the standard ties head height to socket size. DIN 7991 fixes both, and the pair is a package: a deeper socket buys key engagement and costs web thickness, a lower head buys clearance and costs the same web from the other side. A drawing that lowers the head without reducing the socket is asking the part to do both at once.
Titanium’s stiffness shows up in the seat as well. A steel countersunk head will conform slightly to a countersink that is a degree or two off its own angle. A titanium head stays on its machined faces, so the mismatch turns into a line contact at the rim and the load concentrates exactly where the head is thinnest.
The anodising does not change any of this, and that is one reason it suits a countersunk part: the oxide grows into the metal, so the cone and the socket keep the dimensions they were machined and measured to, and the head that seated on the bench will seat in the joint.
The practical rule is to specify the head as a whole rather than one dimension at a time. Head diameter, head height and socket size belong on the same drawing, with the countersink they will sit in, because each of the three changes what the other two can be.
Titanium flat head cap screws are quoted by head diameter and angle, head height, socket across-flats and depth, thread size and pitch, and length. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation carries the grade, the head, the socket, the thread and the anodising.
| Item | How it is defined | What we control |
|---|---|---|
| Grade | Commercially pure or alloy | Alloy and mechanical properties |
| Head | Countersunk, flat top | Diameter, angle and height |
| Socket | Hex socket | Across-flats, depth and corner radius |
| Thread | Machine thread | Size, pitch and class |
| Length | Overall, head top to point | Length and thread run |
| Finish | Anodised | Film thickness, colour and coverage |
The socket corner radius is written down because it is where the crack starts. A sharp corner concentrates stress at exactly the point where the web is thinnest, and a small radius there costs nothing on the drawing and everything on the part.
The head angle is normally 90 degrees, with 60 and 120 available for special countersinks. On a titanium head the angle has to match the plate rather than be close to it, because the head will not conform.
Length is measured overall, from the top face to the point. On a countersunk screw the head sits inside the plate, so the length is not the same as the grip, and the two are stated separately where the drawing needs both.
Four properties decide this part, and each carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Titanium body | Half the weight, no rust | Material cost and galling risk |
| Countersunk head | A flush finish in the plate | Thin web under the socket |
| Hex socket | High torque without cam-out | The socket eats into the web |
| Anodised finish | Colour with no build | The colour varies with the film |
The value is a flush, light, corrosion-free fixing that takes a real driving torque, on a panel where a raised head would spoil the surface.
The cost is a head that has less metal in it than any other socket form, so the torque ceiling of a titanium flat head cap screw is set by the head geometry rather than by the thread, and the drawing has to say so.
The trade is a flush head in a metal that is harder to machine than steel.
The recorded finish is anodised titanium. The oxide is grown in an electrolyte and its thickness sets the colour, so the finish is a surface rather than a coating: nothing to flake off the cone, and nothing added to the socket that would change how the key fits.
| Option | How it protects | Effect on socket | Typical use |
|---|---|---|---|
| Anodised titanium | Grown oxide, coloured | No build; key as machined | Visible instrument parts |
| Plain titanium | Natural oxide | No build | Mechanical and marine parts |
| Gold plated | Thin metal layer | Build; socket re-checked | Warm decorative finish |
| Dry film lubricant | Low-friction film | Thin; eases galling | Joints opened in service |
| Passivated | Cleaned, thickened oxide | No build | Medical and food equipment |
Anodising is the finish that respects the socket. Because the film grows into the metal, the hex keeps its across-flats and the key seats to the same depth as on the sample.
Where the joint is opened often, a dry film lubricant does more for the part than a colour: titanium galls against titanium and stainless, and the lubricant reduces both the running torque and the wear at the socket corners.
Three assemblies where a flush head and a light body both matter:
| Where it sits | The screw closes a cover into a counterbored panel where the face has to stay flat and light. |
| When it goes wrong | The head stands proud, or the socket rounds on the second assembly. |
| Why it happens | The countersink is shallower than the head, and the socket is driven with a worn key. |
| What we control | Head height and socket depth agreed; first article seated and driven. |
| Where it sits | The screw closes a housing that is immersed and must not rust or seize. |
| When it goes wrong | The thread galls, or the head cracks at a socket corner. |
| Why it happens | Plain titanium on titanium, and a low head with a deep socket. |
| What we control | Mating material and lubricant agreed; sample exposed and dismantled. |
| Where it sits | The screw holds a plate where every gram counts and the surface must stay clean. |
| When it goes wrong | The joint loosens with vibration, or the socket wears. |
| Why it happens | There is no locking element, and the driver torque is set by feel. |
| What we control | Socket size and driving method specified; sample cycled. |
Four points that decide whether a countersunk socket head survives the driver:
|
Head height tied to socket size
The drawing carries both, with the corner radius, because the web between them is what carries the driving torque. Basis: Web treated as a dimension. |
Socket machined before anodising
The hex is cut and checked with the key, and the finish is grown afterwards so it adds nothing inside it. Basis: Key fits the finished part. |
|
Driven in the real plate
The first article is seated in the customer countersink and driven at the joint torque before the batch is run. Basis: Seat and drive proved. |
Same head every lot
Head geometry, socket depth and anodising lot are recorded with the drawing revision, so a repeat batch takes the same key. Basis: Same head across lots. |
A countersunk socket screw fails in one of two places: the seat, if the countersink does not match, and the web, if the head was specified too thin. Both are visible on a first article driven in the real plate, and neither is visible in a tray of parts.
These screws are turned from titanium bar, with the cone formed in the same setup as the head, the hex socket milled or broached, the thread cut or rolled, and the parts anodised. The first piece of every run is measured on head angle and diameter, head height, socket across-flats and depth, thread and length.


|

|
The socket is the machining step that decides the torque the head can take. It is cut after the cone, so the two are concentric, and its depth is set from the head height rather than from the key: a socket that is machined as deep as the key allows may leave too little web for the material.
Titanium work-hardens at the cut, so the socket walls are finished with a light pass and the corners are left with the radius the drawing asks for. A corner that is sharper than drawn is where a crack will start, and it is invisible once the part is anodised.
Anodising follows the machining and is controlled by voltage and time. Because the film grows into the surface, the anodised part is measured against the same head and socket dimensions as the bare one, and that is why the finish is applied after the socket is checked rather than before.
What decides whether a batch of titanium flat head cap screws passes is the cone that seats, the socket that drives it and the web that carries the torque between them. The inspection agreement covers all three.

Head, cone and socket on the projector |

Thread checked with gauges |

Material checked |

Salt-spray testing where a coating applies |
The head is measured for angle, diameter and height, and the cone is checked for a continuous face. On a countersunk socket head the cone is the bearing surface of the joint, so a wavy or stepped cone is a defect even when the angle reads correctly at one point.
The socket is measured for across-flats and depth and driven with the key at the joint torque, then inspected for cracks at the corners. That combination is the check that matters: a socket that measures right and cracks under drive was specified too deep for its head.
The web is checked on a section from the sample lot, where the drawing asks for it. It is the one dimension that cannot be measured from outside, and it is the one that sets the torque ceiling of the part.
Every batch of titanium flat head cap screws is traceable to the bar it was made from and to the anodising lot that coloured it. The material certificate states the grade, the heat number, the chemistry and the mechanical properties; the anodising record carries the film thickness and the lot.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the head, cone and socket, and the anodising record. The records carry the batch number, so a repeat order can be compared with the first on the dimensions that decide the seat and the drive.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a countersunk socket screw the first article is seated in the customer’s countersink and driven at the joint torque, because the seat and the web are both tested by that one step. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the machining cell and the anodising line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
The web between the socket and the cone is thin. A deep socket in a low head leaves too little metal to carry the driving torque.
No. The oxide grows into the metal, so the hex keeps its across-flats and the key seats to the same depth.
The countersink angle or depth does not match the head, and a titanium head will not conform the way a steel one does.
Only with the socket, and only against the countersink. Lowering one without the others eats the web or leaves the head proud.
It can against titanium or stainless. A dry film lubricant or a different mating material prevents it.
Grade, head diameter and angle, head height, socket size and depth, corner radius, thread and length.
How a countersunk socket screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the plate sample
|
→ |
2
Head, socket and seat agreed
|
→ |
3
First article seated and driven
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision used for the first article is what repeat orders are checked against.
For a quotation, send the drawing with the grade, head diameter and angle, head height, socket size and depth, corner radius, thread and finish.
|
Grade
|
Head angle
|
Head height
|
|
Socket
|
Thread
|
Finish
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com