Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
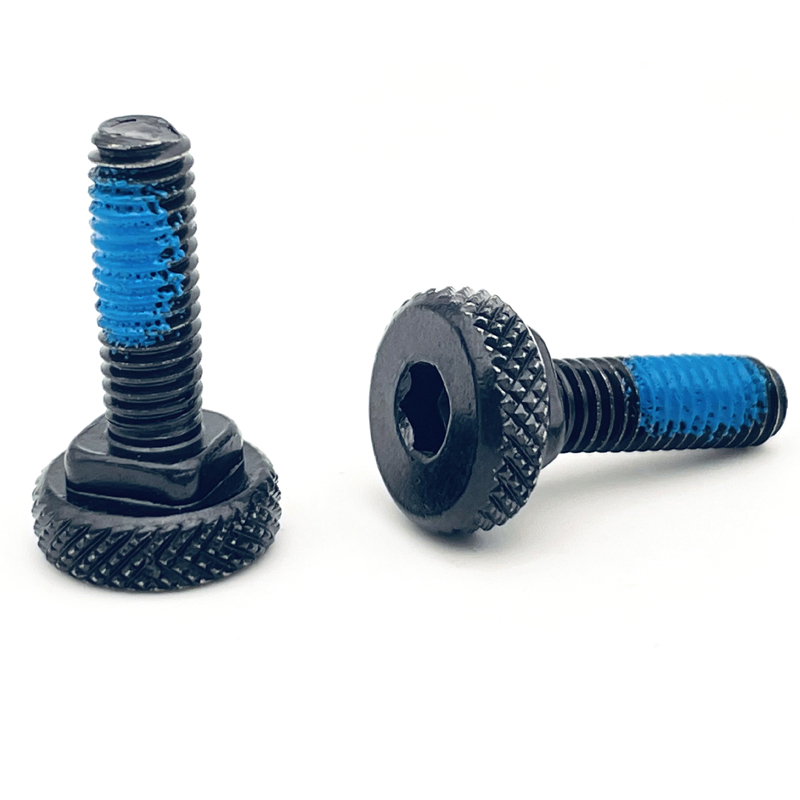
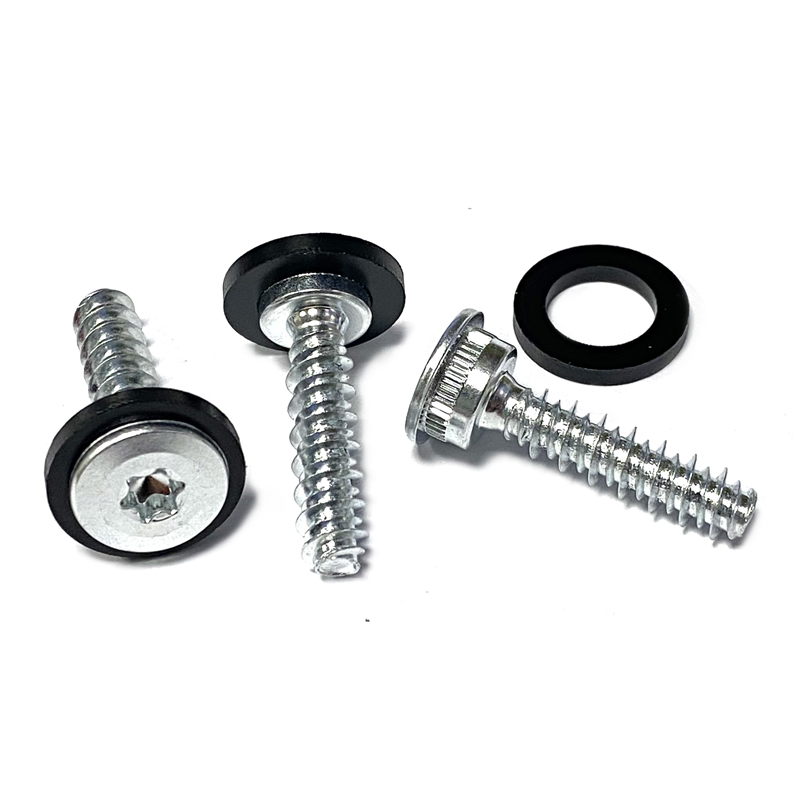
Type:M3 Shoulder Screw
Materials:Stainless Steel
Surface treatment:Plain
Head Type:Small head with shoulder
Drive:Torx six-lobe recess
Thread:Machine thread, partial
Point:Plain, chamfered
Forming:CNC turning and grinding; recess milled
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
We make M3 shoulder screws in stainless steel with a six-lobe Torx recess, quoting the shoulder and head to the drawing. The recess is sized to the head so the screw can be driven to the shoulder seat with the bit you assemble with, and the first article is fitted into your bore.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
An M3 shoulder screw has a 3 mm thread with a ground shoulder in front of it that locates the part and carries it at a fixed height. The part recorded here is stainless steel left plain, with a six-lobe Torx recess in the head, quoted with the shoulder made to the drawing.
M3 thread. A small machine thread, usually into a tapped hole or a nut.
Ground shoulder. A precision diameter that passes through the bore and sets the position of the part.
Torx recess. A six-lobe recess driven with a matching bit, sized small enough for a 3 mm head.
At M3 the screw is small enough that the recess, not the thread, is what limits how much torque reaches the joint. The shoulder is the only surface that touches the bore, so the joint is defined by two machined features rather than by how deep the thread engages.
On these M3 shoulder screws the thread is rarely the weak point. A 3 mm stainless thread into a tapped hole takes more torque than the head can transmit, which means the drive decides how far the screw gets: it either reaches the shoulder, or it slips before it does.
This is where the recess shape changes the outcome. A cross recess is four slots cut into a small head, so the walls left standing between the slots are thin, and the driver bears on short edges. A six-lobe recess leaves more material between its lobes for the same outside diameter, and the driver engages along six flanks instead of four short edges. The result is that the same head can transmit more torque before the bit starts to climb out.
That matters because a shoulder screw has to reach its seat. Until the shoulder touches, the joint is not positioned; a screw that has been driven to the point of skipping has usually been driven just short of that. On an assembly line the difference shows as a joint that looks tight but has a gap at the shoulder.
The cost is on the other side: a Torx bit is a specific size, and it has to be the right one. A bit that is one size small will turn in the recess and wear its lobes; a bit that is worn does the same. Neither is visible on the part, which is why the bit is part of the assembly method rather than an accessory.
The recess also takes up head material. On an M3 head there is a limit to how deep it can be cut before the head becomes thin over the shoulder, so the drive size has to be agreed with the head diameter and height, not chosen on its own.
The recorded part is quoted to the drawing, with the shoulder, head and drive stated separately. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation for M3 shoulder screws carries the shoulder diameter and tolerance, the shoulder length, the head diameter and height, the Torx size and the thread.
| Item | How it is defined | What we control |
|---|---|---|
| Shoulder diameter | Ground, fits the bore | Diameter, roundness and finish |
| Shoulder length | From the head underside | Length and squareness |
| Head | Small, for M3 | Diameter, height and bearing face |
| Recess | Torx, one size | Size, depth and lobe form |
| Thread | Machine thread after the shoulder | Size, length and start |
| Bore | In the customer part | Agreed with the shoulder |
The recess size is written on the drawing as a Torx number rather than as a diameter, because the bit is defined by that number. Substituting the next size up does not fit the head; the next size down turns out the lobes.
The shoulder and the bore are agreed as a pair, as on any locating part. On an M3 joint the bore is often a small reamed hole or a bearing bore, and the shoulder tolerance is assessed against it rather than on its own.
The head height is the third dimension that has to be agreed, because it sets how much material is available for the recess. A shallow head with a deep recess leaves a thin section over the shoulder, and that section is what fails first under torque.
Four properties decide these M3 shoulder screws, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Torx recess | More torque before slipping | Requires the exact bit |
| Ground shoulder | A defined locating diameter | Bore match needed |
| Stainless, plain | Corrosion resistance, no film | Galling on stainless threads |
| Small head | Low profile in a small assembly | Little material for the recess |
The value is that the screw can be driven to its seat with a hand tool and a fixed bit, without the recess rounding out. On a small assembly that is the difference between a joint that is positioned and one that is merely tight.
The cost is that the bit has to be right. A Torx joint is more tolerant of torque and less tolerant of tooling, which is the opposite of a cross recess in a way that matters on a line where bits are changed often.
The recorded finish is plain stainless steel. On an M3 shoulder screw that keeps the shoulder at its ground diameter and the recess at its cut size, and it avoids a plate that would have to be kept out of a recess this small.
| Option | How it protects | Effect on shoulder and recess | Typical use |
|---|---|---|---|
| Plain, passivated | Passive film, no coating | No build; recess and shoulder as cut | Instruments and small assemblies |
| Passivated 303/304 | Cleaner passive layer | No build; free-machining option | Machined stainless parts |
| Nickel plated | Hard bright barrier | Thin build; recess re-gauged | Visible small fixings |
| Zinc plated, thin | Sacrificial zinc | Build measurable at this size | Cost-driven dry joints |
| Black oxide | Conversion film, oiled | No measurable build | Dark optical assemblies |
At this size a coating is a dimensional decision. A recess that takes a specific bit has no room for a layer that changes the lobe size, and a shoulder measured in hundredths of a millimetre cannot absorb a film without being re-checked.
Stainless against stainless can gall in the thread, which on a small screw shows as a joint that tightens and then seizes before the shoulder seats. Where the joint is assembled and left alone this is manageable; where it is taken apart, the drawing should say so.
Three assemblies where a small, positioned pivot is the requirement:
| Where it sits | The screw locates a small lever, a pointer arm or a carriage inside a frame where the position sets the reading. |
| When it goes wrong | The arm develops play, and the reading drifts without any part appearing broken. |
| Why it happens | The joint is small, the setting is fine, and the bore is a reamed hole. |
| What we control | Shoulder diameter and bore agreed as a pair; first article checked for play. |
| Where it sits | The screw is the pivot of a link or an arm in a compact mechanism that moves repeatedly. |
| When it goes wrong | The pivot loosens, and the link starts to rattle or lag. |
| Why it happens | The joint is small, moves often, and is assembled with a hand driver. |
| What we control | Seat checked under the stated torque; recess proved with the customer bit. |
| Where it sits | The screw aligns a plate or a stop in a fixture where the position repeats from part to part. |
| When it goes wrong | The plate shifts between builds and the fixture loses its setting. |
| Why it happens | The bore wears, or the shoulder is short of the plate thickness. |
| What we control | Shoulder length and diameter checked against the fixture plate. |
Four reasons that matter when the recess has to reach a shoulder seat, each tied to something the drawing or the first article proves. All four are visible in the sample, not only on a certificate.
|
Recess and head agreed together
The Torx size and the head height are stated together on the drawing, because on an M3 head one limits the other. Basis: Recess and head dimensioned. |
Ground, cut, then checked
The shoulder is ground, the recess cut to its size, and both checked on the first article before the batch runs. Basis: Shoulder and recess checked. |
|
Driven with your bit
The first article is driven with the bit the customer uses, so the recess is proved with the tool that will assemble it. Basis: Recess proved with the bit. |
Same seat and same recess
Shoulder limits and the recess size are recorded with the drawing revision, so a repeat batch seats the same way. Basis: Same limits across orders. |
These screws are turned from stainless bar in a single setup, with the shoulder turned and then ground, the head faced, the Torx recess cut, and the thread cut behind the shoulder; the parts are passivated and inspected. The first piece of every run is measured on shoulder diameter and roundness, shoulder length, head height, recess size and depth, and thread.


|

|
Cutting the six-lobe recess is the operation that sets how the part behaves in assembly. The tool has to cut six flanks to the right size and to a depth that leaves enough material over the shoulder; a recess that is cut deep to make the bit seat better thins the head, and a recess cut shallow stops the bit from reaching full engagement.
The head is faced before the recess is cut, so the recess is measured from a finished face. On a small head the face is also the bearing surface, so tool marks left by the recess cut are visible around the recess on a part that is seen.
Grinding the shoulder after the head and thread keeps the locating diameter on a part that is not disturbed afterwards. On a small diameter, the step between shoulder and thread has to be square, because that step sets where the part stops.
What decides whether M3 shoulder screws pass is the shoulder, the recess and the thread start. The inspection agreement covers those, and the criteria come from the drawing.

Shoulder and head on the projector |

Thread and start checked |

Material checked |

Salt-spray testing where plated |
The recess is checked with the matching bit on a sample from each batch, and for depth and lobe width on the projector. A recess that measures right but will not take the bit is usually a burr on a lobe rather than a size problem.
The shoulder is measured for diameter, roundness and length, and the step for squareness. The head is checked for diameter and height and for flatness of the face, since on a small head a dished face bears on its rim.
The thread start is checked for burrs, and a sample is assembled at the stated torque to confirm that the screw seats on the shoulder rather than stopping early on the thread.
Every batch of M3 shoulder screws is traceable to the bar it was made from and to the passivation lot that finished it. The grade and heat number appear on the material certificate supplied with the parts, and the dimensional results are recorded against the drawing revision.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing, including the shoulder and the recess, and the passivation report. The records carry the drawing revision and the batch number, so a repeat order of M3 shoulder screws seats at the same depth.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a small pivot the first article is fitted into the customer bore and driven with the customer bit, because the recess is only proved by the tool that assembles it. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the turning cell and the inspection bench can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
Because the head is small. A six-lobe recess leaves more wall between the drive features, so more torque reaches the thread before the bit slips.
It is the whole drive. A bit one size down turns out the lobes, and a worn bit does the same, so the bit is part of the assembly method.
Yes. Depth takes material from over the shoulder, and a head that is thin there fails before the thread does.
Only if the fit allows it. On a locating shoulder the plate is a film inside the fit, so plain stainless is the usual choice at this size.
Yes. The shoulder tolerance and the bore form the fit together, so both are needed to assess the part.
Shoulder diameter and tolerance, shoulder length, head diameter and height, Torx size, thread size and length, and the assembly torque.
How an M3 shoulder screw project runs from drawing to repeat delivery:
|
1
Send the drawing, the bore and the bit
|
→ |
2
Shoulder and recess agreed
|
→ |
3
First article fitted and driven
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the shoulder diameter and tolerance, shoulder length, head diameter and height, the Torx size, thread size and length, and the bore.
|
Shoulder diameter
|
Shoulder length
|
Head size
|
|
Torx size
|
Thread
|
Bore
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com