Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
Type:Ti Screw
Materials:Titanium
Surface treatment:Plain
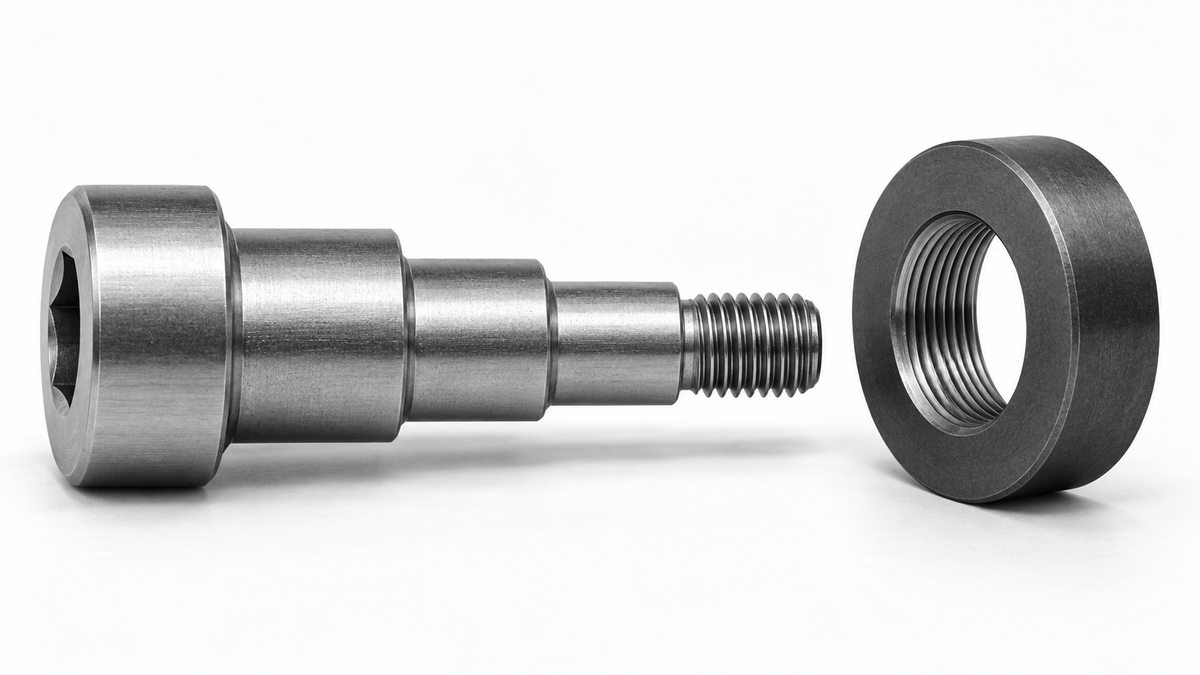
Head Type:Cap head, no recess
Drive:No head recess; assembly per drawing
Thread:Machine thread
Point:Plain, chamfered
Forming:CNC turning; thread cut
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
Number:189
We make titanium screws turned from titanium bar, in the grade the joint needs, with the head and shank to the drawing. Titanium buys weight, corrosion resistance without a coating and non-magnetic behaviour, and it charges for them with galling, so the lubricant and the assembly method are agreed first.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Titanium screws are machine screws turned from titanium bar, used where weight, corrosion resistance or magnetic behaviour matter more than cost. The part recorded here is titanium left plain, with a cap head that carries no drive recess, a stepped shank and a machine thread, quoted from M1 upward.
Titanium body. About half the weight of steel for a comparable strength, and no rust in ordinary conditions.
Cap head without a recess. A plain cylindrical head, so the assembly method comes from the shank or the nut rather than from the head.
Machine thread. A thread that goes into a tapped hole or a nut, with the joint defined by the pair.
They are used in lightweight mechanisms, marine and laboratory equipment, and anywhere a screw has to sit outside a magnetic field. Titanium screws are also chosen where a plated screw would fail visibly: a scratched plate on a steel screw rusts, while a titanium one simply shows a scratch.
Titanium is not simply a better screw material. It buys four specific things and it charges for them in ways that show up in manufacture rather than on a drawing. Knowing which of the four is being bought is what decides the grade and the process.
It buys weight. A titanium screw is roughly half the mass of a steel one of the same size, and on a mechanism that moves or is carried, that matters cumulatively: dozens of screws in a light assembly are a measurable share of the mass. It buys corrosion resistance without a coating, which means no plate to chip at an edge and no rust bloom where the screw meets a wet or washed surface. It buys a non-magnetic body, which matters next to a sensor, a compass or a magnetic drive. And in the commercially pure grades it buys compatibility with tissue and with food contact, which is why titanium fasteners appear in medical and food equipment.
The first cost is galling. Titanium seizes against titanium more readily than stainless does: the thread can pick up and weld at the contact, and the joint then stops turning before it reaches its preload. A lubricant, a coating or a controlled thread fit is not optional on a titanium-to-titanium joint, and the drawing usually has to state which.
The second cost is machining. Titanium conducts heat poorly, so the cutting edge stays hot, and it work hardens at the surface. Cutting speeds have to be low, tool life is short, and a small feature such as a thread start is easy to damage and hard to repair. That is why a titanium screw costs several times a steel one before the material price is considered.
The third cost is stiffness. Titanium has a lower modulus than steel, so a fine thread in titanium deflects more under the same load and the load is shared less evenly across the engaged turns. On a small titanium screw this shows as a joint that feels soft before it seats, and it is why the thread form and the engagement matter more than on a steel part.
The part is quoted to the drawing with the grade, the thread and the head stated separately. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation for titanium screws carries the grade, the thread and pitch, the head and shank, the length, and the mating part.
| Item | How it is defined | What we control |
|---|---|---|
| Grade | Commercially pure or alloy | Alloy and mechanical properties |
| Thread | Machine thread | Size, pitch and start |
| Head | Cap head, no recess | Diameter, height and face |
| Shank | Stepped or plain | Diameter and step position |
| Finish | Plain or anodised | Surface and colour |
| Mating part | Customer part | Thread depth and material |
On titanium screws the grade is the first decision. Commercially pure titanium is softer, very corrosion resistant and easy to form; the alloy grade is stronger and is used where the screw carries load. Two screws that look identical can be made from either, and only the certificate tells them apart.
The thread on titanium screws is cut rather than rolled, because rolling a small titanium thread tends to pick up and tear the crest. Cutting keeps the crest clean, at the cost of a thread that is slightly less strong in fatigue.
On titanium screws the head is specified with its assembly method. A cap head with no recess, as on the part recorded here, cannot be driven from above: the screw is turned from the shank, from a nut on the thread, or held while the mating part is turned. That is a drawing decision, not a workshop preference.
Four properties decide titanium screws, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Light body | Half the mass of a steel screw | Material cost several times higher |
| Corrosion resistance | No coating needed | Cost, and galling at the thread |
| Non-magnetic | Safe next to sensors and drives | Grade must be confirmed on the certificate |
| Plain head | No recess to trap dirt | Assembly must come from the shank or nut |
The value of titanium screws is that they do something a steel screw cannot: it removes weight, it survives without a coating, and it stays out of a magnetic field. Those are functional gains, and on the right application they justify the price.
The cost is in manufacture and assembly. Titanium is slow to cut, it seizes on itself, and a plain head commits the joint to a particular way of being assembled.
The recorded finish is plain titanium, cleaned. That is the natural surface of the material: it forms its own passive oxide layer and needs no coating for corrosion resistance, and the surface stays metallic rather than coloured.
| Option | How it protects | Effect on head and thread | Typical use |
|---|---|---|---|
| Plain, cleaned | Natural passive layer | Thread and head as turned | Mechanical and marine parts |
| Anodised, clear | Thicker oxide film | No measurable build | Wear at the head and thread |
| Anodised, coloured | Oxide film, coloured | No build; colour by voltage | Visible and identifier parts |
| Dry film lubricant | Low-friction film | Thin; reduces galling | Serviced titanium joints |
| Passivated | Cleaned passive layer | No build | Medical and food contact |
On titanium screws anodising is the finish that belongs to the material. It is an oxide grown on the surface rather than a coating added to it, so it does not build a dimension, and the colour comes from the film thickness. For a small screw that has to be identified by eye, a coloured anodised head is a practical marking method that does not rub off.
A lubricant on titanium screws is the treatment that addresses galling, and on titanium it is often more important than any cosmetic finish. It does not change the thread, and it is what allows the joint to reach its preload instead of seizing part way.
Three settings where weight, corrosion or magnetic behaviour decides the material:
| Where it sits | The screw is part of a mechanism that moves or is carried, where total mass matters more than unit cost. |
| When it goes wrong | The mass budget is exceeded, or the joint seizes during assembly. |
| Why it happens | A steel screw was used for strength, and the weight or the galling was not accounted for. |
| What we control | Grade and lubricant agreed; first article assembled and weighed against the drawing. |
| Where it sits | The screw sits in salt spray or immersion where plated steel would fail and stainless would pit. |
| When it goes wrong | The screw corrodes at a scratch, or the joint seizes after a season. |
| Why it happens | The grade is not suitable for chlorides, or the thread has no lubricant. |
| What we control | Grade confirmed on the certificate; first article exposed and inspected. |
| Where it sits | The screw sits next to a magnetic sensor or a drive where a steel part would disturb the field. |
| When it goes wrong | The reading drifts, or debris collects at the screw. |
| Why it happens | The screw is magnetic, and its position is close to the sensing element. |
| What we control | Grade and magnetic behaviour confirmed; first article assembled in the assembly. |
Four reasons that matter on titanium screws, which are bought for what they do not do, each tied to something the drawing or the first article proves. All four show in the sample and in the certificate that travels with it.
|
Grade and assembly stated
The drawing states the titanium grade and how the screw is assembled, because a plain cap head cannot be driven from above. Basis: Grade and method agreed. |
Cut thread, clean crest
The thread is cut rather than rolled, so a small titanium crest stays clean instead of tearing during forming. Basis: Thread crest controlled. |
|
Joint proved without seizing
The first article is assembled with the agreed lubricant, because titanium galling only shows once the thread is loaded. Basis: Seizing checked in assembly. |
Same grade on repeat runs
Grade, thread and finish are recorded with the drawing revision, so a repeat batch behaves the same in the joint. Basis: Same grade across orders. |
These screws are turned from titanium bar, with the head formed and faced, the shank stepped to the drawing and the thread cut; the parts are cleaned and inspected. The first piece of every run is measured on head diameter and height, shank diameters and step position, thread and length.


|

|
Titanium is turned at a lower surface speed than steel and with more coolant, because the heat of the cut has nowhere to go and the edge of the tool stays hot. The effect on a small screw is that the thread start and the head face are the features most likely to be damaged, and both are checked on the first piece rather than at the end of the run.
The head on this part has no recess, so it is faced and finished as a plain surface. That removes the recess operation but puts more weight on the head face: it is the surface that is seen and, in some assemblies, the surface that is gripped.
The thread is cut and then cleaned carefully, because a titanium thread with a burr at the start will seize in a stainless nut before it seats. The parts are packed clean, and where a lubricant is specified it is applied to the thread rather than to the head.
What decides whether titanium screws pass is the grade, the thread and the head. The inspection agreement covers those, and the criteria come from the drawing.

Head and shank on the projector |

Thread and start checked |

Material checked |

Salt-spray testing where a coating is used |
The grade is confirmed against the mill certificate for each heat, since no dimensional check can distinguish a commercially pure screw from an alloy one. Where the customer specifies magnetic behaviour, a sample from each batch is checked with a magnet.
On titanium screws the thread is gauged and the start inspected at magnification. On titanium the start is the feature that seizes first, and a burr there is a joint failure rather than a cosmetic defect.
The head and the stepped shank are measured on the projector, and a sample is assembled with the mating part using the agreed lubricant to confirm that the joint reaches its seat without galling.
Every batch of titanium screws is traceable to the bar it was made from. The grade, heat number and mechanical properties appear on the material certificate supplied with the parts, and the dimensional results are recorded against the drawing revision.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing, including the head and shank, and the finish record. The records carry the drawing revision and the batch number, so a repeat order of titanium screws is made from the same grade.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a titanium part the first article is assembled with the agreed lubricant, because galling is the failure that dimensions do not show. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Repeat orders of titanium screws are made from the same grade, because a substitute grade changes both the weight and the seizing behaviour. Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the turning cell and the inspection bench can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
Weight, corrosion without a coating, and non-magnetic behaviour. It costs several times more, so the application has to need one of those.
Commercially pure for corrosion and forming, the alloy grade for load. The drawing states which, and the certificate confirms it.
Galling. Titanium picks up against titanium and against stainless, so a lubricant or a controlled thread fit is needed.
From the shank, or by turning a nut on the thread. The assembly method is part of the drawing, not a workshop choice.
Yes, by anodising. The colour comes from the oxide thickness and adds no measurable build.
Grade, thread and pitch, head and shank, length, finish and lubricant, and the mating thread.
How a titanium screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the mating part
|
→ |
2
Grade, thread and assembly agreed
|
→ |
3
First article assembled without seizing
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the grade, thread and pitch, head and shank, length, finish and lubricant, and the mating thread.
|
Grade
|
Thread
|
Head and shank
|
|
Length
|
Finish
|
Lubricant
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com