Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
Type:Small Screws
Materials:Stainless Steel
Surface treatment:Plain
Head Type:Pan head
Drive:Phillips cross recess
Thread:Coarse self tapping thread
Point:Sharp self tapping point
Forming:Single-die cold heading; thread rolled
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
Number:411
We make small screws in stainless steel with a pan head, a Phillips recess and a sharp self tapping point, quoted from M1 upward. The head comes from one die, so a batch is consistent inside itself, and the head height is held in a narrow band so a row of fixings lines up.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Small screws are machine screws in the small end of the metric range, used where the assembly is smaller than a fingertip. The part recorded here is stainless steel left plain, with a pan head, a Phillips recess and a sharp self tapping point, quoted from M1 upward.
Small diameter. A thread of a millimetre or two, with a head only a few times that wide.
Pan head. A shallow dome with a flat bearing face and enough height for a full-depth cross.
Sharp self tapping point. A point that starts the thread in plastic or thin sheet rather than needing a tapped hole.
They are used in small housings, instruments and electronics, where several of them sit side by side on the same surface. Small screws in that position are judged as a group rather than one by one, which is why consistency matters as much as the individual tolerance.
Small screws are usually headed in a single die, which means the shape of the head on every part in a run comes from one tool. That is efficient, and it has a consequence that matters on small products: within a batch, the head is consistent because it comes from one die, but across batches the die wears and is replaced, and the difference between two runs shows.
On a large assembly nobody notices. On a small product with eight screws in a row along a panel, a few hundredths of a millimetre of head height difference between batches reads as a wavy line, and on a visible surface that is what the customer sees. The individual screws are all in tolerance; the product does not look consistent.
That is why the useful specification for small screws includes lot consistency, not just individual tolerance. The head diameter and height have to be held to a band that is narrower than the drawing tolerance would suggest, and the die condition has to be part of the process rather than something noticed after a complaint.
The point is the other end of the part. A sharp point starts its own thread in plastic or thin sheet, and its form decides how the screw enters: a point that is too blunt will not start, and one that is too sharp will skid across a hard surface before it bites. On a small screw the point is a proportionally large feature, so it is checked rather than assumed.
The result is that small screws are bought on consistency. The thread, the head and the point are all ordinary dimensions, but the batch-to-batch agreement is what makes a small product look finished.
The part is quoted to the drawing with the head, the recess and the point stated separately. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation for small screws carries the head diameter and height, the recess, the thread and point, the length, and the material it enters.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Pan head | Diameter, height and bearing face |
| Recess | Phillips | Depth and width |
| Thread | Coarse self tapping | Diameter, pitch and length |
| Point | Sharp self tapping | Form and concentricity |
| Batch | One die per run | Consistency and die condition |
| Material | Sheet or boss | Thickness and hardness |
On small screws the head height is the dimension that shows in a row. It is held in a narrow band so that consecutive parts on a panel line up, and it is checked on a sample from the start and the end of each run rather than once at the beginning.
The point is written by form rather than by angle alone, because it has to start the thread in the material specified. A point that suits a ductile plastic will skid on a hard one.
The recess and the head are agreed together: on a small pan head the cross has to be deep enough for the bit and shallow enough to leave a head that does not collapse.
Four properties decide small screws of this form, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Small size | Fits inside a small product | Batch variation shows on a visible row |
| Single-die heading | Consistent heads within a run | Die wear shows between runs |
| Sharp point | Starts its own thread | Form must suit the material |
| Stainless | No rust from handling | Galling on stainless threads |
The value of small screws is a fixing small enough to disappear into a product, made in runs that are consistent enough to look uniform along a panel.
On small screws the cost is that consistency has to be bought deliberately. The tolerance on the drawing describes one part; what the customer sees is a row of parts from the same batch, and that row is what the page is really about. The drawing tolerance is only the starting point; what the customer compares is the batch.
The recorded finish is plain stainless steel. On a small screw a coating is a large fraction of the features: it can fill a pan head’s cross and change a head height that is already being held in a narrow band.
| Option | How it protects | Effect on head and recess | Typical use |
|---|---|---|---|
| Plain, passivated | Passive film, no coating | Head and recess as made | Small housings and instruments |
| Passivated 316 | Higher alloy passive layer | No build; better in chlorides | Medical and marine |
| Dry film lubricant | Low-friction film | Thin; reduces galling | Serviced joints |
| Nickel plated | Hard bright barrier | Thin build; recess re-gauged | Visible hardware |
| Black oxide | Conversion film, oiled | No measurable build | Dark mechanisms |
On small screws where a coating is used, the head height is checked again after plating, because that is the dimension the row depends on. A plate that adds a few microns to every head is invisible on one part and visible on eight in a line.
Passivation is the finish that changes nothing dimensionally, which is why it is standard on small parts: the delivered batch and the recorded drawing describe the same geometry.
Three products where several small fixings appear together:
| Where it sits | The screws close a cover and sit in a row along an edge that is seen. |
| When it goes wrong | The heads are not level, or one sits proud of the others. |
| Why it happens | Batch variation in head height, or a burr on one head. |
| What we control | Head height checked across the batch; first article assembled along the row. |
| Where it sits | The screws hold plates and sub-assemblies inside a compact frame. |
| When it goes wrong | The plate sits at an angle, or a screw does not reach its seat. |
| Why it happens | The point does not start in the material, and the screw is forced. |
| What we control | Point and thread agreed with the material; first article driven into the real part. |
| Where it sits | The screws are part of a product that is handled and seen at close range. |
| When it goes wrong | The finish marks, or the recess wears during service. |
| Why it happens | The head is at the limit of its recess depth, and the bit is not matched. |
| What we control | Recess proved with the bit; first article cycled in the product. |
Four reasons that matter on small screws, where the batch is judged as a row, each tied to something the drawing or the first article proves. All four show in the sample.
|
Head height specified as a band
The drawing states the head height in a narrow band, because that is what makes a row of fixings look level. Basis: Height band agreed. |
One die, checked at both ends
A run is headed in one die and the head checked at the start and the end, so die wear is caught inside the batch. Basis: Die condition monitored. |
|
Joint proved on the part
The first article is driven into the customer material, because the point and the recess only prove themselves there. Basis: Joint proved in the part. |
Same head across orders
Head limits, die and plate are recorded with the drawing revision, so a repeat order lines up with the first. Basis: Same head across orders. |
These screws are cold headed from stainless wire in a single die, with the pan head formed, the point formed, the cross recess cut and the thread rolled; the parts are cleaned, passivated and inspected. The first piece and the last piece of every run are measured on head diameter and height, recess, point form and thread.


|

|
The head comes from the die, so its height and diameter are a property of the tool rather than of a later operation. That is what makes a batch consistent, and it is also where consistency is lost: a die that is worn produces heads at the edge of the band, and the next run after replacement produces heads at the other edge.
The point is formed in the same operation as the head, and its concentricity with the thread is what lets the screw start where it is aimed. On a small screw a point that is off-centre will wander in a small boss, and the thread that follows is then off-axis.
The parts are passivated after the last operation, and the head height is checked again on the plated sample. Where a run follows a die change, the first article is compared with the previous batch, because a step between batches is what the customer notices.
What decides whether small screws pass is the head, the recess and the point. The inspection agreement covers those, and the criteria come from the drawing.

Head and point on the projector |

Thread gauged |

Material checked |

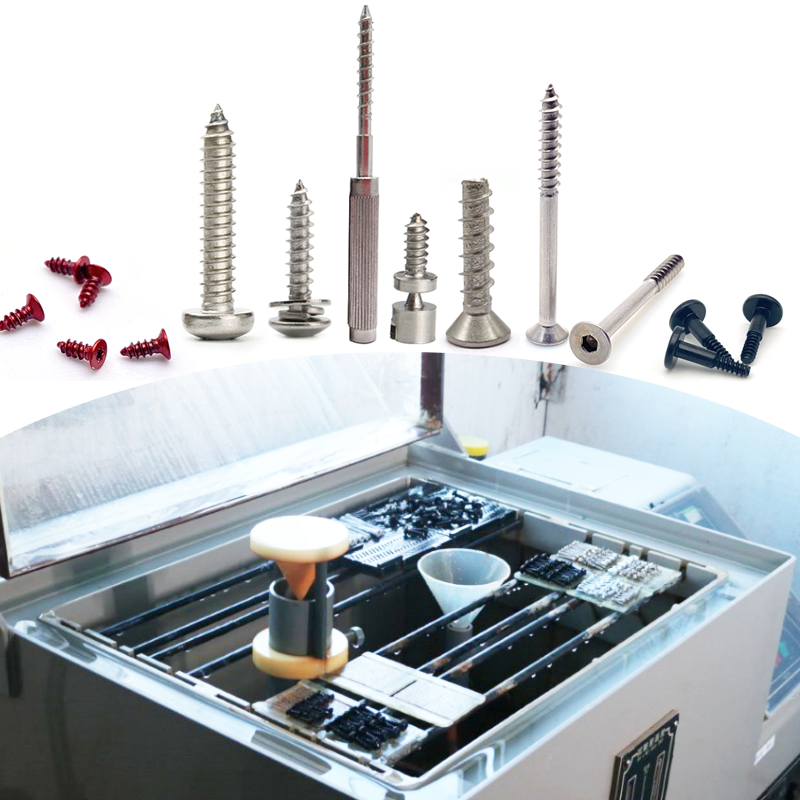
Salt-spray testing where plated |
The head is measured at the start and the end of the run, and the two results are compared as well as checked against the drawing. A batch that drifts from one end to the other passes each individual check and still looks uneven on a panel.
The point is checked for form and for concentricity with the thread. A point that is off-centre is the defect that shows up as a screw that will not start in a small boss.
The recess is checked with the matching bit, and a sample is driven into the customer material to confirm that the point starts and the thread holds. That test is the one that matches how the part is used.
Every batch of small screws is traceable to the wire it was made from and to the passivation lot that finished it. The grade and heat number appear on the material certificate supplied with the parts, and the dimensional results are recorded against the drawing revision.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing, including the head and point, and the passivation record. The records carry the drawing revision and the batch number, so a repeat order of small screws lines up with the first.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a small part the first article is assembled in the customer’s own row, because the eye compares parts rather than measuring them. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Repeat orders of small screws are compared with the first article as a row, not one at a time, because that is how the customer sees them. Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the heading cell and the passivation line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
The head comes from a die. Within a run the head is consistent, and between runs die wear or replacement changes it slightly.
On a small product with several screws in a row, yes. The eye compares heads, and a small step reads as an uneven panel.
A narrow band on head height and diameter, and a note that consecutive batches must match the first article.
So the screw starts its own thread. The form has to suit the material, or the point skids instead of biting.
It can. A plate that adds to every head is invisible on one part and visible on eight in a line, so the head is checked after plating.
Head diameter and height, recess, thread and point form, length, grade, and the material and thickness it enters.
How a small screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the material
|
→ |
2
Head, point and thread agreed
|
→ |
3
First article assembled in the row
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the head diameter and height, recess, thread and point form, length, grade, and the material and thickness it enters.
|
Head diameter
|
Head height
|
Recess
|
|
Thread
|
Point
|
Material
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com