Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
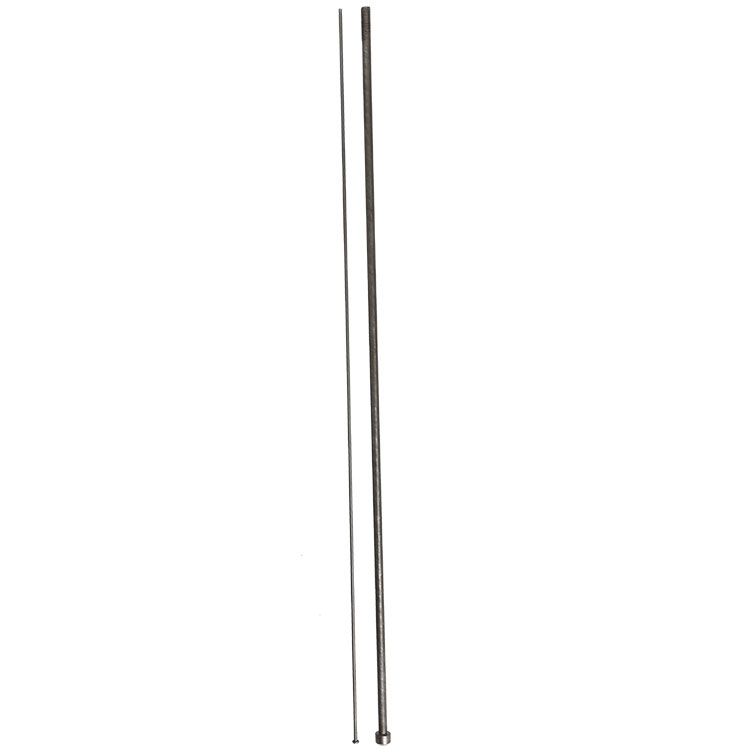
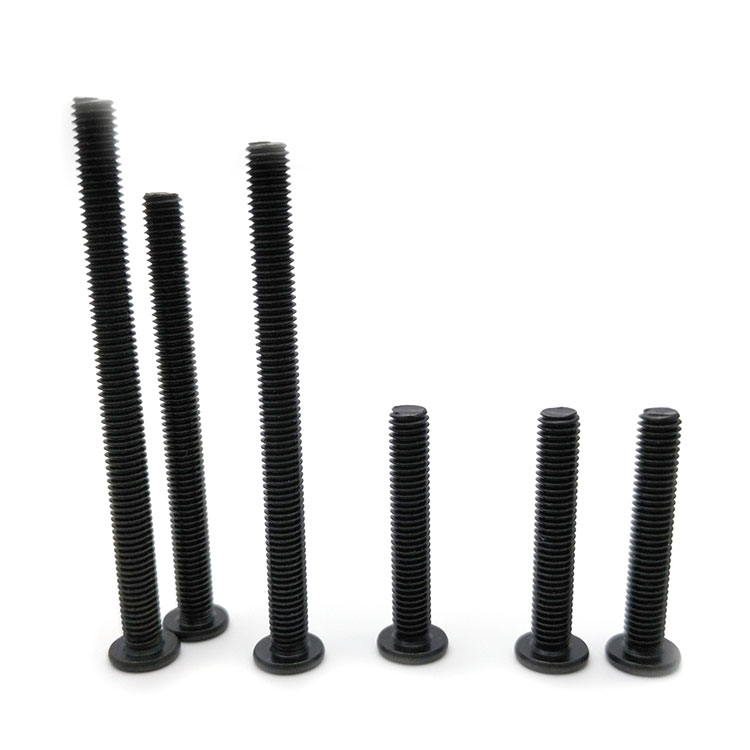
Type:Really Long Screws
Materials:Stainless Steel
Surface treatment:Plain
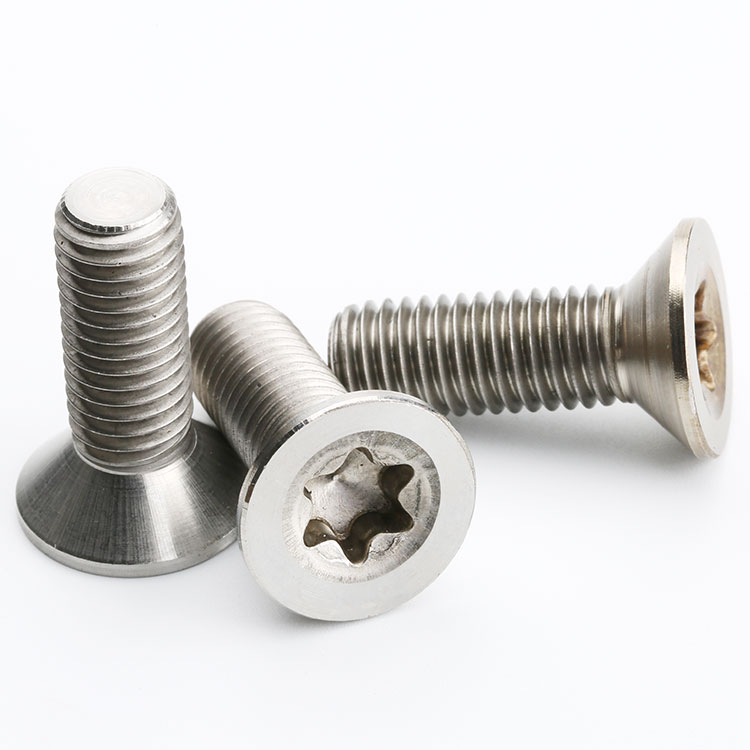
Head Type:Flat (countersunk) socket cap
Drive:Hexagon socket (Allen)
Thread:Machine thread, partial
Point:Plain, chamfered
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
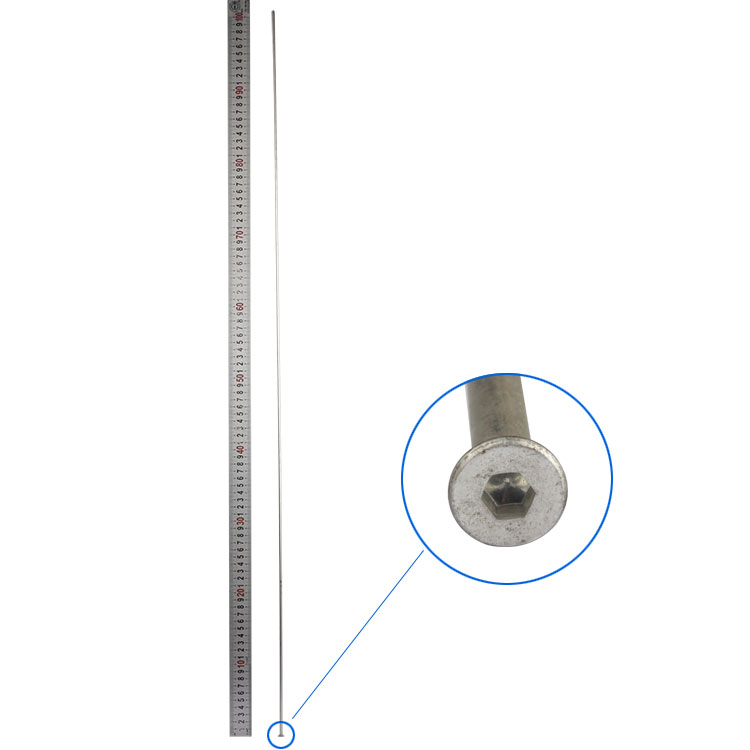
We make really long screws with a flat countersunk head and a hexagon socket, in stainless steel, quoted with lengths made to the drawing. The cone angle, head height and socket depth are agreed with the length, and the first article is fitted into your stack.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
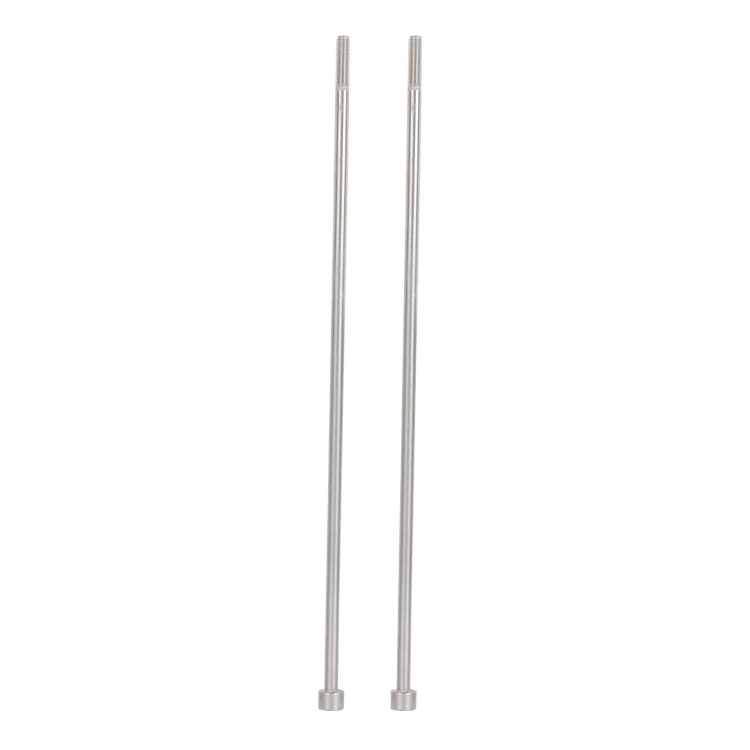
Really long screws with a flat head are countersunk socket screws made in lengths that span several components, so the head finishes flush in the top member while the shank passes through everything below. The part recorded here is stainless steel, plain finish, quoted with lengths made to the drawing.
Long length. The shank crosses a stack of parts before the thread engages.
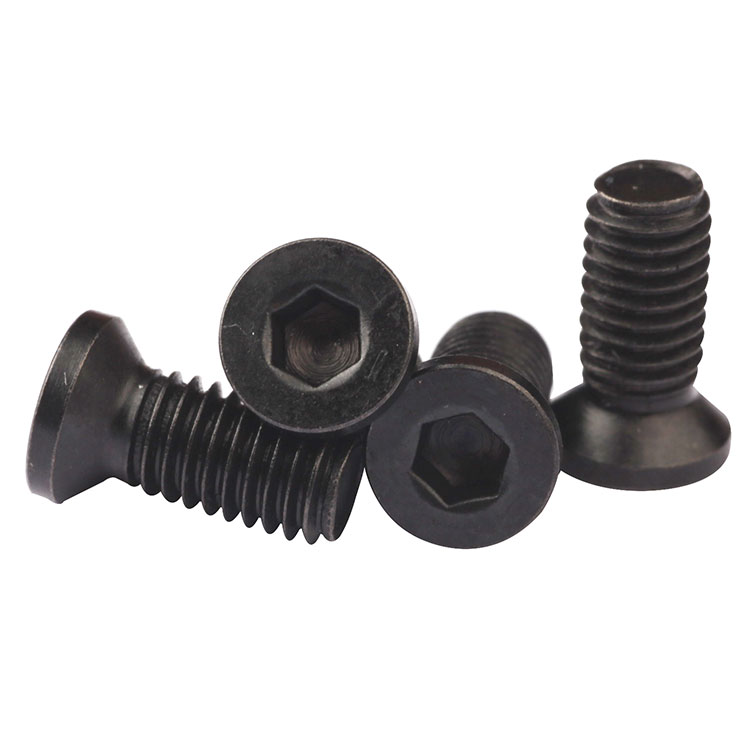
Flat head. A 90 degree cone that seats in a countersink cut into the top member only, leaving nothing above the surface.
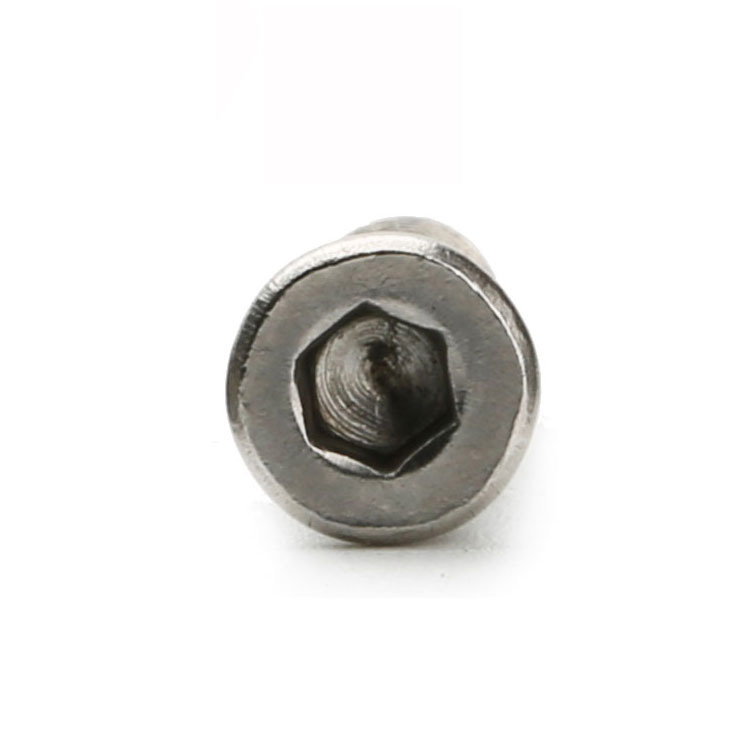
Hexagon socket. A socket in the small disc above the cone, driven with a key that has to reach its floor.
Stainless, plain. No coating, so the cone seats metal on metal and the thread stays as rolled in a deep hole.
They are used on machine beds, slide plates, die plates and instrument frames where a long fixing has to be flush with a working surface and pass through a stack behind it.
A cap head can afford a deep socket because its height is solid metal. A flat head cannot: the cone takes most of the height, and what remains is a thin disc with a socket cut into it. Put that head on a long screw and you have a part where the drive is the smallest feature and the friction is the longest.
That combination is what makes really long screws with flat heads awkward to drive. The thread runs a long way through the stack, so every turn adds friction and the key is being asked to transmit torque over a long distance of thread with a short engagement in the head. The socket is not the limit because the screw is weak; it is the limit because it has the least material to work with.
On really long screws with flat heads the countersink adds a second constraint. The cone has to be cut into the top member, and only the top member: the parts below it are clearance holes. A seat that is cut too deep leaves the head below the surface, and a seat that is not cut at all leaves the head standing on the panel.
On really long screws the shank then has to be guided. Over a long run through several components, the clearance holes decide whether the screw reaches the thread in line or binds halfway. That is a stack-dimension issue rather than a screw-dimension one, and on a flush fixing it decides whether the key can still turn the screw at the point where it seats.
Stainless is the practical choice on these lengths because the thread is buried. A coating that wears inside a deep hole cannot be inspected or repaired, while a plain stainless thread keeps its surface and does not rust into the tapped hole behind the stack.
The recorded product covers the long range, with lengths made to the drawing. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation for really long screws carries the overall length, the countersink angle, the head diameter and height, the socket size and depth, the threaded length and the thread itself.
| Item | How it is defined | What we control |
|---|---|---|
| Overall length | Under the head to the point | Length to the drawing |
| Cone | Countersink angle, usually 90 degrees | Angle and depth |
| Head height | Top face to the cone top | Height and face flatness |
| Socket | Hexagon per diameter | Depth and floor thickness |
| Threaded length | Thread from the point upward | Where the thread ends |
| Stack | Clearance holes in the members | Aligned with the thread |
The cone depth is measured against the top member rather than against the screw, because that is where the seat is cut. A head that is correct in the drawing sits wrong if the seat in the panel was cut shallow, and the fixing will be judged on the seat.
Socket depth is the number that gets left out and always matters. On a flat head it is bounded by the head height, and on a long screw the key has to reach that floor while the thread is already loaded, so a socket that is a fraction shallow is discovered in the middle of the drive rather than at the start.
Threaded length and overall length are stated separately. A long flush screw is usually partially threaded: the plain shank crosses the clearance holes and the thread engages only in the last member, which is the arrangement that keeps the clamp on the shank rather than on threads in mid span.
Four properties decide really long screws with flat heads, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Long length | Spans a stack of parts | Friction accumulates along the thread |
| Flat head | A surface with nothing standing up | Shallow socket in a thin disc |
| Partial thread | Plain shank across the holes | Boundary must be specified |
| Stainless body | No coating buried in the stack | Lower strength than a graded steel part |
The value of really long screws with flat heads is a joint that is both flush and far reaching. Where a working surface has to stay clear and the fixing has to pass through several plates to reach its thread, this is the combination that does it with one part.
The cost is that the drive is small and the friction is long. That is a joint that has to be designed around the key, the seat and the alignment rather than around the thread alone.
The recorded finish is plain stainless. On a fixing whose thread ends up several components deep, that is the finish that can be specified without a site visit: nothing is deposited or added, and the thread keeps the geometry it was rolled to.
| Option | How it protects | Effect on cone and socket | Typical use |
|---|---|---|---|
| Passivated, plain | Removes free iron; rebuilds oxide | No build; cone and socket as cut | Default for stainless |
| Electropolished | Levels the surface | Socket edges rounded; cone brightened | Food and medical beds |
| Black oxide on stainless | Colours the surface | Thin film; seat unchanged | Dark machine beds |
| Nickel plated | Hard barrier deposit | Build in socket and thread; gauged after | Visible dry assemblies |
| Zinc plated steel equivalent | Sacrificial zinc | Build on thread; friction rises with length | Where stainless is not needed |
A plated finish on a long threaded section is felt as extra friction over every turn, which is precisely what a flush head has least capacity to overcome. That is the practical reason these parts are often specified in plain stainless rather than in a coated steel.
Where colour matters, black oxide on stainless changes almost nothing dimensionally and keeps the parts dark, which is usually a better answer than a deposit on a shallow socket.
Three settings where a flush fixing has to reach through a stack:
| Where it sits | The screw holds a wear plate flush to a bed through a spacer and the bed itself. |
| When it goes wrong | The head sits below the surface because the seat was cut too deep, and the plate rocks. |
| Why it happens | The surface is machined, the stack is deep, and the joint is dismantled. |
| What we control | Cone angle and seat agreed; first article fitted and checked for flatness. |
| Where it sits | The screw pulls a plate down through a stack where the top face has to stay clear for the workpiece. |
| When it goes wrong | The key cannot reach the socket floor once the thread is loaded and the drive marks. |
| Why it happens | The head is shallow, the thread is long, and the joint is repeated. |
| What we control | Socket depth and key proved; first article driven with the production key. |
| Where it sits | The screw fixes a component flushed into a frame where nothing may protrude into the optical path. |
| When it goes wrong | A proud head shifts the component and the measurement changes. |
| Why it happens | The surface is precision, the stack is thin, and the fixing is small. |
| What we control | Head height and cone checked; first article fits in the customer frame. |
Four reasons that matter on a part where the drive is small and the run is long, each tied to something the drawing or the first article has to prove:
|
Cone and socket stated with the length
The countersink angle, head height and socket depth are agreed alongside the length, because on a flush long screw those three decide whether the head seats and whether the key can drive it. Basis: Cone and socket stated. |
Headed, broached, threaded and passivated
The cone and head are formed in one stroke, the socket broached, the thread rolled over the agreed length and the batch passivated. Basis: One route, socket kept to depth. |
|
Socket proved with your key
The socket is driven with the production key at the joint torque, because a shallow socket is discovered halfway through a long thread rather than at the start. Basis: Key proved at joint torque. |
Same seat, same drive
The heading punch, broaching depth and thread boundary are recorded with the drawing revision, so a repeat order seats and drives the same. Basis: Same fit across orders. |
These screws are headed on single-die machines that form the cone and the top face, broached with a hexagonal punch, thread rolled over the agreed length and passivated. The first part of every run is measured on head diameter, cone angle, head height, socket size and depth, overall length, threaded length and thread.


|

|
Forming the cone while leaving a disc for the socket is the first balance, and it is harder on a long part because the blank is longer to handle at the press. A punch set a little deep leaves the top face too thin to hold the hexagon; set shallow, the head stands taller than the drawing and will not finish flush.
Broaching follows on really long screws, and the depth is set against the head height. On a flat head the floor under the socket is the feature that fails first, and on a long screw that failure arrives when the thread is already engaged and the operator has no way to back out.
Rolling the thread over a long length on really long screws sets the boundary between shank and thread, which is what puts the plain section across the clearance holes. Handling between steps stays in trays, since a long part that has been dropped will not start straight in a deep stack.
What decides whether really long screws pass is the cone, the head height, the socket, the thread and the boundary between shank and thread. The inspection agreement covers those, and the criteria come from the drawing.

Cone and socket on the projector |

Thread and start checked |

Hardness against the stainless spec |

Salt-spray testing of the plain surface |
Cone angle, head diameter and head height are measured as one set, and the socket depth is read against them. The threaded length is measured from the point, so the boundary is recorded as a value rather than inferred from the overall length.
The socket is proved with the production key at the torque the joint calls for, and the floor is inspected under magnification afterwards. That check happens on a sample that has already been screwed into a test stack, because the drive only loads the socket once the thread is engaged.
A sample from every batch is fitted into the customer stack and checked for the head finishing flush and for the shank reaching the thread without binding. That is the check that turns the dimensions into a joint.
Every batch is traceable to the heat of stainless it was made from. The grade and heat number appear on the material certificate supplied with the parts, and the inspection record carries the measured head, socket and thread boundary against the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing including the socket depth and thread boundary, and the passivation records for the batch. The documents carry the drawing revision and the batch number, so a repeat order of really long screws seats and drives the same way.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a flush long screw the first article is fitted into the customer stack and driven with the production key. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the broaching station can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
The cone takes most of the head height, so the socket is cut into a thin disc. The key then has to reach that floor while a long thread is already loaded.
In the top member only. Everything below is a clearance hole, and a seat cut too deep leaves the head below the surface.
Usually the seat: a shallow or wrong-angle countersink, or a burr at the hole edge. The screw is rarely the cause.
Usually not. A partial thread leaves a plain shank across the clearance holes, which is what keeps the clamp on the shank.
The thread is buried several components deep, where a coating failure cannot be inspected or repaired.
Overall length, cone angle, head height, socket size and depth, threaded length and the thread specification.
How a flush long screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the stack
|
→ |
2
Cone, socket and boundary agreed
|
→ |
3
First article fitted in your stack
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the overall length, countersink angle, head height, socket size and depth, threaded length and thread specification.
|
Overall length
|
Cone angle
|
Head height
|
|
Socket size
|
Threaded length
|
Thread
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com