Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
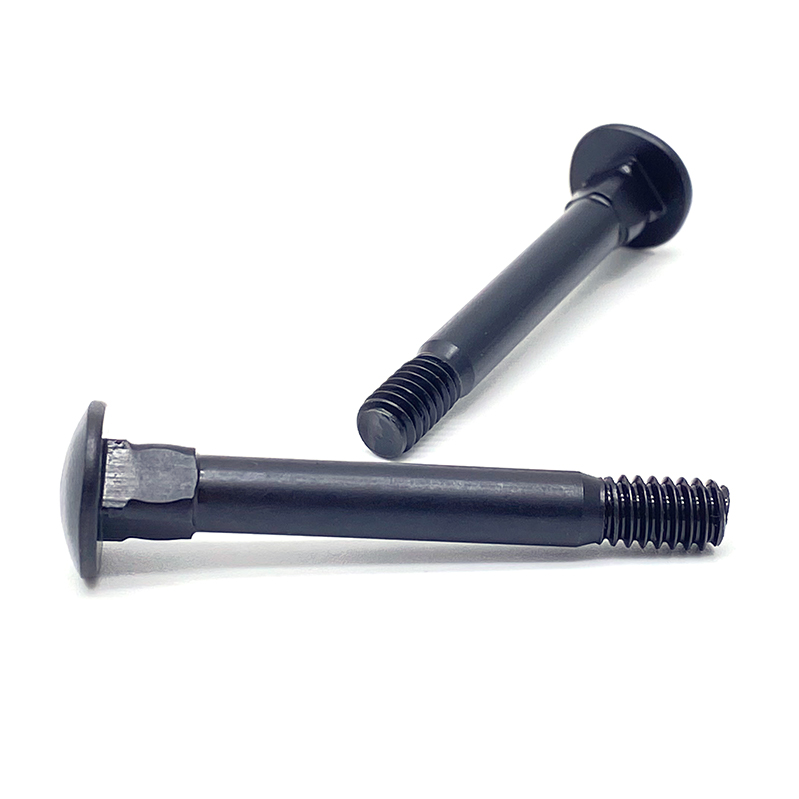
Type:Ultra Low Profile Shoulder Screw
Materials:Stainless Steel
Surface treatment:Plain
Head Type:Ultra low profile with shoulder
Drive:Phillips cross recess
Thread:Machine thread, partial
Point:Plain, chamfered
Forming:CNC turning and grinding
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
We make ultra low profile shoulder screws in stainless steel with a cross recess, quoting the shoulder diameter and length to the drawing. The head height and recess depth are agreed with your driver, and the first article is fitted in your bore and driven with it.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
An ultra low profile shoulder screw has a head reduced to almost the height of the shoulder, a precision shoulder that locates the part, and a small cross recess in what remains of the head. The part recorded here is stainless steel with a plain finish, quoted with the shoulder dimensions made to the drawing.
Ultra low head. A head so shallow that a plate can pass over the fixing with almost no clearance at all.
Shoulder. A ground diameter between the head and a smaller thread, acting as the locating or bearing surface.
Cross recess. A drive cut into the few tenths of a millimetre left above the shoulder.
Stainless, plain. No coating on the shoulder, and no film inside a recess that has no depth to spare.
They are used where a mechanism closes down onto its fixings: thin phone and laptop assemblies, sliding covers, folding frames and any joint where a conventional head would be too tall to be covered.
Every head form trades height for drive. A cap head spends height on a socket, a button head spends it on a dome, and an ultra low head spends almost all of it on being low. What remains above the shoulder is a thin disc, and a cross recess needs depth to hold a bit: the arms have to be deep enough that the bit reaches the floor and wide enough that they do not collapse.
On ultra low profile shoulder screws those two requirements meet at their limits. The recess is cut as deep as the disc allows, and the result is a drive that works at hand torque and not much more. That is not a defect in the part; it is the consequence of the head height, and it is why these screws are specified where the shoulder does the locating work and the head only has to hold the assembly together.
The shoulder carries the load. Because the head is shallow, the bearing face is small and the clamp it can spread is limited, so the joint is designed with the shoulder in the bore taking the load and the head preventing separation. A low head asking for a high clamp is a design that will mark its recess before it seats.
Stainless belongs here for two reasons. The shoulder is a bearing surface, and a plain finish keeps the ground diameter as it was made; and the recess is too shallow to survive a coating that changes which bit seats. A plated ultra low head is a part whose drive and fit both drift with the film.
What the customer has to accept is the torque. These are not parts to be tightened with a powered driver. The bit has to match, the recess has to be proved at the intended torque, and the assembly has to be done by someone who can feel the head seat rather than by a clutch setting.
The recorded part is quoted to the drawing, with the shoulder diameter and length stated separately from the thread. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation for ultra low profile shoulder screws carries the shoulder diameter and tolerance, the shoulder length, the head diameter and reduced height, the recess size and depth, and the thread.
| Item | How it is defined | What we control |
|---|---|---|
| Shoulder diameter | Ground diameter through the bore | Diameter, roundness and finish |
| Shoulder length | From the head underside | Length and squareness |
| Head | Ultra low profile | Diameter and minimal height |
| Recess | Cross, matched to the driver | Depth and floor thickness |
| Thread | Smaller thread behind the shoulder | Size, length and start |
| Finish | Plain stainless | No build in the recess |
The recess is the feature to agree first, because it is the one with no margin. Its size follows the diameter and the driver, and its depth is bounded by the head height, so the two numbers are set together with the customer’s tool in mind.
Head height is stated as a value rather than as a name. “Ultra low” covers a range, and two suppliers can deliver parts that both qualify and differ in how much recess they can carry, which is exactly the difference that matters here.
The shoulder fit is agreed against the bore. On a part whose head cannot clamp hard, the shoulder has to locate without play, because there is no reserve of clamp to hold a loose joint together.
Four properties decide ultra low profile shoulder screws, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Ultra low head | Almost no height above the surface | Very shallow recess; hand torque only |
| Ground shoulder | A defined locating diameter | Turned and ground part |
| Cross recess | A driver that fits a small tool | Arms at the limit of the head height |
| Stainless body | No coating in the recess | Lower strength than a graded steel part |
The value is clearance. Where a cover closes to within a tenth of a millimetre of the fixing, nothing else fits, and the ultra low head is the part that makes the assembly possible.
The cost is the drive. There is no reserve of head material, so the recess works at the limit and the assembly has to respect that.
The trade is a head low enough to disappear and thin enough to limit the recess depth.
The recorded finish is plain. On an ultra low head that is the only finish that leaves the recess as cut, and the recess is the feature with the least margin on the whole part.
| Option | How it protects | Effect on shoulder and recess | Typical use |
|---|---|---|---|
| Passivated, plain | Removes free iron; rebuilds oxide | No build; recess as cut | Default for stainless |
| Electropolished | Levels the surface | Recess edges rounded; fit changes | Clean equipment |
| Black oxide on stainless | Colours the surface | Thin film; recess fit kept | Dark assemblies |
| Nickel plated | Hard barrier deposit | Build in recess; re-gauged | Where a bright finish is wanted |
| Zinc plated steel | Sacrificial zinc | Build in recess; drive changes | Where stainless is not needed |
Where a coating is used, the recess is gauged after plating and proved with the driver. A film that would be invisible in a cap head is decisive in a head this shallow, and the failure shows as a bit that will not reach the floor.
Black oxide on stainless is the practical way to get a dark ultra low head: it changes almost nothing dimensionally and keeps the drive usable, which a deposit does not.
Three settings where clearance above the fixing is measured in tenths:
| Where it sits | The screw locates a plate inside a housing where a cover closes down onto the fixings. |
| When it goes wrong | A standard head holds the cover off and the assembly does not close. |
| Why it happens | The stack is thin, the parts are small, and the joint is adjusted. |
| What we control | Head height and recess proved; first article assembled with the cover. |
| Where it sits | The screw is the pivot of a part that folds flat where the head would otherwise foul. |
| When it goes wrong | A taller head catches the folding part and the mechanism stiffens. |
| Why it happens | The part moves, the clearance is minimal, and the joint is serviced. |
| What we control | Shoulder fit and head height checked; first article cycled. |
| Where it sits | The screw fixes a cover that must sit flat with nothing standing above the surface. |
| When it goes wrong | The head marks the cover from underneath, or the cover will not sit flush. |
| Why it happens | The panel is visible, the clearance is tight, and the joint is opened. |
| What we control | Head height and bearing face checked; first article fitted under the cover. |
Four reasons that matter on a part where the head has no reserve, each tied to something the drawing or the first article has to prove:
|
Height and recess agreed as one pair
The ultra low head height and the recess depth are agreed together with the driver, because the recess is cut out of the head height and there is no material in reserve. Basis: Height and recess agreed together. |
Turned, ground and recessed in one setup
The shoulder, head and recess are machined in one setup, so the recess sits on the same axis as the shoulder and the part locates without play. Basis: One setup, one axis. |
|
Recess proved with your driver
The recess is driven with the driver the customer uses at the intended torque, because a recess that is a fraction shallow cannot be recovered on this head. Basis: Driver proved on the part. |
Same fit across orders
The grinding setting and the recess tool are recorded with the drawing revision, so a repeat order locates and drives the same way. Basis: Same fit across orders. |
These screws are turned from stainless bar, with the shoulder, the ultra low head and the recess machined in one setup, the shoulder ground to its diameter and the thread cut behind it; the parts are then passivated. The first piece of every run is measured on shoulder diameter and roundness, shoulder length, head diameter and height, recess size and depth, and thread.


|

|
On an ultra low head the recess is the operation that decides the part. The cutting depth is measured against a head height of a few tenths, so a tool that is a fraction off either leaves a floor too thin to carry the drive or a recess too shallow for the bit. Both are checked on the first piece, and neither is visible from the outside of the finished screw.
Machining the recess in the same setup as the shoulder keeps the two on one axis, which is what lets the part locate without play. A second operation would introduce a runout that shows as a joint that binds at one point of each revolution.
Passivation follows and reaches the recess. On a disc this thin the recess floor is the surface that holds contamination after cutting, so the batch is checked inside it rather than only on the face.
What decides whether ultra low profile shoulder screws pass is the head height, the recess, the shoulder and the thread. The inspection agreement covers those, and the criteria come from the drawing.

Height and recess on the projector |

Thread and start checked |

Hardness against the stainless spec |

Salt-spray testing of the recess |
Head height and recess depth are read together, because on this part one defines the other. The shoulder is measured for diameter and roundness and its length is taken from the head underside, and the recess is proved with the production driver at the intended torque.
The functional check is a drive into the customer assembly and a removal. On a head this shallow the cycle shows a recess that accepts a bit but cannot transmit the torque, which no dimensional check alone reveals.
A sample from every batch is fitted into the customer bore to confirm the shoulder locates without play. On a part whose head cannot clamp hard, that fit is what holds the joint.
Every batch is traceable to the heat of stainless it was made from. The grade and heat number appear on the material certificate supplied with the parts, and the inspection record carries the measured head height, recess and shoulder against the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record with measured values, and the passivation records for the batch. The documents carry the drawing revision and the batch number, so a repeat order of ultra low profile shoulder screws locates and drives the same way.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On an ultra low head the first article is driven with the customer’s driver and fitted in the bore. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the turning cell and the inspection bench can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
The head is reduced almost to the height of the shoulder, so there is a thin disc left for the cross. The recess is cut as deep as that disc allows.
By hand, with a driver that reaches the floor of the recess. It is not a part for a powered driver at a clutch setting.
The shoulder in the bore, with the head preventing separation. The head is too small to develop a high clamp on its own.
Only by removing the drive. Below a certain height there is no room for a cross, and the part would have to be turned by hand or driven by a knurl.
Yes. A film that is invisible in a cap head fills this recess, so plated parts are gauged and proved with the driver.
Shoulder diameter and tolerance, shoulder length, head diameter and height, recess size and depth, thread and the driver used.
How an ultra low shoulder screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the driver
|
→ |
2
Head height and recess agreed
|
→ |
3
First article fitted and driven
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the shoulder diameter and tolerance, shoulder length, head diameter and height, recess size and depth, thread and the driver used.
|
Shoulder diameter
|
Shoulder length
|
Head height
|
|
Recess size
|
Thread
|
Driver
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com