Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
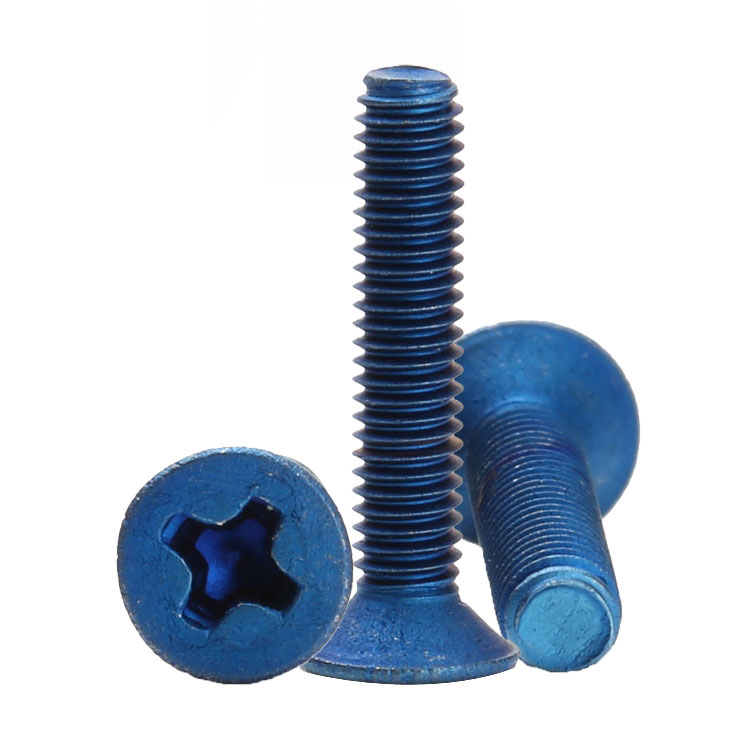
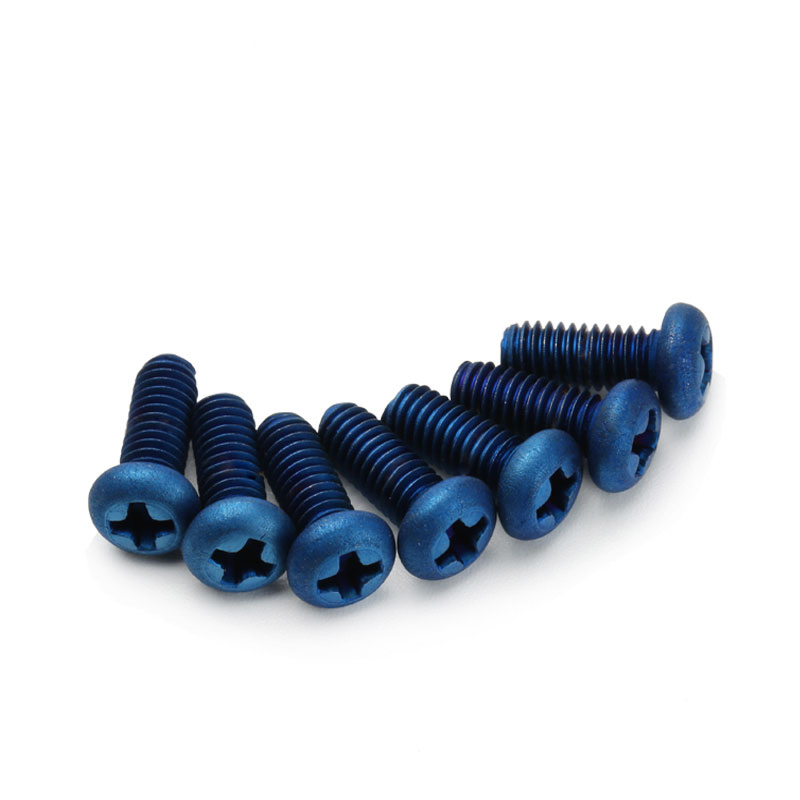
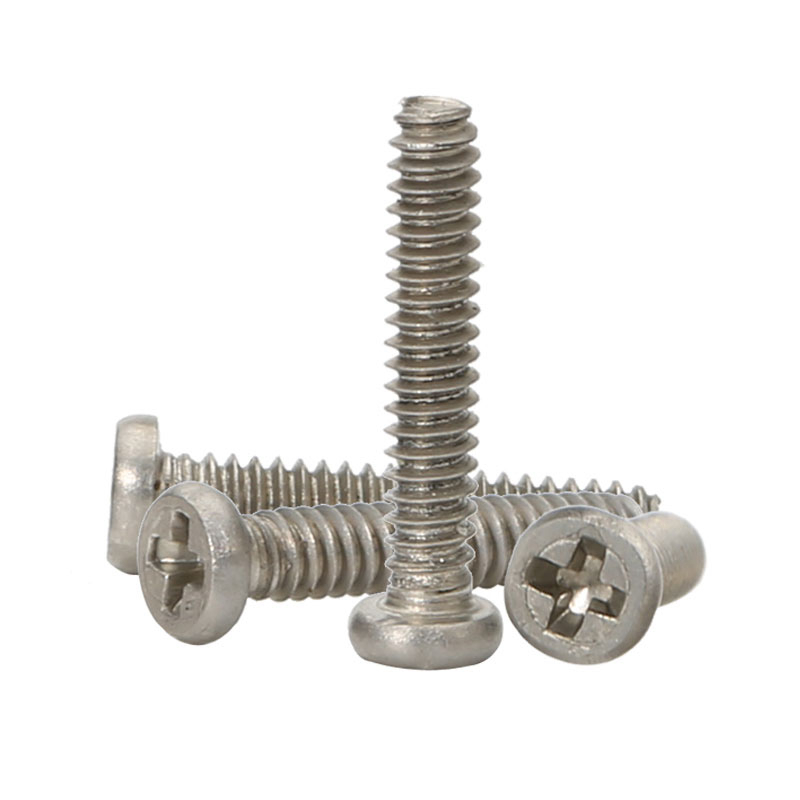
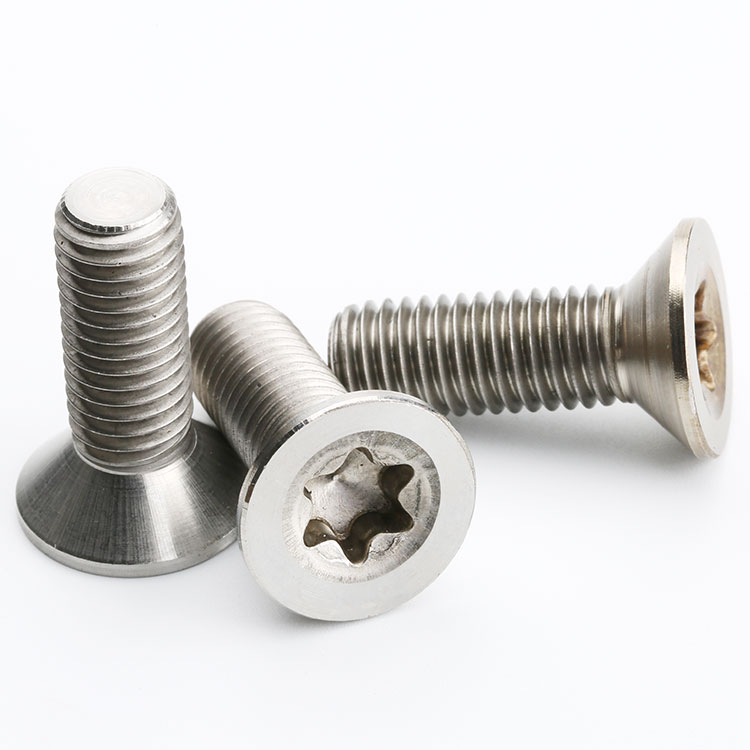
Type:Phillips Flat Head Countersunk Screw
Materials:Titanium
Surface treatment:Anodized
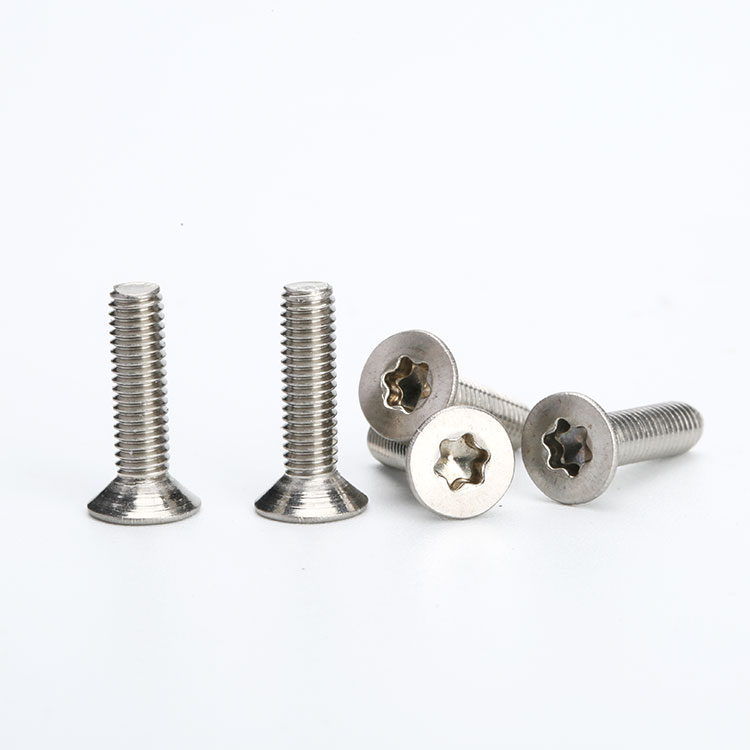
Head Type:Flat (countersunk)
Drive:Phillips cross recess
Thread:Machine thread
Point:Plain, chamfered
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
We make titanium flat head screws with a Phillips cross recess and an anodised finish, quoting them from M1 to M10 with lengths made to the drawing. The recess depth is agreed with your bit and measured after anodising, and the first article is driven before the batch runs.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
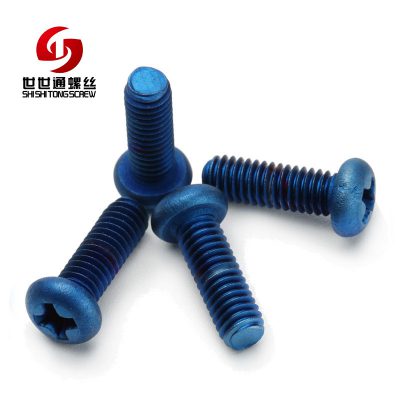
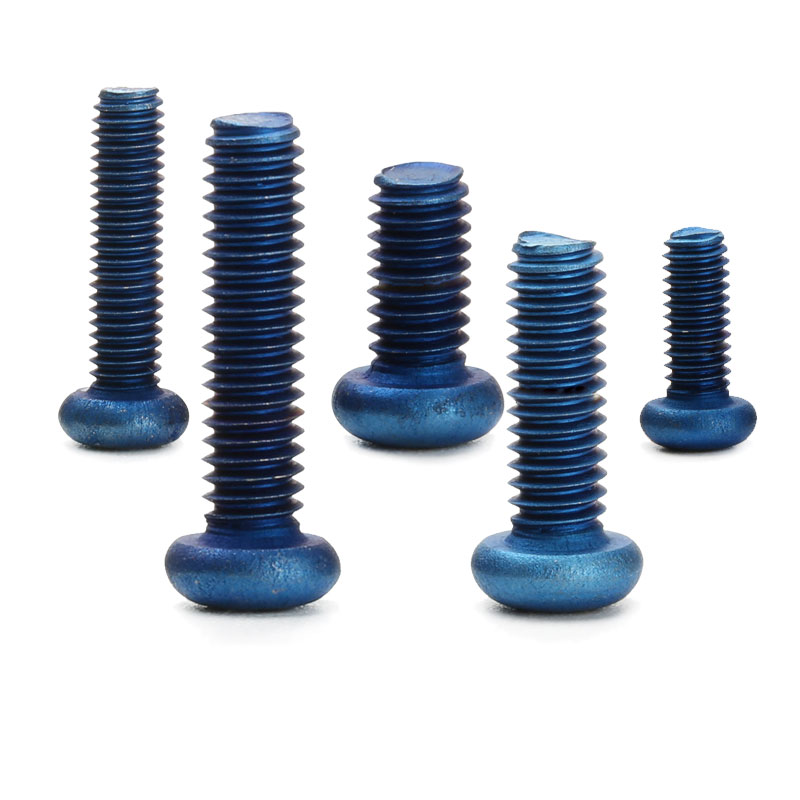
Titanium flat head screws are countersunk machine screws made in titanium, with a cone that seats flush and a drive in the top face. The part recorded here has a Phillips cross recess and an anodised finish, quoted from M1 to M10 with lengths made to the drawing.
Flat head. A 90 degree cone that seats in the countersink so the head finishes level with the surface.
Phillips recess. Four tapered arms in a head that has very little height to give, because the cone has taken most of it.
Titanium body. Light and corrosion resistant, but soft against its own oxide and quick to gall when the drive is poor.
Anodised finish. A grown oxide layer that colours the part and hardens its surface without changing the head geometry.
They are used on drones and model airframes, sports hardware, marine fittings and lightweight instruments, wherever a flush fixing is needed in a material chosen for its weight.
Each element of this part takes something away from the drive. The cone uses the head height that a socket or a Phillips recess would otherwise occupy. The Phillips recess spreads the torque over four relatively thin arms. And titanium works against the driver twice: it galls when the bit rubs, and it work-hardens at the contact, so a recess that slips once does not recover.
The result is that the drive, not the thread, is the limit. On a steel screw of the same geometry the arms wear gradually and the joint survives many assemblies; in titanium the same arms can take a set on the first slip, and after that the bit no longer seats and the clamp the thread could deliver becomes irrelevant.
Anodising helps at the surface and not in the geometry. The oxide is harder than the metal under it, so the arms resist a slipping bit a little better, but the layer grows in place rather than adding height, and the recess depth, arm width and floor thickness are unchanged. The torque the joint can take is still set by the shape of the drive.
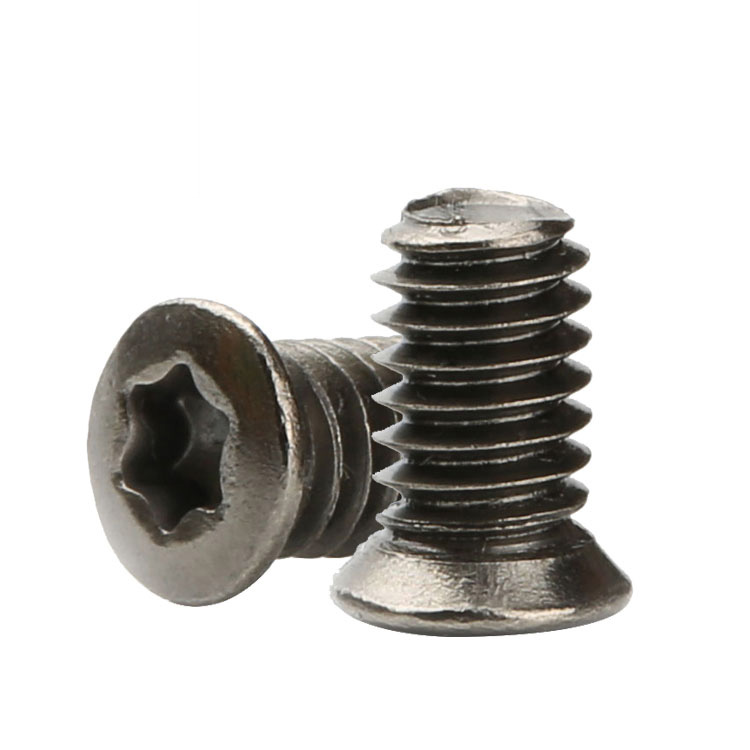
That is why the same part is often specified with a star drive instead. A Torx recess in the same head presents six flanks with a much larger contact area, drives on the flanks rather than the arm tips, and does not lift the bit out under torque. Where the customer’s tooling allows it, that is the change that makes a flush titanium joint practical.
What the Phillips recess keeps is availability. The bit is in every toolkit, the recess self-centres, and a flush head with a cross can be serviced anywhere. On a part where weight and appearance matter more than torque capacity, that trade is often the right one, provided the torque is set low enough to respect the arms.
The recorded range is M1 to M10, with lengths made to the drawing. Custom lengths up to 2,000 mm are subject to the drawing submission and DFM review. The quotation for titanium flat head screws carries the titanium grade, the head diameter, the countersink angle, the head height, the PH size and recess depth, the anodising colour and the thread.
| Item | How it is defined | What we control |
|---|---|---|
| Alloy | Titanium grade per the drawing | Grade stated on the certificate |
| Cone | Countersink angle, usually 90 degrees | Angle and concentricity |
| Head height | Top face to the cone top | Height and face flatness |
| Recess | Phillips, PH size per diameter | Depth, arm width and floor |
| Finish | Anodised, colour | Colour against a retained sample |
| Thread | Machine thread in titanium | Pitch, length and start position |
Head height and recess depth are one pair on this part. The cone consumes most of the head, so the recess sits in a thin disc, and a head that is a fraction low has lost a visible part of the depth the bit needs.
The countersink angle belongs on the mating drawing as well. A 90 degree head in an 82 degree seat bears on the rim and stands proud, and on a flush titanium joint that also misloads the drive.
The anodising colour is specified by reference rather than by name, because the colour comes from an oxide thickness and a name covers a range. Two batches can both be “blue” and sit a shade apart.
Four properties decide titanium flat head screws, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Titanium body | About half the weight of steel | Galls easily; lower stiffness |
| Flush cone | Nothing above the surface | Head height spent on the cone |
| Phillips recess | A bit in every toolkit | Thin arms in a soft metal |
| Anodised finish | Colour and a harder surface | Colour varies between runs |
The value is a flush fixing in a material that saves weight and does not corrode. On an airframe or a marine fitting, the alternative is either heavier or plated, and neither is acceptable.
The cost is the drive. The joint has to be designed around a lower torque than the thread could take, and the assembly has to be controlled rather than judged by feel.
Those properties are what decide whether the part suits a visible joint or a hidden one.
The recorded finish is anodised. On titanium the oxide grows out of the metal, so there is no film edge to lift, no flaking, and no build in the recess that would change which bit seats.
| Option | What it does | Effect on cone and recess | Typical use |
|---|---|---|---|
| Anodised | Grown oxide, coloured | Micrometres thick; geometry unchanged | Visible hardware |
| Plain, as formed | Native oxide only | No build | Where colour is irrelevant |
| Polished | Mechanical smoothing | Recess edges softened | Bright visible heads |
| Bead blasted | Matte surface | Matte inside the recess | Equipment and enclosures |
| Dry film lubricant | Anti-galling layer | Thin, even film | Joints assembled more than once |
A lubricant is often specified alongside anodising on these parts. The harder surface resists wear, but it does not stop the metal from galling against a mating titanium part, and on a joint that is opened more than once that is the difference between a screw that comes out and one that strips.
Where colour matters, a retained sample per anodising lot is the only practical control. The colour is a measurement of oxide thickness, and the judgement is made against a physical reference.
Three settings where a flush head and light weight are both required:
| Where it sits | The screw closes a frame where the head must not catch on a surface and mass affects flight time. |
| When it goes wrong | A magnetic or heavier screw is substituted and either the weight or the sensor behaviour changes. |
| Why it happens | The frame is light, the joint is small, and the fixing is repeated. |
| What we control | Grade and colour confirmed; first article assembled and checked for interference. |
| Where it sits | The screw holds a component where the joint is visible, the surface is handled, and the finish is part of the product. |
| When it goes wrong | An anodised batch differs in colour and the mismatch shows across the component. |
| Why it happens | The part is visible, the fixings are numerous, and the assembly is inspected. |
| What we control | Colour sample per lot; first article fitted on the finished component. |
| Where it sits | The screw fixes hardware where salt water would attack a steel part within a season. |
| When it goes wrong | A coated screw breaks down at the recess and corrosion starts where the bit bears. |
| Why it happens | The joint is wet, the fixing is flush, and the appearance matters. |
| What we control | Salt-spray sample checked; first article fitted on the fixture. |
Four reasons that matter on a drive with less margin than the tool, each tied to something the drawing or the first article has to prove:
|
Recess depth agreed with the bit
The recess size and depth are agreed against the driver the customer uses, because a flush titanium head has no height to spare and a shallow recess is marked on the first turn. Basis: Recess matched to your bit. |
Headed, recessed, threaded, anodised
The cone and top face are formed in one stroke, the cross cut, the thread rolled and the batch anodised so the geometry is unchanged by the finish. Basis: One route, geometry kept. |
|
Height and recess measured after finishing
Head height and recess depth are measured after anodising on the first article, because that is the state the bit meets and the state the customer sees. Basis: Measured after anodising. |
Same colour, same drive
The anodising lot and the recess tool are recorded with the drawing revision, so a repeat order matches in colour and in drive. Basis: Colour and drive held. |
These screws are headed on single-die machines that form the cone and the flat top in one stroke, cut with the cross recess, thread rolled on the titanium and anodised as a batch. The first part of every run is measured on head diameter, cone angle, head height, recess size and depth, thread and length, with the measurement repeated after anodising.


|

|
Forming the cone while leaving a disc for the recess is the balance. The metal flows out into the cone and up into a thin top face, and titanium resists that flow more than steel, so the punch does more work and wears faster. A worn punch leaves a top face slightly thicker and a cone slightly under diameter, which looks acceptable and seats badly.
Cutting the cross into titanium is where the part is decided. Titanium shear-cuts less cleanly than brass or steel, so a dull punch tears the arm corners rather than shearing them, and the damage is inside the recess where it cannot be seen until the part is driven. The punch interval is kept in the tooling record and the recess is checked on the first part after any change.
Anodising finishes the batch and is checked against the retained colour sample. Because the oxide grows in place, the dimensions measured after anodising should match those measured before it, and any difference is a process problem rather than a coating thickness.
What decides whether titanium flat head screws pass is the cone, the recess, the thread and the colour. The inspection agreement covers those, and the criteria come from the drawing and the retained sample.

Cone and recess after anodising |

Thread and start checked |

Hardness against the titanium grade |

Salt-spray testing of the anodised surface |
Cone angle, head diameter and head height are measured as one set on the projector, then the recess depth is read against them. The recess is proved with the production bit at the torque the joint calls for, because a recess that measures correctly can still fail if the arm corners were torn.
Colour is checked against the retained sample under the same light, since the interference colour shifts with viewing angle. A spot check in different conditions proves nothing, and the check is recorded with the batch.
A sample from every batch is seated in a countersunk plate of the agreed angle and driven once, then removed. That cycle shows a cone that does not match, a head that stands proud, or a recess that has begun to mark.
Every batch is traceable to the titanium bar or wire it was made from. The grade and heat number appear on the material certificate supplied with the parts, and the anodising lot is recorded against the colour sample.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing including the recess depth, and the anodising record with the colour sample reference. The documents carry the drawing revision and the batch number, so a repeat order of titanium flat head screws matches in colour and in drive.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On an anodised flush head the first article is compared with the customer sample and driven with their bit. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers, the recess station and the anodising line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
The cone uses most of the head height, so the recess is cut into a thin disc. On titanium that leaves very little margin at the arm corners.
Where the tooling allows, yes. A star drive has more contact area and does not lift the bit, which is why it is common on flush titanium parts.
It hardens the surface a little, but it does not change the geometry, so the torque is still set by the recess shape.
Titanium seizes against itself and many metals when dry. An assembly lubricant or a defined procedure is agreed with the drawing.
Only in a countersink of the same angle and depth. A 90 degree head in an 82 degree seat bears on the rim and stands proud.
The titanium grade, head diameter, countersink angle, head height, PH size and recess depth, anodising colour and thread.
How a titanium flush screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the colour sample
|
→ |
2
Recess depth and cone agreed
|
→ |
3
First article driven with your bit
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the titanium grade, head diameter, countersink angle, head height, PH size, anodising colour and thread.
|
Titanium grade
|
Cone angle
|
Head height
|
|
PH size
|
Anodising colour
|
Thread
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com