Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
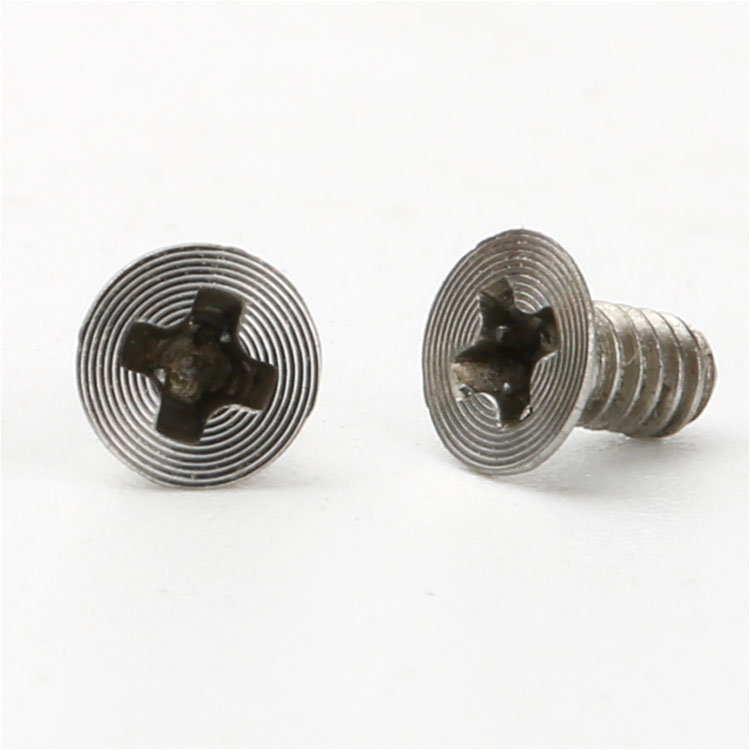
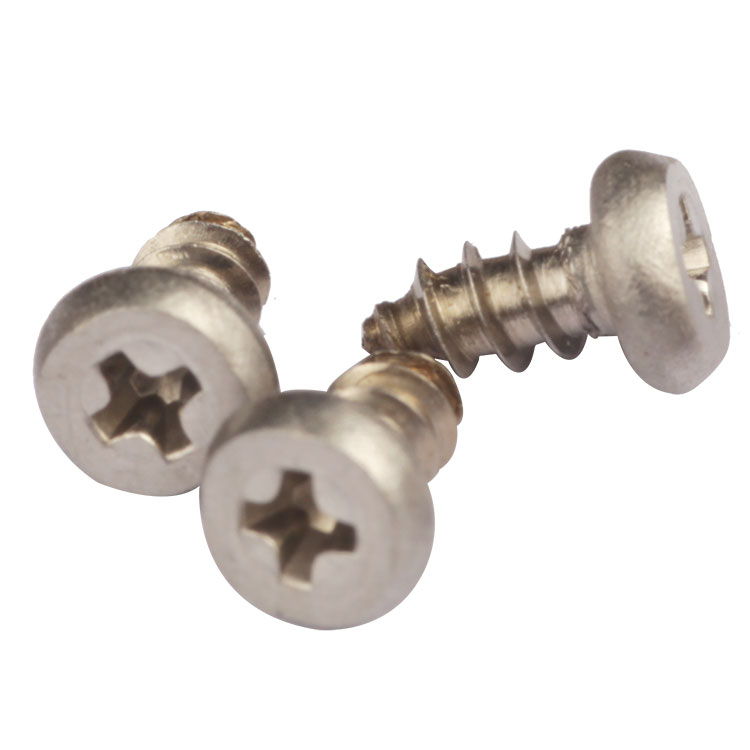
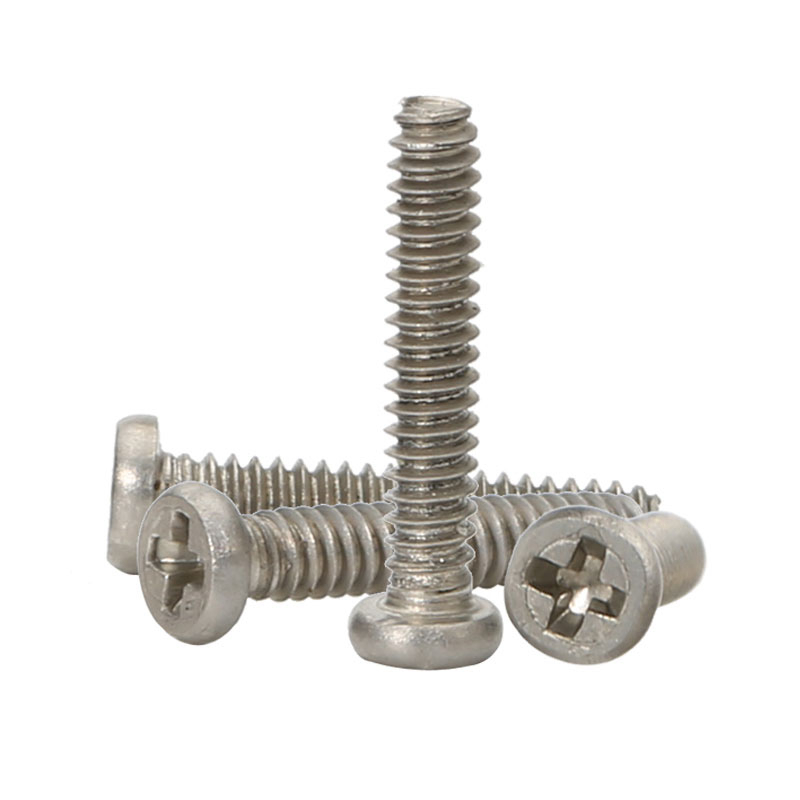
Type:Micro Self Tapping Screws
Materials:Stainless Steel
Surface treatment:Plain
Head Type:Pan head
Drive:Phillips cross recess
Thread:Coarse self tapping thread
Point:Pointed, per drawing
Forming:Cold heading and thread rolling
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
We make micro self tapping screws in stainless steel with a pan head and Phillips recess, quoting the thread, recess and length to the drawing. At this size the bit and the pickup decide the joint, so the recess and the thread start are controlled and the first article is assembled with your driver.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Micro self tapping screws are screws small enough that the handling matters as much as the thread, typically in the M1 to M2 range, with a coarse thread and a small head. The part recorded here is stainless steel left plain, with a pan head and a Phillips recess, quoted from M1 upward.
Micro size. A thread diameter of a millimetre or two, where a few hundredths of a millimetre is a working tolerance.
Self tapping thread. A coarse thread that forms its own thread in a plastic or light alloy boss.
Pan head with a cross. A small bearing face and a recess sized to the smallest standard bit.
They are used in wearables, hearing instruments, camera modules and other products where the whole assembly is smaller than a fingernail. What they have in common is a plastic or light alloy boss and no room for an insert, so the screw has to make its own thread in a wall that is itself only a millimetre or two thick.
On a 6 mm screw, the limits are mechanical: how much torque the recess takes, how much clamp the head spreads. On micro self tapping screws the limits move. At a millimetre of thread diameter the crest is a few hundredths of a millimetre high, the recess may be a third of a millimetre deep, and the head can be narrower than the driver tip that turns it. What decides whether the part works is no longer strength; it is whether it can be held, aligned and seated without damage.
The first consequence is the driver. A bit at this scale cannot afford runout: a tip that is a little off-centre climbs out of the cross before the screw has started, and the recess is too small to survive that. The driver is therefore part of the process, not an accessory, and the bit is checked for wear far more often than on a larger screw.
The second is retention. A screw this size cannot be pushed into place with a finger; it has to be held on the bit, usually by a magnetic tip or by a vacuum pickup, and the same holding method that places it also has to release it once it is engaged. That is a design constraint on the head: a very shallow recess holds badly on a magnetic bit and releases badly from a vacuum nozzle.
The third is tolerance stacking at the hole. A micro screw entering a boss has perhaps a tenth of a millimetre of alignment to spare, and the thread start is what guides it in. A start that is slightly ragged will catch on the boss rim, tilt, and form a thread that is off-axis, and at this size the result is a stripped joint that cannot be repaired.
The fourth is that the part disappears. A dropped micro screw is not retrievable in a normal workshop, and a screw that is not seated looks exactly like one that is until the assembly is tested. That is why micro self tapping screws are usually specified with a fixed torque and a defined bit, and why the first article is assembled rather than measured in isolation.
The part is quoted to the drawing with the thread, the head and the boss stated separately. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation for micro self tapping screws carries the diameter and pitch, the point, the head and recess, the length under the head, and the boss hole and wall.
| Item | How it is defined | What we control |
|---|---|---|
| Thread | Coarse self tapping | Diameter, pitch, start and point |
| Head | Pan head | Diameter, height and bearing face |
| Recess | Smallest standard Phillips | Depth, width and edge |
| Boss | In the customer part | Agreed hole and wall |
| Driver | Bit in the assembly | Stated with the part |
| Torque | Assembly torque | Fixed, not by feel |
The recess is the dimension that constrains everything else. It has to be deep enough for the bit to engage, wide enough for the bit to fit, and shallow enough to leave a head that does not collapse; on a pan head of this size there is very little room between those three.
The thread start is treated as a controlled feature rather than a by-product of the roll. It is checked for a clean lead-in, because the start is what finds the boss and what decides the axis.
The boss hole and wall are agreed with the customer. At this size the hole is often a moulded feature a fraction of a millimetre in tolerance, and the screw has to suit the hole that can actually be moulded rather than the one that suits the drawing.
Four properties decide micro self tapping screws, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Micro size | Fits inside a tiny assembly | Hard to hold, align and inspect |
| Self tapping thread | No insert or tapped hole | Boss must be moulded precisely |
| Pan head | A small flat bearing face | Little room for the recess |
| Stainless | No rust from handling | Soft under a worn bit |
The value is that a whole joint exists at all. A tapped insert cannot be made this small and a nut cannot be placed, so a screw that forms its own thread is the only fixing that fits the space.
The cost is process instead of part. The driver, the pickup and the torque become part of the specification, and a supplier that only ships screws leaves half the problem with the customer.
The recorded finish is plain stainless steel. At this size a coating is a large fraction of the features it sits on: a zinc layer can fill a recess that is a third of a millimetre deep and change a thread whose pitch is a quarter of a millimetre.
| Option | How it protects | Effect on head and thread | Typical use |
|---|---|---|---|
| Plain, passivated | Passive film, no coating | Recess and thread as formed | Micro assemblies |
| Passivated 316 | Higher alloy passive layer | No build; better in chlorides | Medical and marine |
| Nickel plated | Hard bright barrier | Thin build; recess re-gauged | Visible decorative parts |
| Zinc plated | Sacrificial zinc | Can fill a shallow recess | Avoid on micro parts |
| Black oxide | Conversion film, oiled | No measurable build | Dark optical assemblies |
Where a coating is unavoidable, the recess is the first feature to check after plating. A cross that is a third of a millimetre deep has no room for a layer that adds a tenth of that to both walls and the floor.
Passivation is the finish that changes nothing dimensionally and does the most for handling, which is why it is the default on parts this small.
Three products where the fixing is smaller than the tool that places it:
| Where it sits | The screw closes a case or holds a module inside a housing a few millimetres thick. |
| When it goes wrong | The screw is lost during assembly, or the recess is destroyed by a worn bit. |
| Why it happens | The part is too small to handle, and the driver is not controlled. |
| What we control | Recess and start checked; first article assembled with the customer bit. |
| Where it sits | The screw holds a faceplate or a small bracket where nothing may stand above the surface. |
| When it goes wrong | The head catches on a finger or a case, or the thread strips in the plastic shell. |
| Why it happens | The head is taller than the clearance, and the boss is thin. |
| What we control | Head height and thread matched to the shell; first article closed and opened. |
| Where it sits | The screw locates a small board or a lens carrier where a fraction of a millimetre changes the focus. |
| When it goes wrong | The module shifts, and the image is out of adjustment. |
| Why it happens | The screw is not seated, or the bore in the module is worn. |
| What we control | Seat and head checked; first article assembled in the module. |
Four reasons that matter when the part is smaller than the process around it, each tied to something the drawing or the first article proves. All four show in the sample.
|
Bit and torque asked for
The quotation asks which bit and which torque the assembly uses, because at this size the driver decides whether the recess survives. Basis: Bit and torque agreed. |
Start and recess controlled
The thread start and the recess are made as controlled features, so the screw finds its boss and takes the bit squarely. Basis: Start and recess controlled. |
|
Assembled, not only measured
The first article is assembled with the customer driver rather than only gauged, because the failure mode appears in handling. Basis: Assembled in the check. |
Same feel on repeat runs
Recess size, thread start and material are recorded with the drawing revision, so a repeat batch handles the same way. Basis: Same handling across orders. |
These screws are cold headed from stainless wire, with the pan head formed, the point formed, the thread rolled and the recess cut; the parts are cleaned, passivated and inspected. The first piece of every run is measured on head diameter and height, recess depth and width, thread diameter and pitch, start form and point.


|

|
Cutting the recess is the operation that limits the part. The cutter has to be smaller than the finished cross and stiff enough not to deflect, and the depth has to leave a head that will not collapse under the bit. On a pan head this small, a few hundredths of a millimetre too deep is a head that fails on the first tightening.
The thread start is formed with the roll rather than left to break from the blank. A clean lead-in is what lets the screw find a boss hole that is barely larger than the thread, and a torn start at this size will not straighten itself in the hole.
Handling after the last operation matters as much as the operations themselves. Micro parts are counted and packed in a way that the customer can pick them, and parts that are dropped or mixed are not recovered; that is why the packing is part of the specification on parts this small.
What decides whether micro self tapping screws pass is the recess, the thread start and the head. The inspection agreement covers those, and the criteria come from the drawing.

Recess and head on the projector |

Thread gauged |

Material checked |

Salt-spray testing where plated |
The recess is checked with the matching bit on a sample from each batch and measured for depth and width on the projector. At this size a recess that measures correct but does not hold the bit is usually a burr on one wall, and the burr is found by trying the bit rather than by measuring.
The thread start is inspected at magnification, because a torn lead-in is a fraction of a millimetre and does not show at normal size. The point is checked for form and for damage in handling.
The head is checked for diameter and height and for flatness of the bearing face. On a pan head this small the face is what stops the screw, and a dished face leaves the joint tight at the rim and loose in between.
Every batch of micro self tapping screws is traceable to the wire it was made from and to the passivation lot that finished it. The grade and heat number appear on the material certificate supplied with the parts, and the dimensional results are recorded against the drawing revision.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing, including the recess and the thread start, and the passivation record. The records carry the drawing revision and the batch number, so a repeat order of micro self tapping screws handles the same way.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a micro part the first article is assembled with the customer’s driver and pickup, because handling is where the failure shows. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the heading cell and the recess cutting can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
Down to a millimetre of thread diameter, and the limit is usually the recess rather than the thread.
At this size the recess is a fraction of a millimetre deep, so a worn or off-centre bit destroys it before the screw starts.
Usually on a magnetic tip or by vacuum, which is why the head form and the recess depth are chosen with the pickup in mind.
Yes, and that is the usual joint. The boss hole and wall are agreed with the screw, because the hole has to be mouldable.
A coating can fill a shallow recess. Passivation changes nothing dimensionally and protects the surface.
Diameter and pitch, point, head and recess, length under the head, material and finish, and the boss hole and wall.
How a micro self tapping screw project runs from drawing to repeat delivery:
|
1
Send the drawing, the boss and the bit
|
→ |
2
Thread, recess and length agreed
|
→ |
3
First article assembled with your driver
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the diameter and pitch, point type, head and recess, length under the head, material and finish, and the boss hole and wall.
|
Diameter
|
Pitch
|
Point
|
|
Head and recess
|
Length
|
Boss hole
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com