Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
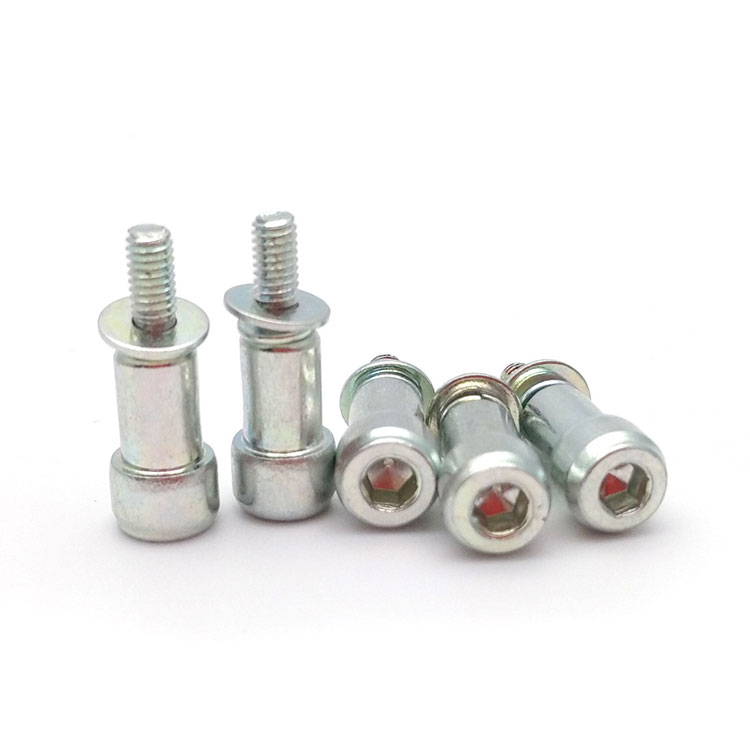
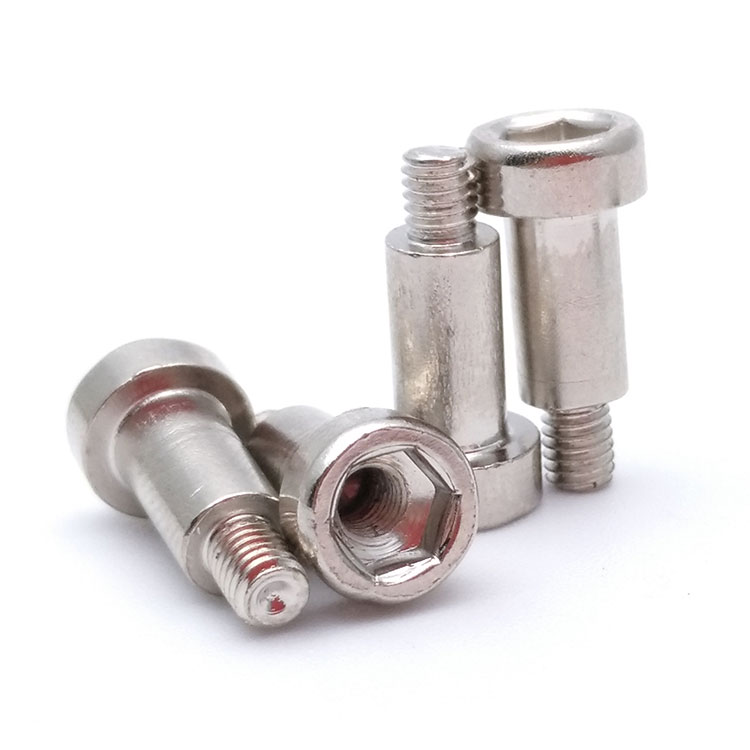
Type:Allen Head Screws
Materials:Stainless Steel
Surface treatment:Plain
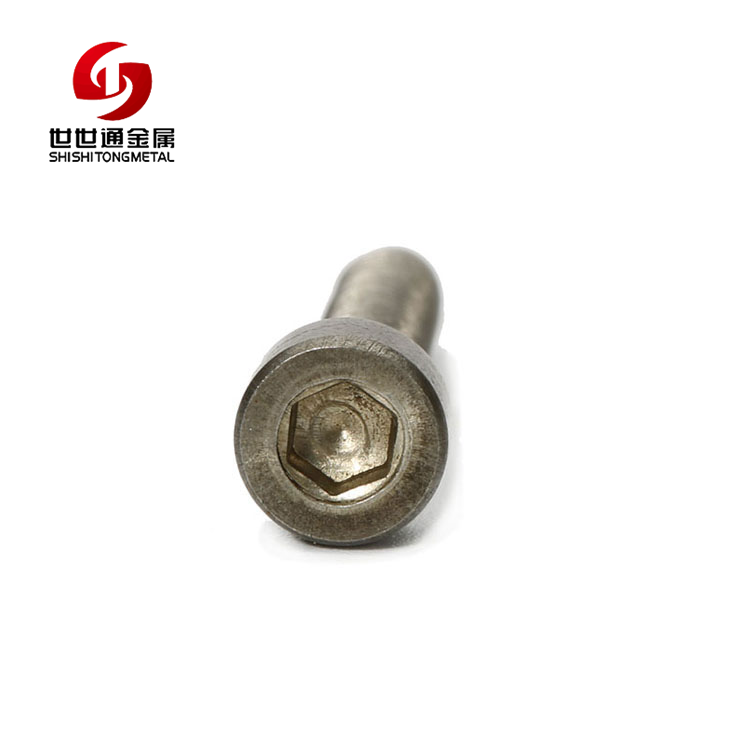
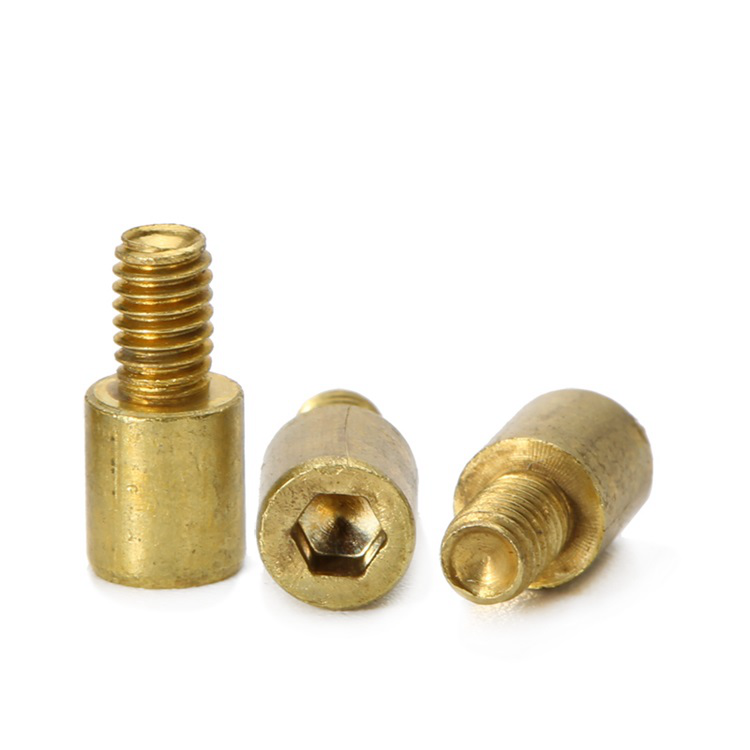
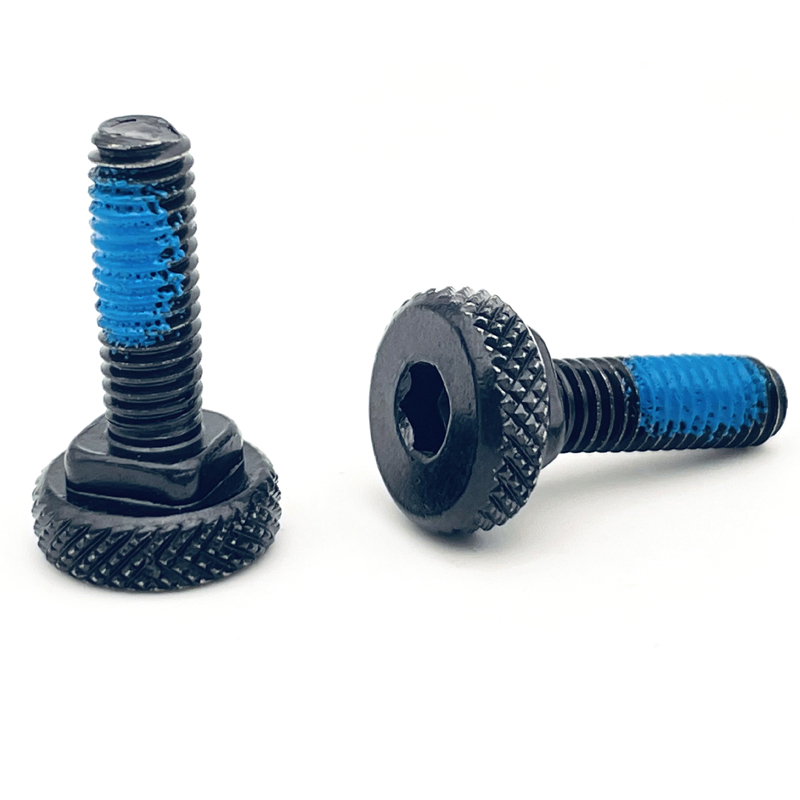
Head Type:Cylindrical socket head
Drive:Allen hex socket
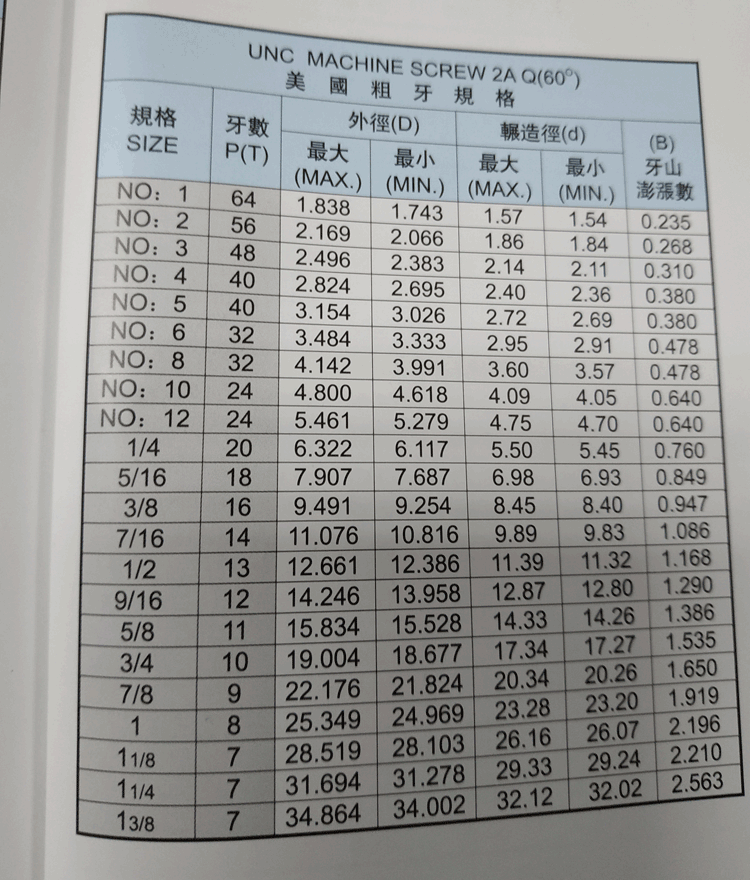
Thread:Machine thread
Point:Plain, chamfered
Forming:Turned or formed; socket cut
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
Number:8-1
We make Allen head screws in stainless steel with a cylindrical head and a hex socket, quoted with socket size, thread and engagement to the drawing. A socket does not slip, so the joint takes the preload the tool applies, and the first article is tightened with your key and torque setting.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Allen head screws are socket head cap screws driven with a hex key, with a cylindrical head and a hexagon cut inside it. The part recorded here is stainless steel left plain, quoted in metric sizes from M1 upward with the length made to the drawing.
Socket head. A cylindrical head with a hexagon inside, so the key drives on the axis rather than from the side.
Defined bearing face. A flat underside that seats in a counterbore and spreads the clamp.
Machine thread. A thread that engages a tapped hole or a nut over a defined length.
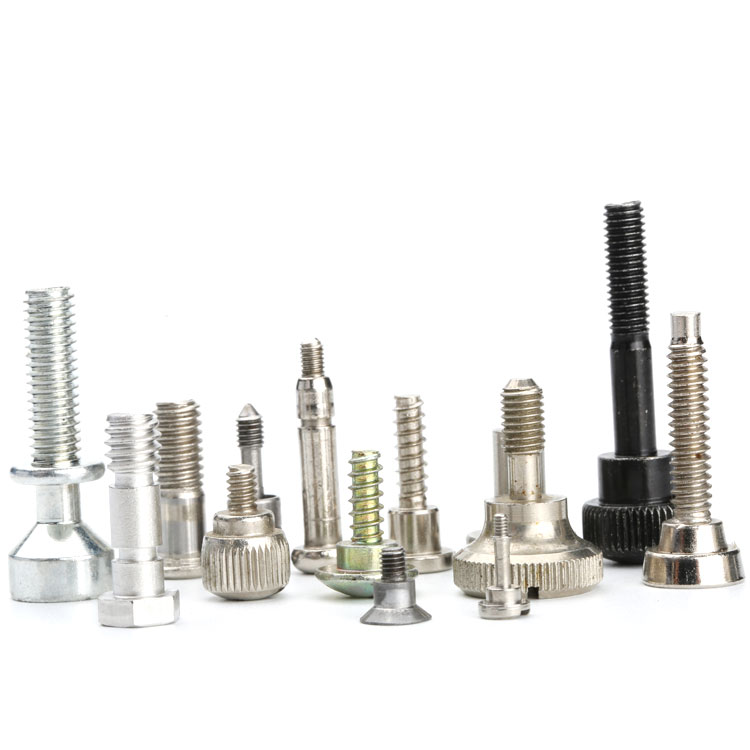
They are used wherever a joint has to be tightened to a set preload rather than to a feel, on equipment and instruments built to metric hardware. The same family covers everything from a 3 mm cover screw to a 10 mm frame bolt, so the drawing has to state the size and the engagement rather than the name.
The hexagon in an Allen head screw does not climb out the way a cross recess does. That is the property everything else follows from: the drive transfers torque cleanly to the thread, so whatever the tool applies reaches the joint. On a cross recess the bit slips at a certain point and protects the thread by accident; on a socket head there is no such limit, and the limit has to come from the tool.
That is a strength and a risk at the same time. The strength is control: a torque wrench on a hex key or a torque-limited driver can set a preload repeatably, which is what a structural or instrument joint needs. The risk is over-tightening: without a set limit, a strong hand on a long key can pull a thread past its elastic range, and the failure appears later as a loose joint rather than as a stripped thread at the time.
The second factor is engagement. A socket head screw usually engages one diameter or a little more of thread, and the load it can take depends on that engagement rather than on the head. On a thin plate the engagement is short, and the screw then fails by pulling the thread out rather than by breaking; that is a joint design issue, not a screw fault.
The third is the bearing face. The head seats on the floor of a counterbore or on a washer face, and the area of that face sets the pressure on the part. On a soft or thin part the pressure matters more than the torque, because the face can embed before the thread is loaded.
And the fourth is the material. Stainless socket head screws are strong and do not rust, but stainless against stainless galls: the thread can seize before it reaches the preload, and then the torque reading means nothing. A lubricant or a controlled thread fit is what makes a stainless joint repeatable.
The part is quoted to the drawing with the head, the socket, the thread and the engagement stated separately. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation for Allen head screws carries the head diameter and height, the socket size and depth, the thread size and length, and the material it engages.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Cylindrical socket head | Diameter, height and bearing face |
| Socket | Hexagon in the head | Across flats and depth |
| Thread | Machine thread | Size, pitch and length |
| Engagement | In the customer part | Thread depth agreed |
| Torque | Preload control | Set by the tool, stated for the joint |
| Material | Stainless steel | Grade and finish |
The socket size is fixed by the head diameter, and it is the feature that decides whether the joint can be tightened to its stated torque. A key that is too small for the socket is worse than useless on a stainless part: it rounds the hexagon and the screw cannot be removed.
The head height sets how much material is around the socket and how deep the hexagon can be cut. On a low head the socket takes most of the available section, and the head then fails before the thread does.
The engagement length is a customer dimension. It is written as a thread depth in the tapped part, and it is what the joint’s strength depends on more than the screw’s length does.
Four properties decide Allen head screws, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Hex socket | Torque without slip | No built-in limit, so over-tightening is possible |
| Cylindrical head | A flat bearing face | Needs a counterbore or a clear area |
| Machine thread | A repeatable joint | Needs a tapped hole or a nut |
| Stainless | No rust and high strength | Galling on stainless threads |
The value is a joint that can be set rather than felt. A torque setting on a socket head screw is meaningful, because the key does not slip; the same setting on a cross recess is only an upper bound.
On Allen head screws the cost is that the setting has to exist. Where a socket head is driven by hand without a torque tool, the joint is as uncontrolled as any other, and on a stainless thread it may also seize before it is tight.
The recorded finish is plain stainless steel. On a socket head that keeps the hexagon at its cut size and the bearing face flat, and it avoids a plate that would sit inside the socket where the key has to fit.
| Option | How it protects | Effect on socket and head | Typical use |
|---|---|---|---|
| Plain, passivated | Passive film, no coating | Socket and face as cut | Instruments and assemblies |
| Passivated 316 | Higher alloy passive layer | No build; better in chlorides | Marine and medical |
| Dry film lubricant | Low-friction film | Thin; reduces galling | Frequently serviced joints |
| Zinc plated | Sacrificial zinc | Build inside the socket | Cost-driven dry work |
| Black oxide | Conversion film, oiled | No measurable build | Dark mechanisms |
Inside the socket the plate is the problem: a layer a few microns thick reduces the effective across-flats, and a key that fitted before plating may not enter afterwards. Where a plated socket head is used, the socket is checked with the key in the plated state.
On stainless parts a dry film lubricant is often the more useful treatment than a coating. It does not change the socket, and it reduces the galling that can seize the thread before the joint reaches its preload.
Three assemblies where the preload has to be known:
| Where it sits | The screw holds a plate, a stop or a jaw where the joint is tightened to a set torque during setup. |
| When it goes wrong | The joint loosens under cutting forces, or the thread strips during tightening. |
| Why it happens | The torque is set by feel, and the engagement is short. |
| What we control | Engagement and socket checked; first article tightened with a torque tool. |
| Where it sits | The screw closes a housing or holds a mount where a repeatable preload keeps an alignment. |
| When it goes wrong | The alignment drifts after assembly, or a screw backs out. |
| Why it happens | The joint is not tightened to a defined value, and stainless galling makes it variable. |
| What we control | Thread pair and lubricant agreed; first article assembled with a torque driver. |
| Where it sits | The screw joins brackets and plates in a frame that is assembled on site. |
| When it goes wrong | The joint works loose in service, or a screw is over-tightened and pulls its thread. |
| Why it happens | No torque is specified, and the key used is longer than the screw can take. |
| What we control | Torque stated per size; first article assembled and checked for seat. |
Four reasons that matter on a part where the torque has to be set rather than felt, each tied to something the drawing or the first article proves. All four show in the sample.
|
Socket, head and engagement stated
The drawing states the socket size, the head height and the engagement, because those three decide whether the joint can take its preload. Basis: Three dimensions agreed. |
Socket cut in a finished head
The socket is cut after the head is faced, so its depth is measured from the surface the key meets. Basis: Socket depth controlled. |
|
Key and torque tool used
The first article is driven with the customer key and a set torque, because a socket head only gives what the tool asks it to. Basis: Torque proved with the tool. |
Same limits on repeat runs
Socket, head and thread are recorded with the drawing revision, so a repeat batch takes the same setting. Basis: Same limits across orders. |
These screws are turned or formed from stainless bar and wire, with the cylindrical head formed and faced, the hexagon broached, and the thread cut behind the head; the parts are cleaned, passivated and inspected. The first piece of every run is measured on head diameter and height, socket across flats and depth, thread, and length.


|

|
The socket is the operation that limits the head. It is broached or milled after the head is faced, and the depth has to leave enough material under the hexagon for the head to take the torque the key will apply. A socket cut too deep is a head that splits or rounds out; one cut too shallow stops the key from engaging over its length.
The head face is finished square to the thread so the screw bears flat on the counterbore floor. On a socket head that face is the bearing surface, and a face that is out of square loads one side and leaves the joint rocking.
The thread is cut rather than rolled on stainless parts, so the crest stays clean and the major diameter stays predictable. The parts are then passivated, and every batch is checked with a key in the socket, since the fit is what the assembly depends on.
What decides whether Allen head screws pass is the socket, the head face and the thread. The inspection agreement covers those, and the criteria come from the drawing.

Socket and head on the projector |

Thread and start checked |

Material checked |

Salt-spray testing where plated |
The socket is measured across flats and for depth, and checked with the key on a sample from each batch. A socket that measures right but will not hold the key is usually a burr at a corner, and one that lets the key rock is usually too deep.
The head is checked for diameter, height and flatness of the bearing face, and for the transition into the shank. On a part that is tightened to a torque, that transition is where the head bends first.
The thread is gauged and the start checked. A sample is driven to the stated torque into a tapped test block to confirm that the joint reaches its preload without galling, which is the property a stainless socket head screw is bought for.
Every batch of Allen head screws is traceable to the bar or wire it was made from and to the passivation lot that finished it. The grade and heat number appear on the material certificate supplied with the parts, and the dimensional results are recorded against the drawing revision.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing, including the socket and head, and the passivation record. The records carry the drawing revision and the batch number, so a repeat order of Allen head screws takes the same torque.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a socket head part the first article is tightened with the customer’s key and torque tool, because the joint only exists once it has been set. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Repeat orders of Allen head screws are checked against the same first article, so the torque that was proved once is reproduced. Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the machining cell and the inspection bench can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
A key does not slip, so the torque that is applied reaches the thread. That makes a set preload possible.
There is no built-in limit. Without a torque tool, a long key can pull a thread past its elastic range.
Usually one diameter or a little more. On a thin plate the joint then fails by pulling the thread out, which is a design issue.
Galling between stainless surfaces. A lubricant or a controlled thread fit is what makes the joint reach its preload.
Yes. A layer inside the hexagon reduces the across-flats, so the socket is checked with the key after plating.
Head diameter and height, socket size and depth, thread size and length, the engagement in the tapped part, and the material and finish.
How an Allen head screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the tapped part
|
→ |
2
Head, socket and engagement agreed
|
→ |
3
First article tightened to torque
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the head diameter and height, socket size and depth, thread size and length, the engagement in the tapped part, and the material and finish.
|
Head size
|
Socket AF
|
Socket depth
|
|
Thread
|
Engagement
|
Torque
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com