Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
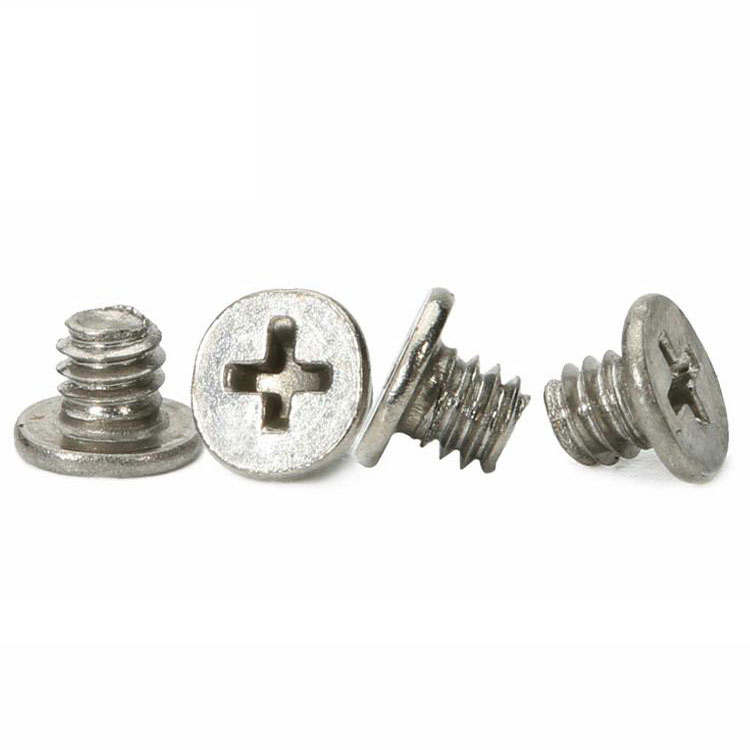
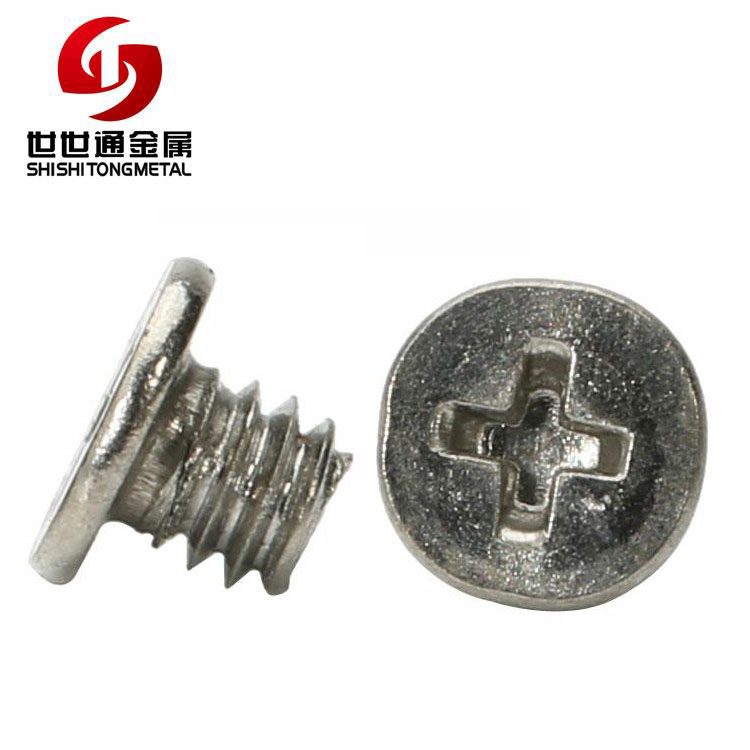
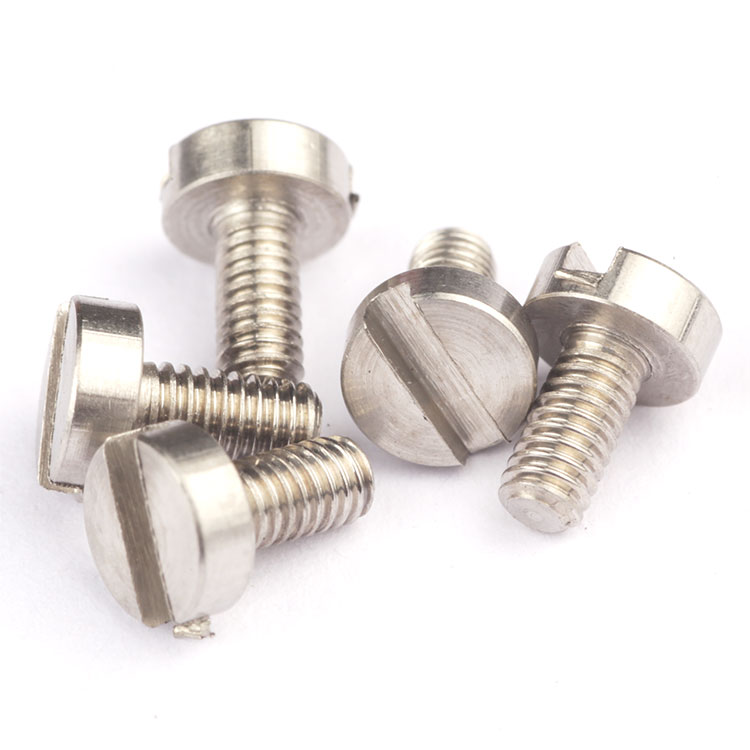
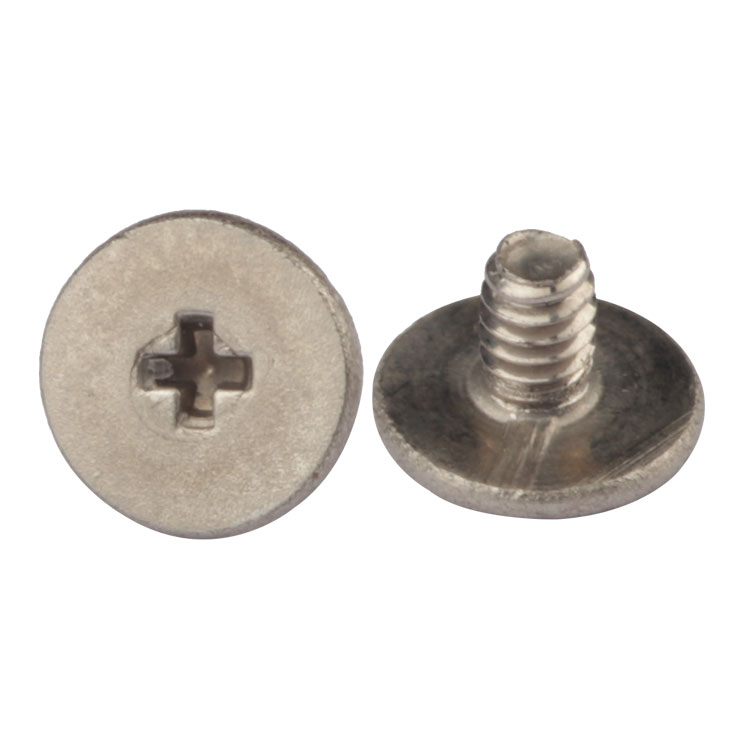
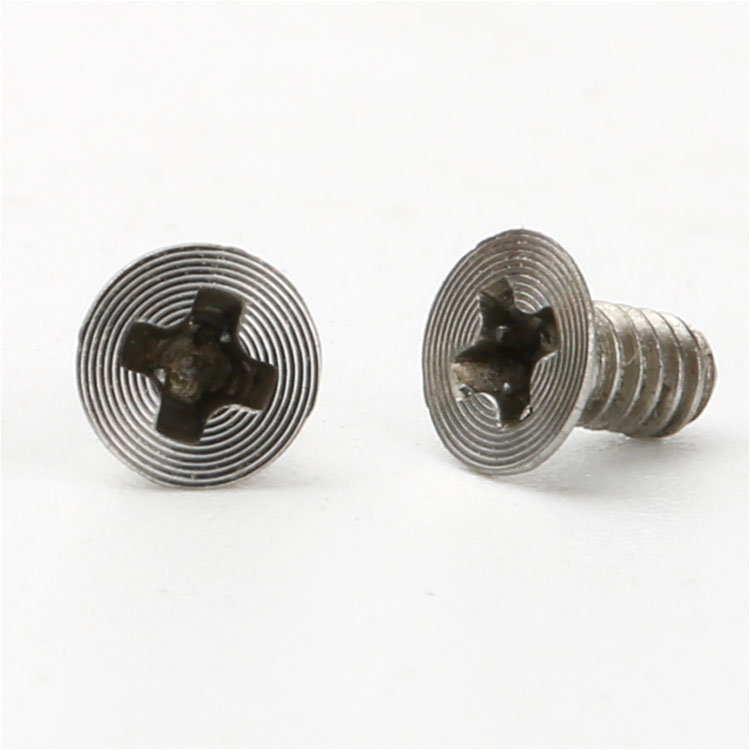
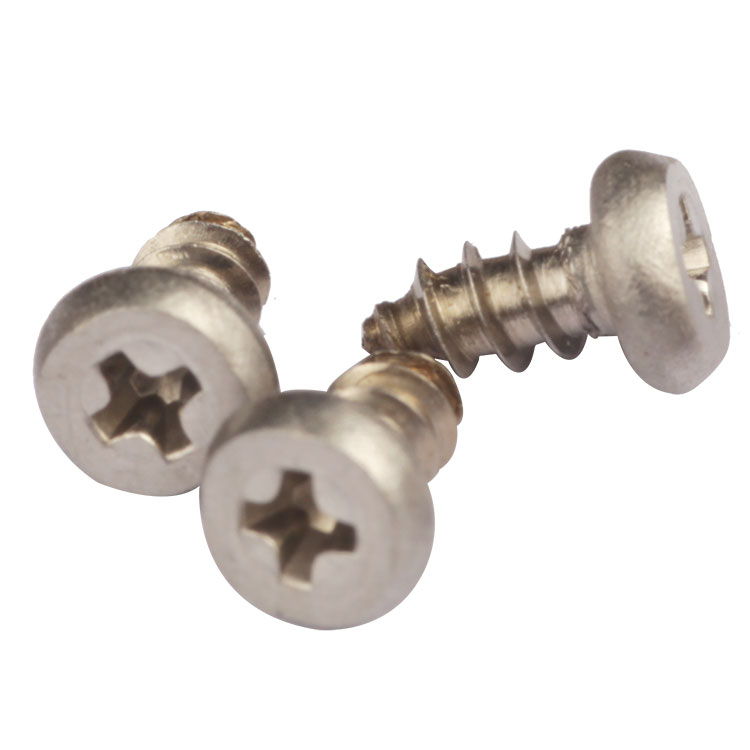
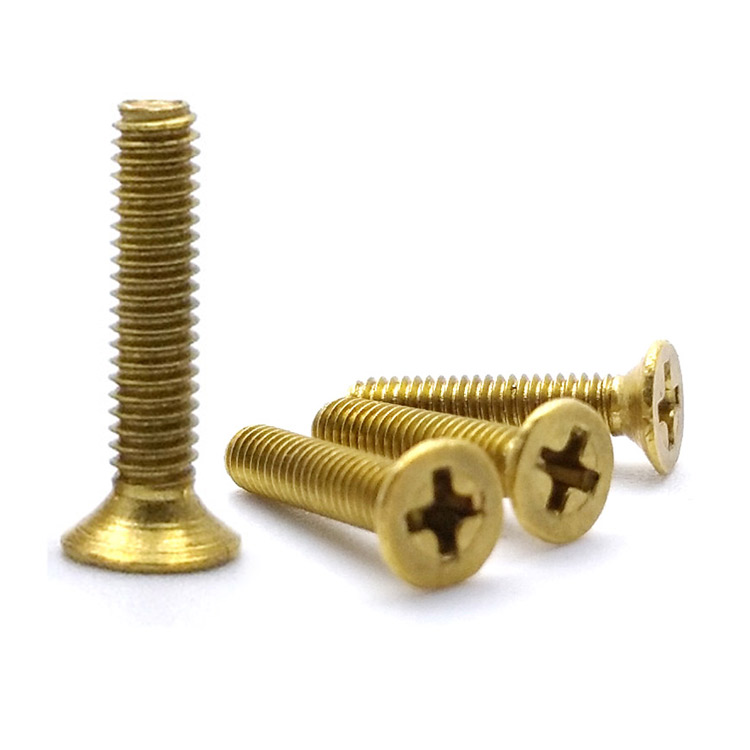
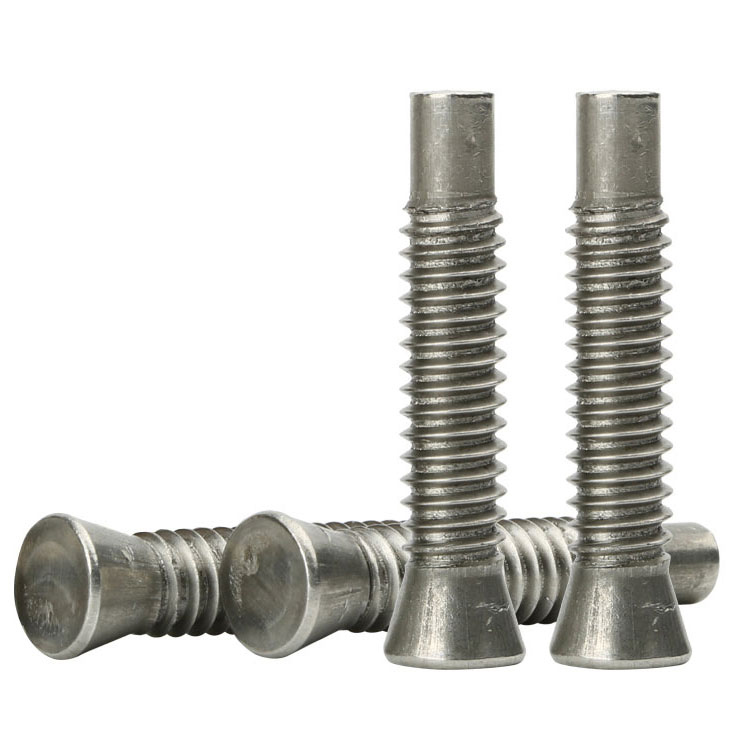
Type:Small Watch Screws
Materials:Stainless Steel
Surface treatment:Plain
Head Type:Low head
Drive:Phillips cross recess
Thread:Fine machine thread
Point:Plain, chamfered
Forming:CNC turning; recess milled
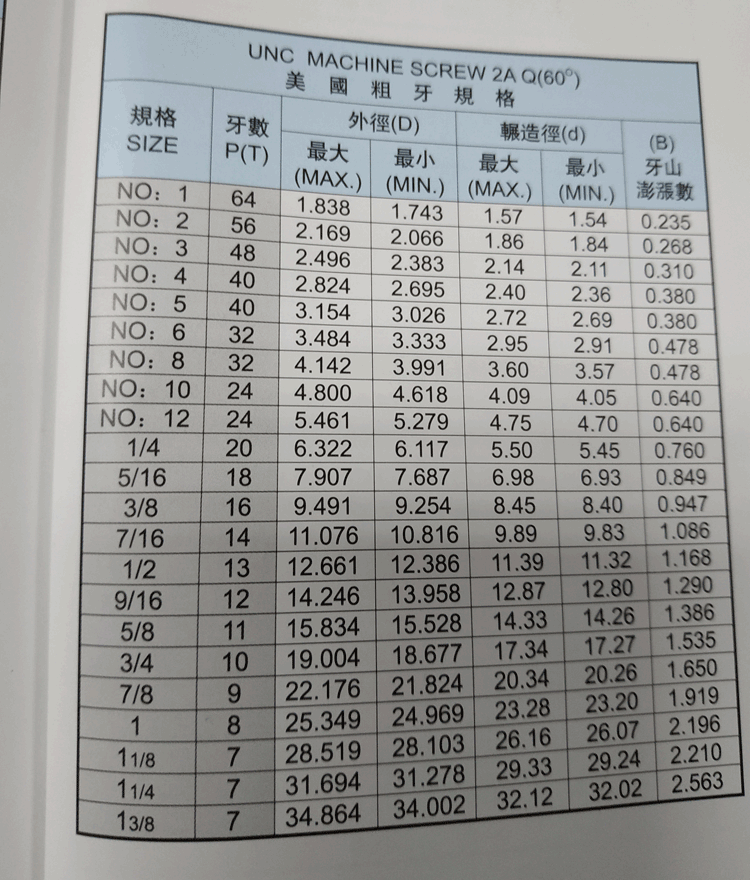
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
We make small watch screws in stainless steel with a Phillips recess and a machine thread, quoting head height, recess size and thread to the drawing. The cross gives a service centre a standard bit, and the recess is cut as deep as a low head allows so the thread sets the torque.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Small watch screws are screws in the sub-millimetre to two-millimetre range used to close watch cases, hold strap fittings and secure parts inside a movement. The part recorded here is stainless steel left plain, with a Phillips recess and a machine thread, quoted from M1 upward.
Small machine thread. A fine thread that goes into a tapped hole in the case or the movement rather than forming its own.
Phillips recess. A cross recess driven with a standard bit, sized to the small head.
Low head. A head that sits close to the surface so the joint disappears into the case or the lug.
They are used where the fixing has to be flush, removable and repairable with a driver that a service centre already has. The same size and material cover case backs, lugs and movement parts, and what changes between them is the head height and the length rather than the thread.
Watch work has traditionally used slotted screws, and for good reason: a watchmaker’s blade gives fine control over a tiny thread, and a slot can be cut shallow in a head only a few tenths of a millimetre high. A cross recess on small watch screws is a different choice, made for the people who service the product rather than for the person who assembles it.
The argument for the cross is the driver. A Phillips bit is a standard part, available in every service kit, and it self-centres in the recess, so a technician who is not a watchmaker can remove a case back without damaging it. A slot demands a blade of the right width, and a blade that is slightly wrong rounds the slot on the first attempt. On small watch screws that difference decides whether a service is a five-minute job or a scratched case.
The argument against is depth. A low head has little material, and a cross needs depth in two directions while a slot needs it in one. On a low-head screw the recess has to be cut shallow and narrow, which reduces the torque it can transmit; the assembly torque then has to be set by what the fine thread can take rather than by what the head can deliver.
The thread is the other half. These are machine screws going into a tapped hole, so the joint depends on the pair of threads rather than on the screw forming its own. A fine thread in stainless into a tapped stainless hole is prone to galling, and galling at this size shows as a screw that tightens and then seizes before it seats.
Put together, the cross-recess route gives a watch screw that any service centre can open, at the cost of a lower torque ceiling and a head that has to be machined carefully to keep enough material around the recess.
The part is quoted to the drawing with the head, the recess and the thread stated separately. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation for small watch screws carries the head diameter and height, the recess size and depth, the thread size and pitch, the length under the head, and the tapped hole in the customer part.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Low, close to flush | Diameter, height and edge |
| Recess | Phillips, smallest size | Depth, width and centre |
| Thread | Fine machine thread | Size, pitch and length |
| Hole | Tapped, in the customer part | Agreed size and depth |
| Grade | Stainless | Alloy and finish |
| Torque | Assembly torque | Set by the thread, not the head |
The recess size is written as a Phillips number, because the bit is chosen by that number. On a low head the next size up will not fit without removing material the head does not have, and the next size down will turn out the cross.
The head height is a dimension rather than a style. A case back needs the screw level with the case; a lug screw needs it below the strap line. The same thread is offered in more than one head height for that reason.
The thread is agreed against the tapped hole in the customer part. On a machine joint the pair is the specification, and a screw quoted without the hole cannot be assessed for fit or for galling.
Four properties decide small watch screws, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Phillips recess | A standard bit and self-centring | Shallow in a low head |
| Low head | Flush in case or lug | Little material for the recess |
| Machine thread | A defined, repeatable joint | Needs a tapped hole and galling control |
| Stainless, plain | No rust from handling | Galling on stainless threads |
The value is a joint that can be serviced. The head is flush, the drive is standard, and the thread is a known fit in a tapped hole, so the same part can be opened and closed by a technician rather than by a specialist.
The cost is a lower torque ceiling. Because the recess is shallow and the thread is fine, the screw is tightened to what the thread allows, and the head is expected to survive that and no more.
The recorded finish is plain stainless steel. On small watch screws it keeps the recess at its cut depth and the thread at its cut size, and it avoids a plating process that could add material inside a recess only a few tenths deep.
| Option | How it protects | Effect on recess and thread | Typical use |
|---|---|---|---|
| Plain, passivated | Passive film, no coating | Recess and thread as cut | Watch cases and lugs |
| Passivated 316 | Higher alloy passive layer | No build; better in chlorides | Dive and sports watches |
| Nickel plated | Hard bright barrier | Thin build; recess re-gauged | Decorative case hardware |
| Dry film lubricant | Low-friction film | Thin film; galling reduced | Frequently serviced joints |
| Black oxide | Conversion film, oiled | No measurable build | Dark mechanisms |
Galling is the finish problem specific to this joint. Stainless thread against stainless thread can seize under the load of a small screw, and a dry film lubricant is the usual way to reduce it without changing dimensions; it is thin enough to leave the recess alone.
Where a coating is chosen for appearance, the recess is checked again after plating. On a low head there is very little margin, and a layer that takes a tenth of a millimetre out of a shallow cross changes which bit will drive it.
Three assemblies where a flush, serviceable fixing is the requirement:
| Where it sits | The screw closes a case back or secures a bezel where the joint has to be flush and repairable. |
| When it goes wrong | The head stands proud, or the recess rounds out when the case is opened. |
| Why it happens | The recess is too shallow for the bit, or the head height is wrong for the case. |
| What we control | Head height and recess checked; first article assembled in the case. |
| Where it sits | The screw holds a strap end link or a lug where the head must sit below the strap. |
| When it goes wrong | The strap catches on the head, or the screw backs out in use. |
| Why it happens | The head is too tall, or there is no locking feature on the thread. |
| What we control | Head height and thread length checked; first article fitted with the strap. |
| Where it sits | The screw holds a bridge or a module where the thread goes into a tapped plate. |
| When it goes wrong | The screw seizes before it seats, or the joint loosens after servicing. |
| Why it happens | The stainless thread galls, and the torque is applied too high for the size. |
| What we control | Thread pair agreed; first article assembled and re-opened. |
Four reasons that matter when the recess and the thread set the torque ceiling, each tied to something the drawing or the first article proves. All four show in the sample.
|
Recess and head agreed together
The drawing states the recess size and the head height together, because on small watch screws one limits the other. Basis: Recess and head dimensioned. |
Recess cut on a finished head
The head is faced before the recess is cut, so its depth is taken from the face that seats and its centre stays true to the thread. Basis: Recess cut on finished face. |
|
Driven with your bit
The first article is driven with the bit the service uses, because the recess is only proved by the driver that enters it. Basis: Recess proved with the bit. |
Same seat on repeat runs
Head height, recess size and thread limits are recorded with the drawing revision, so a repeat batch seats and drives the same. Basis: Same limits across orders. |
These screws are turned from stainless bar with the head formed and faced low, the recess cut, and the thread cut; the parts are cleaned, passivated and inspected. The first piece of every run is measured on head diameter and height, recess depth and width, thread size and pitch, and length under the head.


|

|
Cutting the recess is the operation that limits these screws. A cross in a low head is cut with a very small cutter, and the depth has to leave enough material under it that the head will not collapse when the bit is turned. On a head this low, a few hundredths too deep is a head that fails on the first service.
The thread is cut rather than rolled, so the major diameter stays on size next to a head that cannot be allowed to change, and so the start stays clean for a tapped hole. Cutting also avoids the slight growth that rolling gives at the crest, which on a fine thread in a tapped hole is the difference between a free fit and a tight one.
The parts are passivated after the last operation. Where the customer services the joint repeatedly, a dry film lubricant is applied to the thread and not to the recess, because the recess has to stay at its cut size for the bit.
What decides whether small watch screws pass is the recess, the head height and the thread. The inspection agreement covers those, and the criteria come from the drawing.

Recess and head on the projector |

Thread gauged |

Material checked |

Salt-spray testing where plated |
The recess is checked with the matching bit on a sample from each batch, and for depth and width on the projector. On a low head, a recess that measures right but does not hold the bit is usually a burr on one wall rather than a dimension.
The head is measured for diameter and height, and the face for flatness. That face is what stops the screw in the case, so a dished face on a low head shows as a joint that is tight at the rim and loose in the middle.
The thread is gauged against the drawing, and a sample is assembled into a tapped test hole at the stated torque to confirm that it seats without galling. That test is the one that predicts whether a service centre will be able to re-open the joint.
Every batch of small watch screws is traceable to the bar it was made from and to the passivation lot that finished it. The grade and heat number appear on the material certificate supplied with the parts, and the dimensional results are recorded against the drawing revision.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing, including the recess and the head height, and the passivation record. The records carry the drawing revision and the batch number, so a repeat order of small watch screws seats the same way.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a serviceable part the first article is fitted into the customer case and then opened again, because that is how the joint will be used. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the recess cutting and the inspection bench can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
A Phillips bit is standard and self-centring, so a service centre can open the case without a watchmaker’s blade set.
Depth. A low head gives less room for a cross than for a slot, so the recess is shallow and the torque ceiling is lower.
The fine thread, not the head. The screw is tightened to what the thread can take and the recess is expected to survive that.
Stainless against stainless can gall. A dry film lubricant on the thread reduces it without changing the recess.
Yes, if the grade is specified and confirmed. The material is a drawing requirement, not something a dimension check shows.
Head diameter and height, recess size and depth, thread and pitch, length under the head, grade, and the tapped hole.
How a small watch screw project runs from drawing to repeat delivery:
|
1
Send the drawing, the case and the bit
|
→ |
2
Recess, head height and thread agreed
|
→ |
3
First article fitted and re-opened
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the head diameter and height, recess size and depth, thread and pitch, length under the head, grade, and the tapped hole.
|
Head size
|
Recess
|
Head height
|
|
Thread
|
Length
|
Tapped hole
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com