Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
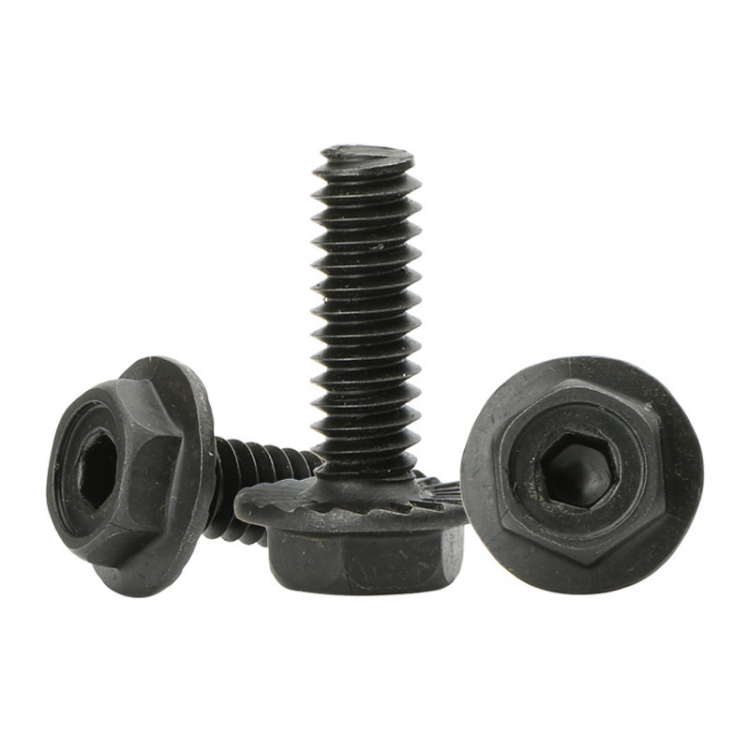
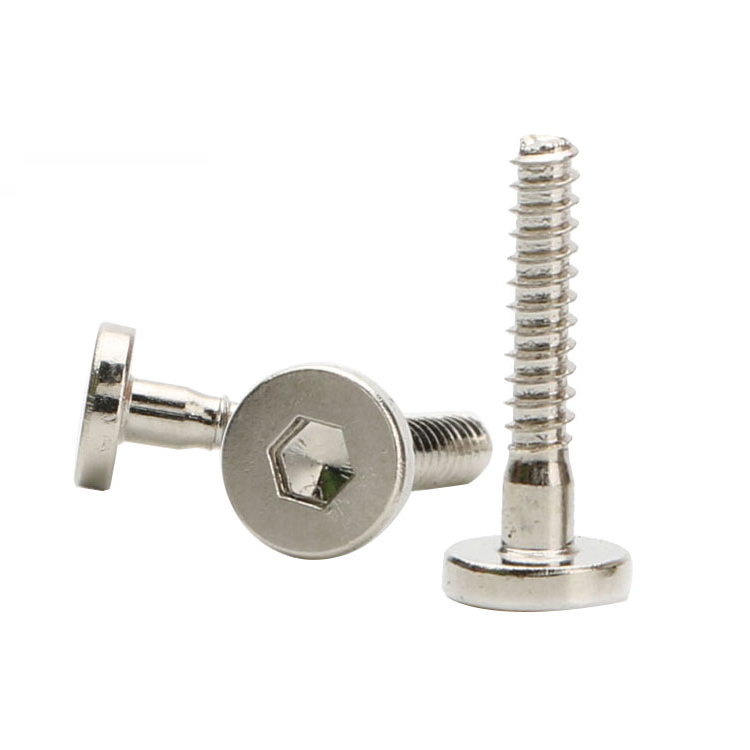
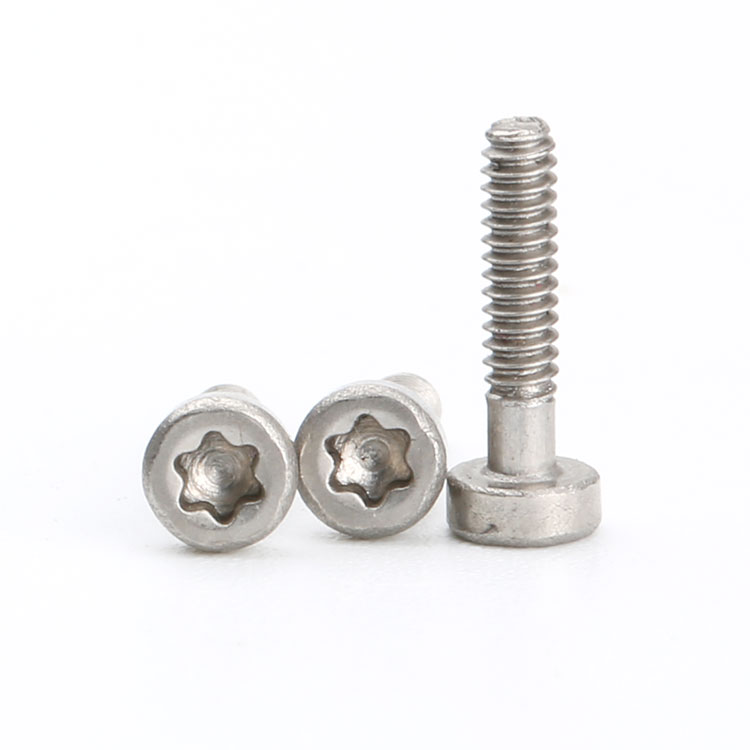
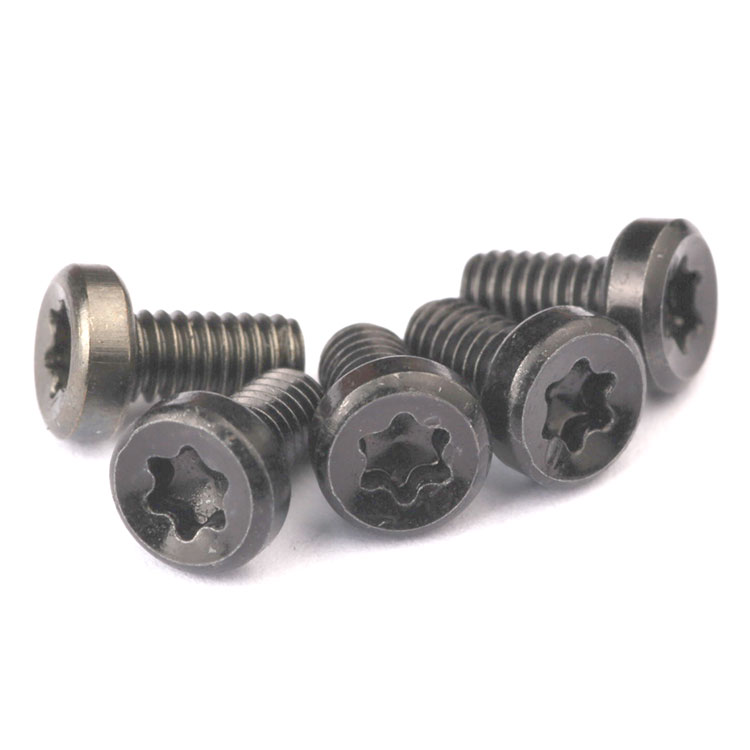
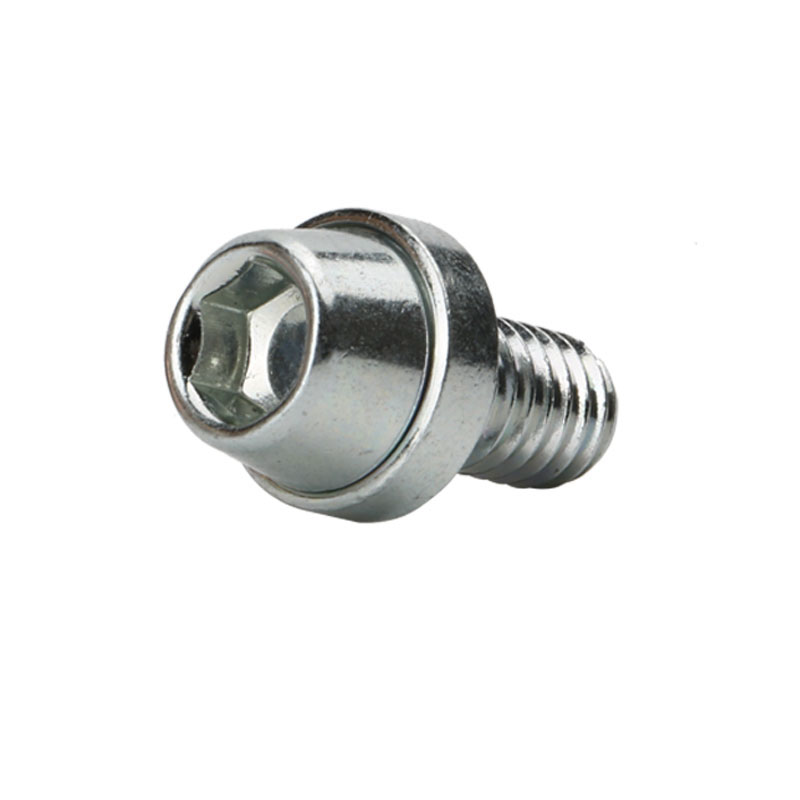
Type:Metric Socket Head Cap Screws Stainless Steel
Materials:Stainless steel
Surface treatment:Plain
Head Type:Cap Head
Drive:Hexagon socket (Allen)
Thread:Metric machine thread
Point:Plain, chamfered
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10 M14
Number:396
We make metric socket head cap screws in plain A2 stainless with a straight-knurled head and a hexagon socket, quoting them from M1 to M14. Head and knurl band, socket depth, thread and length come from your drawing, and the first article is run down by hand before it is tightened with a key.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Metric socket head cap screws are cylindrical-head machine screws with a hexagon socket in the top, driven with an Allen key. These are stainless steel, plain and passivated, with a straight knurl around the head, quoted from M1 to M14 with Number 396. The knurl lets the screw be turned by hand to the shoulder before a key is used to set the load.
Cap head. A full cylindrical head with a flat top, carrying a high clamp on a small footprint.
Hexagon socket. The drive sits inside the head, so no clearance is needed around it and the key cannot slip off the corner.
Straight knurl. A band of fine vertical ridges around the cylinder, which gives a grip for fingers.
Machine thread. A uniform metric thread for a tapped hole, a nut or an insert.
Plain stainless. A2 grade, passivated and uncoated, so the socket and the knurl are as formed.
Metric socket head cap screws are the default high-clamp fastener in machinery, and the knurled version adds one behaviour: it can be run in and out by hand. That matters on covers and adjustments that are set, checked and reset before the final tightening, where reaching for a key every time would slow the job down.
A knurled cap head is designed for two assembly actions. Fingers run it down until the head meets the part, which is fast and needs no tool, and then a key takes over to set the load. The knurl is not decoration; it is the interface for the first action, and its pitch and depth decide whether a hand can turn it without slipping.
The two actions have different limits. Finger torque is a small fraction of key torque, so the knurl only has to transmit enough to close a joint that is already aligned. The key does the work, and the socket is what has to survive it: on a stainless cap head the socket is the feature that fails when a joint is over-torqued, not the thread.
The head geometry of metric socket head cap screws is fixed by the standard form. A cylindrical cap head is taller than a button head and shorter than a pan head of the same diameter, and the hexagon sits in the centre with a wall of material around it. That wall is what makes the form able to take torque, and anything that removes it, such as a deeper socket or a deeper knurl, takes away from the same section.
The knurl interacts with the joint in a way that is easy to overlook. The ridges stand slightly proud of the cylinder, so a knurled head needs a little more clearance in a counterbore than a plain one, and it will mark a soft seating face if it is pulled down against it. In aluminium housings that mark is often the first sign that the screw was seated by hand and not by a key.
Stainless completes the picture. The thread galls in aluminium and in itself, and a stainless cap head screw that has been tightened and released a few times will start to feel rough in an aluminium thread. Assembly lubricant or a coated thread insert is the answer, not a different head.
The recorded range is M1 to M14, with lengths made to the drawing. Custom lengths up to 2,000 mm are subject to DFM review after drawing submission. For metric socket head cap screws the quotation carries head diameter and height, knurl length and pitch, socket size and depth, thread and overall length.
| Item | How it is defined | What we control |
|---|---|---|
| Head | Cylindrical cap head | Diameter and height, top edge |
| Knurl | Straight knurl around the head | Band position, pitch and depth |
| Socket | Hexagon in the head | Across flats and depth against head height |
| Thread | Metric machine thread | Pitch, length and start position |
| Length | Overall, head included | Length tolerance and thread start |
| Material | A2 stainless | Grade and heat number on the certificate |
| Finish | Passivated, plain | Surface condition and socket edges |
Socket depth against head height is the dimension to quote together. A deeper socket looks helpful and removes the material that keeps the head from splitting under a key, so the depth is a compromise that should be stated rather than left to the standard.
Knurl length is the other number. A knurl that runs too far up the head leaves a thin rim at the top, and one that stops too low does not give fingers enough to grip. On a visible part the band also reads as a design line, and customers often specify where it sits.
Four features define these metric socket head cap screws, and each one has a consequence for the joint or the process:
| Feature | What it gives | What it costs |
|---|---|---|
| Cap head | High clamp on a small footprint | Needs a counterbore or a clear area |
| Hexagon socket | Torque without cam-out | Socket depth limited by head height |
| Straight knurl | Hand running before the key | Extra clearance; marks soft seats |
| Machine thread | Repeatable preload in a tapped hole | Needs a thread in the part behind |
| Plain stainless | Knurl and socket as formed | Galls in aluminium and in itself |
The hand-running behaviour is the reason many buyers choose the knurled version of metric socket head cap screws rather than the plain cap head. On a cover with a dozen screws, running each one down by hand and then following with a key is noticeably quicker than doing both with the key, and it also reduces the chance of cross-threading, because fingers feel the thread start.
The cost appears on soft surfaces and in close counterbores. The knurl is a ring of ridges that will print into an aluminium seat, and a head that is a few tenths larger than a plain one may not clear a counterbore that was designed around the plain form.
The recorded finish is passivation on A2 stainless with no coating. On a socket head screw that matters at the socket wall, where a coating would build and narrow the hexagon, and at the knurl, where it would round the ridges that provide the grip.
| Option | How it protects | Effect on socket and knurl | Typical use |
|---|---|---|---|
| A2 stainless, passivated | Passive chromium oxide film | Socket and knurl as formed | Machinery and covers |
| A4 stainless, passivated | Passive film with molybdenum | Socket and knurl as formed | Marine and washdown |
| Alloy steel, black oxide | Conversion film, oiled | No measurable build; a common standard | High-strength joints |
| Steel, zinc plated | Sacrificial zinc | Build in the socket; re-checked | General indoor machinery |
| Stainless, passivated, silver-plated | Passive film plus a soft metal layer | Thin build; reduces galling | Repeated assembly in aluminium |
Where a joint is assembled and released often, the limiting factor is galling rather than corrosion, and a silver-plated or lubricated stainless screw is the practical answer. Where the joint is set once and left, plain A2 is enough for indoor machinery and A4 covers the wet cases.
Where a coated steel screw is specified for strength, the socket is re-checked after plating. A hexagon that was in tolerance before plating can be tight enough to refuse the key, and on a cap head that is the difference between a usable joint and a scrapped screw.
Three assemblies where the hand-running behaviour pays for the knurl:
| Where it sits | The screw holds a cover that is removed for inspection and refitted by hand before the final tightening. |
| When it goes wrong | The socket is used for every turn, and it wears out before the thread does. |
| Why it happens | The cover is opened often, the screws are numerous, and the drive is a key. |
| What we control | Knurl and socket checked; first article fitted and removed several times. |
| Where it sits | The screw sets a position that is adjusted by hand, checked against a gauge and then locked with a key. |
| When it goes wrong | The fitted screw cannot be turned by hand and the setting takes a tool at every trial. |
| Why it happens | The adjustment is iterative, the head is accessible, and the final load is set with a key. |
| What we control | Socket depth and knurl grip checked; first article adjusted and locked. |
| Where it sits | The screw is started by hand where a tool will not fit yet, then tightened once the part is in place. |
| When it goes wrong | The thread is crossed because the key cannot feel the start. |
| Why it happens | The space is tight, the part is heavy, and the thread is the only guide. |
| What we control | Thread start and socket checked; first article assembled in a mock-up. |
Four reasons that matter on a knurled socket head, each tied to something the drawing has to prove:
|
Knurl and socket agreed together
Knurl band, socket depth and head height are agreed as a set, because the knurl and the hexagon are cut into the same section. Basis: Knurl and socket agreed as a set. |
Knurled, socketed and passivated in one route
The head, knurl and socket are formed in one stroke, the thread is rolled and the parts passivated as a batch. Basis: One route from wire to passivated screw. |
|
Socket gauged with the key
The socket is checked with the production key and on the projector, because a shallow hexagon passes measurement and fails a key. Basis: Socket gauged with the key. |
First article run by hand and by key
The first article is run down by hand and then tightened with a key, because both actions are part of how the part is used. Basis: First article run by hand and key. |
Metric socket head cap screws are headed on single-die machines that form the cylindrical head, the straight knurl and the hexagon socket in one stroke, then rolled with the metric thread and passivated as a batch. The first part of every run is measured on head diameter and height, knurl position, socket depth and thread.


|

|
Forming the knurl and the socket in the same stroke is the constraint that shapes the process. The knurl die presses ridges into the outside of the head while the punch cuts the hexagon inside it, and the wall between the two is fixed by the head diameter. A head that is slightly under size produces a screw that gauges correctly and has one or two ridges standing proud at the top, where the metal had nowhere to go.
Stainless is harder to knurl than steel. The ridges form less crisply, the tool wears faster, and the band has to be checked on the first part rather than at the end of the run; a knurl that is shallow enough to look smooth will not give fingers anything to hold.
What decides whether metric socket head cap screws pass is the head, the knurl, the socket and the thread. The inspection agreement covers those four, and the criteria come from the drawing.

Head, knurl and socket |

Thread and start checked |

Core hardness checked |

Salt-spray testing of the grade |
Head diameter and height are measured on a projector, and the socket is checked with the production key as well as by measurement, because a hexagon that is shallow or has a burr at one corner will accept one key and refuse another. The knurl band is checked for position, length and ridge condition on the first part of every run.
A sample from each batch is run down by hand and then tightened with a key at the joint torque. That check proves both behaviours at once, and it is the one that predicts whether a customer’s assembly line will be faster or slower with the knurled version.
Every batch is traceable to the wire it was made from and to the passivation batch that finished it. The grade and heat number appear on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing and, where the grade is listed, the third-party report that covers it. The documents carry the drawing revision and the batch number, so a repeat order keeps the same socket depth and the same knurl.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On metric socket head cap screws the first article is run down by hand and then tightened with a key, because that is how the part is used. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the passivation line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
So the screw can be run down by hand before a key is used. Fingers feel the thread start, which reduces cross-threading.
It needs slightly more clearance in a counterbore than a plain head, and it will mark a soft seating face.
The hexagon size matched to the screw diameter. The socket is checked with the production key because a shallow one can refuse a worn key.
The two materials gall against each other. A lubricant or a silver-plated screw removes most of the problem.
Yes, and the counterbore should allow for the knurl diameter and for a small clearance at the base of the head.
Head diameter and height, knurl band position and pitch, socket size and depth, thread and overall length.
How a socket head cap screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the joint
|
→ |
2
Head, knurl and socket agreed
|
→ |
3
First article run by hand and key
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the head diameter and height, the knurl band, socket size and depth, thread pitch and overall length.
|
Head size
|
Knurl band
|
Socket
|
|
Thread pitch
|
Length
|
Grade
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com