Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
Type:Long Screw
Materials:Stainless Steel
Surface treatment:Plain
Head Type:Cup head (socket cap)
Drive:Hex socket (Allen)
Thread:Machine thread, part or full run
Point:Plain, chamfered
Forming:Formed or turned; thread cut or rolled
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
We make long screws in stainless steel with a cup head socket, quoting length, thread run and a chamfered point to the stack they have to cross. At seventy diameters the hard part is not the clamp but the first turn, so the thread start and the packing that protects it decide whether the joint begins.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
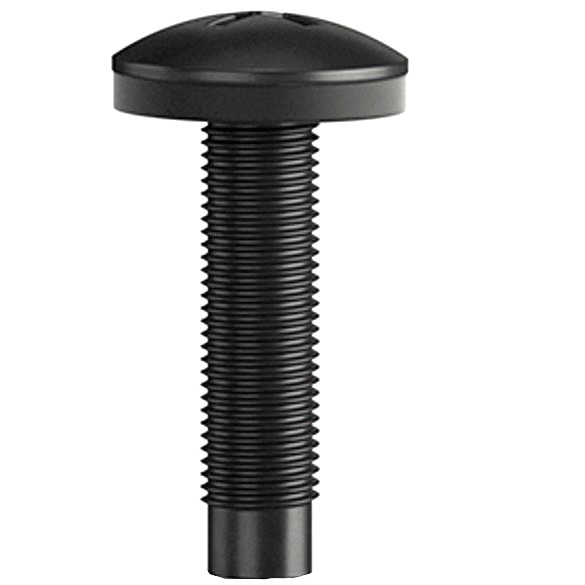
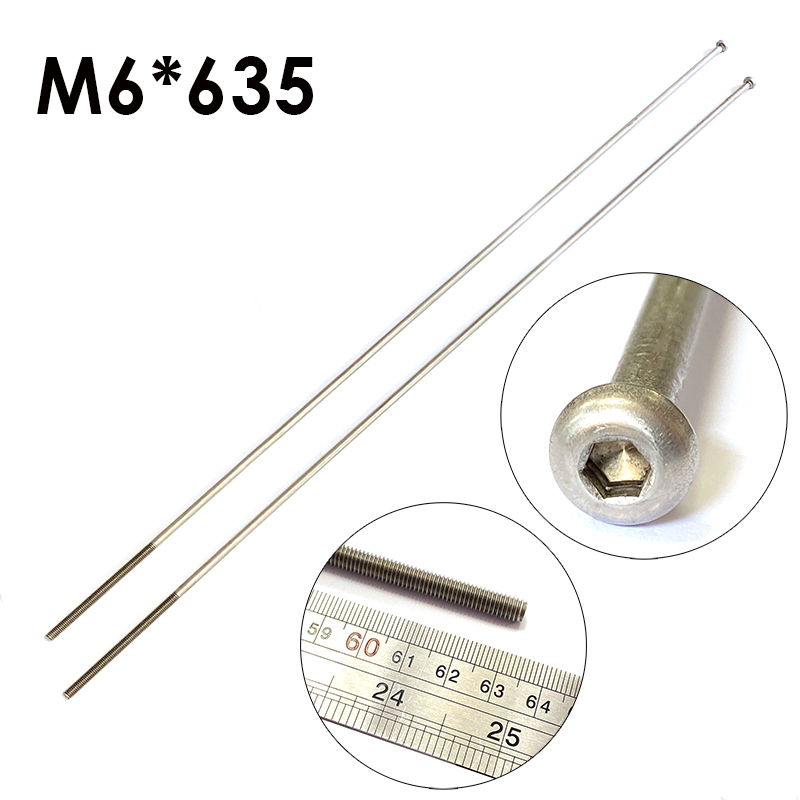
A long screw is a machine screw whose length is many times its diameter, made to reach across a deep stack or to stand off from a surface. This part is an M4 by 280 cup head socket screw in stainless steel, supplied plain, and is quoted with the length and the thread run made to the drawing.
Long shank. Seventy diameters on this size, so the shank dominates how the part behaves in the hand and in the joint.
Cup head socket. A cylindrical head with a hex socket, driven from one face.
Stainless steel. No coating, no rust, and no plating thickness to allow for.
Plain finish. The natural oxide, with the thread and the head exactly as machined.
Long screws are used in stand-offs, through-bolted panels, clamps, equipment frames and deep fixtures, where a standard length will not reach and the far side cannot be accessed.
A long screw is bought for the distance it spans, and the thread only has to hold at the ends.
At 280 mm an M4 screw is not stiff. It deflects under its own weight and it follows the hand that holds it, so before anything is clamped the part has to be guided into a hole that may be 250 mm away and out of sight behind a stack. The first thread has to catch with the two axes nearly aligned, and the thread start is a single turn wide.
That makes the thread start the most vulnerable feature on a long screw. On a short screw a burred or slightly rolled-over thread start can be forced through; here it cannot, because there is no way to press the screw sideways into alignment without bending the shank. A damaged start means the part will not engage, and the joint never begins.
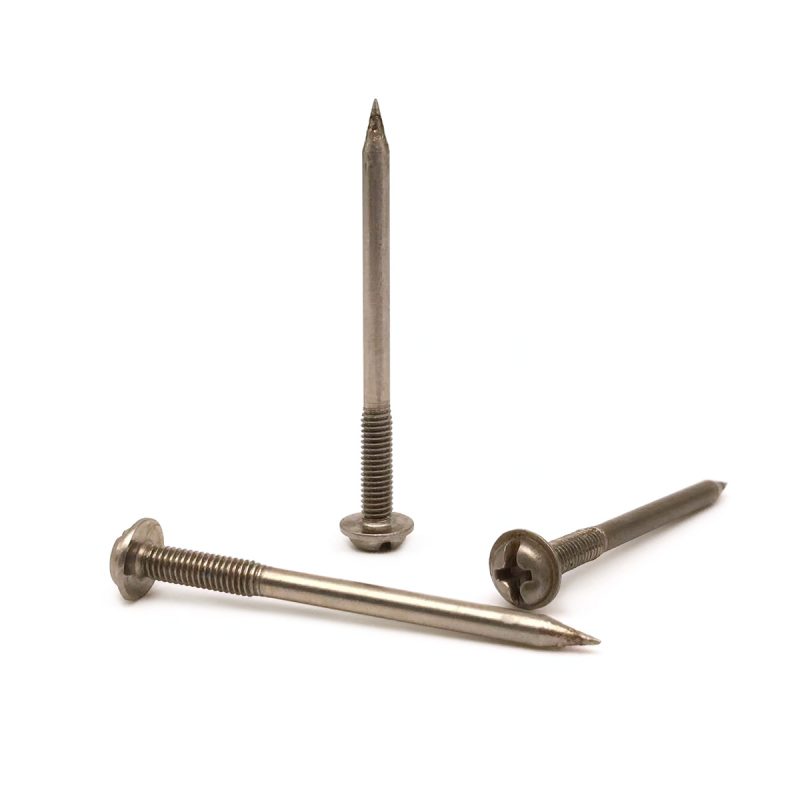
The same applies to the point. A chamfered point is not decoration: it centres the screw as it enters the first hole and leads it into the second. A point that is blunt or off-centre will catch on the far plate and put the whole shaft into a bow that the assembly then has to correct.
The handling between the packing and the assembly matters more than it does for a short part. A bundle of 280 mm screws dropped on a bench lands on a few ends, and the ends are the thread starts. That is why long screws are packed in straight bundles or tubes and why the parts are not simply tipped into a box with short ones.
None of this is a strength story. A long screw fails in assembly far more often than in service, and it fails at the point where it should have started, not at the thread where it should have held. The specification that prevents it is about the ends, the packing and the insertion, not about the torque.
Once the thread does engage, the joint behaves like any other: the head clamps and the thread holds. The difference is that a long part gets only one attempt at engaging without bending, so the design has to make that first attempt easy.
Long screws are quoted by thread size and pitch, overall length, thread length and start position, head diameter and height, socket size and finish. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation carries the grade, the head, the thread run, the length and the finish.
| Item | How it is defined | What we control |
|---|---|---|
| Body | Stainless steel | Grade and condition |
| Head | Cup head, hex socket | Diameter, height and socket depth |
| Thread start | First full thread | Chamfer, clean start and run position |
| Point | Plain, chamfered | Chamfer angle and centring |
| Length | Under the head | Overall length and tolerance |
| Finish | Plain stainless | Surface condition and passivation |
The thread start is written as a requirement rather than left to the process: a chamfered lead, no burr, and the position of the first full thread. On a long part those three decide whether the screw can be started by hand at arm’s length.
The point chamfer is specified for the same reason. A deeper chamfer leads the part into the far hole more gently; a shorter one is stronger but catches more easily, and on a stainless part a catch leaves a mark on the thread start that is there for the life of the screw.
Length is measured under the head, and the tolerance is agreed with the stack. On a stand-off the length is a functional dimension, and a tenth of a millimetre either way changes whether the joint closes.
Four properties decide this part, and each carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Long shank | A joint across a deep stack | Hard to guide into a distant hole |
| Cup head socket | A strong drive from one face | A shallow socket carries the whole torque |
| Stainless body | No rust and no plating to allow for | Galls against stainless under load |
| Plain finish | Thread and head as machined | A damaged start cannot be recoated over |
The value is reach: a single part that crosses a distance a standard screw cannot, driven from one face, in a material that will not rust in a damp plant or in service outdoors.
The cost is that the part is unforgiving in handling. Bent, burred or dropped on its end, it is scrap, and a tray of scrap is expensive in a way that a tray of short screws is not.
The recorded finish is plain stainless: the natural passive oxide, with no coating to add thickness or to wear off. On a long part that is the practical choice, because a coating over 280 mm of shank would add friction along the whole run and would be worn off at the thread start in the first handling step.
| Option | How it protects | Effect on starting | Typical use |
|---|---|---|---|
| Plain stainless | Natural passive oxide | Clean start; galling risk | Indoor and marine joints |
| Passivated | Cleaned, thickened oxide | Cleaner start surface | Food and medical equipment |
| Dry film lubricant | Low-friction film | Eases starting and galling | Joints opened in service |
| Zinc plated steel | Sacrificial layer | Smoother start, wears at the end | Indoor structural use |
| Black oxide | Conversion layer | Dry feel; some lubricity | Tooling and fixtures |
Passivation is the treatment that helps this part most: it removes the free iron left by threading, which is what turns into a rust spot at the thread start of a stainless screw that has been handled with carbon steel tools.
Where the joint is opened regularly, a dry film lubricant on the thread does the same job as on a short part, and it also makes the first turn easier at arm’s length.
Three assemblies where the reach of the screw decides the design:
| Where it sits | The screw crosses a deep stack and closes at a nut on the far face. |
| When it goes wrong | The screw will not start, or it starts and then binds halfway. |
| Why it happens | The thread start was damaged in packing, or the shank was bowed on the bench. |
| What we control | Start and point specified; parts packed in straight bundles; first article assembled. |
| Where it sits | The screw passes through a panel and a frame to a nut that cannot be seen during assembly. |
| When it goes wrong | The screw misses the far hole and the fitter forces it, bending the shank. |
| Why it happens | There is no guidance at the far end and no chamfer to lead the point in. |
| What we control | Point chamfer and hole sizes agreed; sample assembled blind and inspected. |
| Where it sits | The screw draws a clamp together across a span and is opened and closed between jobs. |
| When it goes wrong | The thread start wears bright, or the socket rounds. |
| Why it happens | The part is handled roughly in a mixed tray, and the socket is shallow. |
| What we control | Packing, socket depth and finish specified; sample cycled. |
Four points that decide whether a long screw gets into its joint at all:
|
Start and point written down
The drawing states the thread start, the chamfer and the run position, because those are the features the assembly actually uses. Basis: Entry defined, not left to luck. |
Threaded with a clean lead
The thread is cut or rolled with a chamfered lead, and the lead is inspected before the batch is run. Basis: Clean start every part. |
|
Packed straight
The parts are packed in straight bundles, so the thread starts do not take the impact of a dumped tray. Basis: Starts arrive intact. |
Same run, same lead
Grade, run position and lead chamfer are recorded with the drawing revision, so a repeat lot starts the same way. Basis: Same start across lots. |
A long screw is bought for one moment: the first turn. Everything after that is an ordinary machine screw joint. These four points are how the first turn is made repeatable.
Long screws are formed from stainless wire or turned from bar, with the cup head formed, the shank finished to length and the thread cut or rolled over the run the drawing states. The first piece of every run is measured on head, socket, thread start, thread run and overall length.


|

|
The thread start is the feature that gets the most attention on a part this long. The lead is chamfered, the first thread is checked for a clean crest, and any burr left by threading is removed by hand rather than by tumbling, since tumbling would round the lead it was meant to clean.
Stainless work-hardens, so the threading step has to be set for the material rather than for speed. A pass that is too fast leaves a torn crest at the start of the thread, which is exactly the surface that has to enter the far plate.
After threading the parts are passivated and then packed straight. The packing is part of the process because a 280 mm stainless shank will take a permanent set from a fall, and a set shank cannot be corrected at the bench.
What decides whether a batch of long screws passes is the thread start, the run position and the overall length. The inspection agreement covers those, and the criteria come from the drawing.

Head and start on the projector |

Thread and run checked |

Material checked |

Salt-spray testing of the finish |
The thread start is inspected for a clean chamfered lead with no burr, and then started by hand into a gauge nut. That is the check that matches the assembly, because a start that passes a plug gauge can still refuse to pick up at arm’s length.
The thread run is measured from the point so the position of the first full thread is known at both ends of the tolerance. A run that begins a little late leaves the nut turning on air after the whole stack has been crossed.
Length is checked over the whole part, and a sample is assembled into the customer stack. Both checks are needed: a long screw can be dimensionally correct and still fail because the run started in the wrong place.
Every batch of long screws is traceable to the wire or bar it was made from. The material certificate states the grade, the heat number, the chemistry and the mechanical properties, and the inspection record carries the head, socket, thread start, run and length against the drawing revision.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate and the inspection record for the head, thread start, run and length. The records carry the batch number, so a repeat order of long screws can be compared with the first on the feature that gets the part into the joint.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On long screws the first article is started by hand into the customer’s stack, because that is the step the part has to survive. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the heading cells and the threading can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
The thread start is damaged or the point is not centred. At this length the part cannot be forced into alignment.
In straight bundles or tubes. A bundle dropped on a bench lands on the thread starts and bows the shanks.
Yes. A chamfered point leads the screw into the far hole; a blunt or off-centre one catches and bows the shank.
The shaft twists before the far thread turns, so the torque at the socket is not the clamp at the joint.
It can. Plain stainless galls under load, and the friction builds along the whole thread run.
Thread and pitch, overall length, thread run and start, point chamfer, head and socket, and the stack height.
How a long screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the stack height
|
→ |
2
Thread run and point agreed
|
→ |
3
First article started by hand
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision used for the first article is what repeat orders are checked against.
For a quotation, send the drawing with the grade, thread size and pitch, overall length, thread run and its start, point chamfer, head and socket size, and the finish.
|
Grade
|
Thread
|
Length
|
|
Thread run
|
Point
|
Head
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com