Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
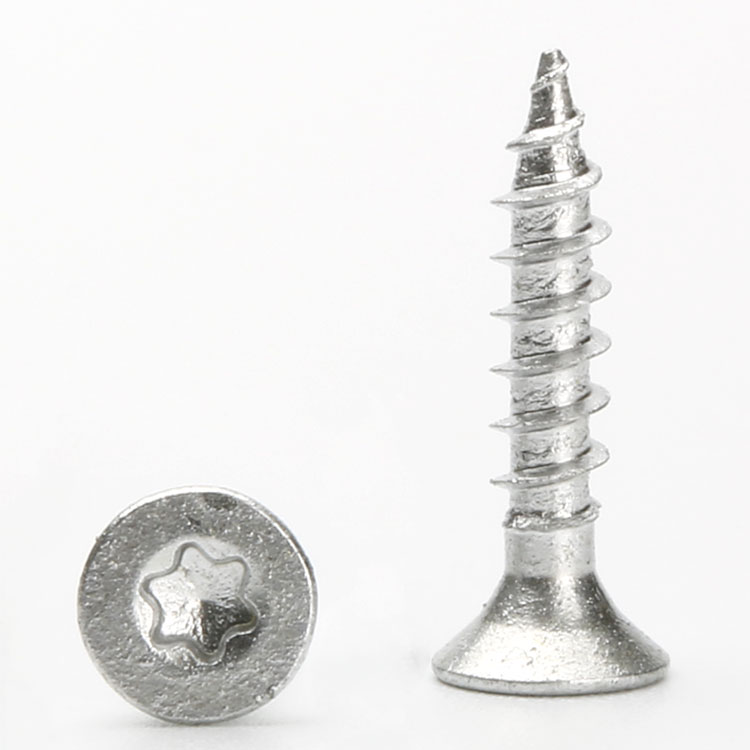
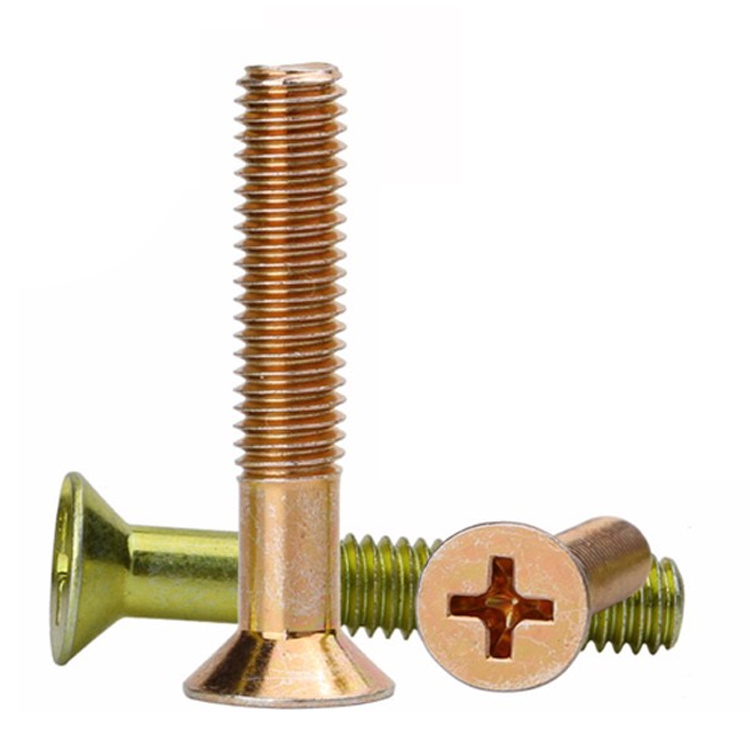
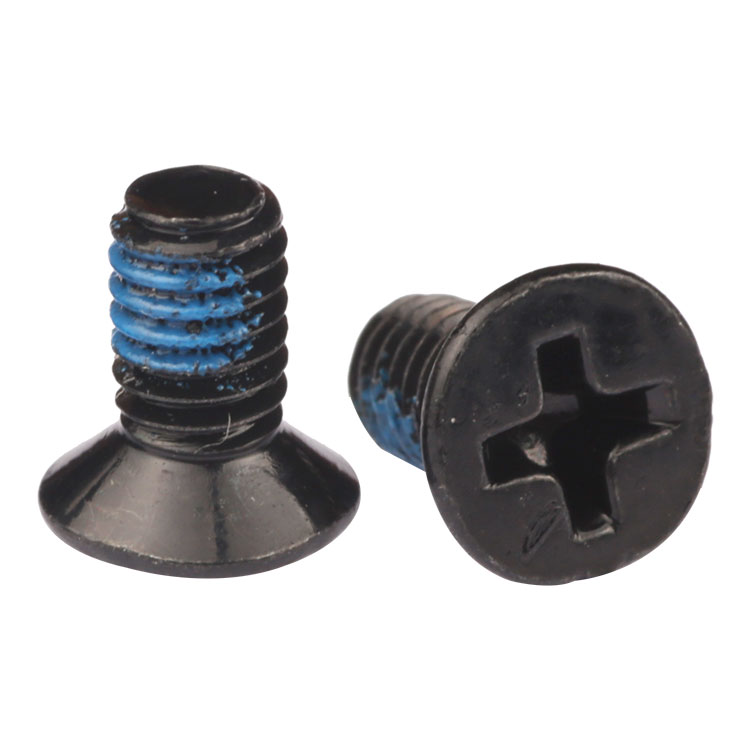
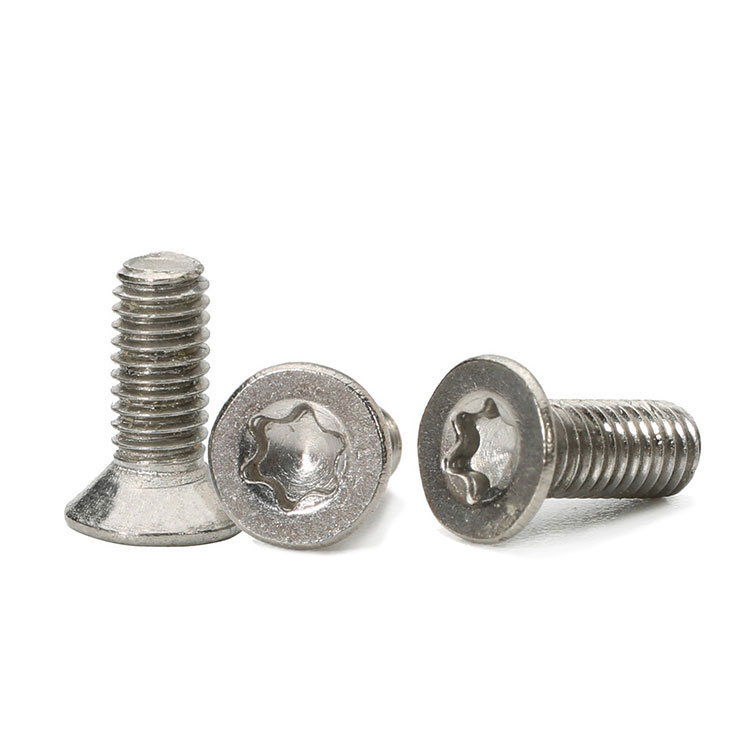
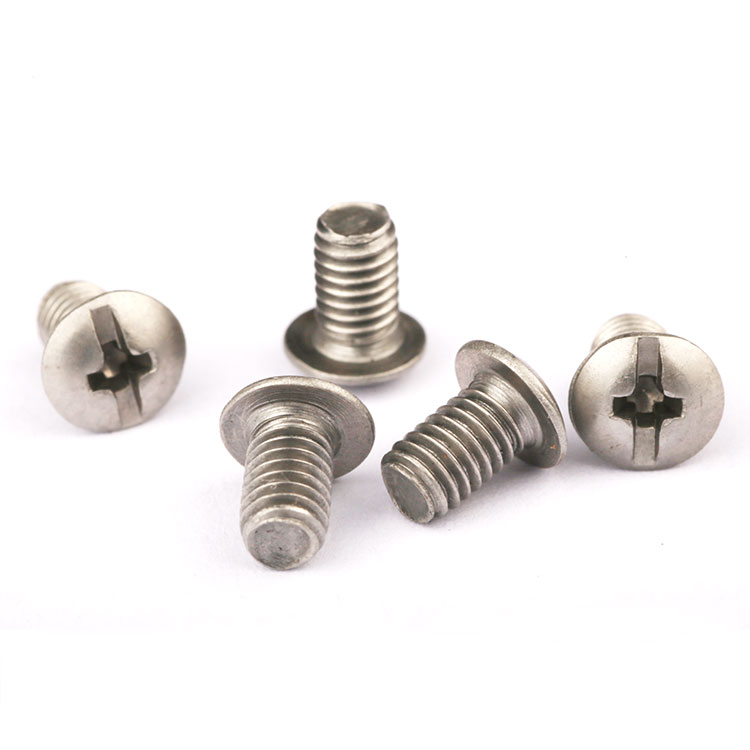
Type:Large Head Screws
Materials:Carbon Steel
Surface treatment:Nickel Plated
Head Type:Large flat head, low profile
Drive:Phillips cross recess
Thread:Machine thread
Point:Plain, chamfered
Forming:Cold heading; recess struck in the header; thread rolled
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
We make large head screws in carbon steel with a wide, low flat head and a Phillips cross, nickel plated and quoted from M1 upward to the drawing. The wide head spreads the load over the panel, and on a thin disc the head bends before the thread strips, so the head height decides what the joint can take.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Large head screws are machine screws with a head diameter several times the thread diameter and a low head height, so a small fixing covers a large bearing area. This part is carbon steel with a flat, low profile head, a Phillips cross and a nickel finish, quoted from M1 upward with the length made to the drawing.
Large head. A diameter of two to three times the thread, with a flat bearing face.
Low profile. The head is shallow, so it sits close to the panel it clamps.
Small body. A fine machine thread that suits thin panels and small tapped holes.
Nickel plating. A hard, bright barrier layer that keeps the thin head edges crisp.
They are used where a small screw has to hold a soft or thin panel without pulling through, and where the head will be seen: cosmetic panels, nameplates, lamp covers and light fittings.
A large head screw is a small shank with a thin disc on top. The disc is what the customer is buying — it spreads the clamp load over an area several times larger than the thread could reach — but it is also the weakest part of the joint. When the screw is tightened, the head behaves like a cantilever: the shank pulls down at the centre, the rim presses on the panel, and the disc bends between the two.
That bending has two visible consequences. The first is that the bearing pressure is not uniform: it peaks at the rim and falls toward the centre, so the area doing the work is a ring, not a disc. The second is that a large part of the tightening torque goes into bending the head rather than into stretching the shank, which means the preload in the joint is lower than the torque suggests.
On a soft panel the head starts to dish and the panel under it compresses; on a hard one the head springs back and the joint relaxes. Either way the screw is working near its head limit, not its thread limit, and the failure — when it comes — is a bent or cracked head rather than a stripped thread.
The head height is therefore the number to argue about, not the head diameter. A head that is a little taller takes a much higher clamp load for the same diameter, because bending resistance rises roughly with the cube of the thickness. That is why two screws with the same head diameter can behave completely differently in the same joint.
The Phillips cross adds its own limit. On a thin, wide head the recess has little material around it, and the driver starts to climb out as the torque rises — which on this part happens just as the head begins to bend. The operator feels the cam-out, stops, and the head never reaches its bearing pressure. A Torx version of the same head avoids that, at the cost of a different driver on the line.
The practical conclusion is that a large head screw is chosen for its bearing area and then limited by its head geometry. The joint works best when the panel is soft enough to conform a little, the head is thick enough to stay flat, and the torque is set by the point where the head stops moving rather than by a general table value.
Large head screws are quoted by thread size, length, head diameter, head height, recess and finish. Custom lengths up to 2,000 mm, subject to DFM review after drawing submission. The quotation carries the body material, the head, the recess, the thread and the plating.
| Item | How it is defined | What we control |
|---|---|---|
| Body | Carbon steel | Grade and hardness |
| Head | Large flat, low profile | Diameter, height and bearing face |
| Recess | Phillips | Depth and width |
| Thread | Machine thread | Size, pitch and class |
| Point | Plain, chamfered | Chamfer and burr |
| Plating | Nickel | Thickness and coverage |
The head diameter is written as a dimension, not as a ratio, because the ratio is what the customer feels and the diameter is what the tool makes. A 6 mm head on an M2 thread and a 6 mm head on an M3 thread are the same disc on two different shanks, and they fail differently.
The head height is the dimension that decides how much the part can take. It is usually the one that gets reduced when a customer wants a flatter appearance, and it is the one that should be reduced last, because the loss of bending resistance is disproportionate.
The thread class is stated on the finished part. Nickel plating adds a few microns to the flanks and to the recess, and a thread cut to the top of its class before plating will not pass a go gauge afterwards.
Four properties decide this part, and each carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Large head | Bearing area several times the thread | The head bends before the thread strips |
| Low profile | A head that sits close to the panel | Less bending resistance in the disc |
| Small machine thread | A small hole and a neat fixing | Limited clamp load in thin panels |
| Nickel plating | Hard, bright, corrosion resistant | Brittle at the thin head edge |
The value is a small, discreet fixing that holds a soft panel without a washer, spreads the load over a wide circle and looks like part of the product rather than a fastener.
The cost is a joint whose weakest element is hidden in the head. There is no visible sign that the head is near its limit until it dishes, and by then the preload is gone.
The recorded finish is nickel plating: a hard barrier layer that keeps the head edges sharp and the bearing face smooth. It does not sacrifice itself at a scratch the way zinc does, so its protection depends on staying continuous, and on a large thin head the edge is the place where that is hardest to guarantee.
| Option | How it protects | Effect on the head | Typical use |
|---|---|---|---|
| Nickel | Hard barrier layer | Bright; keeps edges crisp | Visible panels and fittings |
| Clear zinc | Sacrificial zinc | Matte silver; softer | General hardware |
| Black zinc | Sacrificial zinc plus dye | Dark; wears at the rim | Dark cosmetic panels |
| Black oxide | Conversion layer | Thin, matte, no sacrifice | Dry indoor parts |
| Painted head | Polymer film | Build; matches the panel | Colour-matched fittings |
Nickel is chosen when the head is part of the appearance and the panel is indoors: it wears better than zinc against finger marks and repeated cleaning, and it does not darken in handling.
Where the head is colour-matched to a panel, a painted head is the alternative, at the cost of a film that can chip at the rim where the head bears on the panel.
Three products where a small screw has to cover a large area:
| Where it sits | The screw holds a diffuser or a cover plate in a thin plastic or aluminium housing. |
| When it goes wrong | The head pulls through the plastic, or the panel cracks around the fixing. |
| Why it happens | The bearing area is too small and the plastic creeps under load. |
| What we control | Head diameter against panel thickness; first article clamped and checked. |
| Where it sits | The screw fixes a plate that is seen from arm’s length, where the fixing should read as a detail. |
| When it goes wrong | The head stands proud, or the nickel edge turns dull where it touches the plate. |
| Why it happens | The head is thicker than the design allows, and the plating is thin at the rim. |
| What we control | Head height and plating thickness specified; sample inspected in the product. |
| Where it sits | The screw closes a lid or a bracket into a moulded boss where a washer would be an extra part. |
| When it goes wrong | The boss splits, or the joint loosens after a few openings. |
| Why it happens | The thread is too coarse for the boss and the head bends on tightening. |
| What we control | Thread form and head diameter agreed; sample assembled and re-opened. |
Four points that decide whether a large head screw holds a panel without deforming it:
|
Head diameter and height both written
The drawing carries both dimensions, because the diameter gives the bearing area and the height decides whether the head stays flat. Basis: Head geometry specified. |
Head formed, then plated
The head is formed to size and plated afterwards, so the thin edge is measured as the customer receives it. Basis: Finished edge measured. |
|
Clamped onto the real panel
The first article is clamped onto a sample of the customer panel, and the head is checked for dishing and the panel for marking. Basis: Panel proved, not assumed. |
Same head every lot
Head diameter, height and plating thickness are recorded with the drawing revision, so a repeat lot bears the same way. Basis: Same bearing area. |
A large head screw looks simple and fails in a way that is easy to blame on the panel. These four points are what separates a part that spreads load from one that dishes, and each of them is visible on a sample clamped into the real panel.
These screws are cold headed from carbon steel wire, with the wide head formed in the heading tool and the Phillips recess struck in the same blow, the thread rolled, and the parts nickel plated. The first piece of every run is measured on head diameter and height, recess, thread and length, and clamped onto a sample panel to check the bearing face.


|

|
A head this wide is formed by a punch that spreads the metal outward, so the thickness of the rim depends on how the wire volume flows in the die. A die that is slightly worn leaves a rim thinner than the centre, and that is the edge that dishes first under load.
The recess is struck after the head is formed, which keeps the cross concentric with the shank. Off-centre recesses are common on large thin heads, because the punch bears on a wide face, and an off-centre cross pushes the head sideways as it is driven.
Plating follows the thread. On a thin head the coating at the rim is the thinnest in the part, so the plating current is set with the head edge in mind rather than only the thread gauge.
What decides whether a batch of large head screws passes is the head that bears, the recess that drives it and the plate that clamps. The inspection agreement covers all three, and the criteria come from the drawing and from the clamping test.

Head and recess on the projector |

Thread checked with gauges |

Body hardness checked |

Salt-spray testing of the plating |
The head is measured for diameter and height on the projector and checked for a flat bearing face. A head with a slight dome on the underside contacts the panel at the rim only, and on a large head that is the difference between a bearing area and a line.
The recess is checked for depth and driven with the bit at the joint torque, because the cross in a thin head rounds earlier than in a cup head. The head is then inspected for dishing and for cracks at the rim.
The thread is gauged after plating and the coating thickness checked at the head rim, which is where it is thinnest and where a dull edge shows first.
Every batch of large head screws is traceable to the wire, the heading lot and the plating lot. The material certificate states the grade, the heat number and the mechanical properties; the plating record carries the coating thickness and the lot, and the inspection record carries the head, recess and thread dimensions against the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the head, recess and thread, and the plating record. The records carry the drawing revision and the batch number, so a repeat order of large head screws can be compared with the first on the dimension that matters to the panel.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a large head screw the first article is clamped into the customer’s own panel, because the bearing behaviour depends on the panel as much as on the head. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the heading cell and the plating line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
The head is a thin disc several times wider than the shank, so it is the most flexible part of the joint. It dishes before the thread is loaded to its limit.
Up to a point. The bearing area grows with the diameter, but the bending resistance depends much more on the head height.
A thin wide head leaves little material around the Phillips cross, so the bit climbs out as the torque rises.
Yes, and that is where the large head earns its place, provided the head does not dish and the boss is thick enough.
The rim is the thinnest coated area and takes the bearing load. It is the first place to look on a returned part.
Thread and class, head diameter and height, recess, length, plating type and thickness, and the torque the joint uses.
How a large head screw project runs from drawing to repeat delivery:
|
1
Send the drawing and a panel sample
|
→ |
2
Head diameter and height agreed
|
→ |
3
First article clamped and inspected
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision used for the first article is what repeat orders are checked against.
For a quotation, send the drawing with the body material, head diameter and height, recess, thread and class, length and plating.
|
Body
|
Head diameter
|
Head height
|
|
Recess
|
Thread
|
Plating
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com