Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
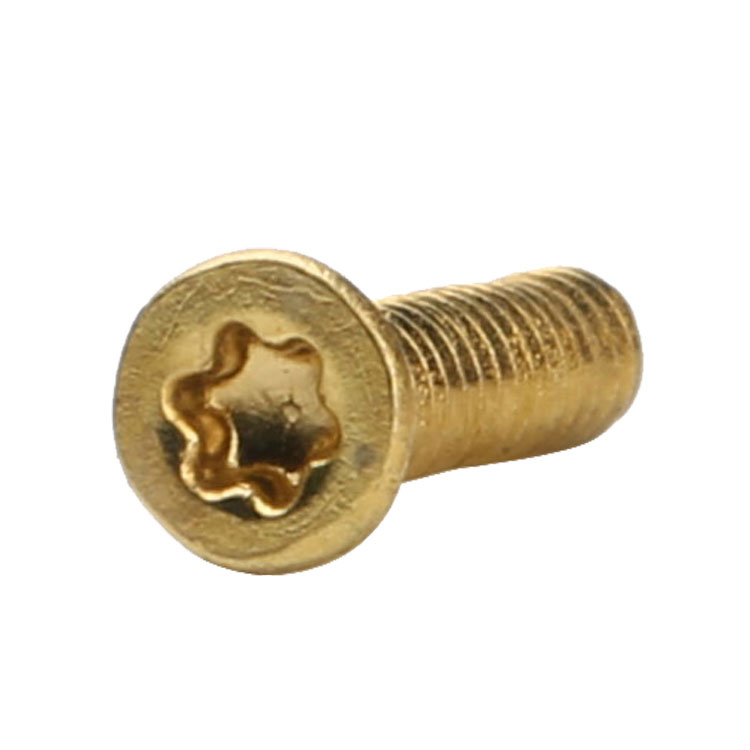
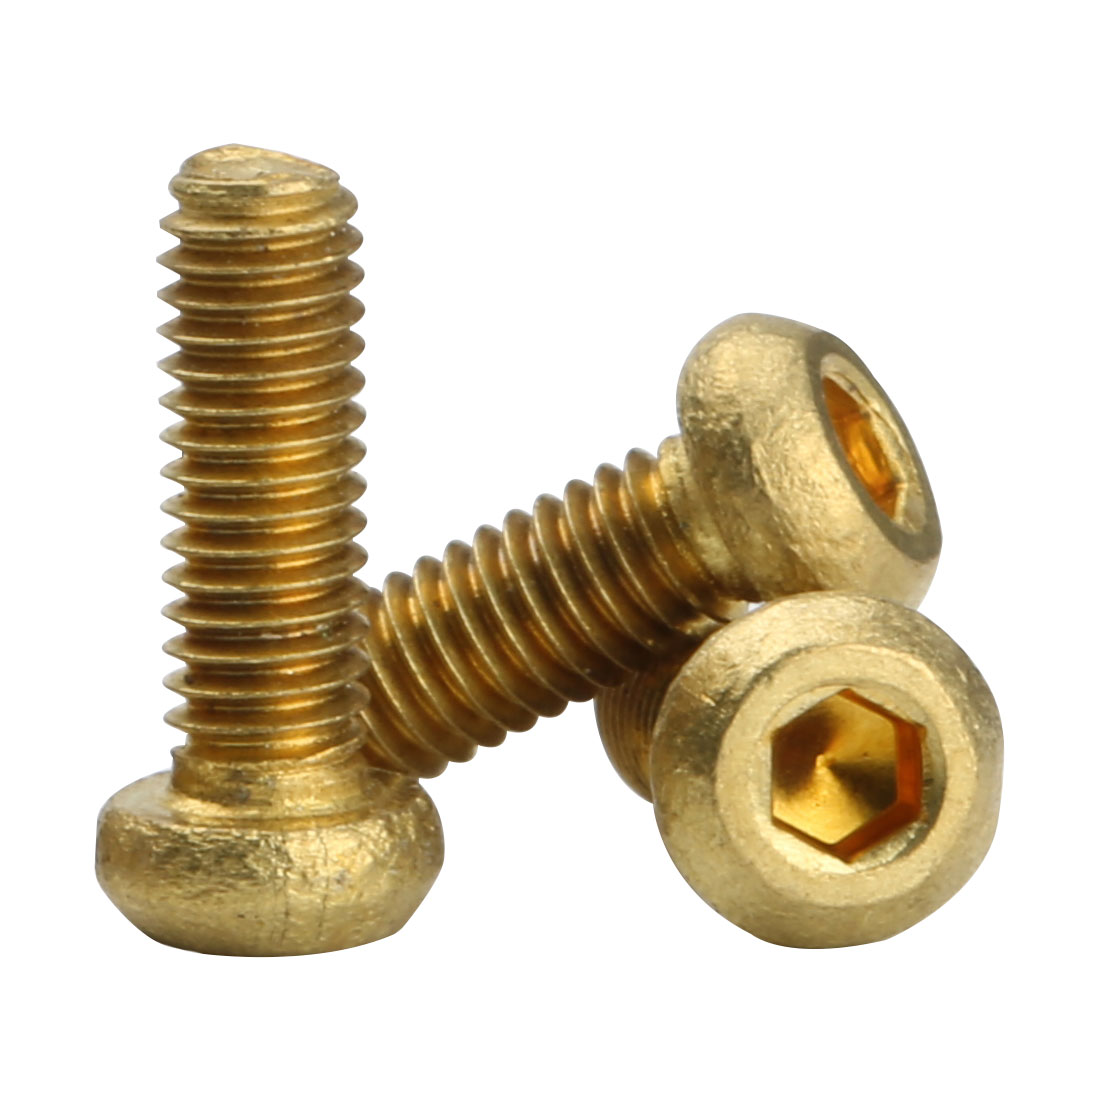
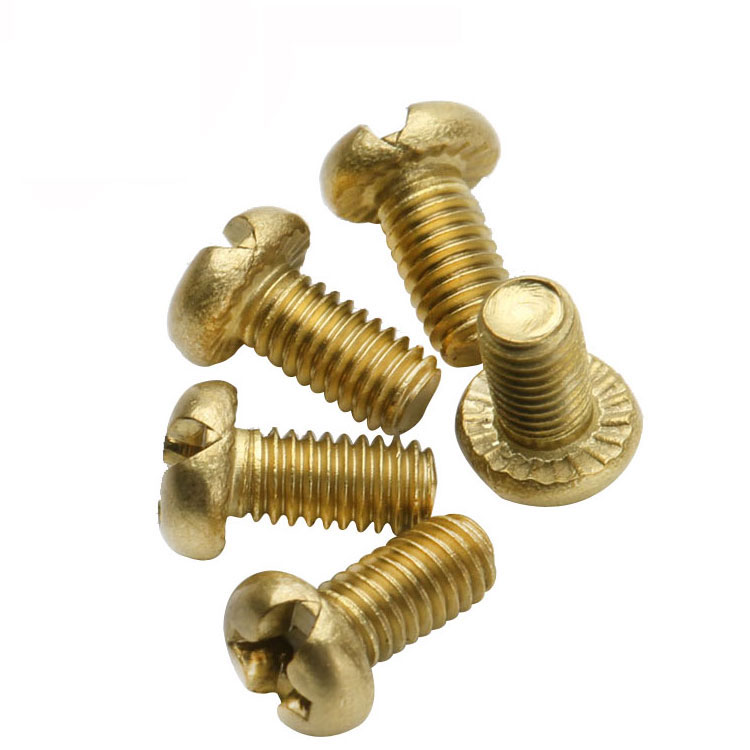
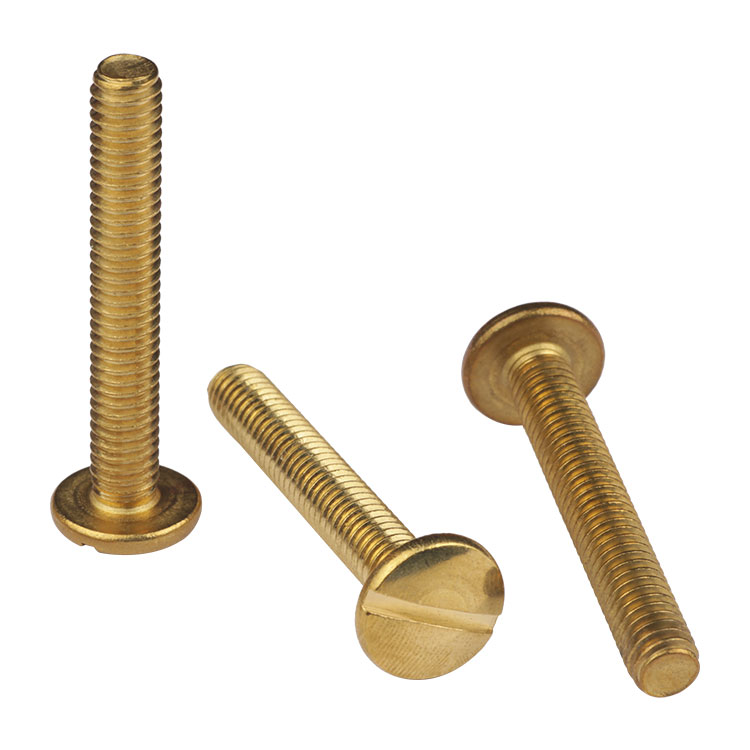
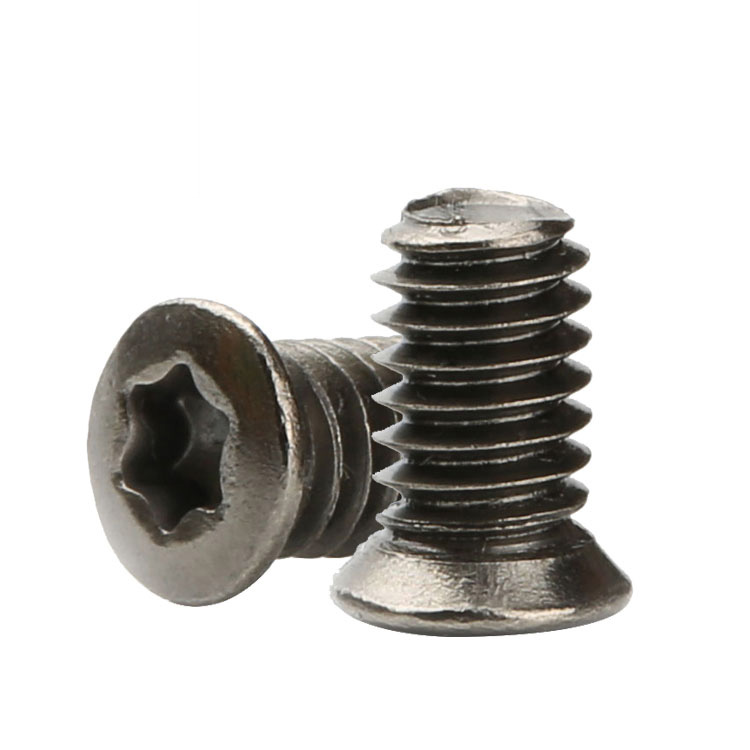
Type:Brass Countersunk Machine Screws
Materials:Brass
Surface treatment:Plain
Head Type:Flat (countersunk)
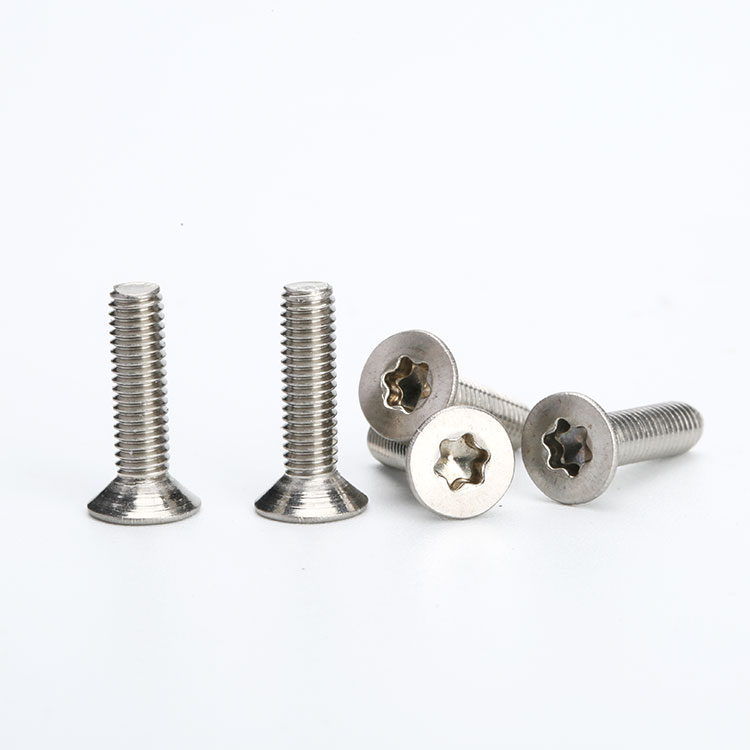
Drive:Torx (six lobe)
Thread:Machine thread
Point:Plain, chamfered
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
We make brass countersunk machine screws with a Torx drive and a plain finish, quoting them from M1 to M10 with lengths made to the drawing. The cone angle and the drive size are stated on the drawing, and the first article is seated in your own plate.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Brass countersunk machine screws are machine screws cut in brass with a conical head that seats flush in a countersink. The part recorded here has a Torx drive and a plain finish, quoted from M1 to M10 with lengths made to the drawing.
Countersunk head. A 90 degree cone that seats in the countersink, so the head finishes level with the surface.
Torx drive. A six-lobe recess driven with a star key, with contact on the flanks rather than at four thin arms.
Brass body. Free-cutting, non-magnetic and conductive, and soft enough that the drive is the first thing that wears.
Plain finish. The alloy is the surface, so the parts can be polished or aged after assembly without stripping a coating.
They are used on instruments, small electrical assemblies, decorative hardware and shopfitting details, where the head has to disappear into the surface and the material has to look like brass.
A cross recess drives on four tapered arms. When a bit is slightly worn it climbs out of those arms, and the load moves to the thinnest part of the recess. In steel that shows as a marked screw; in brass, which is much softer, the arms take a permanent set on the first slip and the recess is effectively finished.
A Torx recess works differently. The six lobes present a much larger contact area, and the drive force is taken on the flanks of the lobes rather than on the tips. The bit centres itself and stays seated, so the torque goes into turning the screw instead of into pushing the bit out. On a soft metal that difference is the whole reason the drive exists.
The trade is that the tool has to be right. A cross recess tolerates an approximate bit, because four arms will still find something to push against; a star recess with the wrong size simply does not enter. That makes the drive size a line on the drawing rather than a workshop preference, and it makes bit availability part of the customer’s assembly planning.
The countersunk geometry adds its own constraint. The cone consumes most of the head height, so the recess is cut into a thin remaining disc, and on a flush head there is no material to spare. That is why the head height and the recess depth are measured together: a part that is slightly low in head height has quietly lost part of its recess.
Plain brass keeps that geometry intact. There is no plating to build inside the lobes, so the bit that fits the first screw fits every screw in the batch, and a replacement part years later still takes the same key.
The recorded range is M1 to M10, with lengths made to the drawing. Custom lengths up to 2,000 mm are subject to the drawing submission and DFM review. The quotation for brass countersunk machine screws carries the head diameter, the countersink angle, the head height, the Torx size and depth, the thread pitch and the overall length.
| Item | How it is defined | What we control |
|---|---|---|
| Cone | Countersink angle, usually 90 degrees | Angle and concentricity |
| Head diameter | Widest point of the cone | Diameter and edge form |
| Head height | Top face to the cone top | Height and face flatness |
| Drive | Torx, size per diameter | Lobe depth and floor |
| Thread | Machine thread in brass | Pitch, length and start position |
| Length | Overall, head included | Length tolerance and thread start |
The countersink angle is the first number to state. Ninety degrees is the metric practice; 82 degrees appears on older drawings, and a 90 degree head in an 82 degree seat bears on the rim and stands proud however hard it is driven.
Drive size follows the diameter but is worth writing down. Torx sizes step in small increments, and a drawing that says only “star drive” can be met by two sizes that both look right and need different keys.
Length is measured over the head so the datum agrees with the seat. In a joint where the head sits in a machined countersink, the usable thread length is the overall length minus the cone depth, and that is what decides engagement.
Four properties decide brass countersunk machine screws, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Flush head | Nothing stands above the surface | Head height is spent on the cone |
| Torx drive | Large contact area, no cam-out | A dedicated key is required |
| Brass body | Non-magnetic, conductive, decorative | Soft; thread strips before steel |
| Plain finish | Can be polished or aged later | Tone varies between batches |
The value of brass countersunk machine screws with a star drive is a flush fixing that can be driven hard without damaging the drive. On brass that combination is only available with a drive that spreads the load, and that is what the star recess does.
The cost is that the joint is still limited by the brass. The drive will now take the torque the thread can carry, which means the thread becomes the point of failure, and a brass thread strips earlier than a steel one of the same size.
The recorded finish is plain. On a countersunk screw that matters more than on a raised head, because the cone is a bearing surface and a coating on it changes both the fit and the friction of seating.
| Option | What it does | Effect on cone and drive | Typical use |
|---|---|---|---|
| Plain, as supplied | The alloy itself | No build; drive as cut | Electrical and instrument work |
| Polished | Mechanical smoothing | Cone brighter; lobes rounded slightly | Visible flush fixings |
| Aged or darkened | Chemical colouring | Colour even inside the drive | Restoration and period work |
| Nickel plated | Hard bright barrier | Build on cone and lobes; re-gauged | Where a bright steel look is wanted |
| Black plated | Dark coating over brass | Thin build; colour uniform | Dark housings and panels |
Where a plated version is used, the cone and the drive are gauged after plating. A film on the cone makes the head seat a fraction higher, and on a flush joint that shows as a high spot; a film inside the lobes changes which key seats.
Plain brass needs no such correction. The head that leaves the heading machine is the head the customer fits, and the only variable left is the colour of the batch.
Three settings where a flush head and a soft decorative metal meet:
| Where it sits | The screw clamps a terminal where the fixing is part of the current path and must not corrode into a resistive joint. |
| When it goes wrong | The thread strips at the first tightening and the terminal no longer pulls down. |
| Why it happens | The joint carries current, the fixing is small, and the assembly is inspected. |
| What we control | Drive size and torque agreed; first article cycled at the specified torque. |
| Where it sits | The screw closes a faceplate where the head must be flush and must not attract a magnet. |
| When it goes wrong | A steel screw is substituted and the plate reads differently, or the head stands proud. |
| Why it happens | The panel is visible, the joint is serviced, and the material is specified. |
| What we control | Head height and cone angle checked; first article fitted in the plate. |
| Where it sits | The screw closes a detail where brass is the intended finish and the head must disappear. |
| When it goes wrong | Plating is used instead and wears at the drive, showing a steel core. |
| Why it happens | The piece is seen at close range, and the fixings are numerous. |
| What we control | Tone matched to the sample; recess proved with the fitting’s key. |
Four reasons that matter on a flush head in a soft metal, each tied to something the drawing has to prove:
|
Drive size and cone angle named
The Torx size and the countersink angle are written on the drawing, because a star drive needs the exact key and a flush head needs the exact seat. Basis: Drive and angle stated. |
Headed, recessed, threaded, left plain
The cone and head are formed in one stroke, the star recess cut, the thread rolled, and the parts left plain so no coating changes the seat. Basis: One route, no coating build. |
|
Height and drive measured together
Head height and lobe depth are measured as a pair and the key driven to the floor, because a shallow star in a thin head is the failure that looks like a good part. Basis: Height and drive as one pair. |
Same key across orders
The recess tool and the head punch are recorded with the drawing revision, so a repeat order takes the same key and sits at the same height. Basis: Same key across orders. |
These screws are headed on single-die machines that form the cone and the head in one stroke, cut with the star recess, thread rolled on the brass and left plain. The first part of every run is measured on head diameter, cone angle, head height, drive size and depth, thread and length.


|

|
Cutting the star into the head of a brass countersunk machine screw is easier than cutting a cross, because the lobes are cut rather than sheared and brass cuts cleanly. What it demands is precision: the lobes have to be even, the floor has to be flat, and the punch has to be sharp, since a dull punch leaves rounded lobe tips and the key then seats on the wrong surface.
Forming the cone at the same time is the balance. The metal flows out into the cone and up into the thin disc that becomes the head top, and a punch set slightly deep leaves that disc too thin to hold the drive. Both measurements are taken on the first article because each one alone looks acceptable.
Because brass countersunk machine screws are left plain, the process ends at thread rolling and inspection. There is no plating bath that could change the head height or the lobe depth, which is one reason the batch-to-batch consistency of a plain brass part is easier to hold than a plated one.
What decides whether brass countersunk machine screws pass is the cone, the head height, the drive and the thread. The inspection agreement covers those, and the criteria come from the drawing.

Cone and drive on the projector |

Thread and start checked |

Hardness against the brass spec |

Humidity exposure on the plain surface |
Head diameter, cone angle and head height are measured as one set, then the drive size and depth are read against the head height. On a countersunk head those four define whether the screw seats flush and whether the key reaches the floor.
The drive is proved by turning it with the customer’s key at the agreed torque and inspecting the lobes under magnification. On brass the lobes do not shear cleanly; they deform, so the check looks at the shape of the flanks rather than at a single dimension.
A sample from every batch is seated in a countersunk plate of the agreed angle and checked for rocking and proudness, then driven and removed. That cycle is what catches a head height that does not match the seat.
Every batch is traceable to the brass rod it was made from. The alloy and heat number appear on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing including the drive size and head height, and the RoHS report for the alloy. The documents carry the drawing revision and the batch number, so a repeat order of brass countersunk machine screws sits at the same height.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a flush brass head the first article is seated in the customer plate and driven with the customer key. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers and the recess station can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
A star drive spreads the load over six lobes instead of four thin arms, and the bit does not climb out. In brass that is the difference between a drive that survives and one that marks.
The Torx size that follows the diameter, stated on the drawing. A star drive does not tolerate an approximate key the way a cross recess does.
Yes. With a star drive the drive is no longer the weak point, so the brass thread becomes the limit and the torque is set accordingly.
Only in a countersink of the same angle. A 90 degree head in an 82 degree seat bears on the rim and stands proud.
Yes, and that is the advantage of plain brass. No coating has to be removed first, and the drive geometry does not change.
Head diameter, countersink angle, head height, Torx size and depth, thread pitch and overall length.
How a brass countersunk screw project runs from drawing to repeat delivery:
|
1
Send the drawing and the key size
|
→ |
2
Cone angle and drive depth agreed
|
→ |
3
First article seated in your plate
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the head diameter, countersink angle, head height, Torx size and depth, thread pitch and overall length.
|
Head diameter
|
Cone angle
|
Head height
|
|
Torx size
|
Thread pitch
|
Length
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com