Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
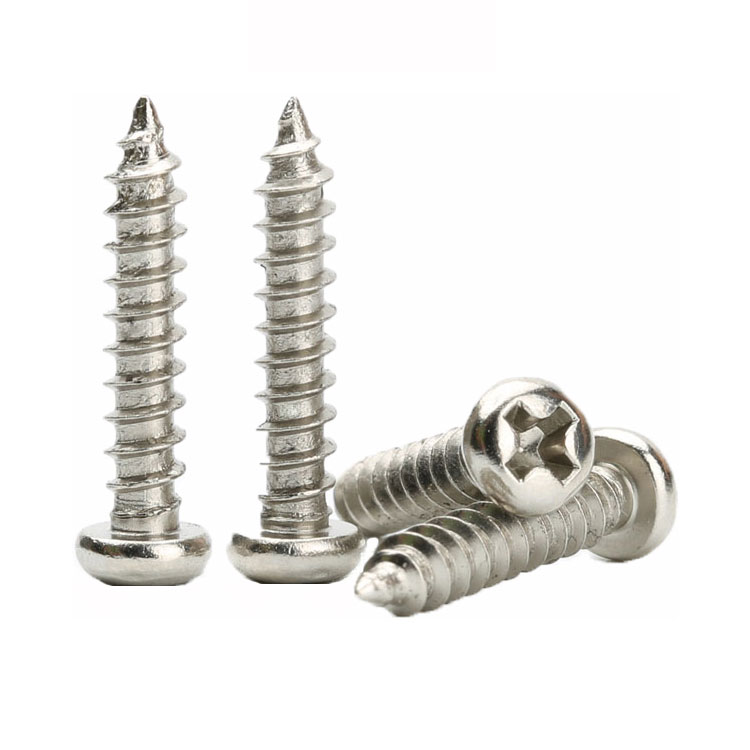
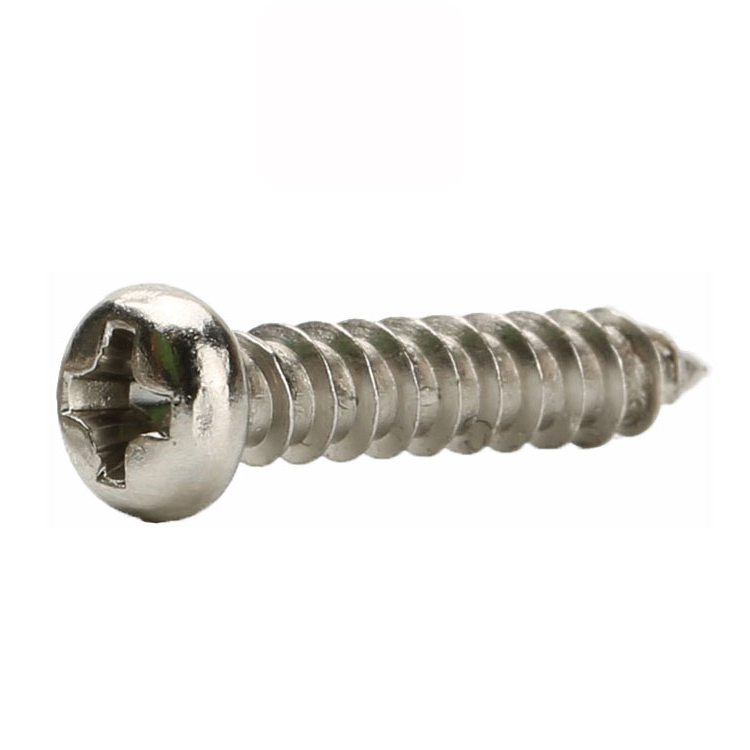
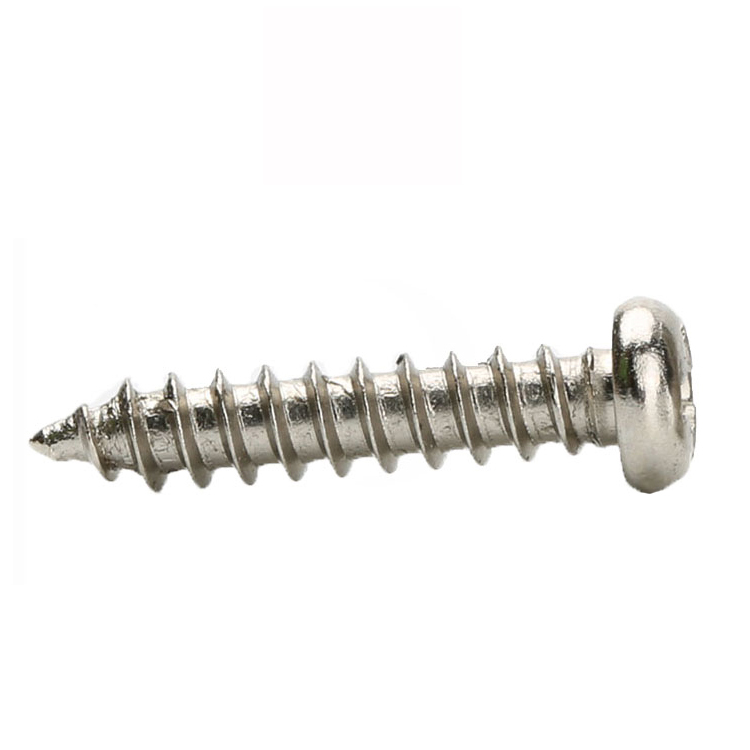
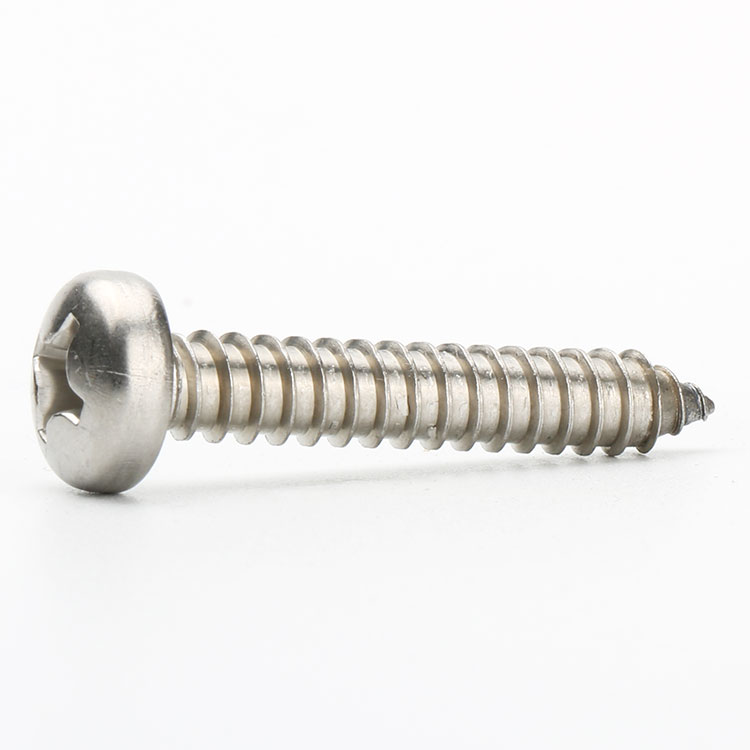
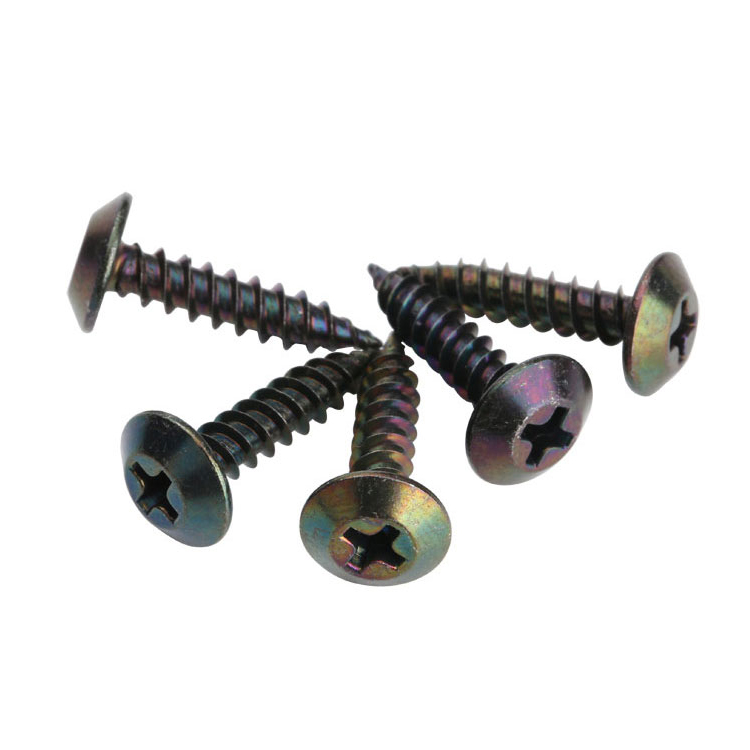
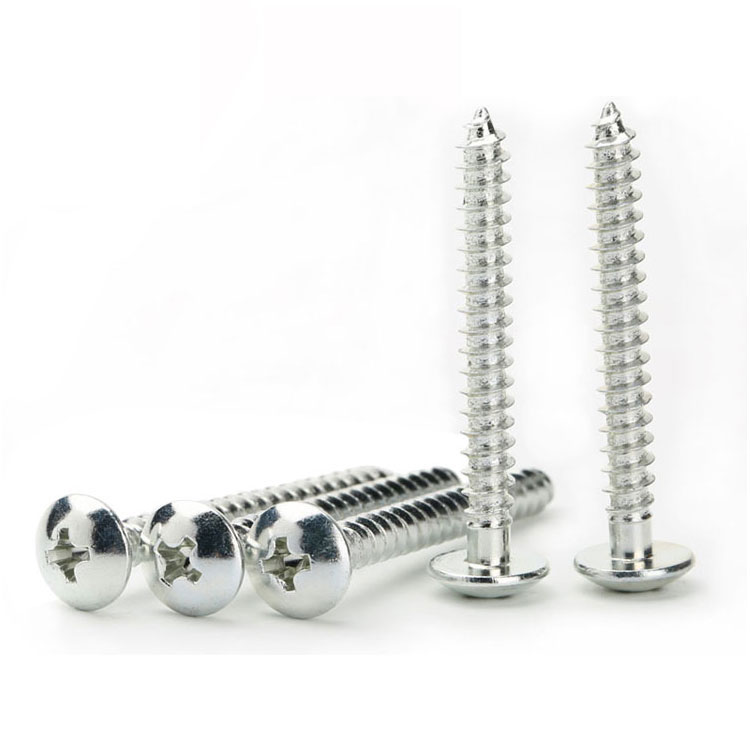
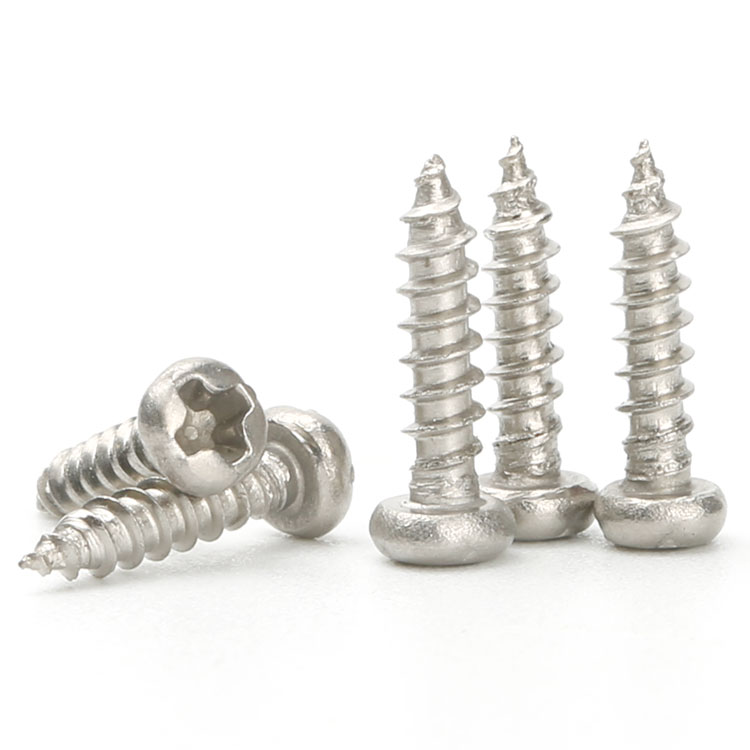
Type:Pan Head Self Tapping Screws, Phillips Pan Head Screw
Materials:304 Stainless Steel
Surface treatment:Plain
Head Type:Pan head
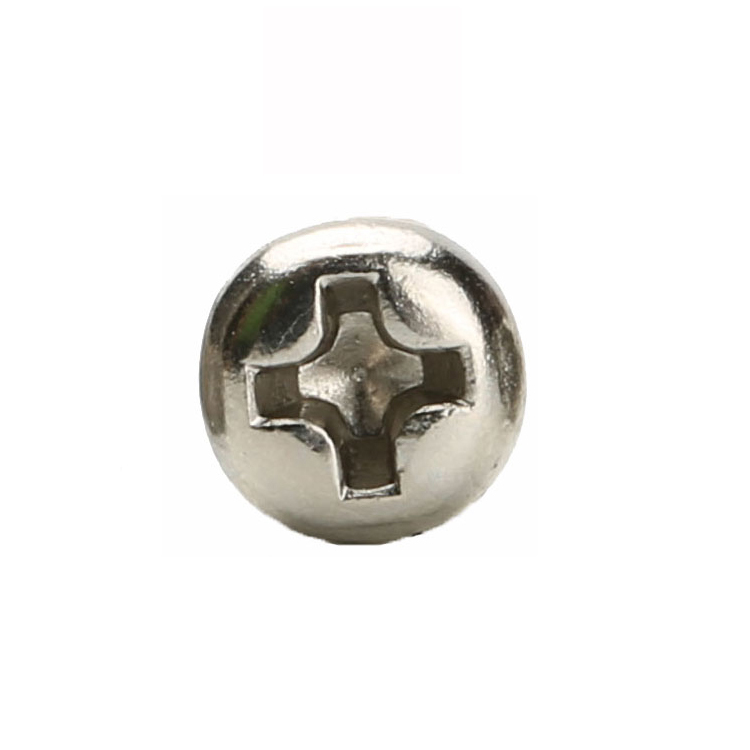
Drive:Phillips cross recess
Thread:Self-tapping (spaced thread)
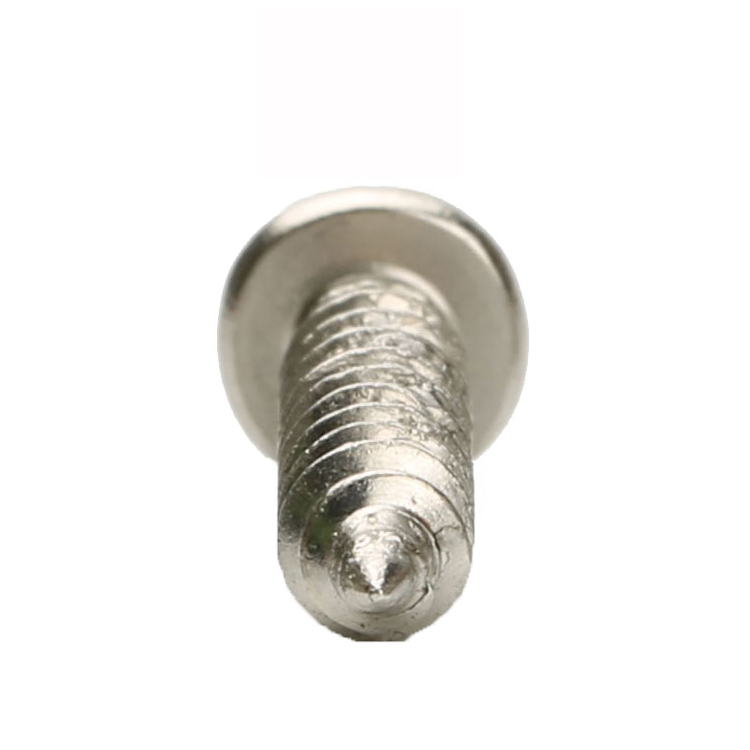
Point:Sharp, tapered
Forming:Single Die Heading
Size:M1 M2 M3 M4 M5 M6 M7 M8 M9 M10
We make automotive self tapping screws in 304 stainless steel, pan head with a cross recess, quoting them from M1 to M10 and in the equivalent imperial sizes. The size designation and its diameter are both written down, and the first article is driven into your own panel or boss.
Watch the factory video·Email sst@szsst88.com
ISO 9001:2015 · Manufacturing since 1998 · 8,678+ customers · 89 countries and regions
Made to order – there is no stock catalogue. Each part is produced to your drawing, and production starts after drawing review and first-article approval.
Automotive self tapping screws are screws with a spaced thread and a sharp point that form their own path in sheet, plastic or a cored boss, used in vehicle assembly and trim. The part recorded here is 304 stainless, plain finish, pan head with a cross recess, quoted from M1 to M10 and in the equivalent imperial sizes.
Self-tapping thread. A wide-pitched thread that cuts or forms a thread in the material as it is driven.
Sharp point. A tapered point that starts the hole and opens it as the thread engages.
Pan head. A rounded head with a wide bearing face that sits on the surface rather than into it.
304 stainless, plain. Corrosion resistance without a coating, which matters where trim is exposed to weather and road spray.
They are used on brackets, trim, interior panels, lamp housings, underbody shields and accessory fittings, where the joint is assembled at speed and may never be opened again, or may be opened many times over the life of the vehicle.
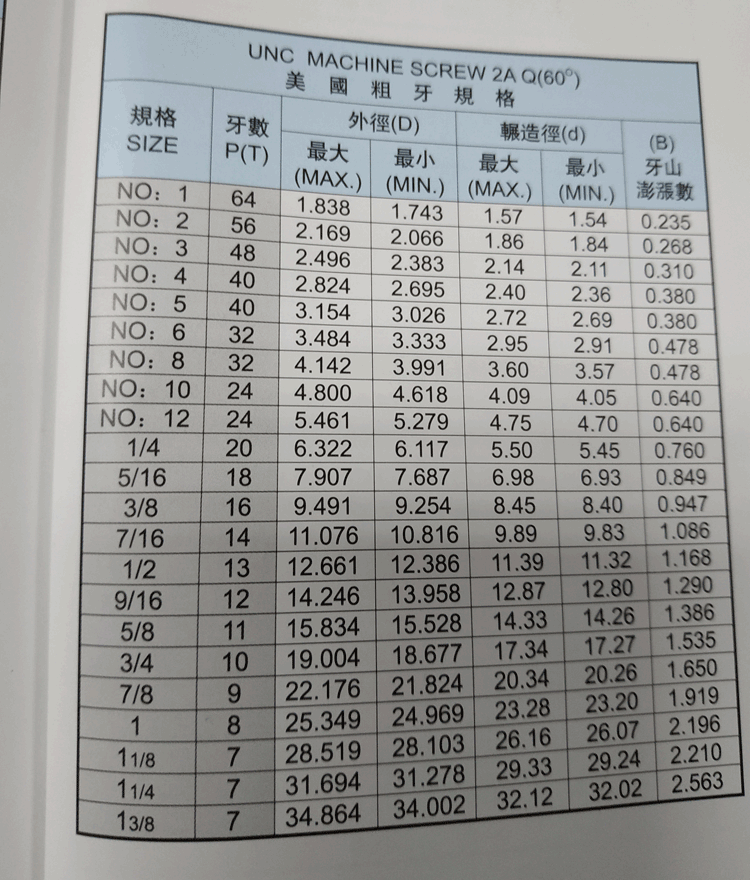
The first is the size system. A designation like NO 10 belongs to an imperial series; it is not a diameter and it does not convert by a formula. A #10 screw is a known diameter in that series, and a drawing that carries the number without the diameter leaves the supplier to interpret a convention that differs between markets. The number and the actual diameter belong on the drawing together.
The second is why these joints come loose. It is rarely the thread failing. In a vehicle the joint is loaded by vibration and by repeated thermal cycling, and the material it is driven into is usually plastic, a thin metal panel or a trim clip. Under those loads plastic creeps, a thin panel frets, and the clamp load that was correct when the screw was driven is gone a few thousand cycles later.
That is why the thread pitch and the engagement depth matter more than the head. A coarse pitch displaces more material per turn and holds better in plastic that can flow; a fine pitch cuts cleaner but reaches its limit sooner in a thin panel. Engagement depth in a moulded boss has to be long enough to spread the load and short enough to avoid splitting the boss, and that balance is set by the boss design as much as by the screw.
The bearing face then decides whether the clamp survives on automotive self tapping screws. A pan head spreads the load on the panel, so the panel deforms less and the joint keeps its preload longer. A small head concentrates the load, the panel yields locally, and the screw is loose without anything having failed.
304 stainless adds one more consideration that matters in a vehicle: it is a different metal from the aluminium, magnesium or coated steel it is often driven into. Where the joint is wet, that couple is the corrosion mechanism, and the answer is the material choice or an isolating feature rather than a heavier coating on a steel screw.
The recorded range is M1 to M10, with lengths made to the drawing, and the imperial designations in the same envelope. Custom lengths up to 2,000 mm are subject to the drawing submission and DFM review. The quotation for automotive self tapping screws carries the size designation and its actual diameter, the head diameter and height, the PH size, the thread pitch and point form, and the overall length.
| Item | How it is defined | What we control |
|---|---|---|
| Size | Metric thread or imperial number | Designation and actual diameter both stated |
| Head | Pan head, on the surface | Diameter, height and bearing face |
| Recess | Phillips, PH size per diameter | Arm depth and floor thickness |
| Thread | Self-tapping, spaced | Pitch, spacing and engagement length |
| Point | Sharp tapered or blunt | Point angle and length |
| Length | Overall, head included | Length tolerance and thread start |
Writing both the number and the diameter removes the most common error in these orders. A #10 part and an M5 part are neighbours in size but not interchangeable in a hole, and a drawing that names only one of them can be satisfied by a part that will not go in.
Point form follows the material. A sharp point suits sheet and a through hole; a blunt point suits a moulded boss where the screw must form its thread without piercing the material behind. In vehicle work both appear on the same drawing set, which is why the point is specified per joint rather than per size.
Length is measured over the head. On a trim joint the usable length is the overall length minus the panel thickness it passes through, and that remaining engagement is what holds the part.
Four properties decide automotive self tapping screws, and each one carries a cost:
| Property | What it gives | What it costs |
|---|---|---|
| Self-tapping thread | One-step assembly, no tapping | Engagement limited by the material |
| Sharp point | Starts in a pilot hole | Can pierce the part behind the panel |
| Pan head | Wide bearing face on the panel | Stands above the surface |
| 304 stainless | Corrosion without a coating | Different metal from the panel it meets |
The value is speed and repeatability. A line that drives thousands of screws shifts needs a fixing that starts, cuts and seats in one motion, and a self-tapping screw does that without a tapping operation or a nut behind the panel.
The cost is that the joint’s endurance depends on the material it is driven into. The screw can be perfect and the joint can still loosen because the plastic boss crept, and that is a design conversation rather than a purchasing one.
The recorded finish is plain over 304 stainless. The alloy carries the corrosion resistance, passivation restores the oxide layer after forming, and there is no coating to chip at the head or to be worn off by a clip.
| Option | How it protects | Effect on head and recess | Typical use |
|---|---|---|---|
| Passivated, plain | Removes free iron; rebuilds oxide | No build; recess as cut | Exterior and trim joints |
| Black oxide on stainless | Colours the surface | Thin film; fit unchanged | Dark interior parts |
| Zinc plated steel equivalent | Sacrificial zinc | Build in recess; re-checked | Hidden interior joints |
| Zinc flake coated steel | Lamellar coating | No acid bath; edges covered | High-volume body fixings |
| Electropolished | Levels the surface | Recess edges rounded slightly | Visible bright trim |
Where the joint is visible, the plain finish on automotive self tapping screws keeps its appearance without a coating to fail, which is why it is common on exterior trim and on parts exposed to road spray. Where the joint is hidden and cost matters, a coated steel screw does the same structural job.
The material pair is the part of the finish decision that is often missed. Stainless in an aluminium panel with water present is a corrosion couple; adding a coating to the screw changes the appearance but not the couple, so the answer is an isolating washer, a sealant or a different fastener material.
Three vehicle settings where a self-tapping joint is the norm:
| Where it sits | The screw holds a moulding or a lamp surround where the fixing is visible and exposed to weather. |
| When it goes wrong | A plated screw corrodes at the head and stains the trim, or a loose joint rattles. |
| Why it happens | The joint is exposed, the panel is thin, and the fixing is assembled on a line. |
| What we control | Grade and passivation confirmed; first article fitted in the trim. |
| Where it sits | The screw forms its own thread in a moulded boss behind a panel that has to stay tight. |
| When it goes wrong | The boss splits at the thread start, or the joint loosens as the plastic creeps. |
| Why it happens | The material is plastic, the boss is moulded, and the joint is rarely opened. |
| What we control | Pitch and point proved on a sample boss; first article driven and removed. |
| Where it sits | The screw fixes a shield where the joint is wet, dirty and exposed to vibration. |
| When it goes wrong | The fixing seizes in the clip and cannot be removed for service. |
| Why it happens | The joint is wet, the material is dissimilar, and the part is serviced. |
| What we control | Alloy confirmed; isolating feature agreed; first article assembled and opened. |
Four reasons that matter on a joint that is judged by whether it stays tight, each tied to something the drawing has to prove:
|
Designation and diameter both stated
The size designation and its actual diameter are written into the drawing together, because an imperial number does not convert to a metric diameter by inspection. Basis: Number and diameter both stated. |
Headed, recessed, threaded, passivated
The pan head and cross are formed in one stroke, the self-tapping thread rolled, and the batch passivated so the head and the cut point keep their surface. Basis: One route from wire to part. |
|
Point and pitch proved in your material
The point and the thread spacing are proved by driving into the customer material, because a screw that stalls or splits a boss is a thread design issue, not a torque setting. Basis: Driven into your material first. |
Same engagement across orders
The rolling dies and the point tool are recorded with the drawing revision, so a repeat order engages the same way and does not start splitting bosses. Basis: Same engagement across orders. |
These screws are headed on single-die machines that form the pan head in one stroke, cut with the cross recess, thread rolled with the self-tapping profile and the point formed, then passivated as a batch. The first part of every run is measured on head diameter and height, recess depth, thread and point, and length, and is driven into the customer material before the batch is released.


|

|
Rolling a self-tapping thread on stainless is the operation that decides how the joint behaves. The thread has to cut cleanly rather than smear, because a smeared crest tears a plastic boss instead of forming it, and the damage appears as a split rather than as a loose screw. The rolls are kept clean and the blank diameter is set to displace the metal rather than squeeze it.
The point is formed in the same operation, and its length is what lets the screw start before the thread engages. A point that is too short makes the screw wander on a panel; one that is too long reduces the thread length available for engagement, and on a thin panel that is the difference between holding and stripping.
Passivation follows forming. On automotive self tapping screws the point and the recess are the features that hold contamination, and both are checked after passivation, because a stainless screw that rusts at its point looks like a material failure to the customer.
What decides whether automotive self tapping screws pass is the thread, the point, the head and the surface. The inspection agreement covers those, and the criteria come from the drawing.

Head and recess on the projector |

Thread and point checked |

Hardness against the 304 spec |

Salt-spray testing of the passivated surface |
Thread pitch, spacing and the point angle are measured on the projector and compared with the agreed profile, together with the head diameter and the recess depth. The actual diameter is confirmed against the designation on the drawing, since that is the number that decides whether the part fits the hole.
The functional check is a drive cycle in the customer material. A sample from every batch is driven into a coupon of the panel or boss at the line torque and removed, and the material is inspected for tearing, splitting or a thread that has not formed.
Corrosion is checked where it would show first: the point and the recess go into the salt-spray chamber, and rust at either place rejects the batch.
Every batch is traceable to the heat of stainless it was made from. The grade and heat number appear on the material certificate supplied with the parts, and the inspection records follow the criteria agreed on the drawing.

ISO 9001:2015 |

RoHS test report |

Registered trademark |

Patent: security screw and driver |
With each shipment we supply the material certificate, the inspection record for the dimensions on the drawing including the point form, and the passivation records for the batch. The documents carry the drawing revision and the batch number, so a repeat order of automotive self tapping screws engages the same way.
More than 8,678 customers in 89 countries and regions have ordered from Shi Shi Tong; 87% of orders come from repeat customers and 56% through referrals. Most projects follow the same route: drawing review, first-article approval, then batches checked against that sample. On a self-tapping joint the first article is driven into the customer material, because whether a boss splits or a panel strips only shows there. Buyers visit during the process to review samples.
|
8,678+
customers served
|
87%
of orders from repeat customers
|
56%
of orders through referrals
|
89
countries and regions shipped to
|
Buyers and quality engineers visit for sample review, process discussion and supplier audits; the visit is arranged around production so the headers, the thread rolling station and the passivation line can be seen on the day the parts run.

Customer group visit – sample review |

Customer group visit – process discussion |

Customer group visit – factory tour |

Customer visit – project kick-off |

Danish customer – drawing review |

Industry exhibition – meeting customers |
It is a designation from an imperial size series, not a diameter. The actual diameter belongs on the drawing next to the number.
Usually because the panel or boss crept under vibration and heat, not because the thread failed. Head area and engagement depth decide how long the clamp lasts.
For exposed trim and wet areas it is, because there is no coating to fail. Where it meets aluminium, the pair needs isolating.
Sharp for sheet and through holes, blunt for a moulded boss that must not be pierced. The point is a joint decision, not a size decision.
In plastic a self-tapping screw loses grip a little with each removal, so the design assumes a limited number of cycles.
The size designation and diameter, head diameter and height, PH size, thread pitch, point form, engagement length and overall length.
How an automotive self tapping project runs from drawing to repeat delivery:
|
1
Send the drawing and the joint section
|
→ |
2
Designation, pitch and point agreed
|
→ |
3
First article driven in your material
|
→ |
4
Batch production and repeat orders
|
Each step is confirmed with you before the next one starts; the drawing revision from the first article is what repeat orders are checked against.
For a quotation, send the drawing with the size designation and diameter, head dimensions, PH size, thread pitch, point form and overall length.
|
Size and diameter
|
Head diameter
|
PH size
|
|
Thread pitch
|
Point form
|
Length
|
Sending a drawing? The form below does not take attachments. Email the PDF, DXF or STEP file to sst@szsst88.com with the part name and quantity in the subject line – the drawing is reviewed and a quotation follows.

 +86 13143444311
 sst@szsst88.com