Tel:
+86 13143444311
Email:sst@szsst88.com
Fax:+0086-755-27322278
Address:Building 9, First Industrial Zone, Tantou Industrial City, Songgang Street, Baoan District, Shenzhen 518105, Guangdong, China
SHISHITONG · MANUFACTURING SINCE 1998
Complex Geometry · Extra-Long · High Precision · Selected Special Materials
Shenzhen Shi Shi Tong Metal Products Co., Ltd. specializes in custom screw engineering and manufacturing for difficult applications. We focus on projects where conventional standard fastener solutions are not enough—complex geometries, long and extra-long screws, tight tolerances and selected specialty materials.
Our overall custom screw capabilities cover M0.8–M16 in diameter and 0.4–2000 mm in length. Each product family and material has its own scope; feasible combinations depend on material, diameter, geometry and manufacturing process.

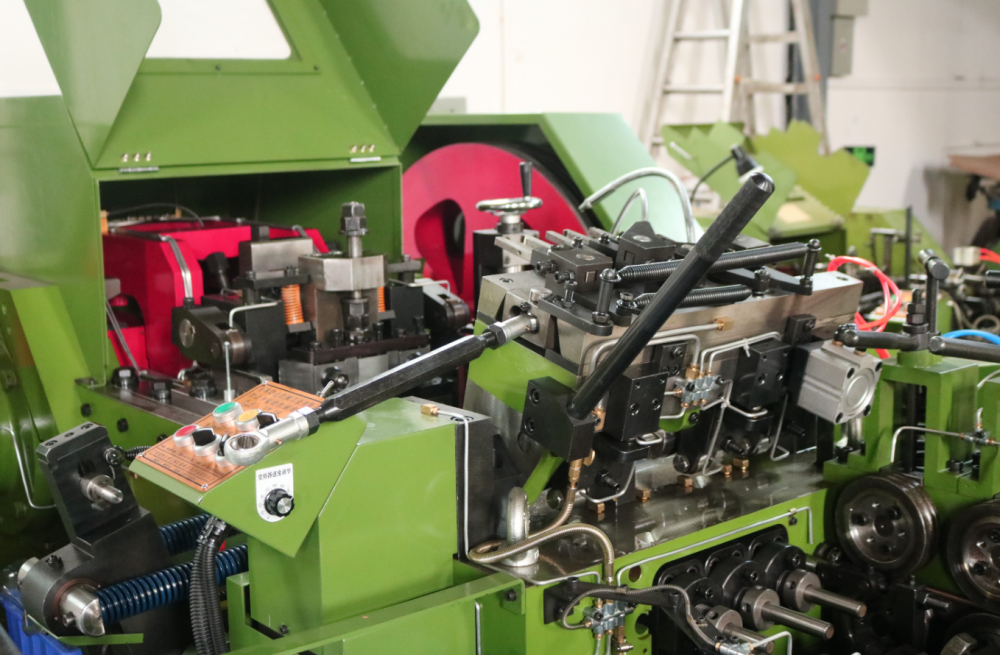
Shi Shi Tong manufacturing facility in Shenzhen
FOUR CORE CAPABILITIES
Complex Geometry
Special heads and drives, thin heads, shoulders, stepped shanks, hollow features and compound geometries. Tooling and manufacturability are reviewed together.
Extra-Long
Long and extra-long screws with control of deformation, straightening, thread quality and the condition after heat treatment.
High Precision
Precision screws, shoulder dimensions, tight-tolerance shanks and threads. Critical dimensions, datums and measurement methods are defined for the part.
Selected Special Materials
Titanium, A286 (GH2132), 321 and other selected grades. Material condition, component geometry and the appropriate manufacturing route are assessed together.
Material, geometry, dimensions, tolerances and process are evaluated as one manufacturing problem. A maximum size in one product family is not a guarantee for every material or structure.
WHO WE ARE
Our screw manufacturing business began in 1998 as Shi Tong Precision. The current legal entity, Shenzhen Shi Shi Tong Metal Products Co., Ltd., was registered in 2009. Today, we focus on the engineering development and manufacture of challenging custom screws.
We primarily support industrial OEMs and manufacturers where material performance, dimensional accuracy, manufacturability, process repeatability and lot-to-lot consistency are critical. Our focus is custom development—not standard catalogue stock.
Making a custom screw is not simply a matter of following a drawing.
Can the part be manufactured consistently? Is the material suitable for the proposed process? Can the required geometry and tolerances be achieved? Can the process be repeated after prototype approval, with consistent quality from lot to lot?
WHAT WE MANUFACTURE
Our core products are custom titanium screws, long and extra-long screws, and custom screws for difficult applications. The work includes complex-geometry fasteners, tight-tolerance precision screws, special-alloy screws and related precision components, with the manufacturing route matched to the material and part.

Representative custom non-standard screw product range
TA1 / Grade 1 · TA2 / Grade 2 · TC4 / Grade 5
Manufacturing diameter range: M1.6–M12. Vented, hollow or axially bored screws, low-profile heads, shoulders and precision geometries for vacuum, precision industrial, corrosion-resistant and underwater equipment. Dimensions and cold-heading, warm-heading or turning routes are reviewed for the specified grade and structure.
M1.4–M12 · Up to 2000 mm
Partially threaded screws, equipment through-connections and special shank, head or end geometries. Lengths of 200–600 mm are common project requirements. Maximum length is assessed against material, diameter, structure and process. One-piece cold-formed long shanks are not replaced by welded extensions.
Complex geometry · Precision fits · Difficult-to-form designs
Special heads and drives, thin heads, shoulders, stepped shanks, hollow features and special threads. A286 (GH2132) and 321 are priority material options, with cold-heading and turning experience. Structure, dimensions, material condition and inspection requirements are reviewed for each component.
MP35N and beryllium copper: primarily turned or precision-machined components. Inconel 718 and aluminum alloys: turning only. Inconel 625 and 17-4PH: manufacturing routes and product scope are confirmed for the specified grade, material condition and component. Stainless steel, carbon steel and copper options are selected against the drawing and order requirements. Material experience does not mean every size, strength or surface requirement can be combined.
MANUFACTURING CAPABILITY
Depending on material properties, geometry and tolerance requirements, manufacturing can involve cold heading, warm heading, multi-station forming, precision machining, thread rolling and inspection. Split-die heading supports suitable one-piece long-screw designs; the tooling and process are confirmed for the component.
Turning and CNC secondary machining are identified separately: secondary machining applies to parts machined after an earlier forming operation. Inconel 718 and aluminum alloys are handled as turned components. Warm heading, grinding, straightening and surface treatment are selected within the applicable project scope.
PROJECT-SPECIFIC PROCESSES
ENGINEERING TO PRODUCTION
Manufacturing Repeatability
The approved drawing, material condition, process route and inspection requirements stay linked as the project moves through tooling, prototype validation and production. The objective is a manufacturable, verifiable and repeatable component.
APPROXIMATELY
±0.1 mm
Cold-headed head dimensions
APPROXIMATELY
±0.05 mm
Head dimensions finished by secondary machining
LENGTH TOLERANCE
+0 / −2 mm
For selected screws longer than 400 mm
These are reference values, not universal tolerances. Final requirements are agreed against the drawing, material, geometry, manufacturing state, datum and measurement method.
EQUIPMENT APPLICATIONS
Applications are assessed around the fastener structure, mating parts, material, operating conditions and acceptance requirements. The examples below describe equipment scope, not a claim that every product is qualified for every application.
Custom screws for relevant equipment and vacuum components, including vented or axially bored titanium designs. Geometry, dimensions and delivery requirements are reviewed for the part.
Long connecting screws for identified equipment components and mobile-power assemblies. The actual connection structure, material, length and acceptance conditions are confirmed.
Precision custom screws assessed against the actual equipment structure, mating features, dimensional requirements and inspection method.
Custom fasteners evaluated against the actual product, assembly and positioning requirements, with critical fit dimensions and inspection criteria defined.
Material, operating conditions, surface requirements and inspection scope are reviewed for the equipment component. Any food-contact or hygienic documentation is confirmed for the specific application.
Custom fasteners for non-implantable equipment, with material, component geometry, precision fits and inspection requirements confirmed for the project.
HOW WE WORK
Our engineers consider fit, loading, repeated assembly and production consistency. When a design presents manufacturing or reliability risks, we discuss them openly and work with the customer on practical improvements before volume production.
Our role is to help turn a challenging design into a manufacturable, verifiable, repeatable and production-ready component. We support customers throughout the development process:
Drawing Review
Confirm the drawing version, dimensions, material, function and customer requirements.
Manufacturability Assessment
Assess material condition, geometry, tolerances and production feasibility.
Process Development
Select the forming or machining route, thread operations and inspection approach.
Tooling
Develop and verify the tooling required by the structure and manufacturing route.
Prototype Validation
Check samples against the agreed drawing and validation requirements.
Stable Production
Link approved drawings, materials, process conditions and inspection records for consistent repeat batches.
QUALITY & TRACEABILITY
Shi Shi Tong is ISO 9001 certified. Drawing versions, material records, physical parts and inspection results are kept aligned. In-process and final checks are defined against the dimensions, threads, appearance and performance requirements relevant to the component.
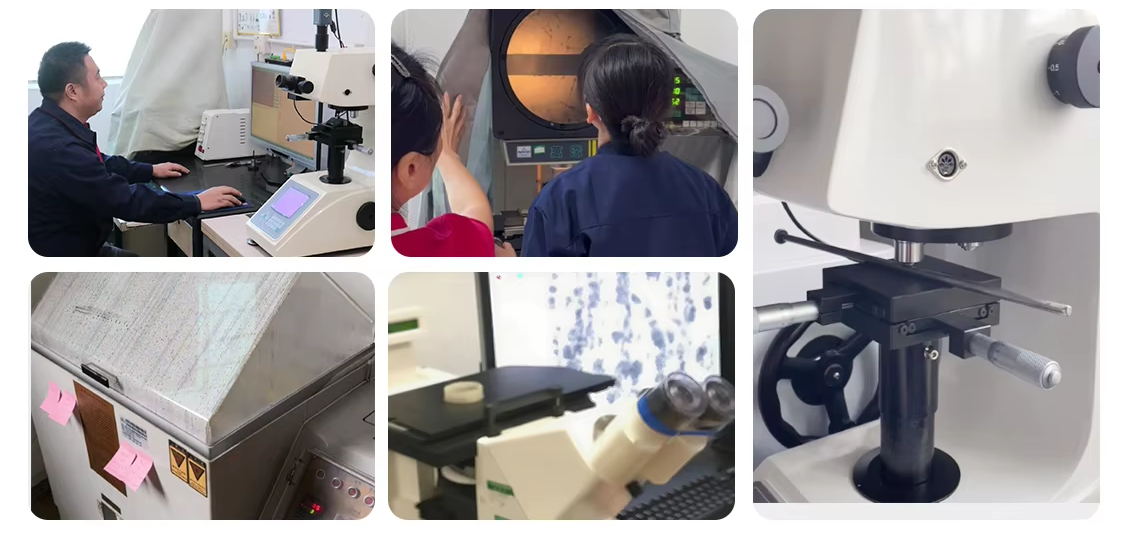
Project-specific inspection can cover dimensions, thread go/no-go, pitch, depth, radii, angles, concentricity, optical projection, metallography, Rockwell and Vickers hardness, torque and material verification. In-house salt-spray testing is available, with the method, duration and acceptance criteria confirmed for the project.
Material and quality documents correspond to the product and batch. Internal salt-spray records are distinguished from third-party reports; XRF analysis and other external tests are identified by their actual source. RoHS and REACH documents are used only within their applicable scope. Specific third-party reports are agreed separately.
FROM PROTOTYPE TO REPEAT ORDERS
Repeat orders depend on more than an approved sample. Drawings, material condition, manufacturing requirements and inspection records must remain aligned. We focus on manufacturing repeatability and lot-to-lot consistency throughout ongoing production.
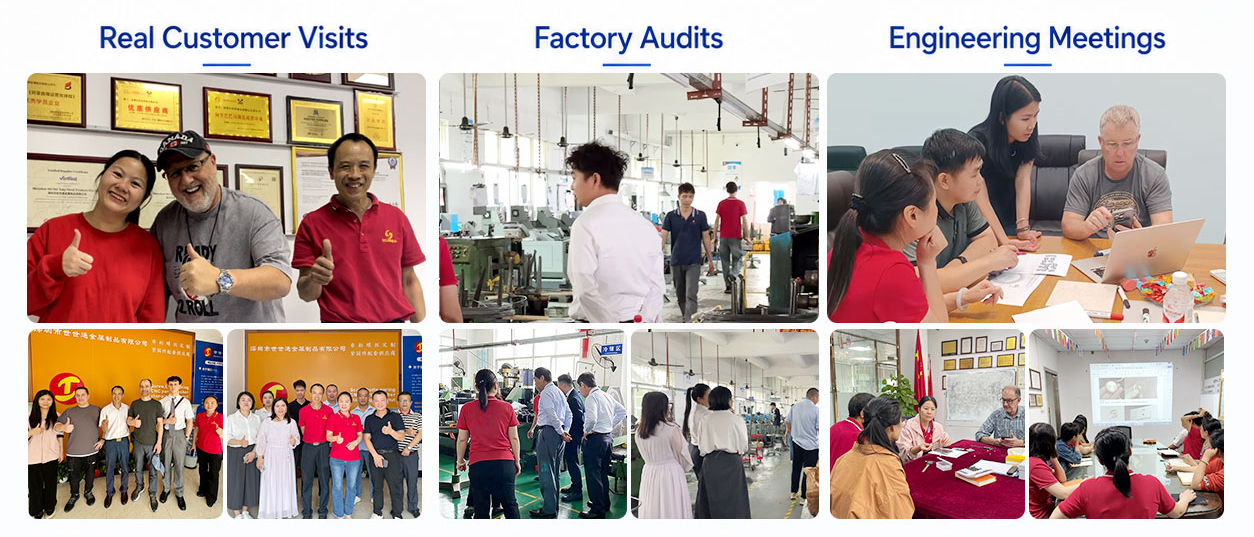
Customer projects and global cooperation
ISO 9001
Quality management system
Material Records
Grade and material condition
Inspection Records
Dimensions and agreed tests
Lot Traceability
Part, drawing and batch
Have a Challenging Custom Screw Project?
Send us your drawing, material specification or technical requirements for an engineering review. Include the application, quantities, key tolerances, surface requirements and requested delivery schedule so the project can be assessed together.
2017.10.23
Joan

 +86 13143444311
 sst@szsst88.com